


DESIGN OF TYPICAL FERMENTOR (AERATED STIRRED TANK BATCH
FERMENTOR)
1) Fermentor Vessel:
A suitable vessel is used to carry out the whole fermentation process. The vessel is
capable of being operated aseptically and meets the control requirements. The vessel is
designed in such a way that it requires minimal labour operation and maintenance. It
has smooth internal surfaces and a similar geometry. Depending upon the fermentation
process two types of vessels are used. For small scale fermentation, glass vessels are
used and for industrial scale stainless steel vessels are used.
Glass vessel:
Glass vessels are smooth which makes it nontoxic, corrosion proof. It also makes it
easy to examine the interior of the vessel. The large vessels are usually borosilicate
battery jars with a round or flat bottom and a top flanged carrying plate. These vessels
require autoclaved sterilization. The diameter of glass fermentor is nearly 60cm
Stainless steel vessel:
Stainless steel is the most satisfactory material for large scale fermentations. These
vessels can be sterilized in situ and hence have the capability to withstand pressure and
corrosion. The corrosion resistance of stainless steel is dependent upon the thin
hydrous film on the surface of the metal. This film is stabilized by chromium and is
continuous, non-porous, insoluble and self-heating. Corrosion resistance can be
improved by tungsten, silicone and other elements.

Capacity:
The capacity of the fermentor may range from a few hundred to several thousand
gallons. The capacity of the fermentor is usually stated on the basis of the total volume
capacity of the same. Thus, based on total volume capacity the fermentors are of
following types:
i) Small Laboratory fermentors (range from 1-2 liters with a maximum up to of 12 –15
liters.)
ii) Pilot plant fermentors (range from 25 –100 gallons up to 2000 gallons) (100 to 400
liter)
iii) Large industrial fermentors (range form 5,000-10,000 gallons up
a. to 1, 00,000 gallons.) (20000 to 40000 liter)
iv) Horton spheres fermentors (range from 2, 50,000 to

Actually the working volume in a fermentor is always less than that of the total volume.
In other words, a ‘head space’ is left at the top of the fermentor above the level of
fermentation media. The reason for keeping a head space is to allow aeration,
splashing and foaming of the aqueous medium. This head space usually occupies a fifth
to a quarter or more of the volume of the fermentor.
2) Heating and cooling apparatus (Temperature control):
Temperature control is achieved by a water jacket around the vessel. This is often
supplemented by the use of internal coils, in order to provide sufficient heat-transfer
surface. Heat is provided by passing hot water through these coils. During fermentation
process, heat is generated due to microbial activity and mechanical agitation which is
removed by passing cold water through these coils. Thus optimum temperature is
maintained by observing readings on thermometer fitted to fermentor.
3) pH Control:
pH control is achieved by acid or alkali addition, which is controlled by an auto- titrator.
The auto-titrator in turn is connected to a pH probe.
4) Impellers (Agitation):
Impeller is used for agitation. Agitation is required to ensure that a uniform suspension
of microbial cells is achieved in an homogeneous nutrient medium. The agitating device
consists of a strong and straight shaft to which impellors are fitted. An impeller, in turn
consists of a circular disc to which blades are fitted with bolts. Different types of blades
are available and are used according to the requirements. The shaft passes through a
bearing in the lid of the fermentation tank. It is rotated with the help of an electric motor

mounted externally at the top of the tank. The liquid medium is thrown up towards the
walls of the fermentor while rotating the impeller blades at a high speed.
Impellers are classified as:
Disc turbine: It consists of a disc with a series of rectangular vanes. The vane disc
again has a series of rectangular vanes attached vertically on the underside.
Air from the sparger hits underside of the disc and is displaced towards the vanes
where the air bubbles are broken up into smaller bubbles.
Variable pitch open turbine: It also contains vane disc, the vanes of which are attached
to the blades of a marine propeller on the agitator shaft. The air bubbles in this turbine
do not hit any surface before dispersion by vanes or blades.
5) Baffles (to prevent vortex and to improve aeration capacity):
The liquid medium is thrown up towards the walls of the fermentor while rotating the
impeller blades at a high speed. This results in the formation of a vortex, which is
eliminated, usually by four equally spaced baffles attached to the walls of the fermentor.
Baffles are metal strips nearly one tenth of the vessel diameter and attached radially to
the wall. They are incorporated into agitated vessels of all sizes to prevent vortex and to
improve aeration capacity. Baffles maintain a gap between them and the vessel wall to
enable scouring action thus minimizing microbial growth on the walls of the fermentor.
6) Sparger (Aeration):
Sparger is used for aeration. The purpose of aeration is to provide sufficient oxygen to
the aerobic microorganisms for metabolic requirements. Sparger introduces air into
liquid in the fermentor.

Usually, the aerating device consists of a pipe with minute holes, through which
pressurized air escapes into the aqueous medium in the form of tiny air bubbles. The
size of the holes in a sparger ranges from 1/64 to 1/32 of an inch or larger, holes
smaller than this requires too high air pressure for economical bubble formation. One
should always remember that the smaller the air bubbles, the greater is the bubble
surface area. It is desirable to adjust the size of the air bubbles to give the greatest
possible aeration without greatly increasing the overall cost of the fermentation process.
The reason for this is that sterile air is a costly item for large-scale fermentation.

The cheapest means of sterilization of air is to pass it through a sterile filter composed
of glass wool, carbon particles or some other finely divided material that will trap
microorganisms present in the air. Spargers in fermentors for growth of mycelium
forming organisms often utilize 1/4 inch holes to prevent plugging of the holes by hyphal
growth. Pipes crimped at the end or with a single small hole to produce a stream of air
bubbles also are employed in some instances.
The air bubbles from the sparger are picked up and dispersed through the medium by
the action of the impeller blade mounted above the sparger. In some very large

fermentation tanks, an impeller is not utilized. The medium is stirred by the directed rush
of air bubbles from a sparger at the bottom of the tank. These tanks are specially
designed and usually do not contain baffles.
7) Feed ports:
Feed ports are silicone tubes connected to the nutrient reservoir. They are used to add
nutrients and acid/alkali in the fermentor. They are sterilized in situ with stem after
connection has been completed and before any additions are made.
8) Foam Control (Antifoam agents):
Foams are dispersions of gas in liquid. Aeration and agitation of a liquid medium can
cause the production of foam. This is particularly true for the media containing high
levels of proteins or peptides. If the foam is not controlled, it will rise in the head space
of the tank and be forced from the tank along with the exit valve. This condition often
causes contamination of the fermentation from organisms picked up by breaking of
some of the foam which then drains back into the tank. Excessive foaming also causes
other problems for fermentation.
Foams in industrial fermentations are controlled either by chemical or mechanical
means. Chemicals controlling foams have been classified into antifoams, which are
added in the medium to prevent foam formation, and defoamers which are added to
knock down foams once these are formed. Some may not see much in the distinction
and in this discussion the term antifoam will refer to both. The usual procedure for
controlling foam is to add an antifoaming agent, although a supplementary impeller
blade mounted high in the tank may at times be effective.

When antifoam is required in a tank, it is added either manually or electrically.
Obviously, manually addition requires that someone continuously observe the tank so
that the antifoam can be added as required. addition of antifoam is usually preferred. To
accomplish this automatic addition, a sensing mechanism is employed to determine
when the foam has risen into the head space of bioreactor. Such a device is provided
with two electrodes mounted in the top of the fermentor. These electrodes are
connected to a pump associated with a reservoir of sterile antifoam and as the foam
rises in the reactor it touches the two electrodes in the process allowing current to flow
between them so as to activate the pump for addition of antifoam. The foam then
collapses away from the electrode thus breaking the electrical connection between them
and stopping further addition of antifoam agent.

9) Valves:
Valves are required to control the flow of gases and liquids in a variety of way. Five
types of valves are used.
Globe valves: They are suitable for general purposes on stem or a water line for use
when fully opened or fully closed. They do not regulate flow.
Butterfly valves: They are used in large diameter pipes operating under low pressure.
They are not suitable for aseptic operation.
Ball valves: They are suitable for aseptic condition. They can handle mycelial broths
and can be operated under high temperature.
Diaphragm valves: They are used for flow regulation and for stem services within
pressure limits.
Safety valves: Safety valve is incorporated in every air or stem vessel and pipe layout
which is subjected to work under pressure. These valves ensure that the pressure never
exceeds the safe upper limit of the specified value. In simple safety valves, a spindle is
lifted from its seating against the pressure of gas. Once the pressure falls below the
value set by the spring, the spindle returns to its fermentor.
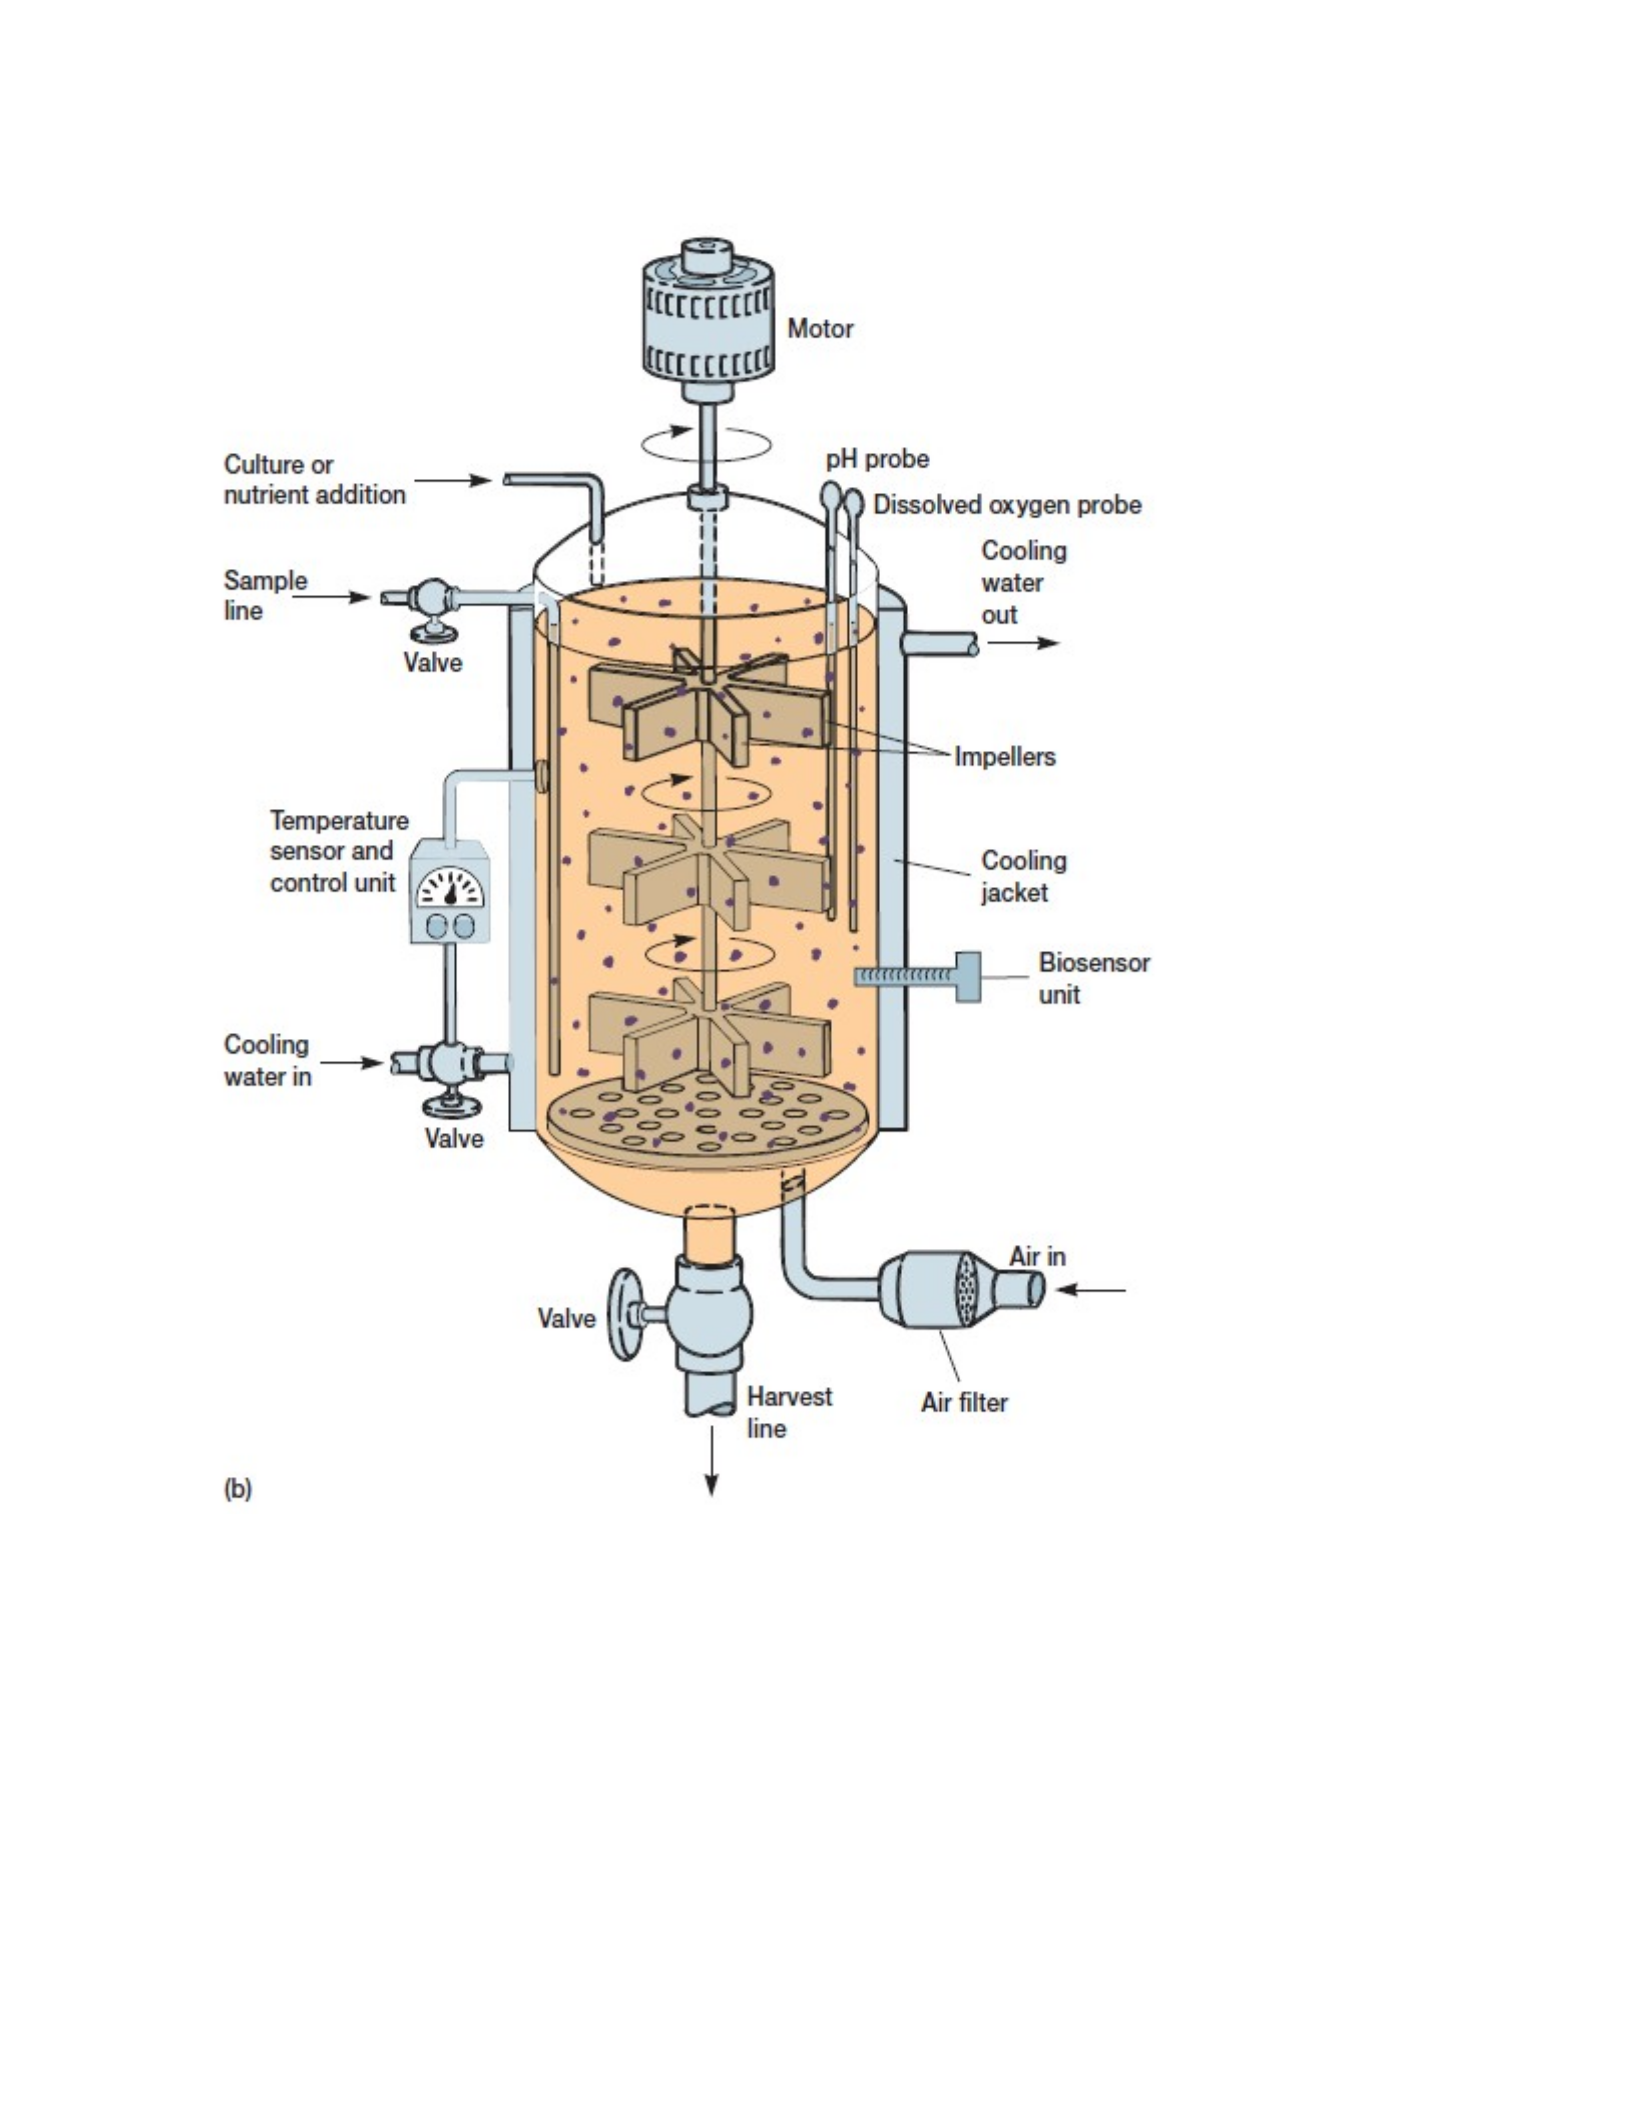
Part of Bioreactor Function
Motor Provides energy to the impeller in order to
generate it.
Impeller Mix the media by stirring.
Sparger Introduces air in the form of bubbles
Baffles Prevent vortexing of culture.
Inlet Air Filter Remove contaminants; adjust flow rate
Exhaust Ait Filter Filter used air moving out to the
environment
Rotameter Measures the flow rate of the air.
Pressure Gauge Measures the pressure.
Temperature Gauge Measures temperature, giving the culture
broth an appropriate warmness to maintain
in.
Coolinng Jacket Control Temperature
pH probe Measures pH
Dissolved Oxygen Probe Measures the amount of dissolved oxygen
Foam Probe Detect the presence of foam
Acid Added when pH too high (Alkaline)
Base Added when pH too low (Acidic)
Antifoam pump Adds anti-foam agent when foam is present
in the fermentor with a peristaltic pump.
Sampling Tube Inoculation, addition of acid or base, and
sample removal.
Control Panel Controls the fermentor that is working
Level Probe Measures the level of probe
Types of Bioreactors / Fermentors
Depending on the design of the reactor, the bioreactors are of following types:
i) Batch (Stirred tank batch) bioreactors
ii) Continuous stirred tank bioreactors a) Single-stage continuous bioreactors
b) Multiple-stage continuous bioreactors
c) Recycled single or multiple stage continuous bioreactors
d) Semi-continuous bioreactors
iii) Bubble column bioreactors
iv) Airlift bioreactors
v) Fluidized bed bioreactors
vi) Packed bed bioreactors
vii) Photobioreactors

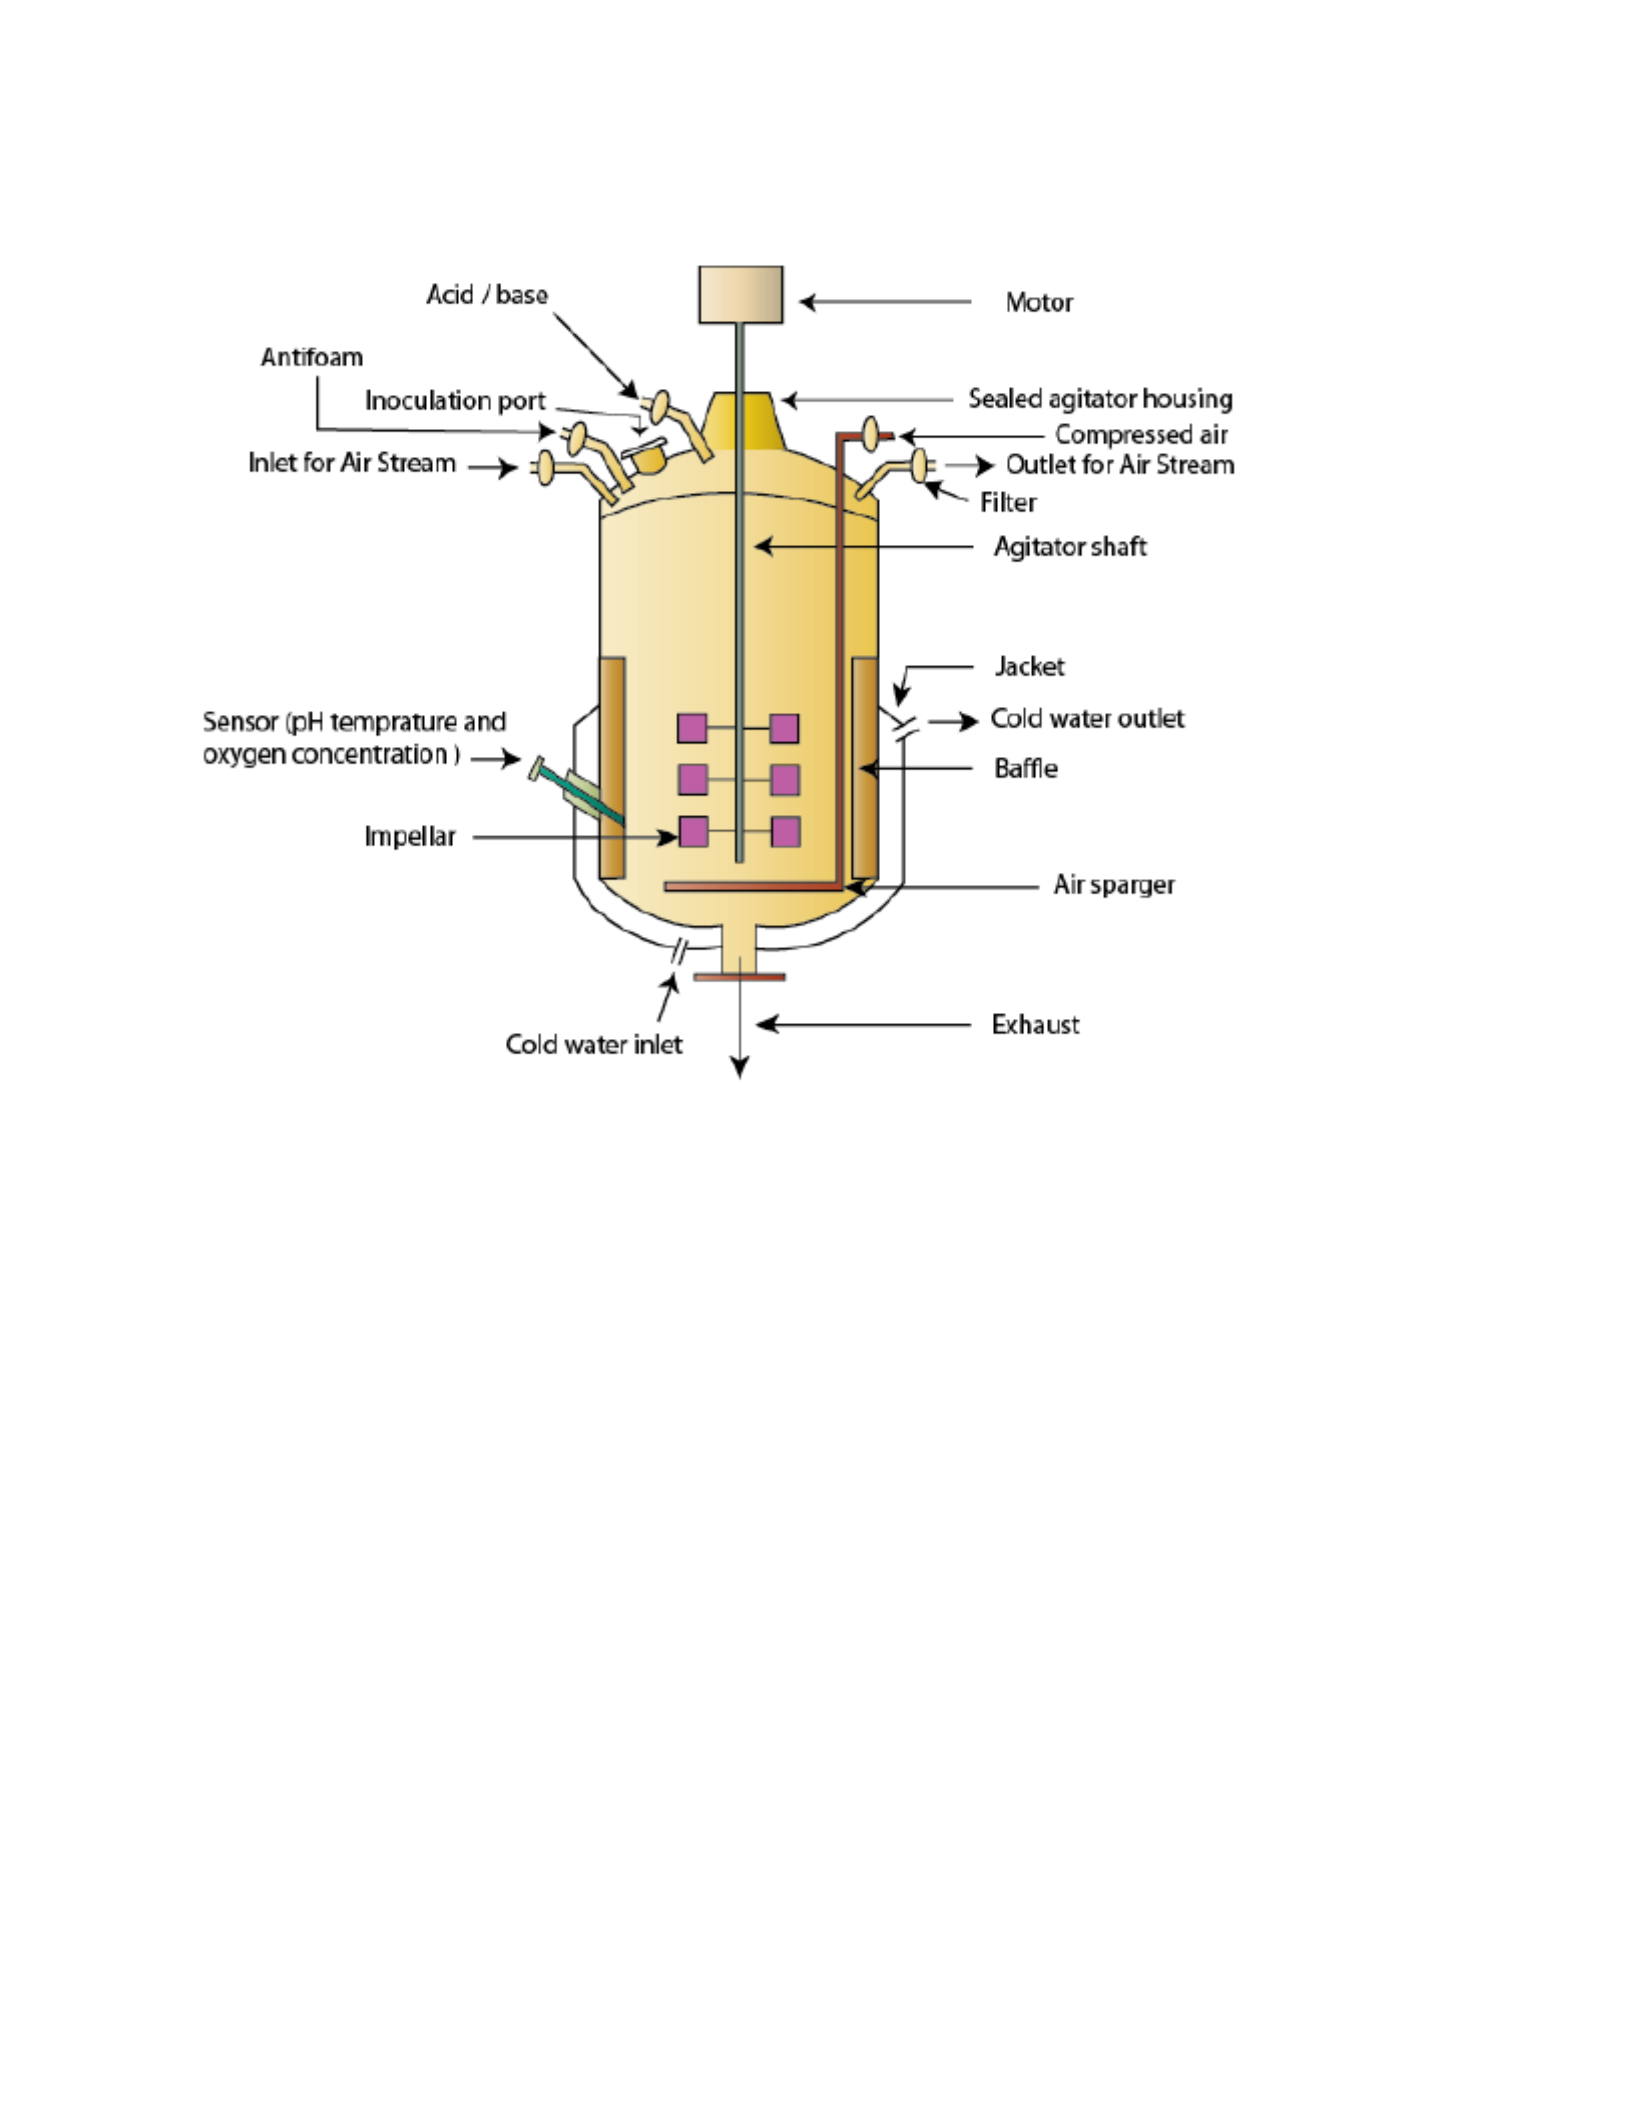
i) Batch (Stirred tank batch) bioreactors -
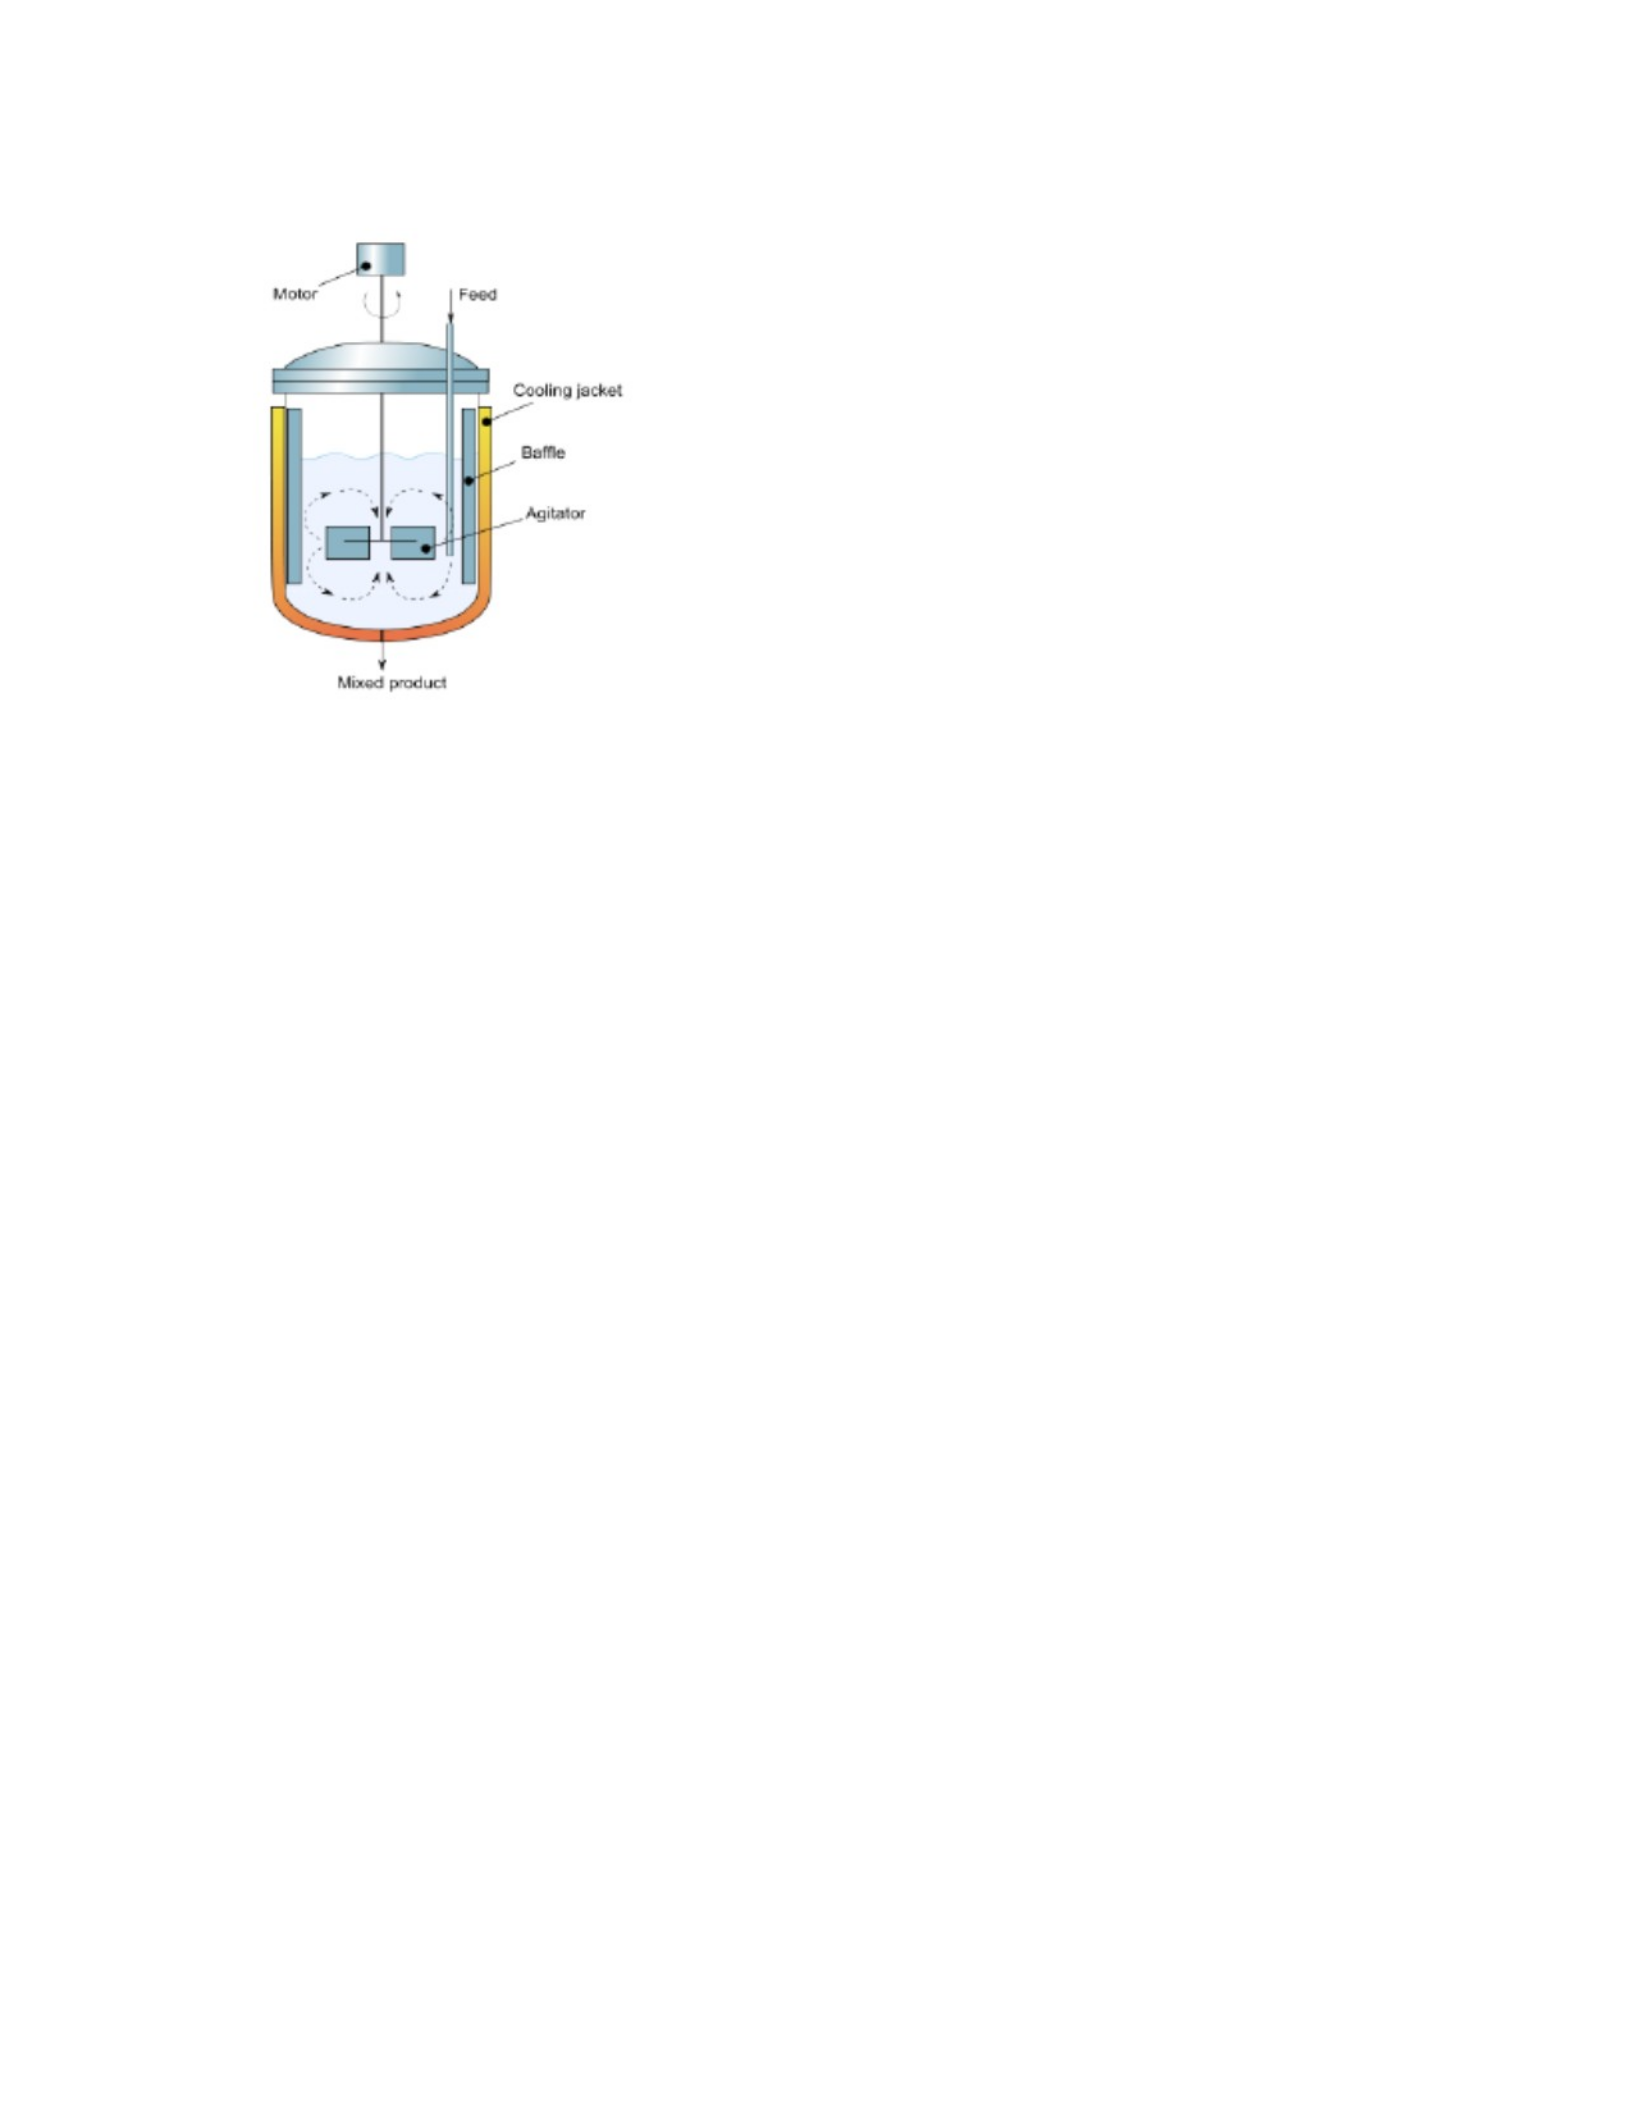
These bioreactors have a cylindrical vessel with motor driven central shaft which gives
support to one or more agitators (impellers). The shaft is fitted at the bottom of the
bioreactor. The diameter of the impeller is usually one third of the vessel diameter. The
impellers are available in different designs like- Rustom disc, concave bladded, marine
propeller etc. In stirred tank reactors, the air is added to the culture medium under
pressure through a device called sparger. The sparger along with the impellers
(agitators) enables better and efficient gas distribution throughout in the vessel. The
advantages of using stirred tank reactors are: the efficient transfer of gas to growing
cells which keeps the growth of cells in healthy limits, stirring ensures good mixing of
the contents, the operating conditions are flexible and the bioreactors are easily
available which makes them commercially viable products.
(ii) Continuous stirred tank bioreactors:
The tank used in this system is essentially similar to that of the batch fermentor. It
differs only in so far as there is provision for the inlet of medium and the outlet of broth.
In continuous fermentations nutrients are continuously added, and products are also
continuously removed. There are four types of continuous stirred tank fermentors –
a) Single-stage continuous bioreactors
There are fermentations in which the entire operation is carried out in one vessel, the
nutrient being added simultaneously with broth outflow. This system is suited for growth
related fermentations such as yeast, alcohol, or organic acid production.
B) Multiple-stage continuous bioreactors
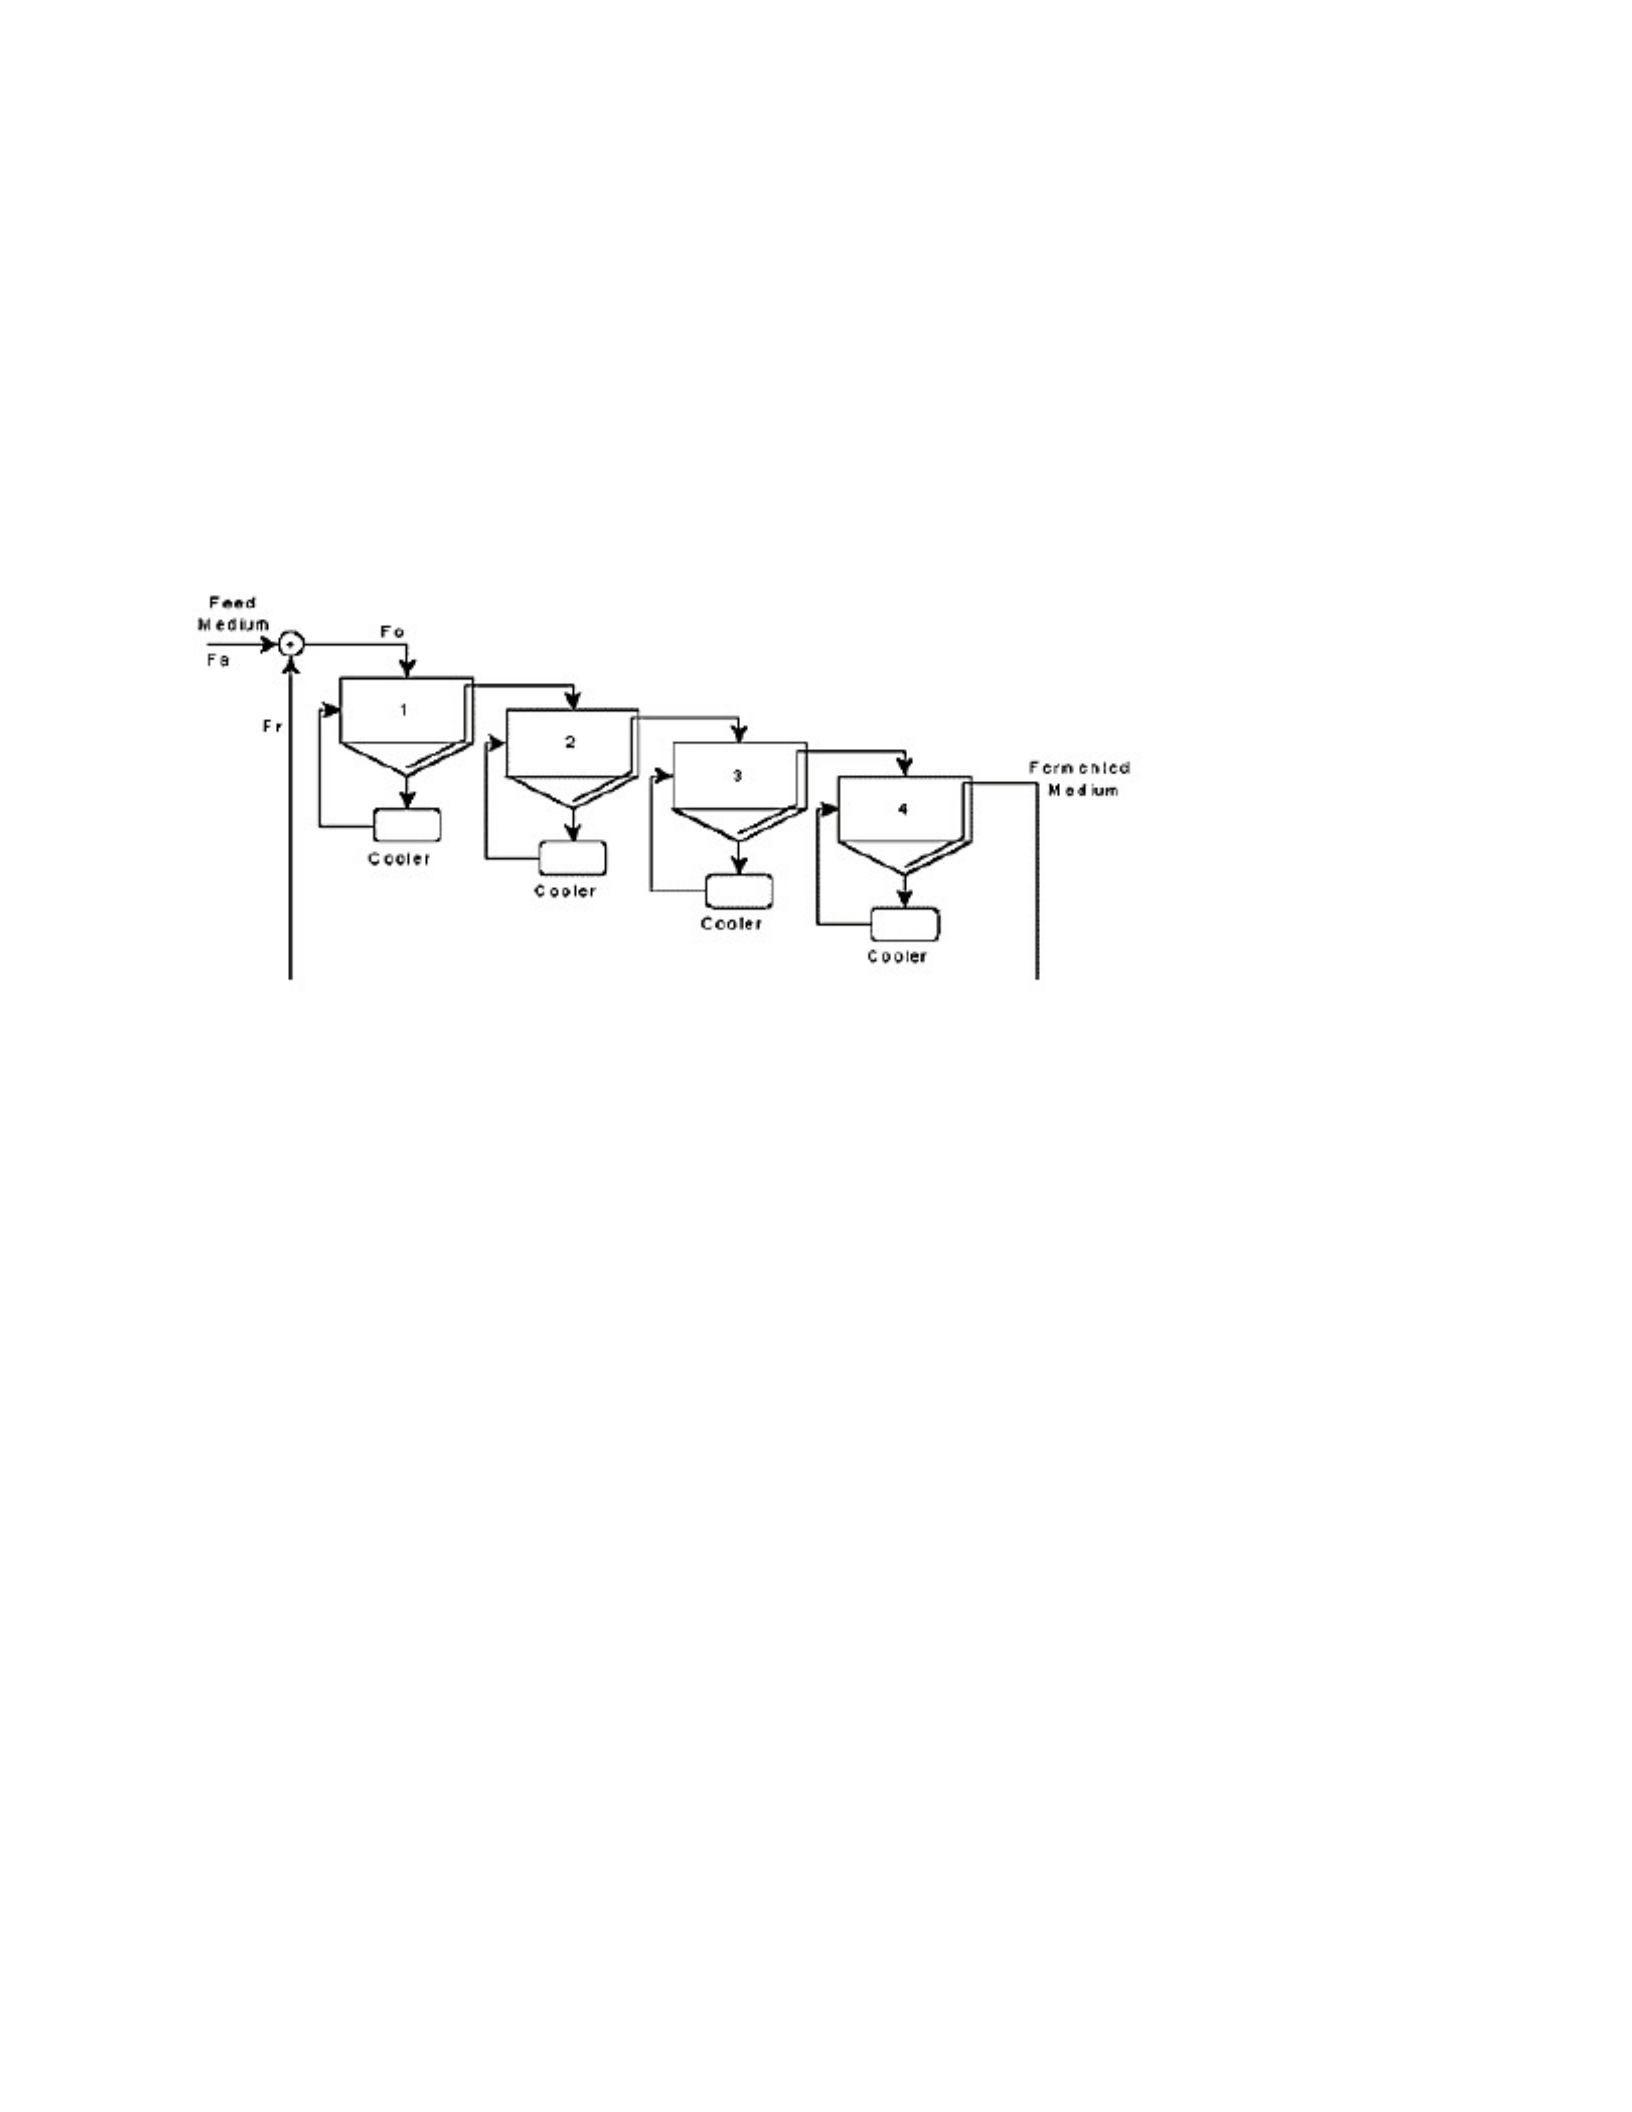
This consists of a series of fermentation tanks. The medium is led into the first and the
out flow into the second, third, or fourth as the case may be. This is most frequently
used for the fermentation involving metabolites. The first tank may be used for the
growth phase and subsequent tanks for production.
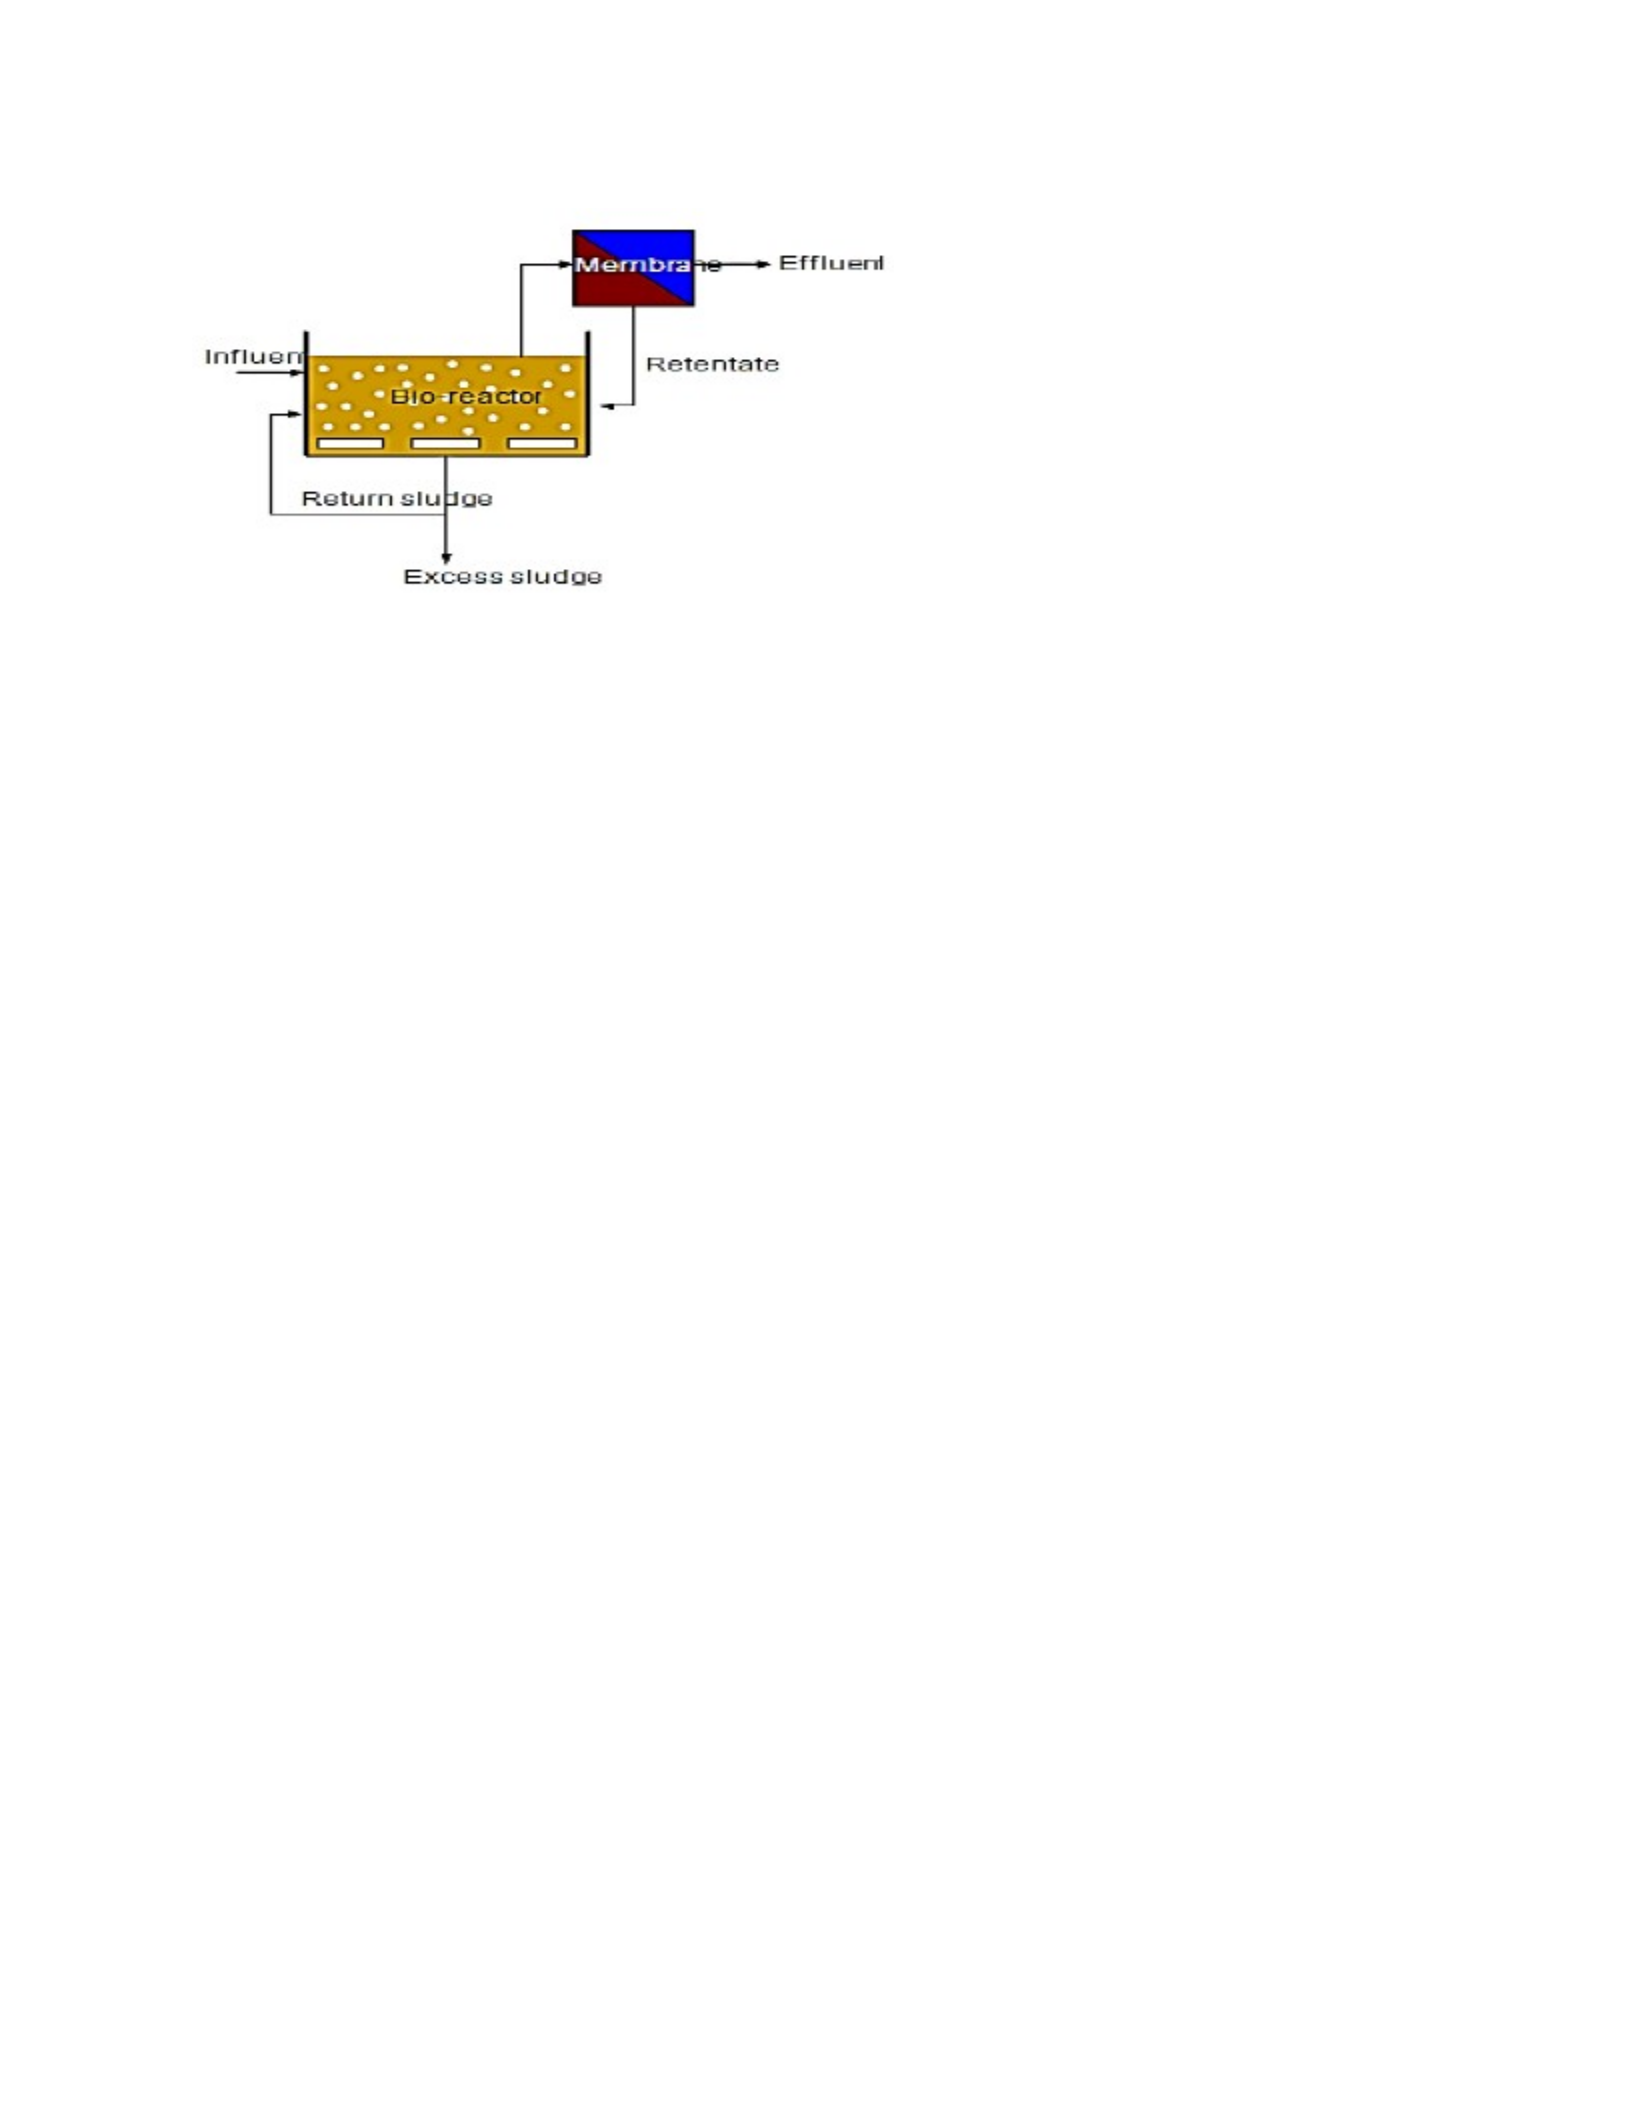
c) Recycled single or multiple stage continuous bioreactors
The out flowing broth may be feed of the organisms by centrifugation and the
supernatant returned to the system. This system is particularly useful where the
substance is difficult to degrade or not easily miscible with water such as in
hydrocarbons. Recycling can be applied in a single stage fermentor. In a multiple stage
fermentor, recycling may involve all or some of the fermentation vessels in the series
depending on the need.
d) Semi-continuous bioreactors
In semi-continuous fermentations, simultaneous nutrient addition and outflow withdrawal
are carried out intermittently, rather than continuously.
iii) Bubble column bioreactors–
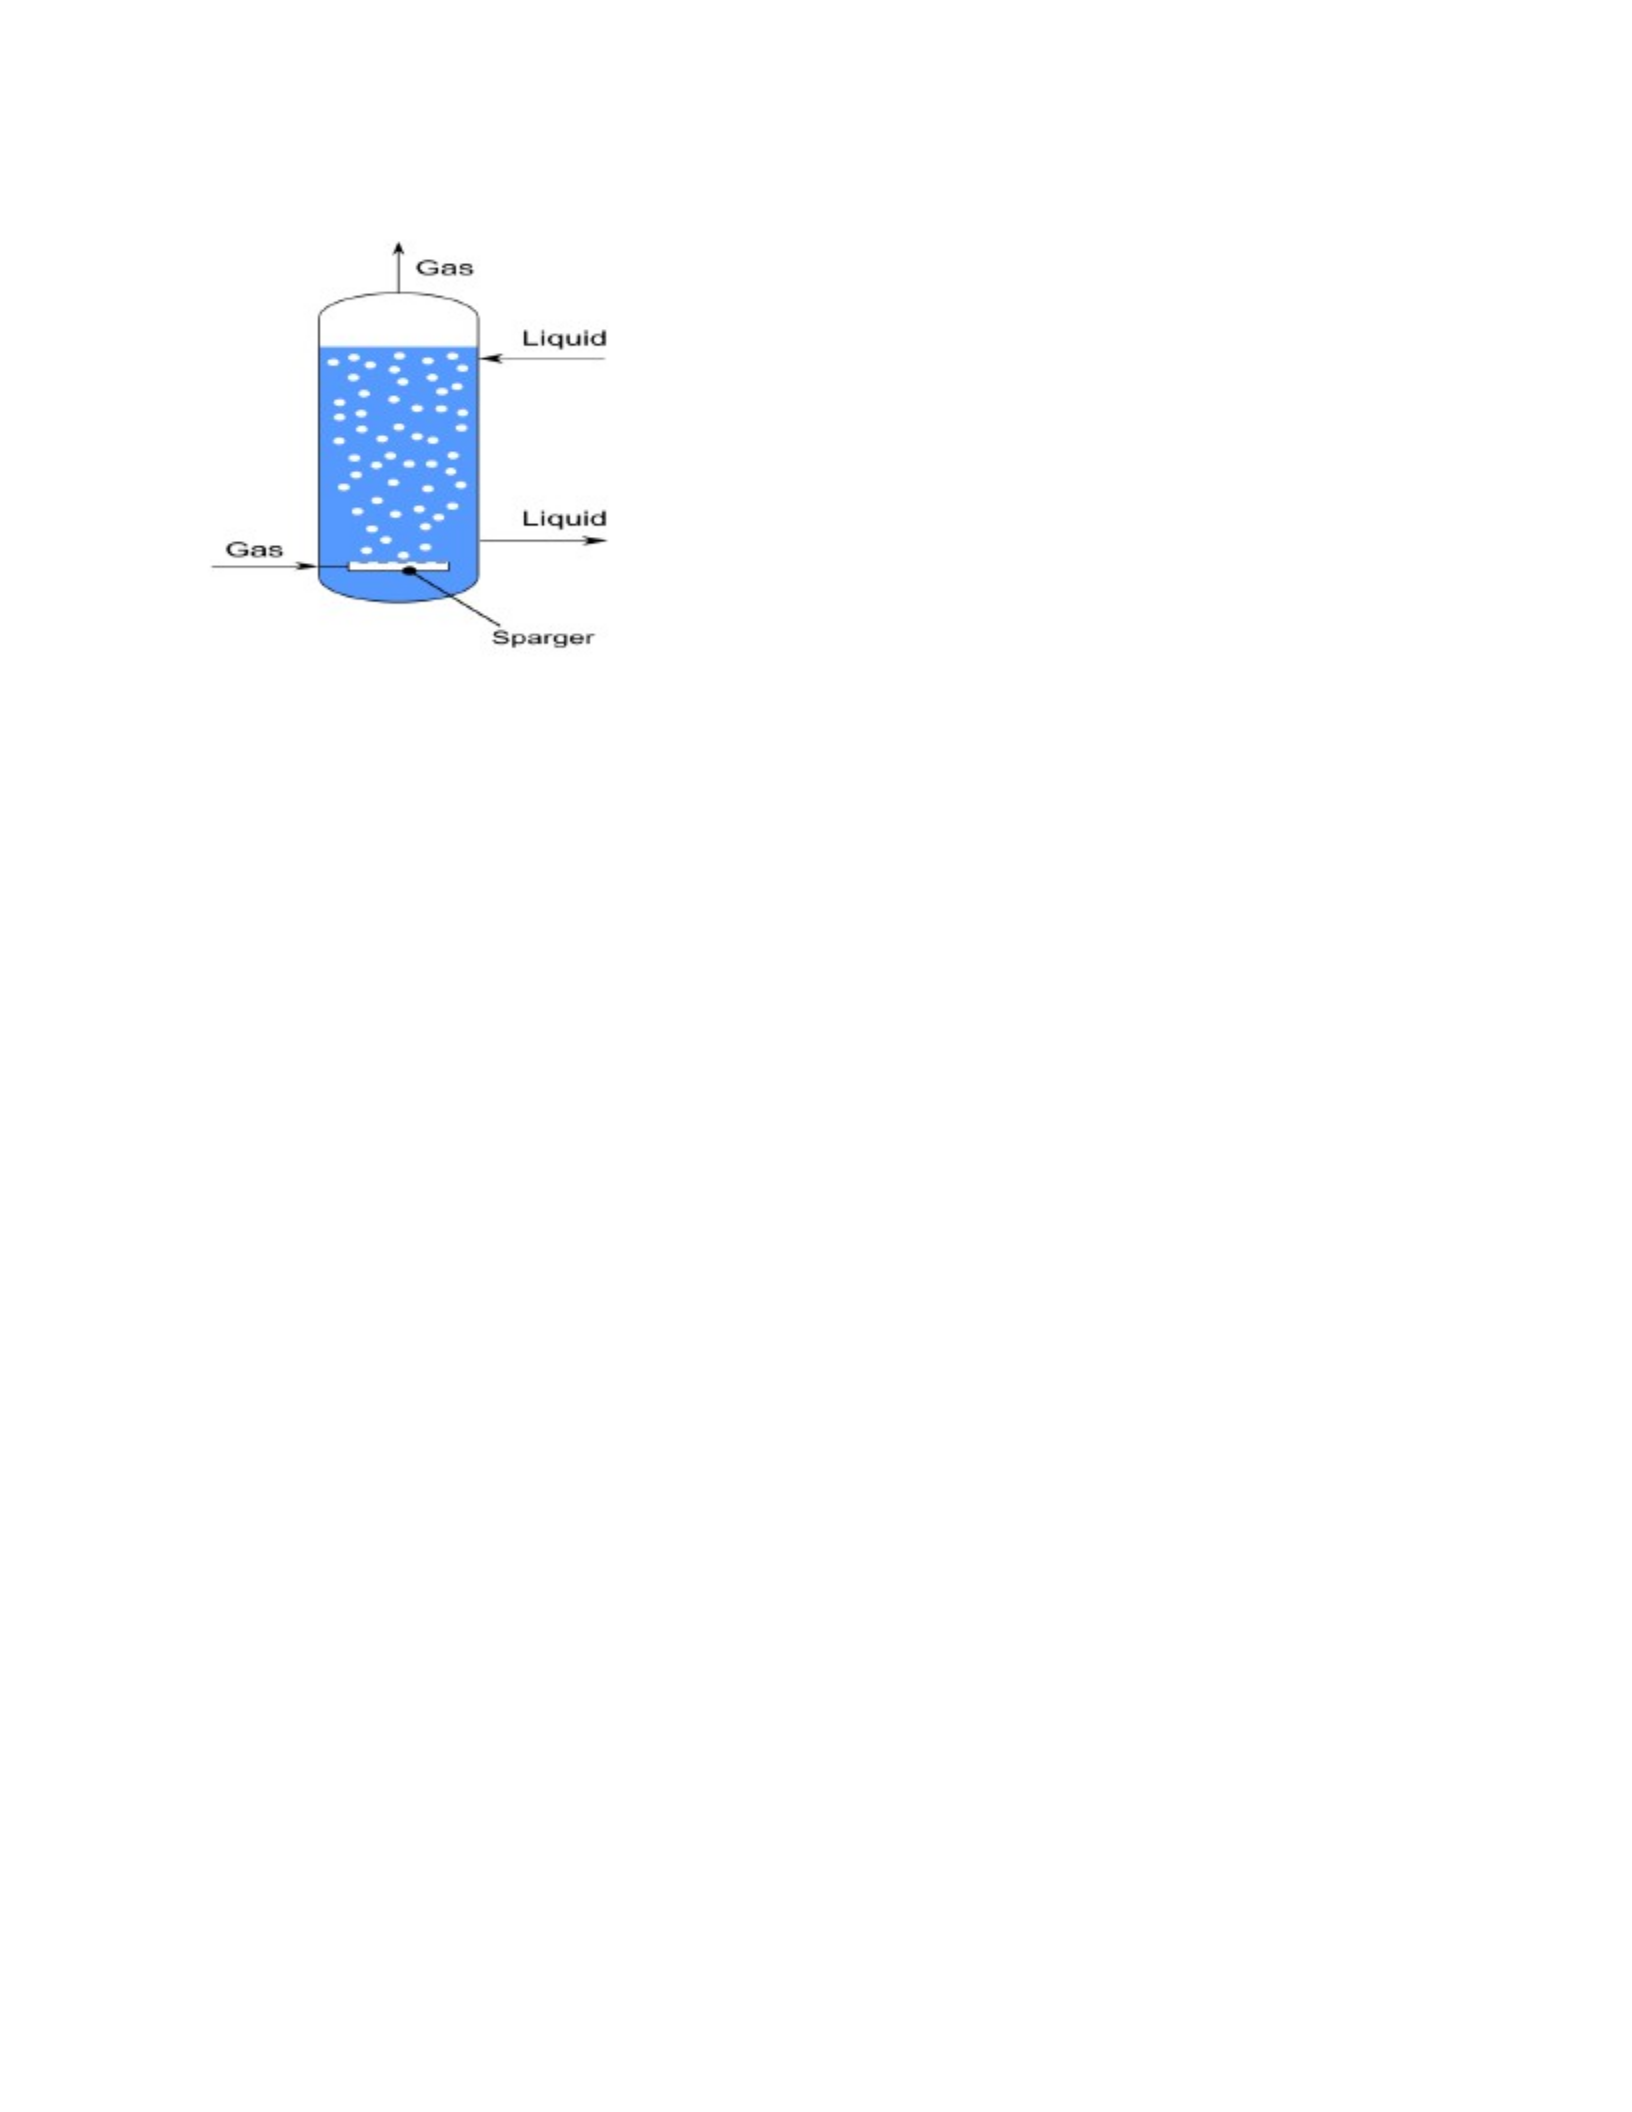
In these bioreactors, the gas or air is introduced at the base of the column through
perforated pipes or plates, or metal microporous spargers. The vessel used for bubble
column bioreactors is usually cylindrical with an aspect ratio (height to diameter ratio) of
4-6. The rate of flow of gas affects the O2 transfer and mixing.
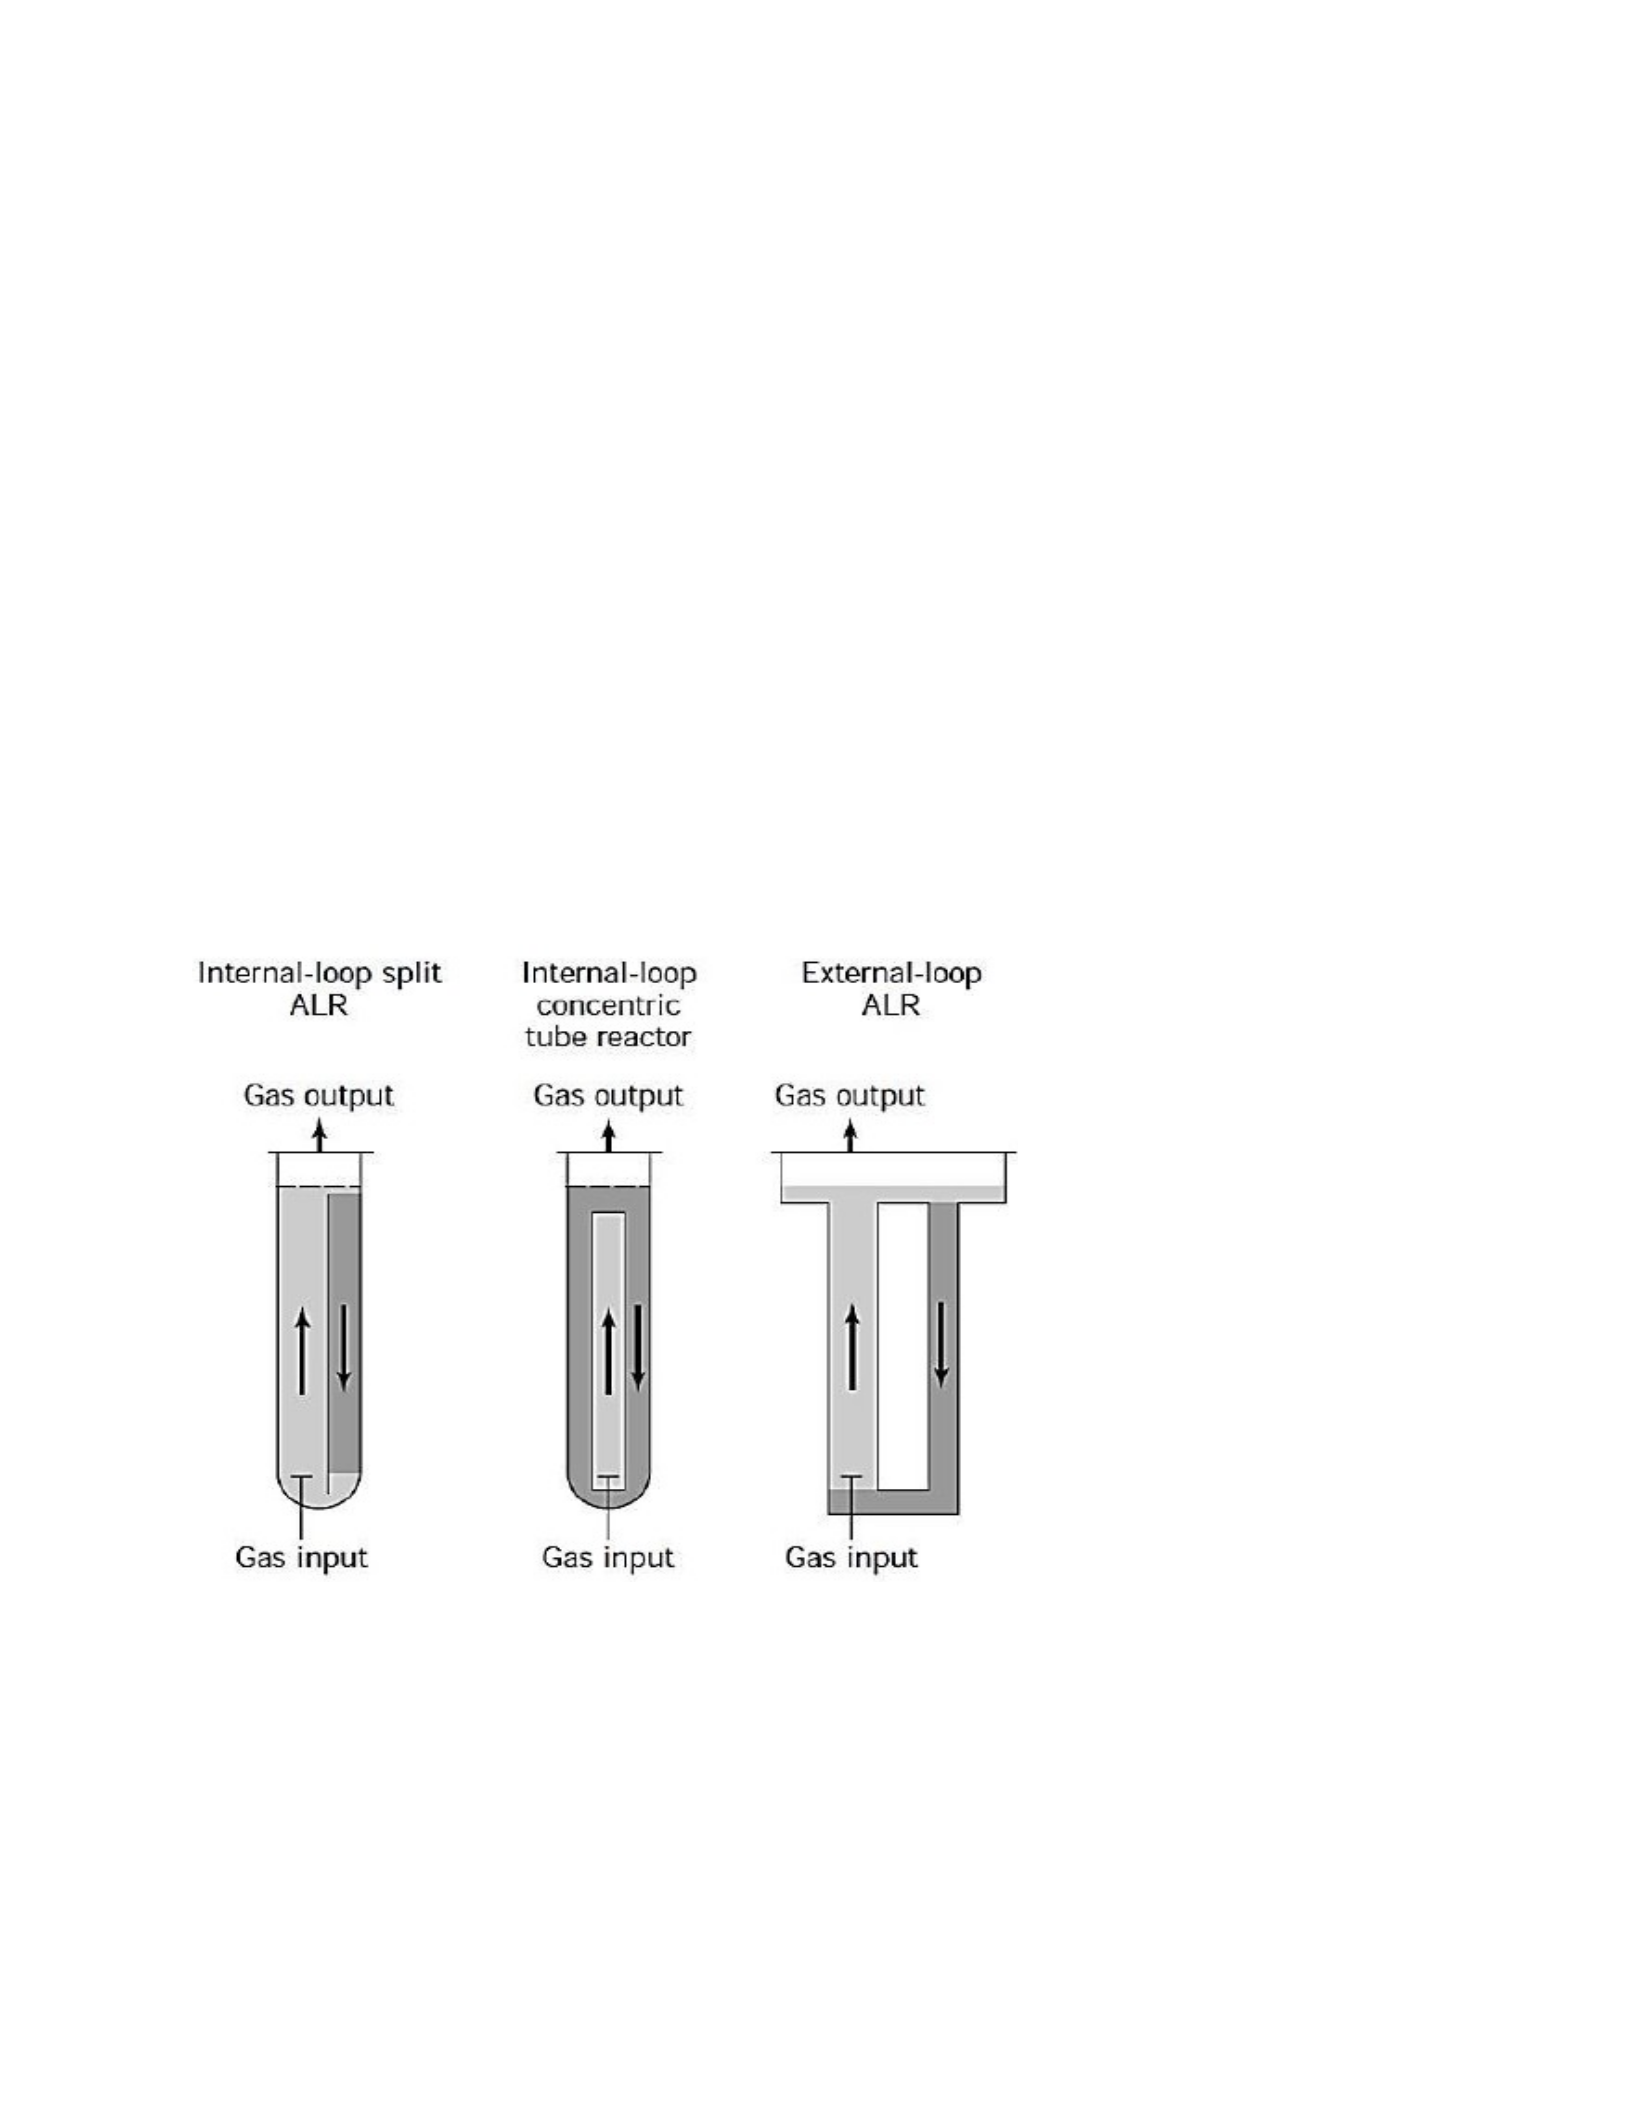
iv Airlift bioreactors – Airlift bioreactors are commonly used for aerobic bioprocessing
technology. In the airlift bioreactors, the medium of the vessel is divided into two
interconnected zones by means of baffle or draft tube. The air/gas is pumped into one
of the two zones referred to as ‘riser’ and the other zone that receives no gas is known
as ‘downcomer’. The dispersion flows up the riser zone while the down flow occurs in
the downcomer. Further there are two types of bioreactors.
1) Internal loop bioreactor - These bioreactors have a single container with a central
draft tube that creates interior liquid circulation channels which keeps the volume and
circulation at a fixed rate for fermentation.
2) External loop airlift bioreactor-These have an external loop to keep the liquid in
circulation through separate independent channels. The modifications can be made in
these bioreactors depending on the requirements of different fermentation processes.
3) Two stage airlift bioreactors -These bioreactors have two bioreactors which are
basically used for the temperature dependent formation of products. The growing cells
from one bioreactor (maintained at temperature 300C are pumped into another
bioreactor (at temperature 420C). This is done because it is very difficult to increase the
temperature quickly from 300C to 420C in the same vessel. The cells are grown in the
first bioreactor and with the help of the fitted valves and a transfer tube and pump, they
are transferred into the second bioreactor, where the actual bioprocessing takes place.
4) Tower bioreactors - In this type of bioreactor, a high hydrostatic pressure is generated
at the bottom of the reactor which increases the solubility of O2 in the medium. Since
the top is expanded, the pressure is reduced which helps in the expulsion of CO2. The
cycle completes with the medium flowing back into the downcomer. The advantage with
Tower bioreactor is that it has high aeration capacities without having moving parts.
v) Fluidized bed bioreactors–
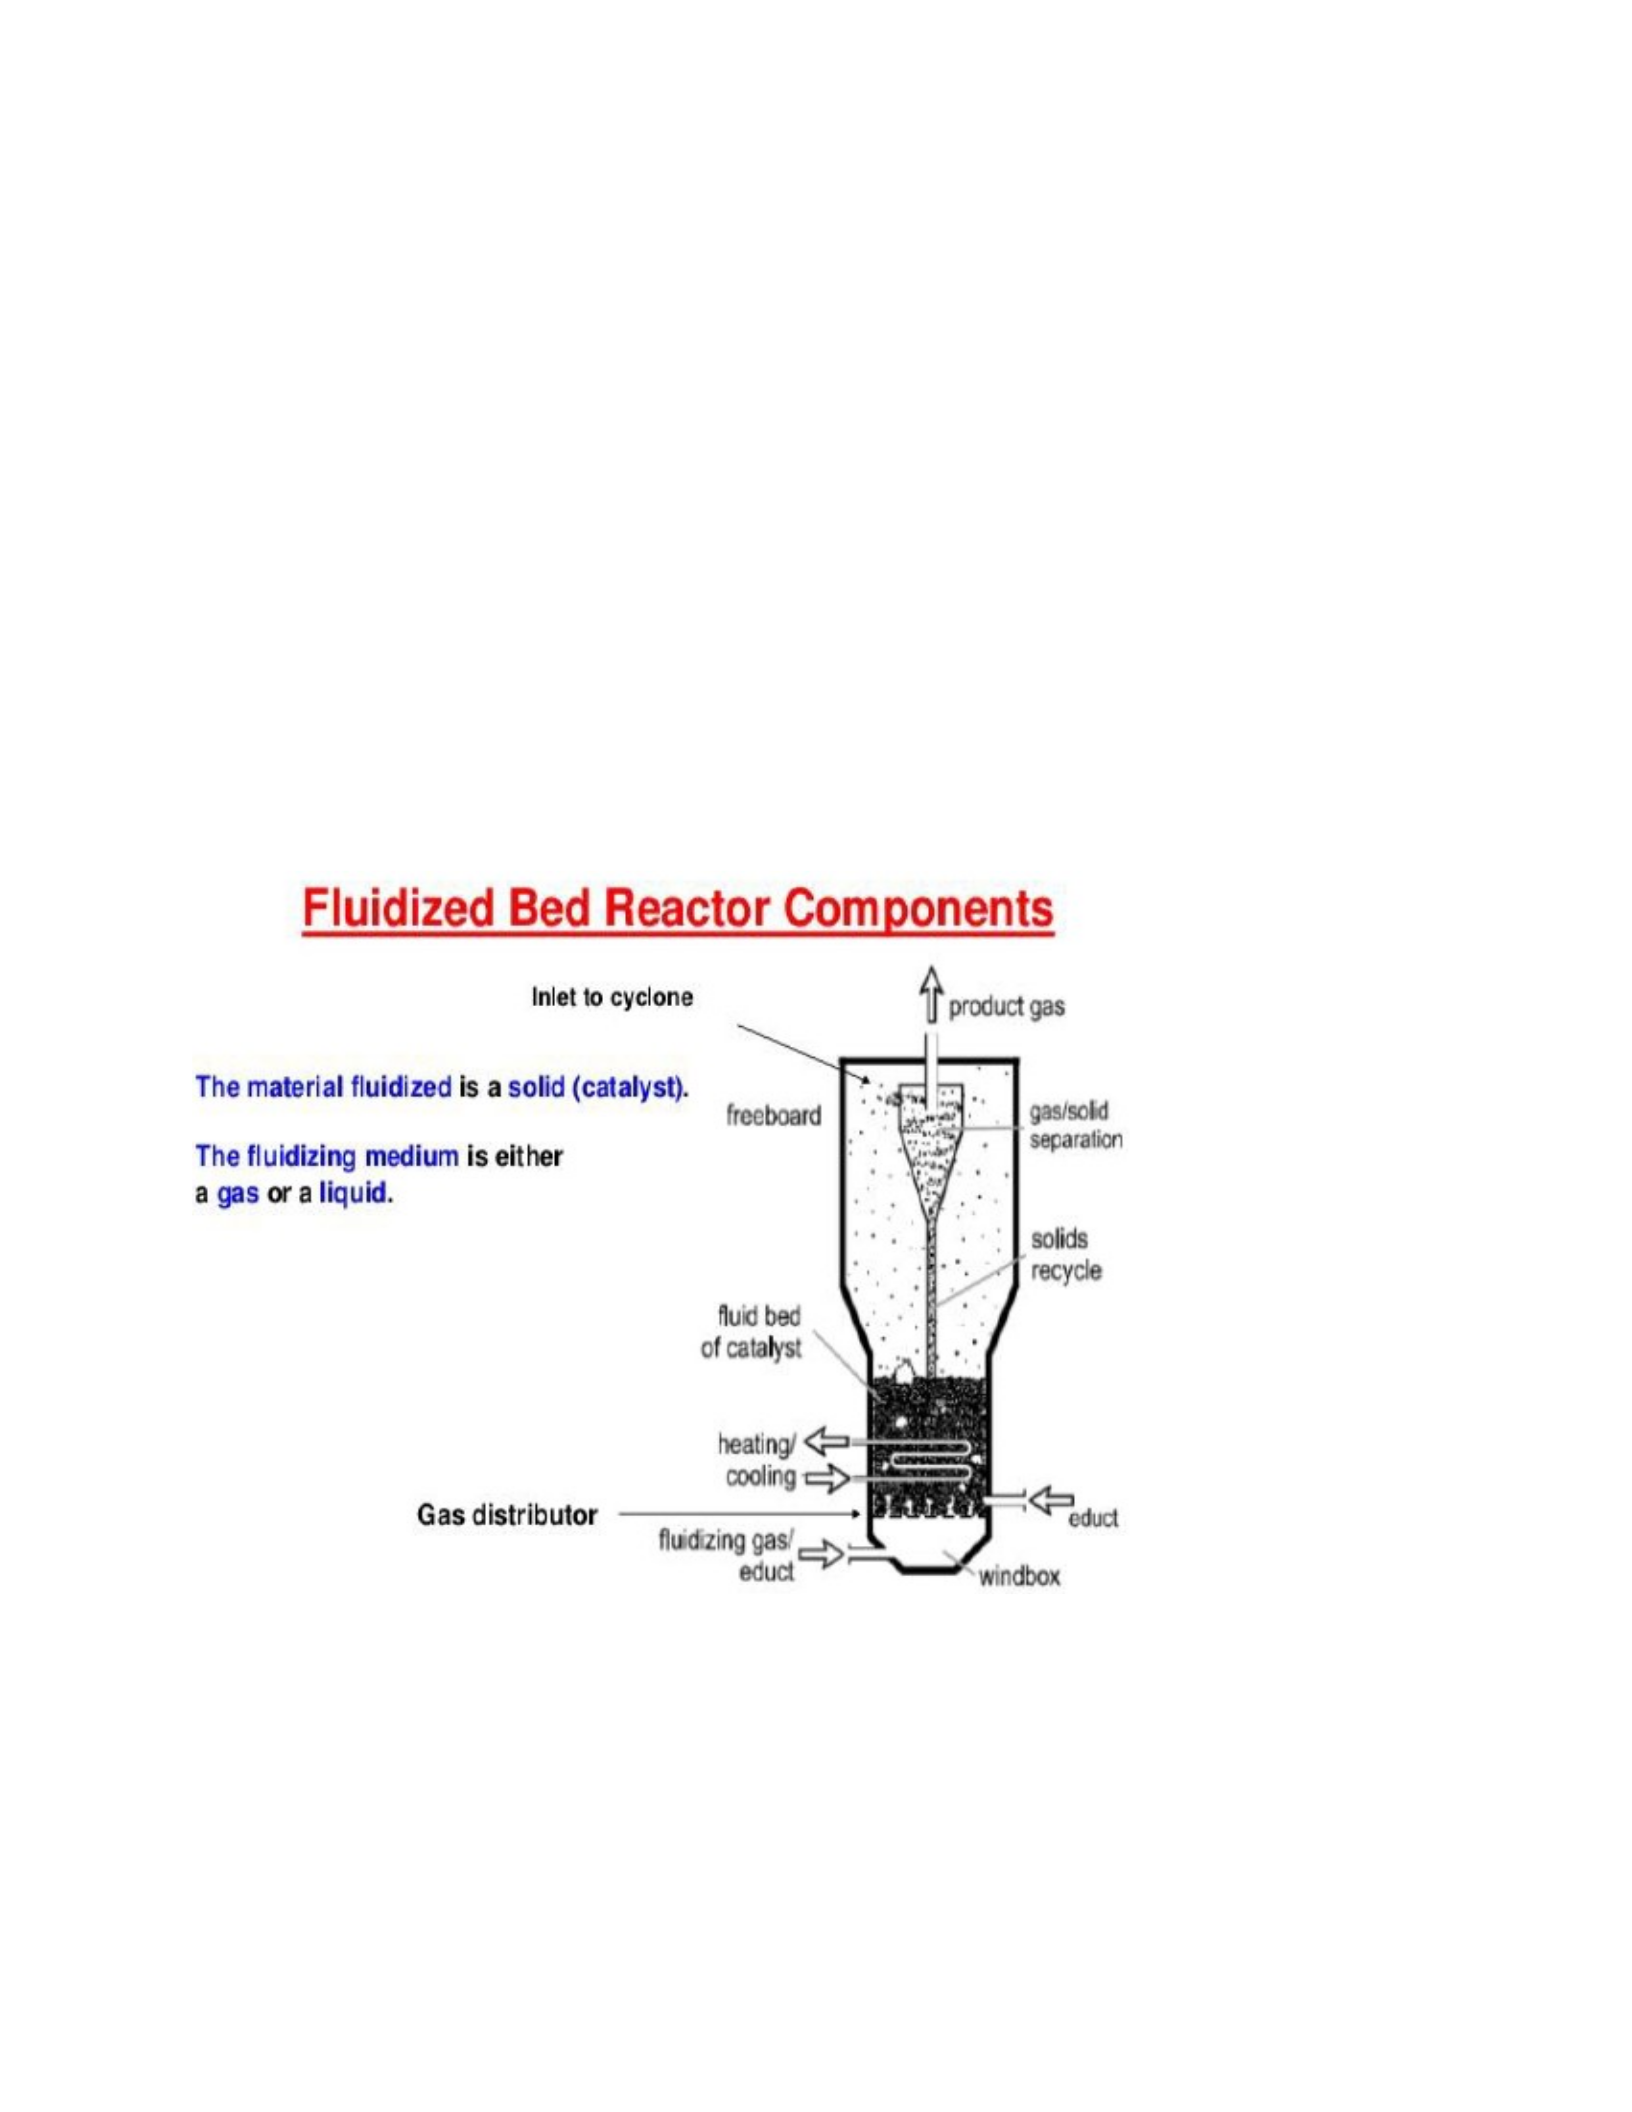
These bioreactors are mainly suitable to carry out reactions involving fluid suspended
biocatalysts such as immobilized enzymes, immobilized cells, microbial flocs etc. The
design of the bioreactors is such that the top is extended and the reaction column is
narrow which retains the solids in the reactor and allows the liquids to flow out. To
maintain an efficient operation of fluidized beds, gas is sparged to create a suitable gas-
liquid-solid fluid bed. The recycling of the liquid ensures continuous contact between the
reaction contents and biocatalysts which increases the efficiency of bioprocessing.
vi) Packed bed bioreactors-
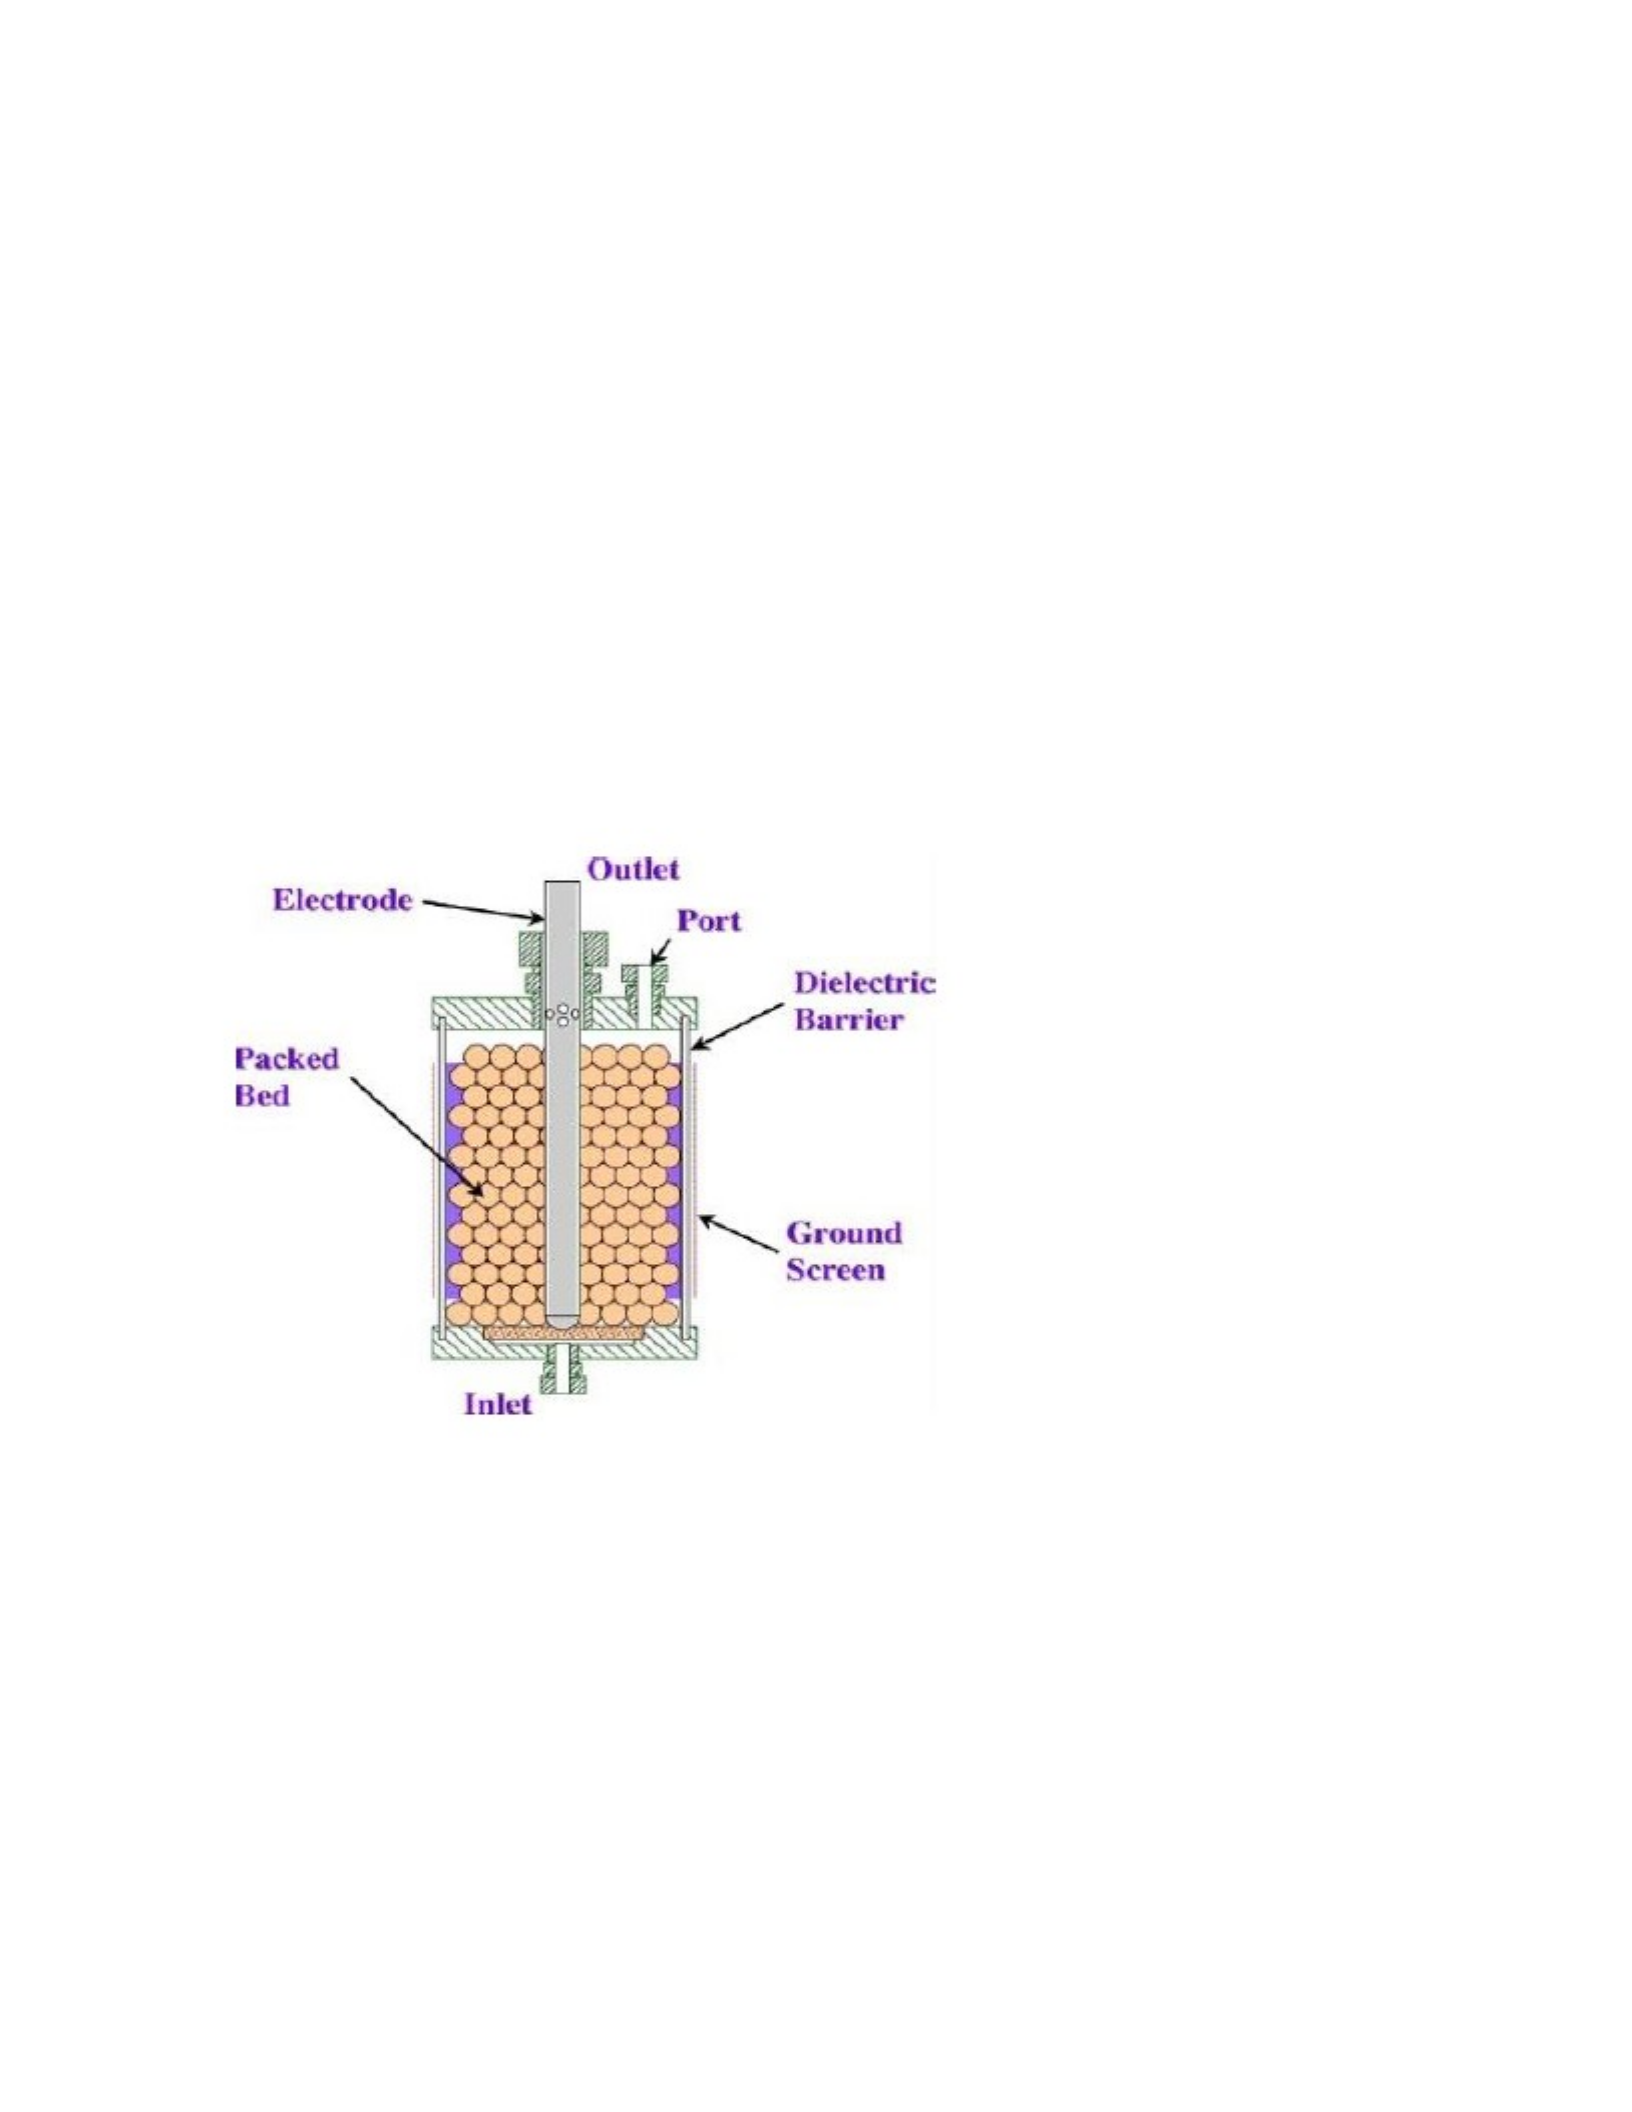
A packed bed bioreactor consists of a bed of solid particles, with biocatalysts on or
within the matrix of solids, packed in a column. The solids are generally porous or non-
porous gels which may be compressible or rigid in nature. The nutrient broth
continuously flows over the immobilized biocatalyst and the products are released into
the fluid from where they are removed. However, due to poor mixing, it is difficult to
control the pH of packed bioreactors by the addition of acid or alkali.
iv) Photobioreactors–
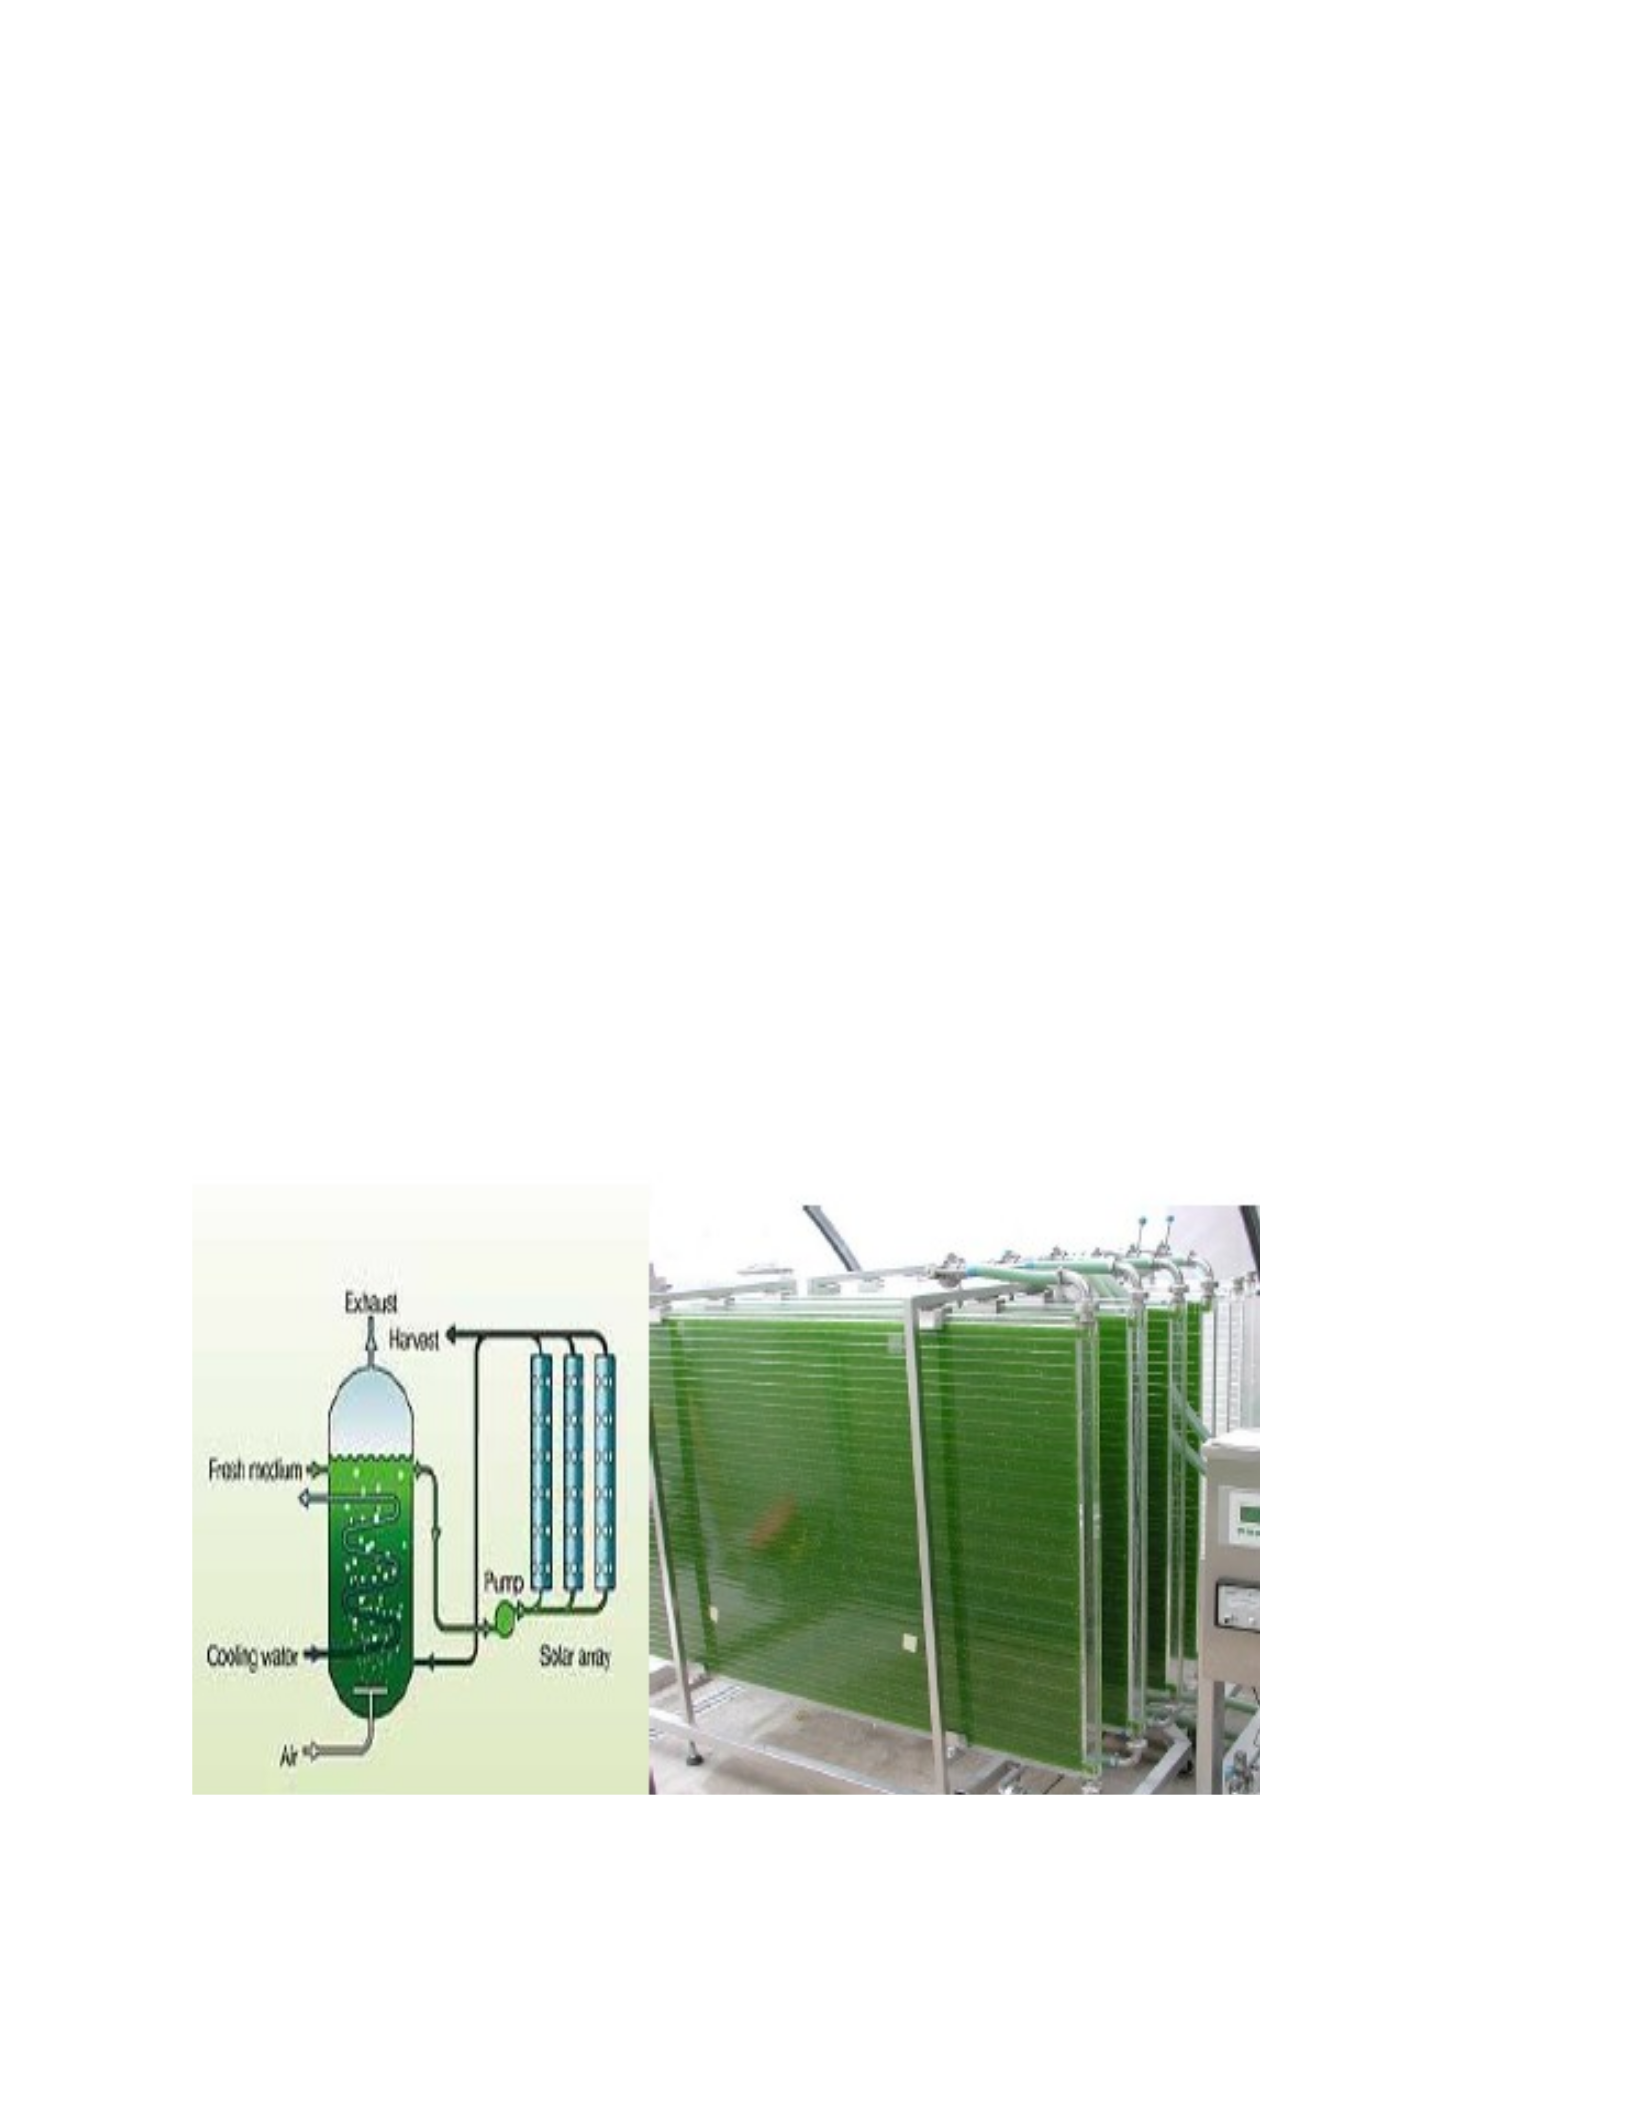
These bioreactors are specialized for fermentation that can be carried out either by
exposing to sunlight or artificial illumination. The photobioreactors are made up of glass
or transparent plastic which are the solar receivers. The cell cultures are circulated
through the solar receivers by using centrifugal pumps or airlift pumps. These
bioreactors work in the temperature which ranges from 25-400C. In these bioreactors,
the microorganisms e.g. microalgae, cyanobacteria etc. grow during the day time while
the products (e.g. beta-carotene, asthaxanthin) are produced during the night.
===================================================

Scale up and scale down of fermentation
Two of the most common phrases one often met in fermentation technology research
are 'Scaling up' and 'Scaling down' studies. However, the phrase 'scaling up' is more
commonly understood and practiced during the designing of industrial scale fermentors.
Whereas 'scaling down' studies are rarely heard that frequent.
A good example is when we intend to start with a fermentation process with the ultimate
objective of producing the fermentation products on the level of industrial scale.
Products need to be produced at large volume so that the process is economically
viable. This requires scaling up. We do scaling up studies to ensure that the
fermentation process is technically and economically viable to be produced in the end at
a large scale.
SCALE UP STUDIES
Scale up studies are studies carried out at the laboratory or even pilot plant scale
fermentors to yield data that could be used to extrapolate and build the large scale
industrial fermentors with sufficient confidence it will function properly with all its
behaviours anticipated. More important during scale up exercises you are trying to build
industrial size fermentor capable or close of producing the fermentation products as
efficient as those produced in small scale fermentors.
INITIAL SCALE UP STUDIES

Most scale up studies are usually carried at different phases involving different scales of
fermentors. Preliminary work is carried out at the level of petri dishes and small scale
laboratory fermentors to establish whether the process is:
Technically viable, meaning it is possible to produce such fermentation process and the
products on the small scale. Additional parameters not provided by petri dishes studies
and for more confidence are obtained by carrying further studies using submerged liquid
fermentation using various sizes laboratory scale fermentors and even a pilot plant
fermentor.

There are a few rules of the thumb followed when doing scale up studies such as: a)
Similarity in the geometry and configuration of fermentors used in scaling up b) A
minimum of three or four stages of increment in the scaling up of the volume of
fermentation studies. Each jump in scale should be by a magnitude or power increase
and not an increase of a few litres capacity. Slight increase in the working volume would
not yield significant data for scale up operation.
It must be appreciated as the size of fermentation increases during scale up various
parameters measured might not show a predictable linear co relationship. Certain
parameters change some remained constant. Some parameters need to be modified
and adjusted during scale up studies. The objective is to try to get the same
fermentation efficiency as obtained in small scale fermentors at the most economical
values.
The exercise in scaling up involved a number of programmed research or steps that has
to be established so as to predict the final behaviour of the final large scale production
fermentor. Studies carried out during scale up include:
1. Inoculum development.
2. Sterilization establishing the correct sterilization cycle at larger loads.
3. Environmental parameters such as nutrient availability, pH, temperature, dissolved
oxygen, dissolved carbon dioxide,
4. Shear conditions, foam production.
SCALE DOWN STUDIES

In scale down studies the main objective is to carry out studies on smaller bioreactors in
order to gain data and confidence and predict the behaviour how things actually will
behave in large production fermentor. Scales down studies are also used while during
the operation of large industrial scale fermentors in trouble shooting or trying to optimize
the industrial scale fermentation. This method is called the fermentation monitoring
experiment. The goal when scaling down is to create a small-scale or lab-scale system
that mimics the performance of its large-scale (pilot or manufacturing) counterpart,
when both the process parameters are varied within their operating ranges and also
when a process parameter deviates outside its operating range.
The main type of studies in scale down such as:
1. Medium design
2. Medium sterilization
3. Inoculation procedures
4. Number of generations
5. Mixing
6. Oxygen transfer rate

