


Draft a response to another students original discussion board post. This students
post is answering questions related to a case study. This response must include 3
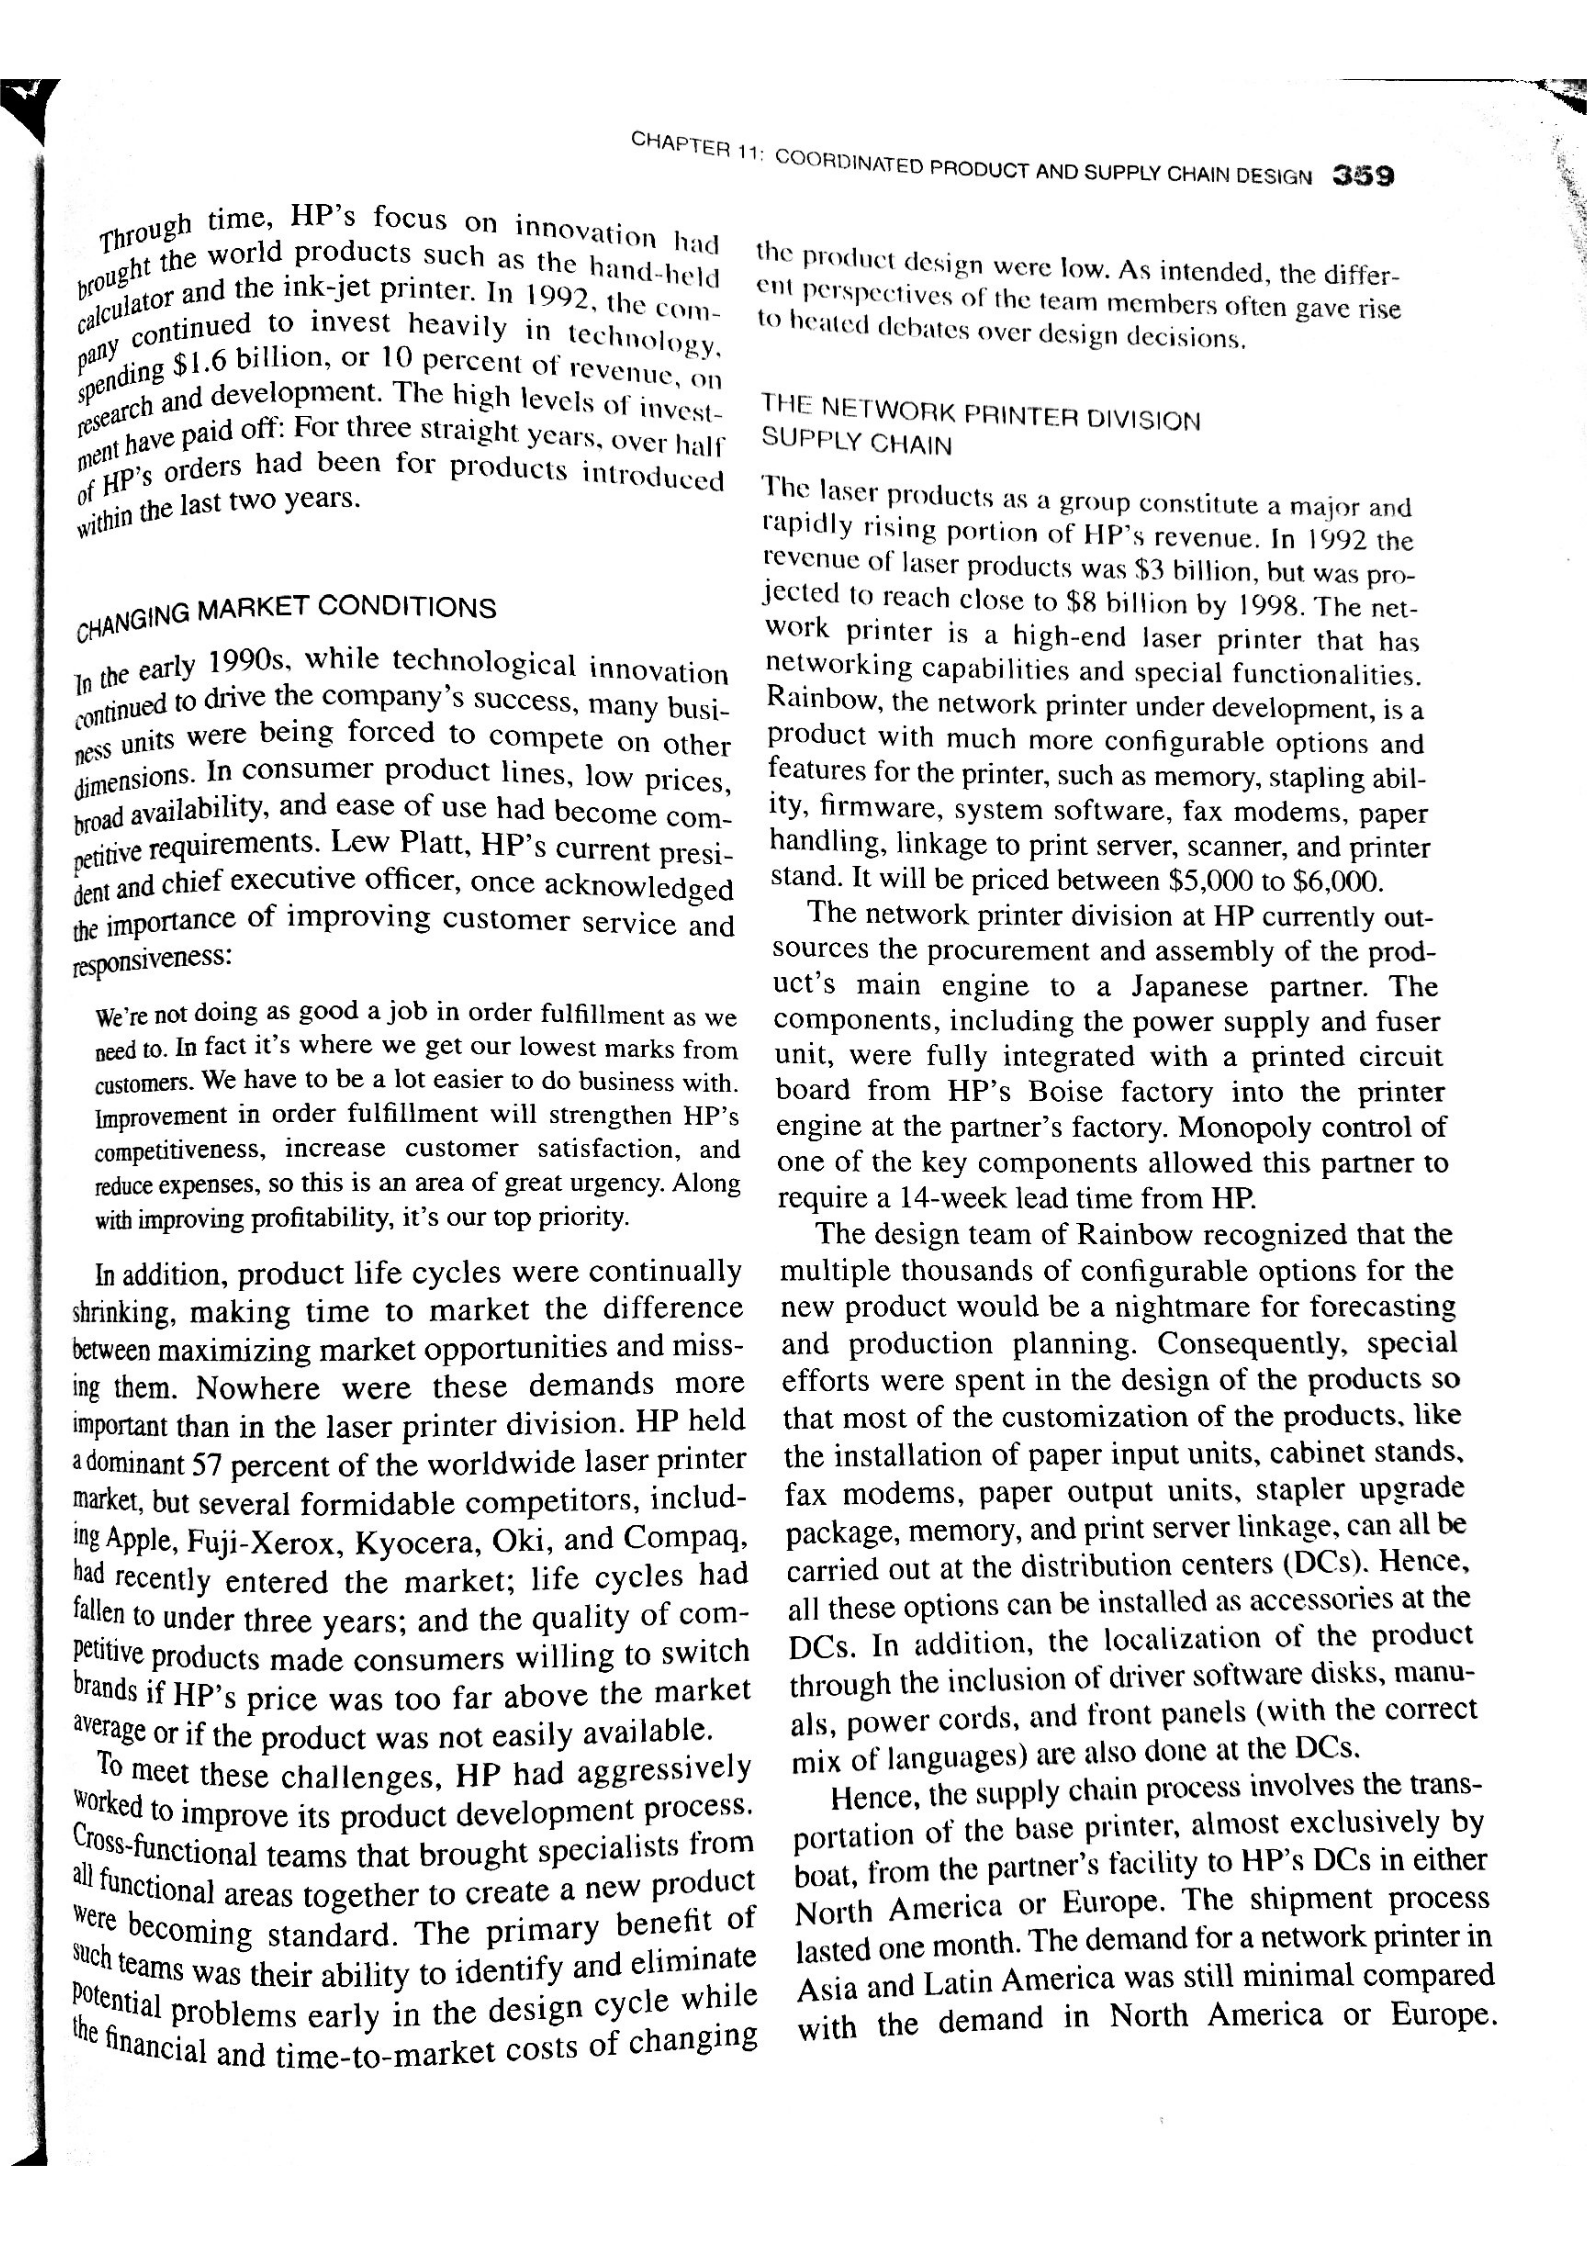
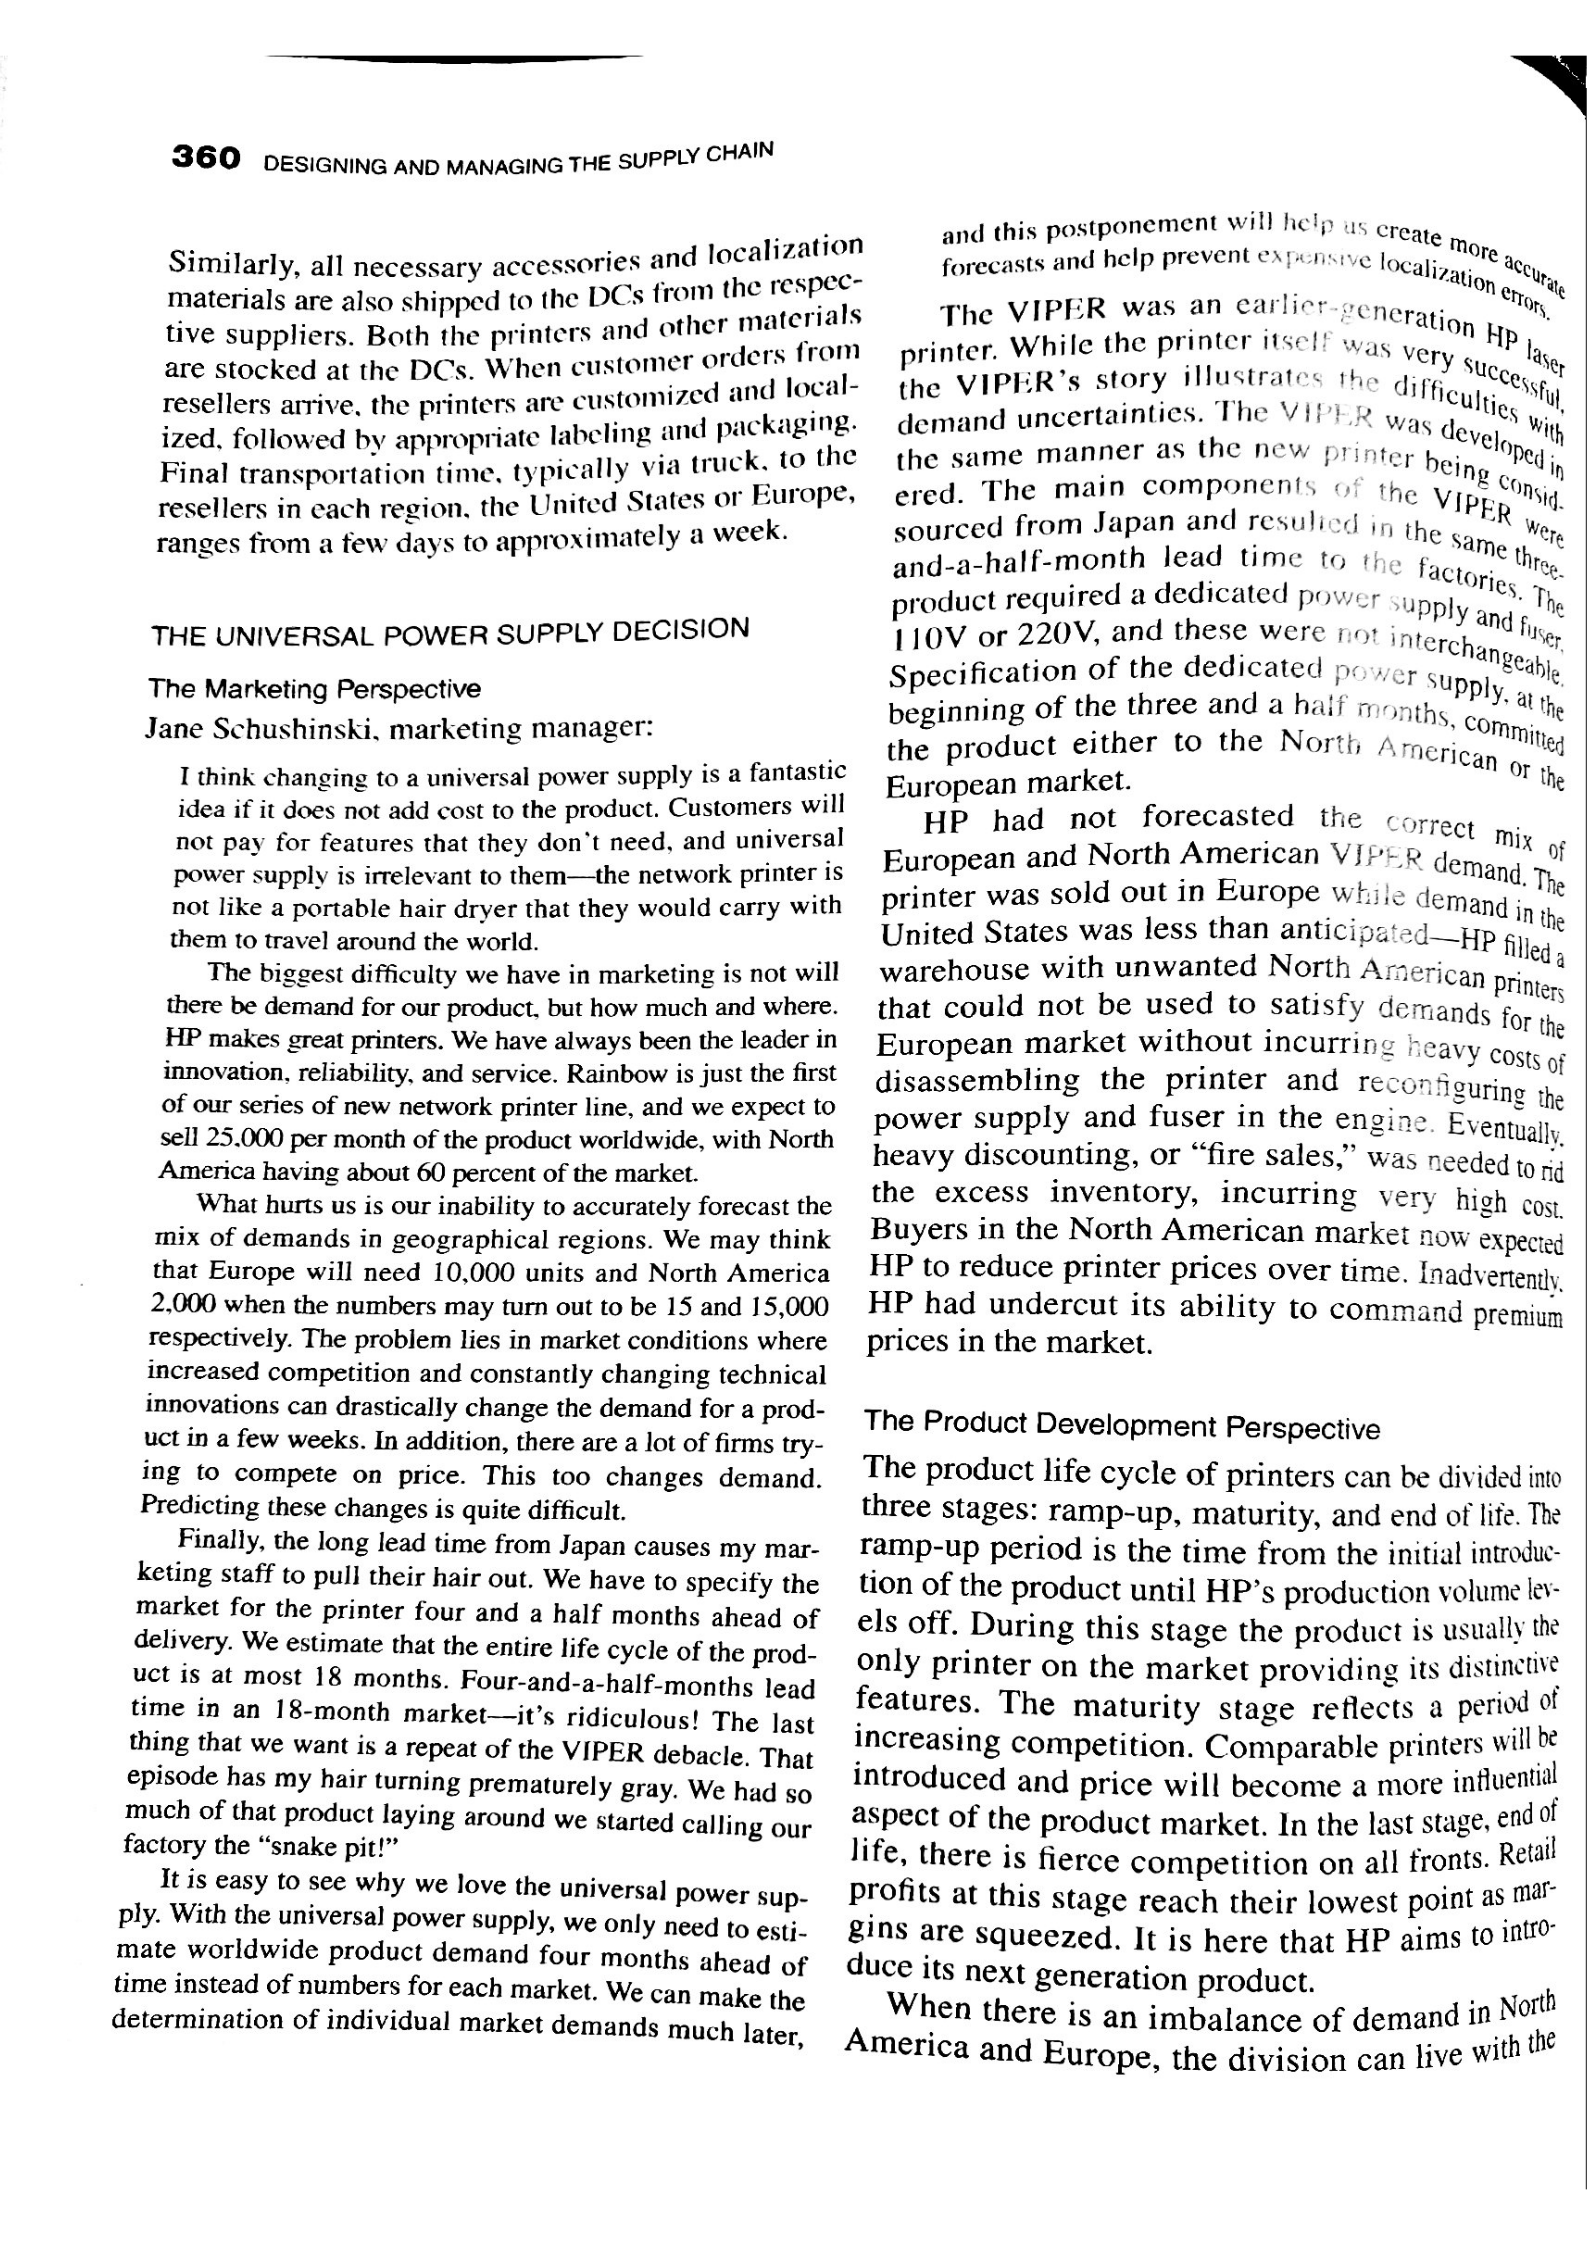
research refrences. I have attached the case study that this post is in reference to for
your refrence material in responding to this students post. .Here is what the students
original post was:
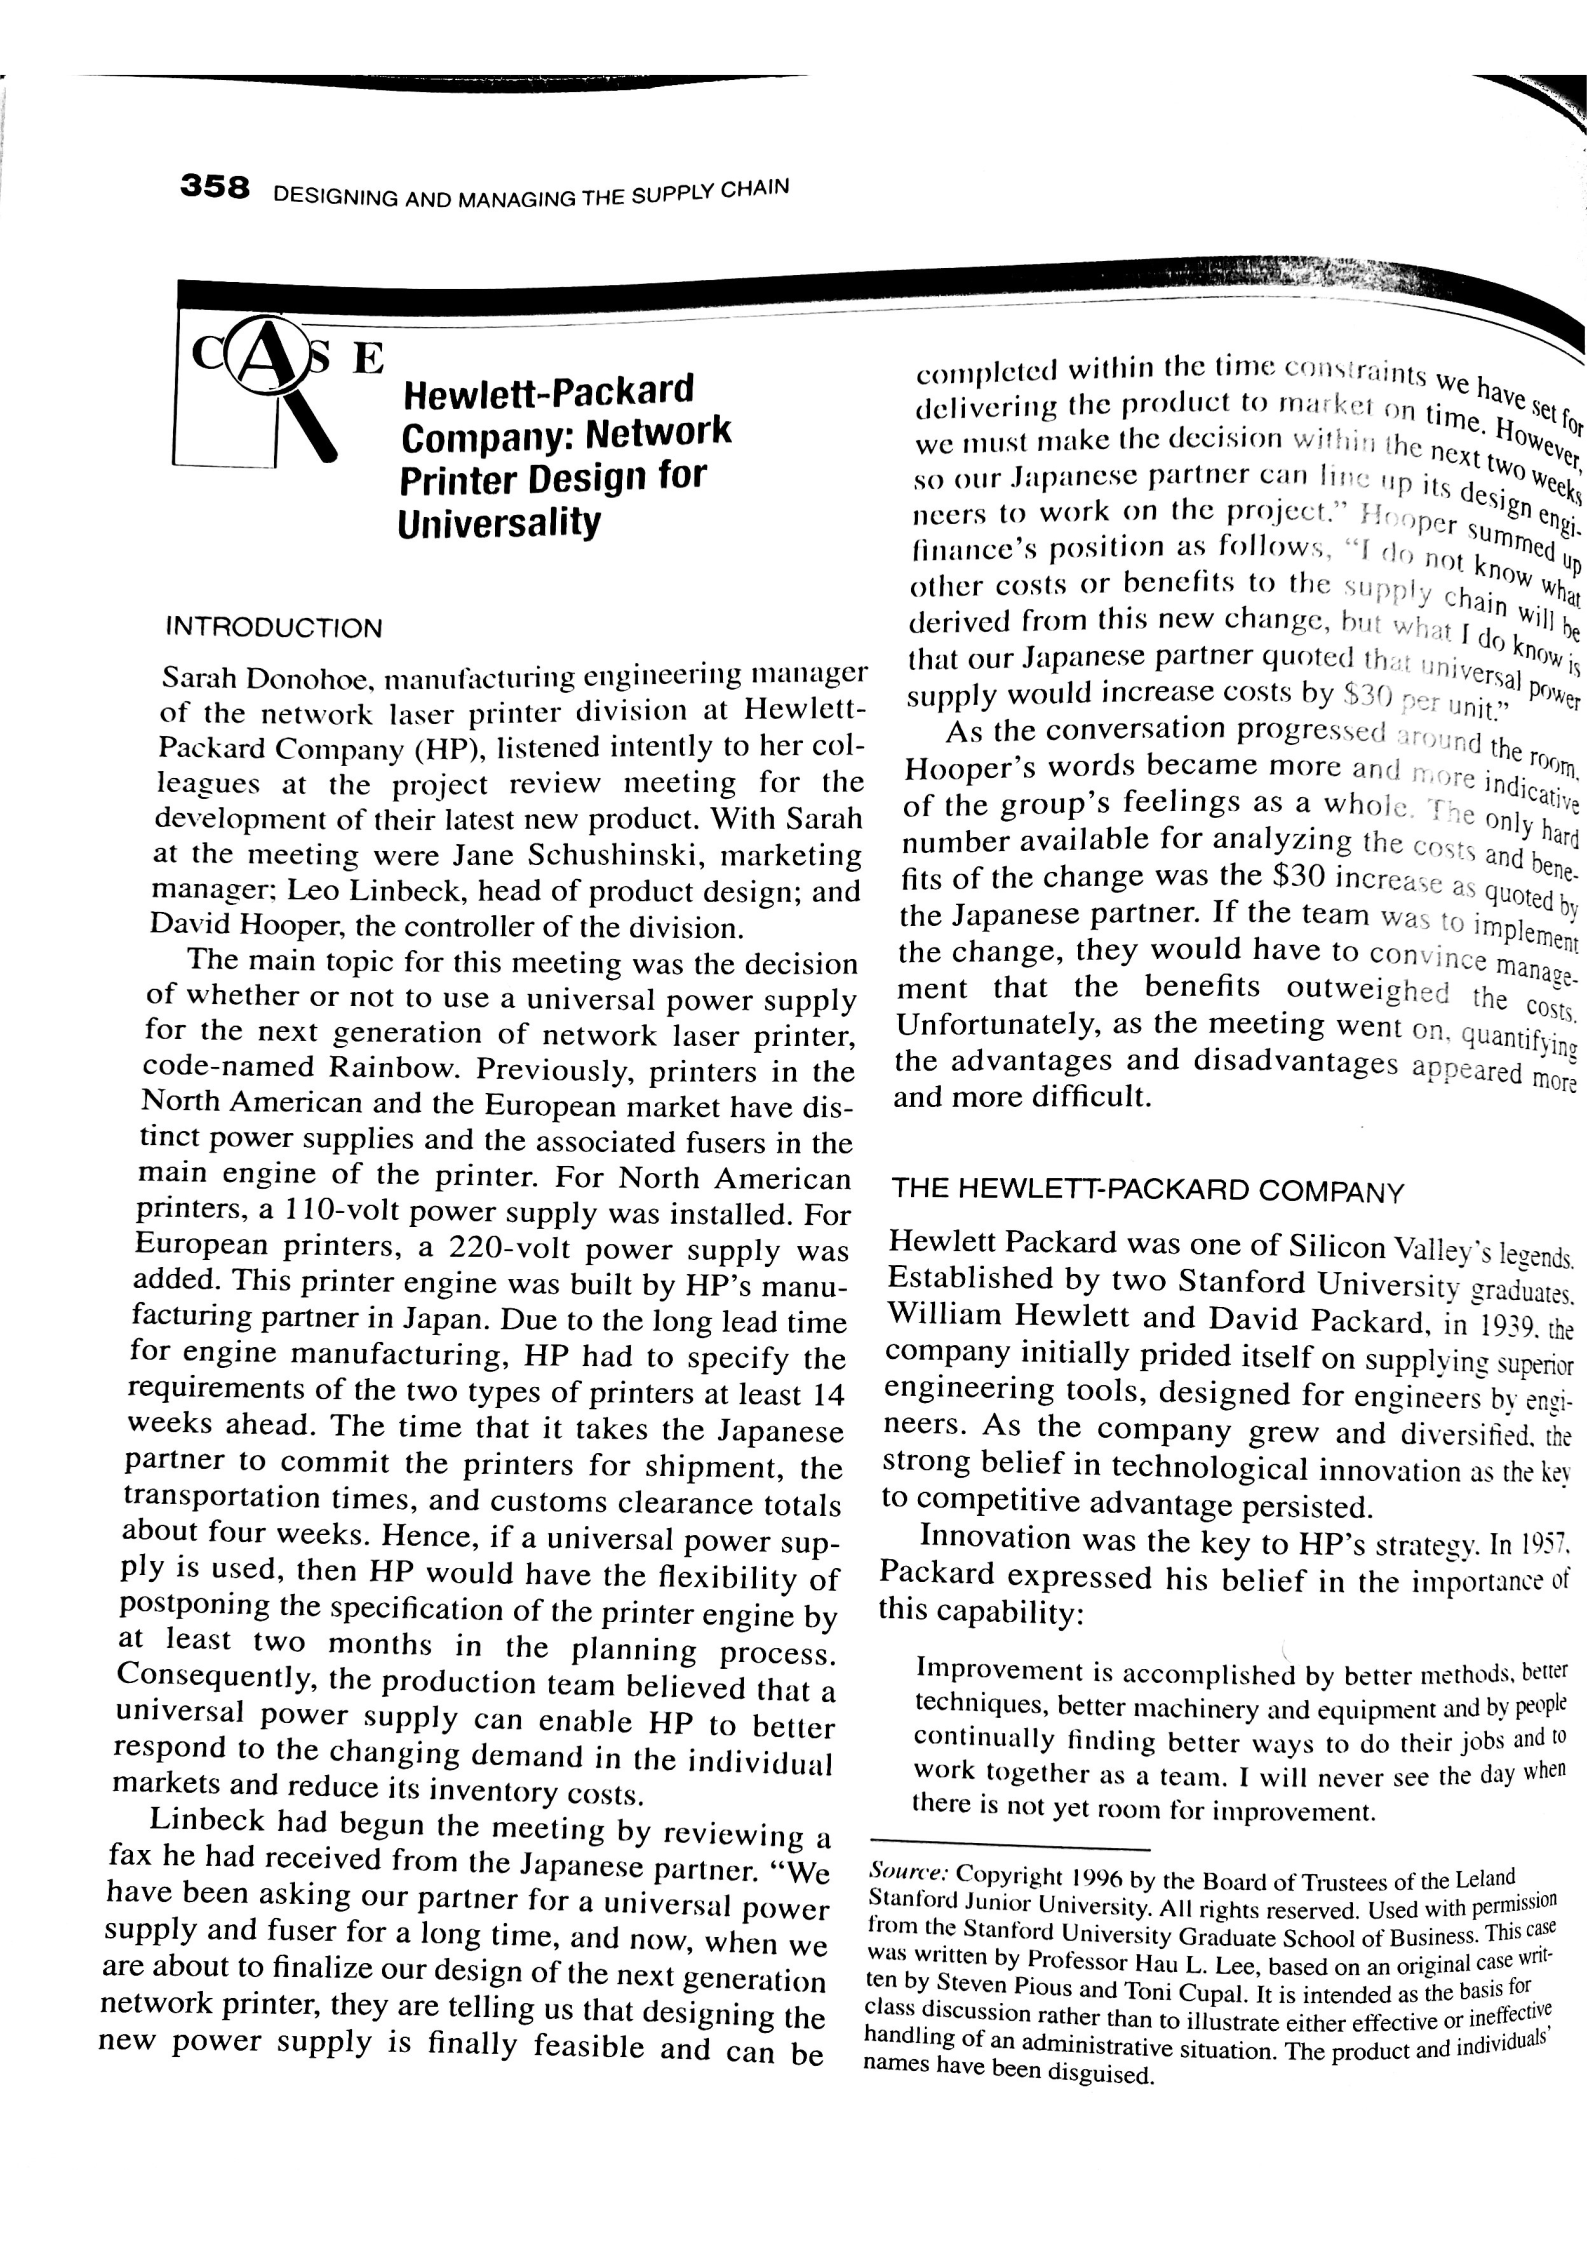
Sarah Donohoe, along with her colleagues, face a unique decision to implement a
universal power supply to the new HP printer, "Rainbow." At first look, the deciding
factor seems to be solely the increased price of manufacturing, but on a further,
detailed analysis many more factors arise.
Postponement Strategy
Currently, HP must provide forecasting for different geographical locations 14 weeks
before production is needed. If HP decides to use a universal power supply, they
eliminate the requirement to forecast separate markets. The move to a universal
power supply would also reduce lead times by two weeks since HP's Japanese
partners would no longer need those two weeks to make different components. This
postponement strategy would align with that of Luo and Zhang's research showing
"many advantages in implementing postponement strategy for manufactures" (Luo &
Zhang, 2018).
Costs and Benefits
The deciding factors for the decision to move to a universal power supply begins with
the cost. The make this change, HP will be required to pay $30 more per "Rainbow"
printer. This cost will need to be passed on to the consumer (of which price sensitivity
present concerns), or HP must take the $13.5 million reduction to their bottom line.
(Simchi-Levi, Kaminsky, & Simchi-Levi, 2008, p. 361) However, the deciding factor
goes well beyond cost. HP must take into consideration an increase in inventory
carrying and holding cost. There could also be an increased risk of stock out cost and
transhipping costs. On the contrary, however, HP could realize substantial benefits
from an operational standpoint as the additional two weeks provided to them would
provide a better chance at forecasting which could significantly reduce all costs
associated with the change to a universal power supply.
Effect on Product Life Cycle
The typical product life cycle for an HP product, specifically printers, is about 18
months (Simchi-Levi et al., 2008). As mentioned in the case study, a 14 week lead
time for a product with an 18 life cycle is "ridiculous!" (Simchi-Levi et al., 2008, p.
360). Never-the-less, HP is positioned to make such operational mountains move.
The universal power supply decision can significantly help in the ramp-up time, which
is the most crucial to establishing a market position before other entries in the

maturity cycle. (Simchi-Levi et al., 2008) This skill will also reap benefits at the end of
life by HP reducing the amount of stale inventory due to better forecasting.
HP Boise Improvements
The operations at the HP Boise factory integrate the power supply and fuser unit with
the printed circuit board. To minimize operational delays, HP should leverage air
shipment when a pending stock-out is expected. Where forecasting provides time,
and it should increasingly, HP should use the more cost-effective sea freight option.
Universal Power Supply Recommendation
HP should move to a universal power supply for the "Rainbow" printer as the benefits
outweigh the associated costs. Apart from the pros/cons analysis on this printer, this
decision will positively shift all future productions to a universal power supply having
an exponential return on the perceived "Rainbow" specific costs. HP could look at
this move as a longterm sunk cost. Santos concluded in his research that "even
moderately sized sunk costs of R&D can boost the gains" (Santos, 2017). This move
will change consumers expectations about the convenience HP provides as better
forecasting and inventory should allow HP to internally consume the increased cost
and not pass it on to consumers.
References
Simchi-Levi, D., Kaminsky, P., & Simchi-Levi, E. (2008). Designing and managing the
supply chain: Concepts, strategies and case studies (3rd ed.). New York, NY:
McGraw-Hill Irwin.
Luo, J., & Zhang, Q. (2018). Operations mechanism of postponement strategy for
service-oriented manufacturing. The International Journal of Advanced
Manufacturing Technology, doi:10.1007/s00170-018-3092-5
Santos, C. D. (2017), Sunk Costs of R&D, Trade and Productivity: The Moulds
Industry Case. Econ J, 127: 1626-1664. doi:10.1111/ecoj.12343
IN
358
DESIGNING
AND
MANAGING
THE
SUPPLY
CHA
Hewlett-Packard
Company:
Network
Printer
Design
for
Universality
INTRODUCTION
Sarah
Donohoe,
manutacturing
engineering
manager
of
the
network
laser
printer
division
at
Hewlett-
Packard
Company
(HP),
listened
intently
to
her
col-
leagues
at
the
project
review
meeting
for
the
development
of
their
latest
new
product.
With
Sarah
at
the
meeting
were
Jane
Schushinski,
marketing
manager;
Leo
Linbeck,
head
of
product
design;
and
David
Hooper,
the
controller
of
the
division.
The
main
topic
for
this
meeting
was
the
decision
of
whether
or
not
to
use
a
universal
power
supply
for
the
next
generation
of
network
laser
printer,
code-named
Rainbow.
Previously,
printers
in
the
North
American
and
the
European
market
have
dis-
tinct
power
supplies
and
the
associated
fusers
in
the
main
engine
of
the
printer.
For
North
American
printers,
a
110-volt
power
supply
was
installed.
For
European
printers,
a
220-volt
power
supply
was
added.
This
printer
engine
was
built
by
HP’s
manu-
facturing
partner
in
Japan.
Due
to
the
long
lead
time
for
engine
manufacturing,
HP
had
to
specify
the
requirements
of
the
two
types
of
printers
at
least
14
weeks
ahead.
The
time
that
it
takes
the
Japanese
partner
to
commit
the
printers
for
shipment,
the
transportation
times,
and
customs
clearance
totals
about
four
weeks.
Hence,
if
a
universal
power
sup-
ply
is
used,
then
HP
would
have
the
flexibility
of
postponing
the
specification
of
the
printer
engine
by
at
least
two
months
in
the
planning
process.
Consequently,
the
production
team
believed
that
a
universal
power
supply
can
enable
HP
to
better
respond
to
the
changing
demand
in
the
individual
markets
and
reduce
its
inventory
costs,
Linbeck
had
begun
the
meeting
by
reviewing
a
fax
he
had
received
from
the
Japanese
partner.
“We
have been
asking
our
partner
for
a
universal
power
supply
and
fuser
for
a
long
time,
and
now,
when
we
are
about
to
finalize
our
design
of
the
next
generation
network
printer,
they
are
telling
us
that
designing
the
new
power
supply
is
finally
feasible
and
can
be
completed
within
the
time
constraints
We
hay
delivering
the
product
to
market
on
tithe
i
Seti,
we
must
make
the
decision
withjs;
the
next
yO
so
our
Japanese
partner
can
line
up
jt,
des
Weey,
neers
to
work
on
the
project.”
Fy;
per
ni
Chg,
finance’s
position
as
follows,
“f
dq
not
kre
ed
‘
other
costs
or
benefits
to
the
supply
chai”.
ha
derived
from
this
new
change,
bit
what
|
.
il
be
that
our
Japanese
partner
quoted
th:;
;,;
nit
n
supply
would
increase
costs
by
$3)
ne;
es
As
the
conversation
progressed
3,,,;
Hooper’s
words
became
more
anc
more
j
of
the
group’s
feelings
as
a
whole.
f>,
-
number
available
for
analyzing
the
cos:<
and
h
fits
of
the
change
was
the
$30
increase
a.
quoted
the
Japanese
partner.
If
the
team
was
to
imple
the
change,
they
would
have
to
convince
manae
ment
that
the
benefits
outweighed
the
4
Unfortunately,
as
the
meeting
went
on.
quantify
ine
the
advantages
and
disadvantages
appeareg
mon
and
more
difficult.
Tt
THE
HEWLETT-PACKARD
COMPANY
Hewlett
Packard
was
one
of
Silicon
Valley's
legends,
Established
by
two
Stanford
University
graduates,
William
Hewlett
and
David
Packard,
in
1939.
the
company
initially
prided
itself
on
supplying
superior
engineering
tools,
designed
for
engineers
by
engi-
neers.
As
the
company
grew
and
diversified,
the
strong
belief
in
technological
innovation
as
the
key
to
competitive
advantage
persisted.
Innovation
was
the
key
to
HP’s
strategy.
In
1957,
Packard
expressed
his
belief
in
the
importance
of
this
capability:
Improvement
is
accomplished
by
better
methods,
better
techniques,
better
machinery
and
equipment
and
by
people
continually
finding
better
ways
to
do
their
jobs
and
t
work
together
as
a
team.
I
will
never
see
the
day
whet
there
is
not
yet
room
for
improvement.
———
Source:
Copyright
1996
by
the
Board
of
Trustees
of
the
Leland
sion
Stanford
Junior
University.
All
rights
reserved.
Used
with
permis
from
the
Stanford
University
Graduate
School
of
Business.
This
¢
Was
written
by
Professor
Hau
L.
Lee,
based
on
an
original
case
wae
ten
by
Steven
Pious
and
Toni
Cupal.
It
is
intended
as
the
basis
Tor
€
class
discussion
rather
than
to
illustrate
either
effective
or
ne
handling
of
an
administrative
situation.
The
product
and
individu
names
have
been
disguised.
wy
UCSIGNING
AND
MANAGING
ING
vw"
Hewlett-Packard
Company:
Network
Printer
Design
for
Universality
INTRODUCTION
Sarah
Donohoe,
manufactu
a
of
the
network
laser
printer
division
Packard
Company
(HP).
listened
intently
to
her
col-
leagues
at
the
project
review
meeting
for
the
development
of
their
latest
new
product.
With
Sarah
at
the
meeting
were
Jane
Schushinski,
marketing
manager:
Leo
Linbeck,
head
of
product
design;
and
David
Hooper,
the
controller
of
the
division.
The
main
topic
for
this
meeting
was
the
decision
of
whether
or
not
to
use
a
universal
power
supply
for
the
next
generation
of
network
laser
printer,
code-named
Rainbow.
Previously,
printers
in
the
North
American
and
the
European
market
have
dis-
tinct
power
supplies
and
the
associated
fusers
in
the
main
engine
of
the
printer.
For
North
American
printers,
a
110-volt
power
supply
was
installed.
For
European
printers,
a
220-volt
power
supply
was
added.
This
printer
engine
was
built
by
HP’s
manu-
facturing
partner
in
Japan.
Due
to
the
long
lead
time
for
engine
manufacturing,
HP
had
to
specify
the
requirements
of
the
two
types
of
printers
at
least
14
weeks
ahead.
The
time
that
it
takes
the
Japanese
partner
to
commit
the
printers
for
shipment,
the
transportation
times,
and
customs
clearance
totals
about
four
weeks.
Hence,
if
a
universal
power
sup-
ply
is
used,
then
HP
would
have
the
flexibility
of
postponing
the
specification
of
the
printer
engine
by
at
least
two months
in
the
planning
process.
Consequently,
the
production
team
believed
that
a
universal
power
supply
can
enable
HP
to
better
respond
to
the
changing
demand
in
the
individual
markets
and
reduce
its
inventory
costs.
Linbeck
had
begun
the
meeting
by
reviewing
a
fax
he
had
received
from
the
Japanese
partner.
“We
have been
asking
our
partner
for a
universal
power
supply
and
fuser
for a
Jong
time,
and
now,
when
we
are
about
to
finalize
our
design
of
the
next
generation
network
printer,
they
are
telling
us
that
designing
the
new
power
supply
is
finally
feasible
and
can
be
ring
engineering
manager
at
Hewlett-
ithin
the
time
constraints
we
4
,
leted
w
com
e
product
to
market
on
time.
itil
h
apne
Ae
the
decision
within
the
next
twonetth
so
our
Japanese
partner
can
dn
UD
its
design
tks
neers
to
work
on
the
project.
Hooper
sume
finance’s
position
as
follows,
“TI
do
nox
know
“tp
other
costs
oF
benefits
to
the
supply
chain
win
derived
from
this
new
change,
but
what
|
do
krone
S
partner
quoted
that
univercai
that
our
Japanese
supply
would
increase
costs
by
$30
per
u
As
the
conversation
progressed
around
the
7,
~
TOO)
s
words
became
more
and
more
indica
.
lVe
Hooper’
‘
of
the
group’s
feelings
as
a
whole.
Thi
only
hard
number
available
for
analyzing
the
costs
anq
Beng
fits
of
the
change
was
the
$30
increase
as
quoteg
by
the
Japanese
partner.
If
the
team
was
to
implement
the
change,
they
would
have
to
convince
manage.
ment
that
the
benefits
outweighed
the
cos,
Unfortunately,
as
the
meeting
went
on,
quantifying
the
advantages
and
disadvantages
appeared
more
and
more
difficult.
THE
HEWLETT-PACKARD
COMPANY
Hewlett
Packard
was
one
of
Silicon
Valley’s
legends.
Established
by
two
Stanford
University
graduates,
William
Hewlett
and
David
Packard,
in
1939,
the
company
initially
prided
itself
on
supplying
superior
engineering
tools,
designed
for
engineers
by
engt-
neers.
As
the
company
grew
and
diversified.
the
strong
belief in
technological
innovation
as
the
key
to
competitive
advantage
persisted.
Innovation
was
the
key
to
HP’s
strategy.
In
1957,
Packard
expressed
his
belief
in
the
importance
of
this
capability:
better
Improvement
is
accomplished
by
better
methods.
techniques,
better
machinery
and
equipment
and
by
people
continually
finding
better
ways
to
do
their
jobs
and
10
work
together
as
a
team.
I
will
never
see
the
day
whe?
there
is
not yet
room
for
improvement.
—_
So
urce:
Copyright
1996
by
the
Board
of
Trustees
of
the
Stanford
Junior
University,
All
rights
reserved.
Used
wit
from
the
Stanford
University
Graduate
School
of
Business.
Thi
was
written
by
Professor
Hau
L.
Lee,
based
on
an
original
case
WH
°
ea
oy
Steven
Pious
and
Toni
Cupal.
It
is
intended
as
the
basis
for,
‘
pan
discussion
rather
than
to
illustrate
either
effective
or
ineffective
andling
of
an
administrative
situation.
The
product
and
individuals
names
have
been
disguised,
Leland
h
permission
s
case
VY
i
rough
time,
HP’s
focus
on
innoy
ht
the
world
products
Such
as
the
hand-he}
von
ator
and
the
ink-jet
printer.
In
1992.
the
i
.
continued
to
invest
heavily
in
technology,
ing
$1.6
billion,
or
10
percent
of
revenue
=
hand
development.
The
high
levels
of
\
«
.
f
r
invest-
ave
paid
off:
For
three
straight
years,
over
h
ation
had
q
«spin
the
last
two
years.
wi
HANGING
MARKET
CONDITIONS
ait
early
1990s,
while
technological
innovation
vot
ued
to
drive
the
company’s
success,
many
busi-
es
units
were
being
forced
to
compete
on
other
gimensions.
In
consumer
product
lines,
low
Prices,
road
availability,
and
ease
of
use
had
become
com-
ritive
requirements.
Lew
Platt,
HP’s
current
presi-
gent
and
chief
executive
officer,
once
acknowledged
the
importance
of
improving
customer
service
and
esponsiveness:
We're
not
doing
as
good
a
job
in
order
fulfillment
as
we
need
to.
In
fact
it’s
where
we
get
our
lowest
marks
from
customers.
We
have
to
be
lot
easier
to
do
business
with.
Improvement
in
order
fulfillment
will
strengthen
HP’s
competitiveness,
increase
customer
satisfaction,
and
reduce
expenses,
so
this
is
an
area
of
great
urgency.
Along
with
improving
profitability,
it’s
our
top
priority.
In
addition,
product
life
cycles
were
continually
shrinking,
making
time
to
market
the
difference
between
maximizing
market
opportunities
and
miss-
ing
them.
Nowhere
were
these
demands
more
important
than
in
the
laser
printer
division.
HP
held
adominant
57
percent
of
the
worldwide
laser
printer
market,
but
several
formidable
competitors,
includ-
ing
Apple,
Fuji-Xerox,
Kyocera,
Oki,
and
Compaq,
had
recently
entered
the
market;
life
cycles
had
fallen
to
under
three
years;
and
the
quality
of
com-
Petitive
products
made
consumers
willing
to
switch
"ands
if
HP’s
price
was
too
far
above
the
market
Werage
or
if
the
product
was
not
easily
available.
To
meet
these
challenges,
HP
had
aggressively
Worked
to
improve
its
product
development
process.
‘0ss-functional
teams
that
brought
specialists
from
fie
Unctional
areas
together
to
create
a
new
prea
‘
"
becoming
standard.
The
primary
benefit
oO
ig
teams
was
their
ability
to
identify
and
eliminate
;atial
problems
early
in
the
design
cycle
while
nancial
and
time-to-market
costs
of
changin&
"
alf
P’s
orders
had
been
for
products
introduced
CHAPTER
AAG
COORDINATED
PRODUCT
AND
SUPPLY
CHAIN
DESIGN
349
the
pr
t
desi
i
ne
Product
design
were
low.
As
intended,
the
differ-
i
ee
meats
of
the
team
members
often
gave
rise
healed
debates
over
design
decisions,
THE
NETWORK
PRINTER
DIVISION
SUPPLY
CHAIN
The
laser
products
rapidly
rising
post
reve
AS
a
group
Constitute
a
major
and
:
ton
of
HP’s
revenue.
In
1992
the
revenue
of
laser
products
was
$3
billion,
but
was
pro-
jected
to
reach
close
to
$8
billion
by
1998.
The
net-
work
printer
is
a
high-end
laser
printer
that
has
networking
capabilities
and
special
functionalities.
Rainbow,
the
network
printer
under
development,
is
a
product
with
much
more
configurable
options
and
features
for the
printer,
such
as
memory,
stapling
abil-
ity,
firmware,
system
software,
fax
modems,
paper
handling,
linkage
to
print
server,
scanner,
and
printer
stand.
It
will
be
priced
between
$5,000
to
$6,000.
The
network
printer
division
at
HP
currently
out-
sources
the
procurement
and assembly
of
the
prod-
uct’s
main
engine
to
a
Japanese
partner.
The
components,
including
the
power
supply
and
fuser
unit,
were
fully
integrated
with
a
printed
circuit
board
from
HP’s
Boise
factory
into
the
printer
engine
at
the
partner’s
factory.
Monopoly
control
of
one
of
the
key
components
allowed
this
partner
to
require a
14-week
lead
time
from
HP.
The
design
team
of
Rainbow
recognized
that
the
multiple
thousands
of
configurable
options
for
the
new
product
would
be
a
nightmare
for
forecasting
and
production
planning.
Consequently,
special
efforts
were
spent
in
the
design
of
the
products
so
that
most
of
the
customization
of
the
products,
like
the
installation
of
paper
input
units,
cabinet
stands,
fax
modems,
paper
output
units,
stapler
upgrade
package,
memory,
and
print
server
linkage,
can
all
be
carried
out
at
the
distribution
centers
(DCs).
Hence,
all
these
options
can
be
installed
as
accessories
at
the
DCs.
In
addition,
the
localization
of
the
product
through
the
inclusion
of
driver
software
disks,
manu-
als,
power
cords,
and
front
panels
(with
the
correct
mix
of
languages)
are
also
done
at
the
DCs.
Hence,
the
supply
chain
process
involves
the
trans-
portation
of
the
base
printer,
almost
exclusively
by
boat,
from
the
partner’s
facility
to
HP
s
DCs
in
either
North
America
or
Europe.
The
shipment
process
lasted
one
month.
The
demand
for
a
network
printer
in
Asia
and
Latin
America
was
still
minimal
compared
with
the
demand
in
North
America
or
Europe.
HAIN
360
DESIGNING
AND
MANAGING
THE
SUPPLY
C
..
ac
7
salization
Similarly,
all
necessary
accessories
and
ee
renee
materials
are
also
shipped
to
the
DCs
trom
a
aterials
tive
suppliers.
Both
the
printers
and
other
mé
:
;
or
orders
from
‘
7s,
When
customer
0
resellers
arive.
the
pr
nized
and
local-
resellers
arrive,
the
printers
are
custon
A
aging.
ized,
followed
by
appropriate
labeling
and
pac
ag
a
Final
transportation
time,
typically
via
truck.
fe
te
resellers
in
each
region,
the
United
States
or
Europe,
ranges
from
a
few
days
to
approximately
a
week.
THE
UNIVERSAL
POWER
SUPPLY
DECISION
The
Marketing
Perspective
Jane
Schushinski,
marketing
manager:
I
think
changing
to
a
universal
power
supply
is
a
fantastic
idea
if
it
does
not
add
cost
to
the
product.
Customers
will
not
pay
for
features
that
they
don’t
need,
and
universal
power
supply
is
irrelevant
to
them—the
network
printer
is
not
like
a
portable
hair
dryer
that
they
would
carry
with
them
to
travel
around
the
world.
The
biggest
difficulty
we
have
in
marketing
is
not
will
there
be
demand
for
our
product,
but
how
much
and
where.
HP
makes
great
printers.
We
have
always
been
the
leader
in
innovation,
reliability,
and
service.
Rainbow
is
just
the
first
of
our
series
of
new
network
printer
line,
and
we
expect
to
sell
25.000
per
month
of
the
product
worldwide,
with
North
America
having
about
60
percent
of
the
market.
What
hurts
us
is
our
inability
to
accurately
forecast
the
mix
of
demands
in
geographical
regions.
We
may
think
that
Europe
will
need
10,000
units
and
North
America
2,000
when
the
numbers
may
turn
out
to
be
15
and
15,000
respectively.
The
problem
lies
in
market
conditions
where
increased
competition
and
constantly
changing
technical
innovations
can
drastically
change
the
demand
for
a
prod-
uct
in
a
few
weeks.
In
addition,
there
are
a
lot
of
firms
try-
ing
to
compete
on
price.
This
too
changes
demand.
Predicting
these
changes
is
quite
difficult.
Finally,
the
long
lead
time
from
Japan
causes
my
mar-
keting
staff
to
pull
their
hair
out.
We
have
to
specify
the
market
for
the
printer
four
and
a
half
months
ahead
of
delivery.
We
estimate
that
the
entire
life
cycle
of
the
prod-
uct
is
at
most
18
months.
Four-and-a-half-months
lead
time
in
an
18-month
market—it’s
ridiculous!
The
last
thing
that
we
want
is
a
repeat
of
the
VIPER
debacle.
That
episode
has
my
hair
turning
prematurely
gray.
We
had
so
much
of
that
product
laying
around
we
started
calling
our
factory
the
“snake
pit!”
It
is
easy
to
see
why
we
love
the
universal
power
sup-
ply.
With
the
universal
power
supply,
we
only
need
to
esti-
mate
worldwide
product
demand
four
months
ahead
of
time
instead
of
numbers
for
each
market.
We
can
make
the
determination
of
individual
market
demands
much
later,
and
this
postponement
will
help
us
create
mmo
forecasts
and
help
prevent
expansive
localiza’
7
The
VIPER
was
an
earlier
“eNeratign
ey
printer.
While
the
printer
its:
IF
was
very
«
the
VIPER’s
story
iNustrates
demand
uncertainties.
The
ViPipe
was
dein
the
same
manner
as
the
new
printer
being
ne
:
ered.
The
main
components
of
the
Vir
Sms
sourced
from
Japan
and
resuli
‘din
the
Sle
Wer
and-a-half-month
lead
time
to
the
Factorig,
"ee,
roduct
required
a
dedicated
power
“upply
im
te
110V
or
220V,
and
these
were
not
interchany
his
Specification
of
the
dedicated
pe
ver
supply
beginning
of
the
three
and
a
half
months.
conn
the
the
product
either
to
the
North
A
merican
ort
Ie
European
market.
HP
had
not
forecasted
the
correc
ty
European
and
North
American
VJP=R
demand
printer
was
sold
out
in
Europe
while
de
.
United
States
was
less
than
anticipated—yp
filed.
warehouse
with
unwanted
North
Americ
a
European
market
without
incurring
“AVY
costs
of
disassembling
the
printer
and
rec
figuring
the
power
supply
and
fuser
in
the
engine
Eventually,
heavy
discounting,
or
“fire
sales,”
was
needed
to
rid
the
excess
inventory,
incurring
very
high
cost,
Buyers
in
the
North
American
market
now
expected
HP
to
reduce
printer
prices
over
time.
Inadvertently,
HP
had
undercut
its
ability
to
command
premium
prices
in
the
market.
oO
The
Product
Development
Perspective
The
product
life
cycle
of
printers
can
be
divided
into
three
stages:
ramp-up,
maturity,
and
end
of
life.
The
ramp-up
period
is
the
time
from
the
initial
introduc-
tion
of
the
product
until
HP’s
production
volume
lev-
els
off.
During
this
stage
the
product
is
usually
the
only
printer
on
the
market
providing
its
distinctive
features.
The
maturity
stage
reflects
a
period
ol
increasing
competition.
Comparable
printers
will
be
introduced
and
price
will
become
a
more
influential
aspect
of
the
product
market.
In
the
last
stage,
end
of
life,
there
is
fierce
competition
on
all
fronts.
Retail
Profits
at
this
stage
reach
their
lowest
point
as
ma
gins
are
squeezed.
It
is
here
that
HP
aims
to
int
duce
its
next
generation
product.
h
When
there
is
an
imbalance
of
demand
in
Ne
America
and
Europe,
the
division
can
live
with!
CH
APTER
11;
COORDINATED
PRODUCT
AND
SUPPLY
CHAIN
DESIGN
364
ence
of
having
excess
inventory
in
one
¢
ant
and
shortages
in
another,
or
ship
the
in
onsed™
con-
ne
continent
to
another
(an
operation
known
rransshipment
),
where
the
printer
is
recontig-
as
gand
sold.
.
we
ce
the
end-of-life-stage,
in
addition
to
transship-
‘
roducts
across
the
continent
to
correct
for
pa
of
the
imbalances,
the
division
can
also
dis-
some
the
product
to
create
demand,
dismantle
the
cou
ct
and
sell
the
parts
to HP's
service
division
in
aeeville.
OF
just
write
the
product
off.
-
Linbeck’s
office
was
Stacked
high
with
what
aust
have
represented
every
available
trade
journal
“
ed
to
printing
technology.
From
behind
his
HP
M
rkstation.
he
explained
his
point
of
view
regarding
the
yniversal
power
supply:
while
Jane
gains
“responsiveness,”
I’m
Staring
at
a
$30-
_ynit
cost
increase.
With
the
pressure
to
lower
material
costs.
the
design
team
would
find
it
hard
to
justify
this
seemingly
unnecessary
increase
in
material
cost.
Although
the
printer
engine
costs
about
$1,000
each,
so
that
$30
may
not
seem
that
much,
every
single
dollar
increase
in
material
cost
is
a
decrease
of
a
dollar
in
our
profit.
That
is
why
our
design
group
is
getting
so
much
heat
to
get
the
material
cost
down.
My
concern
is
that
we
have
no
way
to
reliably
predict
how
much
value
the
so-called
benefits
of
universal
power
supply
truly
represent.
Now,
I’m
the
first
to
admit
that
’m
no
marketing
expert,
but
it’s
pretty
clear
to
me
that
if
we
could
just
learn
to
forecast
demand
better,
this
universal
supply
would
literally
be
a
worthless
idea.
Maybe
pumping
$30
per
unit
into
improving
the
forecasting
process
makes
more
sense
than
sending
it
out
the
door
in
a
cardboard
box.
At
least
in
the
first
case
we
have
some
hope
of
recov-
ering
it
again.
I
do
agree
with
Jane’s
point
regarding
the
benefits
late
in
the
product
life
cycle.
Currently,
reconfiguring
the
prod-
uct
with
a
different
power
supply
is
a
real
pain.
We
have
to
purchase
new
power
supplies
rated
at
the
correct
voltage,
ship
the
printers
across
the
Atlantic
from
the
undersold
region,
swap
the
power
supply,
change
the
fuser
electronic
circuit
and
the
fuser
bulb,
and,
finally,
distribute
the
prod-
uct
to
retailers.
The
old
power
supplies
have
to
be
dis-
posed
of.
To
make
matters
worse,
there
are
all
kinds
of
Tegulatory
issues
that
surface.
A
universal
power
supply
eliminates
all
rework
that
is
now
required,
but
whether
the
gains
it
provides
outweigh
the
increase
in
materials
cost
Temains
unclear.
Whichever
way
we
end
up
going,
one
thing
is
certain.
We
cannot
delay
our
development
schedule
in
order
to
make
this
decision.
We
need
to
decide
on
a
strategy
quickly
and
GO!
As
early
as
1991,
in
order
to
improve
their
cost
Position
and
speed
up
time
to
market,
the
printer
divisions
in
Boise
had
implemented
two
new
product
development
metrics.
First,
they
had
instituted
cost
reduction
goals
for
each
new
generation
of
printer.
The
costs
captured
in
this
measure
included
labor,
material,
and
manufacturing
overhead.
The
second
metric,
called
break-even
time
(BET),
had
been
man-
dated
by
upper
management.
It
measured
the
time
from
project
initiation
to
break
even,
defined
as
the
point
where
total
discounted
cash
outflow
equaled
total
discounted
cash
inflow.
The
Finance
Perspective
Neatly
arranged
on
David
Hooper’s
desk
were
the
lat-
est
sets
of
pro-forma
income
statements
and
balance
sheets
for
the
new
project.
Pointing
out
the
effect
of
the
universal
power
supply
on
income,
he
noted,
If
we
incorporate
the
universal
power
supply
and
sell
450,000
units
of
Rainbow,
it
will
cost
us
approximately
$13.5
million
in
additional
material
costs.
If
we
are
not
able
to
pass
this
increase
along
to
the
customer,
or
at
least
our
retailers,
that
comes
straight
out
of
our
bottom
line.
I
sure
agree
that
there
will
be
benefits
from
universal
power
supply.
May
be
we
should
take
a
hard
look
at
the
costs
of
stockouts
and
inventory.
Demand
fluctuates
during
each
of
the
three
life-cycle
periods
and
so
do
the
costs
of
making
or
missing
a
sale.
We
typically
estimate
that
for
each
lost sale
we
actually
forgo
multiple
times
our
profit
margin.
The
reason
for
this
is
that
if
a
customer
buys
a
competitive
brand
due
to
our
inability
to
keep
the
resellers
on
stock,
there
is
a
chance
that
he
will
stay
with
that
brand
when
he
purchases
a
printer
in
the
future.
This
effect
might
cover
three
or
four
generations
of
printers.
Moreover,
we
may
lose
the
profits
from
the
sales
of
consumables
such
as
toner
cartridges
and
perhaps
even
other
HP
peripheral
products.
The
cost
of
stockouts
when
the
product
is
first
intro-
duced
into
the
market
is
even
higher,
as
the
potential
word-of-mouth
and
publicity
effects
can
damage
the
future
sales
and
ultimate
success
of
the
product.
On
the
other
hand,
the
cost
of
stockouts
at
the
end-of-life
stage
is
probably
considerably
lower,
as
there
is
less
fear
of
adverse
effect
on
future
sales,
and
the
resellers
might
in
some
cases
steer
the
customer
to
wait
for
the
new,
incom-
ing,
replacement
product.
Although
the
cost
of
stockouts
in
the
ramp-up
stage
is
the
highest,
it
is
also
this
stage
when
we
know
the
least
about
the
market
response
to
our
new
product,
and
our
forecast
errors
are
usually
much
greater.
I
understand
that
Sara’s
material
planning
people
had
done
some
homework
and
found
that
the
standard
deviation
of
our
~
=
SUPPLY
CHAIN
362
DESIGNING
AND
MANAGING
TH
4
AOU
of
forecast
accu
)
was
close
to
h
mar
monthly
forecast
error
(a
new
He
racy
that
the
group
has
started
(o
ear
ol
40
percent
of
the
average
monthly
de
Tel?
nce
kets
in
the
mature and
end-of-life
ere
iM
aoa56
tion
is
that
the
corresponding
peree
to
moniter
is
inv
stimated
that
our
ly
30
percent,
t
of
capital.
percent
inthe
ramp-up
sage.
ane
The
other
major
cost
that
T
have
‘
tory.
My
financial
analysts
have
©
_
annual
holding
cost
rate
is
approxima
a
which
covers
warehousing.
insurance,
COS
and
shrinkage.
The
Manufacturing
Perspective
anagét
z
ii
ring
mé
>
Sara
Donohoe,
manufacturing
engineering
commented,
eat
idea.
This
pond
to
orders
in
of
delaying
months.
I
think
the
universal
power
supply
is
a
gr
innovation
will
improve
our
flexibility
to
res|
in
two
key
ways.
The
first
is
the
obvious
ga
the
regional
allocation
decision
by
two
and
a
half
mo
I'm
sire
marketing
has
expounded
on
this
ad
infinitum.
The
second
gain
is
more
subtle.
You
see,
while
transship-
ment
has
always
been
possible
in
theory,
we
have
avoided
it
whenever
possible.
Let
me
explain.
.
At
the
ramp-up
stage,
we
always
try
to
stockpile
our
DC’s
with
loads
of
printers
so
that
we
don’t
ever
run
out
of
stock,
and,
given
the
high
cost
of
shortage
at
this
stage,
this
seems
reasonable.
There
is
not
much
of
a
need
for
transshipment.
In
the
mature
phase,
if
we
keep
doing
what
everyone
at
HP
does
and
keep
enough
safety
stock
to
meet
the
standard
service
target
of
around
98
percent
then
again,
the
chance
of
our
needing
transshipment
is
still
small.
However,
I
am
not
sure
if
we
want
to
keep
having
98
percent
service
goals
at
the
end-of-life
stage,
and
indeed
that
is
when
transshipments
will
be
most
needed.
The
whole
idea
behind
transshipment
is
to
adjust
inventories
in
response
to
market
demand.
To
do
this
effectively,
you
need
to
move
the
product
quickly.
Unfortunately,
to
send
a
printer
by
air
across
the
Atlantic
costs
us
$75.
Sea
shipment
reduces
costs
significantly
to
approximately
$15/unit,
but
a
month
out
on
the
ocean
does
not
do
much
for
responsiveness,
which
is
exactly
what
you're
trying
to
achieve!
In
addition
to
the
transportation
cost,
we
know
how
tedious
and
complex
it
is
to
reconfig-
ure
the
power
supply
and
fuser.
I
would
put
my
conserva-
tive
estimate
of
the
activity-based
cost
for
reconfiguration
to
be
at
least
$250
per
printer.
As
you
might
imagine,
the
quality
people
go
nuts
when
they
find
out
we’re
doing
this.
How
can
you
establish
a
controlled
Process
if
you
only
do
something
once
a
year?
Even
worse,
since
the
rework
involves
electrical
compo-
nents,
safety
standards
require
the
reconfiguration
process
to
be
certified
by
Underwriter’s
Laboratory.
If
you’ve
ever
Werealize
|
\
dealt
with
UL,
you'll
realize
how
much
or
{ting
a
process
like
this
approved,
yoy
re
.
.
The
universal
powe!
supply
would
allo
Mt
this
mess,
making
transshipment
a
distings
U4
iguration
i
10
WSsihe
a
cost
of
reconfiguranion
1s
almost
“00.
Hig
r
sii
‘y
;
*
sure
wu
Sat
Jo,
y
bility,
although
Pm
not
sur
ke
Wolild
a
ei
shi
fei
ay
‘
decide
when
to
ship...
our
friends
in
digg
ing
-
My
only
real
concern
with
«lk
veloping
1
it
supply
is
the
potential
power
play
that
could
Bi
time
of
allocation
of
the
production
buita
et
regions.
Again,
I
would
like
sorq
visibiti
ony
s
over
how
many
units
Pcan
count
on
receiving
i
ty
The
Distribution
Perspective
Rob
Seigel
runs
the
North
America
distribu
ter,
Rob
worked
in
a
variety
of
posit;
19N
«,
moved
to
management
and
his
present
posit
2
Given
a
universal
product,
transshipment
won't
problem
for
the
DC;
it’s
just
another
shi
can
easily
“localize”
the
produci
by
ha
plug
adapters
at
the
DC.
Personal!
ys
however,
|
feet
like”
great
way
to
chew
up
company
profits.
T
can
just
Sea
ing
1,000
units
to
Germany
in
February
only
to
ha
ship
another
1,000
back
to
me
in
Ma
seem
to
make
sense
at
the
time
the
decision
was
made.
py
the
end
the
company’s
out
hundreds
of
thousands
of
dol
Who
is
going
to
make
the
decision
to
shift
inventor
from
DC
to
DC?
I
can
see a
real
firetight
if
one
pc
wig
more
but
the
other
is
unwilling
to
give
up
its
excess,
Wea
have
pressures
for
high
customer
service
and
even
if]
have
some
excesses
now,
that
does
not
mean
that
|
Mav
ay;
need
it
next
month.
Sending
the
product
to
Europe
helps
their
performance,
but
what
about
mine?
I
hope
I
do
a:
have
to
do
it!
One
thing
I
don’t
have
time
for
is
spen
half
of
my
day
on
the
phone
to
Germany
trying
to
negotiate
a
transfer.
I
guess,
though,
if
we
can
avoid
what
happened
with
te
VIPER
we
have
got
to
be
better
off.
That
was
an
interestag
time.
See
that
warehouse,
pretty
big.
It
was
so
full
we
stopped
leaving
the
aisles
clear
and
just
stacked
prinen
solid,
from
floor
to
ceiling,
all
the
way
from
front
to
back
would
pay
money
to
prevent
that
from
happening
again
All
other
work
grinds
to
a
halt
when
a
crisis
like
that
emer
Us
ng
VE
them
h.
Both
actions
».,
S
ma
THE
DECISION
The
team
had
decision-making
authority,
but
the}
would
have
to
defend
their
decision
to
uppet
Te
agement.
From
past
experience,
they
knew
i
they
decided
to
adopt
the
universal
power
Sup?
management
would
want
to
ensure
they
had
perfor
adequate
analyses
of
all
the
costs
and
benefits
of
CHAPTER
11:
COORDINATED
PRODUCT
AND
SUPPLY
CHAIN
DESIGN
363
as
well
as
some
estimate
of
the
risks
a
:
.
2.
W
benefits
of
a
universal
addition,
some
consideration
of
how
the
hat
are
the
costs
and
ecision
ad
d.
In
‘gol
VE
‘
:
ower
supply
(feel
free
to
make
assumptions)?
ipo
act
futu
Pp
pply
1
gecision
ae
made
re
generations
of
products
3.
How
would
such
costs
and
benefits
be
different
ii)
have
£0
,
over
the
product
life
cycle?
4.
Besides
deciding
on
a
universal
power
supply,
Se
DISCUSSION
QUESTIONS
what
other
operational
improvements
can
you
cA
suggest
to
HP
Boise?
5.
What
would
be
your
recommendations
about
the
adoption
of
a
universal
power
supply?
a
what
Way
is
a
universal
power
supply
a
post-
.
ponement
strategy?

Universal power supply Outline
I. Postponement Strategy
II. Costs and Benefits
III. Effect on product life cycle
IV. Operational improvements for HP Boise
V. Recommendations on the adoption of the universal power supply

Running head: UNIVERSAL POWER SUPPLY RESPONSE 1
Universal Power Supply Response
Institution Affiliation
Date

UNIVERSAL POWER SUPPLY RESPONSE 2
Postponement Strategy
A postponement strategy allows for deliberate delays on final manufacturing activities
until customers confirm their orders. I agree that HP's universal power supply would reduce lead
times and scrap the need for long periods of forecasting. The existing printer’s function on either
a 110V or a 220V power supply systems, which fit in printers for respective regions. Due to the
current lead times in Japan, these two power supply systems would need specifications four and
a half months ahead of delivery. The ever-changing market demands of these two products in
their respective regions makes it difficult for the creation of accurate specifications. The
universal power supply would erase the need for constant adjustments that currently exist in the
two power supply systems. Therefore, the universal power supply system will provide for the
delayed manufacture of the products until the creation of accurate forecasts (Saghiri & Barnes,
2016).
Costs and Benefits
The universal power supply system has to exhibit more advantages than disadvantages. I,
therefore, agree that a decision for implementation is dependent on the weighing of the pros and
cons. The universal would require an additional cost of $30 for each unit produced. These
additional costs will make a higher impact in the end as HP would exhibit reduced profits. To
counter profit loss, the additional costs of the printers would increase the overall price of the
product to the consumer. Although the universal power supply system benefits manufacturing, it
is of no use for the consumers. They may view the price increase as unnecessary and switch to
other, more affordable brands. However, the power supply modification will increase the
flexibility of the manufacturing and transshipment teams.

UNIVERSAL POWER SUPPLY RESPONSE 3
Effect on product life cycle
I agree that the implementation of the universal power supply system will help reduce the
accumulation of unneeded stock due to production under inaccurate forecasts. A uniform power
supply system will ease the transshipment process in case of imbalanced demand in the different
regions. Transshipment occurs typically in the maturity stage of the product lifecycle when one
region's market goes higher than another does. The universal power supply will eliminate the
current costs of reassembly and regulatory issues. However, the increased cost per unit will result
in higher prices of the raw materials needed to manufacture the product (Simchi-Levi, Kaminsky
& Simchi-Levi, 2008).
Operational improvements for HP Boise
Shipping periods often add to the operational delays due to the use of a sea freight option
when there is limited time available. I, therefore, agree that considering air shipment strategies
would hinder these operational delays. Also, I would suggest that HP improve its demand
forecasts to provide adequate time for Japan to make necessary adjustments to the existing power
supply systems. Accurate estimates would further erase the need for excessive stockpiles during
the ramp-up stage in the product's life cycle (Kochak & Sharma, 2015). Aligning manufacturing
with demand will also avoid unnecessary transshipments sue to balanced distributions in the
different regions.
Recommendations on the adoption of the universal power supply
I also believe that the approval of the universal power supply system would provide HP
with the most benefits. The VIPER crisis, which involved the accumulation of printers that were

UNIVERSAL POWER SUPPLY RESPONSE 4
on low demand in particular regions. The main issue with the VIPER crisis was how these
printers were not transferrable to other distribution centers. By adopting the universal power
supply, HP would allow different distribution centers to share inventory to manage the changing
consumer demand (Kochak & Sharma, 2015). I further agree that allowing a long-term sunk cost
would provide maximum consumer satisfaction as the increased costs would not affect them.

UNIVERSAL POWER SUPPLY RESPONSE 5
References
Kochak, A., & Sharma, S. (2015). Demand forecasting using neural network for supply chain
management. International journal of mechanical engineering and robotics
research, 4(1), 96-104.
Saghiri, S. S., & Barnes, S. J. (2016). Supplier flexibility and postponement implementation: an
empirical analysis. International Journal of Production Economics, 173, 170-183.
Simchi-Levi, D., Kaminsky, P., & Simchi-Levi, E. (2008). Designing and managing the supply
chain: Concepts, strategies and case studies (3rd ed.). New York, NY: McGraw-Hill
Irwin.

