


Please write a response with 3 resources to this students original discussion board port. This student
was answering questions at the end of a case study. I have attached the original case study as
reference. Here is what the student posted:
Introduction
Meditech is a company that manufactures endoscopic surgical instruments at a low cost mostly to
hospitals and independent surgeons. The distribution and management are accomplished from a central
storage warehouse that ships these products to domestic and international partners. The organization,
however, has been experiencing concerns that have stemmed from the duration taken to deliver the
products. As the nature of the surgeries requires time management, the equipment must be delivered on
time to perform these surgeries making this the main problem the firm is battling. The approximate
waiting time for Meditech customers is over six weeks. This discussion will address some ways that can
be used to resolve this issue.
1. What are Meditech’s problems in introducing new products? In manufacturing ALL
products?
On average, the company produces one new product every month, which are upgrades of the old
products reducing the life cycle of the product. Each time a new product is launched, the problems
experienced with the old ones are not addressed (Simchi-Levi, Kaminsky, & Simchi-Levi, 2008). There
has to be a lead time that Meditech gives to allow these products to be diffused into the market.
Constantly launching a new product has led to problems such as supply shortages, low customer
satisfaction, inaccurate forecasting, delay in deliveries high Finished Goods (FG) inventory levels.
Meditech has over 200 end – products in their portfolio and working using a scalar chain it makes
information dissemination difficult and communication breakdown is often experienced (Simchi-Levi, et
al., 2008). Meditech also depend on suppliers for the wide range of product supply and with a waiting
period of two – six weeks, it makes it increasingly difficult to constantly supply end products needed on
time. Lack of communication between the departments is another factor that is causing delivery issues.
All departments are supposed to be clear on what products have been ordered and the number that
needs to be supplied to consumers. Communication breakdown is an issue that must be avoided at all
costs as it causes double or triple orders for Meditech (Armbruster, Göttlich, & Herty, 2011).
1. What is driving these problems, both systemically and organizationally?
There are several systematic and organizational issues that are driving the problems that Meditech is
facing. The first problem is panic orders also referred to as bullwhip. This is caused by inadequate
demand forecasting, long assembly lead time and also the constant introduction and launching of new
products, making the inventory level insufficient to supply to consumers (Wang, & Disney, 2016). As the
organization works to keep up with the demand, the resources are becoming increasingly exhausted
every time a new product is launched. Another factor driving these problems is duplicate orders and
redundant orders. Some of the products that are not very popular or necessary are produced in high
numbers leaving products that are actually needed will little to no time in production. Forecasting of the
demand is a factor that leads to poor demand or overproduction, the organization needs to pay attention
to the products that are ordered and the duration it takes to have the end product delivered (Wang, &
Disney, 2016). Looking at data for forecasting can be an asset if used correctly, as seen in this case,
even when the initial demand decreases, there is still a backlog of high demand inventory that still needs
to be produced and this effect is made worse by the launch of each new product, creating poor
customer service.

1. Why is the customer service manager the first person to recognize the major issues?
Meditech is an organization that uses a scalar chain of management which uses a chain of command
that hinders the flow of information, more often than not especially if there is communication breakdown
between departments. Through this chain, the customer a representative will make the customer service
manager know about the complaints, who will, in turn, take the complaints higher up the chain, this
could have been very useful to the company as the representatives work directly with the consumers
and hear about the issues first hand. (Armbruster et al., 2011). Mr. Dan Franklin held many meetings
with the hospital managers and thus arose the issue of customer dissatisfaction, poor service and delay
in delivery.
1. How would you fix the problems?
Some of the suggestion in resolving Meditech’s problems is investing in a data storage system that can
be accessed by all employees. This will reduce the stress of wondering what products were ordered and
how many need to be delivered (Tenhunen, & Harjuniemi, 2013). It is important to keep track of the
products and the data system will also indicate the products that are moving slowly and ones that do not
need to be reproduced. Another solution would be to create a method of communication that will be
adhered to especially on complaints and have a department that handles these issues (Chopra, &
Sodhi, 2004). This will enable the organization to sort out the issues that are pressing and investigate to
see if there is a pattern emerging to resolve the problem with the customer dissatisfaction. Forecasting
is a third solution to the problems that Meditech are facing, when there is a good system of data
collection and implementation in place, the timeline can be seen easily and the duration of production
and delivery reduced from the current six weeks to possibly two or three weeks at the most (Simchi-
Levi, et al., 2008).
Forecasting and data collection will also enable the organization to have products in stock that will be
used as a buffer for consumers that have either large or small orders because when consumers receive
a product, they can continue with their business as they wait to the remaining products. Finally, looking
for a supplier that can handle the demand that the company has will reduce the current lead time of 2 –
6 weeks by possibly half, as the demand increases, the supplier should increase in the production as
well, reducing the break in the supply chain (Chopra, & Sodhi, 2004). However, if this does not resolve
the problems, then reducing the number of items launched each month should be a good place to start.
If the company must produce an item, give the market the opportunity to work with the previous one and
listen to suggestions by consumers on what the new product should contain.
References
Armbruster, D., Göttlich, S., & Herty, M. (2011). A scalar conservation law with discontinuous
flux for supply chains with finite buffers. SIAM Journal on Applied Mathematics, 71(4), 1070-18.
Chopra, S., & Sodhi, M. S. (2004). Managing risk to avoid supply-chain breakdown. MIT Sloan
Management Review, 46(1), 53.
Simchi-Levi, D., Kaminsky, P., & Simchi-Levi, E. (2008). Designing and managing the supply
chain: Concepts, strategies and case studies (3rd ed.). New York, NY: Richard D. Irwin, Inc.
Tenhunen, V., & Harjuniemi, M. (2013). Data storage architecture to support various research
needs and data lifecycle management. EUNIS 2013 Congress Proceedings: 2013: ICT Role for Next
Generation Universities, 1(1)

Wang, X., & Disney, S. M. (2016). The bullwhip effect: Progress, trends, and directions.
European Journal of Operational Research, 250(3), 691-701.
18
DESIGNING AND MANAGING THE SUPPLY CHAIN
8.
Consider a firm selecting a supplier of transportation services? What are the
advantages to using a truckload carrier? A package delivery firm such as UPS?
9.
What are the advantages to a firm of high inventory levels? What are the disad-
vantages? What are the advantages of low inventory levels? The disadvantages?
10.
What are some ways that redundancy can be built into a supply chain? What are
the advantages and disadvantages of building redundancy into the supply chain?
11.
Consider Figure 1-5. What are the reasons for the increase in transportation costs?
Inventory costs? Does one affect the other? How?
Meditech Surgical
Three years after Meditech was spun off from its
parent company, Meditech captured a majority of the
endoscopic surgical instrument market. Its primary
competitor, National Medical Corporation, had prac-
tically invented the $800 million market just over a
decade ago. But Meditech competed aggressively,
developing new, innovative instruments and selling
them through a first-class sales force. The com-
bination paid off, and Meditech had become a phe-
nomenal success in a short period of time. Despite
the success, Dan Franklin, manager of Customer
Service and Distribution, was concerned about
growing customer dissatisfaction. Meditech had
recently introduced several new products that were
central to the entire Meditech product line. New
product introductions, which were critical to
Meditech's strategy of rapid product development,
needed to be introduced flawlessly to protect
Meditech's reputation and sales of other products. But
Meditech consistently failed to keep up with demand
during the flood of initial orders. Production capacity
became strained as customers waited over six weeks
to have their orders delivered. Poor delivery service,
which is fatal in the health care industry, was jeop-
ardizing Meditech's reputation.
COMPANY BACKGROUND
Endoscopic surgical techniques fall under a class of
surgical procedures described as minimally invasive.
Minimally invasive surgery, as opposed to traditional
open surgery, requires only small incisions to
perform an operation. As a result, procedures using
endoscopic techniques often provide substantial
benefits for the patient both physically and
financially. The procedures often shorten patient
recovery, which can translate into reduced surgical
expenses overall. Despite the benefits and the mul-
tidecade history of endoscopic technology, the
procedures have only become popular in the last
10 years. Only three years ago, the market for
endoscopic surgical instruments was expected to
double its size in five years. Growth beyond five
years also looked promising. Largo Healthcare
Company, Meditech's parent company, decided to
spin Meditech off as an independent company
focused solely on producing and selling endoscopic
surgical instruments. Largo management hoped that
the new company would prosper without the dis-
tractions of other Largo businesses and capture
market share of endoscopic instruments as quickly as
possible.
Since its inception just over six years ago,
Meditech has produced innovative, low-cost products.
New products were brought to the market quickly and
pushed by an aggressive sales force. Old products
were updated with innovative features and presented
to the market as new products. Consequently, the
competition between Meditech and National Medical
centered on the continuous development and intro-
duction of new products by both companies. A dozen
or more new products would typically be introduced
by Meditech in any given year.
Source:
Copyright © 1995
by Massachusetts Institute of Technology.
This case was prepared by LFM Fellow Bryan Gilpin under the
direction of Professor Stephen C. Graves as the basis for class
discussion.
CHAPTER 1: INTRODUCTION TO SUPPLY CHAIN MANAGEMENT
19
While the development strategies were similar, the
sales strategies differed dramatically. National Medical
concentrated on selling to surgeons. Meditech's sales
force concentrated on selling to hospitals, material
managers as well as to surgeons. Material managers
tended to be more concerned with cost and delivery
performance. The surgeons, on the other hand, focused
on product features. As the pressures increased on
health care costs, the importance of the material
manager's purchasing position also increased.
Meditech was well positioned to take advantage of
this important shift.
The success of Meditech's strategy quickly
became evident. Within six years, Meditech had
captured the leading share in the endoscopic surgical
instrument market. This was no small feat by any
market's standards, but with surgical instruments this
was especially impressive. Market share changes in
the professional health care industry tended to take
place gradually. Surgeons and doctors often held onto
preferred manufacturers. Hospitals frequently used
group purchasing organizations (GP0s) that took
advantage of extended contracts with suppliers. The
process of "converting" a hospital to a new supplier
often took months of negotiation and convincing.
Most endoscopic surgical instruments are small
enough to fit into the palm of a surgeon's hand.
They are mechanical in nature, typically having
several intricate mechanisms to provide the required
functionality. Materials used to produce the instru-
ments include plastic injection—molded parts, metal
blades, springs, and so forth. In all cases of use,
surgeons use the instrument for one operation and
then immediately dispose of it. Instruments are never
resterilized and reused for another patient. All in all,
the Meditech product line consists of over 200
separate end-products.
DISTRIBUTION
Meditech distributes all its goods from a central
warehouse, using two primary channels—domestic
dealers and international affiliates—to distribute its
products from the central warehouse to end-
customers (i.e., hospitals). The first channel, for
domestic sales only, uses domestic distributors, or
dealers, to ship to hospitals. The dealers order and
receive products from multiple manufacturers,
including Meditech, typically stocking hundreds of
different products. Stocked products range from
commodity items, such as surgical gloves and
aspirin, to endoscopic surgical instruments. By using
dealers to supply products, hospitals do not need to
order directly from manufacturers for their diverse
needs. Additionally, since dealers maintain regional
warehouses all over the United States, the distance
between dealer warehouses and most hospitals tends
to be quite small. The short distance permits frequent
replenishments of hospital inventories; in some
cases, trucks from dealers drop off supplies once or
twice per day. Hospitals enjoy the frequent replen-
ishments, which reduce hospital inventory and, con-
sequently, reduce material costs.
The regional dealer warehouses act as independent
entities, autonomously determining when to order
new supplies and how much to order. Therefore,
while Meditech uses only four or five major dis-
tribution companies, it still receives orders from, and
ships to, hundreds of regional, individually run
warehouses. Each warehouse in turn ships to about a
dozen or more hospitals, resulting in thousands of
hospitals that receive Meditech products.
The distribution channel for international sales
uses Largo Healthcare's international affiliates.
International affiliates are wholly owned subsidiaries
of Largo Healthcare residing outside of the United
States. As with domestic dealers, affiliates distribute
to hospitals in their regional area. However, in
contrast with domestic dealers, which may locate
within just a few miles of customer hospitals, an
affiliate ships product throughout an entire country.
From Meditech's point of view, affiliates' orders
essentially look no different than dealers'—inter-
national affiliates submit orders to Meditech and
Meditech fills them with available product.
INTERNAL OPERATIONS
The production processes to manufacture endoscopic
instruments are composed of three major steps:
assembling of component parts into individual or
"bulk" instruments, packaging one or more bulk
instruments into a packaged good, and sterilizing the
packaged goods. Each of these steps is described
below.
Assembly
The assembly process is manually intensive.
Component parts arrive into the assembly area from
suppliers following a brief inspection by Quality
Plant Manager #1
V.P. Operations,
(K. Strangler)
Director
Supplier
Management
Director
Planning, Distribution, and
Customer Service
Central Planning
(J. Bolbrede)
Customer Service
and Distribution
(D. Franklin)
Inventory
(C. Stout)
Logistics
(B. Slokoski)
Material
Support
Svcs.
Quality
Business
Unit
Business
Unit
Plant Manager #2
20
DESIGNING AND MANAGING THE SUPPLY CHAIN
Assurance (QA). The parts are placed into inventory
until ready for use by one of several assembly lines.
Each assembly line is run by a team of cross-
trained production workers who can produce any of
several instruments within a product family. Line
changeovers within a family are quick and inex-
pensive, merely requiring a warning from the pro-
duction team leader and a supply of the appropriate
component parts. The typical cycle time for assembly
of a batch of instruments—the time required to
schedule assembly of a batch of instruments and then
actually assemble them, assuming that component
parts are available in component parts inventory—is
on the order of two weeks. Lead time for component
parts is on the order of 2-16 weeks. Assembled
instruments are moved from the assembly area into
bulk instrument inventory, where they wait to be
packaged.
Packaging
The packaging process makes use of several large
packaging machines. The machines direct bulk
instruments into plastic containers and then adhere a
flexible sheet of material over the top of the container.
The entire plastic container is then placed into a
finished 16-cardboard container and shipped imme-
diately to the sterilizer. Capacity at the packaging area
has not restricted output.
Sterilization
The sterilization process uses a large Cobalt
radiation sterilizer. After batches of packaged
instruments (cardboard container, plastic container,
and instruments) are placed into the sterilizer, the
sterilizer is turned on for about an hour. The
radiation penetrates cardboard and plastic to destroy
any potentially harmful contaminants. The sterilizer
can sterilize as much product as will fit inside its four
walls. Capacity limitations have not been a problem
thus far. Sterilized instruments are immediately
moved into finished goods inventory.
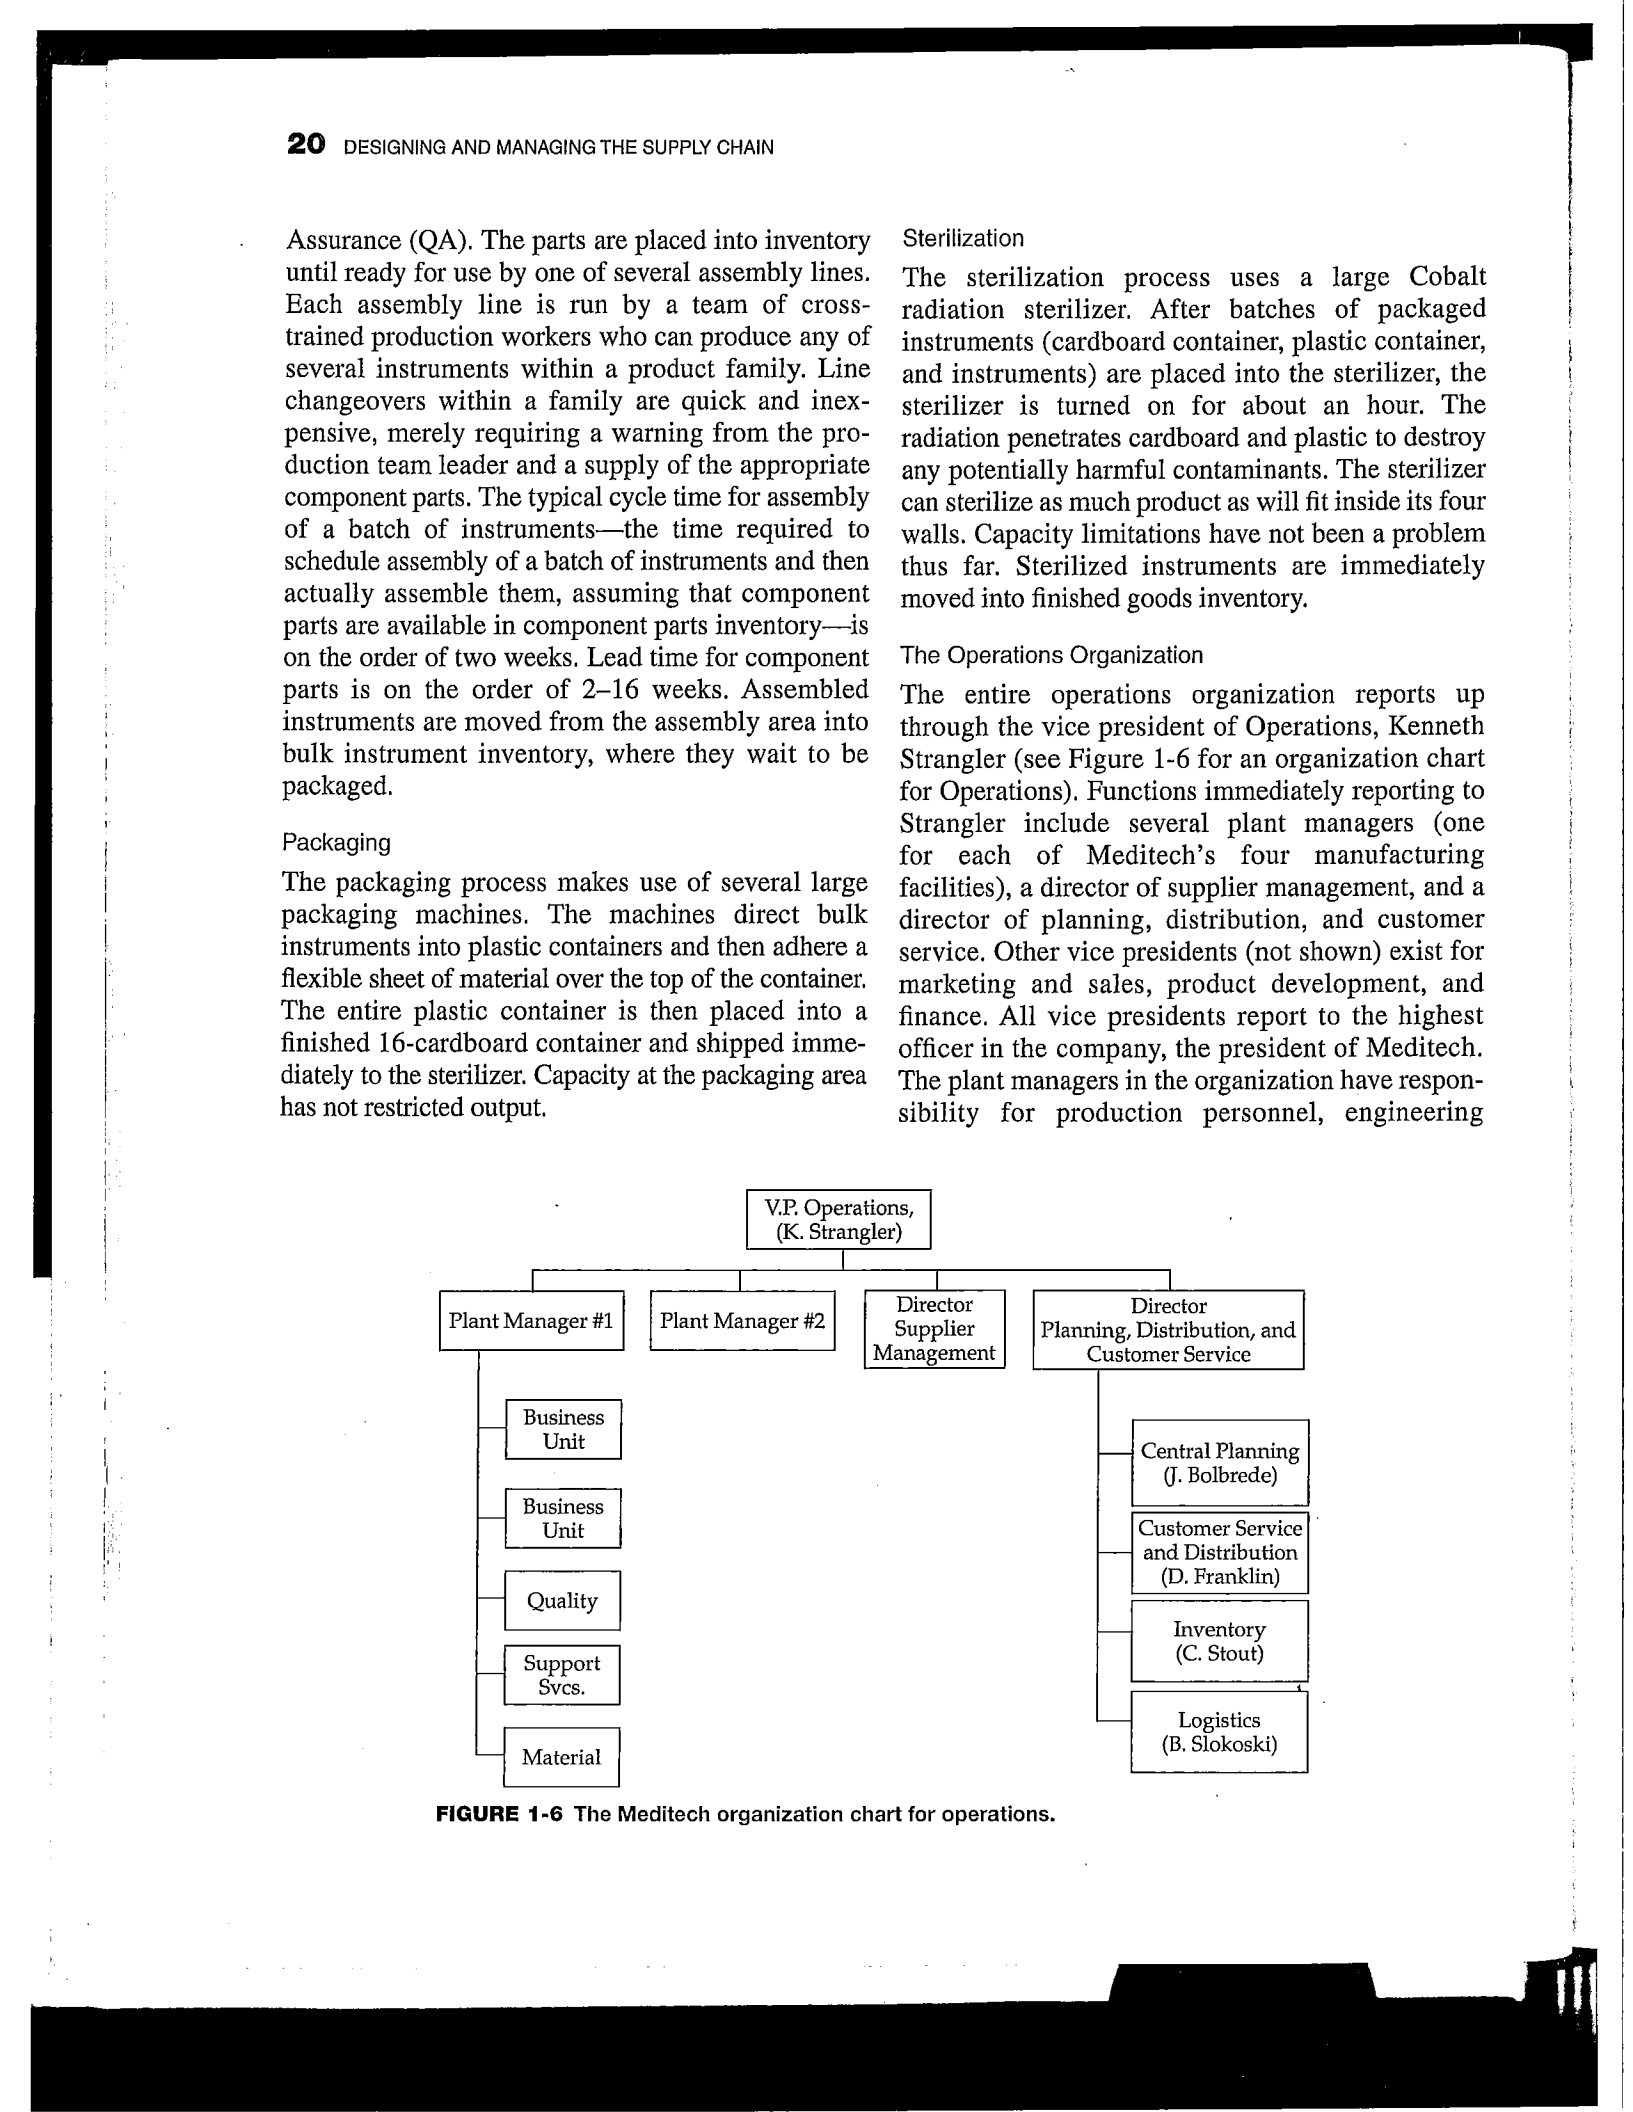
The Operations Organization
The entire operations organization reports up
through the vice president of Operations, Kenneth
Strangler (see Figure 1-6 for an organization chart
for Operations). Functions immediately reporting to
Strangler include several plant managers (one
for each of Meditech's four manufacturing
facilities), a director of supplier management, and a
director of planning, distribution, and customer
service. Other vice presidents (not shown) exist for
marketing and sales, product development, and
finance. All vice presidents report to the highest
officer in the company, the president of Meditech.
The plant managers in the organization have respon-
sibility for production personnel, engineering
FIGURE 1-6
The Meditech organization chart for operations.
CHAPTER 1: INTRODUCTION TO SUPPLY CHAIN MANAGEMENT
21
technicians, quality assurance, support services, and
material supply for their respective facilities.
Reporting directly to the plant managers are
several business units. Each business unit has full
responsibility either for the assembly of a par-
ticular product family or, in the case of packaging
and sterilization, for an entire production process.
The most important job of each assembly business
unit is to meet the production schedule every week.
Meeting the schedule ensures a constant supply of
bulk instruments to the packaging/sterilization
process. The process of determining assembly and
packaging/sterilization schedules will be discussed
below.
Also reporting to the vice president of Operations
are Supplier Management and Planning, Distribution,
and Customer Service. Supplier Management works
on relationships with suppliers, including estab-
lishing purchasing contracts and finding new
suppliers if necessary. The Planning, Distribution,
and Customer Service department does everything it
can to ensure that customers receive product when
needed. The positions within the Customer Service
department include the manager of Customer
Service and Distribution, Dan Franklin; the manager
of Central Planning; the manager of Inventory; and
a manager of Logistics. Customer Service deals
with everything from occasional customer com-
plaints to establishing strategies to improve delivery
service to customers. Customer Service represen-
tatives work with dealers and affiliates to keep them
updated on product delivery schedules and
problems. Often this responsibility places the
Customer Service representative in direct contact
with hospital personnel.
While Customer Service handles issues concerning
the movement of product out of finished goods
inventory, Central Planning ensures that adequate
finished goods are available to meet incoming orders.
They develop monthly production plans that are used
by the business units to determine weekly and daily
schedules.
Charles Stout, the Inventory manager, determines
the finished goods inventory policy and establishes
parts "and bulk inventory guidelines for the business
units. When a mandate to reduce inventory is passed
down from higher levels of management, the Inventory
manager must determine where inventory can be
reduced and then begin enforcing those reductions.
Through recent efforts, Stout had successfully
eliminated several million dollars of obsolete and
slow-moving inventory.
PRODUCTION PLANNING AND SCHEDULING
The production planning and scheduling process is
broken down into two parts: planning, based on
monthly forecasts, of assembly and component parts
orders and daily scheduling of packaging and steril-
ization based on finished goods inventory levels.
During the fourth quarter of each fiscal year, the
marketing and finance organizations determine an
annual forecast. The annual forecast is then broken
down proportionately, based on the number of weeks
in the month, into monthly forecasts. As the year pro-
gresses, the Central Planners work with the Marketing
organization to make forecast adjustments according
to market trends and events. At the beginning of each
month, the month's forecasts are adjusted and agreed
upon by the Marketing organization and the Central
Planners.
The planning of assembly for a particular
instrument begins with the monthly demand forecasts.
Based on the month's forecast, the Central Planners
determine the amount of product that needs to be
transferred from bulk inventory into finished goods
inventory to "meet" the expected demand. This
amount, termed the finished goods "transfer requir-
ement," is determined by subtracting the current
finished goods inventory level from (1) the demand
forecast for the month plus (2) the required safety
stock. (The current safety stock policy is to maintain
three weeks' worth of demand).
The transfer requirements, once completed for all
200-plus product codes, are passed throughout the
organization for approval. This process typically
takes place one to two weeks into the current month.
While not actually used to schedule assembly or to
alter the packaging and sterilization processes, the
transfer requirements provide an estimate of the
required overall production for the month. Any
problems in being able to deliver to the plan can then
be identified and resolved.
Assembly schedules and replenishment orders for
parts are based on the monthly demand forecasts
and current inventory levels. By mid-month, the
completed monthly plans, which contain the monthly
forecasts, are sent to the assembly business units. A
planner in the business unit plugs the forecasts into a
Materials Requirement Planning (MRP) system,
22
DESIGNING AND MANAGING THE SUPPLY CHAIN
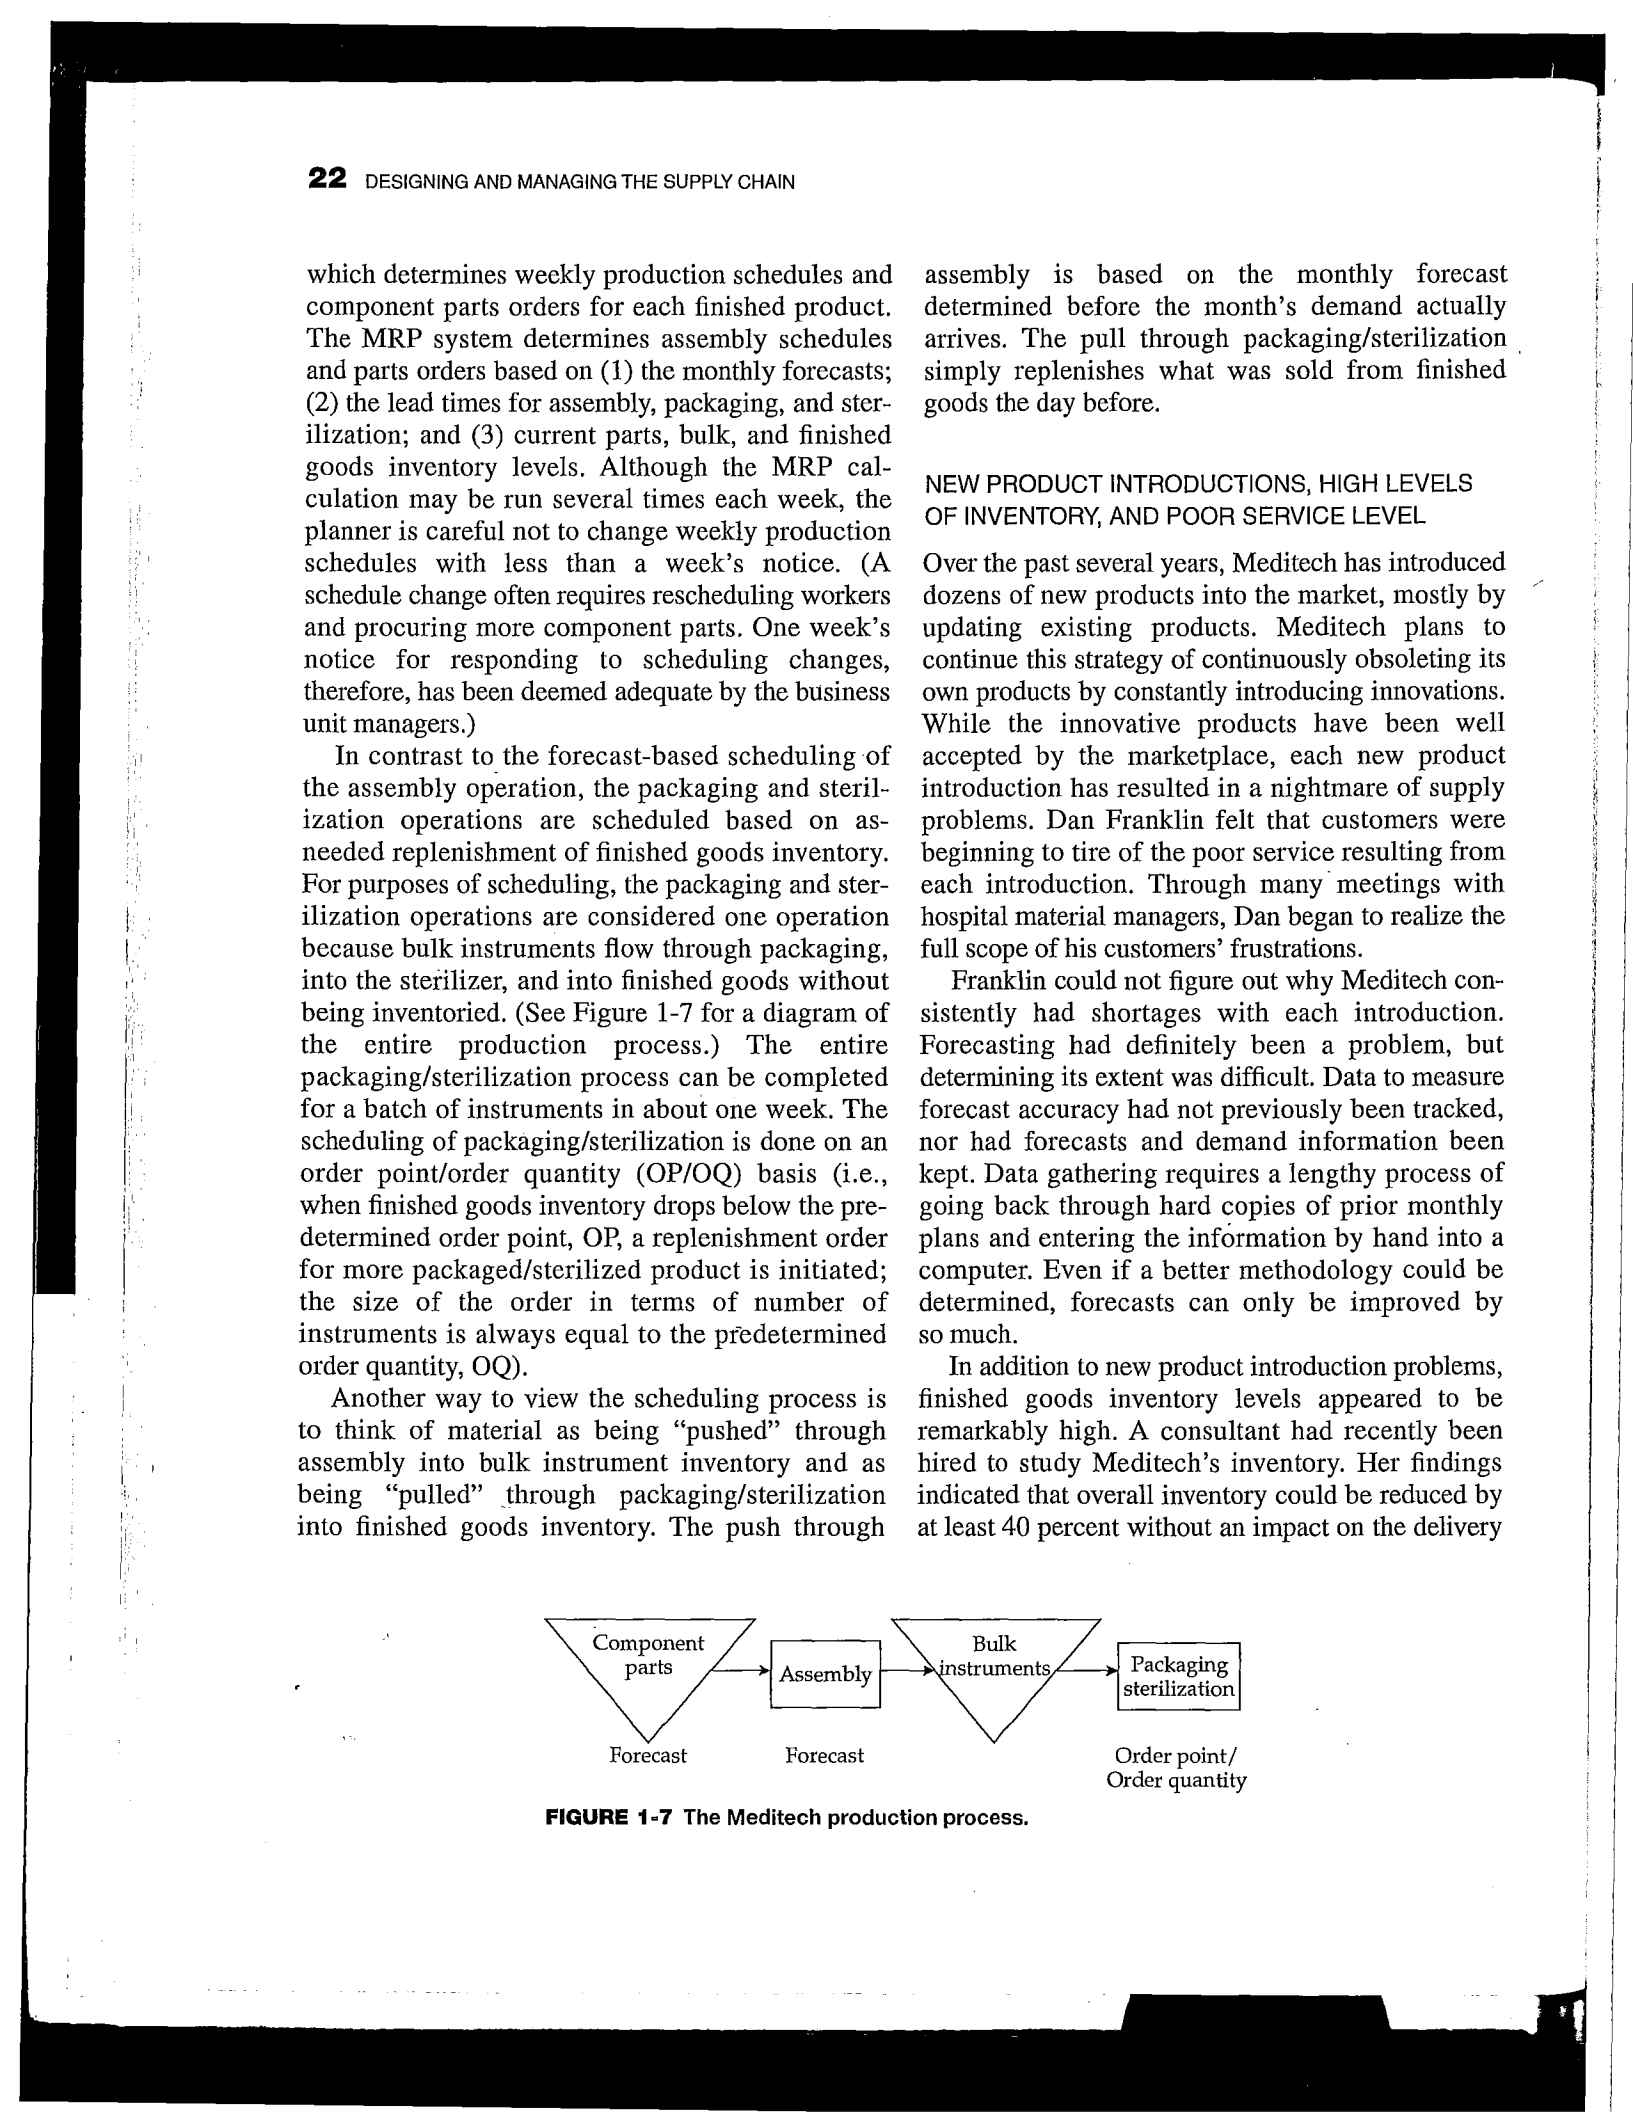
Assembly
Order point/
Order quantity
Packaging
sterilization
which determines weekly production schedules and
component parts orders for each finished product.
The MRP system determines assembly schedules
and parts orders based on (1) the monthly forecasts;
(2) the lead times for assembly, packaging, and ster-
ilization; and (3) current parts, bulk, and finished
goods inventory levels. Although the MRP cal-
culation may be run several times each week, the
planner is careful not to change weekly production
schedules with less than a week's notice. (A
schedule change often requires rescheduling workers
and procuring more component parts. One week's
notice for responding to scheduling changes,
therefore, has been deemed adequate by the business
unit managers.)
In contrast to the forecast-based scheduling of
the assembly operation, the packaging and steril-
ization operations are scheduled based on as-
needed replenishment of finished goods inventory.
For purposes of scheduling, the packaging and ster-
ilization operations are considered one operation
because bulk instruments flow through packaging,
into the sterilizer, and into finished goods without
being inventoried. (See Figure 1-7 for a diagram of
the entire production process.) The entire
packaging/sterilization process can be completed
for a batch of instruments in about one week. The
scheduling of packaging/sterilization is done on an
order point/order quantity (OP/0Q) basis (i.e.,
when finished goods inventory drops below the pre-
determined order point, OP, a replenishment order
for more packaged/sterilized product is initiated;
the size of the order in terms of number of
instruments is always equal to the pfedetermined
order quantity, OQ).
Another way to view the scheduling process is
to think of material as being "pushed" through
assembly into bulk instrument inventory and as
being "pulled" through packaging/sterilization
into finished goods inventory. The push through
assembly is based on the monthly forecast
determined before the month's demand actually
arrives. The pull through packaging/sterilization
simply replenishes what was sold from finished
goods the day before.
NEW PRODUCT INTRODUCTIONS, HIGH LEVELS
OF INVENTORY, AND POOR SERVICE LEVEL
Over the past several years, Meditech has introduced
dozens of new products into the market, mostly by
updating existing products. Meditech plans to
continue this strategy of continuously obsoleting its
own products by constantly introducing innovations.
While the innovative products have been well
accepted by the marketplace, each new product
introduction has resulted in a nightmare of supply
problems. Dan Franklin felt that customers were
beginning to tire of the poor service resulting from
each introduction. Through many meetings with
hospital material managers, Dan began to realize the
full scope of his customers' frustrations.
Franklin could not figure out why Meditech con-
sistently had shortages with each introduction.
Forecasting had definitely been a problem, but
determining its extent was difficult. Data to measure
forecast accuracy had not previously been tracked,
nor had forecasts and demand information been
kept. Data gathering requires a lengthy process of
going back through hard copies of prior monthly
plans and entering the information by hand into a
computer. Even if a better methodology could be
determined, forecasts can only be improved by
so much.
In addition to new product introduction problems,
finished goods inventory levels appeared to be
remarkably high. A consultant had recently been
hired to study Meditech's inventory. Her findings
indicated that overall inventory could be reduced by
at least 40 percent without an impact on the delivery
FIGURE 1-7 The Meditech production process.
CHAPTER 1: INTRODUCTION TO SUPPLY CHAIN MANAGEMENT
23
4500
4000
3500 -
3000 -
2500 -
2000 -
1500
1000
500 -
Current inventory policy —3
/ demand-weeks
Need this much inventory (-2240 sales units
= 11 demand-weeks) at the beginning of
/ each week to remain out of back order
Weekly demand
Average weekly
demand
0
4-Jun
18-Jun 2-Jul
16-Jul
30-Jul 13-Aug 27-Aug 10-Sep 24-Sep
Date
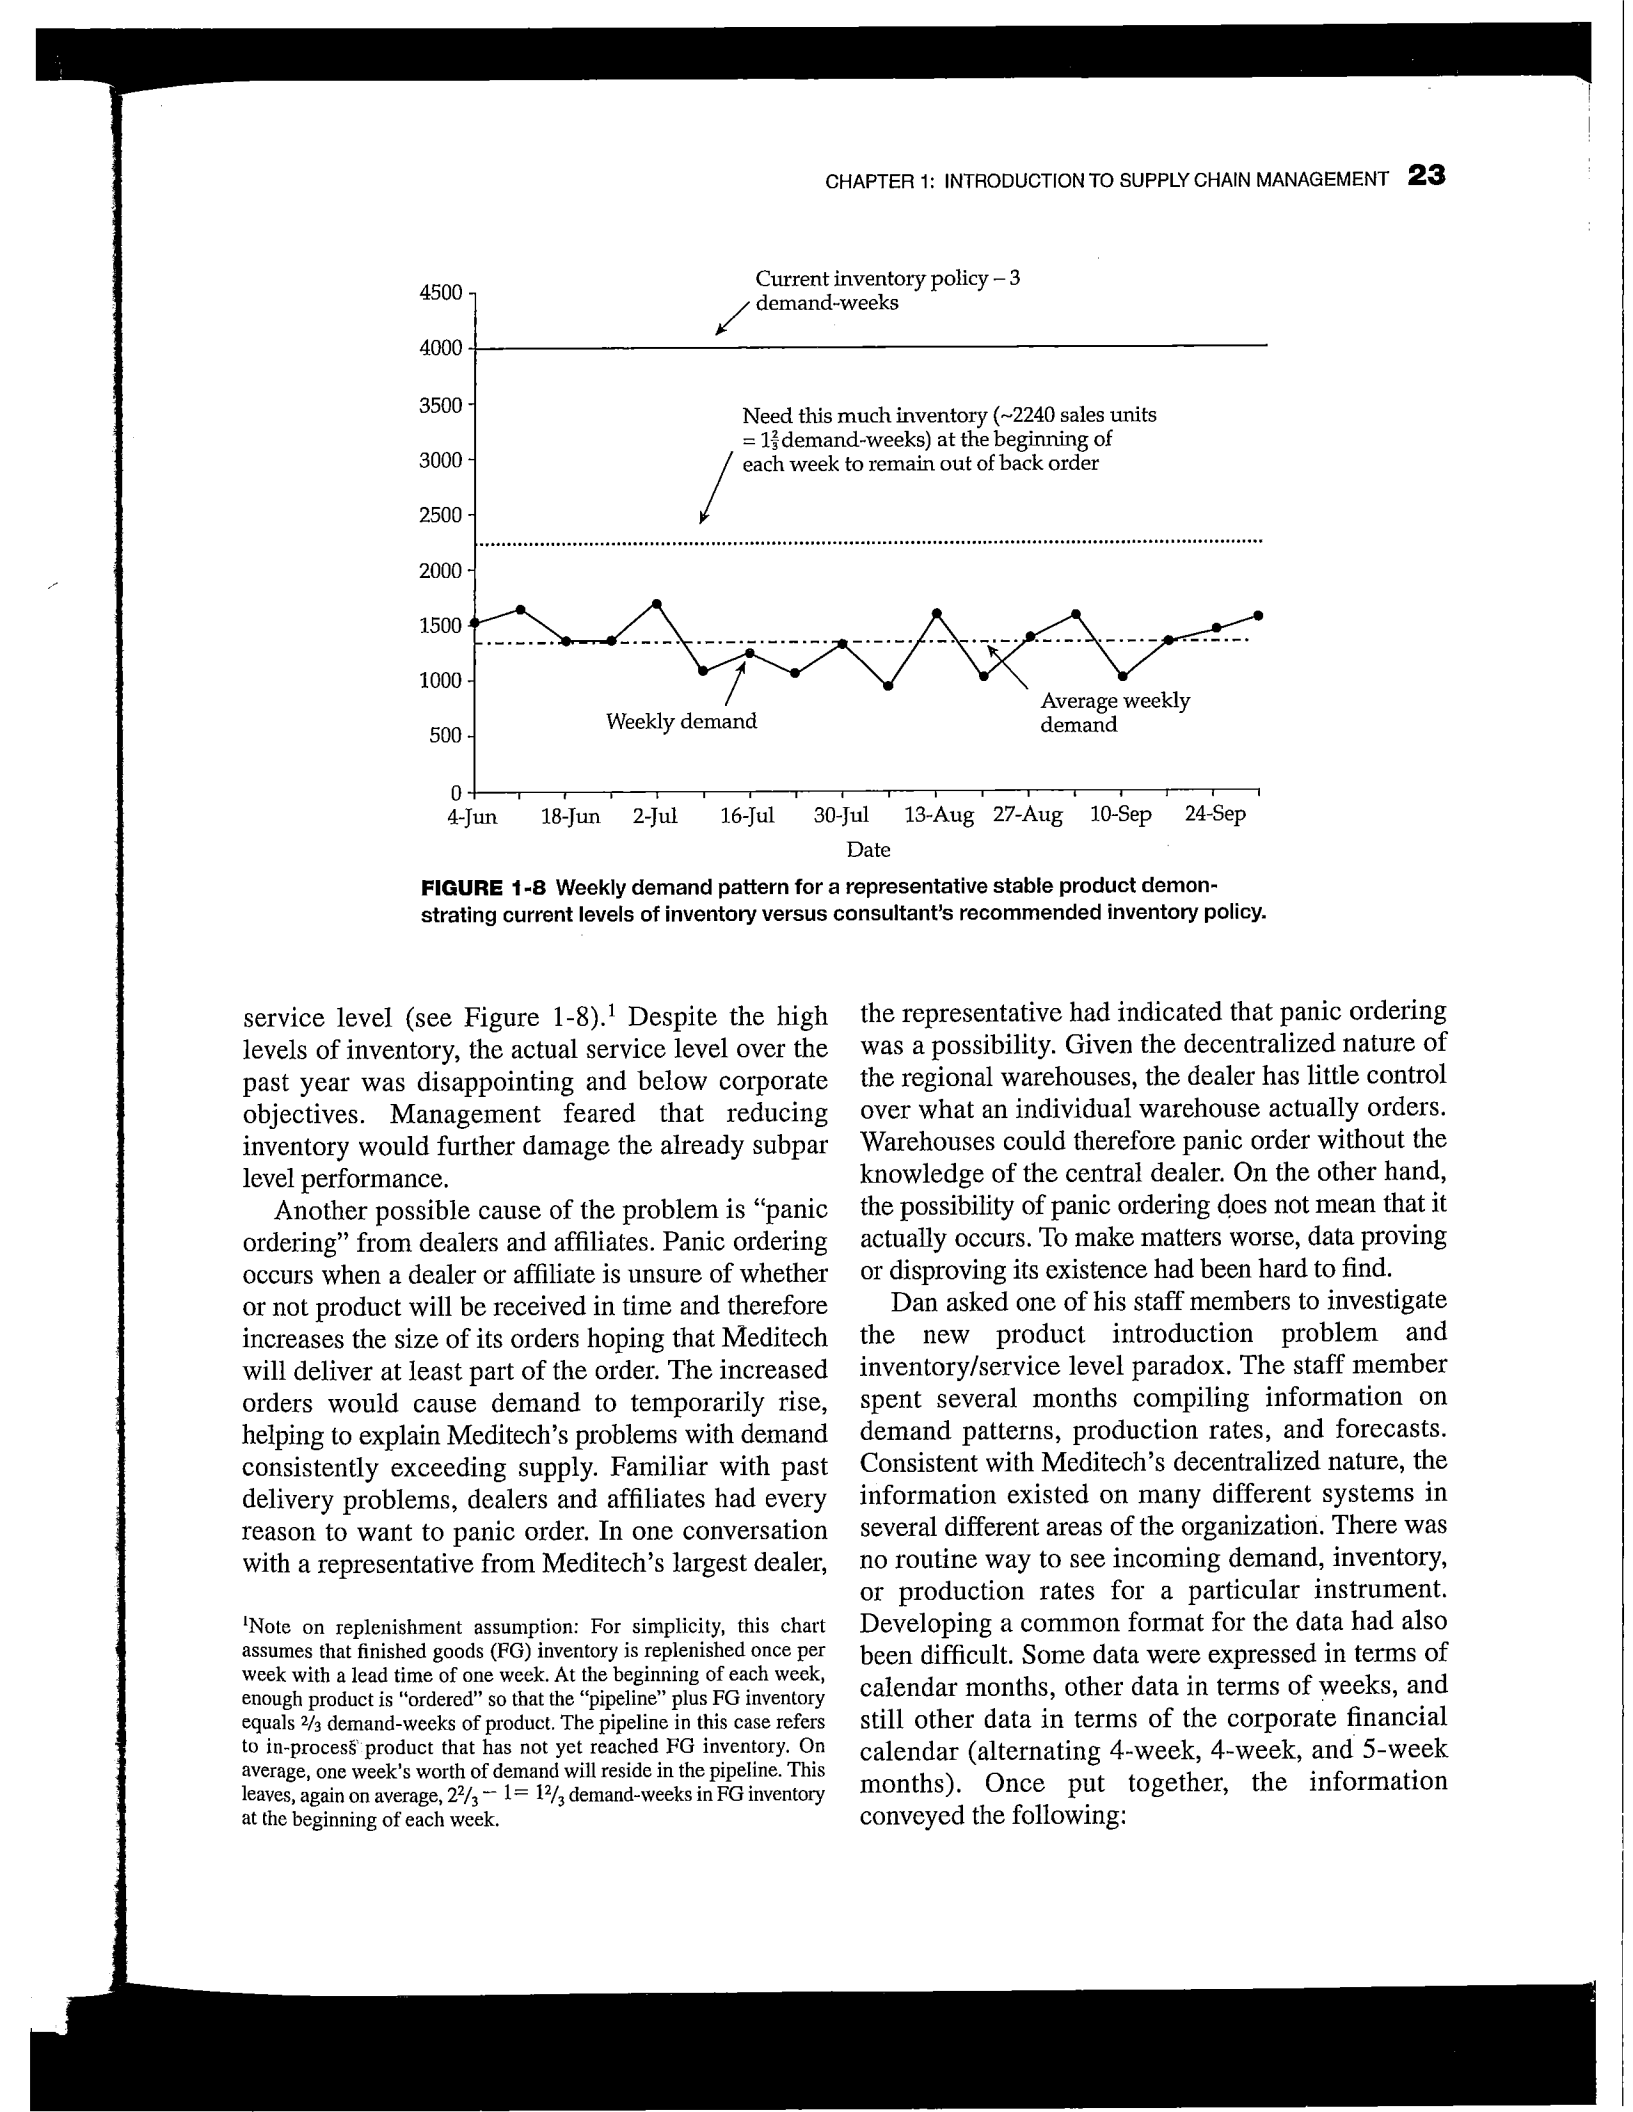
FIGURE 1-8
Weekly demand pattern for a representative stable product demon-
strating current levels of inventory versus consultant's recommended inventory policy.
service level (see Figure
l8).1
Despite the high
levels of inventory, the actual service level over the
past year was disappointing and below corporate
objectives. Management feared that reducing
inventory would further damage the already subpar
level performance.
Another possible cause of the problem is "panic
ordering" from dealers and affiliates. Panic ordering
occurs when a dealer or affiliate is unsure of whether
or not product will be received in time and therefore
increases the size of its orders hoping that Meditech
will deliver at least part of the order. The increased
orders would cause demand to temporarily rise,
helping to explain Meditech's problems with demand
consistently exceeding supply. Familiar with past
delivery problems, dealers and affiliates had every
reason to want to panic order. In one conversation
with a representative from Meditech's largest dealer,
`Note on replenishment assumption: For simplicity, this chart
assumes that finished goods (FG) inventory is replenished once per
week with a lead time of one week. At the beginning of each week,
enough product is "ordered" so that the "pipeline" plus FG inventory
equals
2
/
3
demand-weeks of product. The pipeline in this case refers
to in-procesS product that has not yet reached FG inventory. On
average, one week's worth of demand will reside in the pipeline. This
leaves, again on average, 2
2
/
3
—
1= 1
2
/
3
demand-weeks in FG inventory
at the beginning of each week.
the representative had indicated that panic ordering
was a possibility. Given the decentralized nature of
the regional warehouses, the dealer has little control
over what an individual warehouse actually orders.
Warehouses could therefore panic order without the
knowledge of the central dealer. On the other hand,
the possibility of panic ordering does not mean that it
actually occurs. To make matters worse, data proving
or disproving its existence had been hard to find.
Dan asked one of his staff members to investigate
the new product introduction problem and
inventory/service level paradox. The staff member
spent several months compiling information on
demand patterns, production rates, and forecasts.
Consistent with Meditech's decentralized nature, the
information existed on many different systems in
several different areas of the organization. There was
no routine way to see incoming demand, inventory,
or production rates for a particular instrument.
Developing a common format for the data had also
been difficult. Some data were expressed in terms of
calendar months, other data in terms of weeks, and
still other data in terms of the corporate financial
calendar (alternating 4-week, 4-week, and 5-week
months). Once put together, the information
conveyed the following:
Month 'Month Month /Month
0
1 'S., 2
3
onth Month
-2
-1
-2000
Month Month Month
4
5
6
-0- Net Orders
-
A
-
Planned Production
-
- FG Inventory
(1) Increased demand causes back order
_ _
------- _ ,
./
'
,//
(5) (Beginning of)
,'
•
Steady state
_
(3) FG inventory shoots up
16000
14000
12000
10000
8000
6000
4000
2000
(2) Production increases output
-4000
24
DESIGNING AND MANAGING THE SUPPLY CHAIN
Weekly Net Orders for a New Product
1 2 3 4 5 6 7 8 9 10 11 12 13 14 15 16 17 18 19 20 21 22 23 24 25 26
Week #
—0-- Total Net Orders
FIGURE 1-9
Typical demand pattern for a new product introduction. The product was
officially introduced near the end of week #4.
•
New product demand after an introduction
followed a consistent pattern of reaching a high
peak during the first few weeks, but becoming
relatively stable immediately afterward (see
Figure 1-9).
•
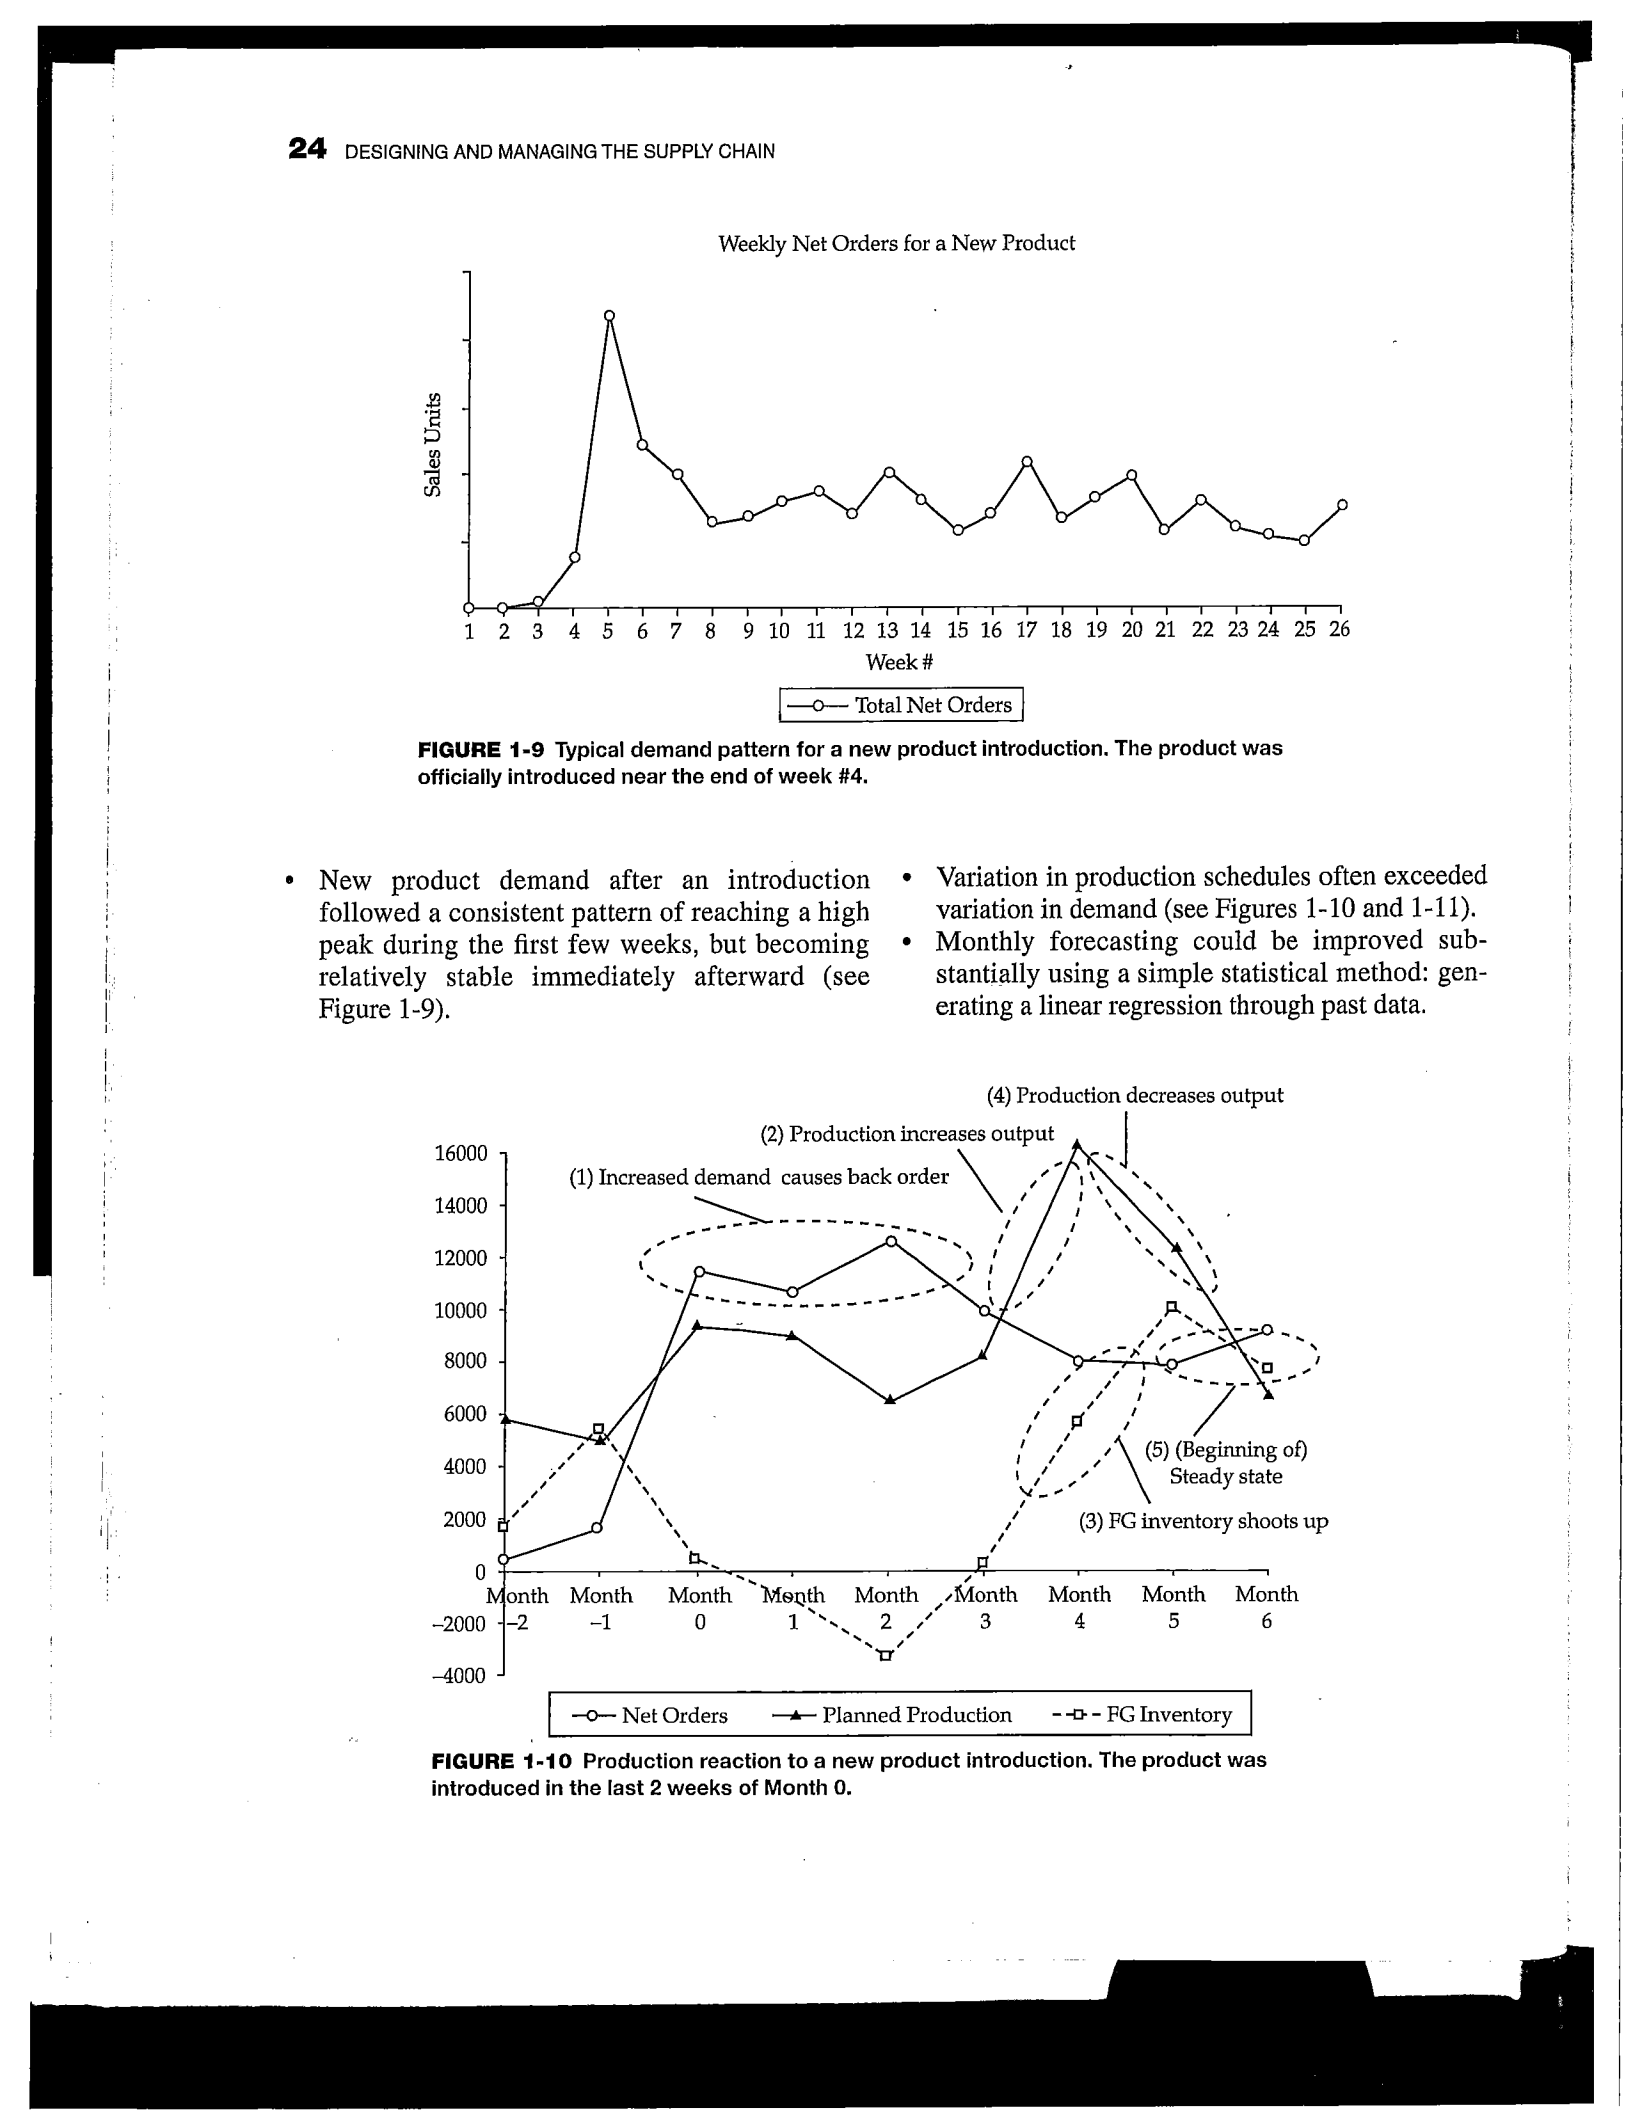
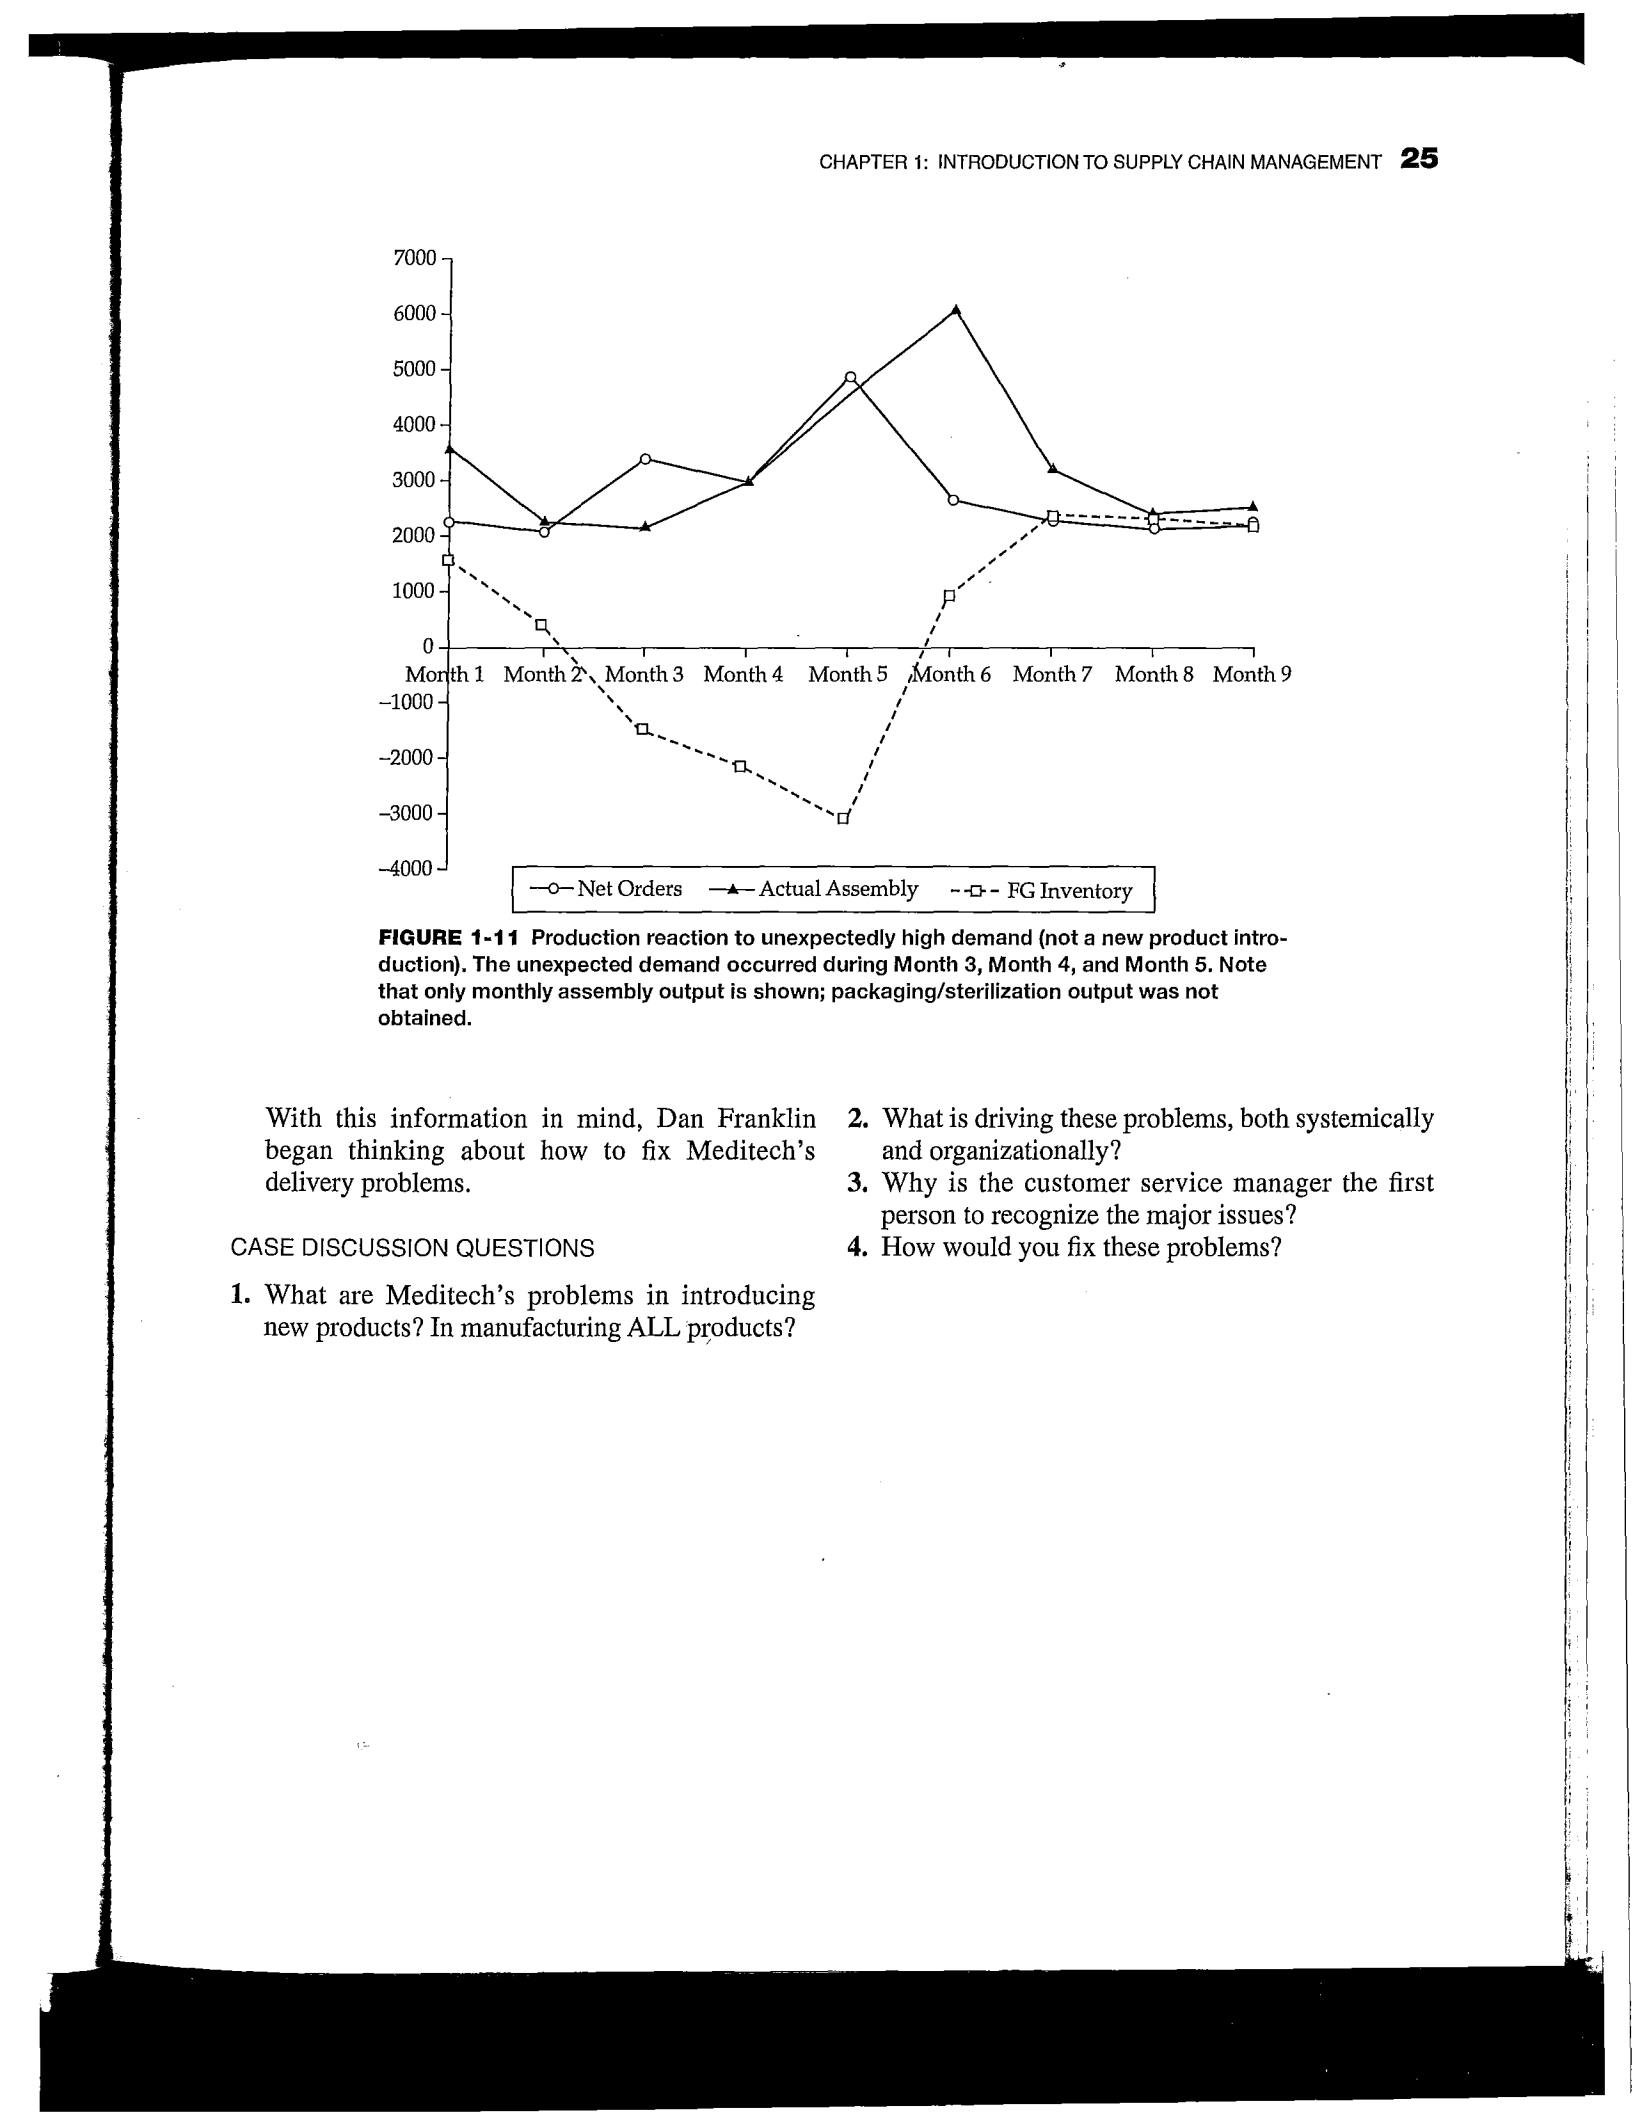
Variation in production schedules often exceeded
variation in demand (see Figures 1-10 and 1-11).
•
Monthly forecasting could be improved sub-
stantially using a simple statistical method: gen-
erating a linear regression through past data.
(4) Production decreases output
FIGURE 1-10
Production reaction to a new product introduction. The product was
introduced in the last 2 weeks of Month 0.
CHAPTER 1: INTRODUCTION TO SUPPLY CHAIN MANAGEMENT
25
7000
6000
5000
4000
3000
2000
1000
0
Mo th 1
-1000
-
2000
-
3000
-4000
e'
Month 2`,
,
Month 3 Month 4 Month 5
,
,Month 6 Month 7 Month 8 Month 9
'DI
—o- Net Orders —A-- Actual Assembly - -o- - FG Inventory
FIGURE 1-11
Production reaction to unexpectedly high demand (not a new product intro-
duction). The unexpected demand occurred during Month 3, Month 4, and Month 5. Note
that only monthly assembly output is shown; packaging/sterilization output was not
obtained.
With this information in mind, Dan Franklin
began thinking about how to fix Meditech's
delivery problems.
CASE
DISCUSSION QUESTIONS
1. What are Meditech's problems in introducing
new products? In manufacturing ALL products?
2.
What is driving these problems, both systemically
and organizationally?
3.
Why is the customer service manager the first
person to recognize the major issues?
4.
How would you fix these problems?

Running head: RESPONSE 1
Response
Institution Affiliation
Date

RESPONSE 2
Introduction
I like your introduction. Meditech is indeed a company that branched off its parent
company, Largo Healthcare, to focus on the endoscopic instruments market. Surgeons, to
perform minimally invasive surgeries, mainly use endoscopic surgical instruments. As an
independent company, Meditech aggressively competed in the endoscopic market while
constantly improving and introducing new instruments into the market. The company, however,
has high levels of customer dissatisfaction regarding the release of new products. This discussion
is a response to a student's original answers to a case study.
Problems in product introduction
I agree that after each product introduction, there should be a time interval before the next
product introduction. Meditech introduces about twelve products annually, which translates to a
new product each month. The first issue that arises from constant product introductions is the
manufacture of these new products. Each month, as the new products are manufactures, it puts a
drag on the continuing production of the existing products. The drag eventually leads to the end
of the production of the previous products as the new products enter the market. The premature
cut off the previous product means that many customers did not receive their orders. Due to this
experience, many clients tend to panic order and double order to get the needed instruments.
(Wang & Disney, 2016). This leads to the buildup of inventory due to numerous orders and
issues regarding product delivery. There is minimal customer satisfaction.
Systemic and organizational issues
The constant product introduction, coupled up with the panic orders creates massive
stress on the system functioning at Meditech. I agree that the high production of less popular

RESPONSE 3
products leads to an even higher number of unpurchased products. The concentration of the
resources on these less popular products results to little or no production of popular products.
The lack of proper forecasting data leads to poor assessment of market demand. This prevents
the creation of clear production schedules that causes a delay in delivery of products to
customers. The company consists of four separate facilities, proving to be greatly decentralized.
This is a challenge regarding the flow of necessary information within the organization.
Customer service and issue identification
The main issue is customer dissatisfaction. I, therefore, agree that the customer service
manager is the first to know of these issues of the broken chain of command. The manager
personally interacts with the customers to promote the products, ensure deliveries, receive, and
review customer complaints. The customer service manager is also responsible for strategizing
ways of maintaining the customer reach and improving relationships between the customers and
the company. The manager is, therefore, in a unique position in customer relations where issues
regarding the service and dissatisfaction can surface. (Jalkala & Salminen, 2010).
Fix to the problems
I agree that a freely accessible data system would be a significant step in solving the
problems at Meditech. The freely accessible data system would address the challenges brought
about by the decentralized system in Meditech. The ease of access to information would assist in
synchronizing production and sharing of demand information throughout the company. Another
solution would be increasing the time between product introductions to better cater for the orders
of the existing products. To better utilize the period, an efficient data collection system should be

RESPONSE 4
set up to study the progress of products and create a forecast for future demand. (Petropoulos &
Kourentzes, 2015).

RESPONSE 5
References
Jalkala, A., & Salminen, R. T. (2010). Practices and functions of customer reference
marketing—Leveraging customer references as marketing assets. Industrial Marketing
Management, 39(6), 975-985
Petropoulos, F., & Kourentzes, N. (2015). Forecast combinations for intermittent
demand. Journal of the Operational Research Society, 66(6), 914-924.
Wang, X., & Disney, S. M. (2016). The bullwhip effect: Progress, trends, and directions.
European Journal of Operational Research, 250(3), 691-701.

Response Outline
I. Introduction
II. What are Meditech’s problems in introducing new products? In manufacturing ALL
products?
III. What is driving these problems, both systemically and organizationally?
IV. Why is the customer service manager the first person to recognize the major issues?
V. How would you fix the problems?

