


3
Human Factors and Ergonomics
The International Ergonomics Association (IEA) Council defines the disciple of
HF/E as; "Ergonomics (or human factors) is the scientific discipline concerned with the
understanding of interactions among humans and other elements of a system. The
profession applies theory, principles, data and methods to the design of systems, for
example, workplace, tasks, processes, in order to optimize human well-being and overall
system performance" (IEA 2000). Thus, HF/E, in microcosm, means fitting humans to
the system by assembling information on human characteristics, such as capabilities,
capacities, limitations, weakness, and frailties. This information is transformed to the
practice in design of products, environment, tasks, equipment, and workplaces (Eastman
Kodak Company 1983). Human factors and ergonomics is an applied science concerned
with designing human-centric systems in which humans and the other elements in the
system interact most efficiently, safely, healthily, comfortably, and productively. In the
economical point of view, “Ergonomics is good business practice, and can effectively
contribute to the economic well-being of the company” (Douphrate and Rosecrance
2004).
In the same parallelism, the IEA defines a human factors specialist and an
ergonomist as a contributor “to the design and evaluation of tasks, jobs, products,
environments and systems in order to make them compatible with the needs, abilities and
limitations of people” (IEA 2000). Human factors specialists and ergonomists first
analyze the actual system while considering the scientific knowledge, and then define the
desired system that complies with human characteristics. Taking action to decrease the
difference between the actual and the desired system is the main focus of human factors

4
specialists and ergonomists. The achievement of the overall system depends on how well
the actual system is observed, the desired system is defined, and ergonomic principles are
handled to solve problems.
Even though HF/E has existed since human beings have existed, ergonomics was
first used to design man-machine or human-machine interfaces. Wojciech Jastrzebowski
is the author of the term “Ergonomics” by deriving it from two Greek words “ergon”
meaning work and “nomos” meaning laws, principles, or rules; therefore, the rules of
work is the literal definition of ergonomics. Jastrzebowski was the first person who
created the foundation of ergonomics and used the term ergonomics in his book titled “An
Outline of Ergonomics, or the Science of Work Based upon the Truths Drawn from the
Science of Nature” in 1875 (Karwowski 2006). Thus, even though the concept of
ergonomics is not new, the term was used in the literature for some one hundred and fifty
years. Chapanis and his colleagues were interested in the interrelationship between men
and machines so as to learn the best way to design a user friendly machine (Chapanis et
al. 1949). These applied experimental psychologists at John Hopkins University
published the first ergonomics textbook, “Applied Experimental Psychology: Human
Factors in Engineering Design” in 1949 (Lavietes 2002). They preferred the term
“human factors” instead of “ergonomics.”
Industrial / Occupational Human Factors and Ergonomics
The discipline of HF/E is made of sub-disciplines. Industrial or occupational
(human factors) ergonomics is one of them. It is mainly about the application of theories,
principles, methods, and data related to HF/E. Applications include evaluation, design,

5
and development of industrial work organizations. Workers, equipment, tools,
workplaces, work environment, and work schedules are the main interest of industrial
[human factors specialists and] ergonomists. The objective of industrial or occupational
HF/E is to optimize productivity of the worker and the total production system while still
enhancing the well being, job satisfaction, and safety of workers (Black and Hunter
2003). To achieve these goals, an optimal fit between work demands and operator
capabilities has to be achieved.
The scope of this study focuses on the aspects of HF/E on an industrial basis.
Product design or issues related to sales and marketing are excluded from the concept of
industrial human factors and ergonomics and also from the concept of this study.
Relationships between Human Factor and Ergonomics and Other Sciences
Human factors and ergonomics must be multidisciplinary in order to handle the
diversity and complexity of human beings, products, and environmental conditions
(Eastman Kodak Company 1983). Human factors and ergonomics uses the knowledge
and techniques shared with other sciences to meet the demands of this diversity and
complexity. Human factors and ergonomics is an applied science whose roots are in basic
sciences (Hermans and Peteghem 2006). Human factors and ergonomics combines
several sciences such as anatomy, anthropometry, bioinstrumentation, biomechanics,
computer science, electrical and mechanical engineering, industrial engineering,
kinesiology, medicine, physiology, psychology, and more.
Human factors and ergonomic has interactions with not only other sciences but its
own sub-disciplines. Macroergonomics, one of its sub-disciplines, is concerned with

6
analyzing, designing, and evaluation systems. In addition to physical aspects of work
systems, macroergonomics includes industrial, organizational, managerial, and personnel
psychological aspects in work systems. The difference between macroergonomics and
traditional HF/E (or microergonomics) is that macroergonomics deals with the interaction
between humans and the organization while microergonomics deals with the interaction
between humans and the other elements of the system such as machine, environment,
software, and job. All these interactions are studied under different sub-disciplines. For
example, hardware [human factors and] ergonomics is interested in the relationship
between human and machine; environmental [human factors and] ergonomics focuses on
the interaction between humans and their environment; cognitive [human factors and]
ergonomics is more related to human-software interaction and how a human perceives,
thinks, and processes information; and work design [human factors and] ergonomics is
interested in the interaction between a human and job (Hendrick and Kleiner 2002).
Manufacturing Systems
Systems, especially manufacturing systems, are organizational structures that
have purposes and production resources to reach desired goals in a specific environment.
Productivity, effectiveness, efficiency, product quality, timeliness, and safety are some of
the parameters that should be satisfied in systems. Manufacturing systems are made of
elements such as the worker, task, material, equipment and tool, and environment. These
elements have interactions among each other. The main element of the system is human.
Humans plan, build, manage, and control the system. However, humans have some
capabilities and limitations as well. Human factors and ergonomics in the industry is

7
based on the concept of matching these capabilities and limitations with task demands.
The guiding principle of HF/E is that capabilities and limitations must be, ideally, bigger
than the task demands. If the demands for the task are bigger than the worker’s
capabilities and limitations, the worker cannot properly perform the task, resulting in lost
productivity, injuries, and illnesses in the workplace (Das and Sengupta 1996). On the
other hand, if the worker's capabilities are too excessive, the worker may become bored
with performing the task. Thus, systems designers have to consider a worker’s
capabilities, restrictions, and limitations in designs.
Human in the System
The main problem for ergonomic systems designs is that workers’ capabilities,
limitations, backgrounds (education, ethnicity, culture, and experience), motivation levels
(needs), and abilities (skills) tremendously vary from worker to worker, which makes
fitting humans to systems complex. Thus, individual differences should be taken into
consideration by managers in the design stage of the system (Genaidy et al. 1999).
Managers are responsible for matching the worker to the system. Managers should
transform the organization into a more humanistic place while complying with the match
between worker and system (Oden 1999). Since management is generally incapable of
harmonization of all the work system’s elements, they should stimulate their employees
to participate actively in decisions and activities that directly affect themselves (Hendrick
and Kleiner 2002). Engineers and human factors specialists and ergonomists should
participate in decisions related to HF/E problems. They have great influence on
preventing HF/E problems arising from the complexity and uncertainties in

8
manufacturing (Broberg 1997). Unfortunately, organizational structure limits the
influence of human factors specialists and ergonomists in the system (Perrow 1983). Dul
and Neumann (2009) added more to Perrow by arguing that human factors specialists and
ergonomists do not have control over an organization’s budget and people in the
organization and that they are supposed to be protectors of safety and health, rather than
taking part in the creation or designing of systems.
Individual differences among humans (the most difficult element to change in the
system) can be categorized in three sections;
1. Physiological differences: body dimensions (height, weight, body segment lengths
and proportions, and disability), strength properties (muscle contraction and
energy storage), and endurance,
2. Psychological differences: inherent properties (intelligence, memory, attention,
adaptation, and reaction time), situation related factors (boredom, happiness, fear,
and satisfaction), and task related factors (fatigue and stress), and
3. Psychosocial differences: work related factors (workload, frequency, boredom, and
time schedule) and organization related factors (organizational demands and in-
situ interactions in the organization).
Environment of the System
Another important element of the system is the environment. The environment
includes both workplaces and the external environment that surrounds the organization. A
workplace can be defined as “a location where a person or persons perform tasks for a
relatively long period of time” (Eastman Kodak Company 1983). A good ergonomic

9
approach to workstation design strives for an adequate balance between the worker’s
capabilities and the work demands including workstation requirements (Black and Hunter
2003). Good HF/E designs comply with biomechanical, anthropometrical, and cognitive
features of workers to promote safety and efficiency in task performance.
Besides the physical workplace environment, the external environment has a great
impact on the system’s success. Open-systems such as manufacturing systems are always
in a relationship with their external environment. All systems are a part of another large
system; all systems consist of some subsystems, which make systems more complex.
Ignoring environmental factors in a system causes the failure of achievement of goals.
Human factors and ergonomics deals with social aspects of systems as well. If a
system includes humans, it is considered a sociotechnical system due to the interaction
between humans and the other elements of the system. Social systems are more than
collections of individuals and inherently include emotionality and unpredictability. The
sociotechnical approach, macroergonomics, helps managers to understand social
dynamics of systems in order to deal with the optimization of human-system interfaces.
Furniture manufacturing systems are, like all production systems, sociotechnical systems.
The perspective of sociotechnical systems assumes that every organization is made of at
least two subsystems; the social system and the technical system. Humans, the social
system parameter, use the technical system parameters like knowledge, technology, and
tools and equipment to produce beneficial goods or services for the other social system
parameter, the customer (Pasmore 1988).
Because manufacturing systems are open systems, change is everywhere (Oden
1999). Products the company produces, manufacturing processes managers follows,

10
equipment and tools employees use, the workforce the company employs, policies the
company is responsible to follow, and markets the company sells its products in are all
dramatically changing every minute (Oden 1999). Companies have to keep up with these
changes in order to survive. The most powerful external forces for organizational
transformation are (Pasmore 1988; Oden 1999):
xtrends in automation,
xeducation,
xchanges in social structure,
xlimited resources,
xincreasing competition,
xnew governmental requirements,
xincreased interdependence to other countries,
xthe shift from manufacturing industry to service industry,
xgreater concern for environmental issues,
xtechnological innovations,
xshifts in demographic characteristic of the workforce, and
xnew attitudes towards work.
Because environments of systems are continuously changing, organizations have
to be flexible so as to comply with these rapid and mostly unpredictable changes. If
organizations are not flexible enough to change, they can have a difficult time handling
difficult environmental factors and reaching their goals in such a competitive world. On
the other hand, the same factors can give flexible organizations the opportunity to
achieve their goals.
Feedback in the System
Fast, accurate, and continual feedback from systems, particularly from employees,
is essential for companies to develop their knowledge and expertise on HF/E while
increasing the efficiency and productivity and reducing occupational injuries and
illnesses (FMSAH and ILO-Safework 2002). In a manufacturing system, feedback,

11
considering HF/E, can be obtained from injury forms, absenteeism forms, and employee
turnover data. Internal and external customers and other stakeholders can supply
beneficial feedbacks as well (Genaidy et al. 1999). The dilemma is that designers,
managers, and human factors specialists and ergonomists get feedback after the design is
implemented, but it is too late to use the feedback for the design (Perrow 1983).
Entropy
It is impossible to create a perfect system that works forever without any problem.
As a rule of nature, systems degenerate sooner or later, but successful designs decrease
the amount and severity of the problems that cause degeneration. Therefore, systems
should be managed by individuals that have the knowledge of entropy and HF/E.
Preventing or solving problems before they happen is the best way to handle entropy.
Managers with broad knowledge and capabilities can find solutions immediately, which
guarantee the integrity of the system.
Motivations for the Study
The furniture manufacturing industry is one of the industries that needs to
establish a culture based human factors and ergonomics due to the high existence of
stressors causing occupational injury and illness. In the perspective of physical stressors,
the furniture manufacturing industry requires considerable physical work demands as a
consequence of a great deal of manual handling of heavy, bulky, and awkward materials
and manual tasks such as sanding, rubbing, stapling, and spraying (Mirka 2005). Even
though the need for HF/E in the furniture manufacturing industry is great, it is not applied

12
as much as it deserves to be. In this problem statement section, the reasons why HF/E is
not applied as much as it should be will be discussed.
Ignoring Human Factors and Ergonomics
Human factors and ergonomics are, unfortunately, ignored in the furniture
manufacturing industry. A work environment survey by the Swedish Union for technical
and clerical employees and the salaried employees’ union was conducted in 2007 to
better understand the opinions of safety representatives and trade union members about
the problems in physical and psychosocial work environments (Andersson 2008). The
survey showed that white-collar workers had a shortcoming of interest and supervision
about HF/E, some workplaces had been poorly designed, and approximately 20 percent
of the companies did not comply with Swedish laws. Namely, white-collar workers were
basically unaware of HF/E. If they were aware, they just ignored HF/E. However,
ignoring HF/E in organizations can cause a myriad of problems for both the organization
and its elements. For instance, poor design can result in a decrease in productivity and an
increase in health problems (Black and Hunter 2003), which results in the organization’s
failure to achieve its potential (Pulat and Alexander 1991). If HF/E is ignored in
workplaces, systems can encounter problems that include but are not limited to the
following (Alexander and Pulat 1985; Pulat and Alexander 1991; AFMA and NCDOL
2003):
xIncreased probability of accidents and errors,
xIncreased injuries, sprains, and strains,
xIncreased lost time, rest breaks, absenteeism, and labor turnover,
xHigher medical costs,
xHigher material waste and cost,
xLess production output,

13
xLower product quality, and
xFrequent worker complaints.
The cost of even a simple mistake can be extremely high, especially when it
occurs over a long period (Beevis and Slade 2003). The solution is to redesign the system
by considering HF/E knowledge. Redesigning is also the logical solution because the
costs of redesigning workplaces, in comparison, are often far less expensive than even the
cost of a single injury (Pulat and Alexander 1991). Human factors and ergonomics is
more than something that is nice; it is a necessity.
Management capable of changing the culture to become more open to HF/E in
most organizations does not seem to be positively motivated to apply HF/E (Dul and
Neumann 2009) because of either misperception or unawareness of HF/E.
Being Unaware of Human Factors and Ergonomics
Human factors and ergonomics awareness has a substantial impact on the
industry, organization, management, employees, and overall well-being the system
(Sundstrom 2000; Vavra 2003; Westgaard and Winkel 2000); however, management, in
general, is not really aware of the advantages of HF/E. Managers in the industry have
some understanding of HF/E, but most of them are not sure how to deal with problems
resulting from the lack of HF/E interventions (Dolhy 2006). Indeed, unawareness of
HF/E discipline is observed not only among managers, but also among employees,
employers, and the rest of society. A survey conducted by the Opinion Research
Corporation revealed that the majority of office workers in the U.S. believed that they
knew the definition of HF/E; however, few of them were able to accurately define it

14
(Steelcase 2006). Although there was confusion over the definition, those workers were
aware of the benefits of HF/E.
There is another dimension in awareness: understanding. Awareness and
understanding do not have the same meaning. The public awareness of the word HF/E
has increased over the past few decades, but public understanding of what HF/E actually
means has been limited and confused (Budnick 2001).
Misperceptions of Human Factors and Ergonomics
Before the discussion of how HF/E is misperceived, providing the reasons why it
is misperceived can be beneficial for comprehensive understanding. There are a few
reasons for misperception such as lack of cost-benefit analysis, inadequate documentation
of HF/E interventions, and poor communication between scientists and businessmen.
Poor Cost-Benefit Analyses: “Needing to Talking with the Language of Money”
Cost-benefit analysis enables managers to justify an investment, whether it
improves the organization’s profit, competitiveness, and survival ability (Hendrick
1996a). The justification of the costs and benefits of HF/E programs is an essential
management tool for an organization’s future steps (Douphrate and Rosecrance 2004).
The cost-benefit analysis enables decision-makers to justify an HF/E program in
business-language: money. That HF/E is “the right thing to do” is not a sufficient reason
for managers to apply it in their organizations (Hendrick 1996b); it has to be gainful.
In general, managers are not willing to spend money unless there are clear
economic benefits (Hendrick and Kleiner 2002). Human factors and ergonomics is,
inherently, highly profitable; but, the problem is that scientists cannot exactly transform

15
their research into “the language of money.” Unless the literature focuses on the
economical benefits of HF/E programs or unless human factors specialists and
ergonomists learn and use “the language of business,” managers cannot realize the
importance of HF/E.
Talking with the business- or money-language is meaningful for management
because an organization’s survival is dependent on money (Vitalis et al. 2001). However,
talking with “the language of money” is not easy due to the difficulty of cost and benefit
calculation. Indeed, costs can be easily calculated, but benefits cannot. The complexity of
calculation is caused from the difficulty of the explanation of benefits. Benefits may be
qualitative or quantitative. The conversion of qualitative benefits (such as healthier and
more satisfied workforces, safer workplaces, and higher quality products) into
quantitative benefits (money) causes researchers difficulty. Moreover, the dimension of
the benefits makes the calculation harder. For example, benefits can be for today or for
the future, and the impact of benefits can be direct or indirect.
Lack of Communication: Poor Literature Documentation
Another problem for not embracing an HF/E culture in an organization is the lack
of communication between scientists and management, and possibly employers. Lack of
literature and lack of scientific evidences to explain the need for HF/E make
communication difficult (Meg 1999). As a broad problem, the U.S. wood products
industry, including the furniture manufacturing industry, has not been very attentive to
HF/E opportunities, so little research has been done on the topic of HF/E (Gazo et al.
2002). Lack of literature related to the financial aspect of HF/E (Beevis and Slade 2003)

16
is one of problems that motivated researchers to conduct this research. If the literature is
reviewed, it can be clearly seen that the benefits of HF/E have not been well documented.
Poor documentation results in inadequate reorganization, weak support, and poor
endorsement of HF/E by the leaders of both business and government (Hendrick 1996b).
Hendrick has blamed himself and his scientist colleagues for inadequate documentation
and publication on the cost-benefit analyses of their ergonomic research (Hendrick
1996a). In his 1996 Human Factors and Ergonomics Society Presidential Address,
Hendrick introduced a variety of ergonomics interventions resulting with financial
benefits. He emphasized that the HF/E community must better document and spread cost
and benefit awareness of HF/E programs (Hendrick 1996b).
Besides, human factors specialists and ergonomists generally publish their
research in HF/E related journals. Unfortunately, managers follow these journals less
than business and/or management journals, which limits the possibility to introduce them
to the benefits of HF/E (Dul and Neumann 2009).
As a result of the lack of awareness, poor cost-benefit analyses, and poor
documentation of HF/E programs, managers in the industry generally misperceive HF/E.
For example, some managers in industry think that HF/E is only related to safety and
health issues. Most of the general public and management have the insight that HF/E is
just about work-related musculoskeletal disorders; and prevention of these disorders
results in heavy financial burdens for companies (Dul and Neumann 2009). In an
operator’s view of point, HF/E can be nothing more than “common sense” (Hendrick
1996b).

17
The Perception That Human Factors and Ergonomic is Costly
The lack of awareness among managers causes the perception that HF/E is costly
(Sundstrom 2000; Dolhy 2006), particularly for small businesses (Vavra 2003). Hendrick
(1996b) asks, “Why is it that both industry associations and members of Congress
sometimes view us as simply adding an additional expense burden and, thus, increasing
the costs of production and thereby decreasing competitiveness?”. It is obvious from
Hendrick’s quote that HF/E is perceived as nothing other than a financial burden to
companies. Mirka (2005) expressed in his paper, explaining a voluntary HF/E program in
the furniture manufacturing industry, that management did not want to be volunteer any
HF/E program because they thought Occupational Safety and Health Administration
(OSHA) would enforce heavy liabilities on them if researchers found HF/E related
problems. Mirka’s paper shows that managers in the industry know of current problems
and admit that HF/E is a beneficial, preventative discipline; however, they are not willing
to embrace HF/E in their organizations because of its misperceived heavy financial
burden.
Human factors and ergonomics is in danger of losing its identity as well (Vitalis et
al. 2001). Managers often associate HF/E with health issues and related health costs such
as costs of absenteeism and compensation caused from occupational injuries and illness
instead of with organizational effectiveness (Dul and Neumann 2009). As long as the
perception is that HF/E focuses on the human needs in workplaces to promote health and
well being rather than the efficiency and productivity of the organization, traditional
management will not be willing to waste their resources on HF/E (Vitalis et al. 2001).

18
To summarize, misperceptions caused by a lack of awareness, poorly documented
literature, and poor communication between scientists and business leaders result in less
commitment to HF/E in the furniture manufacturing industry. However, managers should
realize that HF/E tools and techniques are highly beneficial for systems. Therefore,
individuals responsible for HF/E should give greater efforts to understand the business
aspects of the organization so that they can influence their organization’s strategies.
Scientists should mention the economical aspects in their research results. Introducing
HF/E via well documented cost-benefit analyses helps to spread Hendrick’s expression of
“good ergonomics is good economics” (Hendrick 1996b).
Poor Management Commitment and Employee Involvement
Management commitment and employee involvement are complementary and
essential elements for implementing an HF/E program in an organization. Without their
support, HF/E programs are likely to fail. Human factors and ergonomics offers a
wonderful common ground for management and employee collaboration. Managers can
get benefits if production costs reduce and the productivity improves, and meanwhile,
employees can get benefits if safety, health, comfort, usability of tools and equipment,
and overall improvement of work life quality (Hendrick 1996b).
If managers realize the benefits of HF/E, they will probably be more interested in
HF/E (Hendrick and Kleiner 2002). Especially, financial benefits have an encouraging
impact on managers for commitment to HF/E. If managers experience cost reduction
resulting from HF/E programs, their interest will immediately increase. The benefits of

19
HF/E are not limited only in financial conditions. Social benefits of HF/E also encourage
mangers to support HF/E programs. The more managers that are aware of and use of
HF/E, the more easily they can reach their strategic business goals (Dul and Neumann
2009).
Management Commitment
One of the ultimate objectives of this study was to encourage managers for
initiation of HF/E programs, if there is not one, and to show them the advantages of
commitment to these programs. Researchers have searched to solve problems derived
from ergonomically poor designs and to provide training for workers. However, efforts
are ineffective when they are not supported by the management. The success of these
programs requires participation from all levels throughout an organization.
In highly centralized systems, a few high level individuals make the decisions
while lower-level supervisors and employees have minimal input in the decisions
affecting their jobs (Hendrick and Kleiner 2002). A study in the sawmill industry found
that managers responsible for planning, organizing, and leading tended to use autocratic
and authoritarian management styles in their organization instead of democratic and
participative management styles (Trask et al. 2009). Like the sawmill industry,
management in the furniture manufacturing industry is inherently highly centralized;
therefore, management commitment is critical to establish a culture that values the
human. “Real management commitment,” not just words, increases the probability of the
overall success of any HF/E programs (AFMA and NCDOL 2003; Hendrick 2003). For
example, a joint project between the Finish Ministry of Social Affairs and Health and

20
International Labor Organization (ILO)-SafeWork Program revealed that several factors
affected the productivity of an organization, but management commitment was the most
important factor for high productivity (FMSAH and ILO-Safework 2002). The American
Furniture Manufacturers Association (AFMA) lists some of the ways that furniture
manufacturer managers can demonstrate their commitments to HF/E by (AFMA and
NCDOL 2003):
xUnderstanding the elements involved in an effective HF/E program,
xDeveloping and instituting clear goals and objectives for the program,
xEnsuring adequate education and training for employees,
xEstablishing a system of responsibility and accountability at all levels,
xEncouraging participation and involvement at all levels,
xAllocating resources to address HF/E issues within the organization,
xStriving to identify and eliminate ergonomics hazards in work operations,
xMaintaining a system to address physical complaints promptly and effectively,
xIntegrating safety and health as a value in the workplace while partnering with
productivity and quality issues,
xDefining a system for effective documentation and program evaluation, and
xDeveloping a procedure for equipment evaluation prior to purchase and
installation.
Employee Involvement
A successful integration of HF/E into the overall manufacturing processes
depends not only on management commitment but on employee participation as well
(AFMA and NCDOL 2003; Tornstrom et al. 2008). A human is the most important asset
of an organization, so management should institute a wider level of participation to utilize
this asset (Genaidy et al. 1999; Hendrick and Kleiner 2002). Participation in
manufacturing processes, such as creation, design, implementation, improvement, and
assessment of tasks, tools, equipment, workplaces, and environment, promotes the feeling
of individual ownership and the sense of commitment to supporting programs, which is

21
motivating and beneficial to both individuals and the organization (Robertson 2001;
Pehkonen et al. 2009). Employees should be given opportunities to discuss and address
problems in their jobs. Success requires team effort among the people in the organization
(MacLeod 1995).
Employee involvement at all organizational levels in order to establish and
maintain an organization culture based on HF/E is called participatory ergonomics, or
participatory human factors and ergonomics in a broader point of view. For participatory
ergonomics, most of the encyclopedias and HF/E handbooks have quoted Wilson’s
(1995) definition; “The involvement of people in planning and controlling a significant
amount of their own work activities, with sufficient knowledge and power to influence
both processes and outcomes in order to achieve desirable goals.” As understood from
the definition, conscious involvement is vital for the success of an organization.
There are several factors for the success in the participatory approach. First of all,
an HF/E program is only effective when the employer and management welcome it. For
the success of the participatory program, they should play an active role in analysis,
design, implementation, and control. Another necessity for success is the opportunity
level for involvement provided by the management. The more managers provide the
opportunity for employees, the more employees will participate in the activities and
decisions. The participation is more favorable when the number of participants is high
(Noro and Imada 1991; Tornstrom et al. 2008) and involves people from all levels and
functions (AFMA and NCDOL 2003). Taking an HF/E program as a team approach is
required for the successful organization (Keller 2008). Lastly, availability of resources
such as knowledge, tools, equipment, and power are required to achieve quality

22
improvement in processes and outcomes and to enhance organizational effectiveness
(Nagamachi 1995).
Occupational health teams or practitioners should participate in the HF/E
programs as well (Hignett et al. 2005). In addition to these safety-hygiene personnel and
health care providers, people from all over the organization, such as human resource
personnel, engineering personnel, maintenance personnel, and even union leaders, should
be involved in these programs (Keller 2008).
Participatory HF/E groups are the same as quality circle teams. These groups are
highly motivated to find solutions to their own problems, redesign their own workplaces,
and reform their own organizations for themselves (Nagamachi 1995). Participatory
HF/E provides employees with the opportunity of learning and developing new skills
through collaboration with their colleagues. Some of the advantages of participatory
HF/E are less absenteeism, less compensation costs, increased productivity, improved
communication between employees and management, and reduction in stressful risk
factors (Nagamachi 1995; Hignett et al. 2005). As a result of participatory HF/E,
employee knowledge and awareness increases, so the ability to handle HF/E problems
improves (Pehkonen et al. 2009).
While managers can be involved in establishing and implementing HF/E
programs, employees can demonstrate their commitment by (AFMA and NCDOL 2003):
xIdentifying HF/E issues,
xParticipating in control measure development and implementation,
xContributing to HF/E teams or committees,
xReporting early signs and symptoms of problems.

23
CHAPTER II
FURNITURE MANUFACTURING INDUSTRY OVERVIEW
Furniture Manufacturing Industry in the United States
Furniture is, traditionally, made from solid wood. Hardwoods such as oak,
hickory, birch, beech, ash, and walnut and softwoods like pine, cedar, redwood, fir, and
larch are used as raw materials to manufacture furniture. However, the trend for raw
materials in the current furniture manufacturing industry is changing from solid wood
material to other materials such as metal, glass, plastics, and rattan. The trend results
from the high furniture demands, excessive material costs, shortage on quality and
quantity of solid wood materials, durability problems, aesthetics, and many others. The
most common materials used in the U.S. furniture manufacturing industry are metal and
wood.
Industries in the furniture and related product manufacturing subsector produce
furniture and related products such as mattresses, window blinds, cabinets, and fixtures
by the cutting, bending, molding, laminating, and assembly of materials (Census Bureau
2003). Because furniture is usually made from several materials, the classification based
on the type of furniture is more useful than the classification based on the material used.
For example, some wood, metal, foam, and fabric are used to make a sofa, but the sofa is
not classified as a wood sofa or a metal sofa, but an upholstered sofa. The place the sofa
is used does not change the classification as well. For example, an upholstered sofa is still

24
considered household furniture although it may be used in a hotel room or a business
office (Census Bureau 2003).
The North American Industry Classification System (NAICS) is a classification
system that has replaced the U.S. Standard Industrial Classification (SIC) system in 1997.
The Federal statistical agencies use NAICS for the collection, analysis, and publication of
economic statistics. They no longer use the SIC, and there will be no further revisions of
the SIC system. The furniture and related product manufacturing subsector consists of
three NAICS coded industry groups:
xHousehold and Institutional Furniture and Kitchen Cabinet Manufacturing (NAICS
3371),
xOffice Furniture (including Fixtures) Manufacturing (NAICS 3372),
xOther Furniture Related Product Manufacturing (NAICS 3379).
This research only covers the furniture and related product manufacturing
subsector (NAICS 337). Before NAICS codes, SIC codes were used to classify
establishments. NAICS 337 codes match with SIC 25 codes (Furniture and fixtures) (see
Appendix 1 for the compatibility). There are some establishments in different SIC codes
such as SIC 24 (Lumber and wood products), SIC 39 (Miscellaneous manufacturing
industries), and SIC 57 (Home furniture, furnishings, and equipment stores).
Furniture Manufacturing Industry Statistics
The furniture and related product manufacturing industry (NAICS 337) is an
important industry with 23,565 establishments (BLS 2009a) and 544 thousands
employees (BLS 2009b) in 2007. The industry added $46 billion to the U.S. economy in

25
2006 (Census Bureau 2009). Unfortunately, the U.S. furniture market is facing a
challenging period because of a financial crisis, growing unemployment, falling sales,
and high material costs (Ince et al. 2007).
The furniture manufacturing industry is suffering from the globalization or global
competition in recent years (Pasmore 1988; Ince et al. 2007; Drayse 2008; Lihra et al.
2008). Firms have outsourced production to other countries where the costs are relatively
low. For example, half of the furniture demand in the U.S. is met from China (Ince et al.
2007; Drayse 2008). As a result of the devastating competition, some small companies
have faced an end to their businesses. Some states, such as Mississippi, Alabama, and
North Carolina, have higher dependency on the furniture manufacturing industry; hence,
these vulnerable states are severely affected from the global competition. For example, 40
furniture plants in North Carolina were closed from 2001 to 2003, which sharply dropped
furniture employment trends (Ince et al. 2007). Because the furniture manufacturing
industry is fairly labor intensive, these problems have negatively affected both social and
economic structures of the nation (Ince et al. 2007). In addition to global competition,
national competition, governmental regulations, and internal ineffectiveness increase the
pressure on companies (Pasmore 1988). As a result, financial crisis, falling sales,
expensive material costs, national and international competitions, governmental
regulations, and internal ineffectiveness cause the number of businesses (Figure 1) and
employment (Figure 2) to decrease in the furniture and related product manufacturing
industry.
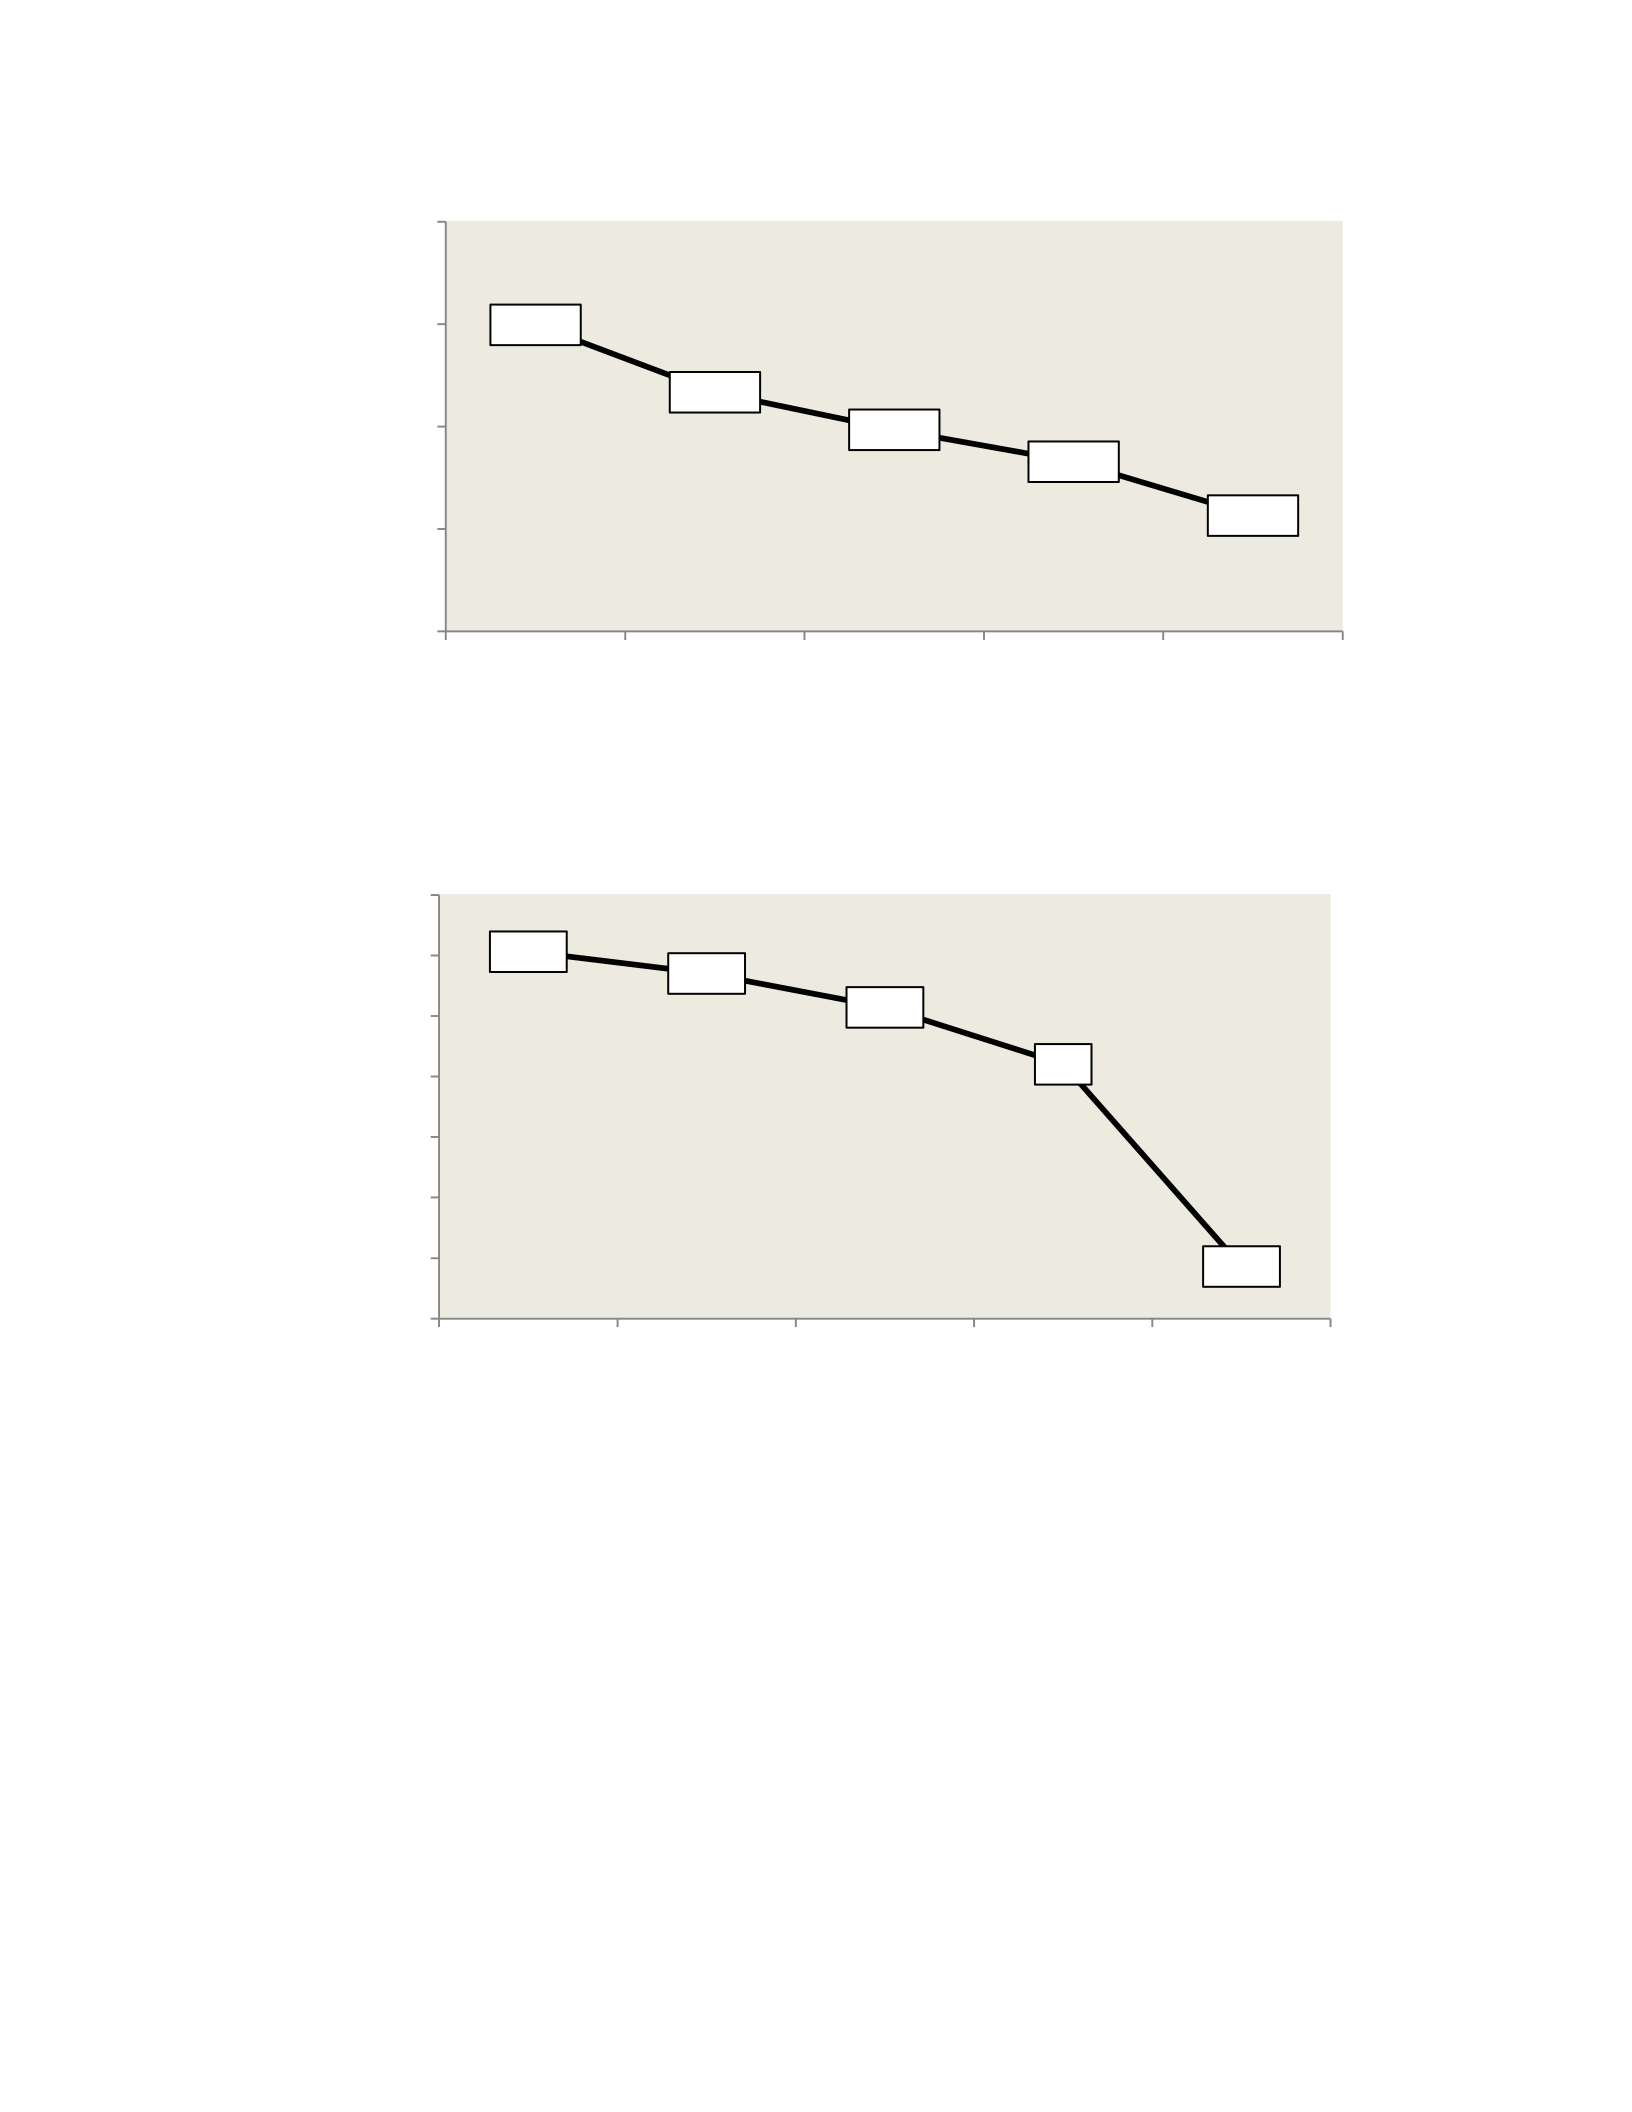
26
Figure 1 Number of establishments (thousands) in NAICS 337 Furniture and related
product manufacturing, Private Industry, All the U.S. from 2003 to 2007
Figure 2 Number of employees (thousands) in NAICS 337 Furniture and related product
manufacturing, Private Industry, All the U.S. from 2003 to 2007
Occupational Injuries and Illnesses Statistics
The furniture industry is characterized by a higher number of occupational
injuries. There are many risk factors in the furniture industry, leading to millions of
people being seriously injured and even dying. According to the recent data by the U.S.
24.496
24.167
23.984
23.828
23.565
23.0
23.5
24.0
24.5
25.0
2003 2004 2005 2006 2007
Establishments (Thousands)
570.3 568.5
565.7
561
544.3
540
545
550
555
560
565
570
575
2003 2004 2005 2006 2007
Employees (Thousands)

27
Department of Bureau of Labor Statistics (BLS), there were total 34.5 thousand
recordable cases in the furniture and related products manufacturing industry (NAICS
337), 32.7 thousand of which were occupational injuries and the remaining 1.8 thousand
were illnesses (BLS 2009b). In the total private industry, there were a total of 4 million
recordable cases, of which 3.8 million were occupational injuries. Of the rest of the cases,
0.2 million were illnesses. As a reminder, the rates may be higher due to under-reporting
of minor injuries or company-paid cases.
The rate of total recordable injury and illness cases in the furniture and related
products manufacturing industry in 2007 was 6.7 cases per 100 full-time workers, which
was fairly higher than the rate of total recordable injury and illness cases in the total
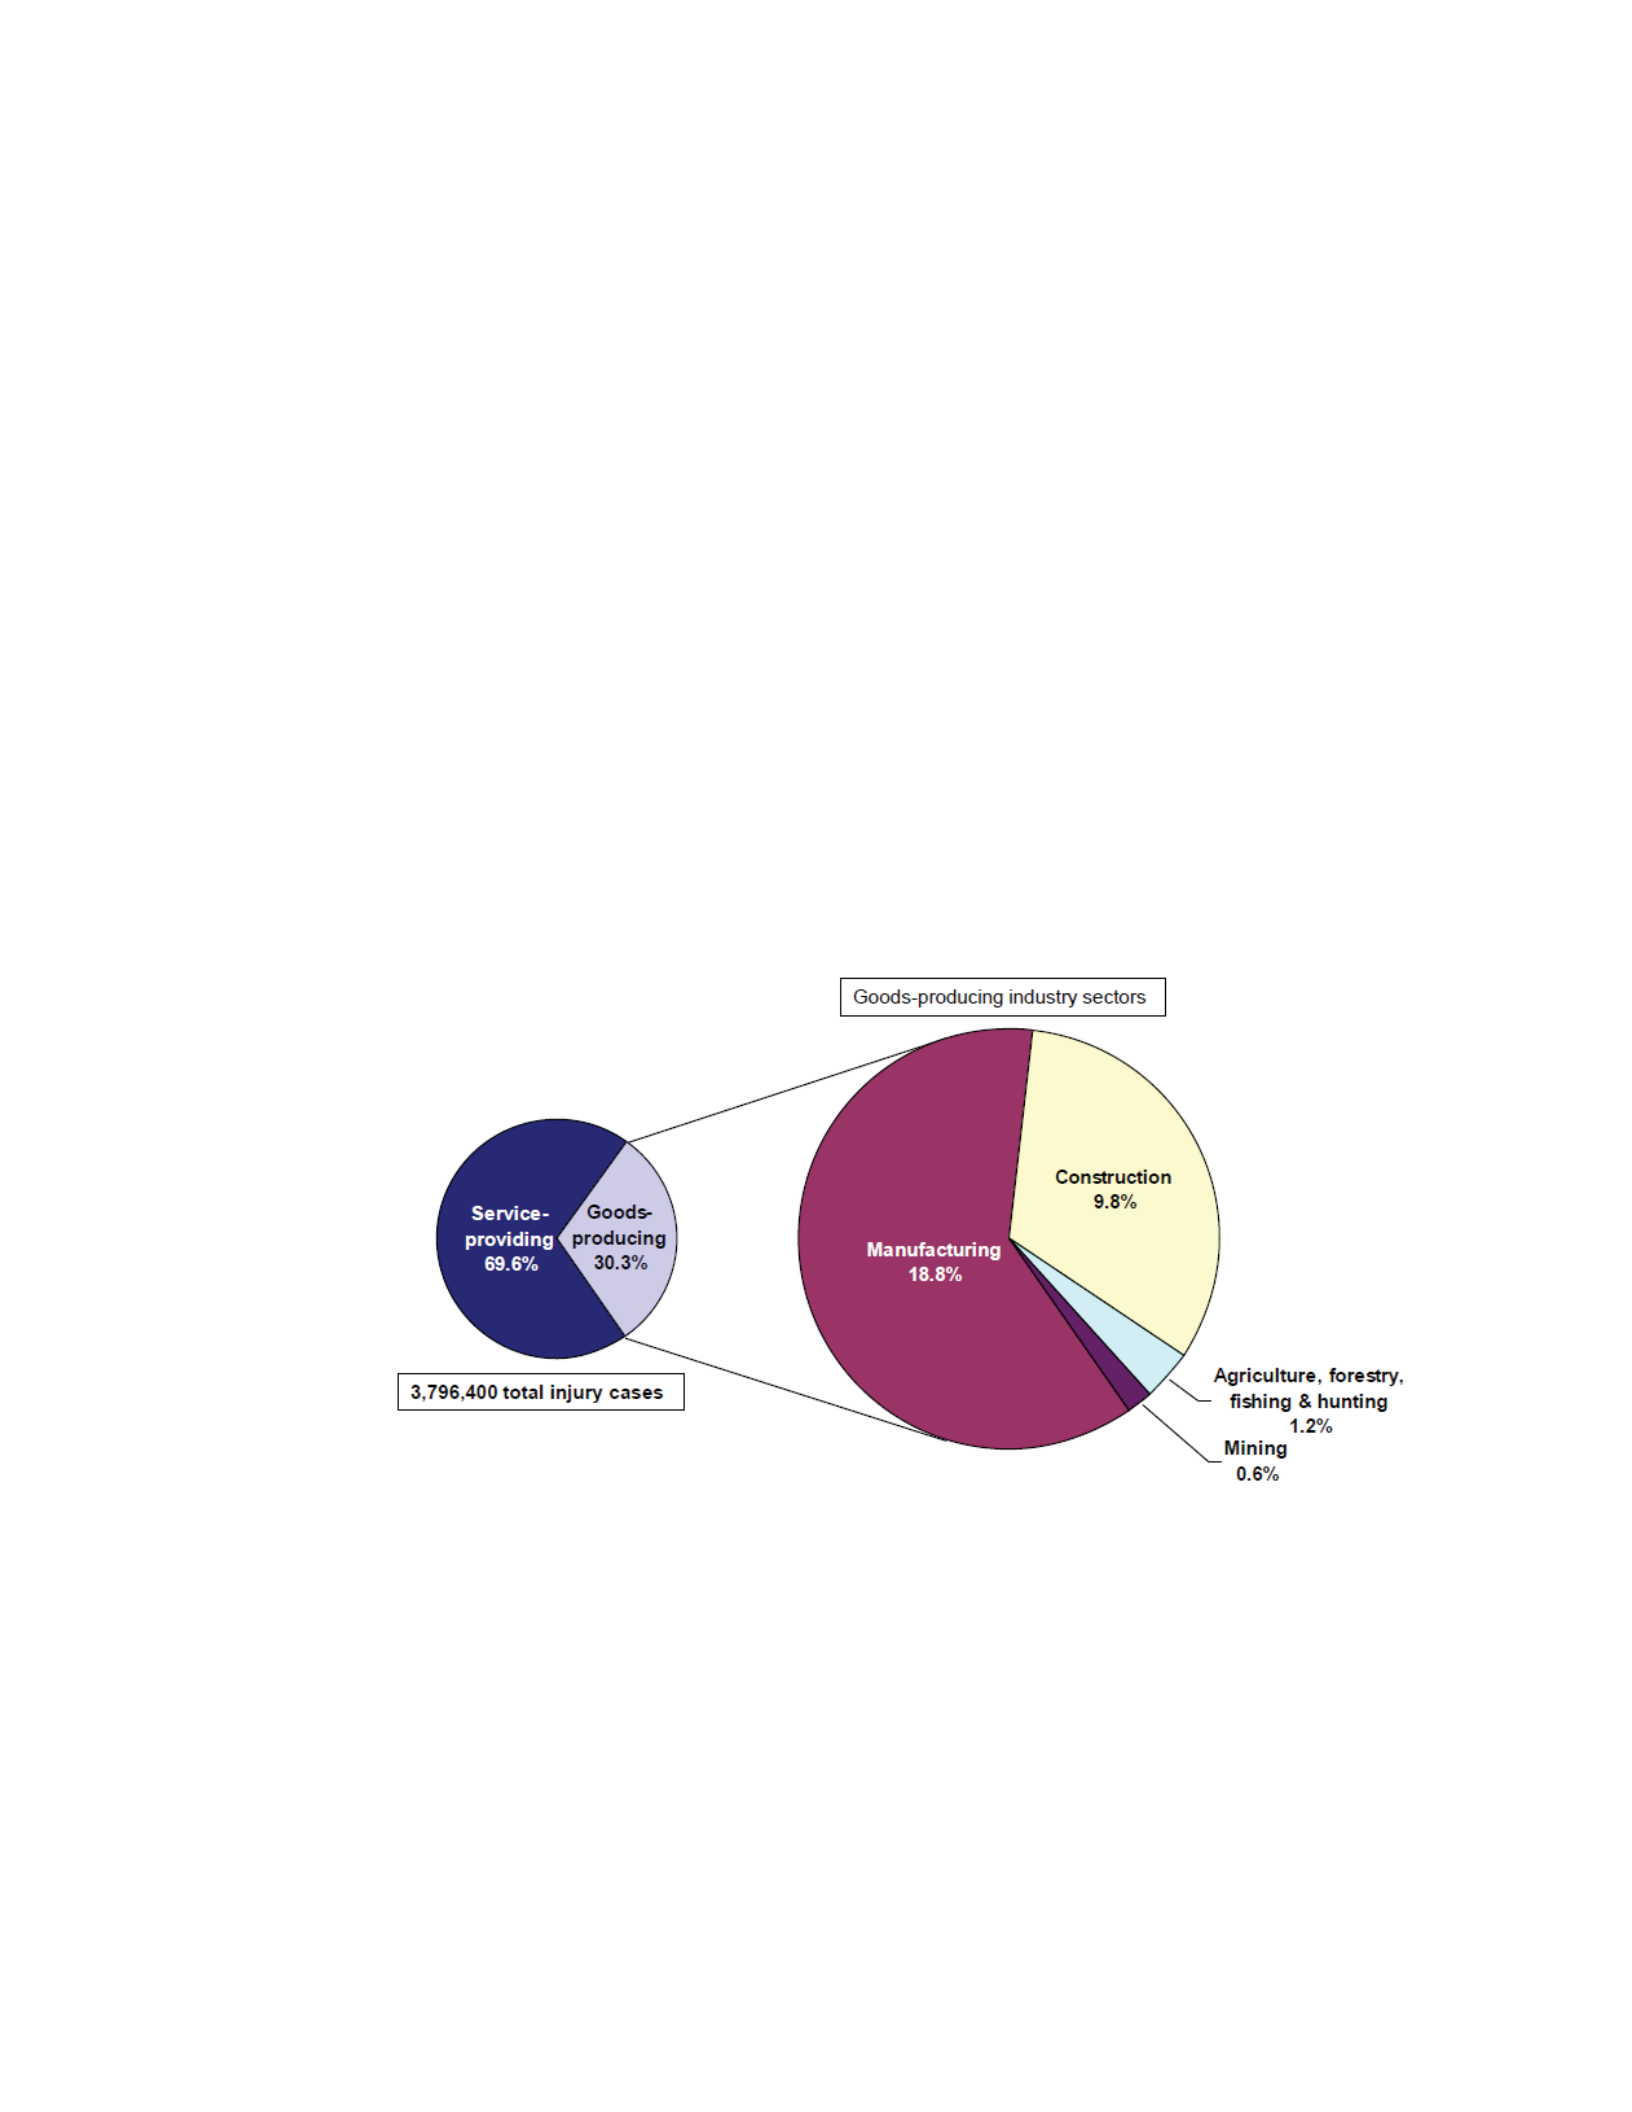
private industry in 2007: 4.2 cases per 100 full-time workers (BLS 2009b). The summary
statistics of the occupational injuries, illnesses, and fatalities in the furniture,
manufacturing, goods producing, service producing, and total private industry (Table 1)
shows that fifty four percent of the occupational cases in the furniture manufacturing
industry resulted in either days away from work (DAFW) or job transfer or restriction
(JTR). In 2007, 8.2 thousand cases resulted in days away from work for recuperation and
10.2 thousand cases resulted in transferring to another job and restriction duties at work.
The remaining 16 thousand injuries and illnesses were called other recordable cases that
28
Table 1 Numbers and rates of fatal and nonfatal occupational injuries and illnesses, Private Industry, All the U.S., 2007
Industry Employment
INJURIES & ILLNESSES
Recordable cases Cases with DAFW & JTR Other
recordable
cases
FATAL
Total Injuries Illnesses Total DAFW JTR INJURIES
N%N%N%N%N%N%N%N*R*
Goods-producing 23500.5 1236.1 5.4 1152.2 5 83.8 0.4 665.3 2.9 349.4 1.5 315.8 1.4 570.8 2.5 2372 7.8
Manufacturing 14071.4 783.1 5.6 711.9 5.1 71.1 0.5 427.1 3 187.2 1.3 239.9 1.7 356 2.5 400 7.1
Furniture 544.3 34.5 6.7 32.7 6.3 1.8 0.4 18.4 3.6 8.2 1.6 10.2 2 16 3.1 6 0.1
Service-providing 91332.9 2766.6 3.8 2644.1 3.7 122.5 0.2 1370.7 1.9 809.4 1.1 561.3 0.8 1396 1.9 2740 2.9
Total private Industry 114833.4 4002.7 4.2 3796.4 4 206.3 0.2 2036 2.1 1159 1.2 877.2 0.9 1967 2.1 5112 4.1
Furniture: Furniture and related product manufacturing
N: Number (thousands), N*: Number
%: the rate of cases per 100 workers, R*: the rate of fatal occupational injuries per 100,000 employed workers
Employment: Annual average employment (thousands), in 2007,
DAFW: Cases with days away from work,
JTR: Cases with job transfer or restriction,
Industry codes:Service providing: SP1AAA, Goods providing: GP1AAA, Manufacturing: GP1MFG, Furniture and related product manufacturing:
NAICS 337
29
did not result in time away from work. Cases with job transfer or restriction involve
shortened work times and temporary job changes and/or restrictions on regular tasks.
The rate of illnesses in manufacturing was 0.5 cases per 100 full-time workers.
The illness rate for the furniture and related products manufacturing industry (0.4) was
about two times higher than that of the national average (0.2 cases).
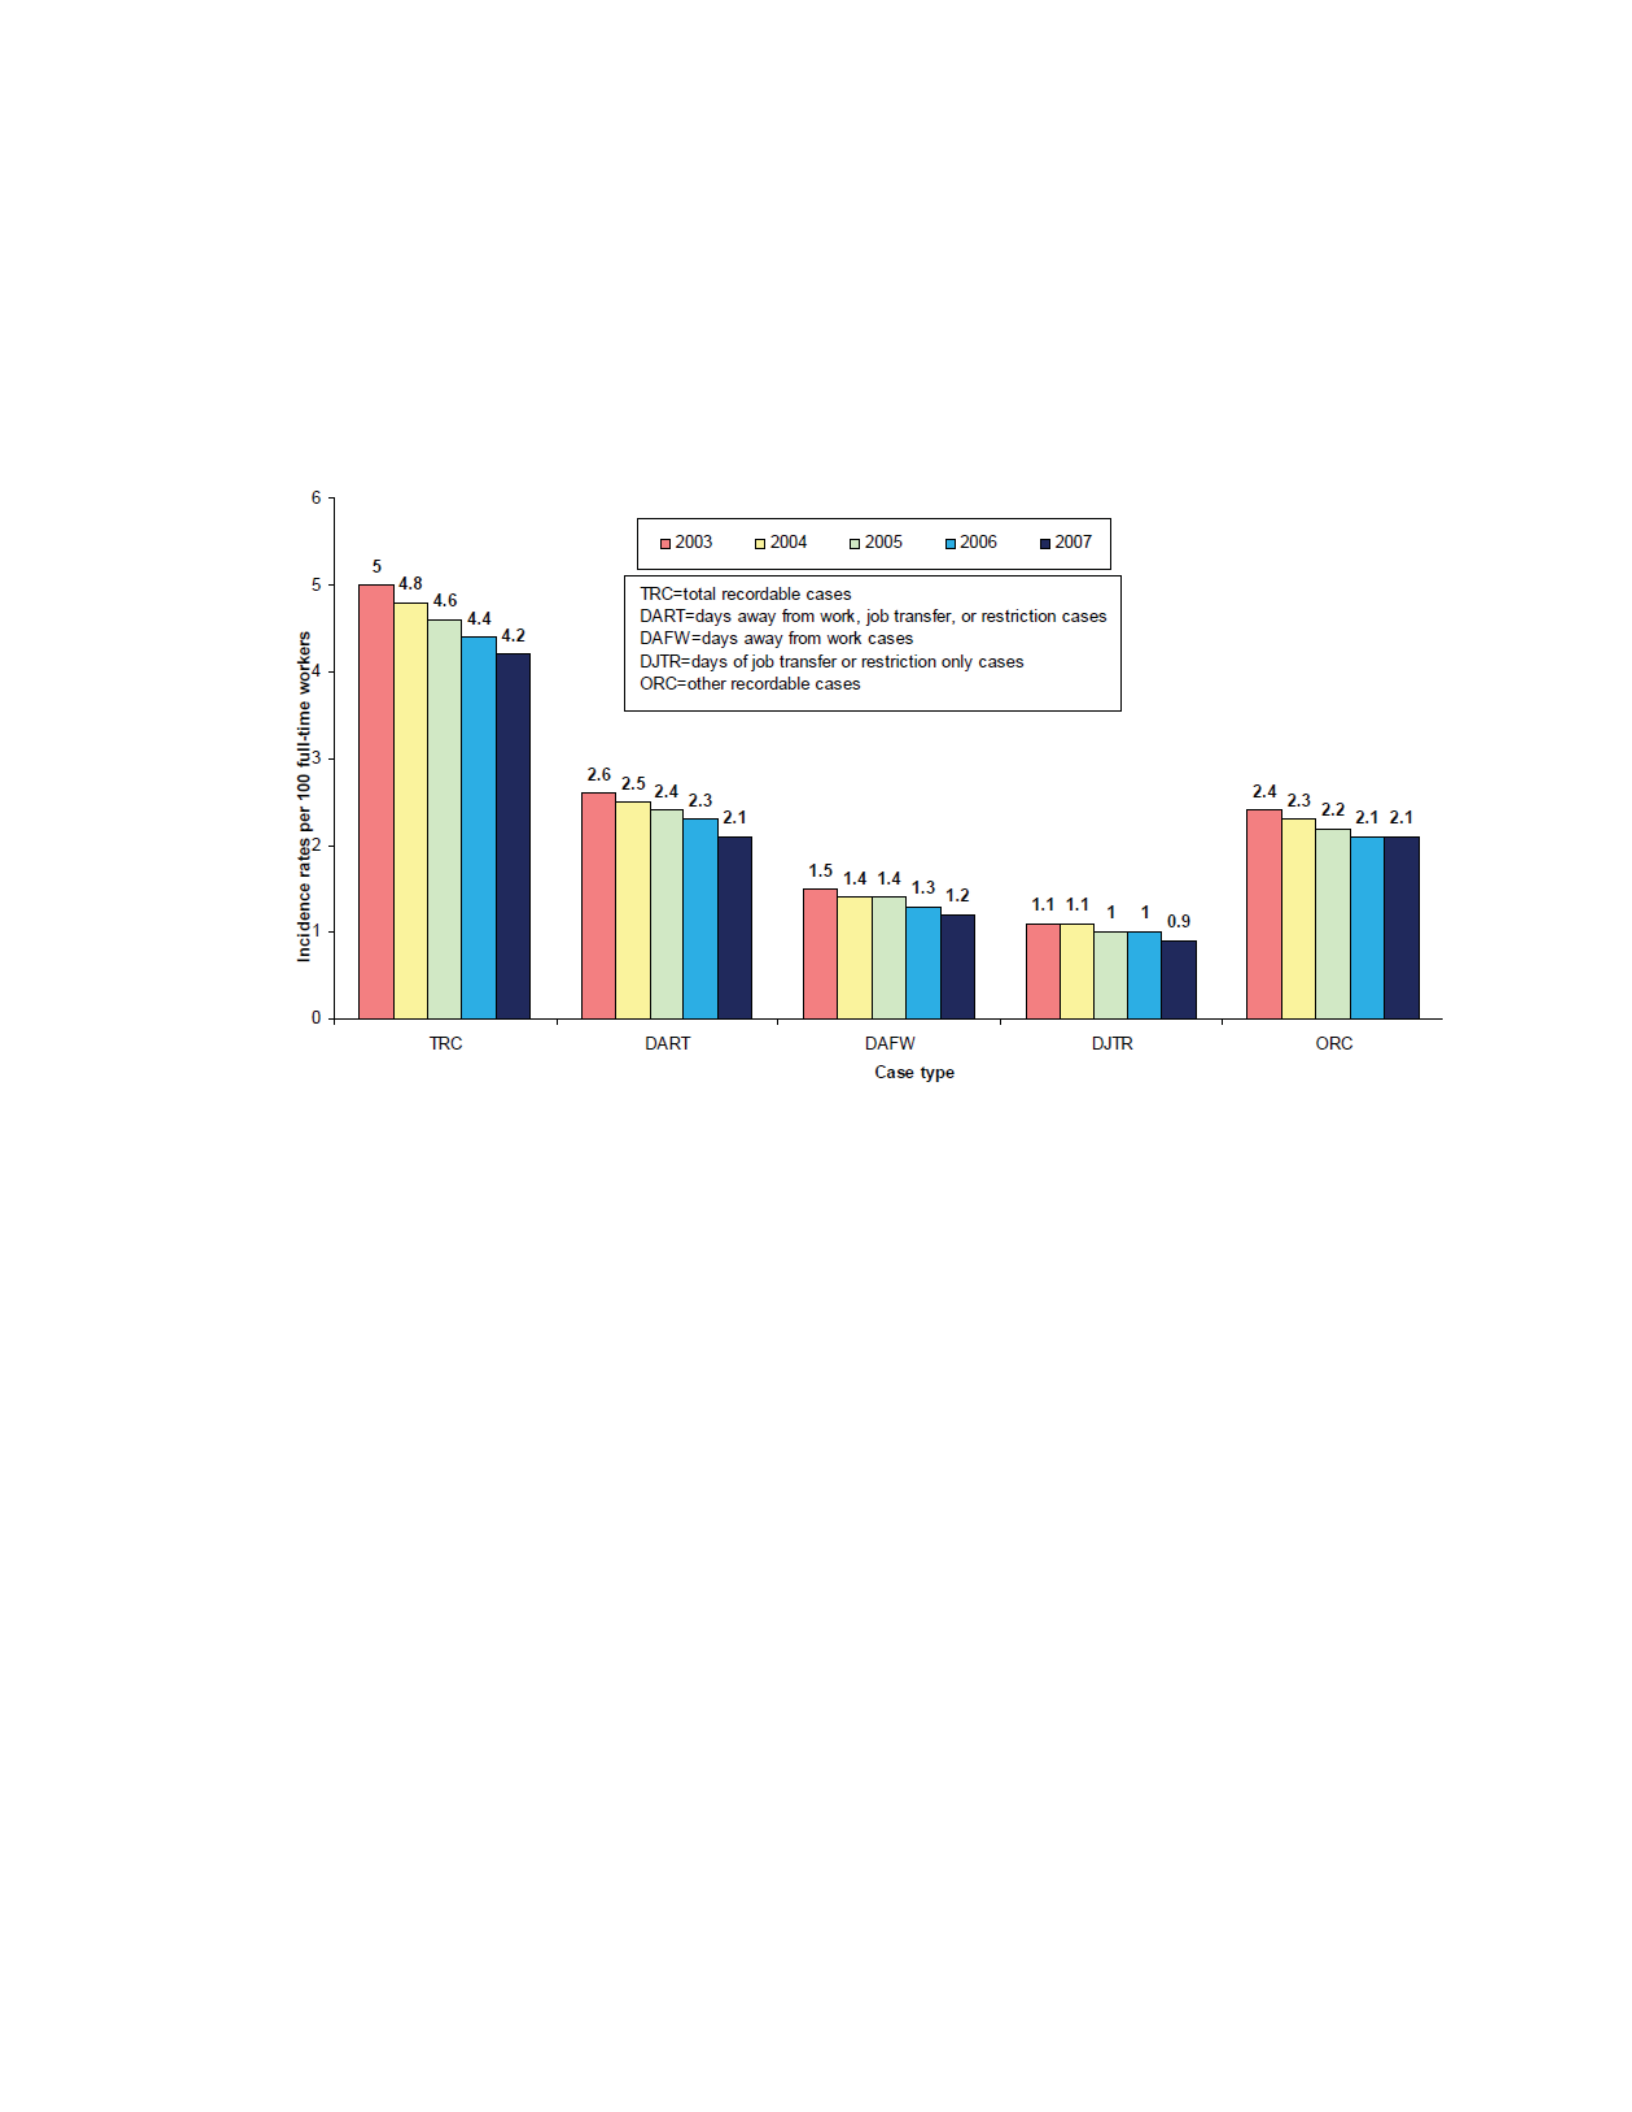
About one over third of all injury cases in private industry in 2007 occurred in the
goods producing industry. Injury cases in the manufacturing industry were approximately
60 percent of the goods producing industry; thus, manufacturing accounted for 18.8
percent of all private industry illness cases (Figure 3).
Figure 3 Distribution of nonfatal occupational injuries by good producing private
industry in 2007
Every year, millions of Americans experience injuries, illnesses, and even deaths
at workplaces. The good news is that trend is going down. As can be seen in Figure 4,
30
total recordable cases, days away from work, job transfer, or restriction cases, days away
from work cases, days of job transfer or restriction only cases, and other recordable cases
are in the trend of reduction from 2003 to 2007 (BLS 2009b).
Figure 4 Nonfatal occupational injury and illness incidence rates by case type, private
industry, 2003-2007
The same trend can be observed in the furniture and related products
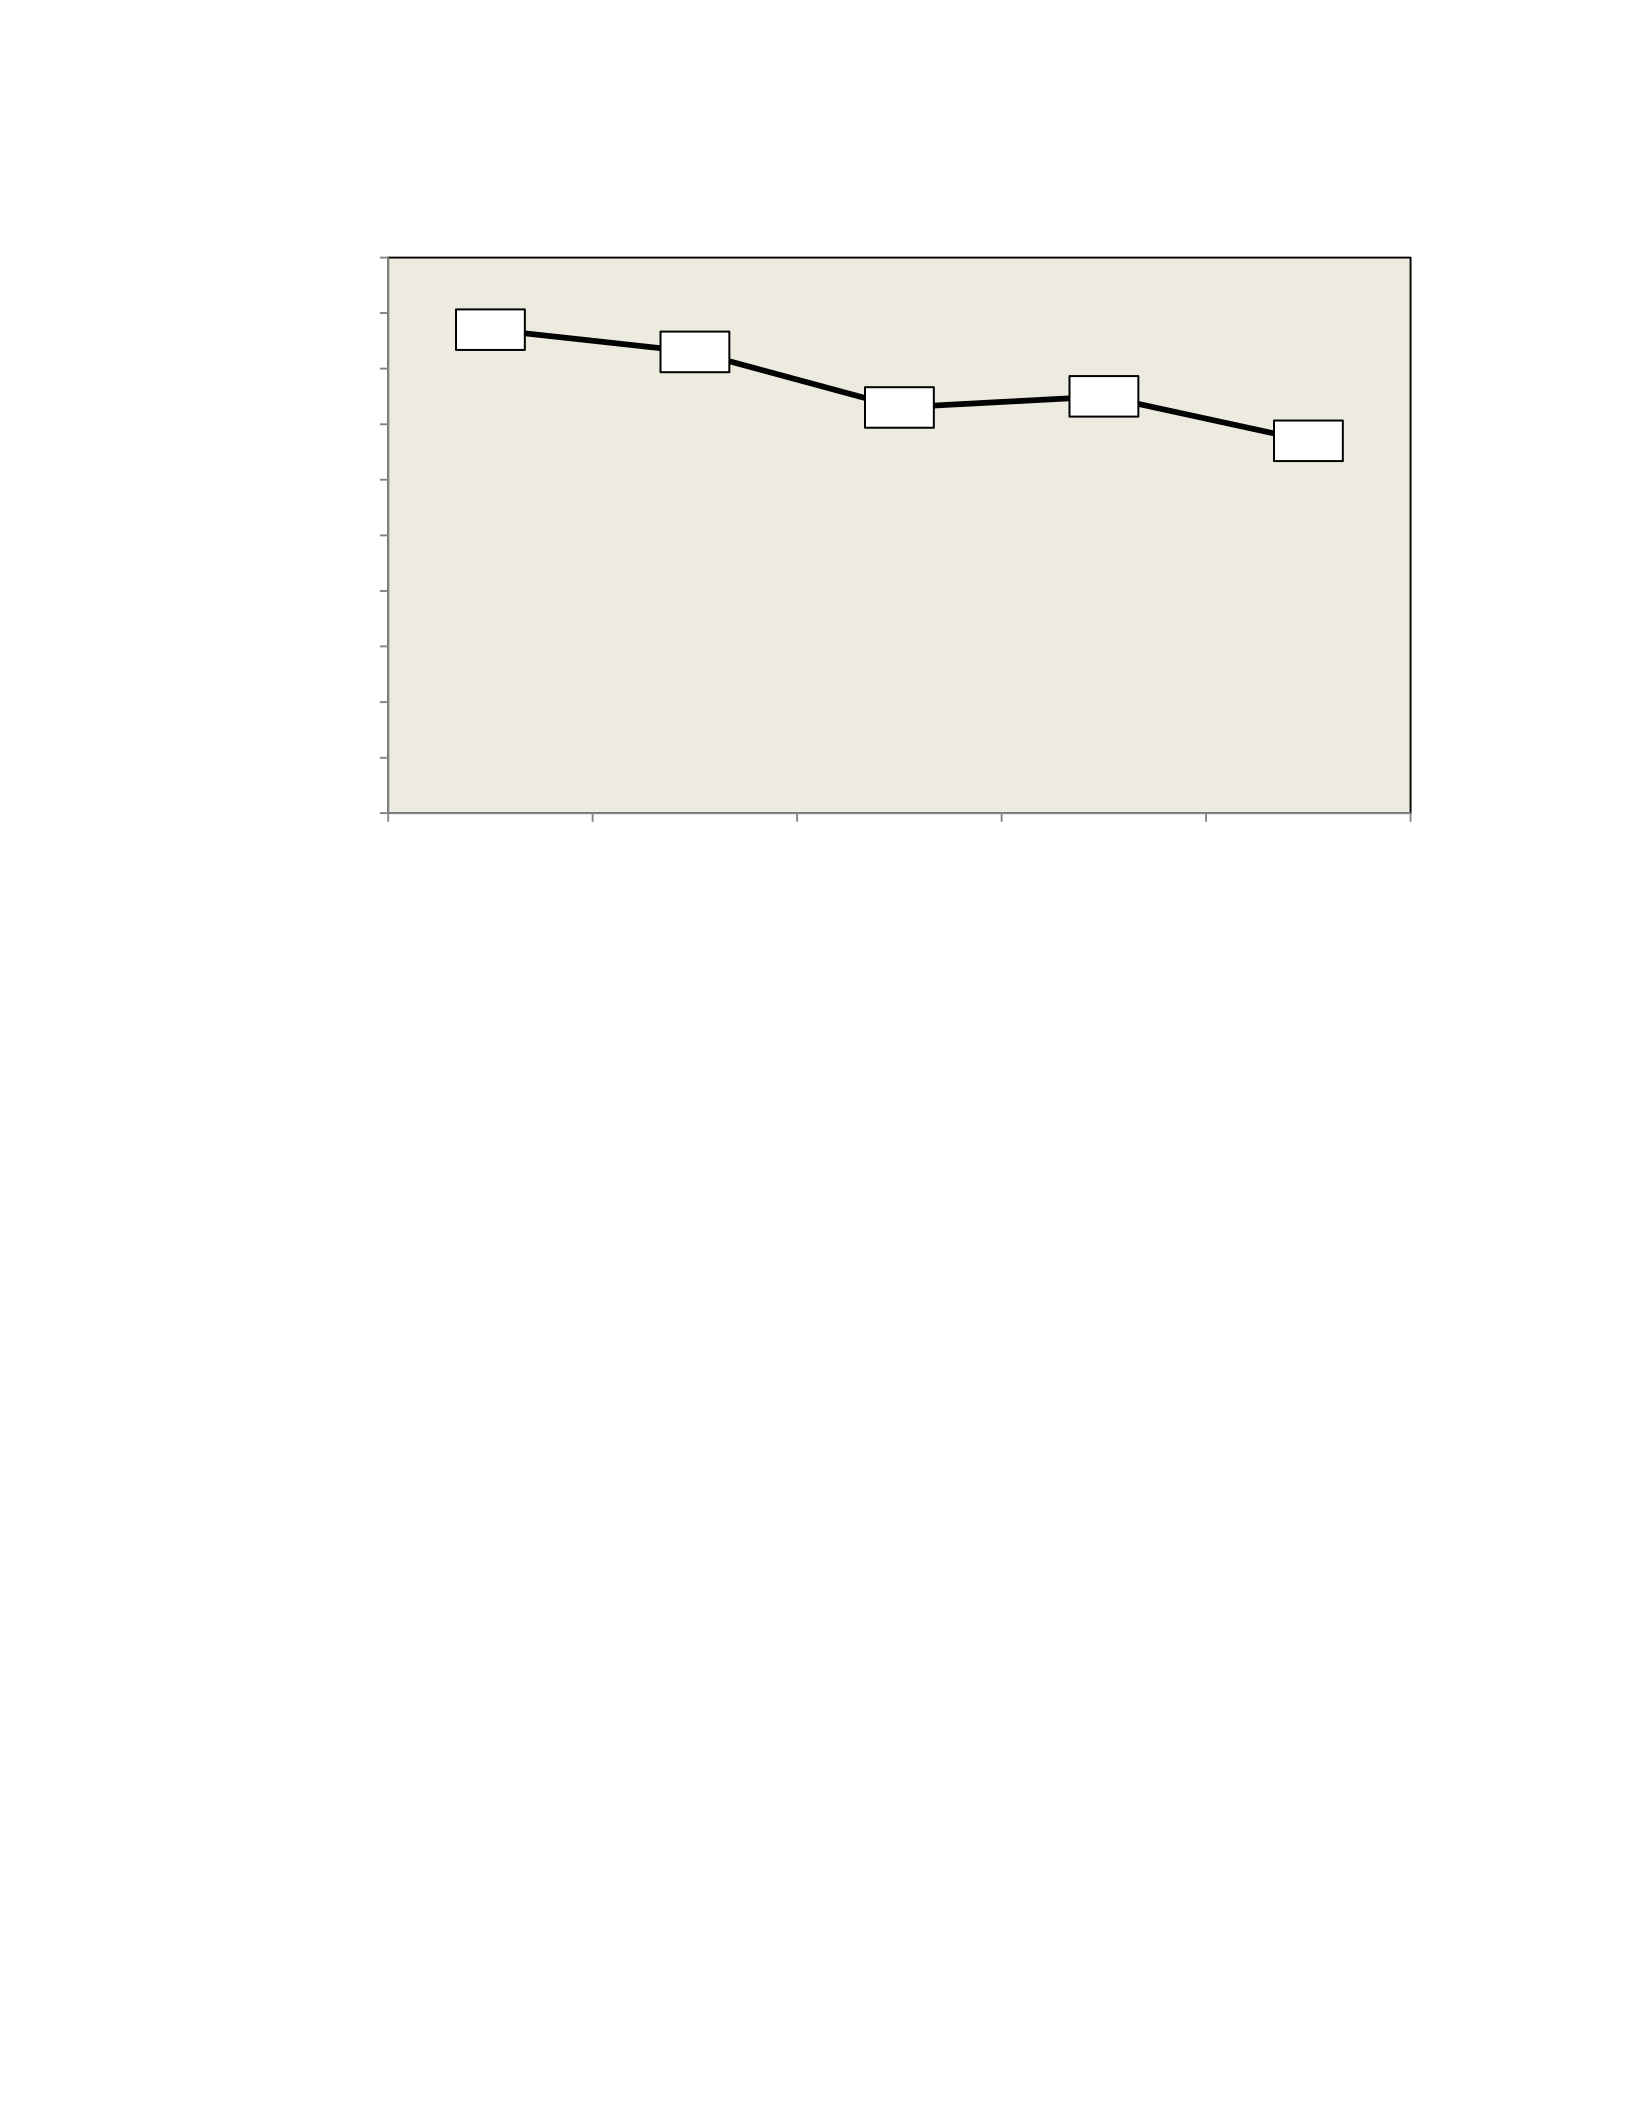
manufacturing industry as well. Figure 5 shows the trend of total recordable injuries and
illnesses in the furniture and related product manufacturing industry from 2003 to 2007 in
the U.S. (BLS 2009b).
31
Figure 5 The trend of incidence rates of total recordable injury and illness cases in
the furniture and related product manufacturing industry from 2003 to 2007
in the U.S.
In 2007, BLS reported that most occupational injuries and illnesses in the
furniture manufacturing industry were sprains, strains (47.1%), cuts, lacerations, and
punctures (37.2%) (Table 2) (BLS 2009c). Most of the injuries and illnesses were related
to contact with objects, equipment (74.6%) and overexertion (39.4%) (Table 2) (BLS
2009c). A study by Ma et al. (1991) found that cut and laceration accidents in the wood-
bamboo furniture manufacturing industry caused by unsafe conditions (approximately
60%) and unsafe acts (approximately 40%) were common work related injuries (Ma et al.
1991). Other reasons and injury illness types can be seen in Table 2. Extensive research
has been conducted showing that HF/E interventions prevent or reduce the risk factors for
occupational injuries and illnesses (Douphrate and Rosecrance 2004).
8.7%
8.3%
7.3% 7.5%
6.7%
0%
1%
2%
3%
4%
5%
6%
7%
8%
9%
10%
2003 2004 2005 2006 2007
32
Table 2 Incidence rates of nonfatal occupational injuries and illnesses involving days
away from work by case characteristics and industry, All U.S.,
private industry, 2007
Nature of injury, illness:
Prv.
Ind.
Fur.
Ind. Event or exposure:
Prv.
Ind.
Fur.
Ind.
Sprains, strains 47.3 47.1 Contact with object, equip.33.5 74.6
Fractures 10.0 8.1 Struck by object 17.2 32.2
Cuts, lacerations, punctures 11.3 37.2 Struck against object 8.0 15.4
Bruises, contusions 10.7 12.9 Caught in object, equip., mat. 5.7 21.3
Heat burns 1.8 0.5 Fall to lower level 8.1 4.1
Chemical burns 0.6 0.5 Fall on same level 17.6 10.2
Amputations 0.8 5.3 Slips, trips 4.0 2.2
Carpal tunnel syndrome 1.3 2.9 Overexertion 27.9 39.4
Tendonitis 0.5 1.4 Overexertion in lifting 14.8 23.7
Multiple injuries 4.9 4.0 Repetitive motion 3.9 10.1
With fractures 1.2 1.6 Exposed to harmful substance 5.6 2.8
With sprains 1.6 0.7 Transportation accidents 5.6 2.1
Soreness, Pain 12.2 12.3 Fires, explosions 0.2 -
Back pain 3.9 3.5 Assault, violent act 2.6 0.3
All other 20.8 27.0 by person 1.8 -
by other 0.8 -
All other 13.3 13.2
Cost of Injuries and Illnesses
The direct and indirect costs associated with occupational injuries, illnesses, and
fatalities in the U.S. in a particular year can be estimated by multiplying the number of
cases by the average costs of wage and productivity losses, medical expenses, and
administrative expenses per case (Leigh et al. 1997). The National Safety Council (NSC)
makes estimates of the average costs of injuries, illnesses, and fatalities and their impact
on the nation's economy (NSC 2009). According to the estimation of the NSC, the
average economic loss due to fatal and nonfatal occupational injuries in 2007 was $30.4
billion for the injuries without employers’ uninsured costs and $33.4 billion for injuries
with employers’ uninsured costs.

33
Estimations are not exact; they are only approximated because of the difficulty of
calculating the costs, especially indirect costs, and the quantity and complexity of factors
in the calculations make the process harder (NSC 2009). Because many costs associated
with occupational injuries, illnesses, and fatalities are ignored, the estimations are likely
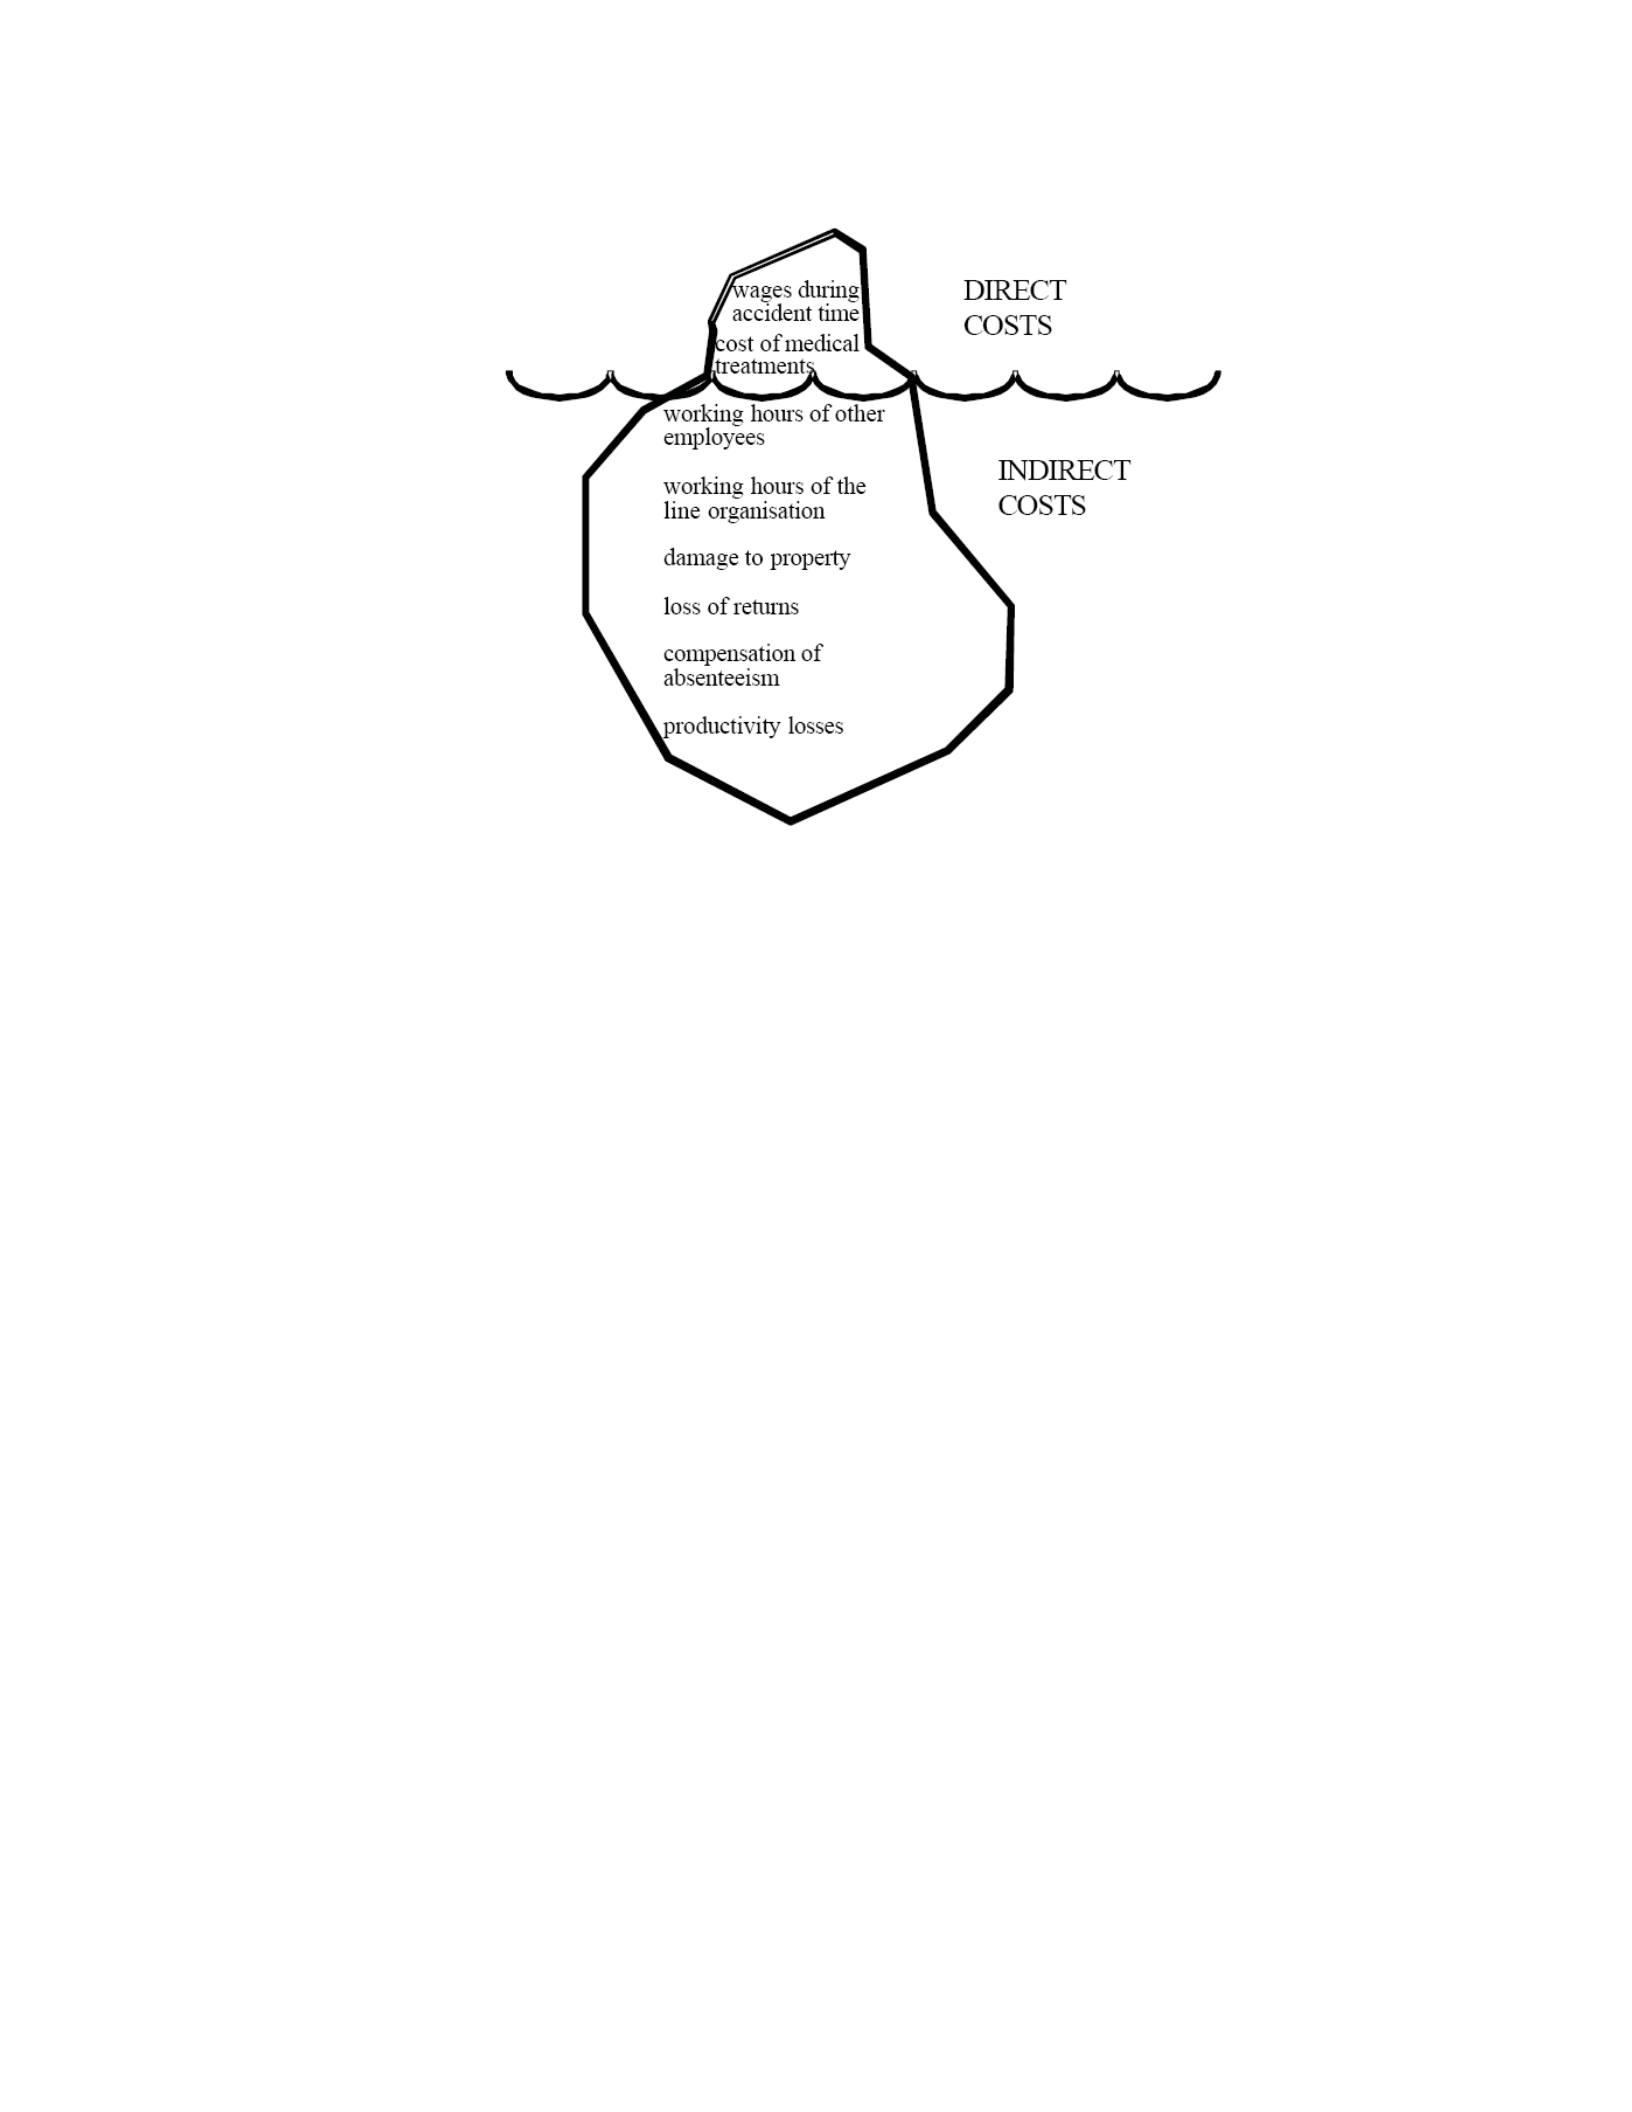
to be low (Leigh et al. 1997). Hendrick’s iceberg theory indicates that direct costs are
only the costs that are seen on the surface, but indirect costs are not seen and consist of
the large percentage of the total occupational injuries and illnesses costs (Figure 6)
(FMSAH and ILO-Safework 2002). For example, workers’ compensation is just the “tip
of the iceberg” when costs for lost workdays, lost production, lost income, employee
replacement costs, training, and community support of the worker’s family are added to
the calculation (AFMA and NCDOL 2003).
To calculate indirect costs, MacLeod (1995) suggests that the ratio 1:4 of the
direct costs to the indirect cost should be used. MacLeod also mentions that some
investigators suggest the ratio 1:10, but many companies have found a good estimation
for the total costs for per case by multiplying direct workers’ compensation costs by 4.
34
Figure 6 Hendrick’s iceberg theory related to direct and indirect costs in occupational
injuries, illnesses, and mortalities
Problem Statement
After providing the motivation factors for the thesis and a statistical industry
overview, summarizing problems in the problem statement section can be beneficial for
readers. As a whole, there are some problems in establishing the HF/E culture in
workplaces: (1) HF/E is not applied as much as it deserves; (2) managers are not
positively motivated to apply HF/E; (3) managers do not pay much attention to HF/E; (4)
HF/E is misperceived by managers; (5) managers are not really aware of the advantages
of HF/E; (6) managers are not sure how to deal with problems caused from the lack of
HF/E interventions; (7) managers have little knowledge about risk stressors and HF/E
principles, issues, and interventions; and (8) there are some problems with
communication between scientists and managers resulting from lack of cost-benefit
analyses in the current literature and inadequate documentation of HF/E programs and

35
their outcomes. In order to solve these problems, understanding the barriers and
limitations of integrating HF/E into the furniture manufacturing industry is required. The
purpose of the present study was to investigate these barriers and limitations to be able to
design more productive, safer, and healthier manufacturing systems.
Research Objectives
The objective of this study was to better understand the knowledge and opinions
of managers regarding HF/E in the American furniture manufacturing industry. This
study explored significant relationships between managers’ properties (including their
companies’ characteristics) and managers’ familiarities with HF/E, knowledge levels on
HF/E, preferred information resources concerning HF/E, opinions on likely benefits and
disadvantages of HF/E, opinions on companies’ resource availabilities, equipment
preferences, opinions of the importance levels of resources, opinions on the likely causes
of occupational injuries, accidents, and illnesses, opinions on who is responsible for
HF/E, and who will get benefits from HF/E. In addition to managers’ attitudes toward
HF/E, the study also explored inspection frequencies and worker involvement and
familiarity with HF/E. Lastly, this study aimed to produce results worthy of publication
and provide some suggestions to managers and scientists.

36
CHAPTER III
METHODOLOGY
After the research objectives were clearly defined, they were translated into the
key research questions. These questions were used to create a web-based questionnaire
survey as the experimental instrument. The survey was created by using a commercial
online survey tool. Development, pre-test, and review stages were followed to design the
final questionnaire survey. After completing an informed consent procedure approved by
the local Institutional Review Board, the link to the survey and descriptions about the
survey were published on the web sites of the Department of Forest Products and the
Franklin Furniture Institute at Mississippi State University. In the recruitment process,
986 managers were invited to participate in the study. Individual e-mail invitations were
sent which included the link of the survey and an individually designated password. 64
managers of sufficient quality were accepted as the subjects for the study.
Participants (Subjects)
The objective of this study was to better understand the knowledge of professional
personnel regarding HF/E issues in the American furniture manufacturing industry. To
reach the objective, managers were surveyed in this study. In this thesis, the term
“managers” involves owners, top-level managers (general managers, chief executives,
and presidents), and lower-level managers (production managers, directors of

37
manufacturing, plant managers, human resource managers, and engineers). Their major
responsibilities in organizations are (Trask et al. 2009):
1. Setting and deciding goals,
2. Organizing resources (labor, capital, and material),
3. Directing and motivating employees for the organization’s goals,
4. Hiring, developing, and training employees, and
5. Monitoring organizational performance and comparing performance with
established goals.
Based on the above, the subjects for the study were selected from managers who
had the capacity for creating and maintaining an organizational culture based on HF/E.
They were selected as subjects for the study because they played key roles in establishing
company-wide missions for HF/E interventions. Their knowledge, perception, and
commitment affected the success.
Population Size
The subject population was limited to managers who work in the U.S. furniture
manufacturing industry (NAICS 337). Managers who work in furniture wholesalers,
retailers, stores, leasers, or importers were not within of the scope of this study.
According to the Occupational Employment Statistics, there are totally 19,320
managers in the furniture and related products manufacturing industry in 2008 (Table 3)
(BLS 2009d). This number was obtained by using the Standard Occupational
Classification code of 110000 for the management occupation. Managers who were not
related to manufacturing were extracted from the total population because this thesis only
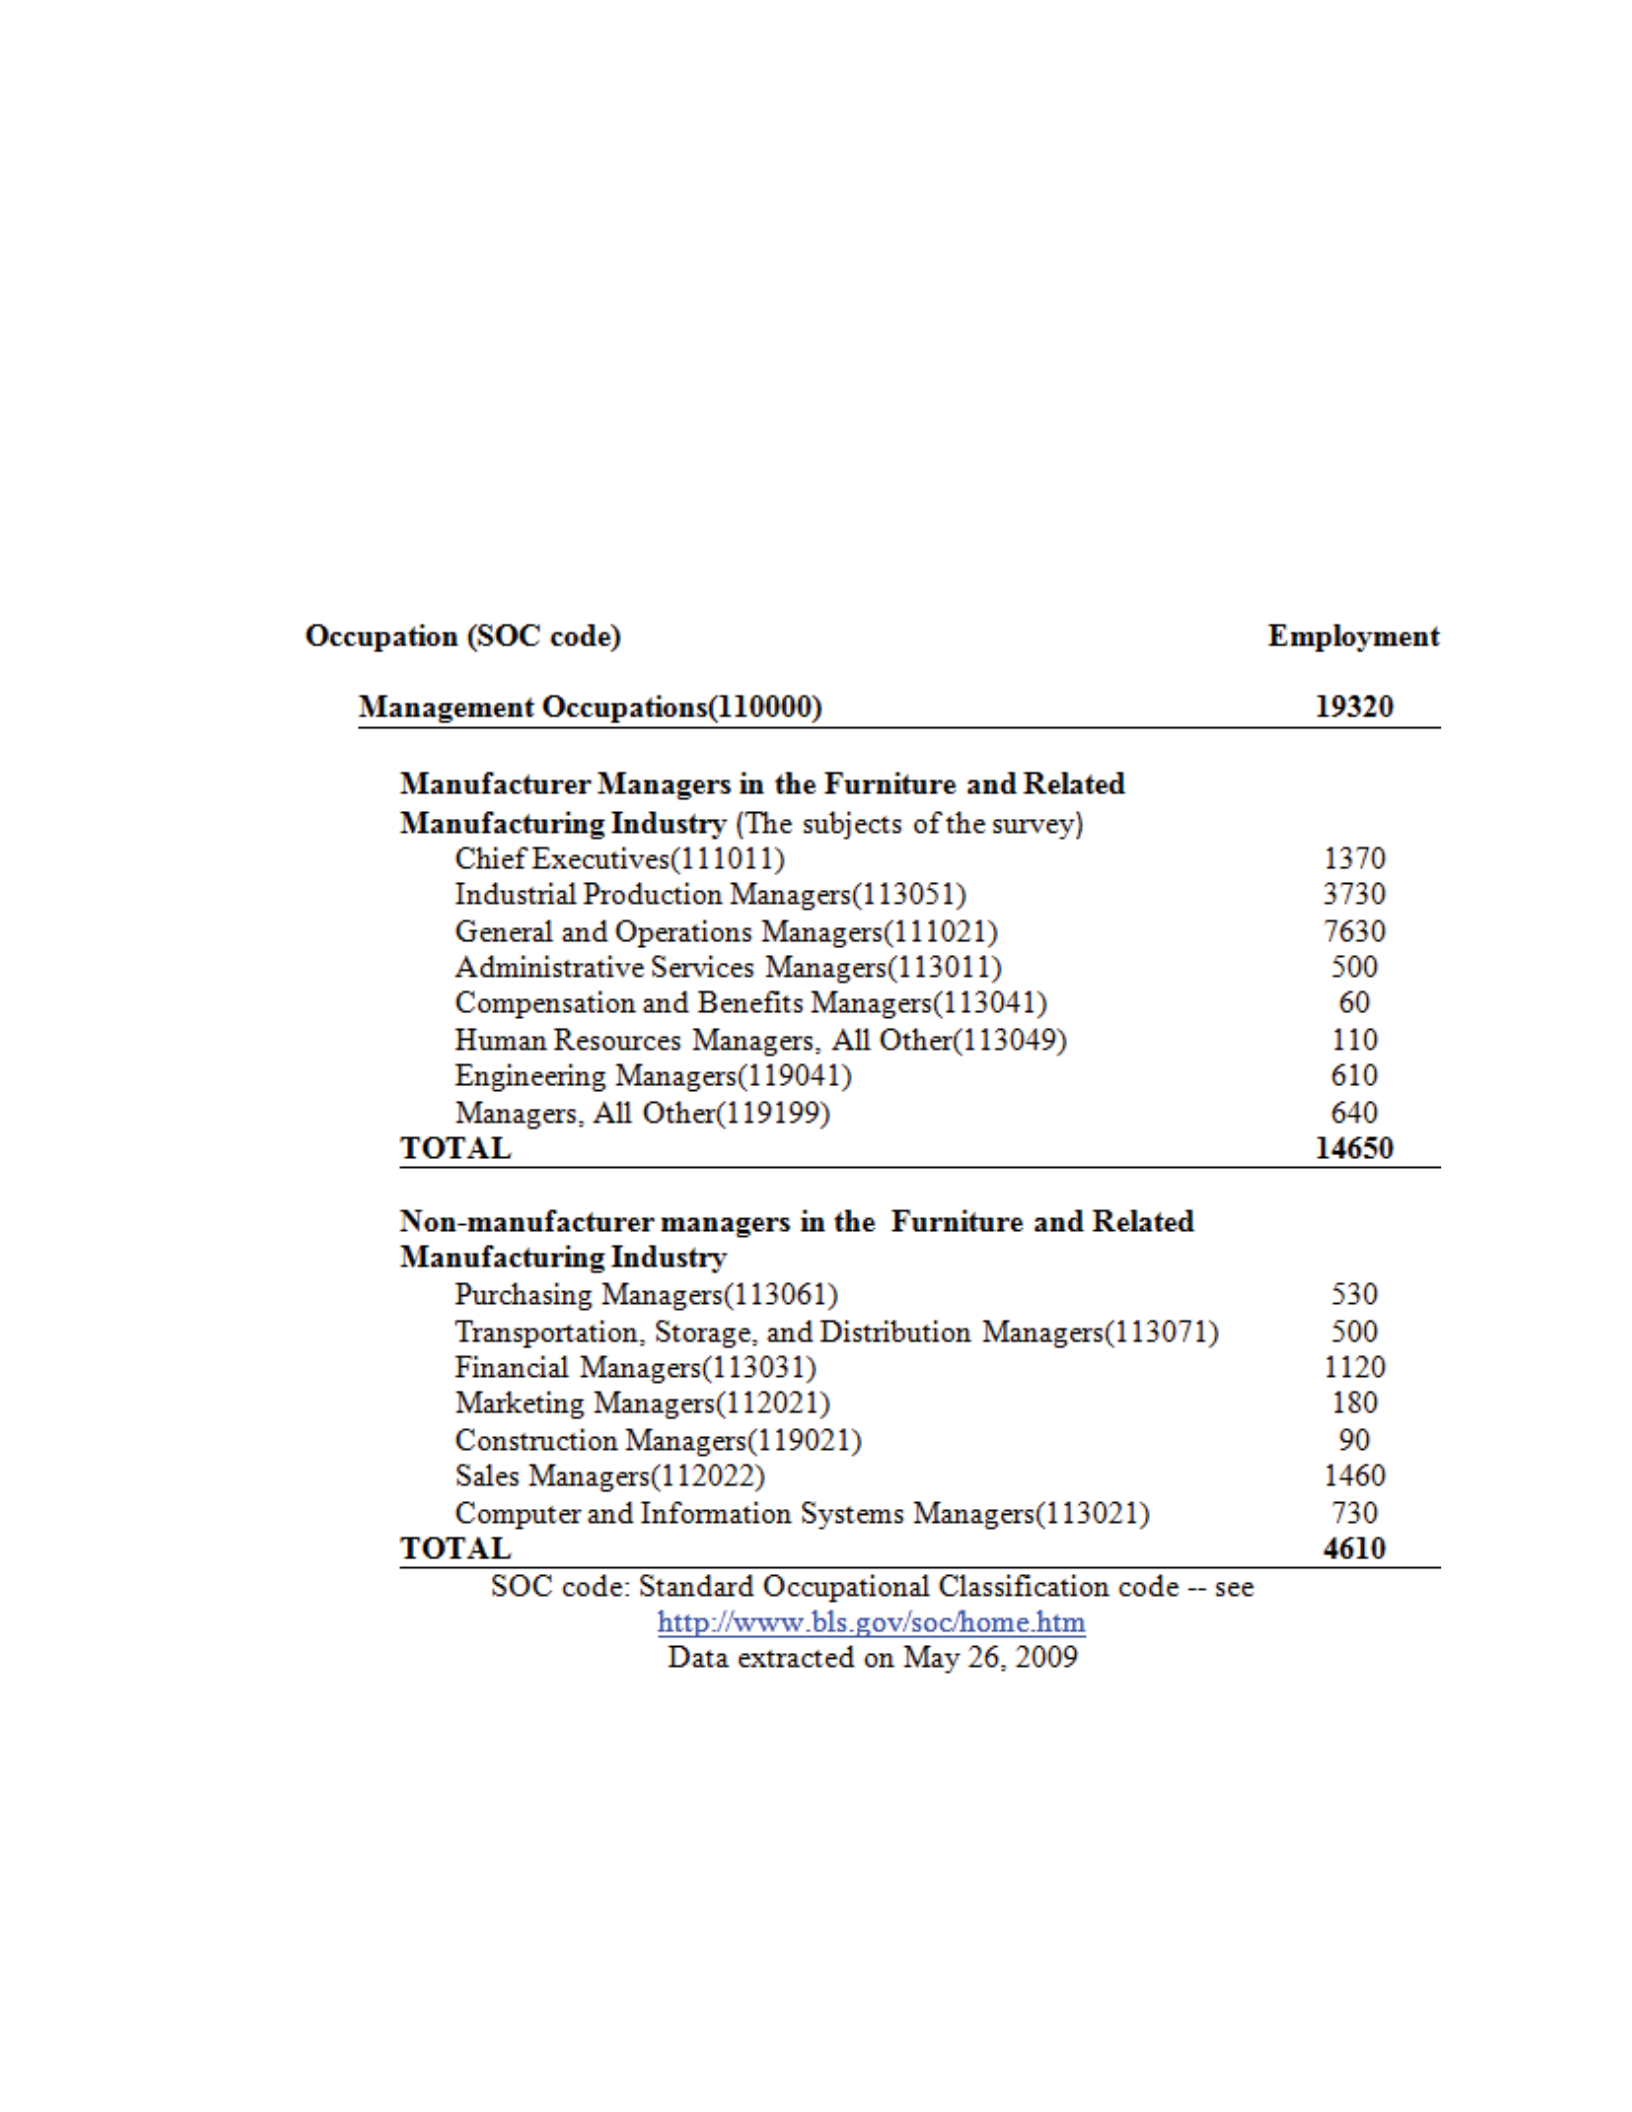
38
covered manufacturer managers. Thus, the actual population size of the managers in
furniture manufacturing was obtained. The population size for this study was 14,650
managers.
Table 3 Occupational Employment Statistics (OES), Furniture and Related Product
Manufacturing Industry (NAICS 337), May 2008

39
Participation Rate
A total of 986 managers were invited to participate in the survey. This number is
6.7 percent of the total manufacturing manager population. Of the 986 managers in the
survey, only 64 of them participated, yielding a participation ratio for this study of 6.5
percent. One of the hypotheses of this study was that professional personnel in the
furniture manufacturing industry were not interested in HF/E. If this response rate is
considered as a measure of managers’ interest, then this low participation ratio supports
that hypothesis.
The overall response rate to the questionnaire was about 4.37 individuals per 1000
managers (64/16,450=0.0043686 person). Therefore, with the population size of 14,650
managers and 64 respondents, the margin of error can be calculated as 12.5 percent by
assuming a 95 percent confidence level and 50 percent response distribution. The margin
of error is the error that researchers are willing to accept. The percent of 12.5 for the
margin of error can be considered as high, but it can be plausible if the limitation of
recruitment is taken into consideration.
Instrument Design
A questionnaire survey was the most suitable instrument to best understand the
opinions, knowledge, awareness, and attitudes of managers in the furniture
manufacturing industries. Possible survey techniques included mail surveys, face-to-face
interviews, telephone surveys, and internet surveys. A web-based survey was preferred as
the instrument because of the increasing use of the Internet as a communication
technology and because of the advantages of web-based surveys. The advantages of

40
electronic surveys over mail surveys include (Czaja and Blair 2005; Stanton et al. 2005;
Leeuw et al. 2008):
xEasy access to samples,
xNo geographic limitation to access of samples,
xSpeed of data collection,
xLower costs (paper, postage, and data entry costs),
xReducing data entry errors,
xHigh response quality,
xGreater flexibility for the respondents for choosing how and when to respond,
xEase of administration,
xEase of formatting for color, sound, image, etc.,
xElimination of unwanted interviewer effects, and
xMore privacy.
On the other hand, web-based surveys have some disadvantages if they are
compared with mail surveys (Czaja and Blair 2005; Stanton et al. 2005; Leeuw et al.
2008):
xResponse bias (limited and biased population),
xHigher coverage, sampling, measurement, and non-response errors,
xLow response rate,
xAnonymity,
xNondeliverabilty, and
xSecurity.

41
Besides these disadvantages, there exists a possibility that participants may not
have internet access. Moreover, participants may have different levels of education,
computer literacy, and computer hardware and software. Therefore, participants with
lower education levels, minimal experience with the use of computers, or older computer
equipment would probably have a difficult time completing the web-based questionnaire.
Survey Design
After a thorough review of the literature on HF/E issues and managers’
commitments to these issues in the furniture manufacturing industry, it became apparent
that the survey must address several key topics frequently mentioned in the industry
literature. Questions were formulated to address these key topics, and a list of questions
was complied. After researchers evaluated the questions, the first draft of the survey was
built.
One of the objectives of researchers in survey design was to create a completely
self-explanatory questionnaire because there would be no interviewer to explain
confusing or complex instructions or questions (Czaja and Blair 2005). Thus, a self-
administered questionnaire was prepared.
Another objective of researchers was to design a short questionnaire survey to
reduce the likelihood of participant attrition. The survey was designed to yield sufficient
information to accurately assess the awareness of managers while still being short enough
to be completed in roughly 5-10 minutes.

42
The choice of vocabulary and the visual design of the survey were carefully
evaluated. Questions that contain unfamiliar or excessively technical terms were avoided
because of the possibility that managers might not know or understand some of the
words. Because visually attractive surveys have higher response rates, the order, form,
and layout of questions were meticulously evaluated.
Survey Content
The final questionnaire was generated with the title of “Human Factors and
Ergonomics Awareness Survey” (see Appendix 2). The questionnaire had eighteen
questions in two sections. The questions in the first section asked for demographic
properties of participants and information about their companies. The questions in the
second section asked for the knowledge and opinions of managers through HF/E.
Questions included a mix of yes-or-no, Likert-type rating scale, and multiple-choice
(single or multiple answers) questions so that the method of response would most
effectively match the individual question. The option of “other” for the multiple
questions was given so that the participant could fill in the blank with his or her own
answer. Yes-or-no type questions included the option of “not sure.” Participants had the
option to skip any question if they did not wish to answer it.
The questionnaire survey also included a welcome page, an informed consent
form page, a definition page, and an appreciation page. In the welcome page, participants
were to enter their individually designated passwords. If they did not have one, they
could see the questions or even respond to them by entering “visitor” as the password, but
those who took the survey as a visitor were not accepted as a participant in analyses. This

43
was to avoid sampling errors. The link of the survey was published on public web sites,
thus people who were not eligible to be a subject might see and participate in the survey.
The first page of the survey included a brief introductory message including the
purpose of the survey, the confidentiality of data, potential risks of harm, contact
information of researchers (if anyone wished to ask questions about the survey or to print
out the survey and return it by mail after filling), and contact information of the local
Regulatory Compliance Office (if any participant wished to ask questions about his/her
rights as a research subject).
Following the questions in the first section, a definition page welcomed
participants. This page included the definition of HF/E as defined by the International
Ergonomics Association (IEA) and the link of IEA in case anyone desired to learn more
about HF/E. The definition page also included a note in all capital letters that “Human
factors and ergonomics are used synonymously in this survey.” The aim of this statement
was to prevent confusion of the minor meaning nuances.
When managers completed the survey, they saw an appreciation page. In this
page, the researchers thanked to them for their participation. Researchers also encouraged
managers to contact them if they had any additional thoughts, comments, or questions.
This page also included the researchers’ detailed contact information.
Review, Pretest, and IRB Approval
Questions in the survey were revised based on relevance of the goals, ease of
answer, effectiveness, comprehension, and professionalism. The questionnaire had to be
clear to those managers who might not have been familiar with the concept of HF/E. To

44
create such a questionnaire, the general scope, vocabulary, visual design of the survey,
and the layout of questions were carefully reviewed by the help of committee members of
this thesis and some other expert academicians. Three committee members, Dr. Steve L.
Hunter, Dr. H. Michael Barnes, and Dr. Jilei Zhang, from the Department of Forest
Products, Mississippi State University; Dr. Gary M. Bakken from the Department of
Systems and Industrial Engineering, University of Arizona; Dr. Gary A. Mirka from the
Department of Industrial and Manufacturing Systems Engineering, Iowa State University;
Dr. Kari Babski-Reeves and Dr. Lesley Strawderman from the Department of Industrial
and Systems Engineering, Mississippi State University; and Dr. Rubin Shmulsky from
the Department of Forest Products, Mississippi State University reviewed the
questionnaire survey.
A pre-test was conducted utilizing more than 20 graduate students. These
graduate students were from different departments at Mississippi State University such as
Chemical Engineering, Mechanical Engineering, Industrial Engineering, Aerospace
Engineering, and Landscape Architecture. Most of the students were international
students. In the pre-test, wordy, complex, uncertain, unrelated, and repeated questions
were reported to the researchers so that researchers could develop the final questionnaire
survey. The survey was tested by using different technologies as well. The survey was
tested in different web browsers, different operating systems, different monitors, and
different screen resolutions. Therefore, problems with the appearance of the questionnaire
on different screens were avoided. Because the time needed to complete the survey was

45
critical, the time was recorded in pre-tests. The feeling of the researchers was: the shorter
a survey, the higher participation ratio.
The survey was reviewed and approved by the Institutional Review Board (IRB)
at Mississippi State University with the IRB approval number of 08-196 (see Appendix
3). The IRB for Human Subjects ensures that the survey would not harm the participants
and would pose them minimal, if any, risk for financial standing, employability,
insurability, or reputation. Researchers have been responsible for the protection of the
rights and welfare of the human subjects in the study. All of these ethical and legal issues
were included in the informed consent form presented to the managers to read and
understand the nature of the research. If managers accepted all conditions and were 18
years old or older, they were required to click the button of “I admit” to start the survey.
They had the option of refusal by clicking the button of “I decline.” Lastly, contact
information of the IRB office was provided to participants if they so wished.
Data Collection
After obtaining the IRB approval to protect human subjects in the research, the
description including the link of the questionnaire was published on the web pages of the
Department of Forest Products (http://www.cfr.msstate.edu/Forestp/furniture_survey.asp)
and the Franklin Furniture Institute, Mississippi State University, and the data collection
process initiated in December 2008.
First, contact names and e-mail addresses of managers in the industry were
collected: 1) from people who had relationships with them through various professional
organizations, associations, and societies managers could be members of; 2) from the

46
directory or yearbooks of associations, organizations, institutions and societies; 3) from
the information of their companies’ web pages; 4) from newspapers, journals, books, etc.
which included their names, positions, and e-mail addresses; and 5) from the directory
lists of conferences, meetings, and fairs; and 6) from direct contact with managers. From
this, a list of 1,252 managers including their names, occupations, company names,
locations, e-mail addresses, if available, was collected. Managers who were not related to
manufacturing (for example, sales or marketing managers) were not included in the list.
Individual invitation e-mails (see Appendix 4) were sent to these managers.
However, 266 of them could not be reached by e-mail, yielding a total of 986 invitees.
Each e-mail included the aim of the study, a password for each participant, the link of the
survey, the data confidentiality, and contact information of researchers. Because the
survey was posted to publicly accessible websites, a unique personal password was given
to participants. Passwords also ensured that only managers in the furniture manufacturing
industry completed the survey and that they completed it only once. For members of
associations and societies, only one password was provided for each organization. For
example, all of the members of the Franklin Furniture Institute were given a single
password to enter and complete the survey. One reminder e-mail was sent to non-
respondents in order to increase the response rate. The sending process of the recruitment
invitations finished in March 2009, and the data collection process was completed in
April 2009.

47
Limitations in the Data Collection
There were some limitations in the data collection process. The first limitation
was related to the sample coverage. The study only covered managers who had an e-mail
address, so the coverage was limited to only those managers. Managers who did not have
an e-mail account or did not want to give their e-mail addresses were not included in the
survey. Incorrect or out-of-date e-mail addresses limited the coverage as well. Another
limitation was that there was a little control over who responded to the questionnaire.
One possibility was that another person in the company was using the e-mail account on
behalf of the manager. Moreover, most of the managers did not want to participate in the
survey. Some of the managers stopped during the survey and decided not to continue, or
clicked the “I decline” button in the survey. Another limitation concerns the possibility
that the invitation e-mails were considered as junk e-mails or spam. There was a high
probability that managers judged the e-mail to be spam and therefore never opened it, or
the managers’ email systems judged the e-mail to be spam and therefore never delivered
it.
Data Analysis Process
Once all the data was collected, the research hypotheses were investigated by
applying statistical analyses. The analyses were performed by the Statistical Package for
the Social Science (SPSS) for Windows version 17.0. First, the data was entered into the
SPSS analysis software by coding, and then the coded data was processed. The Chi-
square statistical test, a cross tabulation of the data, was applied to determine the
association of managers’ demographic properties (first six questions in the survey) and

48
managers’ interests, knowledge, and commitments on HF/E (the remaining questions).
The Chi-square test basically compares observed data (obtained from the sample) with
expected data (that researchers expect to obtain according to their hypotheses). If the
observed data and expected data distributions fit reasonably well, the Chi-square test
assumes there is no significant difference between distributions in a specific significance
level. The significant level for this study was set at p 7KDWLVLIWKHSUREDELOLW\RU
p-value is equal or below 0.05, it is interpreted that there is a significant difference
between the observed value and the estimated value.

49
CHAPTER IV
RESULTS & DISCUSSION
Sixty-four managers from the American furniture manufacturing industry
responded to the questionnaire survey asking about their awareness regarding HF/E in
manufacturing. The distribution of answers, statistical analyses, comparisons with the
literature - if any current literature is available - and discussions will be introduced in the
section of results and discussion. After demographic profiles of responders are provided,
the significant relationships between these profiles and the managers’ answers will be
evaluated by statistical tests.
Demographic Profiles of Managers
Demographic profiles of managers in the furniture manufacturing industry were
asked in the early questions in the survey. A total of sixty-four managers participated in
the survey, thirty-one of those were from Mississippi and the others were from other
states in the U.S. Descriptive statistics of managers’ demographic profiles are reported in
Table 4. All demographic features of managers are classified by the states where
companies were located.
In addition to demographic features of managers, company characteristics were
critical in statistical analyses and interpretations. The data related to company
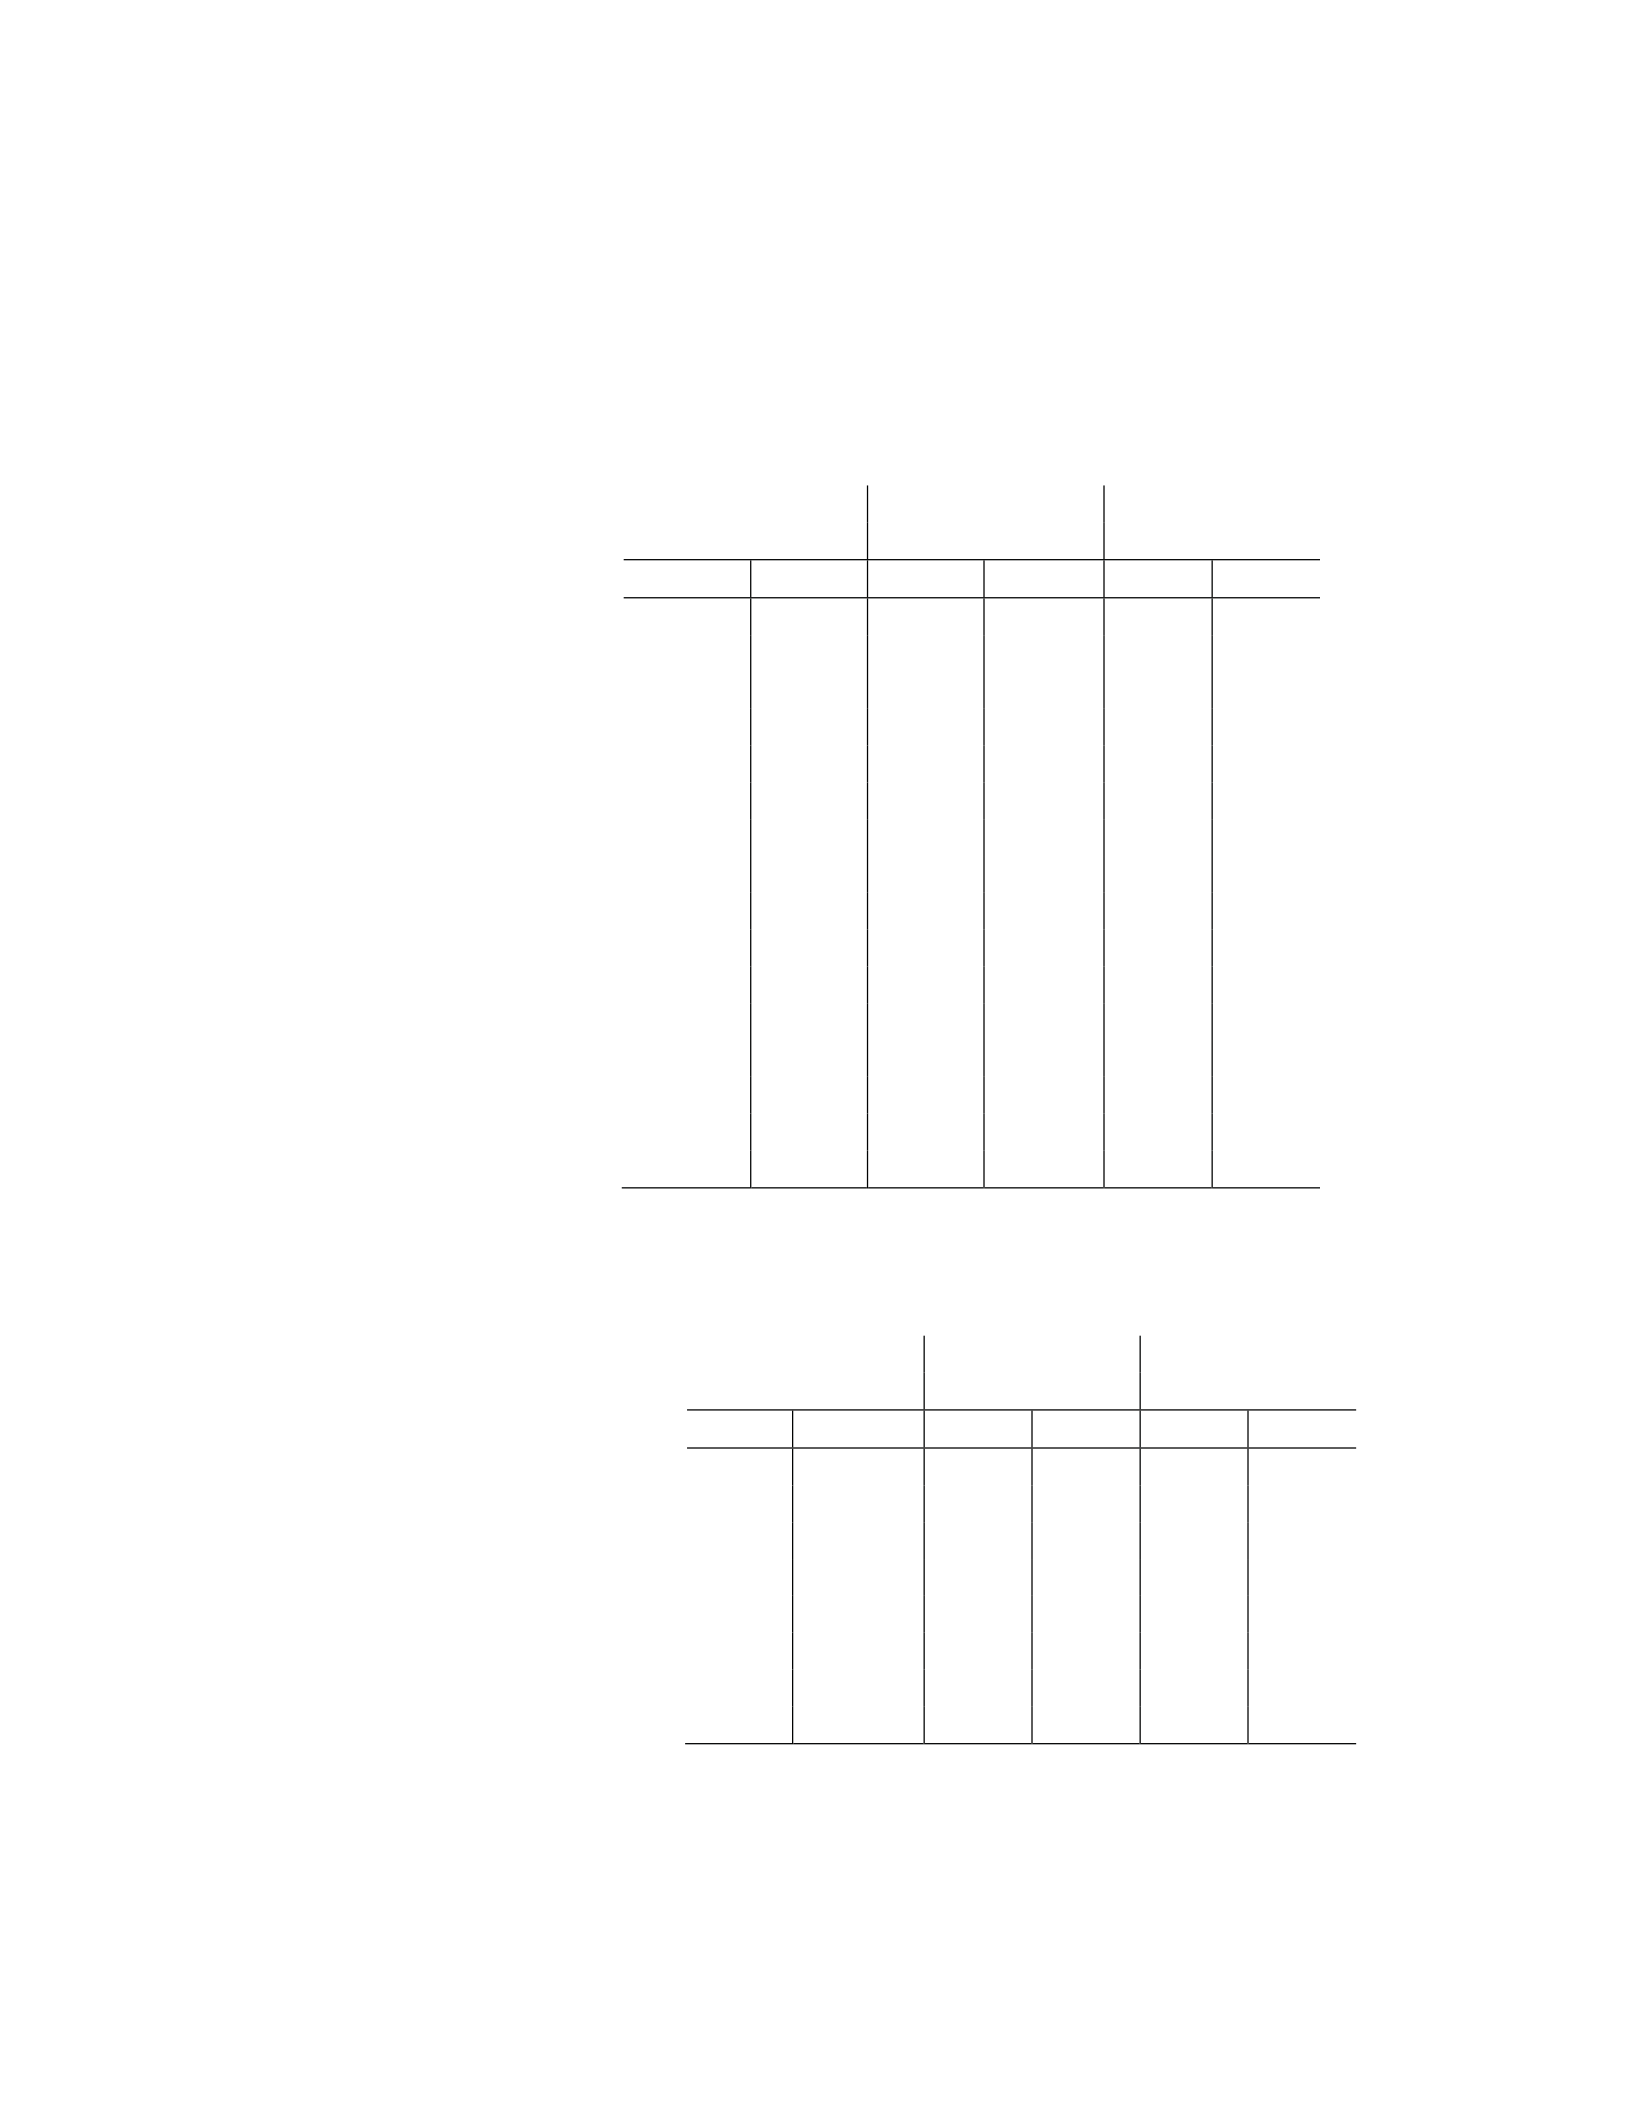
50
characteristics are reported in Table 5. The table provides the data of the sector types and
sizes of the companies where subjects for the survey have worked.
Table 4 Managers’ demographic profiles
All MS Others
(64) (31) (33)
Number Percent Number Percent Number Percent
Position
Owner 24 38.1 4 6.3 20 31.7
Top-level manager 8 12.7 4 6.3 4 6.3
Lower-level manager 31 49.2 22 34.9 9 14.3
Education
High School 9 14.5 2 3.2 7 11.3
College 39 62.9 21 33.9 18 29
Graduate School 14 22.6 7 11.3 7 11.3
Experience in Furniture Industry
Less than 3 years 7 10.9 3 4.7 4 6.2
3-10 years 13 20.3 8 12.5 5 7.8
More than 10 years 44 68.8 20 31.2 24 37.5
Experience in Current Position
Less than 3 years 13 20.3 7 10.9 6 9.4
3-10 years 21 32.8 11 17.2 10 15.6
More than 10 years 30 46.9 13 20.3 17 26.6
Table 5 Company characteristics
All MS Others
(64) (31) (33)
N
umber Percent Number Percent Number Percent
Sector (NAICS Code 337)
Household (NAICS 3371) 37 57.8 25 39.1 12 18.8
Office (NAICS 3372) 15 23.4 2 3.1 13 20.3
Other (NAICS 3379) 12 18.8 4 6.2 8 12.5
Number of employees
0-49 30 46.9 6 9.4 24 37.5
50-249 16 25 10 15.6 6 9.4
249 or more 18 28.1 15 23.4 3 4.7

51
As can be seen in the tables above related to the managers’ profiles and their
companies’ characteristics;
xmost of the owners were from the other states (83.3%), and most of the lower-level
managers were from Mississippi (70.9%),
xmost of the managers have college degrees (62.9%) and less than a quarter of
managers have graduate level degrees (22.6%),
xabout 70 percent of managers have more than 10 years of experience in the
furniture manufacturing industry (68.8%),
xabout half of the managers have worked in the same position for more than 10
years (46.9%),
xhalf of the managers have worked in the Household and Institutional Furniture and
Kitchen Cabinet Manufacturing (NAICS Code 3371). As a detail, the majority of
professional personnel working in the Household and Institutional Furniture and
Kitchen Cabinet Manufacturing (NAICS Code 3371) industry are actually
working in the Upholstered Household Furniture Manufacturing (NAICS Code
337121) sub sector. The rest of the professional personnel have worked in the
Office Furniture (Including Fixtures) Manufacturing (NAICS Code 3372) and the
Other Furniture Related Products Manufacturing (NAICS Code 3379). The Other
Furniture Related Products Manufacturing (NAICS Code 3379) includes mattress,
blind, and shade manufacturing sub sectors, and
xabout half of the companies were small size companies (46.9%), and the rest of the
companies were middle size (25%) and large size (28.1%).

52
The data distribution in this survey shows the same distribution of the actual
population characteristics because (1) Mississippi is one of the nation’s top states in
furniture production, so most of the large companies are located in Mississippi while
other states generally have smaller furniture manufacturing companies; (2) large
companies occupy many top- and lower-level managers while small companies generally
occupy owners and few managers; and (3) generally, large companies occupy employees
who have a high education background. Therefore, if a manager from furniture
production is selected from Mississippi, then there is a high possibility that he will
probably be a top- or lower-level manager with a high level of education and will be
working in a large size furniture manufacturing company. Likewise, if a manager from
furniture production is selected from one of the other states, there is a high possibility that
he will probably be an owner with a lower-level education and working in a smaller sized
furniture manufacturing company.
Managers’ Familiarity with Human Factors and Ergonomics
Managers were asked more questions related to their background or their
familiarities with HF/E. The first question was whether managers had attended a formal
training program in HF/E or not. Human factors and ergonomics education programs
have a significant effect on increasing awareness (Albers et al. 1997; Pehkonen et al.
2009), resulting in safety, health, productivity, and efficiency. Human factors and
ergonomics integrated occupational educational programs, especially participatory based,
play a key role in occupational injury and illness control strategies (Albers et al. 1997).
53
Human factors and ergonomics programs can provide considerable benefits to
organizations when they are properly implemented (Goggins et al. 2008). Guastello’s
literature search (1993) revealed that various accident prevention programs had a
considerable effect on reducing occupational accidents by fifty percent. He also
mentioned that HF/E interventions were not widely applied even though most of them
showed vast achievements in the program (Guastello 1993).
After reviewing literature and searching in the Internet, Goggings and his
colleagues summarized 250 case studies in their report. The average productivity increase
of 60 HF/E programs was 25 percent (Goggins et al. 2008). The summary table of 250
cases is given in Table 6.
Table 6 Effectiveness measures from Goggings et al. 2008 Review (250 case studies)
Number of Studies Average Reduction
Number of MSDs 90 59%
Incidence date 53 65%
Lost workdays 78 75%
Restricted days 30 53%
Workers’ comp. costs 52 68%
Cost per claim 7 39%
Labor cost 6 43%
Errors 8 67%
Turnover 34 48%
Absenteeism 11 58%
Payback period 36 0.7 years
Cost:Benefit ratio 5 1:18.7
The other question in this survey was whether managers had any certification in
HF/E. The breakdown of the answers to each question is shown in Table 7.
54
Approximately, 2 out of 3 managers stated that they have not attended a formal
training program in HF/E. The rate of occupational injuries and illnesses in the furniture
manufacturing industry was 6.7 in 2007 (BLS 2009b). If managers’ participation in HF/E
training programs increases, the awareness level of managers can increase, resulting in
decreased occupational injuries in the industry. Therefore, managers should be advised to
participate in training programs.
Table 7 Managers’ familiarity with human factor and ergonomics
Questions
Yes No Total
(N) (%) (N) (%) (N)
Have you ever attended a formal training
program in human factors and ergonomics?
18 28.6 45 71.4 63
Do you have any certification in
human factors and ergonomics? 0 0 61 100 61
Unfortunately, none of the managers who participated in this survey had
certification in HF/E. Certifications show that individuals participate and complete
training programs and have sufficient knowledge and experience in the subject. Certified
Professional Ergonomist (CPE), Certified Human Factors Professional (CHFP), Certified
User Experience Professional (CUXP), Associate Ergonomics Professional (AEP),
Associate Human Factors Professional (AHFP), Associate User Experience Professional
55
(AUXP), and Certified Ergonomics Associate (CEA) are some common certification
programs (BCPE 2009).
A Chi-square statistical test was performed. According to the test results (Table
8), there is a significant relationship (p EHWZHHQWKHVWDWHZKHUHPDQDJHUVZRUN
and managers’ participation in training programs.
Table 8 Statistical test results of managers’ demographic properties and managers’
familiarity with human factors and ergonomics
State Education NAICS Employees Experience
in FI Position Experience
in P
Attending a formal
training
Ȥ28.231 1.882 1.015 13.199 0.468 6.566 0.105
P0.004* 0.390 0.602 0.001* 0.791 0.038* 0.949
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p: p-value (The level of statistical significance).
The participation in training programs is higher among Mississippian managers
(Figure 7). Three quarters of managers who have ever attended at least one training
program were from Mississippi. On the other hand, 62.2 percent of managers who have
never attended a training program were from the other states.
The higher participation of Mississippian managers might be the consequence of
Mississippi’s leadership in furniture manufacturing. Mississippi has many large furniture
companies. Because large companies have generally more opportunity to provide training
for their employees, there is a high possibility that attending training programs is higher
among Mississippian managers. This interpretation is statistically supported. The test
found a significant relationship (p EHWZHHQFRPSDQ\VL]HDQGDWWHQGLQJWUDLQLQJ
programs. Managers who work in smaller companies, those with less than forty-nine
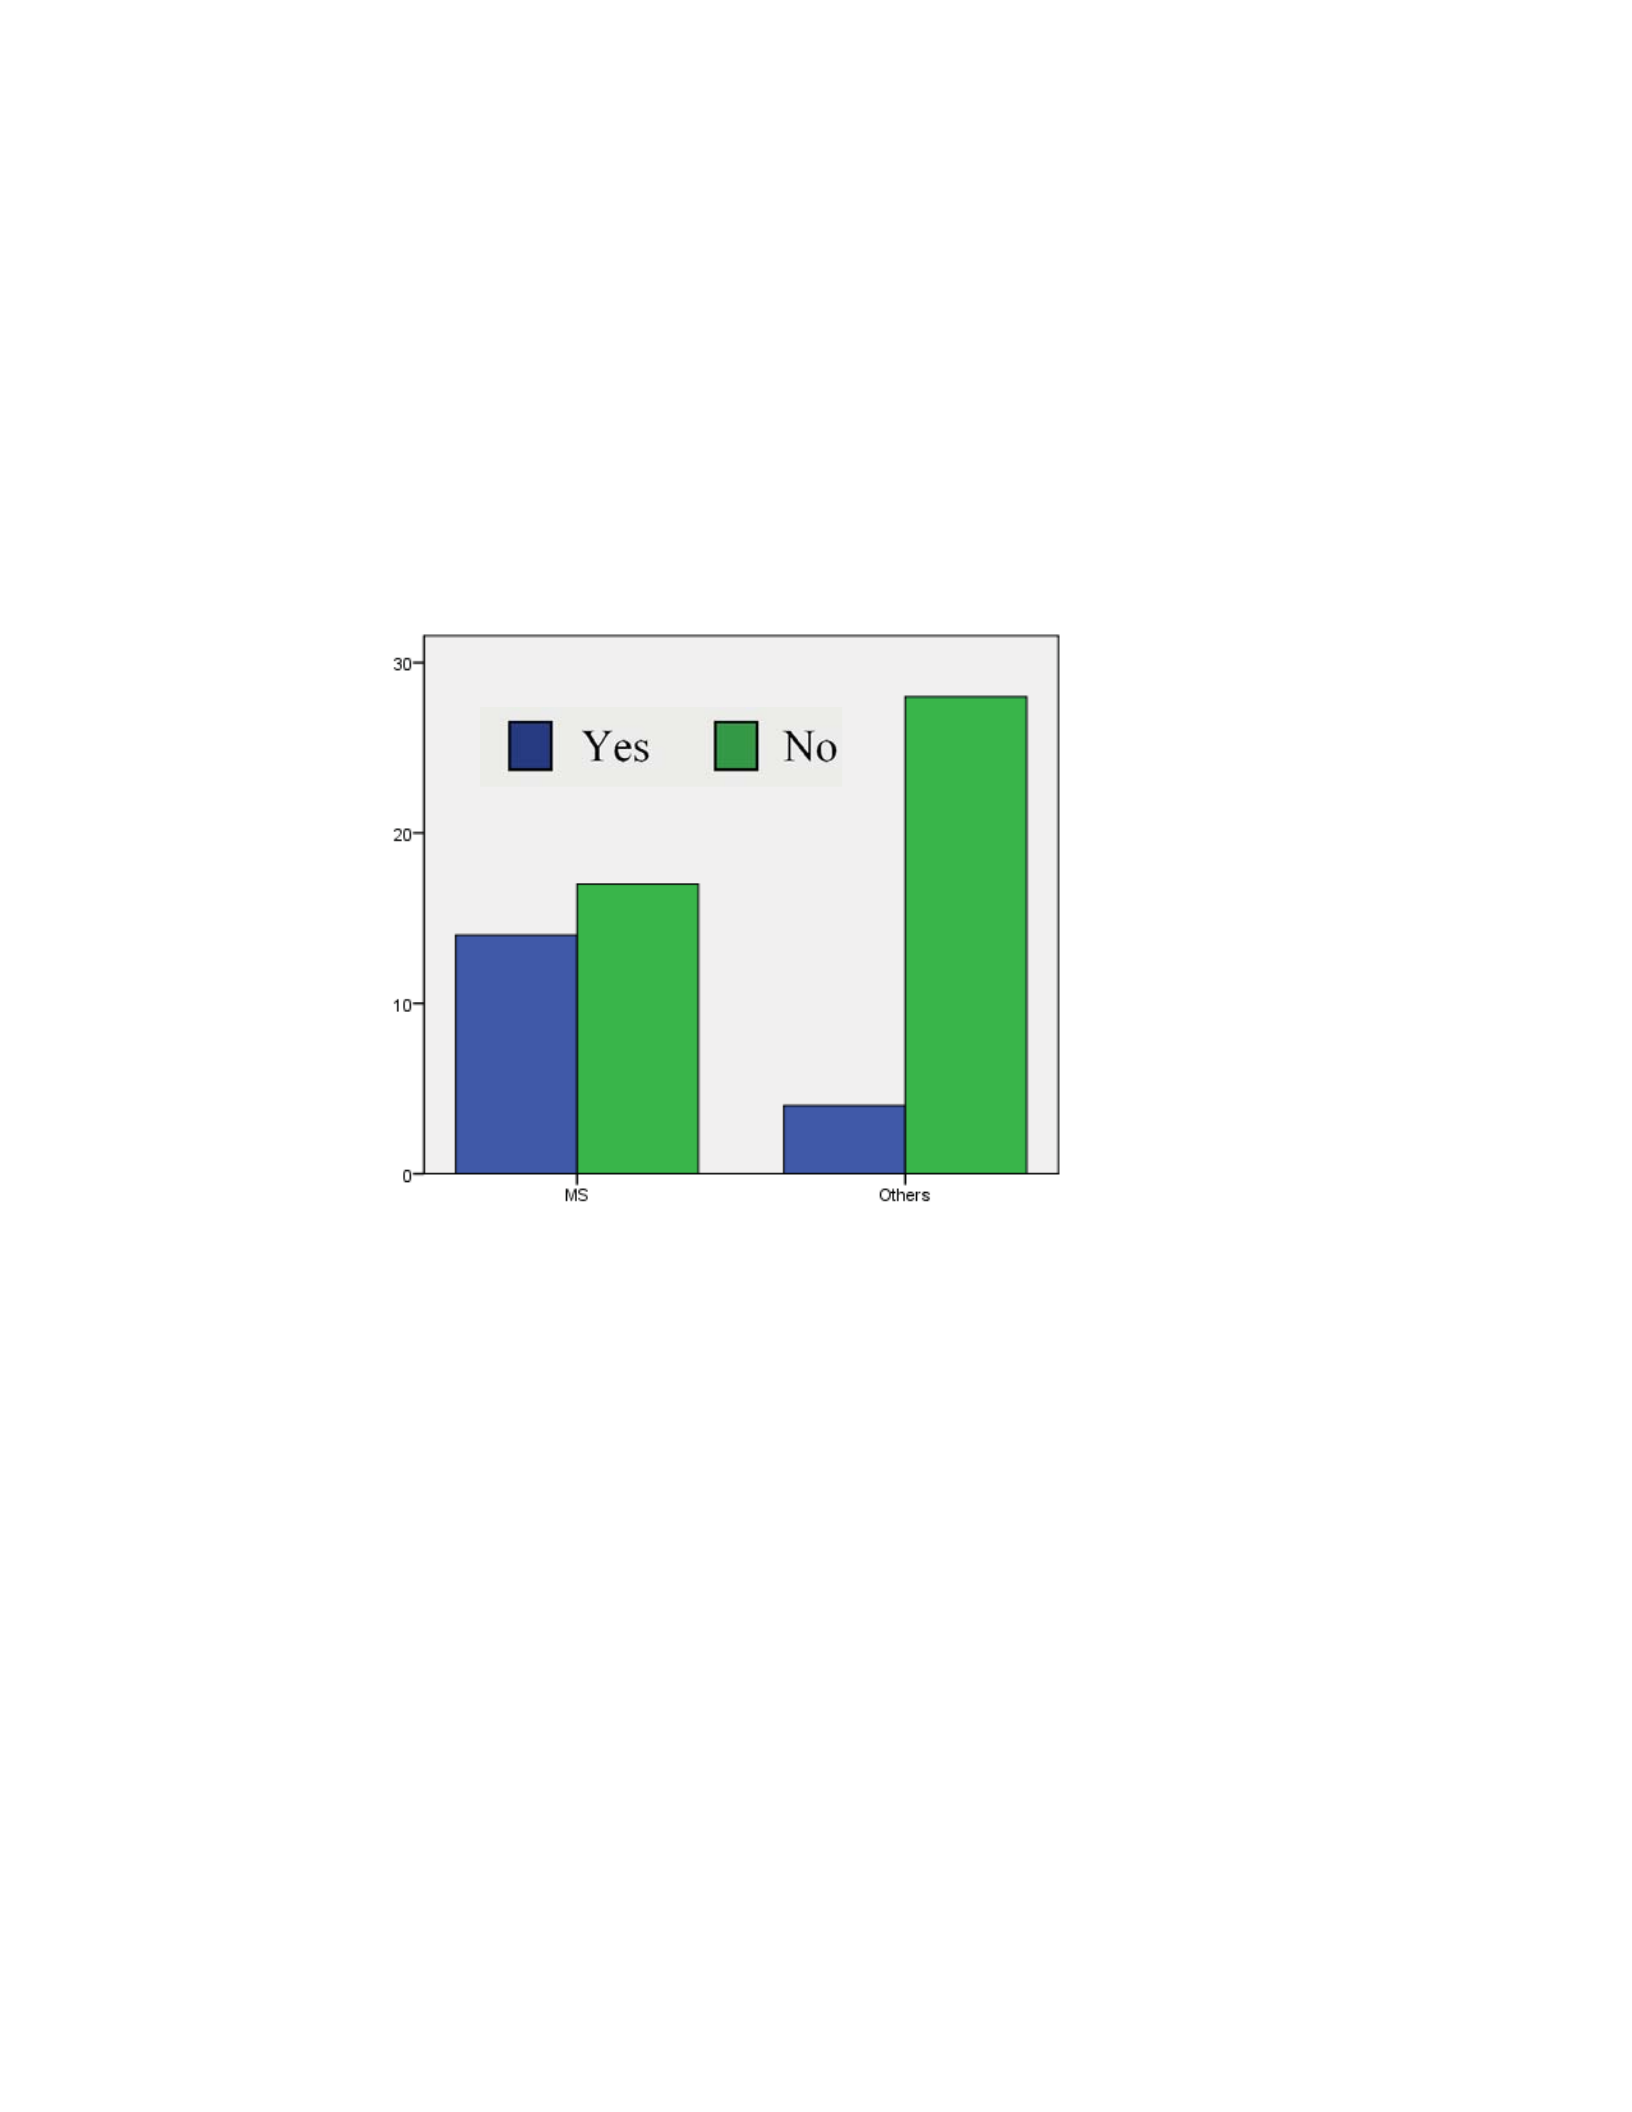
56
employees, have a lower opportunity to attend training programs rather than managers
who work in companies with 250 or more employees (Figure 8).
The last significant relationship (p LVIRXQGDPRQJDWWHQGLQJWUDLQLQJ
programs and managers’ current positions. The ratio of owners’ participation to training
programs is lower than the ratio of lower-level managers’ participation (see Figure 9).
Figure 7 Attending training programs of Mississippian vs. other states’ managers
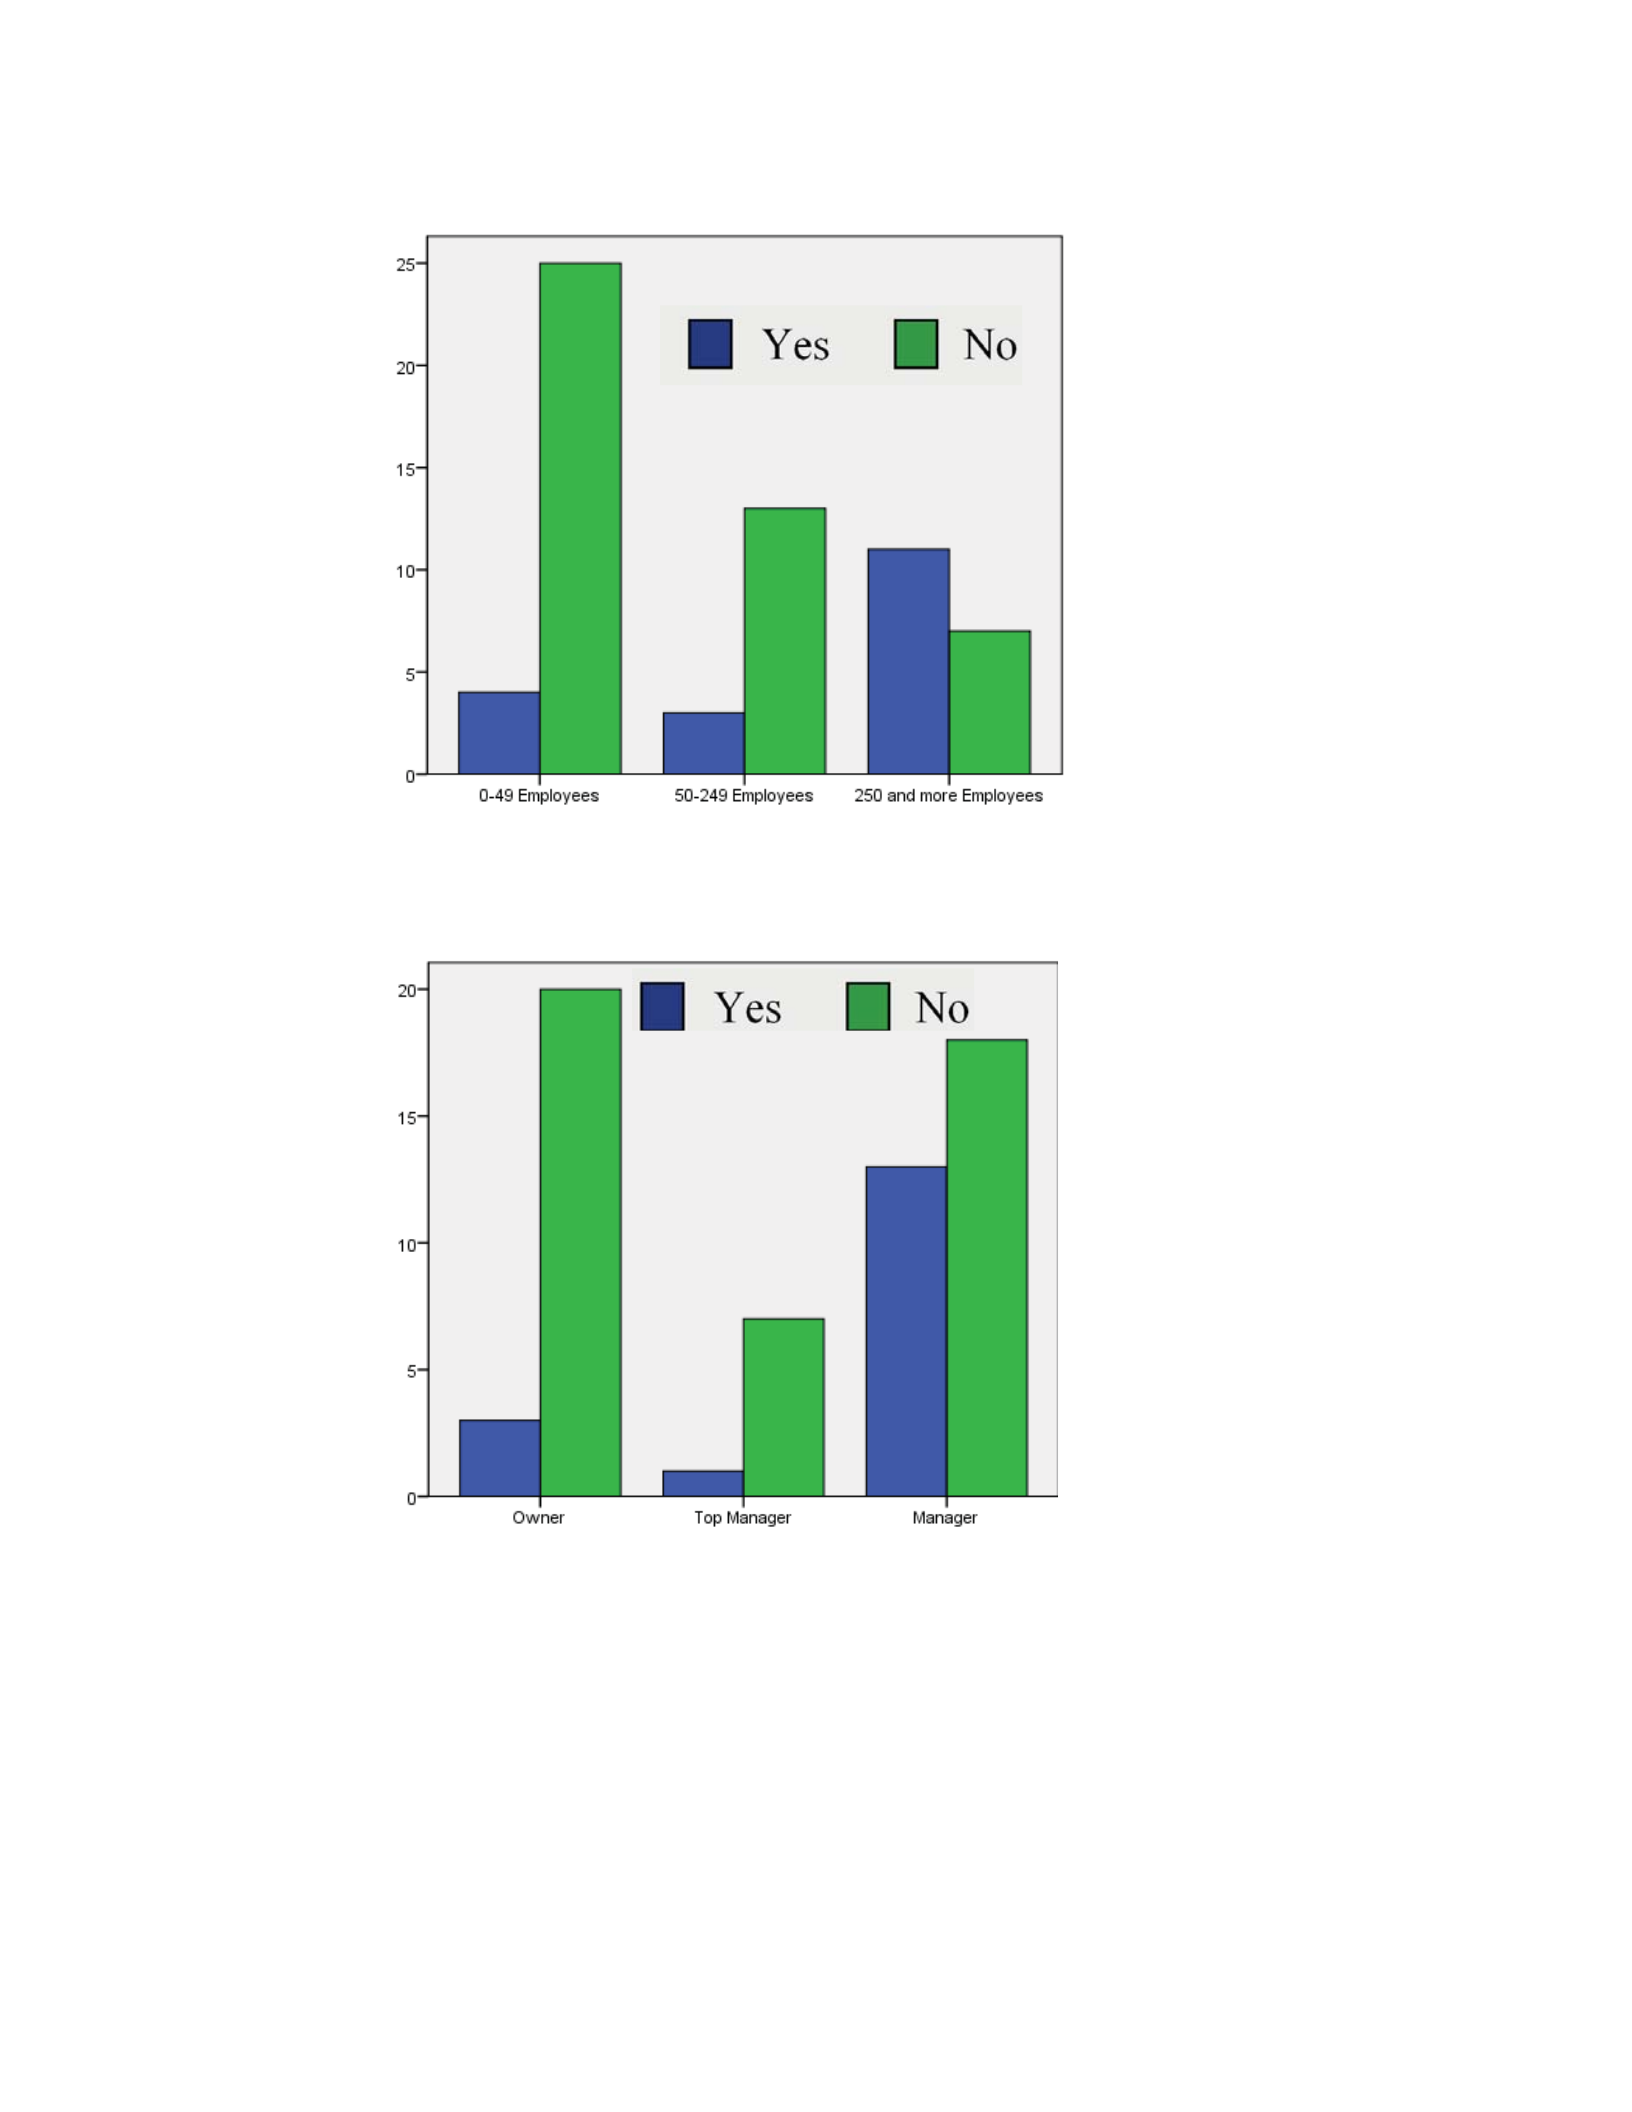
57
Figure 8 Attending training programs of managers who work in different size companies
Figure 9 Attending training programs of owners, top-level managers, and lower-level
managers
Because there were no managers with certification in HF/E, the statistical analysis
could not be performed. Therefore, statistical interpretation was not possible.
58
To summarize managers’ familiarity with HF/E: most of the managers were not
familiar with training programs and, possibly certification programs in HF/E, so they
might be deprived of many advantages of training programs.
Managers’ Knowledge on Human Factors and Ergonomics
Managers were asked to rate their knowledge on HF/E. A five point Likert-scale
was provided for them to evaluate their knowledge. The results of answers are shown in
Table 9.
Table 9 Managers’ knowledge on human factor and ergonomics
Poor
(1)
Fair
(2)
Average
(3)
Very Good
(4)
Excellent
(5)
Rating
Average
(N) (%) (N) (%) (N) (%) (N) (%) (N) (%)
11 17.2 13 20.3 24 37.5 15 23.4 1 1.6 2.72
According to results of managers’ self-evaluations, the average knowledge level
was 2.72. This result means that the knowledge level was between fair and average, but it
was close to the average level of knowledge. Only a quarter of the managers thought that
their knowledge level was higher than the average level; very good (23.4%) or excellent
(1.6%). Eleven managers (17.2%) rated their knowledge level as poor. Consequently, the
result of the knowledge level scale was compatible with the hypothesis that managers
know little about HF/E. There is no significant statistical relationship between managers’
demographic properties and their knowledge levels (Table 10).
59
Table 10 Statistical analysis of managers’ demographic properties and knowledge level
State Education NAICS Employees Experience
in FI Position Experience
in P
Knowledge
Level
Ȥ26.391 8.532 6.854 8.293 2.844 10.637 3.964
p 0.172 0.383 0.553 0.405 0.944 0.223 0.860
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p
: p-value (The level of statistical significance).
Manager’s Preference for Information Resources Concerning
Human Factors and Ergonomics
Amazing developments in science and technology have resulted in the higher
availability of information resources concerning HF/E. The higher availability of
information resources provides a better learning environment for managers (Broberg
2007). However, managers’ preferences on information resources vary from manager to
manager. According to the result of the question about preference of the information
resources (Figure 10), reading books, journals, newspapers, and magazines (76.7%) were
the most preferred information resources.
The Internet (54.7%) was listed as a very important resource for learning about
HF/E as well. Some of the managers mentioned that they had attended conferences,
meetings, and conventions (42.4%), consulted a human factors specialist or an
ergonomist expert (23.4%), used computer software (7.8%), and applied to other types of
information resources (6.3%). Unfortunately, 17.2 percent of managers mentioned that
they were not aware of information resources about HF/E. That is, those managers did
not use any of these information resources to learn about HF/E.
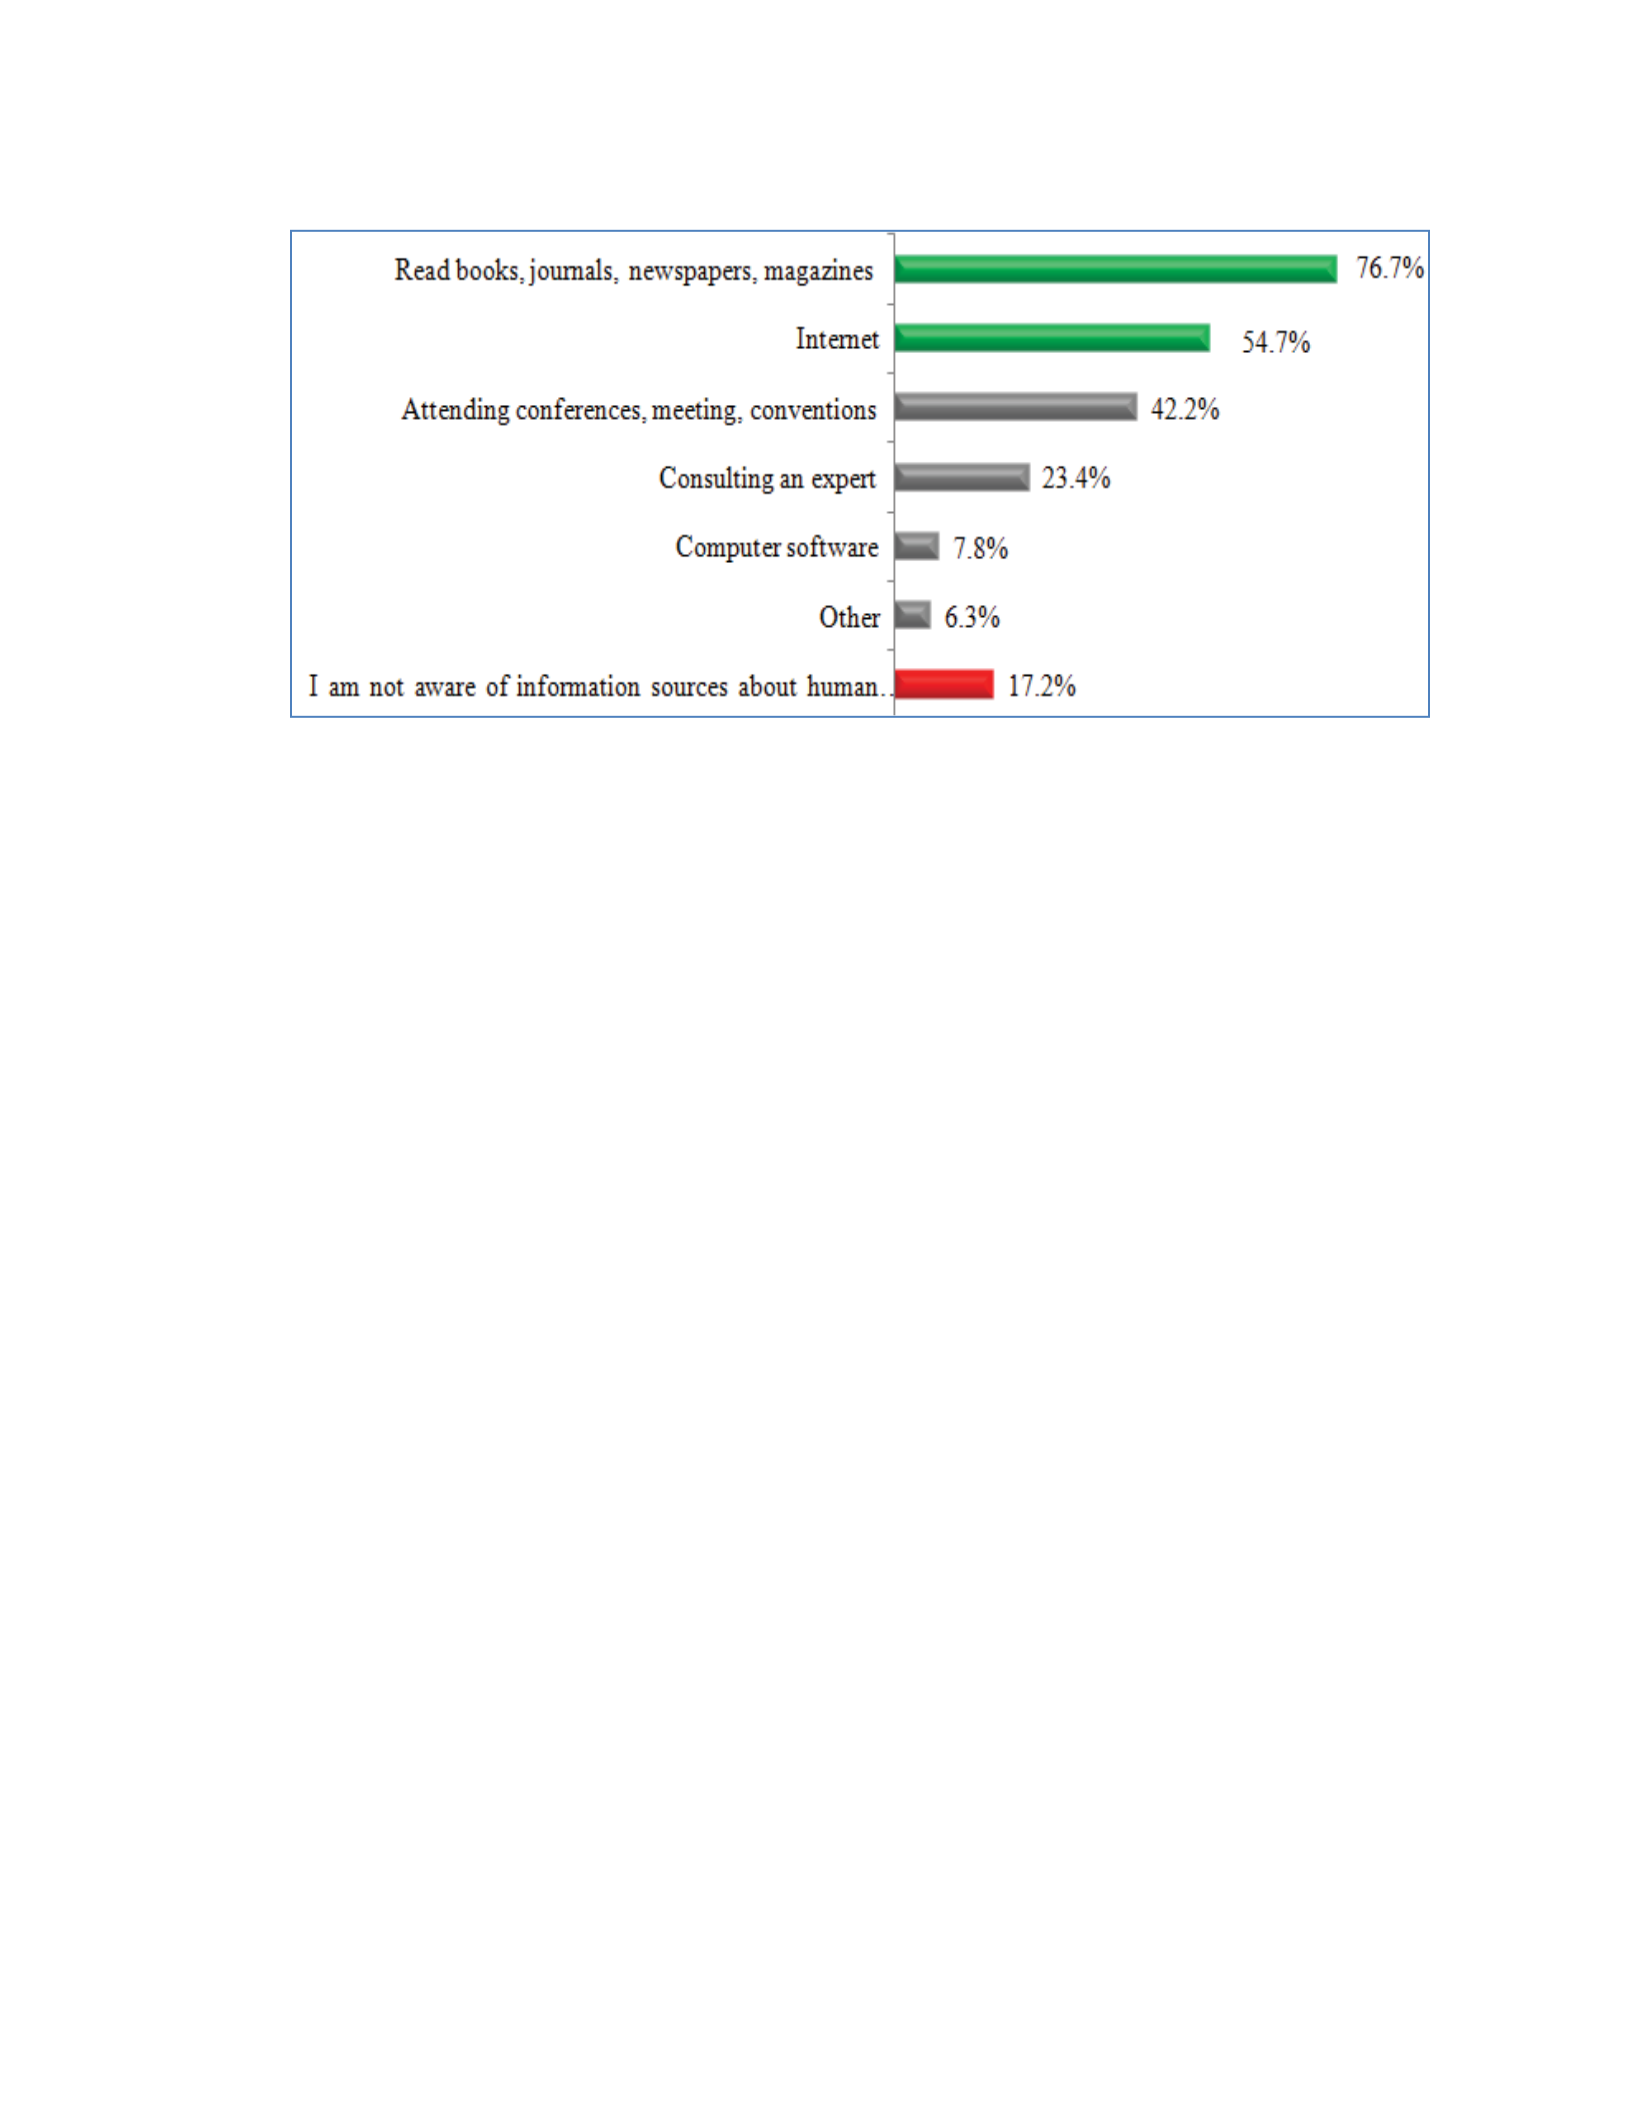
60
Figure 10 Managers’ preference for information resources related human factors and
ergonomics
The Chi-square statistic analysis was performed to understand the relationship
between managers’ demographic properties and managers’ preferences on information
resources. The result of the analysis is given in the Table 11.
The statistical analysis showed that there was a significant relationship between
the states where the companies were located and whether managers attended conferences,
meetings, and conventions (p RUFRQVXOWHGDQH[SHUWS0DQDJHUVIURP
Mississippi attended conferences, meetings, and conventions more than managers from
the other states (Figure 11). They also consulted an HF/E expert to get information or to
find a solution to their problems (Figure 12).
61
Table 11 Statistical analysis of managers’ demographic properties and preference for
information resource
State Education NAICS Employees
Experience
in FI
Position
Experience
in P
Reading Ȥ20.188 1.880 1.525 2.545 0.729 0.051 0.507
p0.665 0.391 0.467 0.280 0.695 0.975 0.776
Attending meetings Ȥ212.290 0.341 0.698 6.006 0.953 7.102 0.094
p0.000* 0.843 0.705 0.050* 0.621 0.029* 0.954
Internet
Ȥ20.001 2.536 1.056 0.643 0.367 1.488 0.077
p0.981 0.281 0.590 0.725 0.832 0.475 0.962
Consulting to an expert Ȥ24.862 2.509 0.410 1.771 0.729 2.180 1.415
p0.027* 0.285 0.851 0.413 0.695 0.336 0.493
Computer software
Ȥ22.163 1.593 1.506 1.827 0.693 0.702 0.471
p0.141 0.451 0.471 0.401 0.707 0.704 0.790
Not aware of
information sources
Ȥ20.047 1.545 6.569 3.003 0.102 2.677 1.476
p0.828 0.462 0.037* 0.223 0.905 0.262 0.478
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p
: p-value (The level of statistical significance).
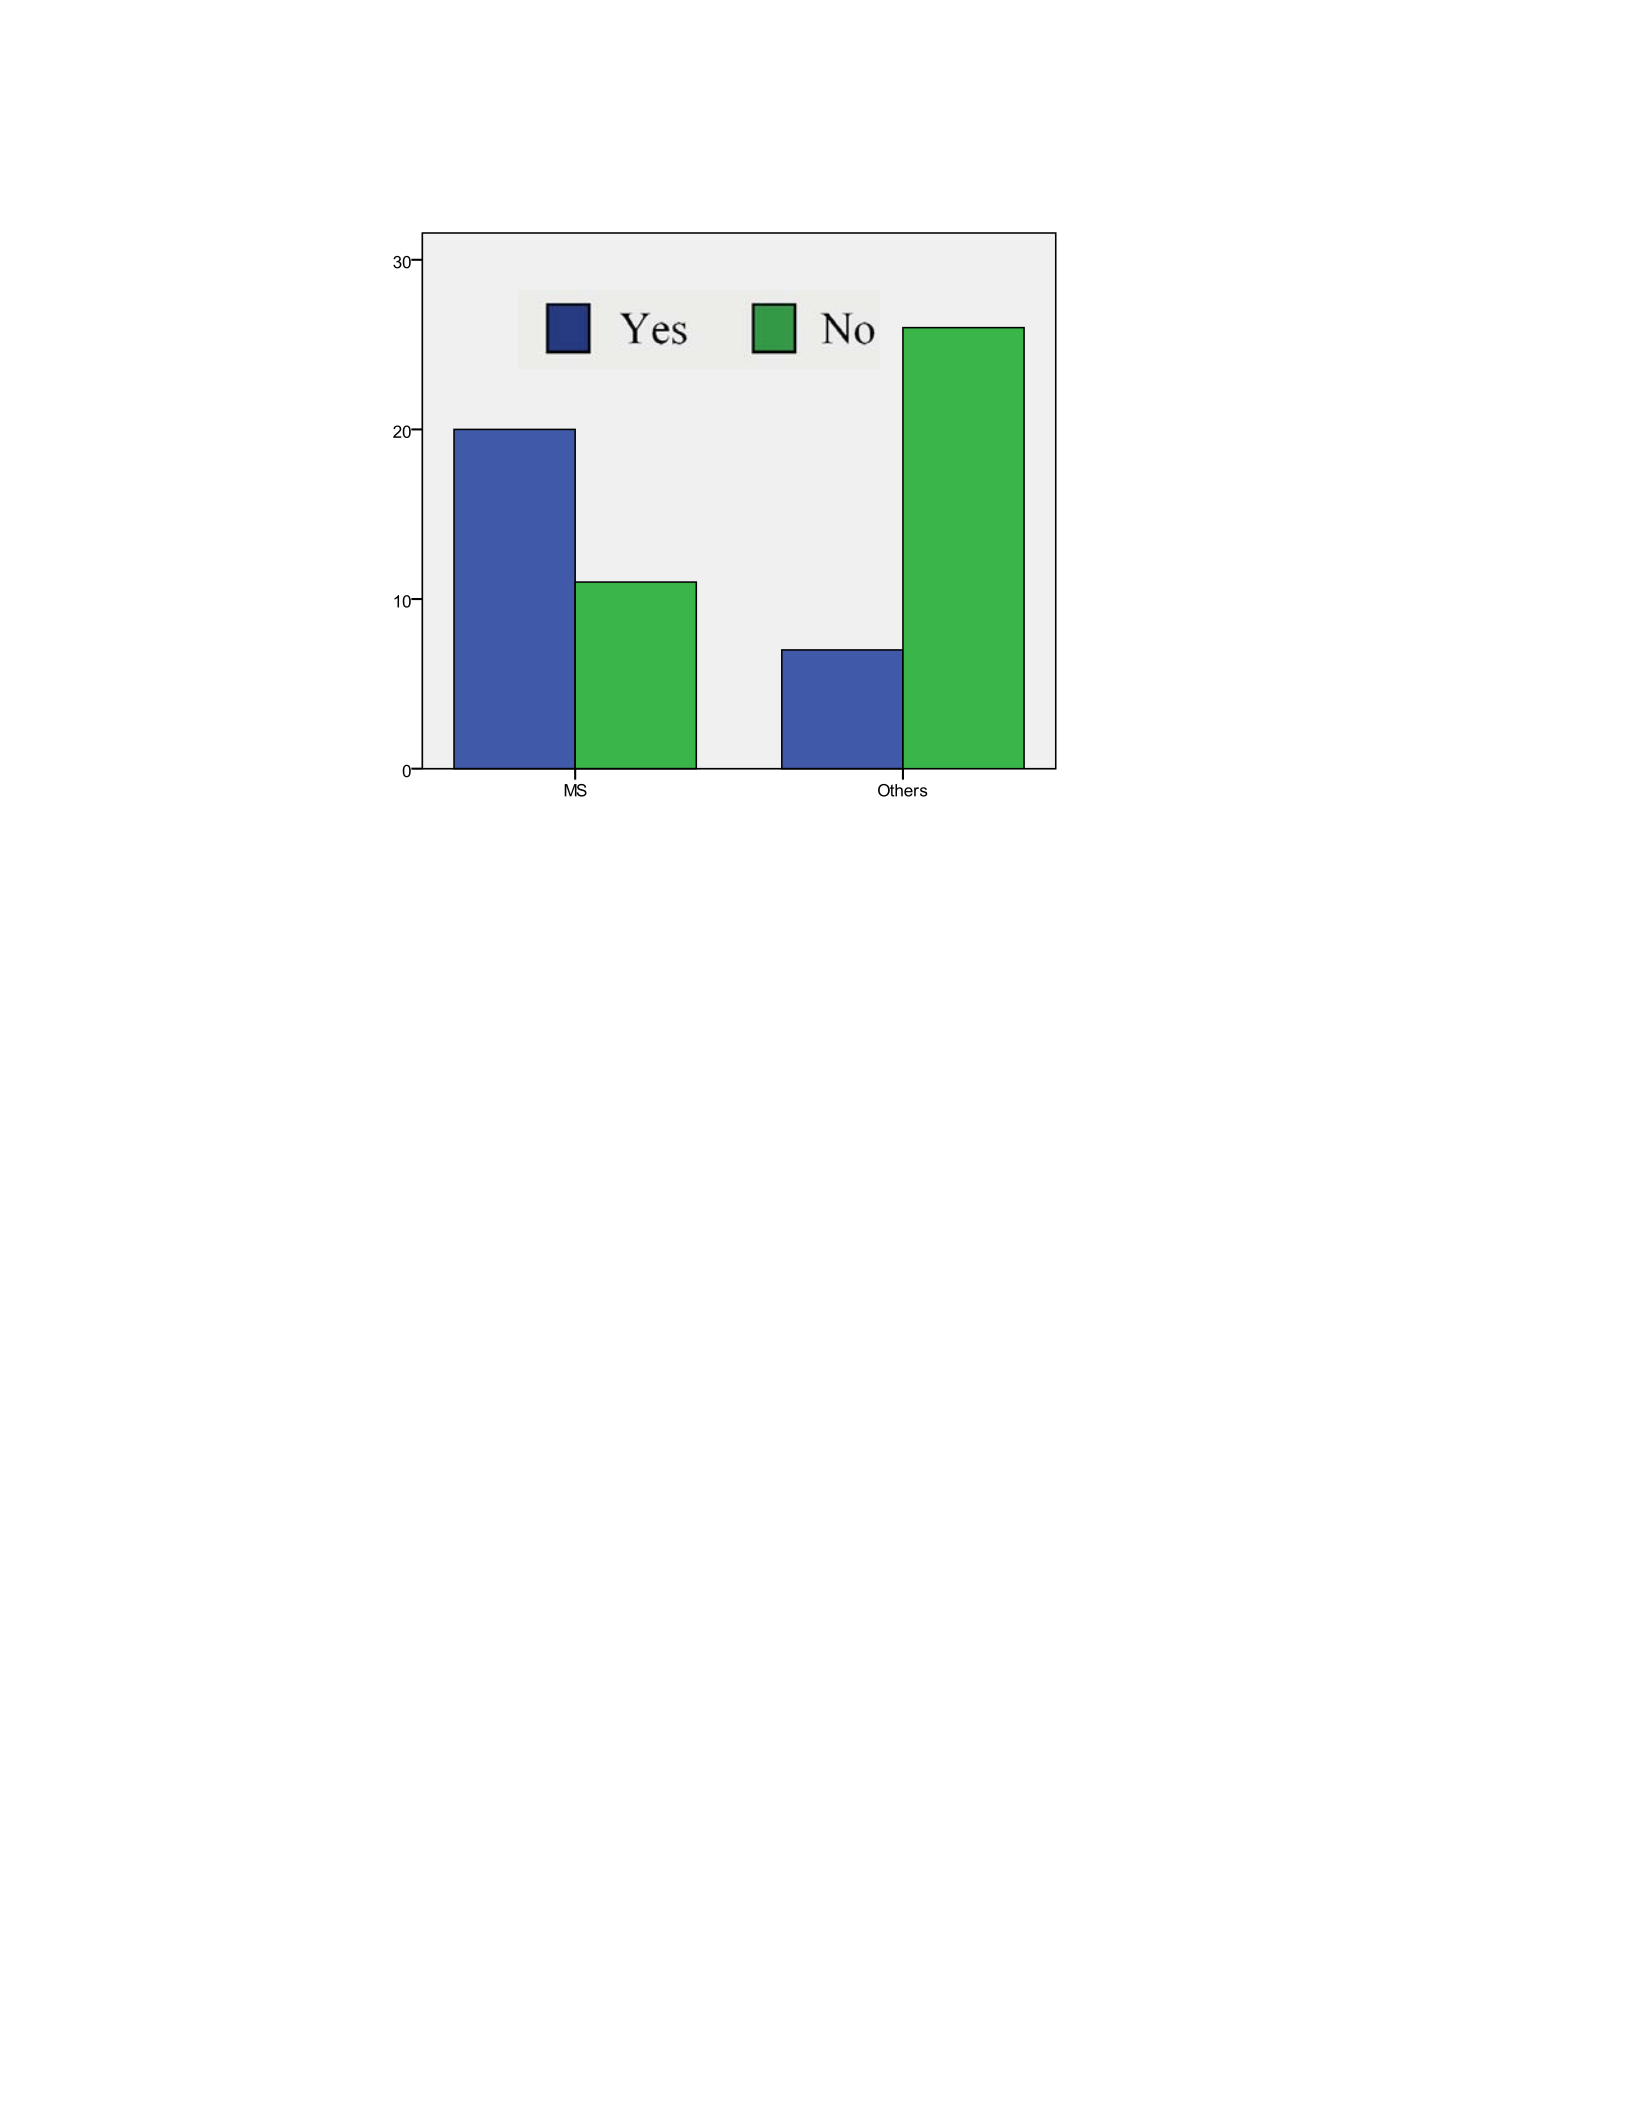
62
Figure 11 Conference, meeting, and convention attendance of managers from
Mississippi vs. other states
In fact, attending conferences, meetings, and conventions was a function of the
companies’ resource availability. Larger size companies have more resources to allocate
for conferences, meetings, and conventions related to HF/E. This significant relationship
(p FDQEe seen in Figure 13.
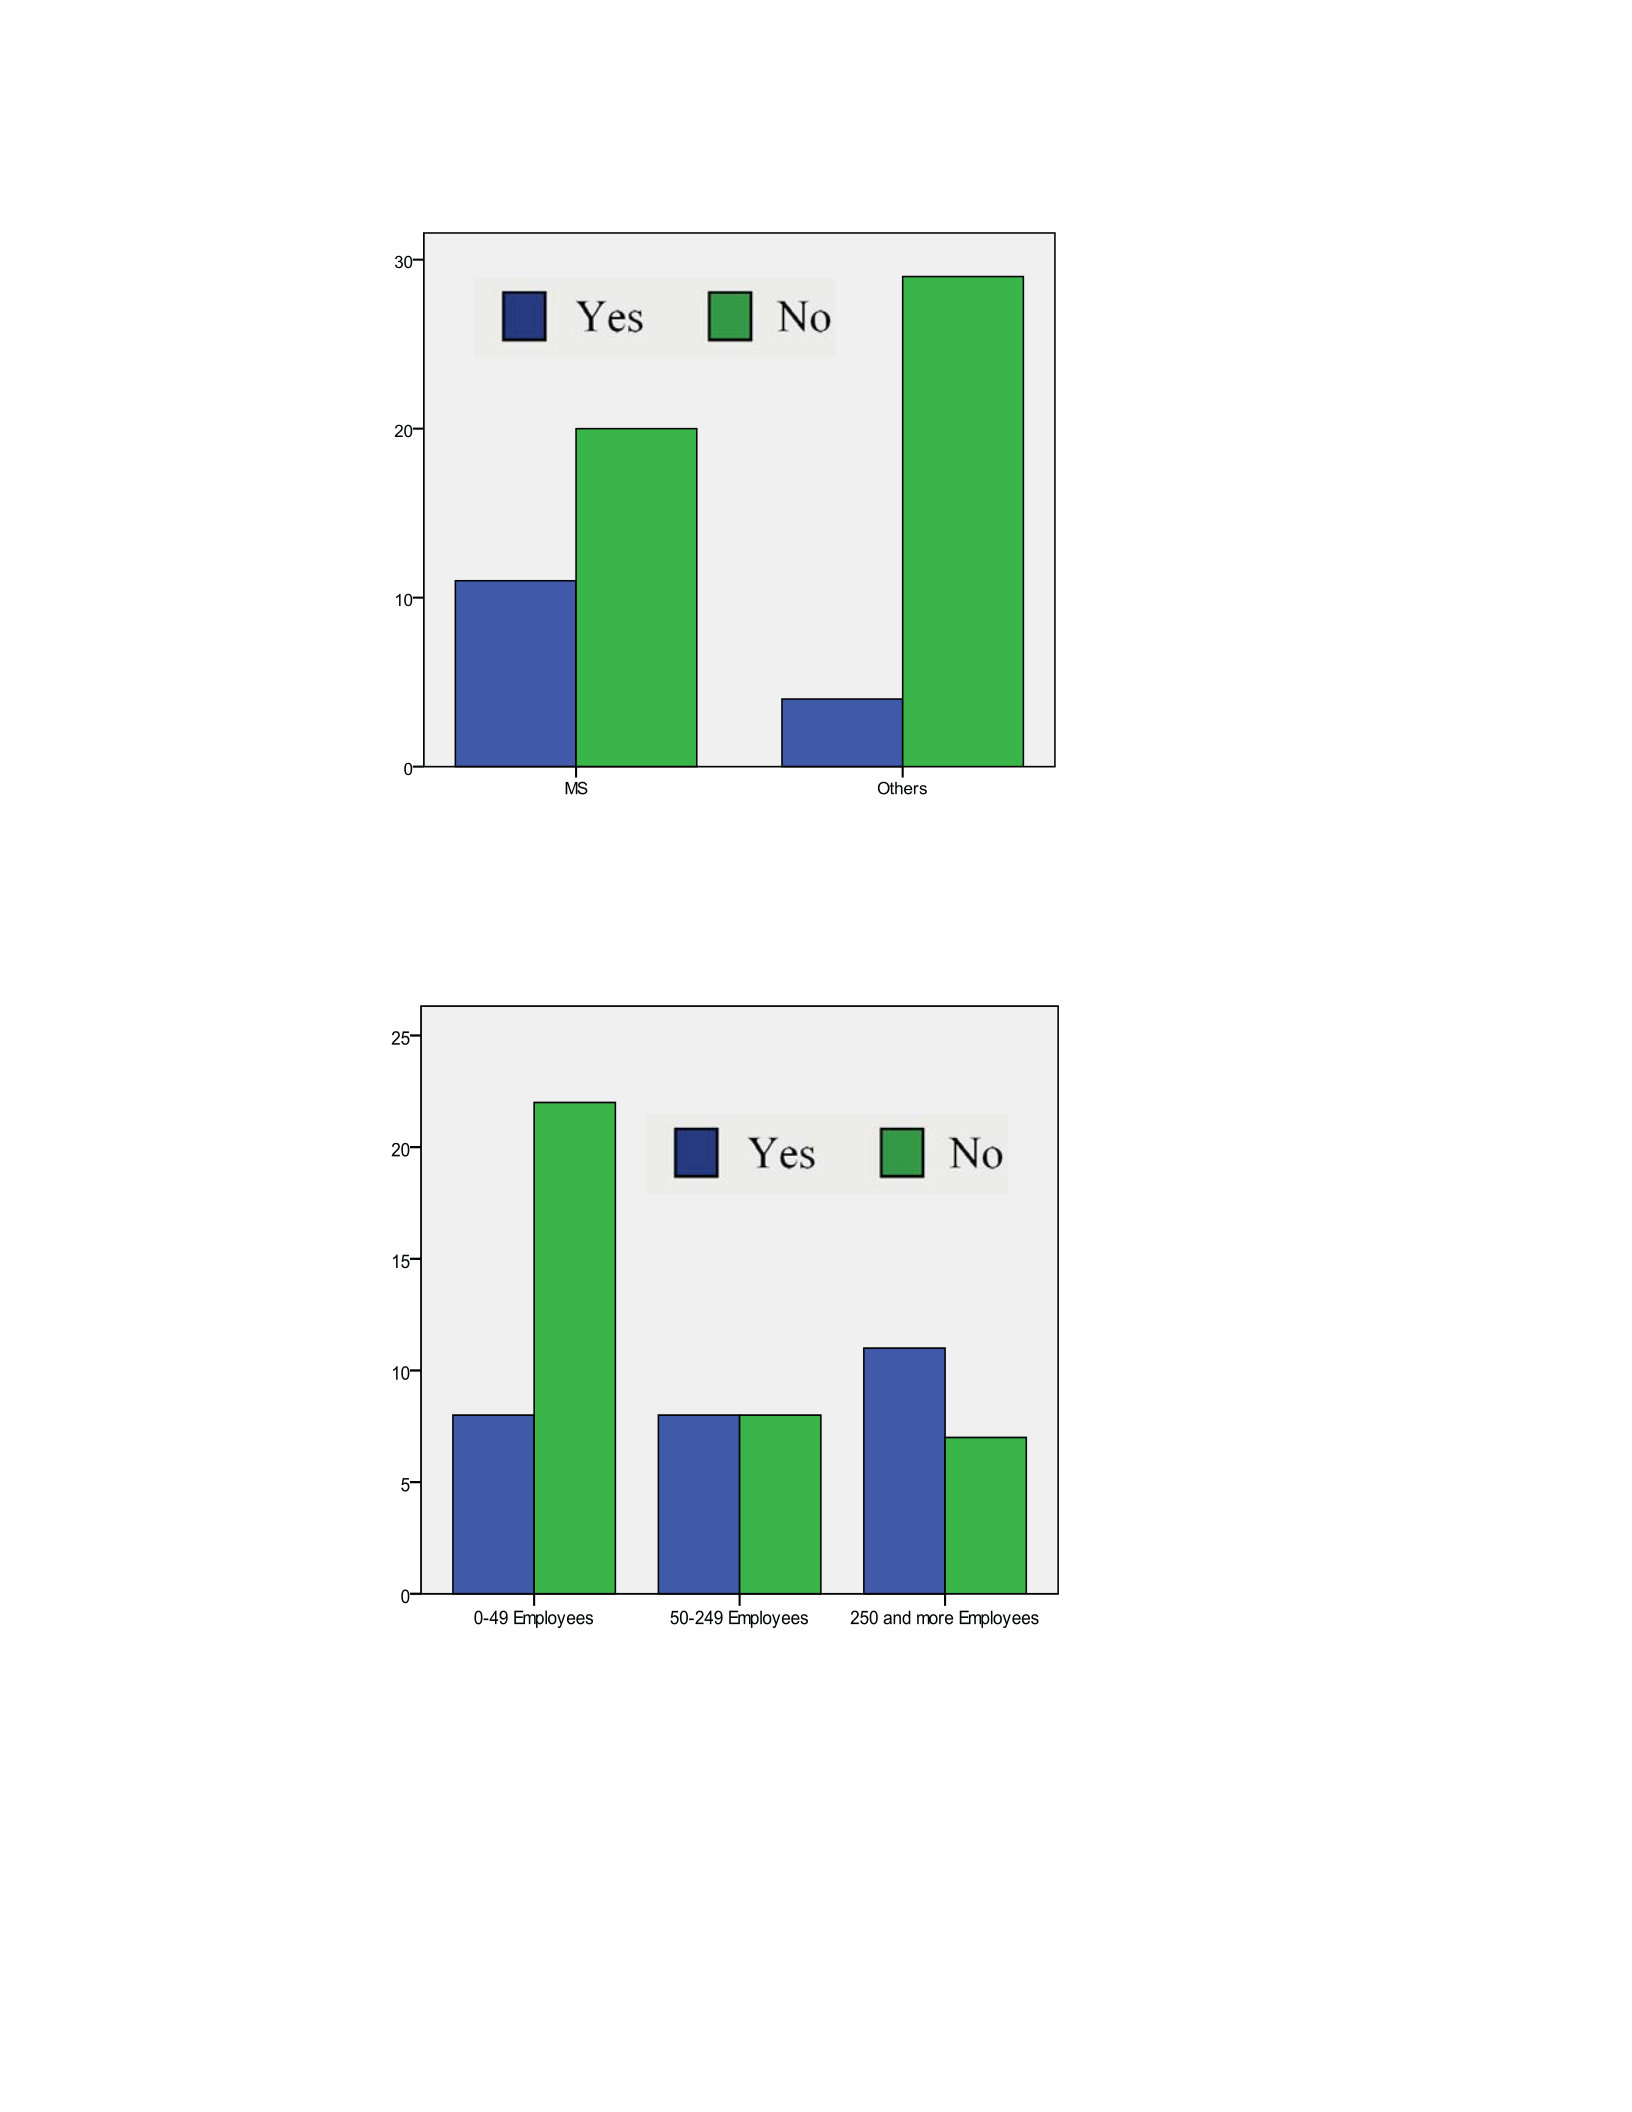
63
Figure 12 Consulting an expert of human factors and ergonomics,
Mississippi managers vs. other states
Figure 13 Conference, meeting, and convention attendance of
managers from different size companies
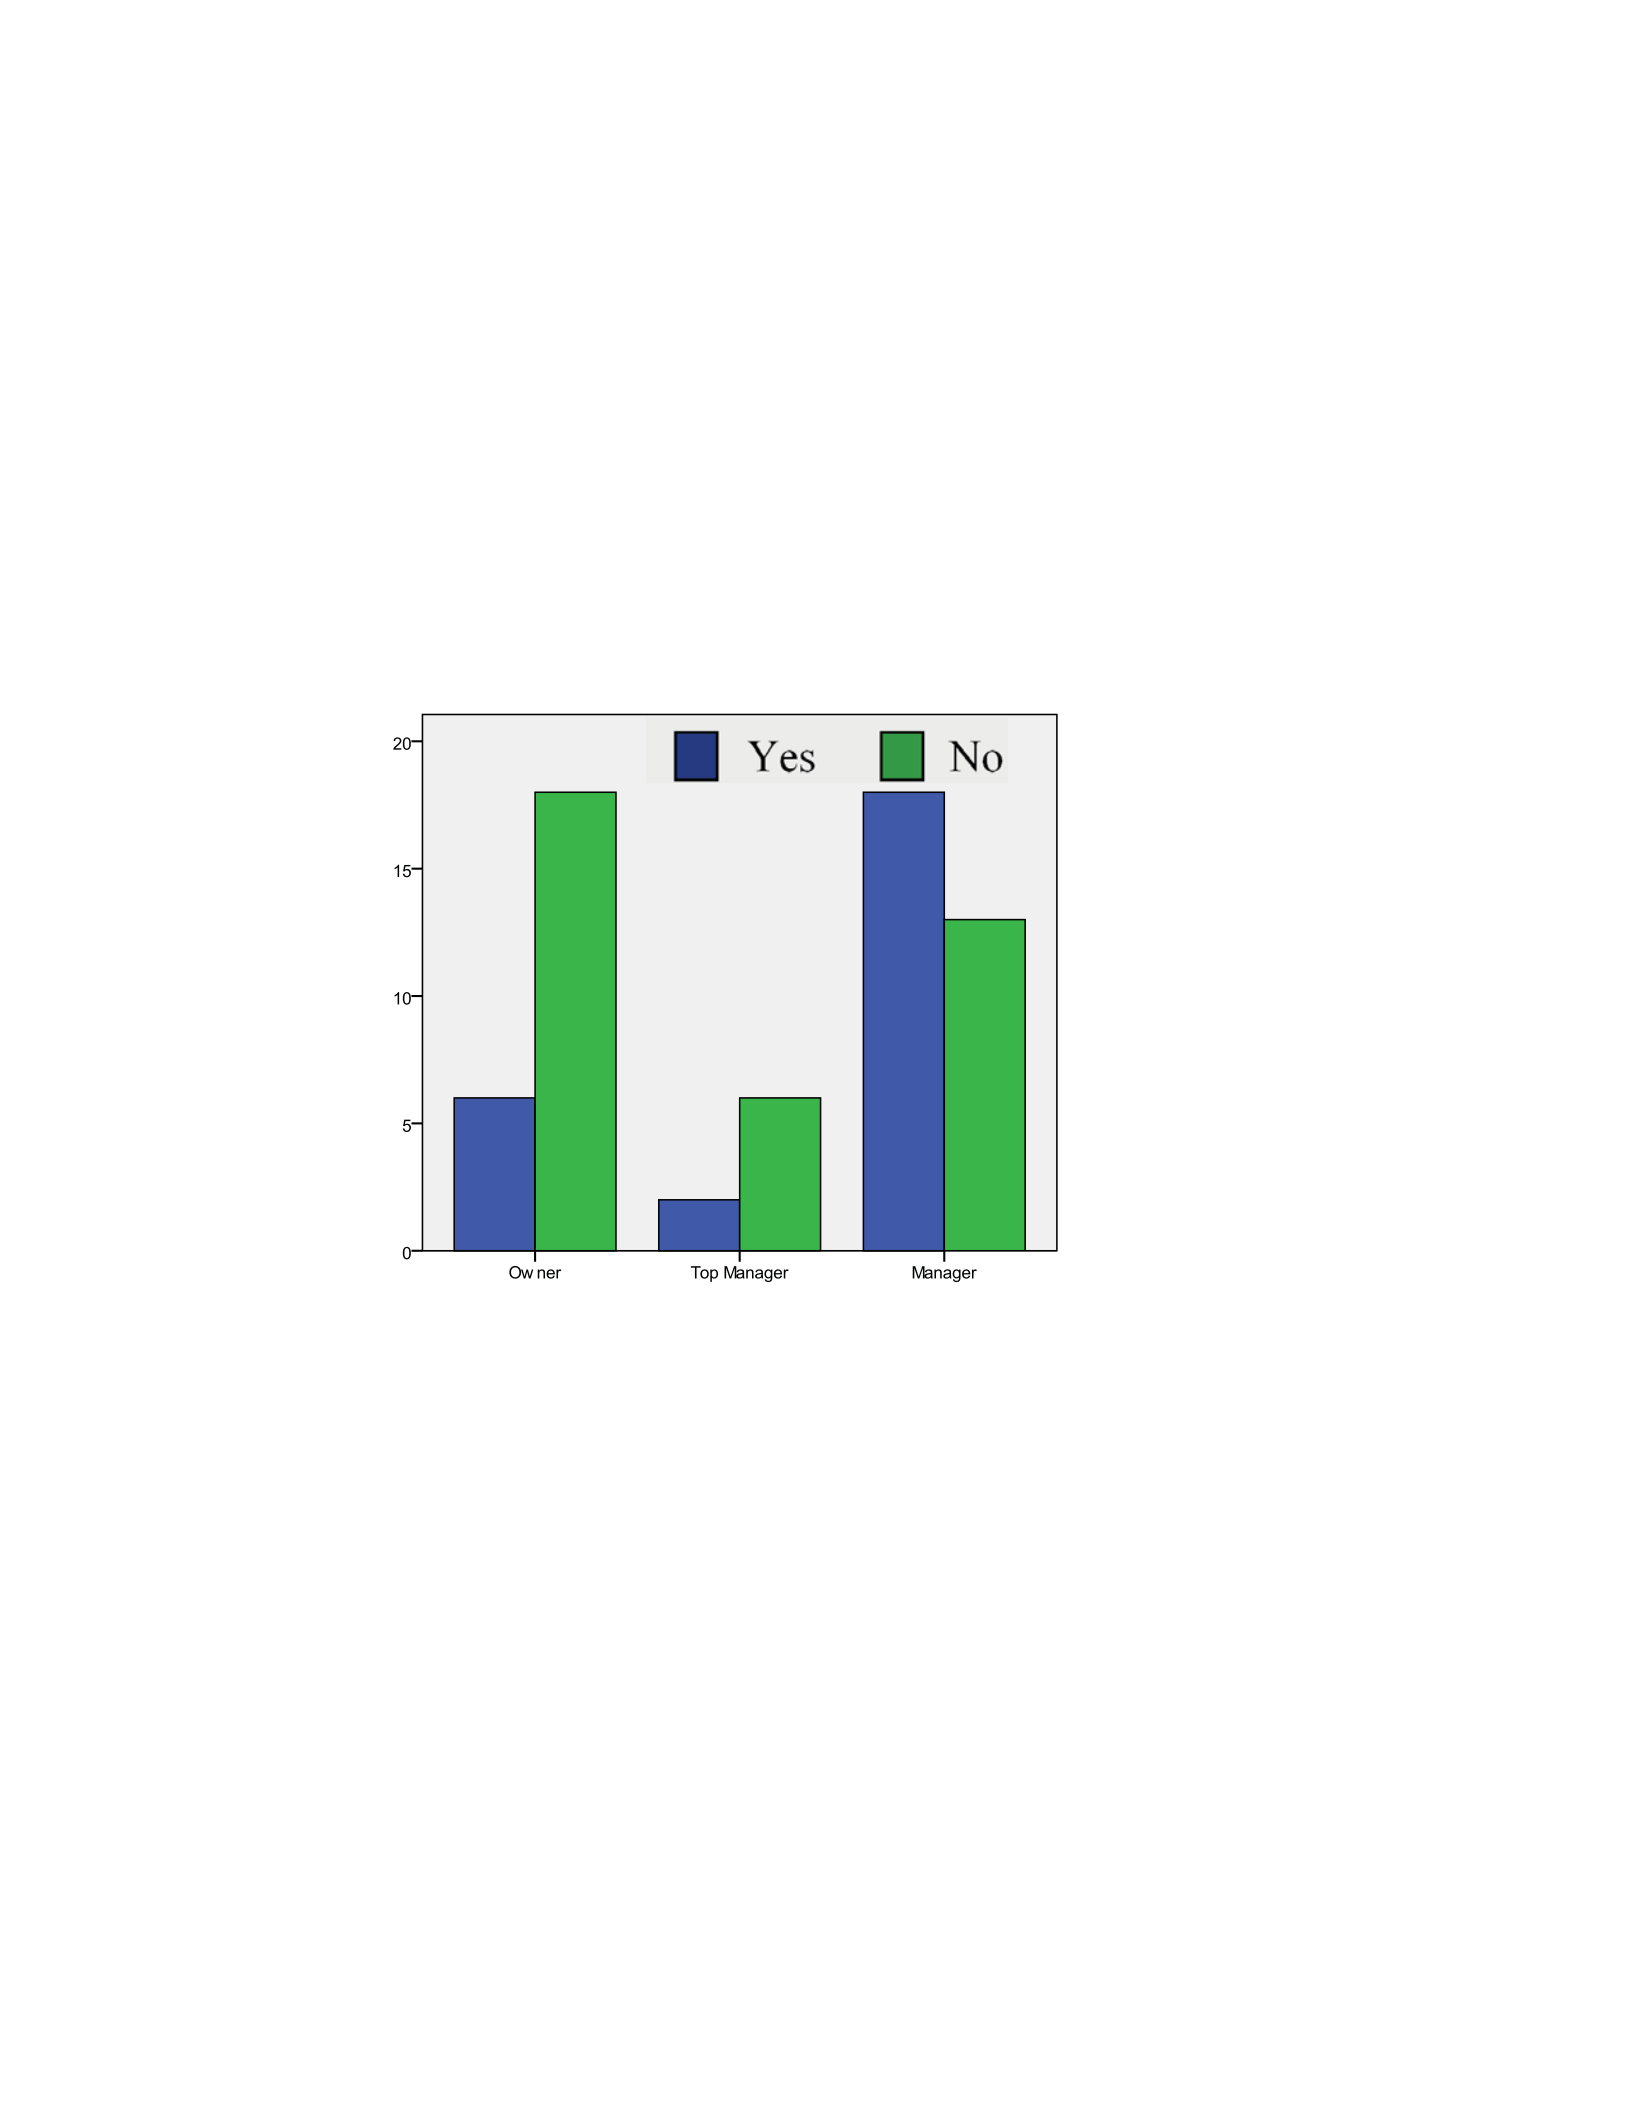
64
There is also a significant relationship (p EHWZHHQDWWHQGLQJFRQIHUHQFHV
meetings, and conventions and managers’ current positions. As can be seen from Figure
14, most of the owners (75%) have not attended any conferences, meetings, and
conventions related to HF/E. However, a huge number of lower-level managers (58.1 %)
attended these meetings. Hence, the interpretation that lower-level managers paid more
attention than owners would not be wrong.
Figure 14 Conference, meeting and convention attendance of
managers from different positions
The subsector of industry is also a factor of awareness about information
resources related to HF/E (Figure 15). Managers in the subsectors of the Household and
Institutional Furniture, Kitchen Cabinet Manufacturing (NAICS 3371), and the Office
Furniture (including Fixtures) Manufacturing (NAICS 3372) expressed that they were not
aware of any information resources related to HF/E. On the other hand, managers who
were working in the Other Furniture Related Product Manufacturing (NAICS 3379)
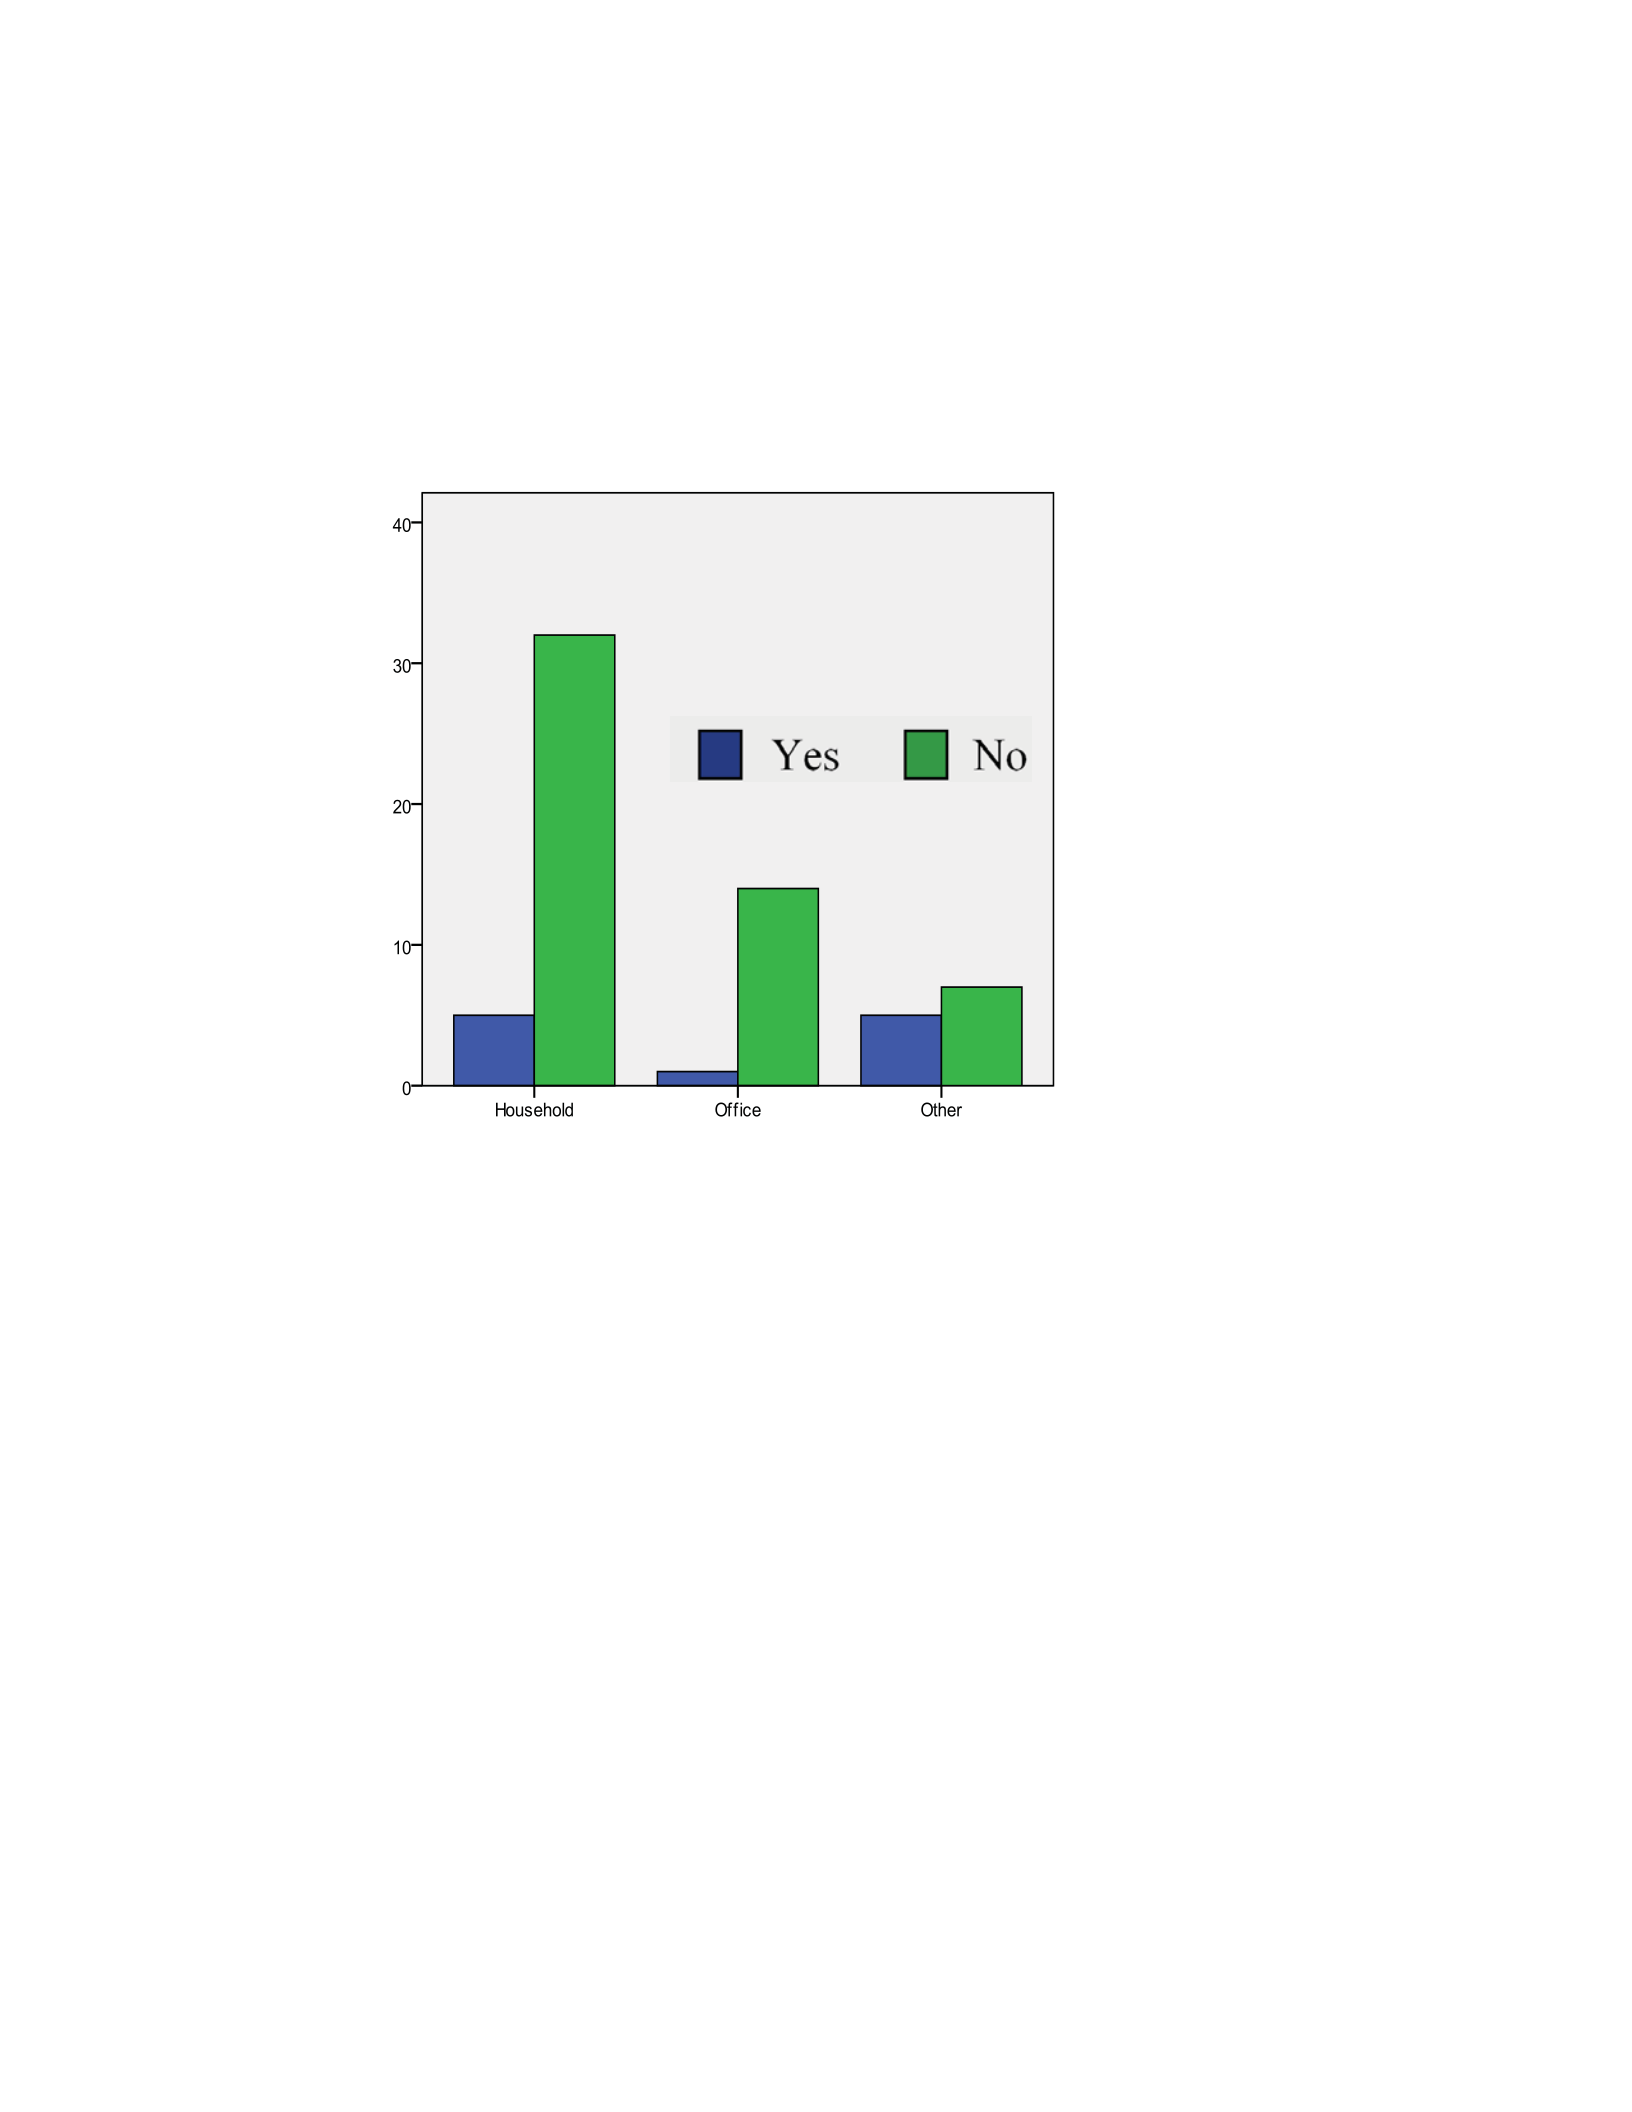
65
subsector showed more awareness of information resources. This relationship is
significantly found in the Chi-square test (p %HFDXVHRWKHUUHODWLRQVKLSVZere
not significantly important, they are not presented here.
Figure 15 Awareness of information resources of managers from different industry
subsectors
Managers’ Opinion on Likely Benefits and Disadvantages of
Human Factors and Ergonomics
Likely Benefits of Human Factors and Ergonomics
There is no doubt that HF/E has a myriad of advantages for both employees and
organizations. Hendrick (1996b) shortly expresses the advantages of HF/E programs in
his comprehensive literature review titled “Good Ergonomics is Good Economics.” He
explained the advantages of HF/E by saying, “a wonderful common ground for labor and

66
management collaboration, for invariably both can benefit – managers, in terms of
reduced costs and improved productivity, employees in terms of improved safety, health,
comfort, usability of tools and equipment, including software, and improved quality of
work” (Hendrick 1996b). However, the problem is whether managers are aware of these
advantages or not.
To mention some current literature for the benefits of HF/E would be beneficial
before sharing the result of the survey. The advantages of HF/E can be given in two
chapters: advantages to workers and advantages to the organization.
Advantages of Human Factors and Ergonomics to Workers
Many researchers agree that HF/E interventions result in an increase in
productivity (Pulat and Alexander 1991; Sundstrom 2000; Hendrick and Kleiner 2002;
Beevis and Slade 2003; Douphrate and Rosecrance 2004; Mirka 2005; Goggins et al.
2008). A research found that five years after a HF/E program was initiated in one
company, productivity more than doubled (MacLeod and Morris 1996).
Improved workers’ well-being (Michael and Wiedenbeck 2004), reduced work-
related injuries (MacLeod and Morris 1996; AFMA and NCDOL 2003; Goggins et al.
2008), increased worker's safety (MWCC 2008), improved quality of work life (Goggins
et al. 2008), more satisfied workers (Schneider 1985; Sundstrom 2000; Hendrick and
Kleiner 2002), improved worker morale (Michael and Wiedenbeck 2004), increased
worker comfort (MacLeod and Morris 1996), less absenteeism (Schneider 1985;
Douphrate and Rosecrance 2004; Michael and Wiedenbeck 2004; Goggins et al. 2008),

67
and more energetic workers (Michael and Wiedenbeck 2004) are some other advantages
of HF/E for workers.
Advantages of Human Factors and Ergonomics to the Organization
In addition to aiding workers, HF/E has many other advantages for companies,
such as increased system productivity (Pulat and Alexander 1991; MacLeod 1995;
Michael and Wiedenbeck 2004), less disruption on the system, less employee turnover
(Schneider 1985; Douphrate and Rosecrance 2004; Michael and Wiedenbeck 2004;
Goggins et al. 2008), reduced labor costs (Pulat and Alexander 1991; Douphrate and
Rosecrance 2004; Goggins et al. 2008; MWCC 2008), reduced workers’ compensation
costs (Pulat and Alexander 1991; MacLeod 1995; Hendrick and Kleiner 2002; AFMA
and NCDOL 2003; Beevis and Slade 2003; Douphrate and Rosecrance 2004; Goggins et
al. 2008; Kim et al. 2008; MWCC 2008), improvements in the working environment
(Beevis and Slade 2003), reduced maintenance personnel and materials (Hendrick and
Kleiner 2002; Hendrick 2003), and reduced training time for employees.
Occupational injuries and illnesses are unappreciated contributors to the total
burden of health care costs in the U.S. (Leigh et al. 1997). If companies reduced costs
with the help of HF/E, they could allocate resources to designing new products to be
brought to market (Douphrate and Rosecrance 2004). Therefore, the reduction in costs
could result in high competitiveness ability for companies. Piegorsch (1994) found that a
20-30 percent reduction in furniture manufacturing costs can be obtained by only
redesigning work processes. It is obvious that reducing costs also results in increasing the
ability of survival in the business world. Likewise, HF/E programs can result in a positive

68
return on investment (Michael and Wiedenbeck 2004; Goggins et al. 2008) because of
reduced workers compensation cost savings (MacLeod and Morris 1996), improvements
in productivity (Schneider 1985; MacLeod and Morris 1996), reduced maintenance
errors, and increased safety (Robertson 2001).
There are several studies indicating that the quality of the product is fairly
influenced by HF/E (Dul and Neumann; Pulat and Alexander 1991; Eklund 1995; Drury
2000; Hendrick and Kleiner 2002; Douphrate and Rosecrance 2004; Michael and
Wiedenbeck 2004; Goggins et al. 2008). This can be caused from high job satisfaction in
workplaces. Eklund (1995) emphasizes the relationship between job satisfaction and high
quality task performance.
In this thesis, managers were asked to check whether they were aware of the
advantages of HF/E. The managers’ responses are given in the Figure 16 by the order of
frequency.
Over seventy five percent of managers believed that HF/E has an impact on
increasing workers’ performance (90.6%), reducing occupational injuries (87.5%),
decreasing worker’s compensation costs (75%), and improving work place quality (75%).
More than seventy percent of managers thought that HF/E also has an impact on
increasing satisfied workers (71.9%), worker safety (71.9%), and worker comfort
(70.3%). Less absenteeism (68.8%), cost savings (65.6%), higher morale (64.1%),
increased system productivity (57.8%), and better product quality (56.3%) were marked
by more than half of the managers. Less than half of the managers believed that HF/E has
positive impacts on higher competitiveness (42.4%), long-term company survival
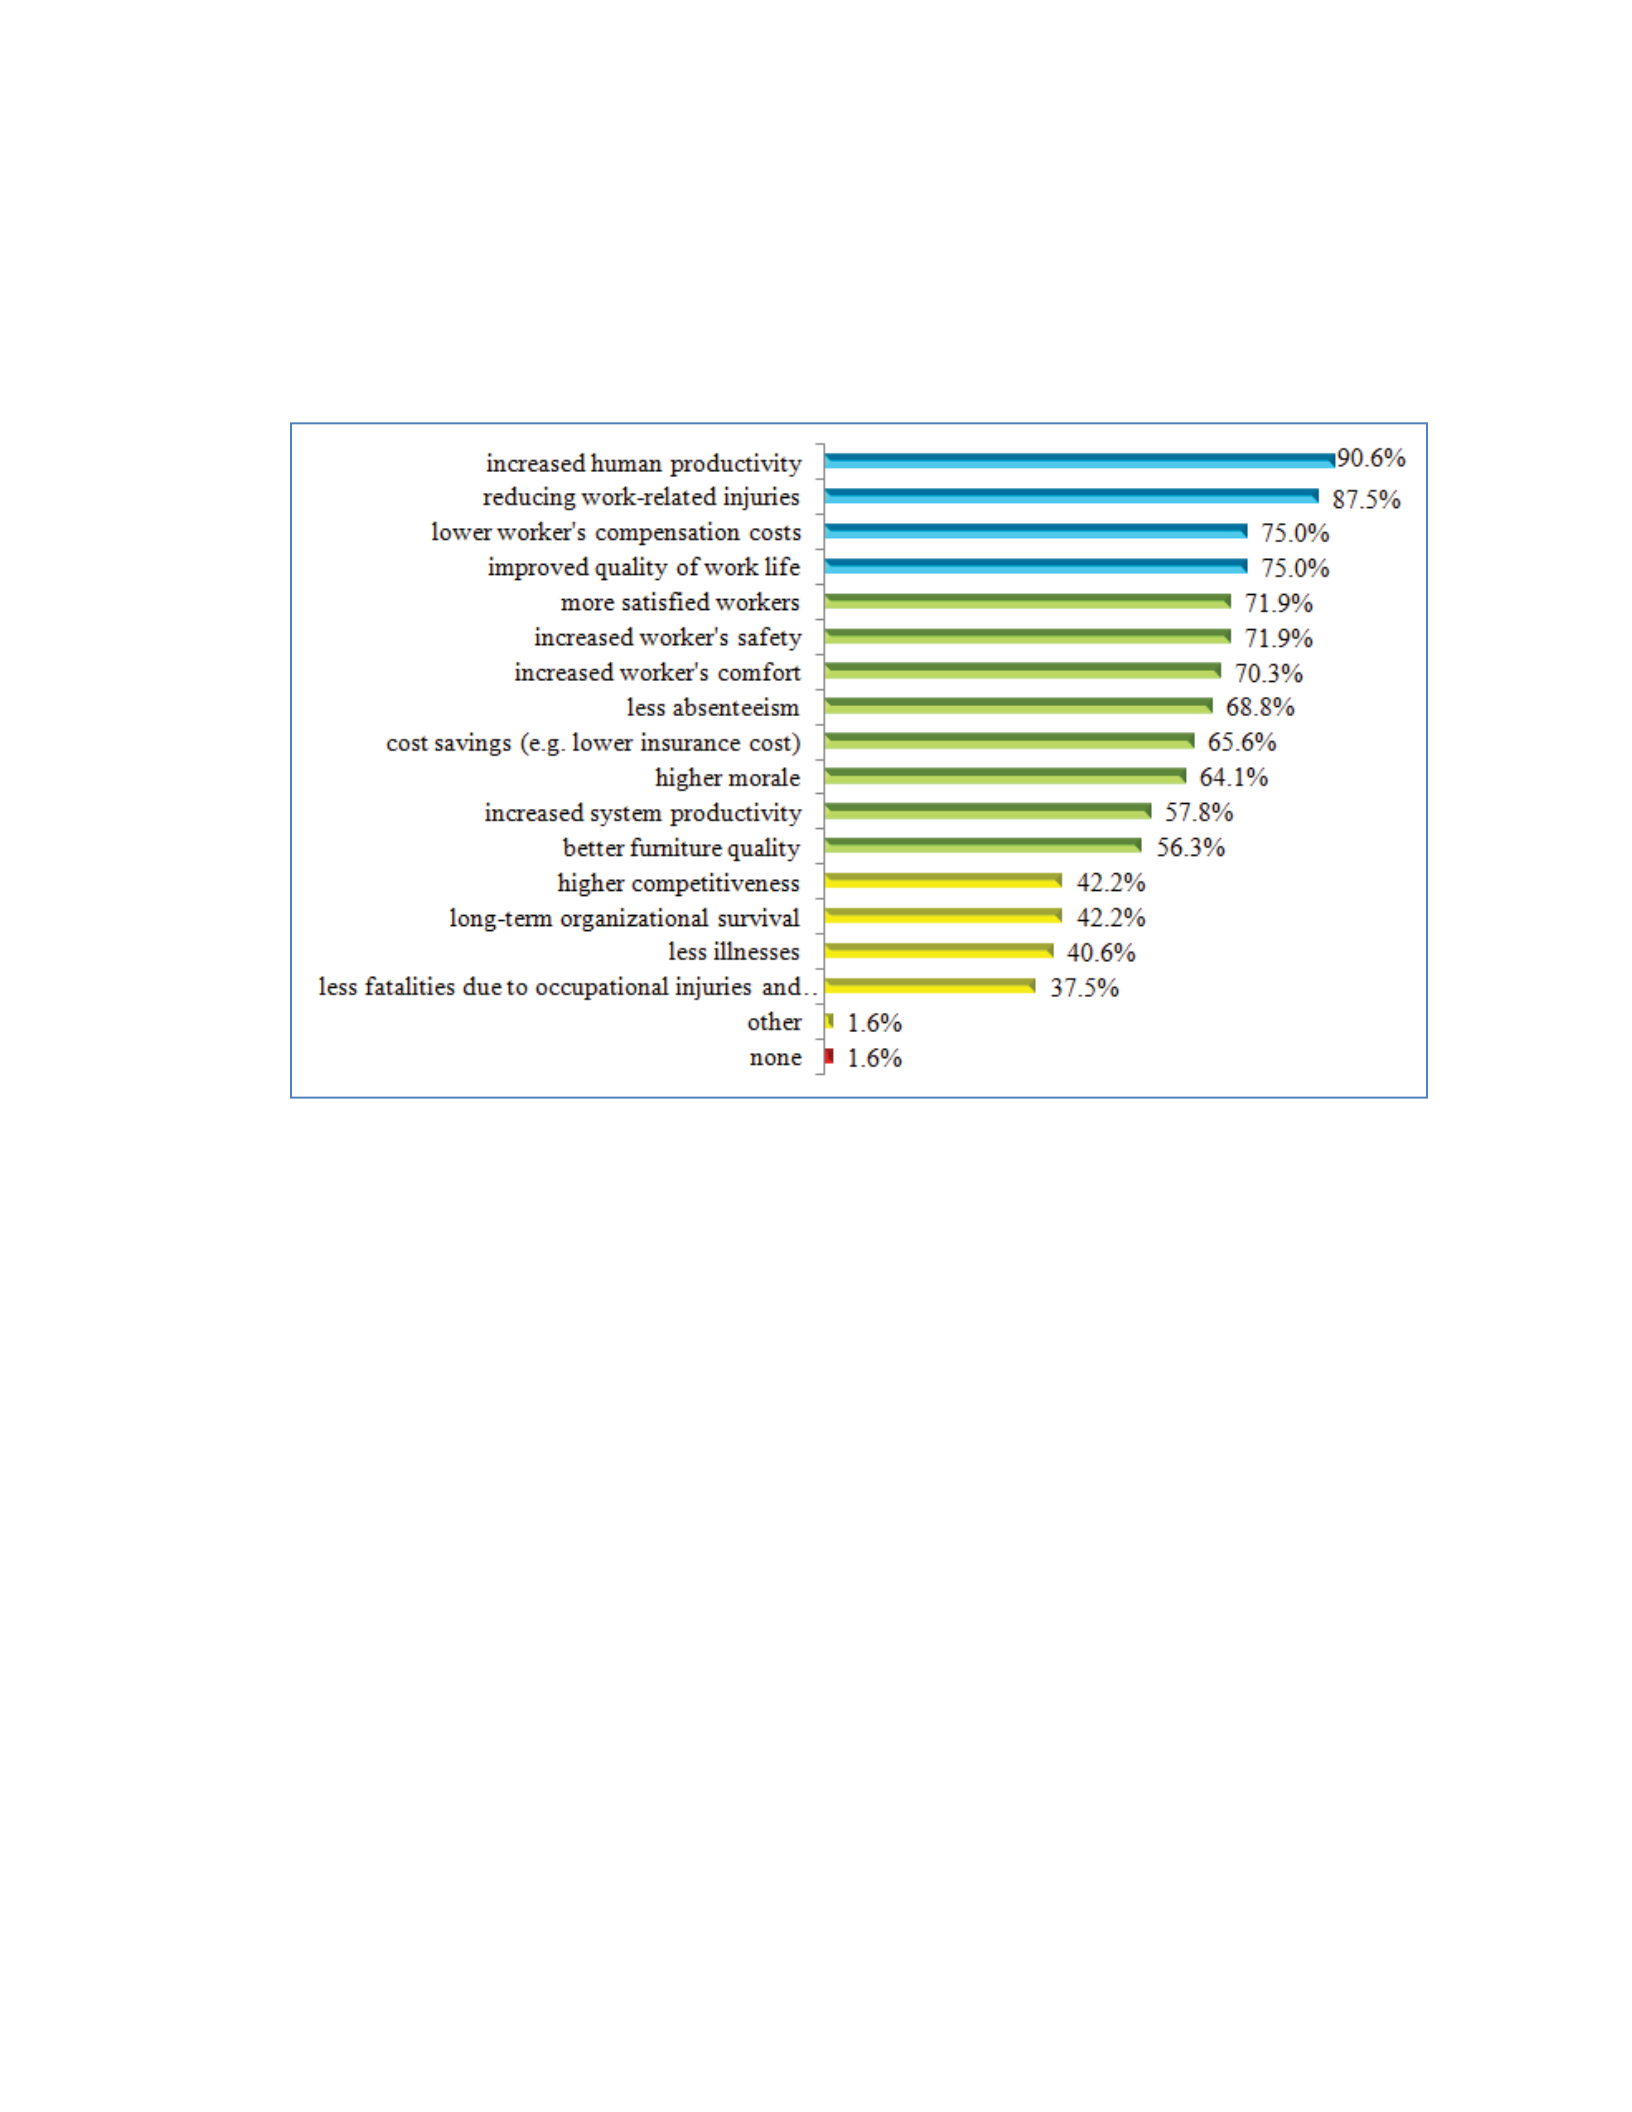
69
(42.4%), and reducing illnesses (40.6%) and fatalities (37.5%). On the other hand, one
manager mentioned that there were no benefits to HF/E.
Figure 16 Likely benefits of human factors and ergonomics
For the aim of finding significant relationships between managers’ demographic
profiles and managers’ opinions about the likely advantages of HF/E, a Chi-square
statistical test was performed. The results of this statistical test are given in Table 12.
70
Table 12 Statistical analysis of managers’ demographic properties and opinions
regarding the likely advantages of human factors and ergonomics
State Education NAICS Employees
Experience
in FI
Position
Experience in
P
Human Productivity Ȥ22.676 0.537 4.264 3.531 3.935 2.930 1.955
p0.102 0.764 0.119 0.171 0.140 0.231 0.376
System productivity Ȥ20.298 1.175 1.599 0.841 2.862 1.230 5.361
p0.585 0.556 0.450 0.657 0.239 0.541 0.069
Reduced injuries Ȥ24.728 1.109 2.277 3.619 5.435 2.524 2.699
p0.030* 0.574 0.320 0.164 0.066 0.283 0.259
Less illnesses Ȥ20.043 1.335 3.061 0.178 3.457 0.826 0.719
p0.836 0.513 0.216 0.915 0.178 0.662 0.698
Less absenteeism Ȥ23.960 4.325 0.094 2.851 2.583 2.799 3.898
p0.047 0.115 0.954 0.240 0.275 0.247 0.142
Lower compensation Ȥ24.692 1.925 4.930 7.563 5.179 10.394 0.672
p0.030 0.382 0.085 0.023* 0.075 0.006* 0.715
Cost saving Ȥ28.873 0.395 4.921 6.009 1.036 7.240 2.116
p0.003 0.821 0.085 0.050* 0.596 0.027* 0.347
Satisfied workers Ȥ22.288 0.095 0.281 1.037 0.900 0.433 0.218
p0.130 0.954 0.869 0.595 0.638 0.805 0.897
Higher morale Ȥ21.245 0.097 0.789 0.077 2.018 1.344 1.378
p0.264 0.953 0.674 0.962 0.365 0.511 0.502
Quality of work life Ȥ22.523 1.354 0.653 0.452 0.810 1.184 0.828
p0.112 0.508 0.721 0.798 0.667 0.553 0.661
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p: p-value (The level of statistical significance).
71
Table 12 (continued)
State Education NAICS Employees
Experience
in FI
Position
Experience
in P
Workers comfort Ȥ20.434 1.366 2.880 0.052 1.524 2.349 1.114
p0.510 0.505 0.237 0.975 0.467 0.309 0.573
Worker safety Ȥ22.288 1.257 6.681 3.676 2.073 5.906 0.477
p0.130 0.533 0.035* 0.159 0.355 0.052 0.788
Less fatalities Ȥ21.506 5.366 2.906 0.646 0.115 1.469 1.860
p0.220 0.068 0.234 0.724 0.944 0.480 0.395
Furniture quality Ȥ25.292 2.010 0.179 0.429 0.039 0.535 1.122
p0.021* 0.366 0.914 0.807 0.981 0.765 0.571
Competitiveness Ȥ23.945 1.937 0.048 1.838 1.978 3.748 1.103
p0.047* 0.380 0.976 0.399 0.372 0.154 0.576
Survive Ȥ23.945 0.661 0.799 1.251 5.082 2.974 5.854
p0.047* 0.719 0.671 0.535 0.079 0.226 0.054
No benefits Ȥ20.954 5.985 4.402 3.048 3.985 1.049 2.080
p0.329 0.050* 0.111 0.218 0.136 0.592 0.353
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value, p: p-value (The level of statistical significance).
According to the results of the statistical test, there were significant relationships
between the state where companies are located and managers’ opinion that HF/E has an
impact on injury reduction (p LQFUHDVHGIXUQLWXUHTXDOLW\SLQFUHDVHG
company competitiveness (p DQGHQVXULQJORQJHUVXUYLYDOS7KH
percent of managers who believed that HF/E does not have an impact on occupational
injury reduction were from other states, while the other 12.5 percent were from
Mississippi (Figure 17). In the same way, managers from other states believed less than
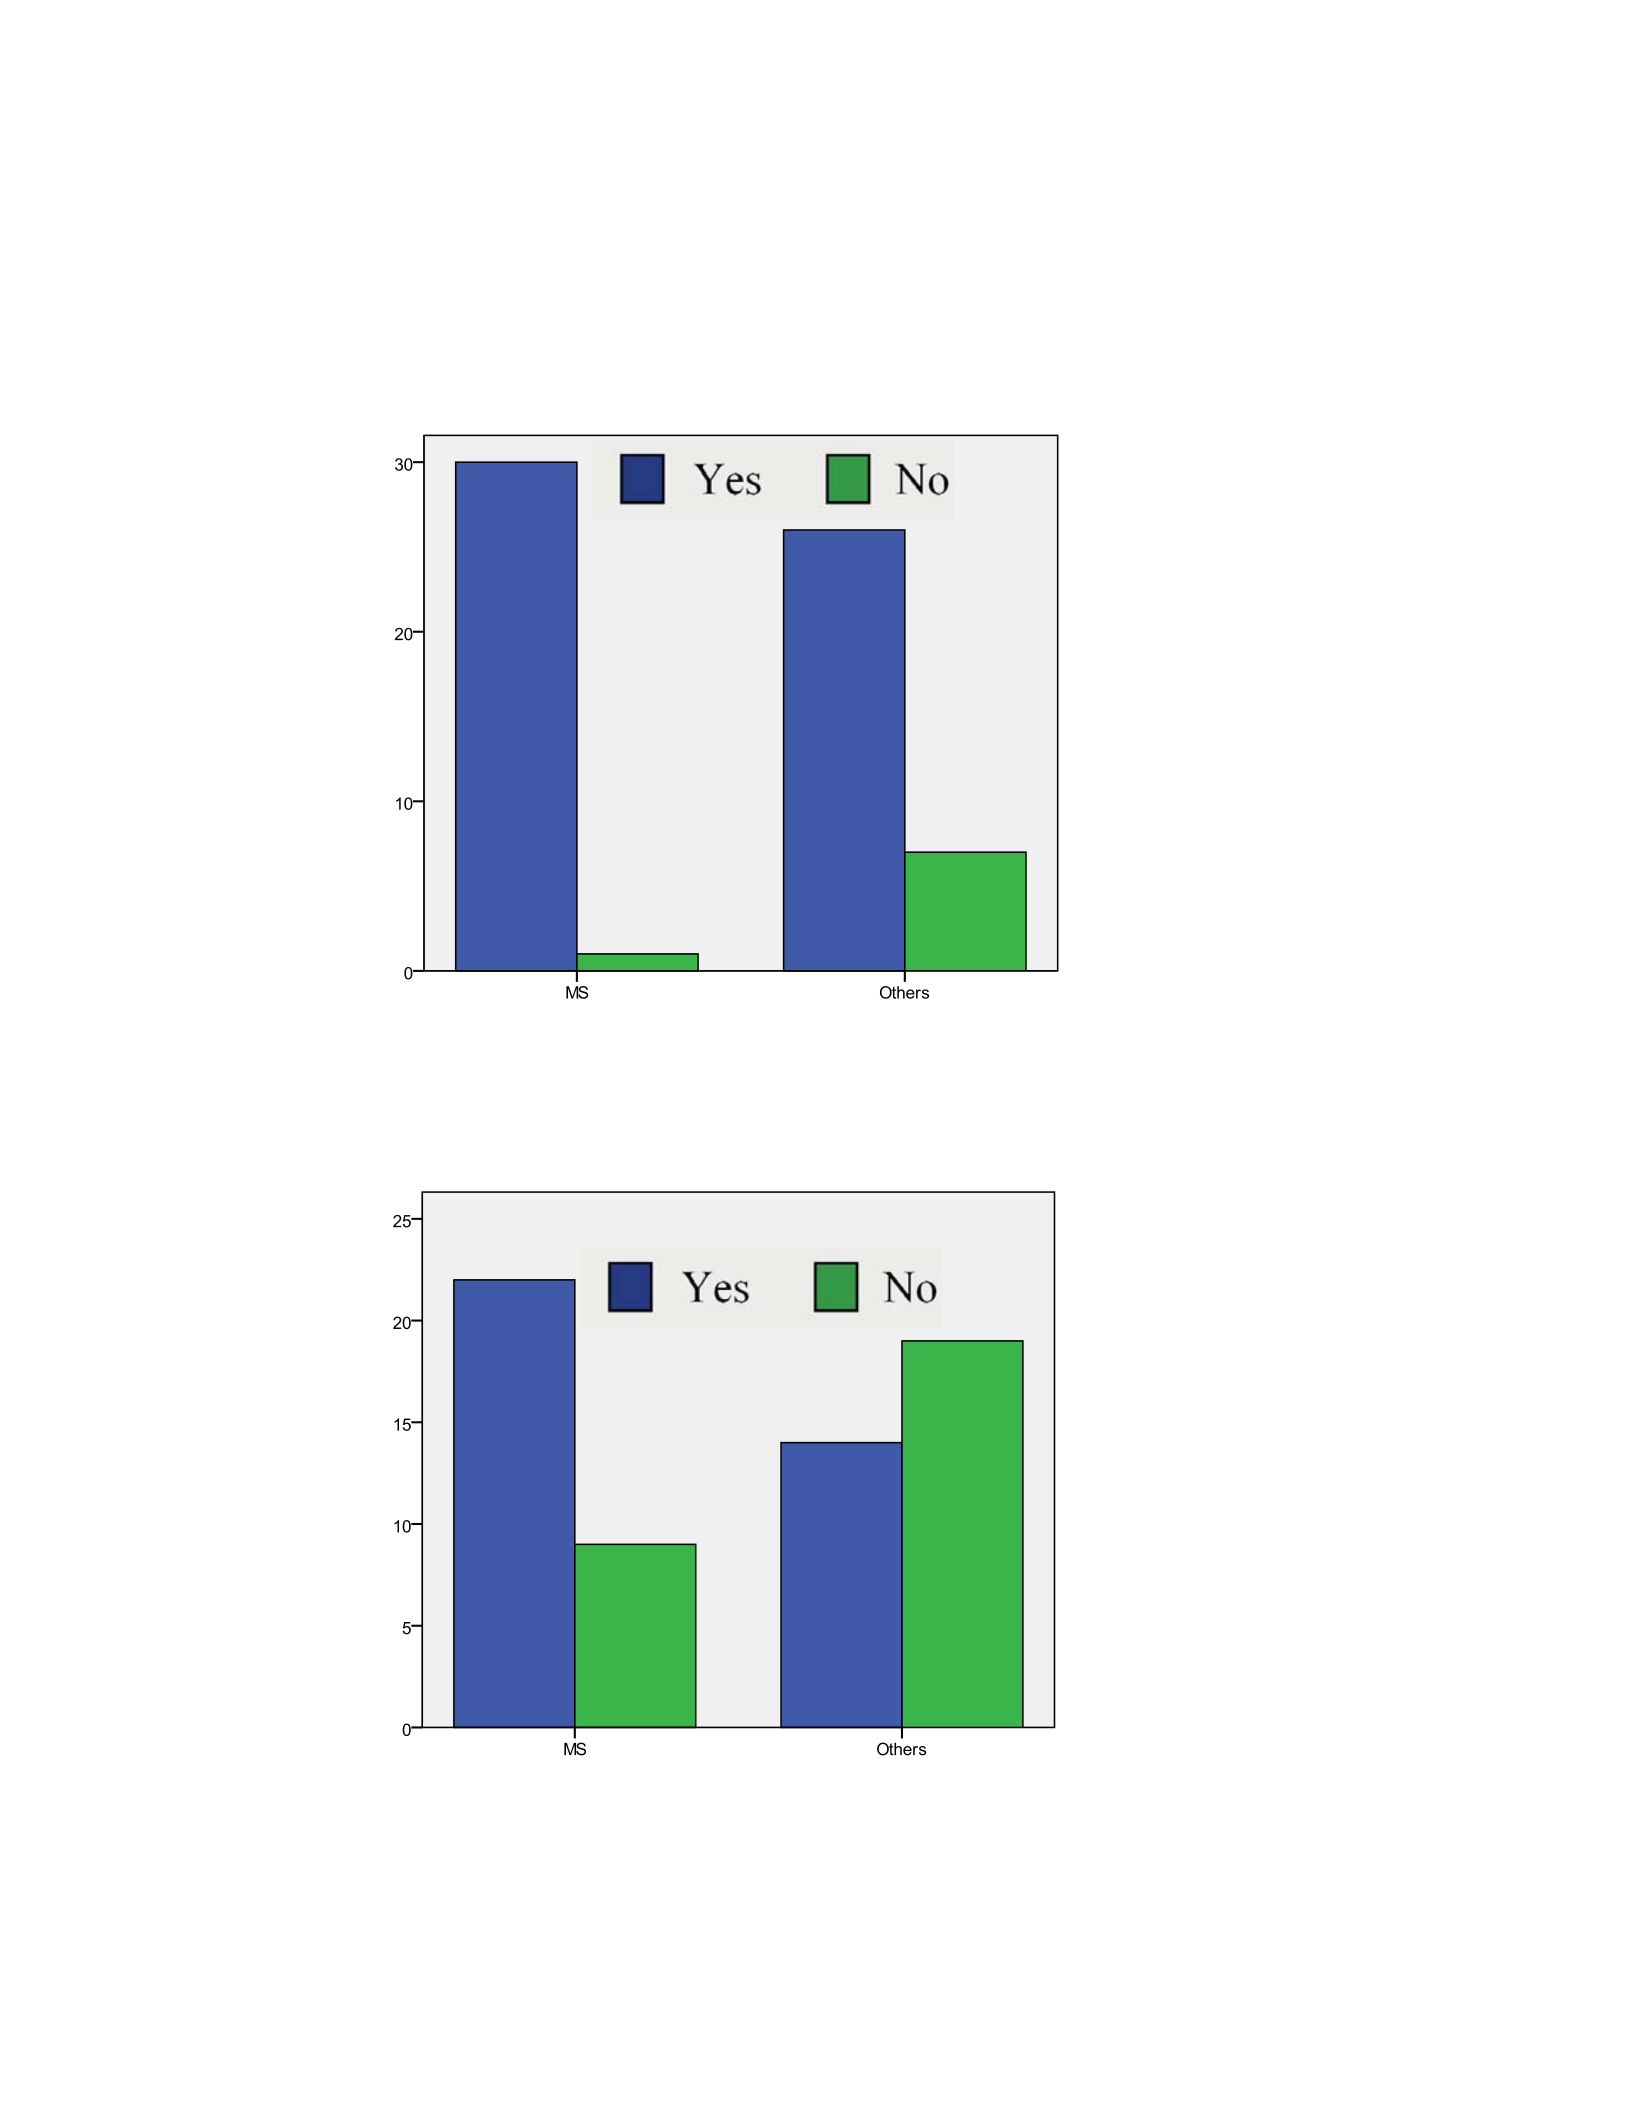
72
managers from Mississippi that HF/E results in increased furniture quality (Figure 18),
higher competitiveness (Figure 19), and longer survival time (Figure 20).
Figure 17 Mississippi vs. other states on managers’ opinions
about reduced injury benefits
Figure 18 Mississippi vs. other states on managers’ opinions
about product quality benefits
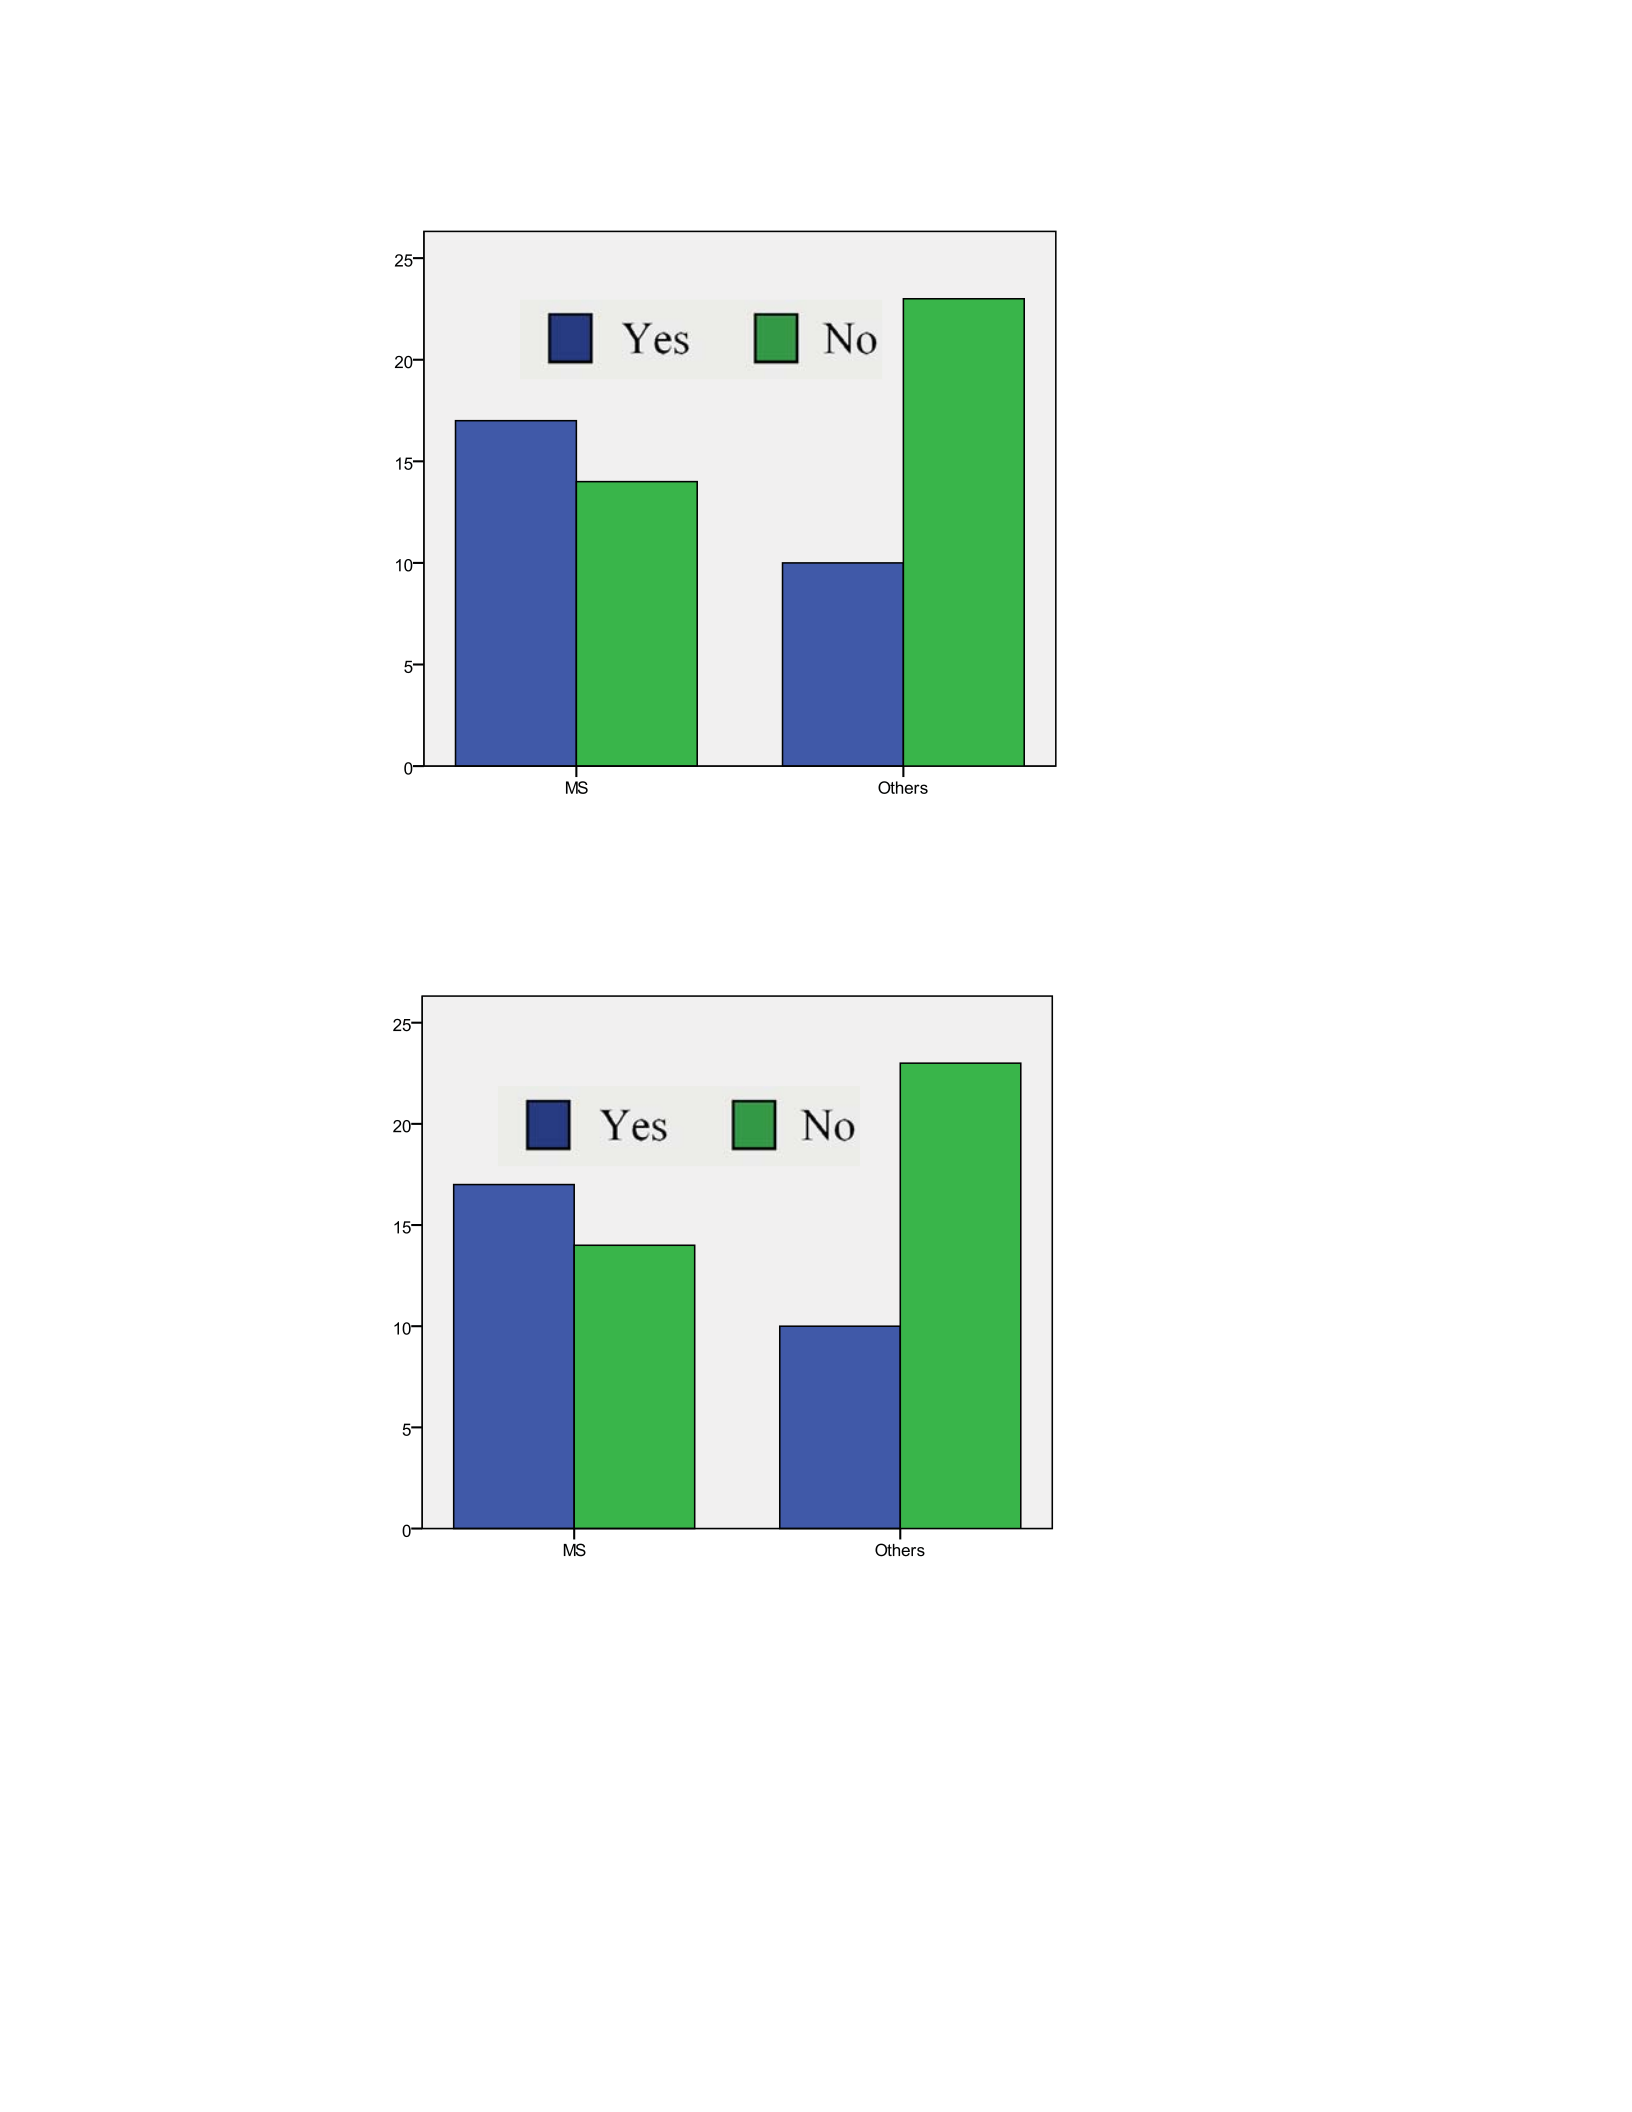
73
Figure 19 Mississippi vs. other states on managers’ opinions
about increased competitiveness benefits
Figure 20 Mississippi vs. other states on managers’ opinions
about increased survival time
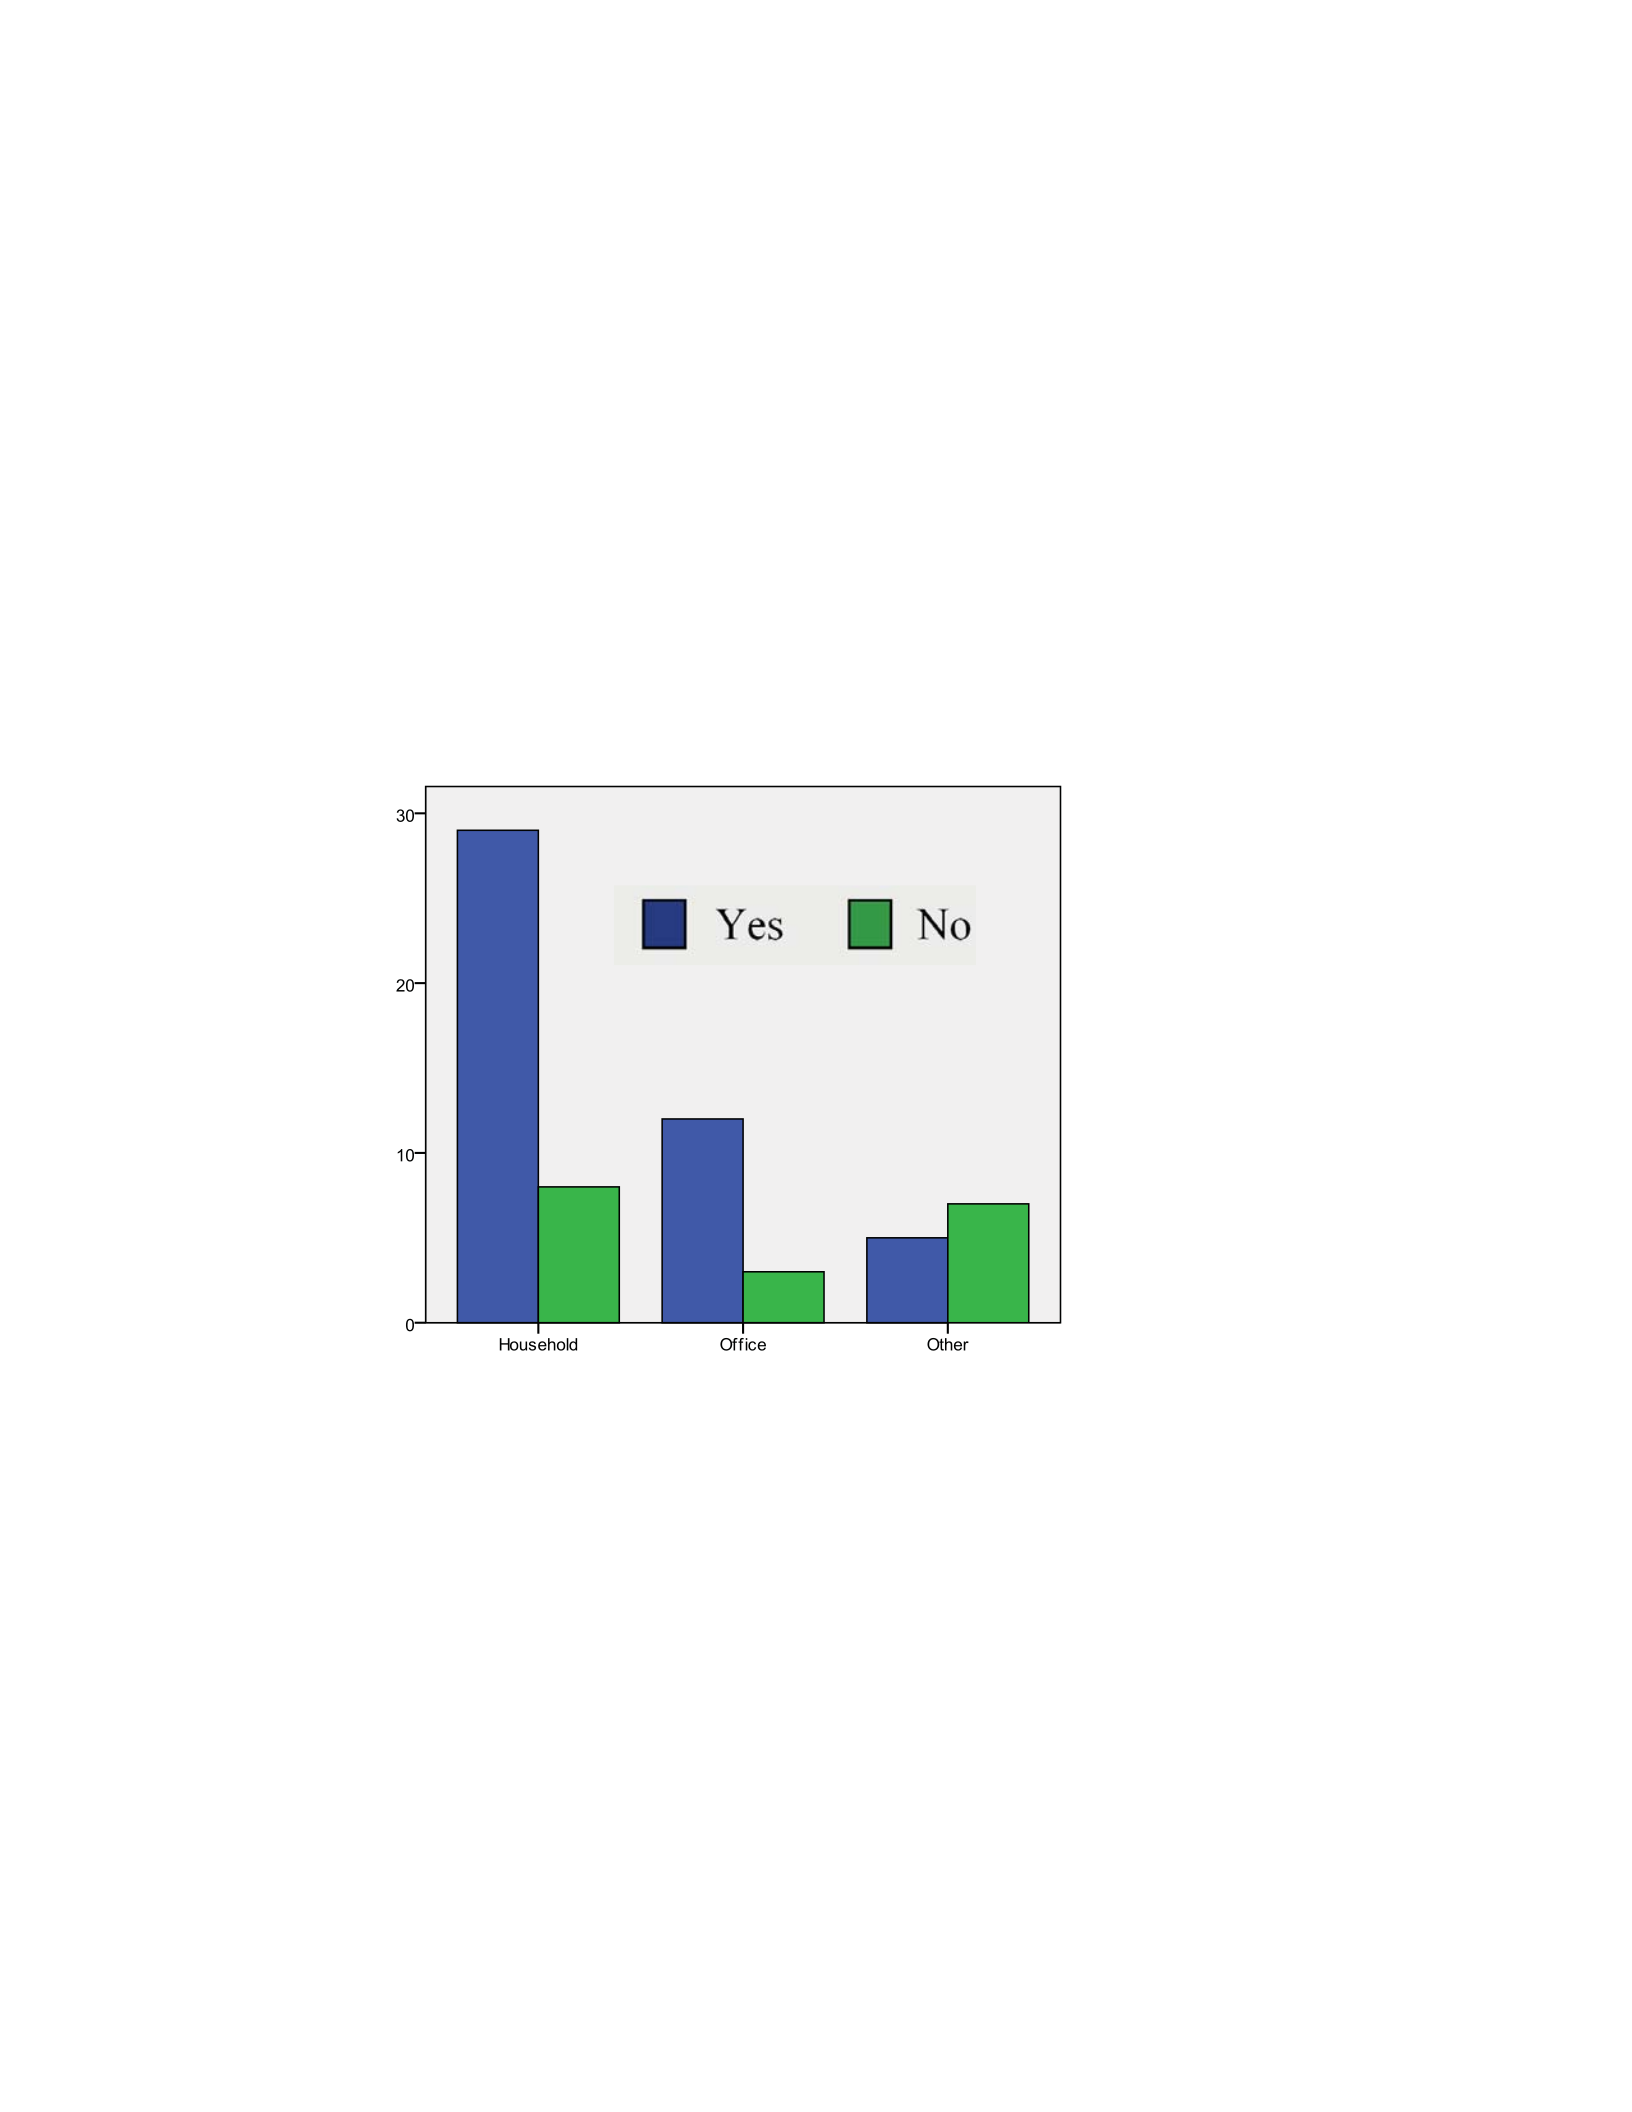
74
Because only one person mentioned that there is no advantage of HF/E, the
interpretation will not be meaningful even though the relationship was statistically
meaningful (p 0).
There was a significant relationship (p EHWZHHQWKHVHFWRUDQGWKH
opinion of increased worker safety. Managers from the Other Furniture Related Products
Manufacturing (NAICS Code 3379) subsector thought that HF/E does not have any
advantages on increased worker safety (Figure 21).
Figure 21 Sector and opinions on worker safety
Employee number or the size of company also has an impact on managers’
opinions relating to the advantages of HF/E. In comparison, managers working in small
companies believed much less that HF/E can reduce compensation costs (p
(Figure 22) and result in cost savings (e.g. lower insurance cost) (p )LJXUH
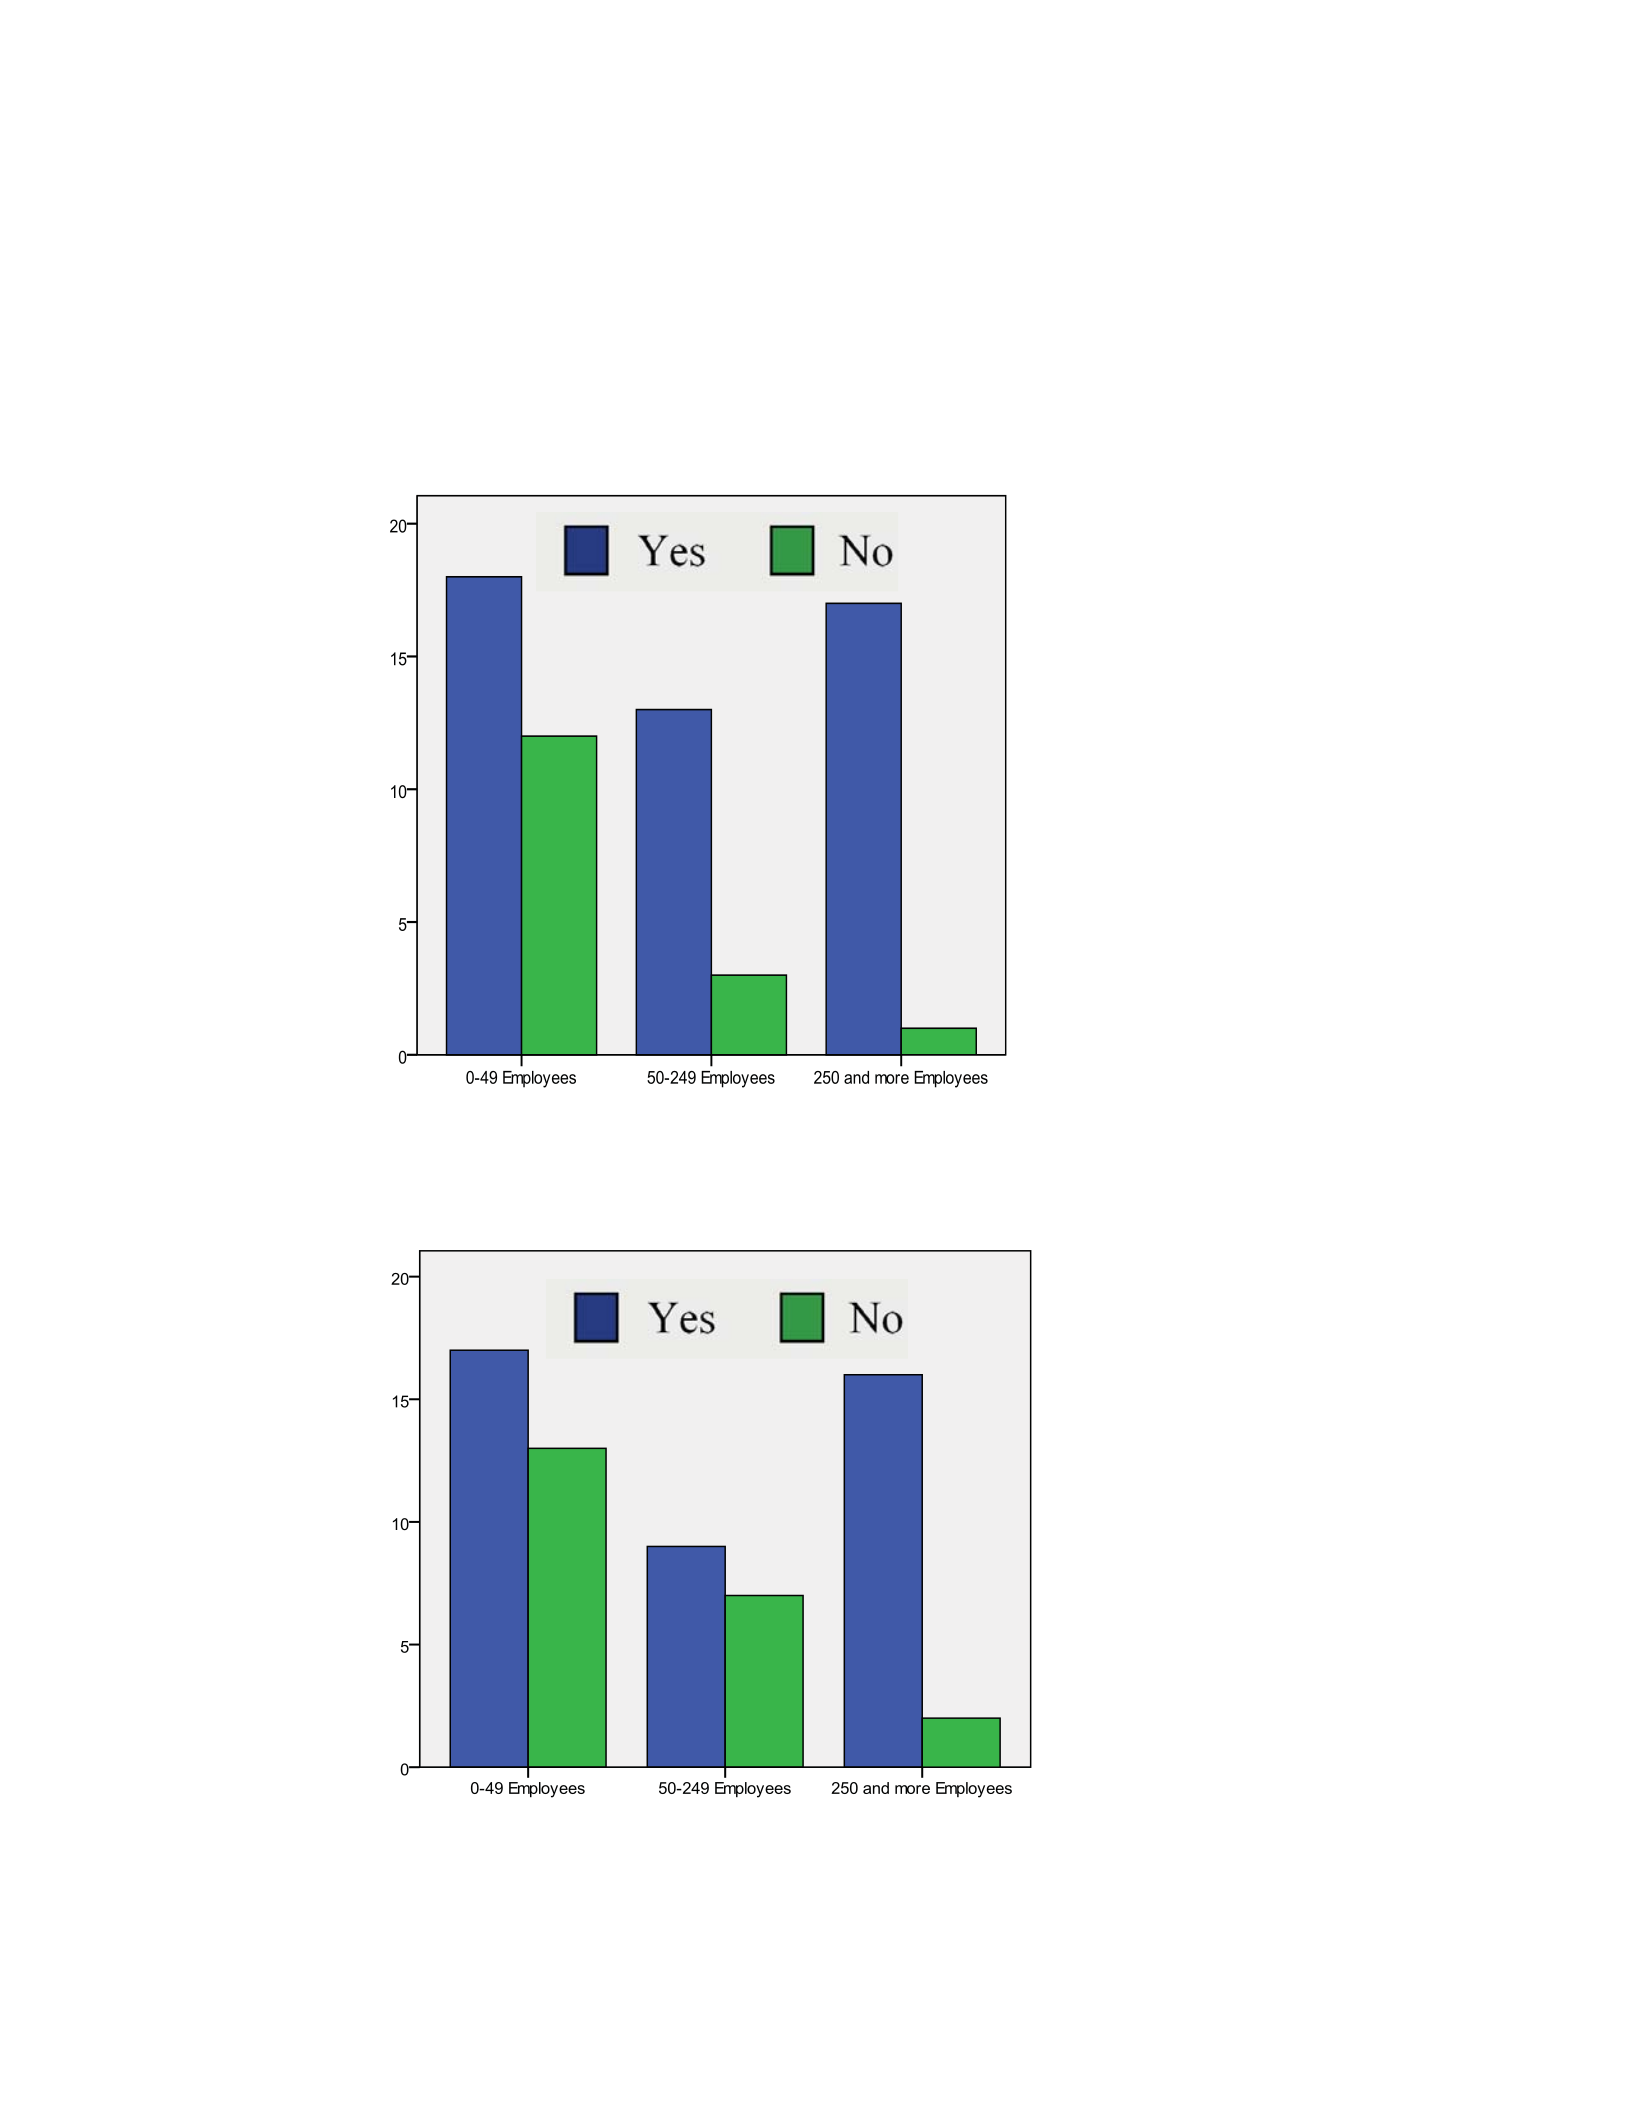
75
Likewise, owners and top-level managers believed less that HF/E can reduce
compensation costs (p )LJXUHDQGUHVXOWLQFRVWVDYLQJVHJORZHU
insurance cost) (p )LJXUHWKDQWKHLUORZHU-level counterparts.
Figure 22 Company size and managers’ opinions about worker’s compensation
Figure 23 Company size and managers’ opinions about cost savings
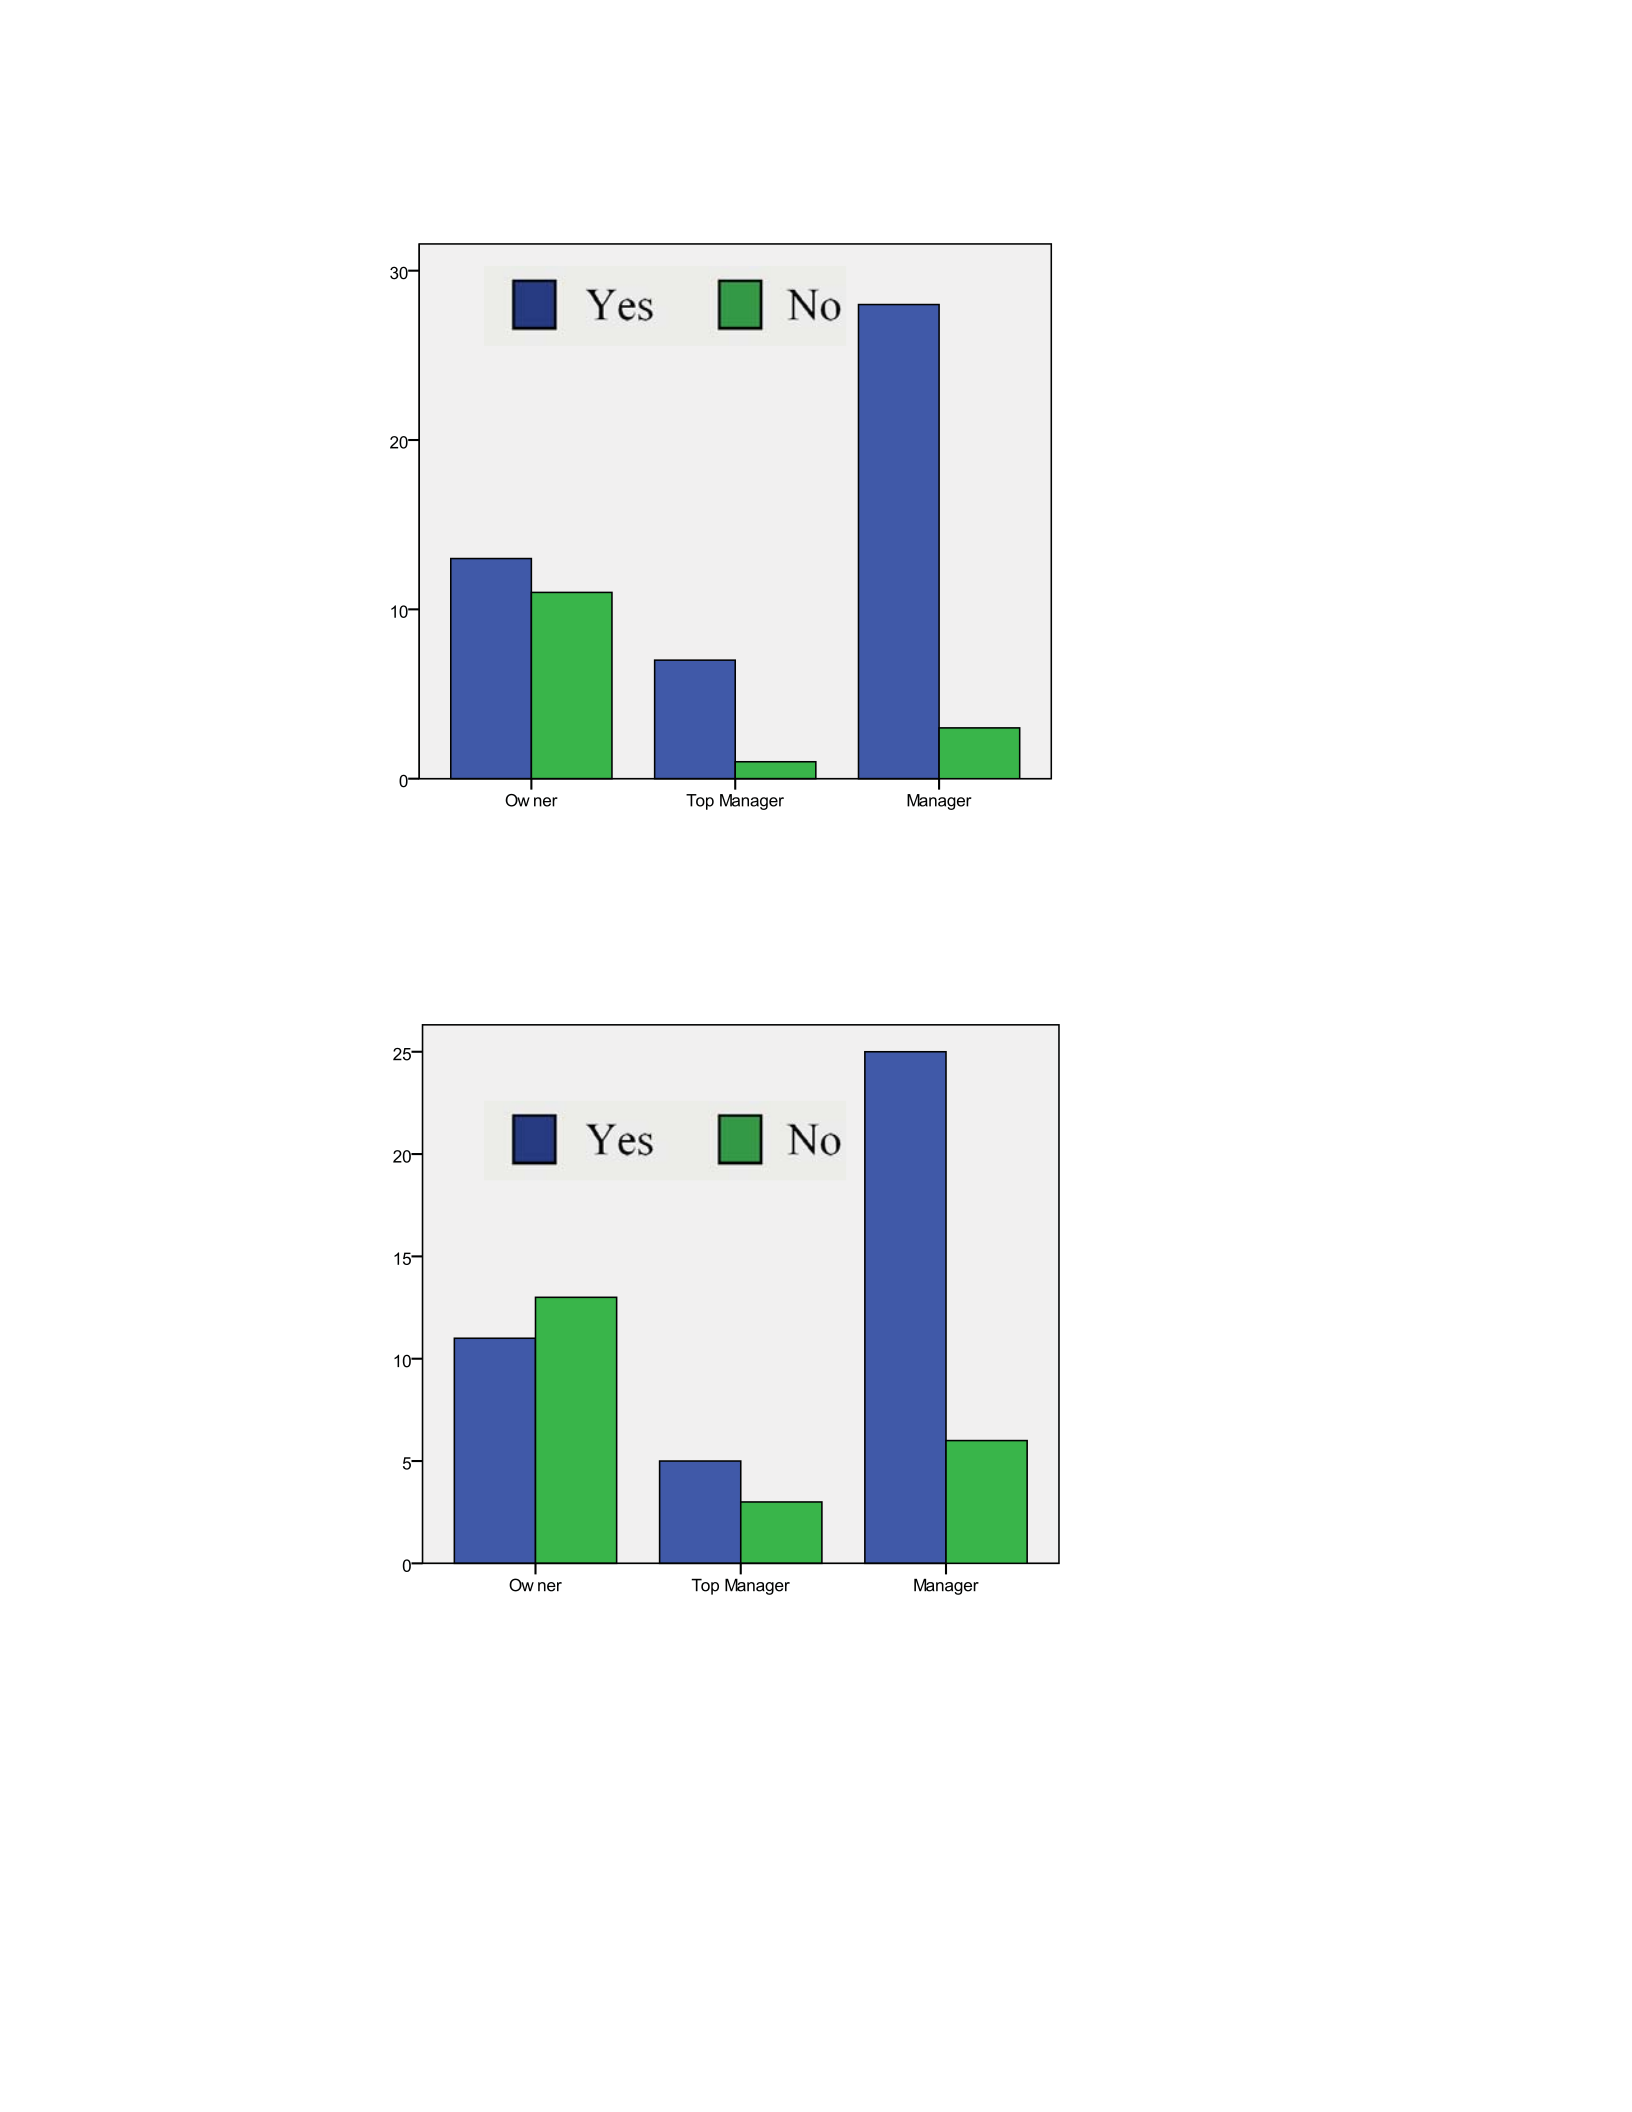
76
Figure 24 Managers’ positions and its affect on their opinion
about reduced compensation
Figure 25 Managers’ positions and its affect on their opinion about cost savings
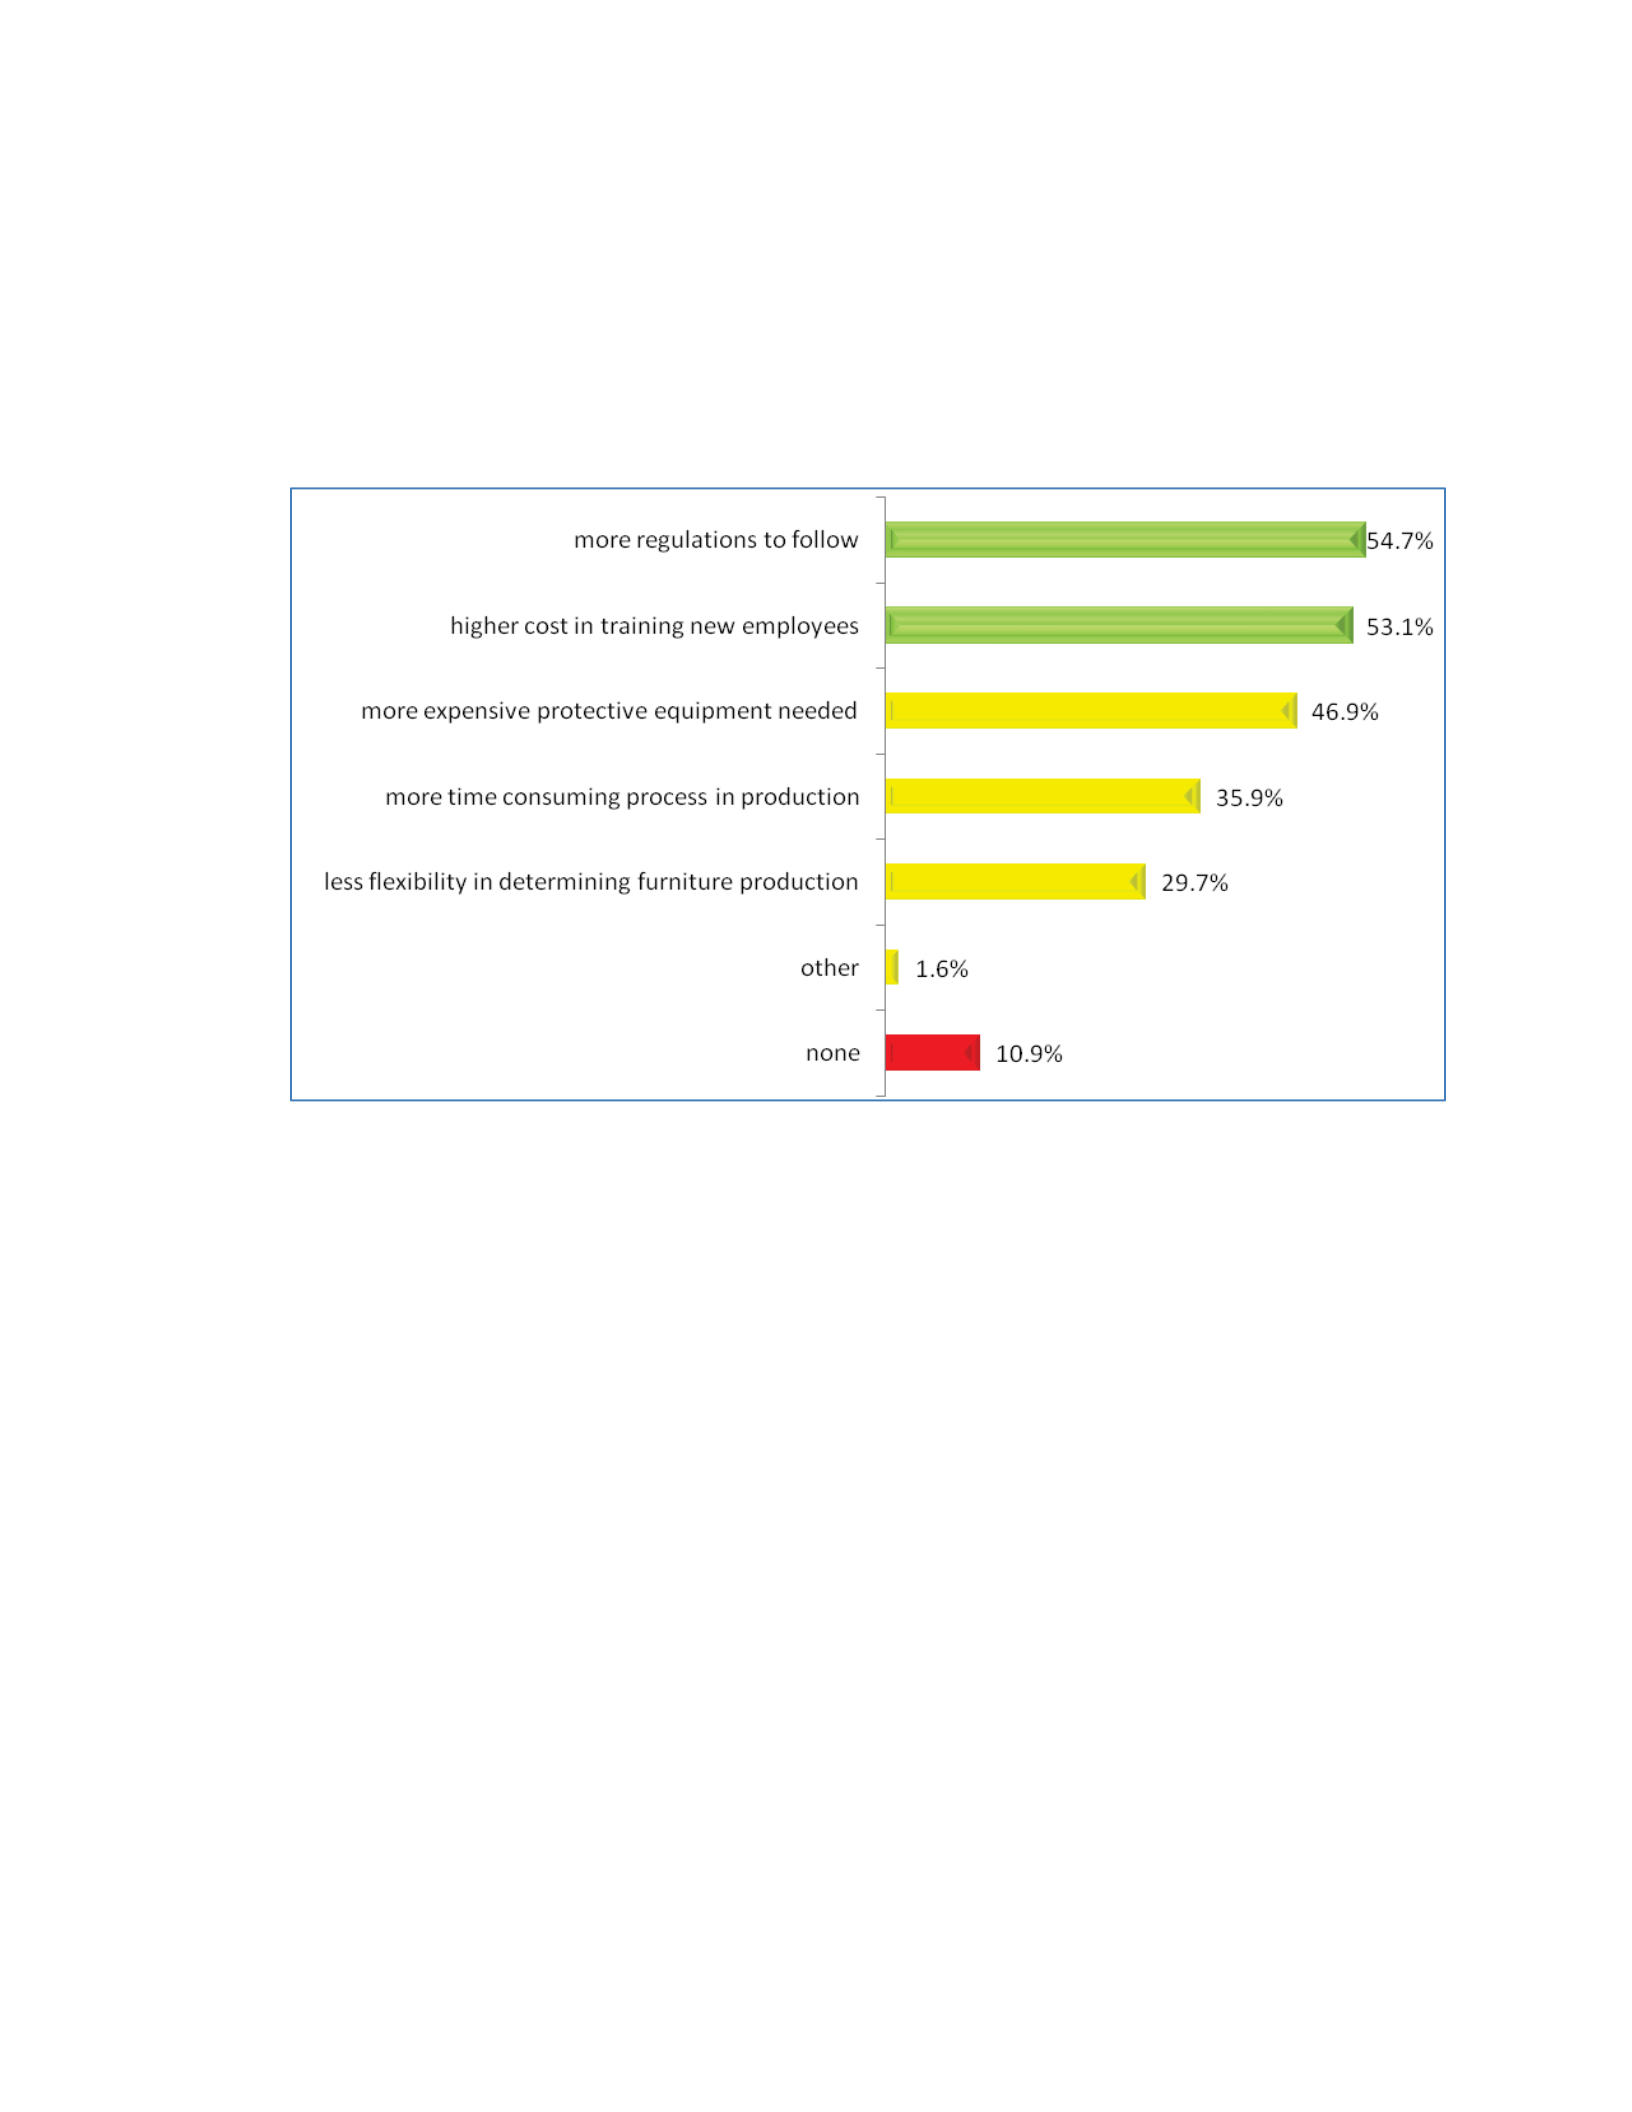
77
Likely Disadvantages of Human Factors and Ergonomics
Likewise, managers were asked whether there were any disadvantages of HF/E.
Managers’ responses are given in Figure 26 by the order of frequency.
Figure 26 Likely disadvantages of human factors and ergonomics
Over half of the managers believed that HF/E resulted in more regulations to
follow (54.7%) and higher cost in training new employees (53.1%). Less than half of the
managers believed that HF/E has some disadvantages such as more expensive protective
equipment needed (46.9%), more time-consuming process in production (35.9%), and
less flexibility in determining furniture production (29.7%). Seven managers (10.9%)
believed that there were no disadvantages of HF/E at all.
After performing statistical analysis to determine relationships between managers’
demographic profiles and managers’ opinions about the likely disadvantages of HF/E, the
results are given in Table 13.
78
Table 13 Statistical analysis of managers’ demographic properties and opinions
regarding the likely disadvantages of human factors and ergonomics
State Education NAICS Employees
Experience
in FI
Position
Experience
in P
More regulation to fallow Ȥ22.202 2.556 0.872 1.204 0.480 0.764 2.619
p0.138 0.279 0.647 0.548 0.787 0.683 0.270
Higher training costs Ȥ23.133 0.564 0.060 2.895 1.823 1.359 1.155
p0.077 0.754 0.970 0.235 0.402 0.507 0.561
Time consuming Ȥ20.939 1.749 2.041 2.158 10.510 3.550 11.115
p0.332 0.417 0.360 0.340 0.005* 0.170 0.004*
Expensive equipment Ȥ20.589 5.344 3.620 0.106 1.117 4.589 3.410
p0.443 0.069 0.164 0.948 0.572 0.101 0.182
Less flexibility Ȥ23.075 0.946 0.222 0.052 1.275 1.124 3.150
p0.080 0.623 0.895 0.975 0.529 0.570 0.207
No disadvantages Ȥ20.098 1.362 0.797 0.752 2.006 2.291 4.722
p0.754 0.506 0.671 0.687 0.367 0.318 0.094
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p
: p-value (The level of statistical significance).
The results of the statistical test showed that HF/E was considered as a more-time
consuming process in production by managers experienced in the furniture industry (p
0.005) (Figure 27) and experienced in the position (p )LJXUH7KHUHIRUHLW
can be said that younger managers or less-experienced managers in either industry or in
their position believed that HF/E was beneficial and did not cause time consuming
processes in production.
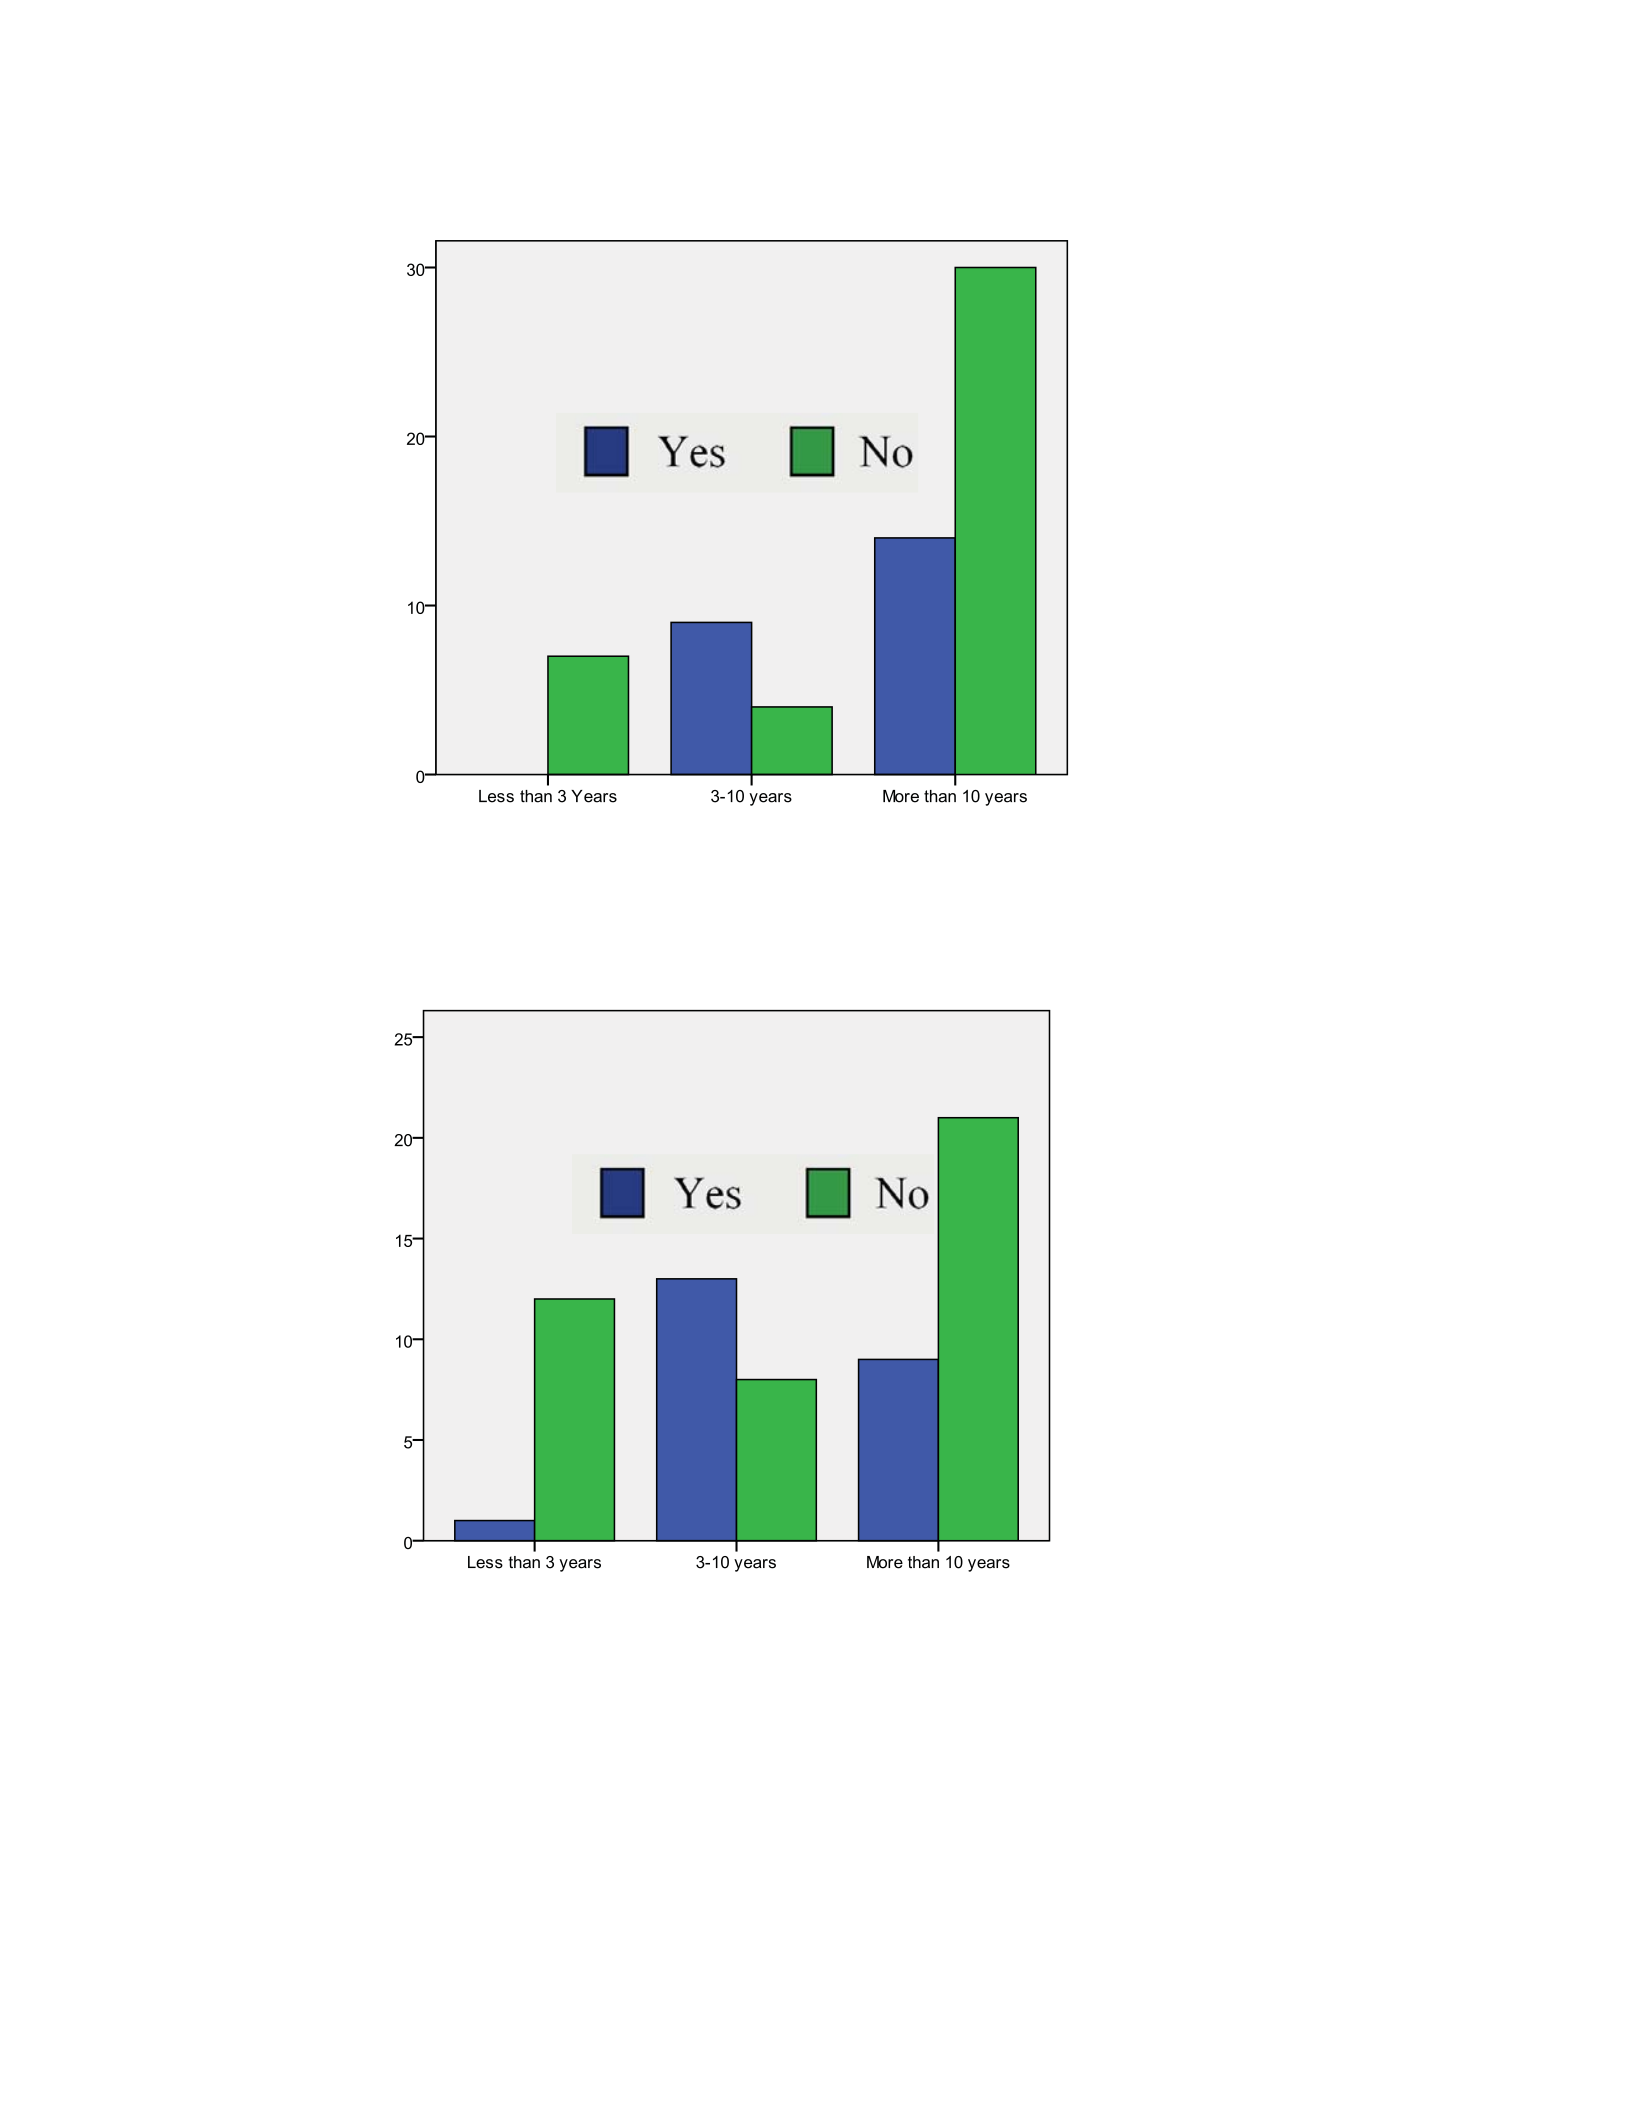
79
Figure 27 Managers’ experience in furniture industry and
its affect on their opinion about time consumption
Figure 28 Managers’ experience in their current position and
its affect on their opinion about time consumption
A similar question was asked by Kim and his colleagues (Kim et al. 2008). Their
aim was to determine current knowledge and opinions of twelve panel designers on the
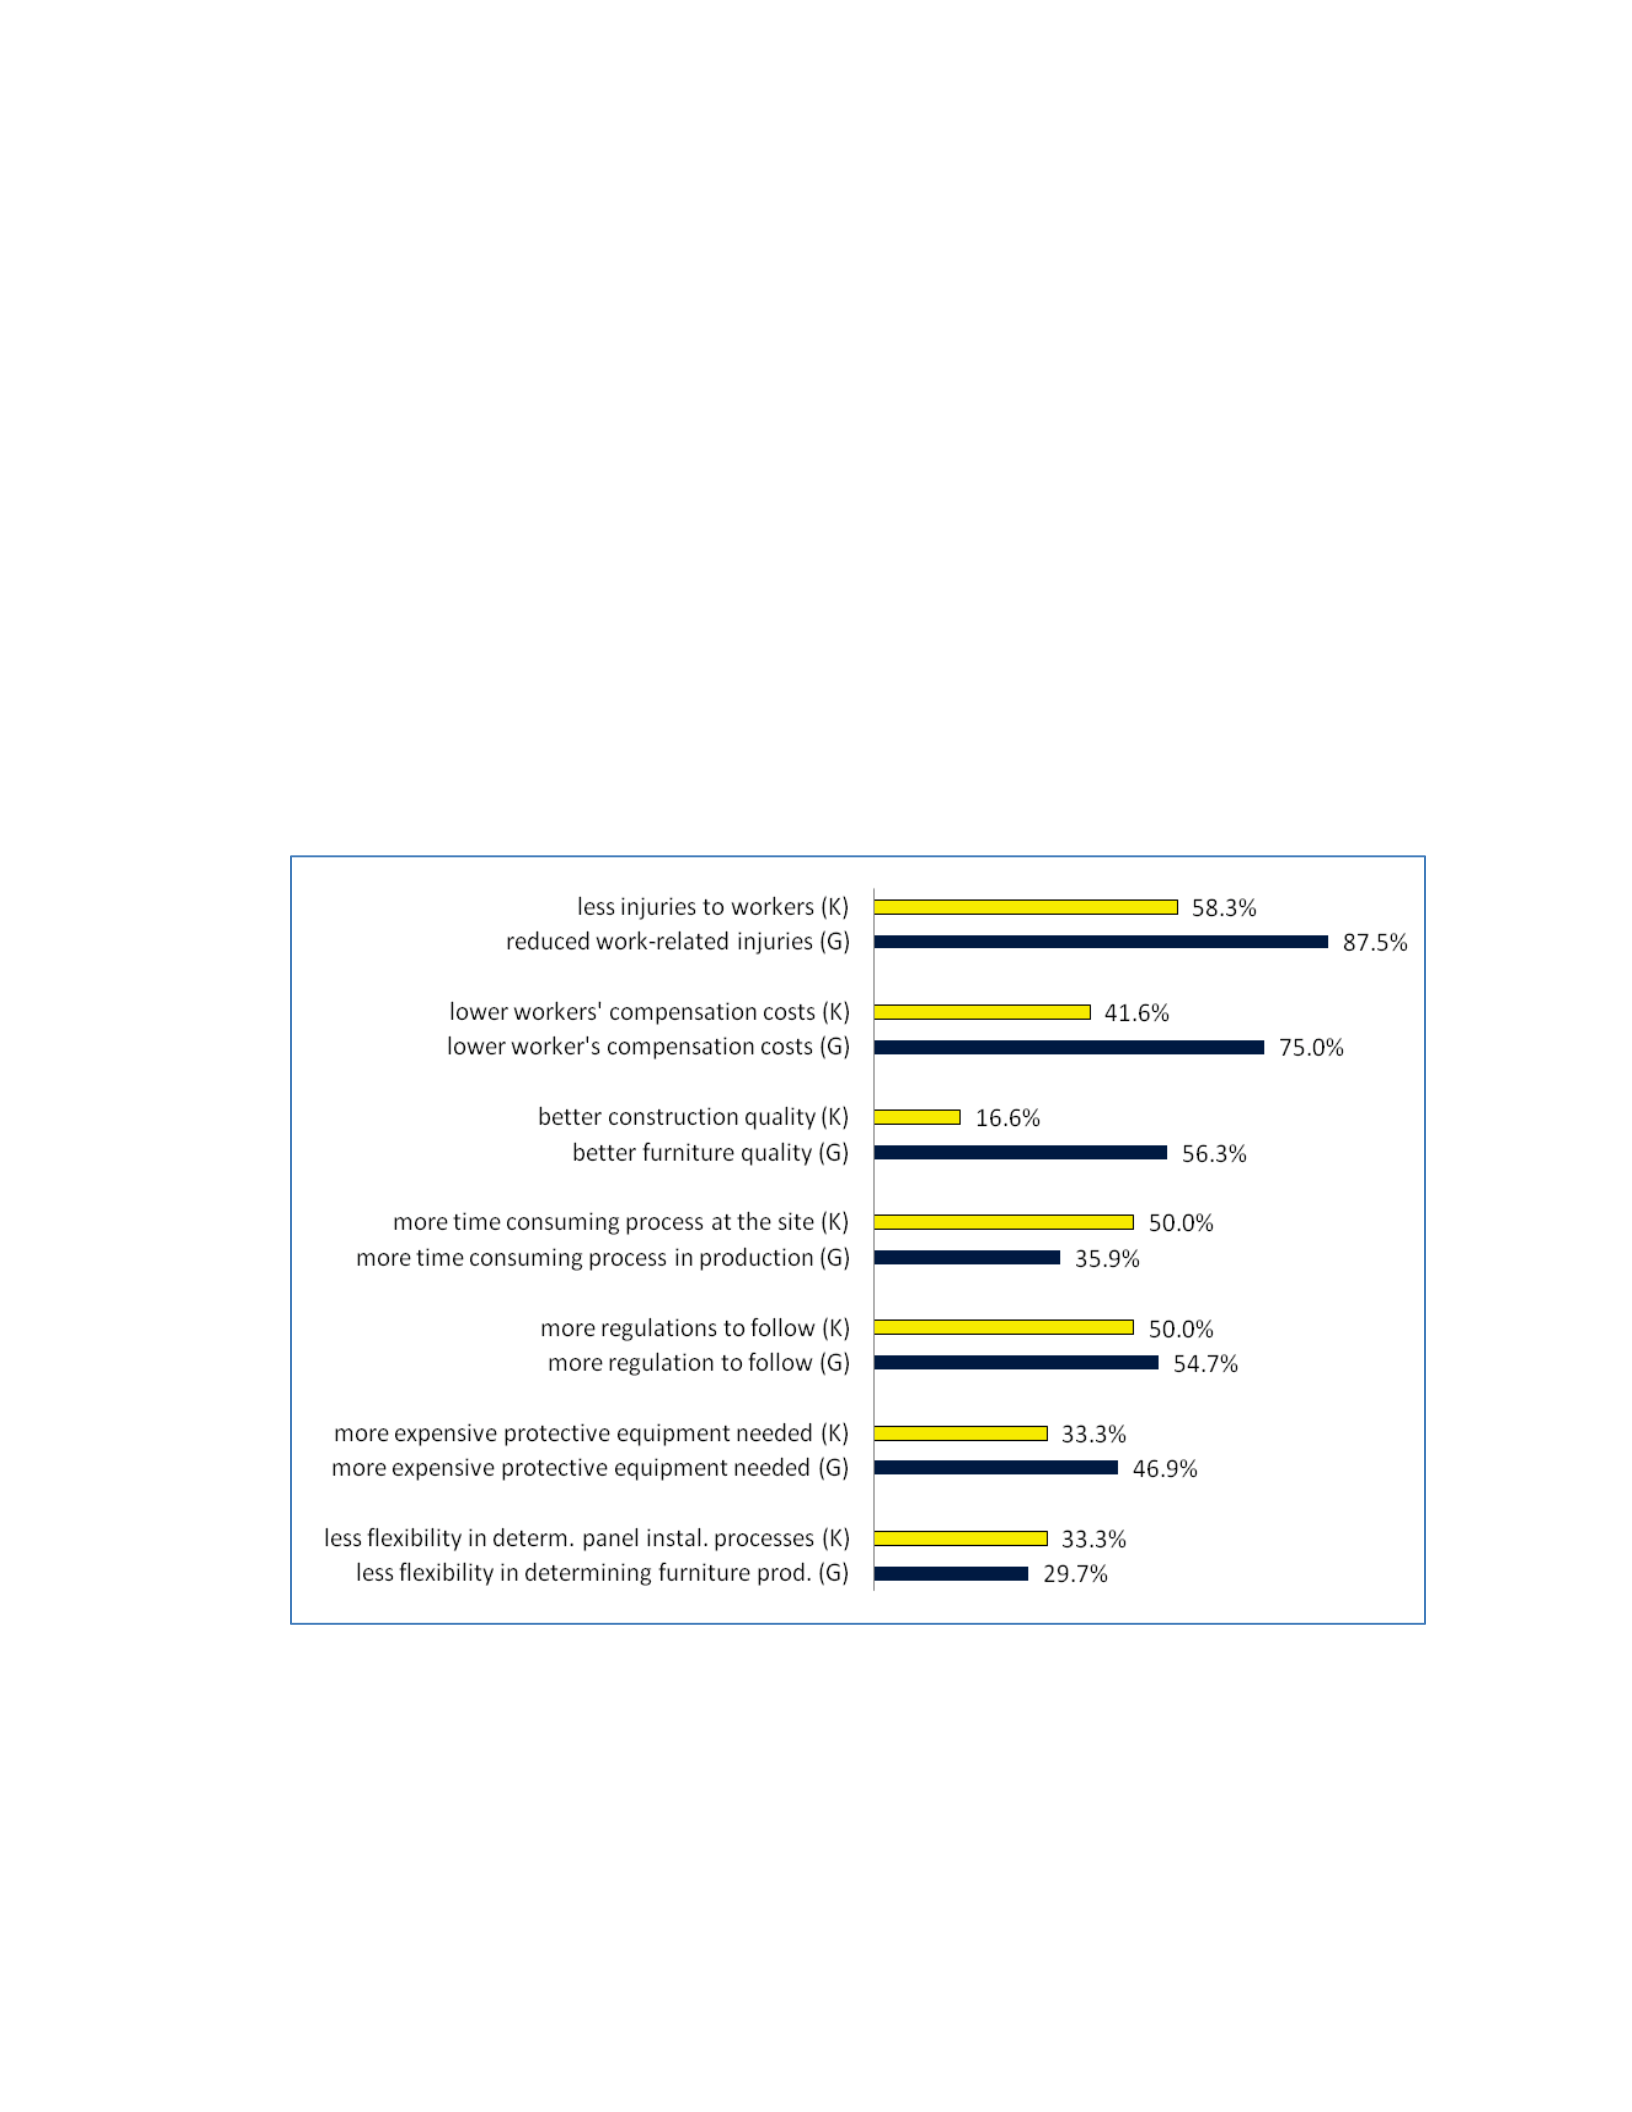
80
subject of workers' ergonomic risks. This aim was shared in this thesis as well. Both
researches were conducted to better understand the knowledge and opinions of decision
makers regarding HF/E. The results of both researched are shown in Figure 29. In the
figure, bars with light color are results of the study conducted by Kim et al. (2008), and
bars with dark color are results obtained in this research. Initials after the answers can
help to understand the figure. The initial of (K) was used to address the questions asked
by Kim and his colleagues, and (G) was used to address the questions asked by the author
of this thesis, Gungor.
Figure 29 Comparison of the result of this thesis with the results of Kim et al. (2008)
In comparison, managers in the furniture industry believed more than panel
designers that HF/E has some advantages such as: less occupational injuries, lower

81
worker’s compensation costs, and better product quality. Likewise, panel designers
believed more than furniture manufacturer managers that HF/E caused some problems
such as: more time-consuming processes in production, more regulations to follow, more
expensive protection equipment, and less flexibility in determining the production
process. As a whole, furniture manufacturer managers were more aware of the
advantages HF/E rather than panel designers. They were also less concerned with the
possibilities of increased production time, cost, and decreased flexibility in production
when they were compared to panel designers.
Managers’ Agreement with Some Statements Concerning
Human Factors and Ergonomics
To better understand the knowledge and opinions of managers, they were asked to
rate their attitudes toward some statements. They rated the questions with a five-point
scale ranging from strong disagreement to strong agreement. The distribution of the
responses is given in Table 14.
Scientific data about a discipline may be considered too complex or hard to
understand and apply in an industry if a person is not familiar with the scientific aspects,
but the discipline of HF/E is not one of these types of disciplines. Participants in the
survey believed so as well. Only 12.5 percent of managers agreed with the statement that
scientific data about HF/E was too complex to understand and apply. The average of
rating was 2.45. Namely, managers, in general, did not agree with the statement.
82
Table 14 Managers’ agreement with some statements concerning human factors and ergonomics
Questions
Strongly
Disagree Disagree Neutral Agree Strongly
Agree
Rating
Average
Total
Respond
(N) (%) (N) (%) (N) (%) (N) (%) (N) (%)
Scientific data about HF/E is too complex to understand
and apply. 10 15.6 25 39.1 21 32.8 6 9.4 2 3.1 2.45 64
HF/E causes more expenses than the benefits returned. 14 21.9 24 37.5 16 25 8 12.5 2 3.1 2.38 64
Small changes in environmental factors in workplaces
can have a considerable impact on worker's productivity,
comfort, health, and safety.
4 6.3 6 9.4 10 15.6 23 35.9 21 32.8 3.80 64
Workers in your factory can understand what HF/E deal
with. 15 23.4 23 35.9 15 23.4 9 14.1 2 3.1 2.38 64
Using personal protective equipment can prevent
occupational injuries and illnesses. 2 3.1 4 6.3 3 4.7 21 32.8 34 53.1 4.27 64
Working posture can cause or prevent musculoskeletal
injuries.
1 1.6 5 7.8 5 7.8 18 28.1 35 54.7 4.27 64

83
In the same way, furniture manufacturing managers replied that HF/E did not
cause more expenses than the benefits returned. The rating average was 2.38 for the
question. The percentage of managers who had the opinion that HF/E causes more
expenses than benefits was 15.6 in total.
Another question was asked whether small changes in environmental factors in
the workplace could have a considerable impact on worker productivity, comfort, health,
and safety. Managers took a neutral stance (15.6%) or a positive stance (68.7%) towards
this statement. Managers’ opinion showed that they were aware of the advantages of
making changes in environmental factors in workplaces.
However, managers believed that workers in their factory could not understand
what HF/E dealt with. The percentage of managers who thought so was 59.3 in total,
while 23.4 percent of managers took a neutral stance. The rest, 17.2 percent of managers,
mentioned that their workers were able to understand what HF/E dealt with.
Most of the managers fortunately showed that they were aware of the advantages
of using personal protective equipment in workplaces to prevent occupational injuries
and illnesses. The ratio of these managers was 85.9 percent. This is a very high ratio, and
it shows that managers actually were aware of the importance of using personal
protective equipment in workplaces.
Another high ratio was obtained from the question related to the importance of
working posture; 82.8 percent of managers believed that good working posture could
prevent musculoskeletal injuries or bad working posture could cause musculoskeletal
injuries.
84
The statistical analysis of managers’ opinions on these questions was performed,
and the results of the analysis are given in Table 15.
Table 15 Statistical analysis of managers’ demographic properties and managers’
agreement with some statements concerning human factors and ergonomics
State Education NAICS Employees
Experience
in FI
Position
Experience
in P
Scientific data Ȥ25.657 4.238 9.136 4.776 3.411 6.841 4.356
p0.226 0.835 0.331 0.781 0.906 0.554 0.824
More expense Ȥ22.893 5.930 10.295 4.707 5.663 2.390 9.903
p0.576 0.655 0.245 0.788 0.685 0.967 0.272
Environmental changes Ȥ23.980 9.374 6.330 6.562 5.884 6.673 7.115
p0.409 0.312 0.610 0.585 0.660 0.572 0.524
Worker understand Ȥ23.429 8.442 19.751 3.707 7.443 6.941 14.277
p0.489 0.392 0.011* 0.883 0.490 0.543 0.075
Using PPE Ȥ21.934 15.816 8.781 4.208 3.606 3.725 8.811
p0.748 0.045* 0.361 0.838 0.891 0.881 0.358
Posture Ȥ26.401 8.134 18.598 6.739 4.557 8.167 3.958
p0.171 0.421 0.017* 0.565 0.804 0.417 0.861
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value, p: p-value (The level of statistical significance).
The relationship between education and the opinion that using personal protective
equipment can prevent occupational injuries and illnesses was significant (p 7KHUHZHUH
also significant relationships between the sector and worker understanding HF/E (p DQG
the opinion that working posture could cause or prevent musculoskeletal injuries in work places
(p 0DQDJHUVLQWKH2IILFH)XUQLWXUH,QFOXGLQJ)L[WXUHV0DQXIDFWXULQJ1$,&6&RGH
3372) subsector agreed more than other subsectors with the statement that workers could
understand what HF/E dealt with.
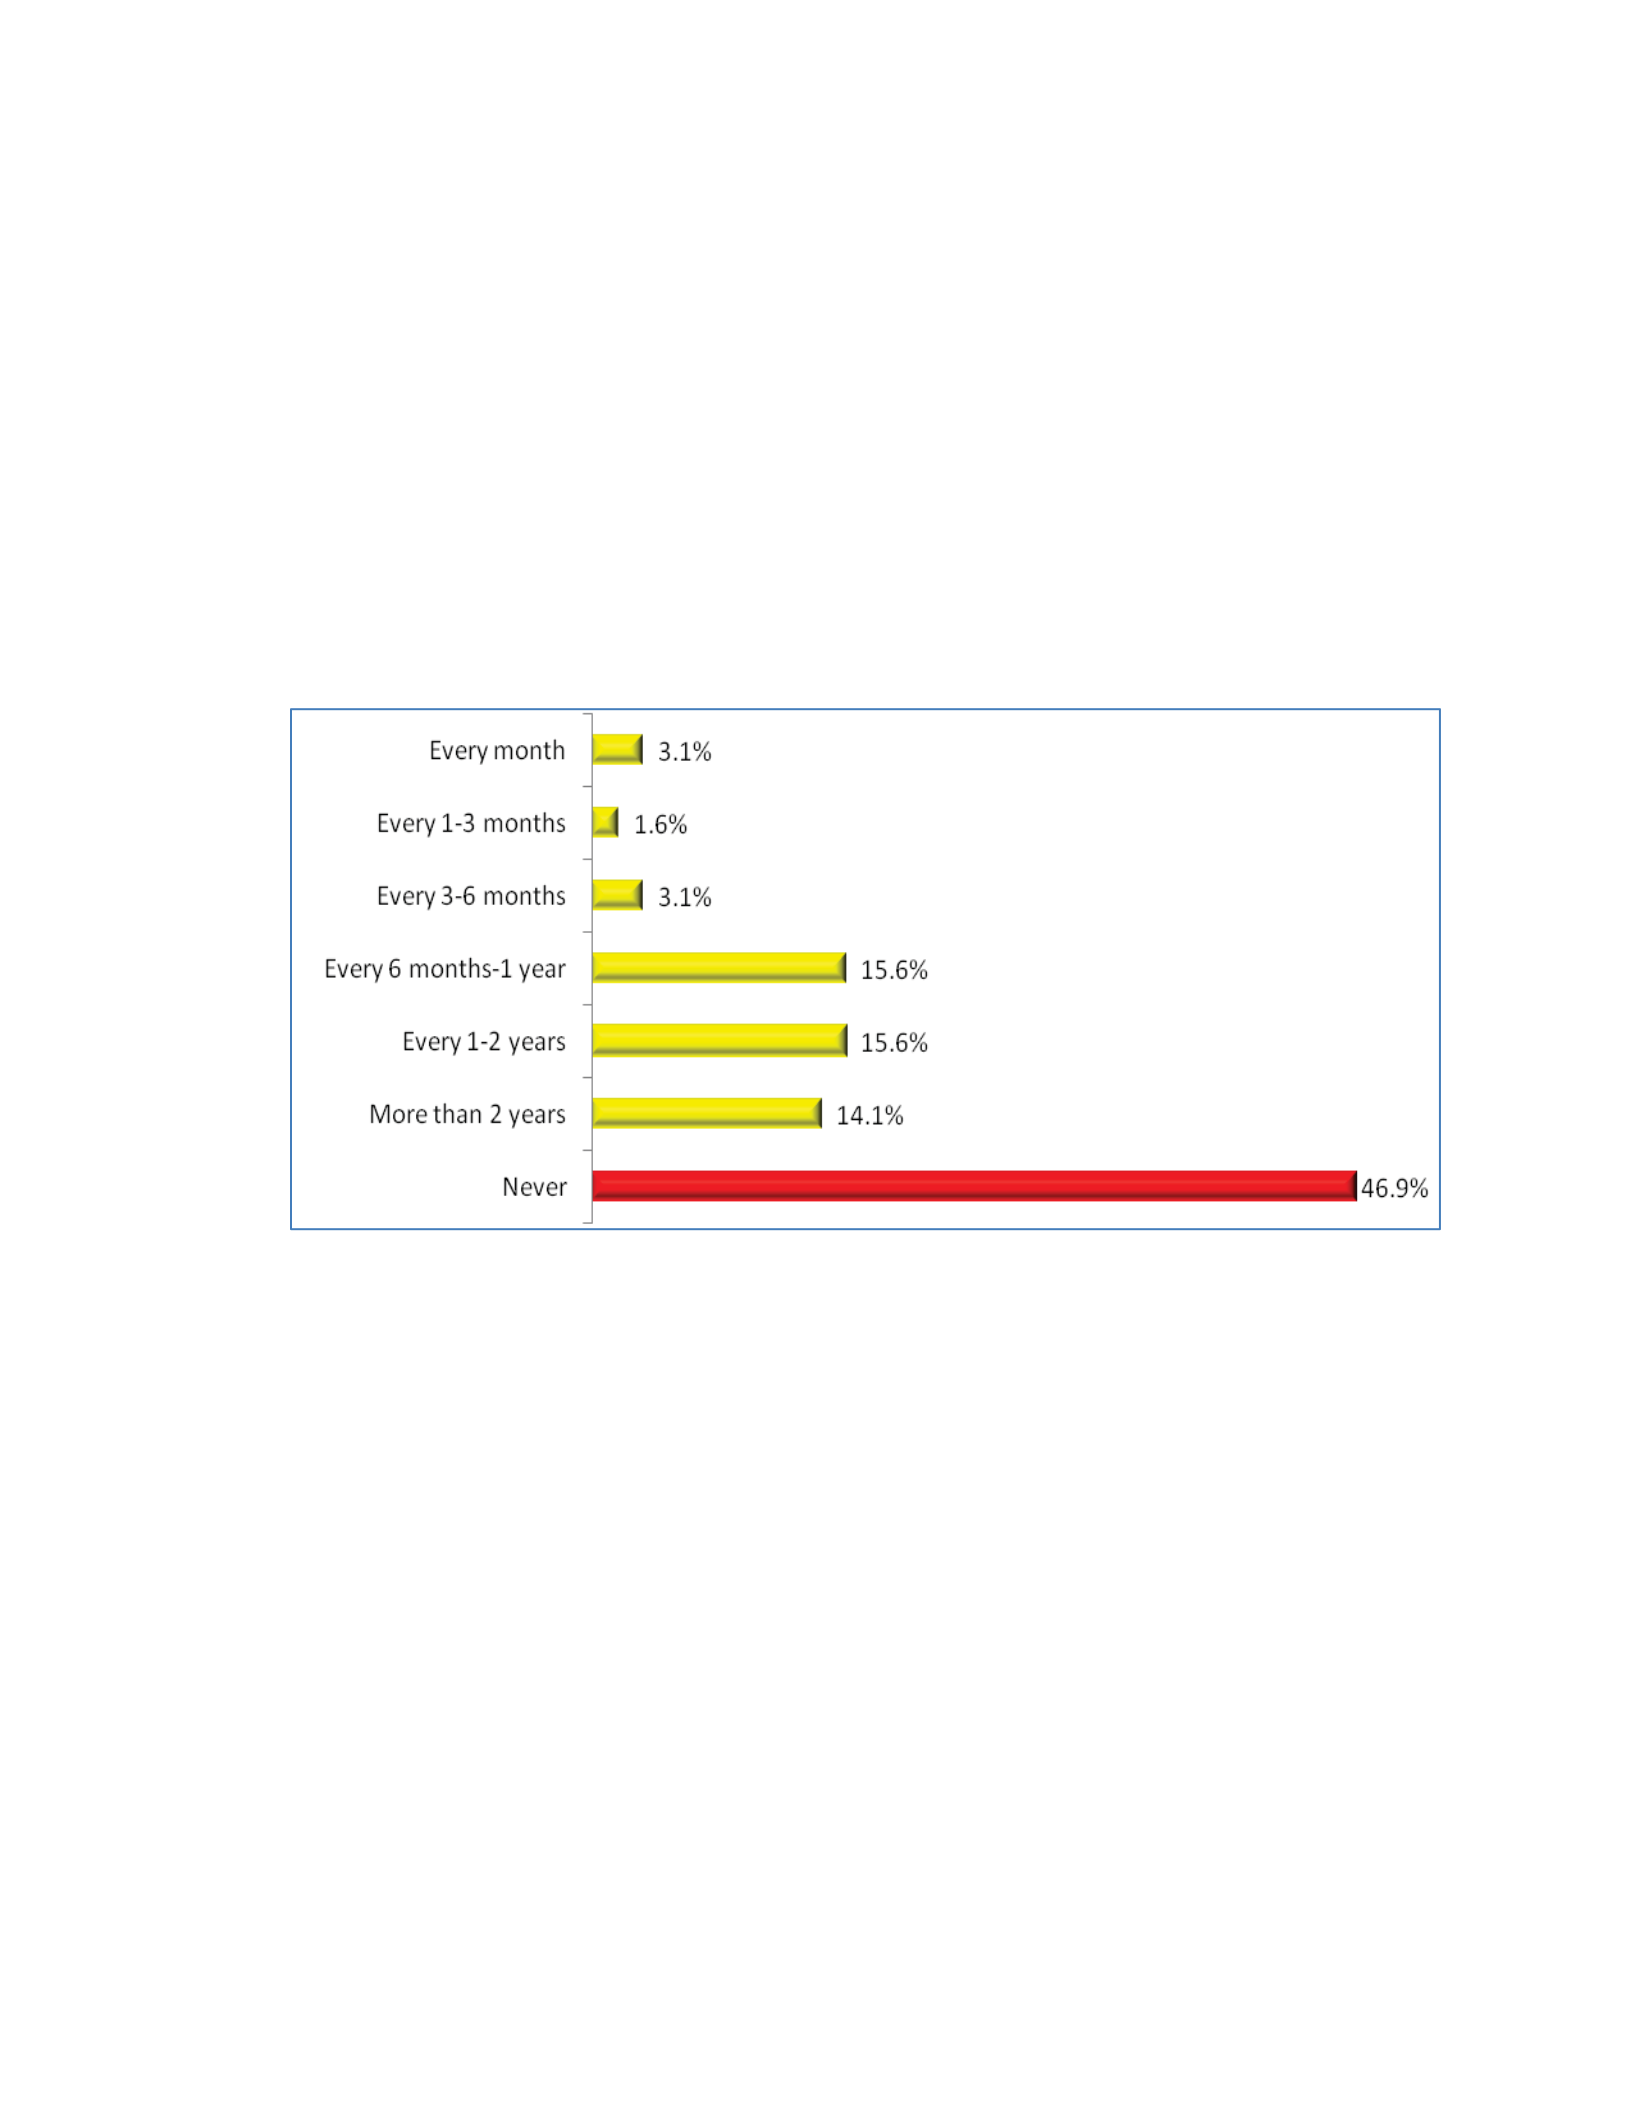
85
The Frequency of Inspections of Companies for
Human Factors and Ergonomic Problems
Inspection for HF/E is an important management control method to prevent
occupational injuries and illnesses in work places. In the questionnaire survey, managers
were asked the frequency of inspection done in workplaces. The distribution of responses
is given in Figure 30.
Figure 30 The frequency of inspections for human factors and ergonomics problems
In order to perform statistical analysis, the answers were combined in three
categories because the observed values of cells were too small for good analysis. The
new distribution is given in Table 16. After the categorization, statistical analysis was
performed (Table 17).
86
Table 16 The frequency of inspections for human factors and ergonomics problems
Inspection
Frequency Number Percentage
Cumulative
Percentage
Every mounth-1 year 14 21.9 21.9
More than 1 year 20 31.3 53.1
Never 30 46.9 100
Total 64 100
Table 17 Statistical analysis of the frequency of inspections for human factors and
ergonomics problems
State Education NAICS Employees
Experience
in FI
Position
Experience
in P
Inspection Ȥ22.016 4.551 1.029 20.761 5.481 5.891 3.061
p0.365 0.337 0.905 0.000* 0.241 0.207 0.548
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p
: p-value (The level of statistical significance).
The size of company and the frequency of inspection for HF/E were significantly
(p related to each other. Some of small companies (66.7%) had never been
inspected (Figure 31). On the other hand, 55.6 percent of large size companies had been
inspected on an annual basis.
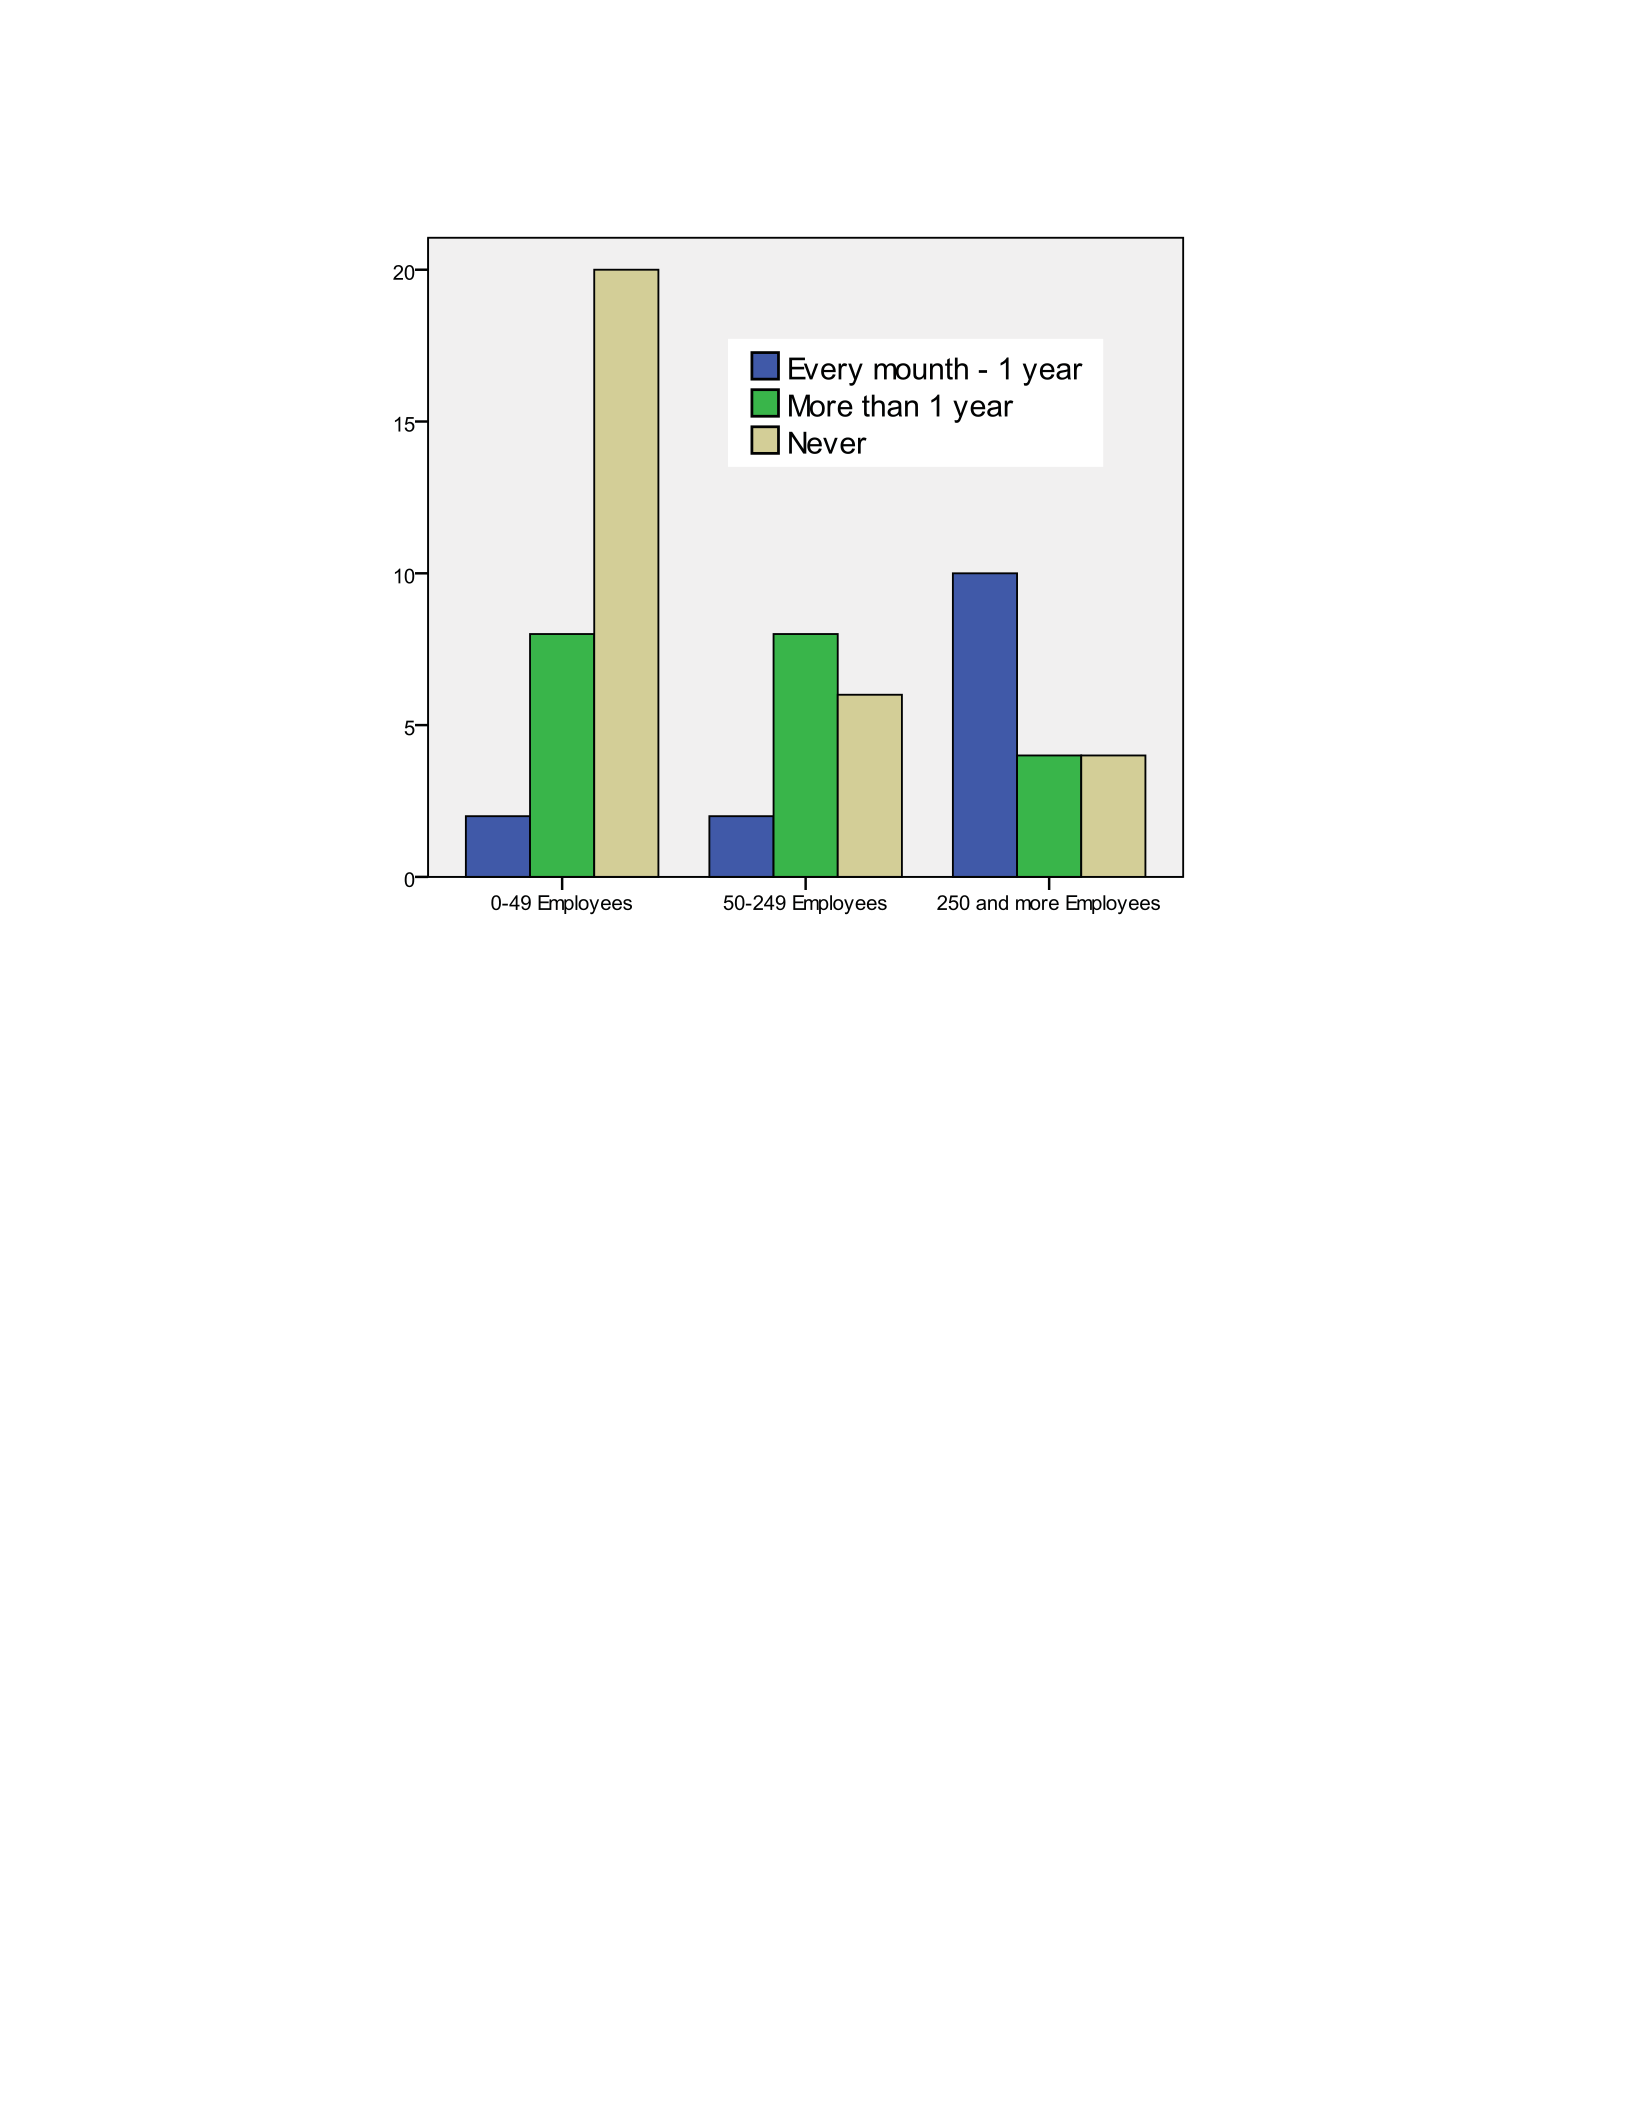
87
Figure 31 Company size and inspection frequency
Employees’ Familiarity with Human Factors and Ergonomics
In addition to managers’ familiarity, it is vital that employees be familiar with
HF/E for the success in prevention of occupational injuries and illnesses. These programs
improve employees’ understanding and identification of occupational injury and illness
risk factors. Educational programs should focus on increasing employee knowledge and
awareness regarding HF/E in their work. These programs also encourage workers to
actively participate in HF/E interventions (Pehkonen et al. 2009).
A study for evaluating a proactive ergonomic control program in three secondary
wood processing companies was conducted by Gazo et al. in 2000 and 2001. The aim
was to help employees to understand the causes, symptoms, treatment, and prevention of
musculoskeletal disorders. The results of the study showed some improvements such as
88
reduced occupational injuries and illnesses, reduced absenteeism, improved employee
health, improved manufacturing productivity, and higher product quality (Gazo et al.
2002).
Another example for the success of an HF/E program in the furniture industry was
revealed by OSHA in 2002. An office furniture manufacturing company with 9,000
employees started an employee-focused workplace ergonomics program aiming to reduce
the unacceptable back injury rate. After a few years, the back injury incidence rate
lowered by 50 percent (OSHA 2002).
In this survey, managers were asked two questions to learn more about their
workers and about general knowledge of their companies. The first question was whether
there was a team or department in their factories to find and correct ergonomics problems
(Table 18). Unfortunately, 56.3 percent of managers expressed that there was no team or
department for HF/E interventions. In 9.4 percent of the companies, managers were not
sure if there were any. For the second question, 40.6 percent of managers noted that
their workers received training programs for HF/E.
Table 18 Employees’ familiarity with human factors and ergonomics
Questions
Yes No Not sure Total
(N) (%) (N) (%) (N) (%) (N)
Is there a team or department in your factory that
finds and corrects ergonomics problems? 22 34.4 36 56.3 6 9.4 64
Do your workers receive training for human
factors and ergonomics?
26 40.6 29 45.3 9 14.1 64
89
Statistical analysis was performed to understand relationships between managers’
demographic features and the existence of a team/department or the providing of a
training program related to HF/E. Chi-square results of this analysis are given in Table
19.
Table 19 Statistical analysis of managers’ demographic properties and the existence of a
team/department and/or a training program
State Education NAICS Employees
Experience
in FI
Position
Experience
in P
Having a team Ȥ23.355 5.234 1.651 13.601 1.337 6.748 1.425
P0.187 0.264 0.800 0.009* 0.855 0.150 0.840
Workers receive training Ȥ24.350 2.297 1.296 14.856 3.055 7.068 1.762
P0.114 0.681 0.862 0.005* 0.549 0.132 0.779
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p: p-value (The level of statistical significance).
The analysis showed that there was a significant relationship (p EHWZHHQ
company size and the existence of a team or department in factories to find and correct
ergonomics problems. The relationship can be seen in Figure 32 that only 16.7 percent of
small companies, unfortunately, had a team or department for ergonomics problems. On
the other hand, 56.3 percent of middle size companies and 44.4 percent of large size
companies had teams or departments for handling HF/E related problems. Of all the
managers, 9.4 percent were not sure whether a team or department existed.
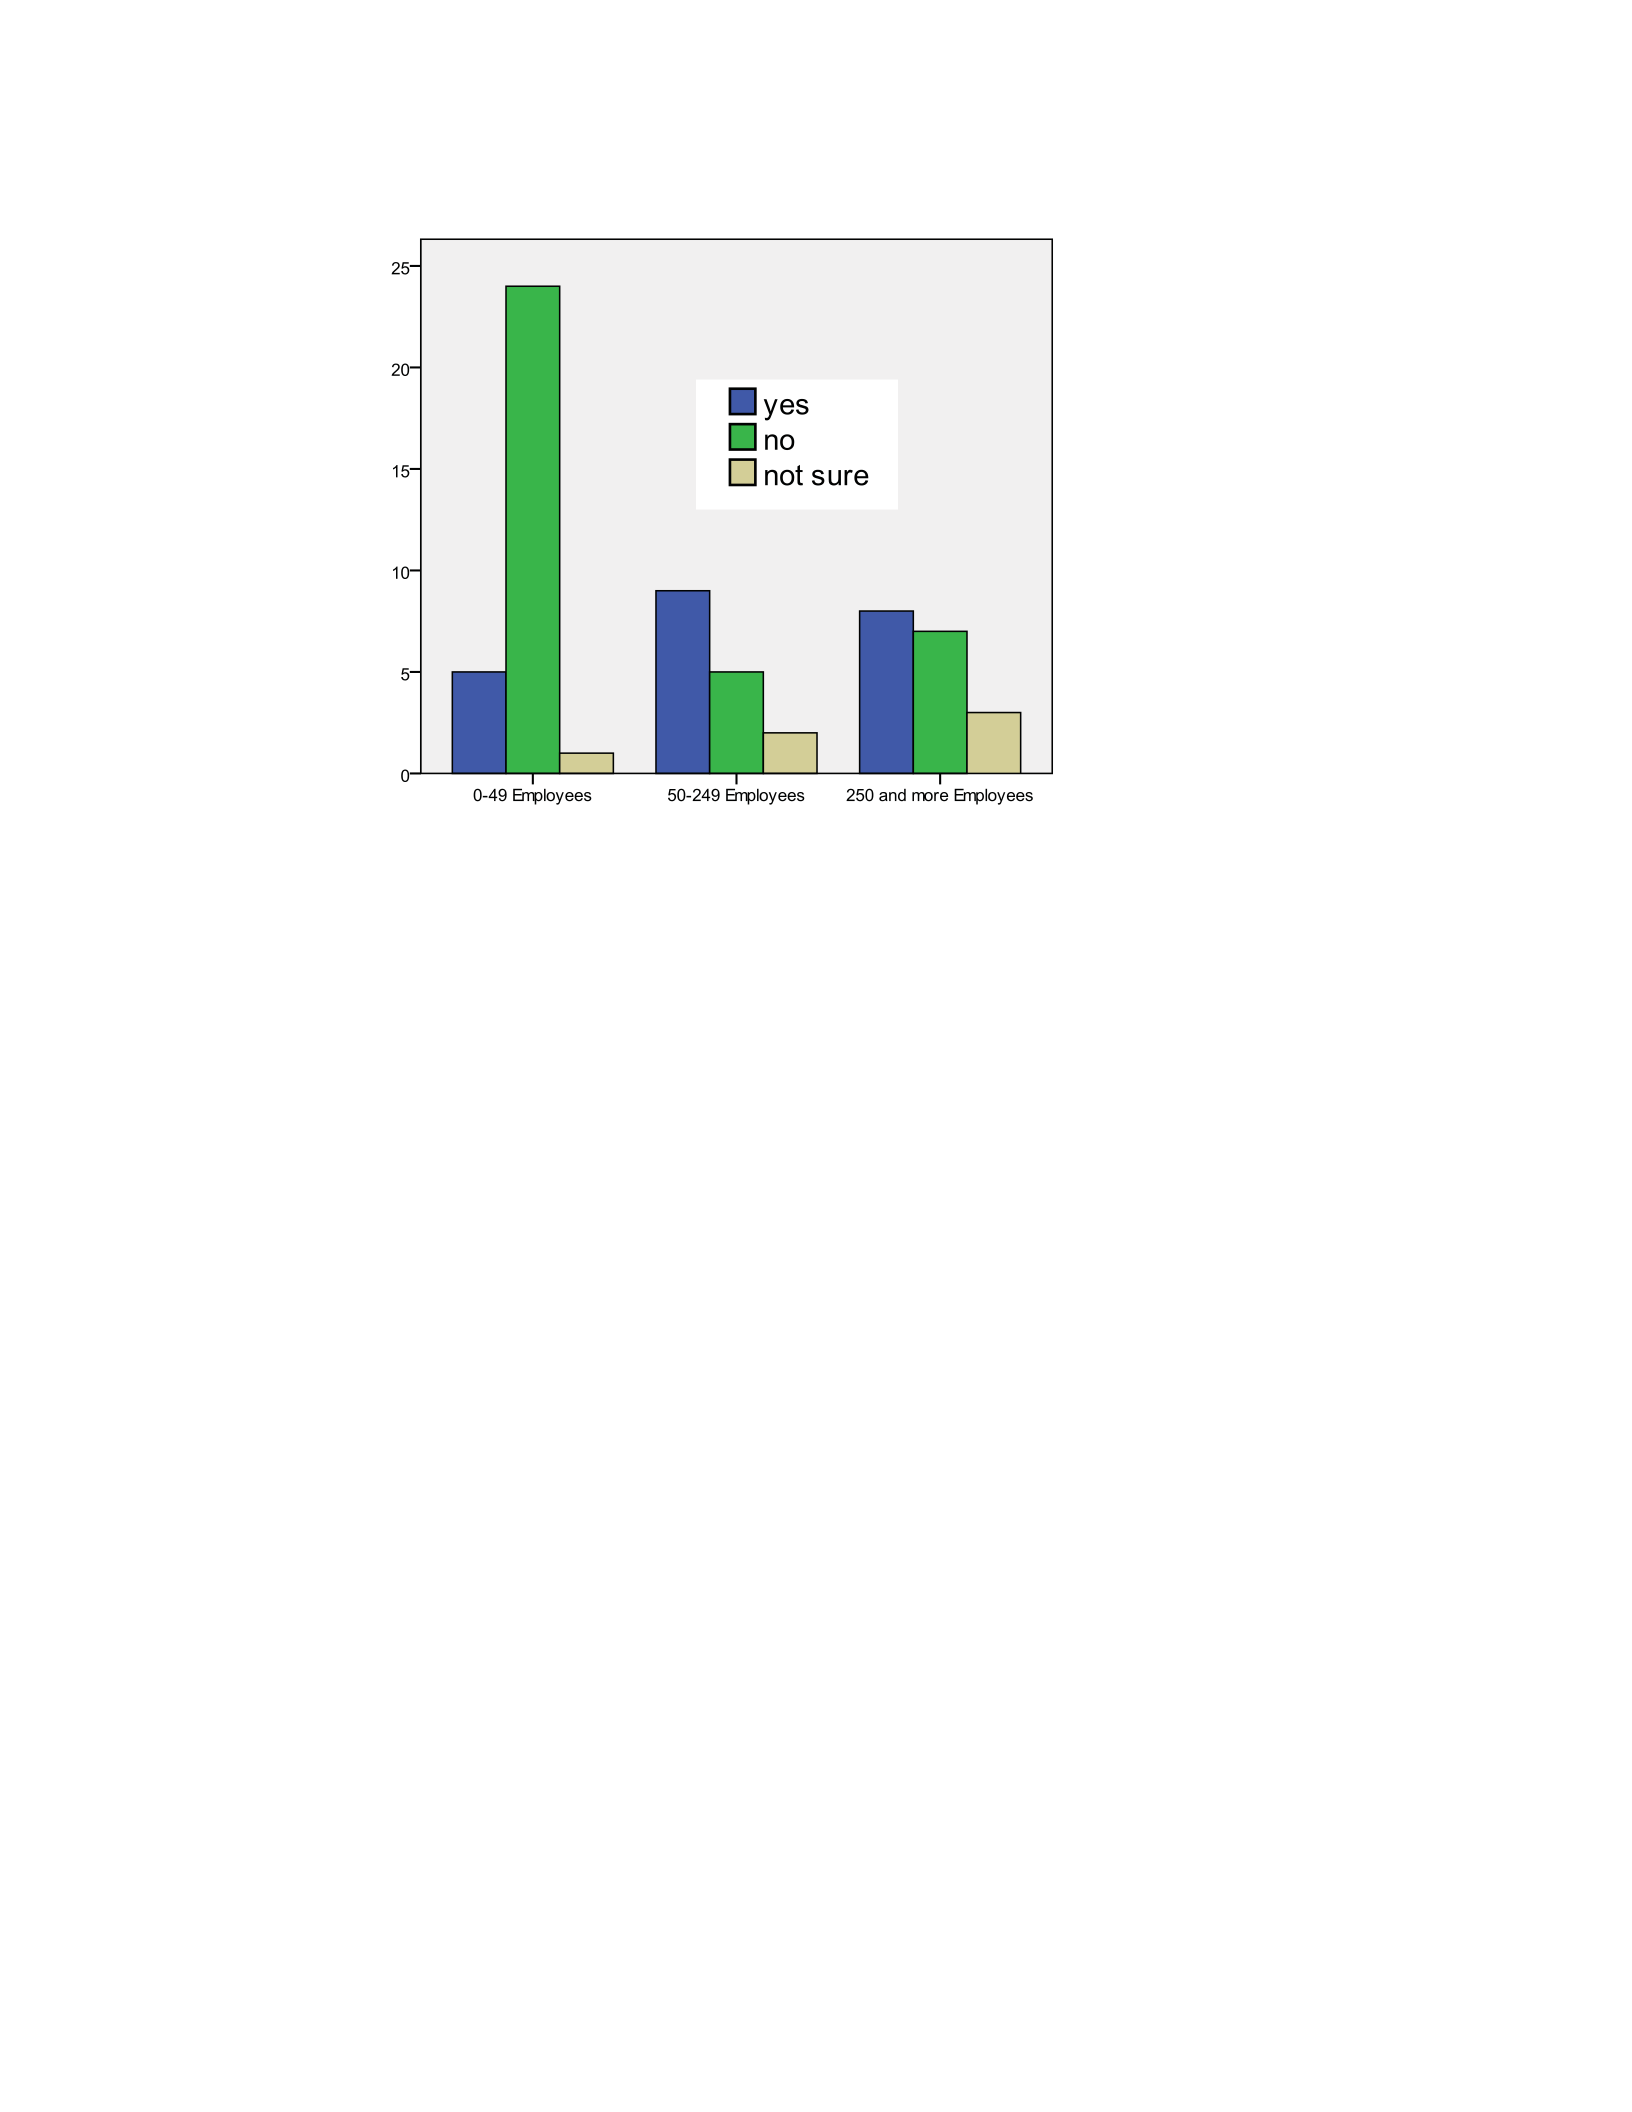
90
Figure 32 Company size and the existence of a team or department for ergonomics
problems
Another significant relationship was related to the company size as well. Because
middle and large size companies have had more opportunities to provide training to their
employees, a statistical test was found significant for company size and workers
receiving training (p 2QO\SHUFHQWRIVPDOOFRPSDQLHVFRXOGSURYLGHWUDLQLQJ
to their employees while 62.5 percent of middle size companies and 55.6 percent of large
size companies provided training for their workers in HF/E issues (Figure 33). There
were 14.1 percent of managers who were not sure about the existence of any training
programs for their employees.
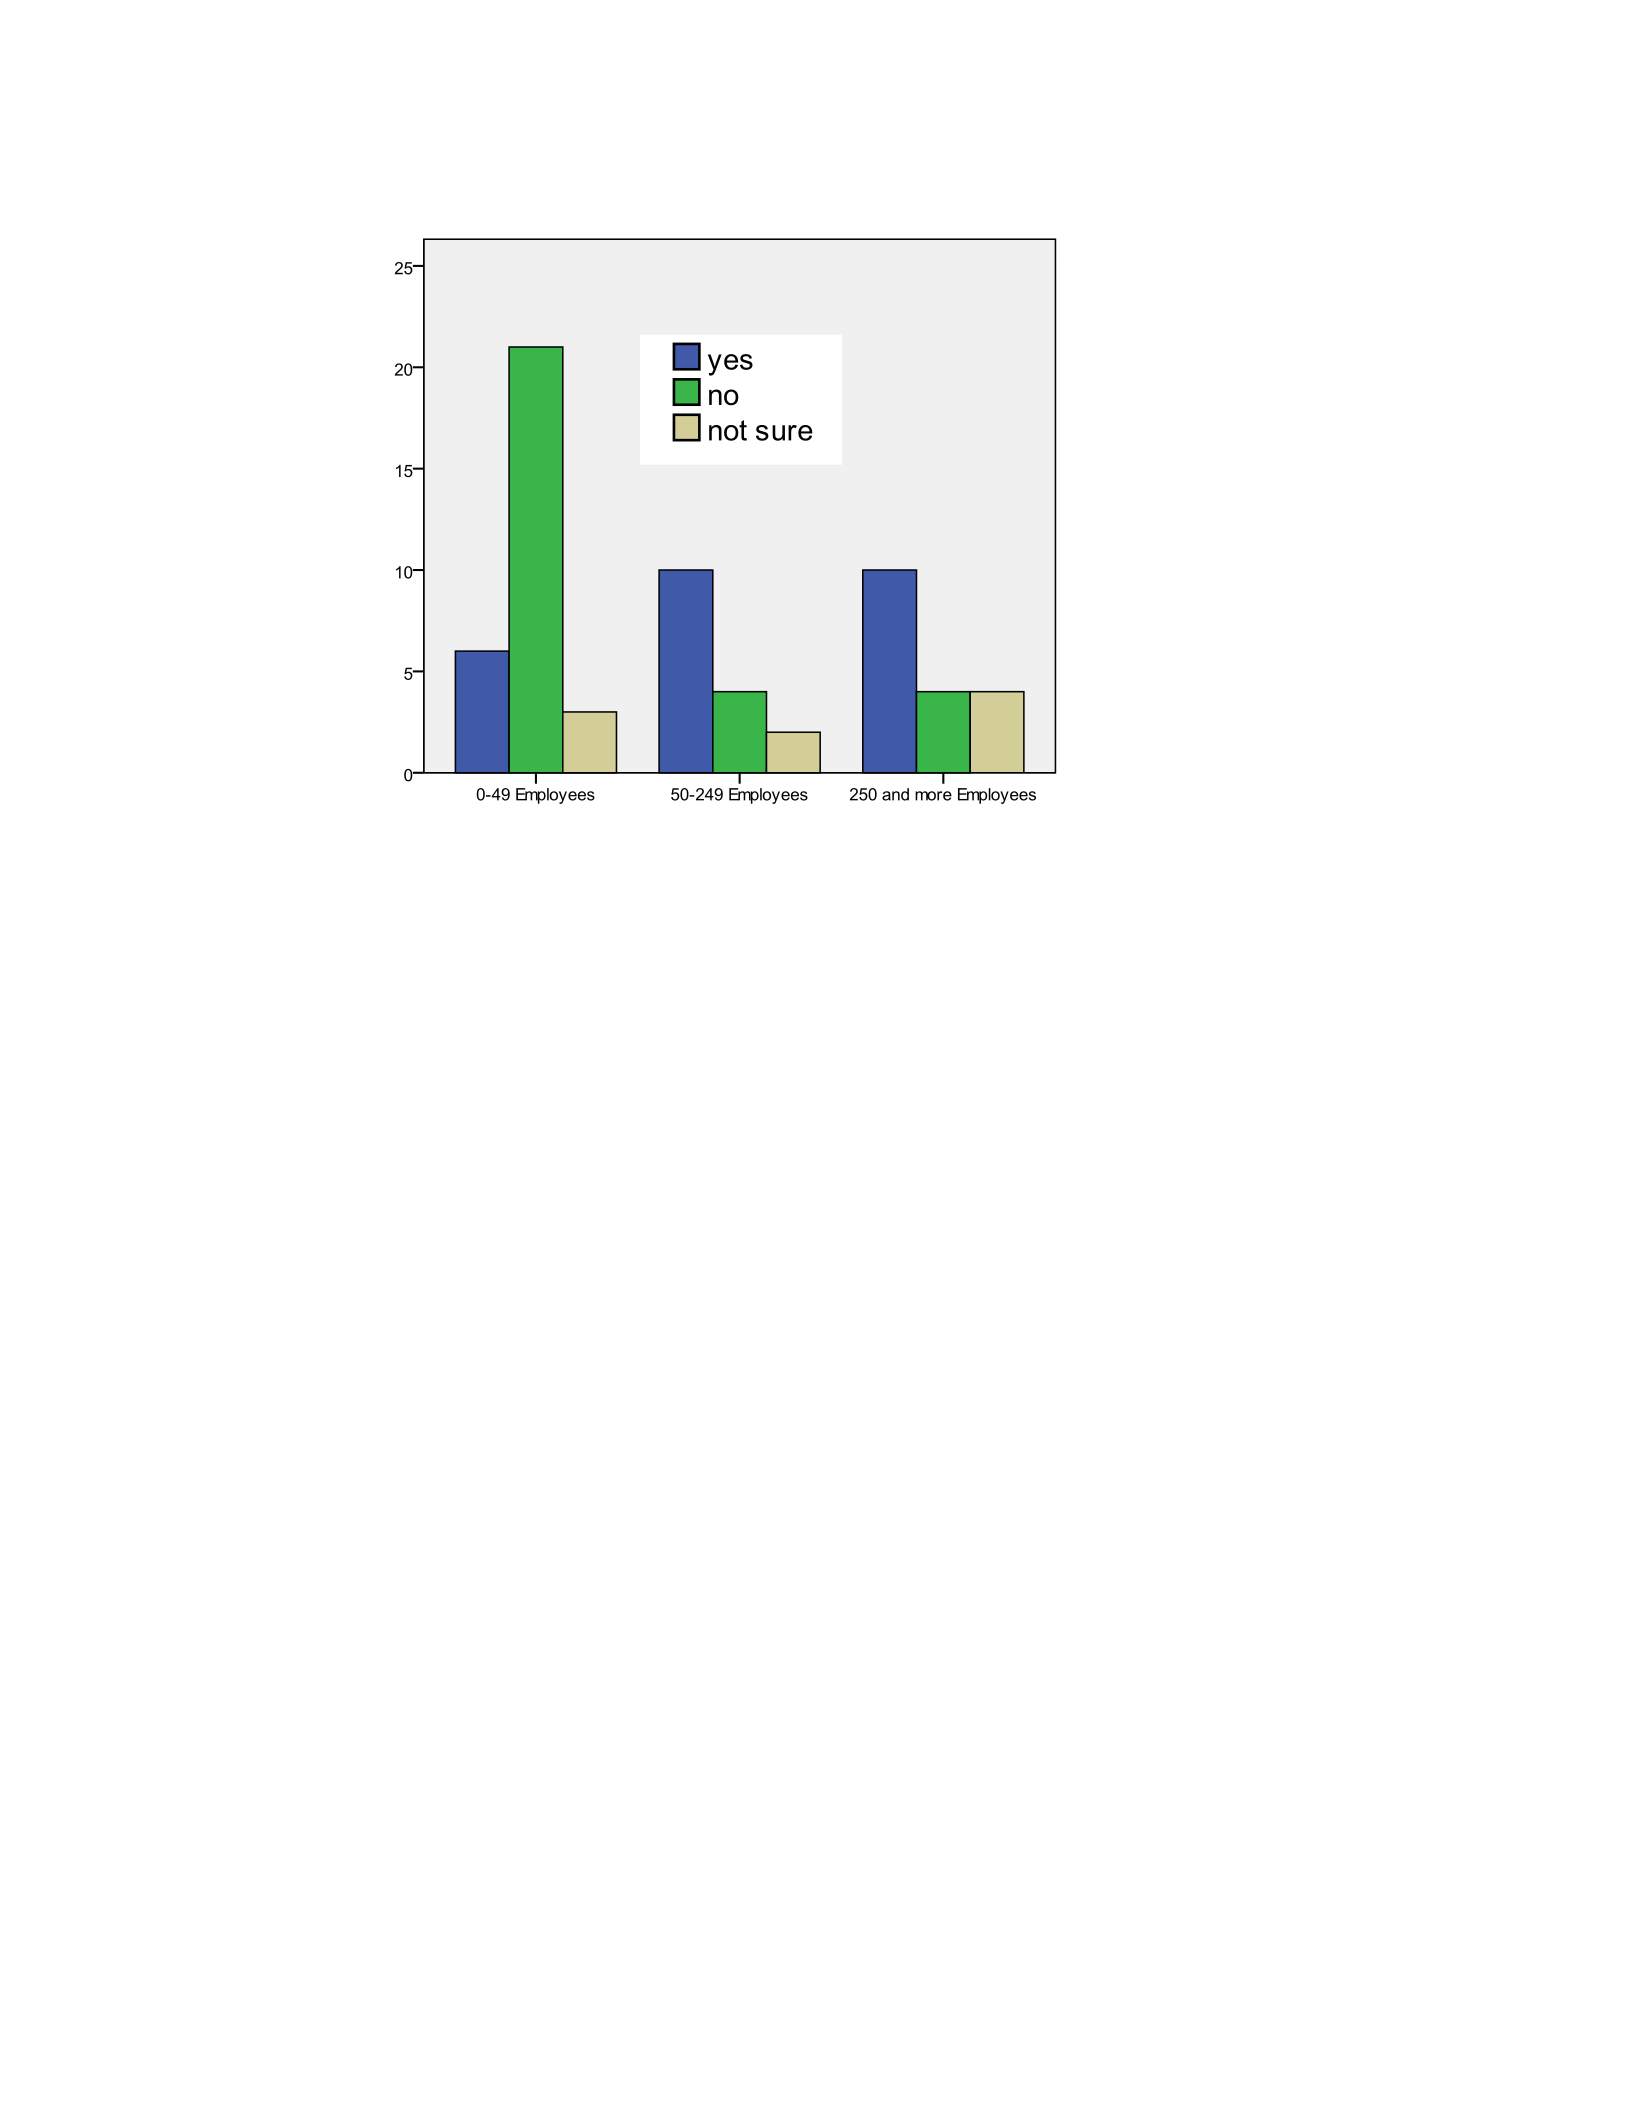
91
Figure 33 Company size and the existence of training programs for workers
Managers’ Preference for Ergonomically Designed Equipment and Availability
of Resources for Human Factors and Ergonomics Interventions
Furniture manufacturer managers were asked a critical question. The question
focused on determining the level of managers’ commitment to HF/E. The question was
whether managers prefer ergonomically designed equipment to decrease the risk of
occupational injuries and illnesses even if the equipment was more costly rather than
conventional equipment. This issue has been a controversial issue for a long time.
Managers have faced this dilemma. Some managers can allocate their resources to obtain
ergonomically designed equipment even if it is expensive. However, the heavy financial
burden of this equipment may compel others to prefer traditional and cheap equipment.
The responders’ distribution to this question is given in Table 20.
92
Table 20 Preference of ergonomically designed equipment and the availability of
sufficient resources
Questions
Yes No Not sureTotal
(N) (%) (N) (%) (N) (%) (N)
Do you prefer "ergonomically designed" equipment
to reduce occupational hazards and accidents even if
they are more expensive than regular equipment?
37 57.8 11 17.2 16 25 64
Are sufficient resources available in your company
to enhance or improve ergonomics activities? 21 32.8 30 46.9 13 20.3 64
Fortunately, 57.8 percent of managers expressed that they would prefer user-
friendly equipment even if it will bring some financial burden to the company. On the
other hand, 17.2 percent of managers expressed that they would not prefer expensive
equipment even though it is ergonomically designed. The ratio of managers who were in
a dilemma about this was 25 percent.
Preference of ergonomically designed equipment depends on the availability of
sufficient resources in the company. Only 32.8 percent of managers mentioned that they
had sufficient resources to allocate ergonomics interventions. About half of the managers
complained about the financial bottle necks.
The difference between the managers working in financially available companies
(32.8%) and the managers preferring ergonomically designed equipment even if
equipment is more expensive than conventional ones (57.8%) was 25 percent. Therefore,
it can be said that at least a quarter of the managers expressed that they would prefer
93
ergonomically designed equipment even though they do not have sufficient resources to
afford them.
The statistical analysis (Table 21) showed that there was a significant relationship
(p EHWZHHQWKHVWDWHDQGSUHIHUHQFHRIHUJRQRPLFDOO\GHVLJQHGHTXLSPHQW
Seventy-one percent of Mississippi managers expressed that they would prefer
ergonomically designed equipment (Figure 34). 22.6 percent of Mississippi managers
were unsure and only 6.5 percent of them took a negative stance toward ergonomically
designed equipment if they were more expensive than conventional equipment.
Table 21 Statistical analysis of managers’ demographic properties and preference of
ergonomically designed equipment and the availability of sufficient resources
State Education NAICS Employees
Experience in
FI
Position
Experience in
P
Ergonomically equipment Ȥ25.972 1.500 1.124 2.576 6.736 3.191 5.828
p0.050* 0.827 0.890 0.631 0.151 0.526 0.212
Sufficient resources Ȥ23.341 0.949 0.734 10.437 2.693 6.591 10.116
p0.188 0.917 0.947 0.034* 0.610 0.159 0.039*
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p
: p-value (The level of statistical significance).
There was some significant relationship between managers’ demographic
properties and the availability of sufficient resources. Small company managers
mentioned that they did not have sufficient resources to allocate HF/E interventions (p
0.034) (Figure 35). Moreover, managers who had 3-10 year experience in their positions
expressed that they had sufficient resources for HF/E issues (p )LJXUH
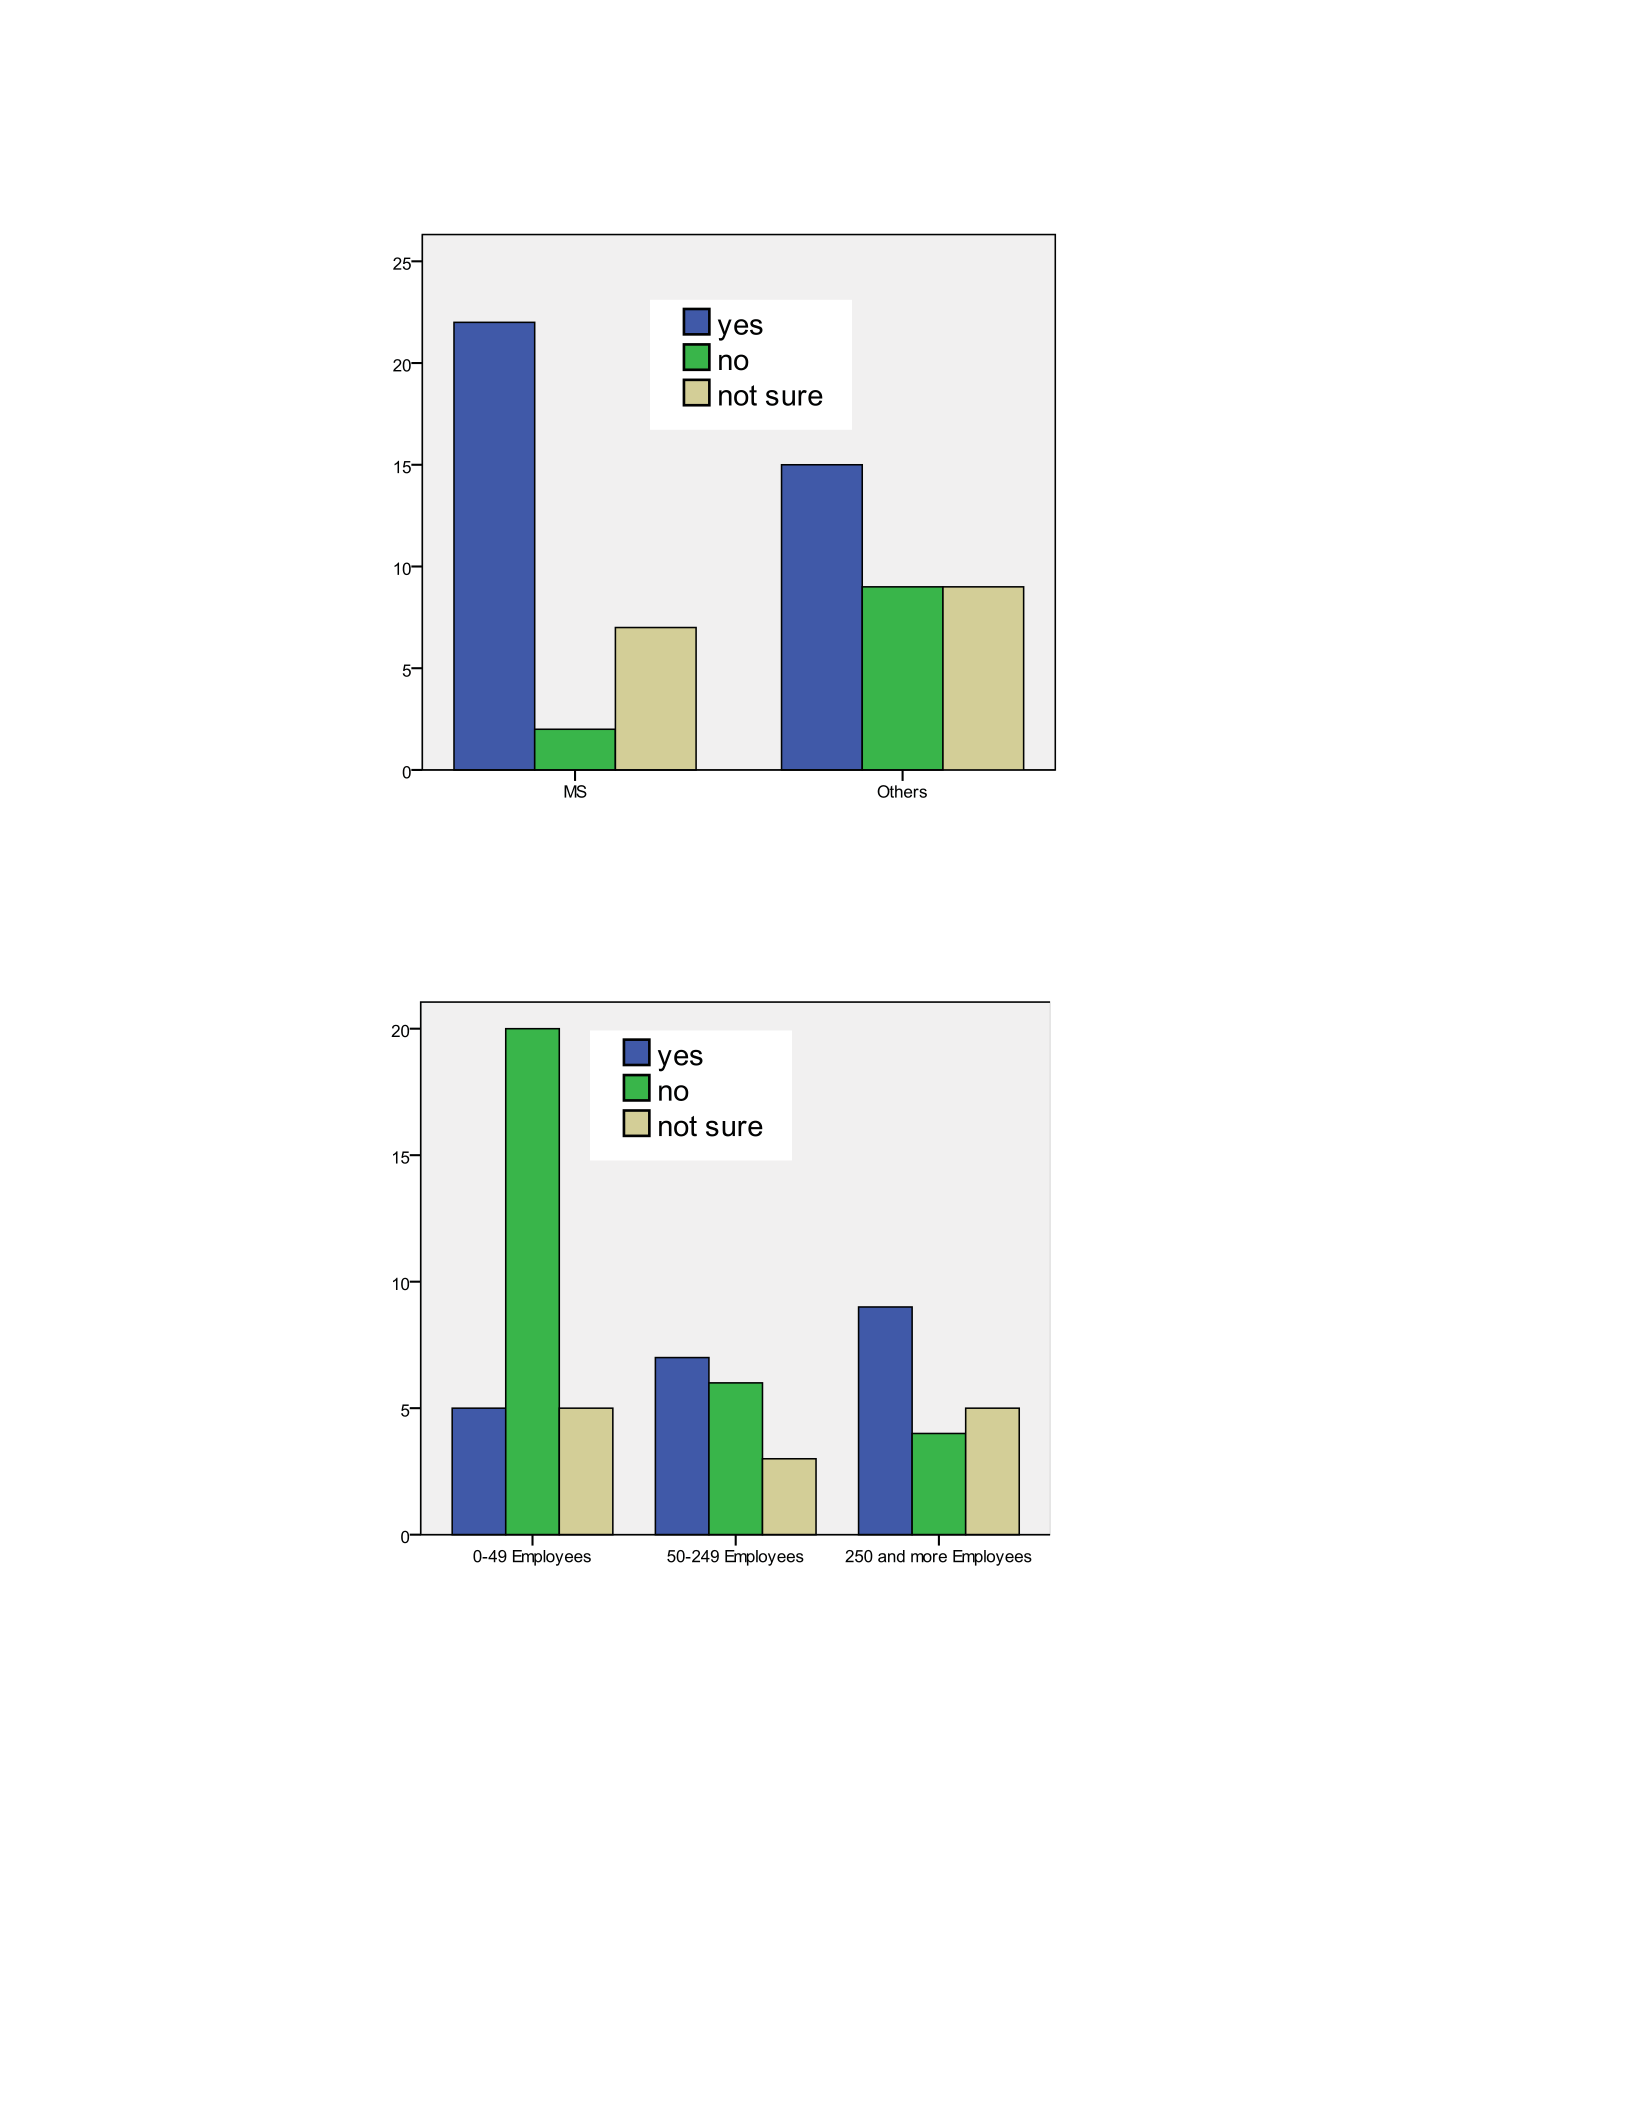
94
Figure 34 Mississippi vs. other states regarding the preference of ergonomically
designed equipment
Figure 35 Company size and effect on answer for resource availability
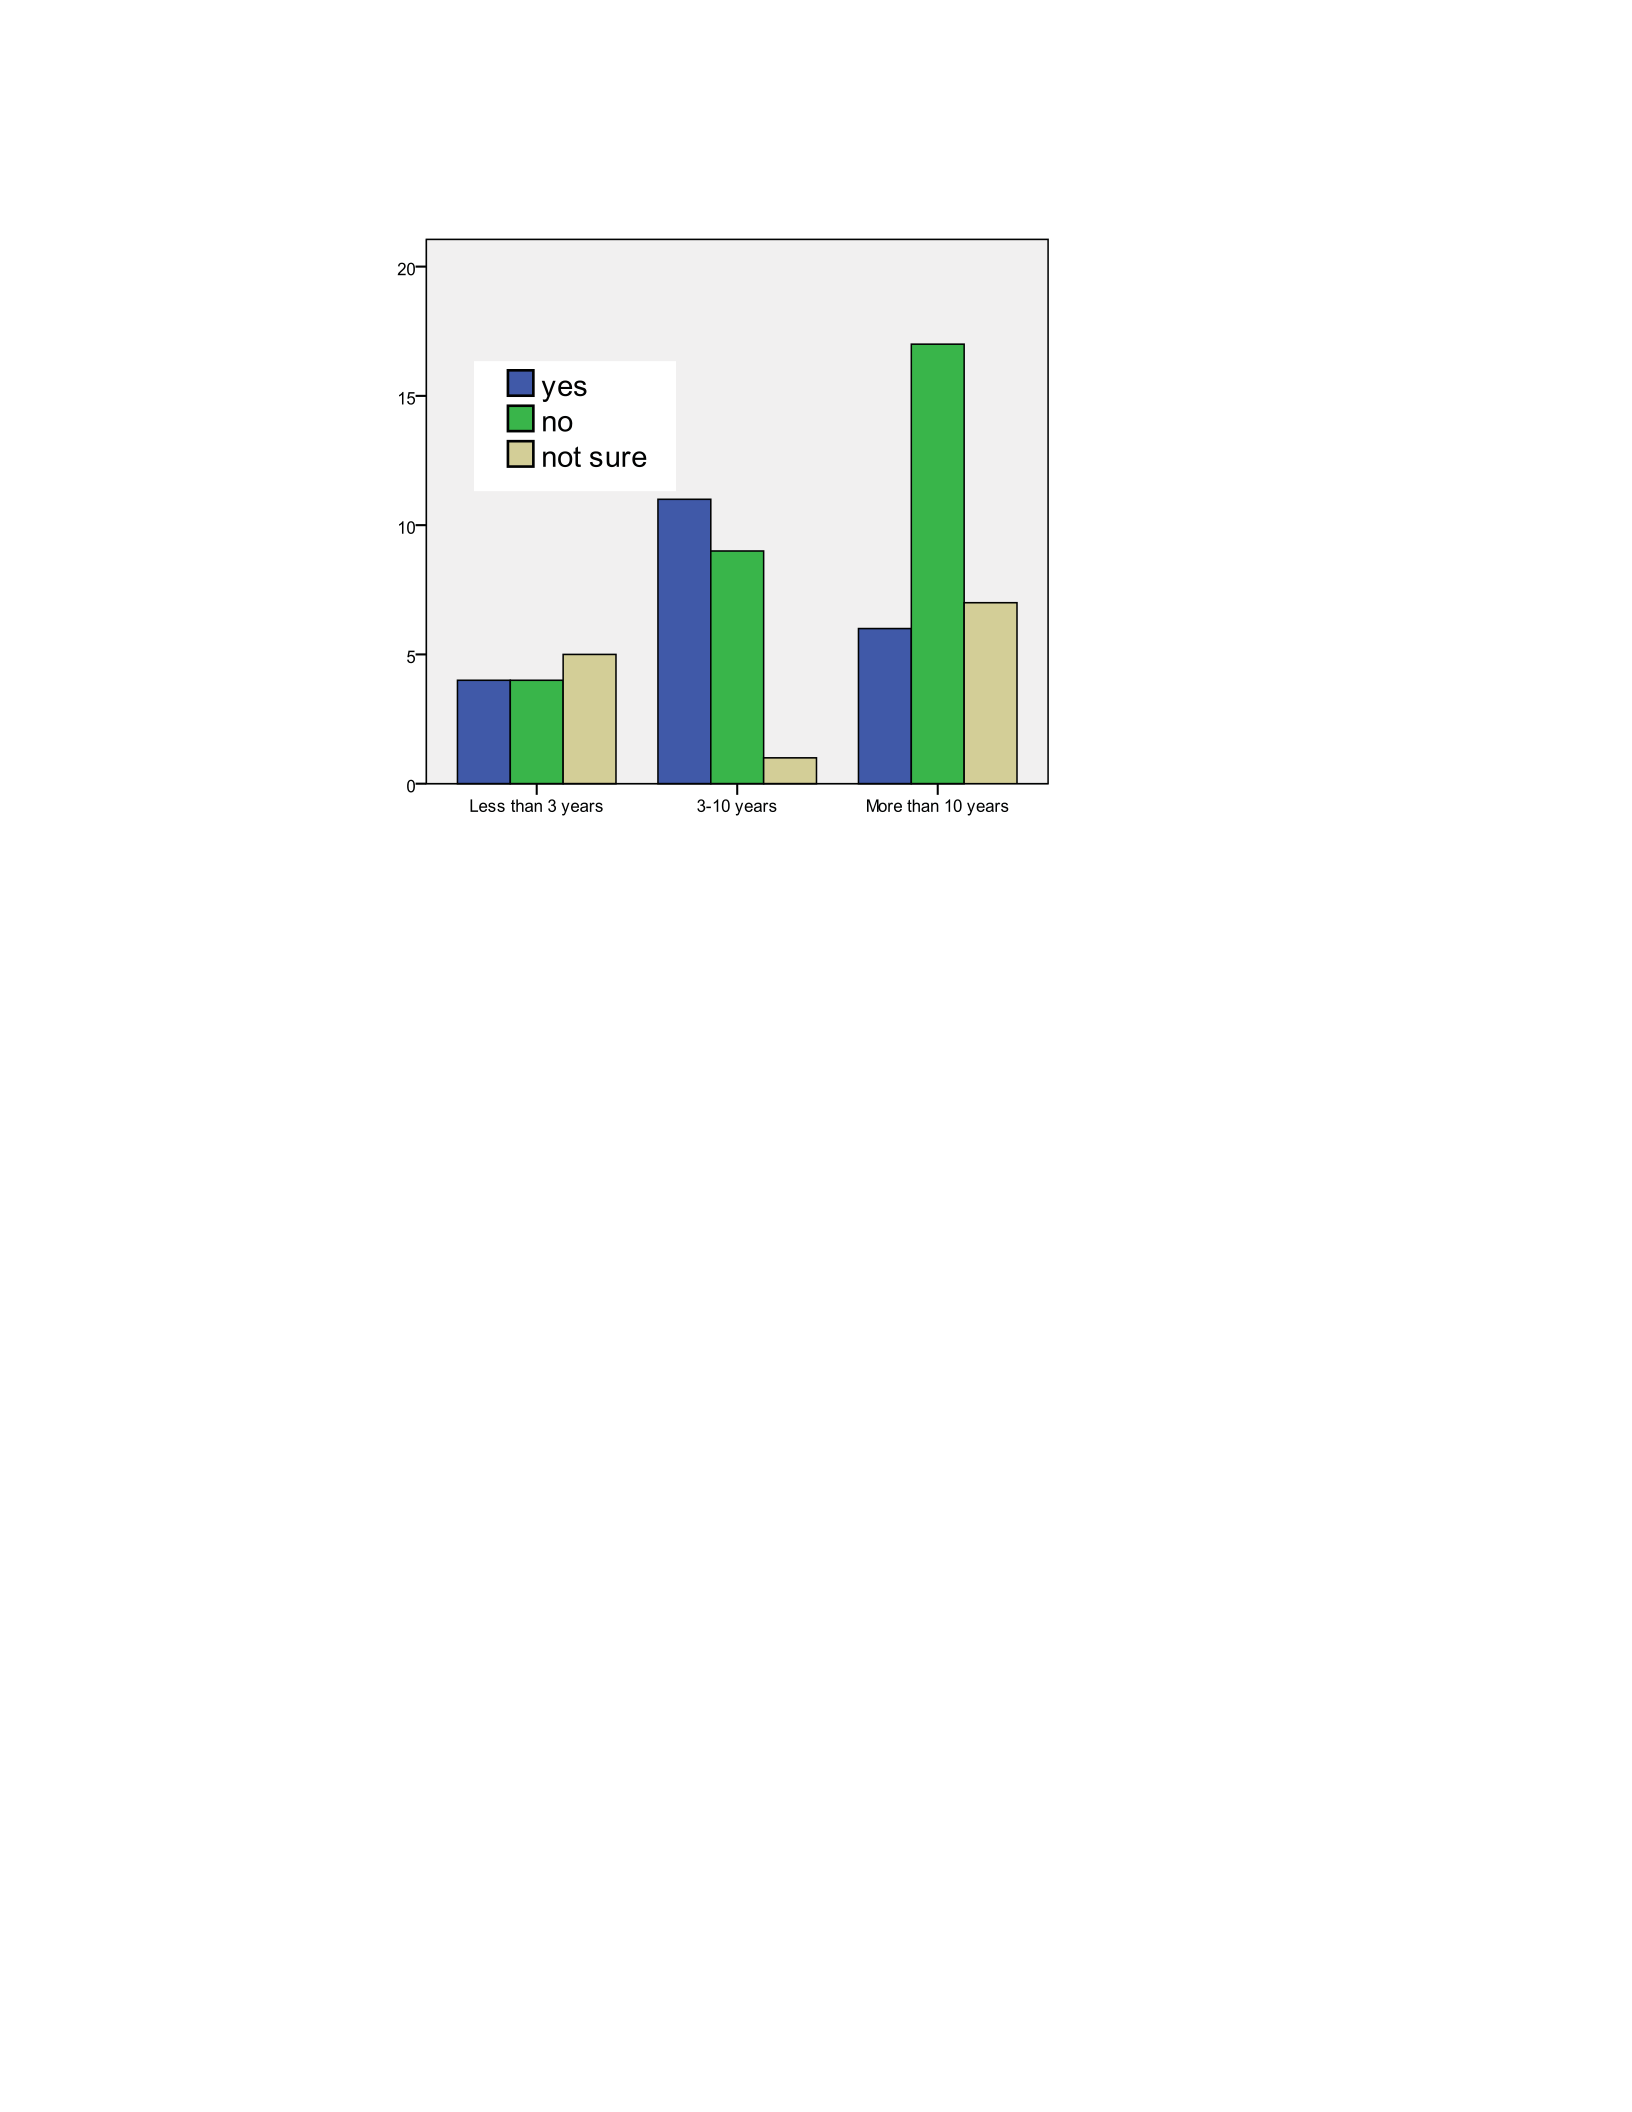
95
Figure 36 Managers’ experience in current position and possible effect
on answer for availability of sufficient resources
Managers’ Opinions about the Necessities for
Human Factors and Ergonomic Sources
The managers were asked to rate their thoughts about the necessity of HF/E
sources on a five-point scale ranging from “not necessary at all” to “strongly necessary.”
The data distribution of the managers’ opinions about necessities was obtained (Table
22).
The mean of the respondents’ scores for the necessity of scientific data about
HF/E was 3.00. This means managers, in general, took a neutral stance on the scientific
data’s necessity. Certainly, scientific data and knowledge is tremendously necessary to
solve problems and create better working environments. This neutral stance could be
caused from the complexity of data and knowledge in HF/E. If the 11th question of this
survey is checked again, it could be seen that 45.3 percent of managers were neutral or in

96
agreement that scientific data about HF/E was too complex to understand and apply.
Thus, there is a possibility that managers may think the scientific data is not necessary
because they have a difficult time understanding and applying the complex data.
Because human factors specialists or ergonomists have an active role in initiating
and continuing an HF/E program, employing a human factor specialist(s) or an
ergonomist(s), particularly at the start of a program, is a necessity (Pehkonen et al. 2009).
Even though participants generally agreed with the importance of HF/E, only 12.5
percent of them considered employing a human factor specialist(s) or an ergonomist(s) in
their organizations. The rest of the participants probably had the opinion that HF/E issues
were the issues should be addressed, but not the issues were necessary to address.
97
Table 22 Managers’ opinion about the necessities for human factors and ergonomic sources
Questions
Not necessary
at all
Not
necessary Neutral Necessary Strongly
Necessary
Rating
Average
Total
Respond
(N) (%) (N) (%) (N) (%) (N) (%) (N) (%)
Scientific data about human factors and
ergonomics 7 10.9 12 18.8 23 35.9 18 28.1 4 6.3 3.00 64
Employing an ergonomist(s) or a human
factors' professional(s) 23 35.9 20 31.3 13 20.3 7 10.9 1 1.6 2.11 64
A team or department to handle HF/E
problems 18 28.1 16 25 13 20.3 14 21.9 3 4.7 2.50 64
Training workers for human factors and
ergonomics 6 9.5 5 7.9 19 30.2 23 36.5 10 15.9 3.41 64
Training management for human factors and
ergonomics 8 12.5 7 10.9 15 23.4 21 32.8 13 20.3 3.38 64
Resources for HF/E issues 6 9.4 10 15.6 16 25 25 39.1 7 10.9 3.27 64

98
A team or department that is supported by professional human factors specialists
or ergonomists can bring success. A total of 26.6 percent of mangers expressed that a
team or department is necessary to handle HF/E problems. Up to 53.1 percent of
managers, on the other hand, expressed that a team or department to handle HF/E
problems is not a necessity. Because of this thinking, managers did not establish a team
or department. The 13th question confirmed this interpretation. The 13th question asked
whether there was a team or department for ergonomic problems. Of the participants,
56.3 percent mentioned there was no team or department in their organizations. As a
result of the statistical test (Table 23), there were significant differences between the
thinking that a team or department is necessary, the state where managers were from (p
0.004) and managers’ positions (p
There were 69.7 percent of managers from other states who believed that a team
or department was not necessary while 35.5 percent of Mississippian managers believed
so (Figure 37).
Small company managers also had a negative stance about the necessity of a team
or department for finding and correcting HF/E problems (Figure 38). The significant
level of this statistical relationship was 0.004.
When the relationship between managers’ position and the necessity of a team or
department was investigated, it could be interpreted that owners (62.5%) believed that a
team or department was not necessary (Figure 39). However, the percentage of lower-
level managers was lower than owners (42.0%).
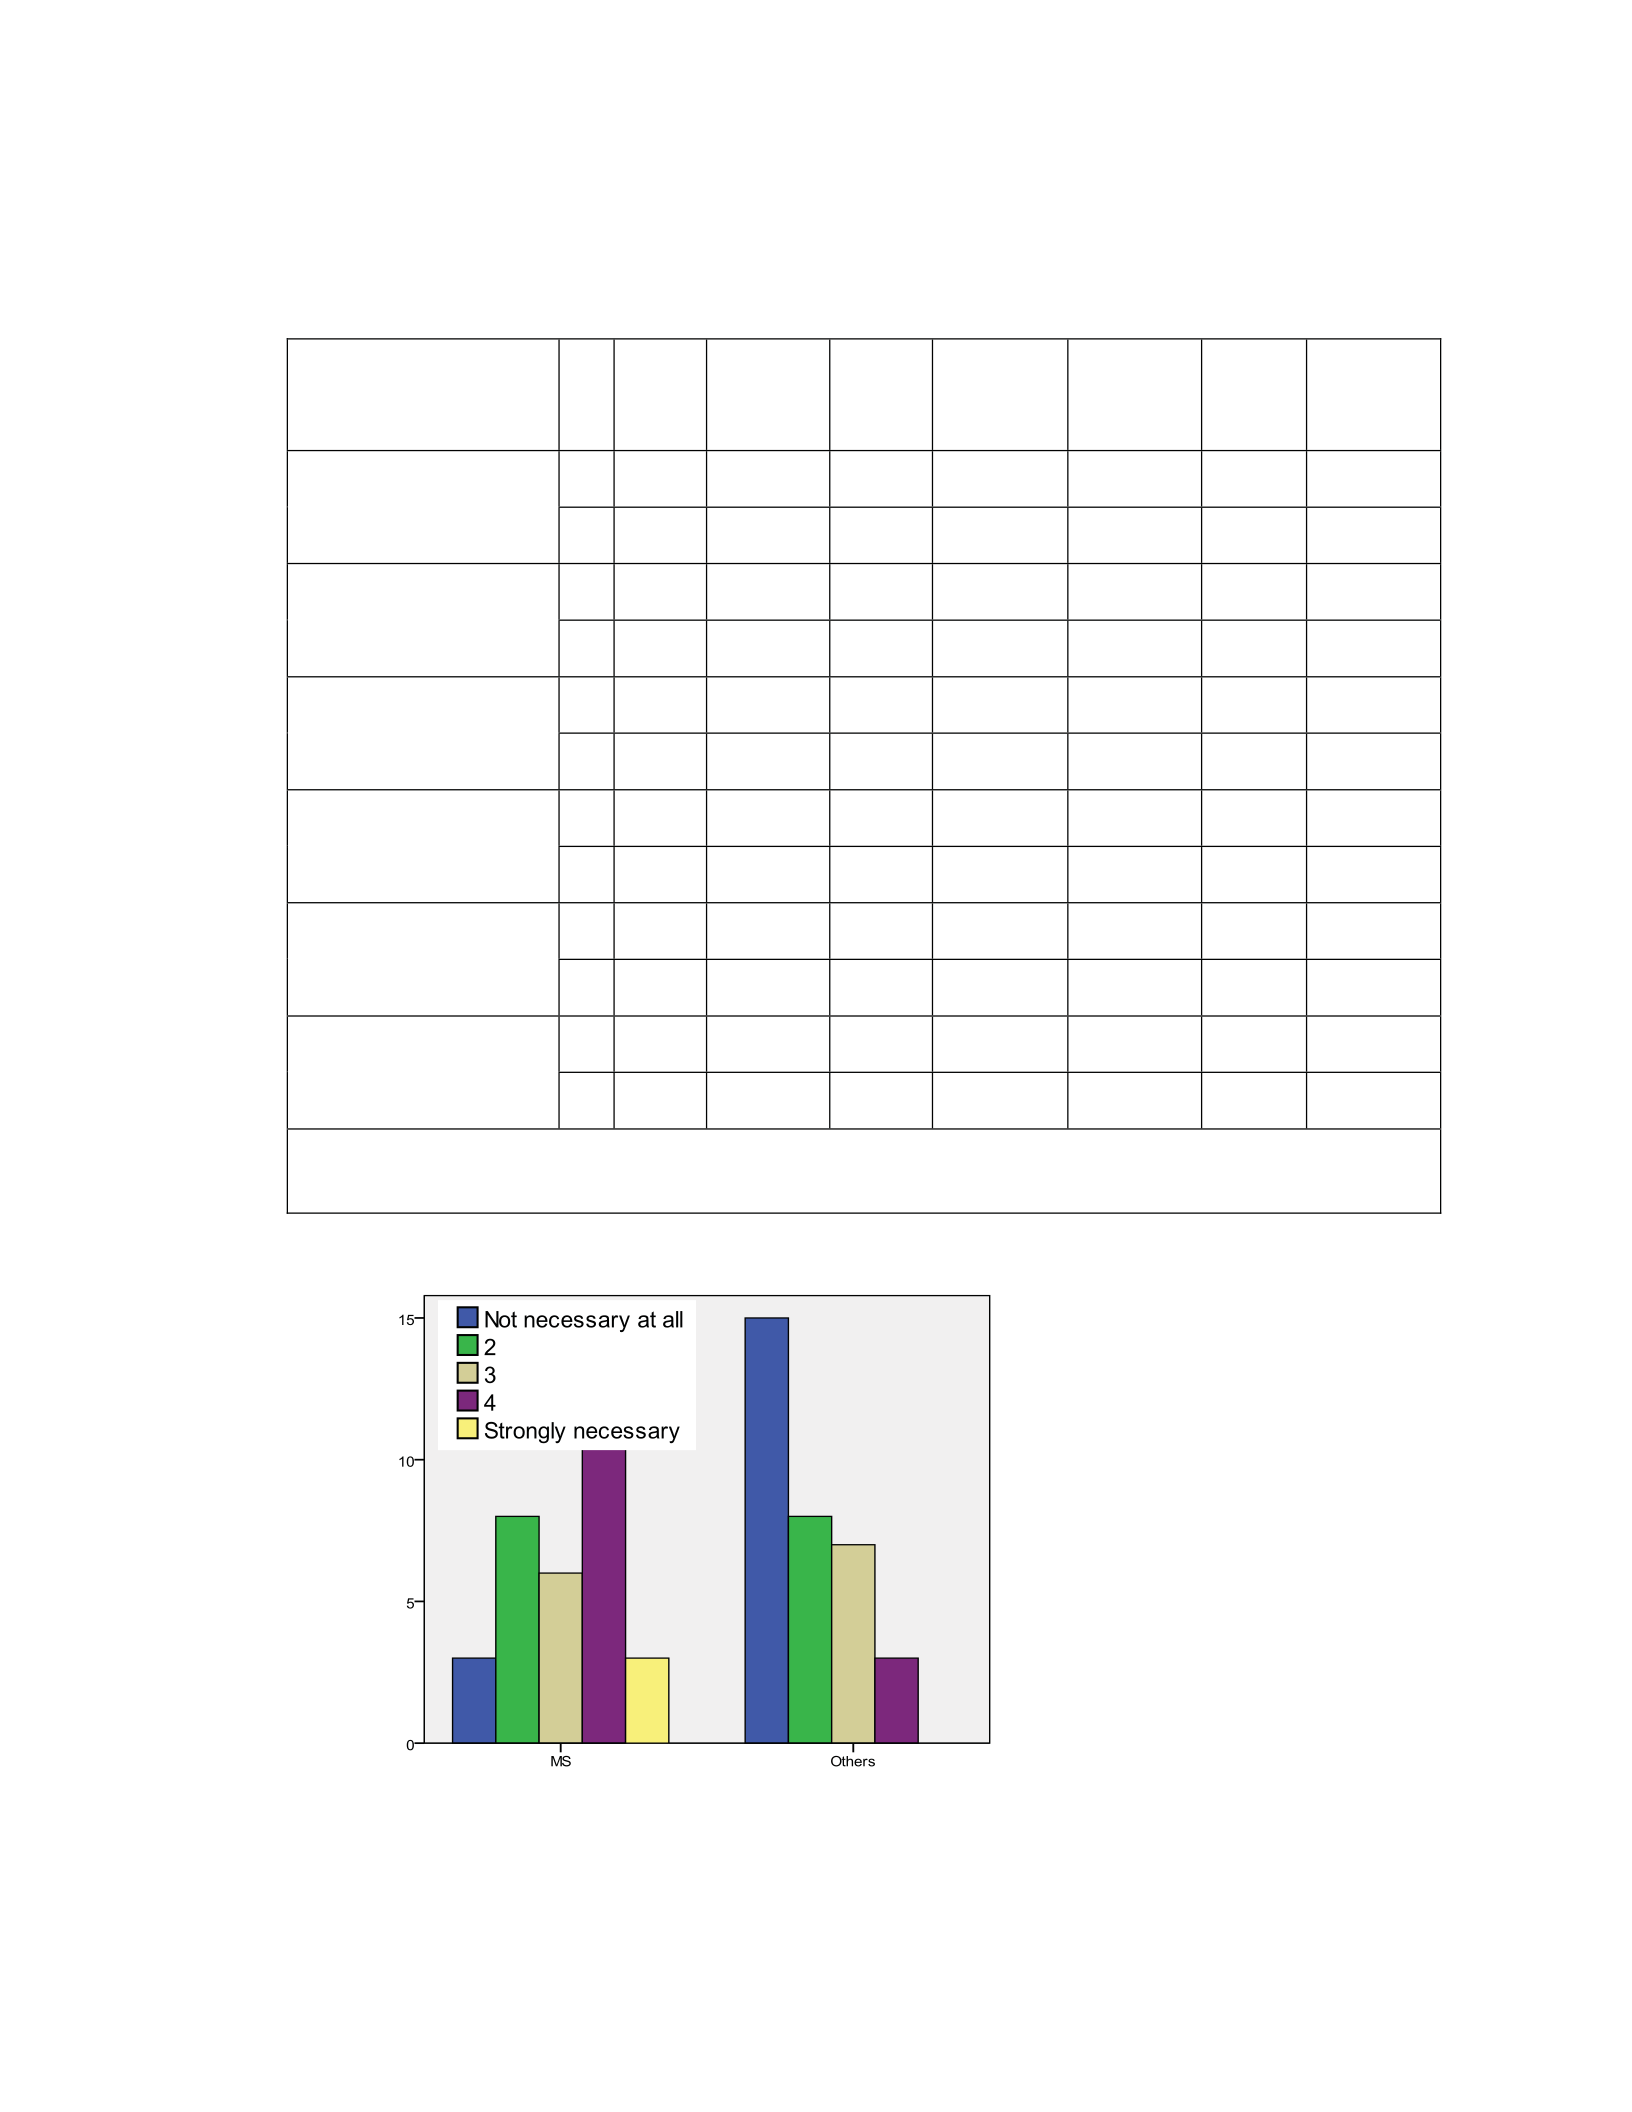
99
Table 23 Statistical analysis of managers’ demographic properties and managers’
opinion about the necessities for human factors and ergonomic sources
State Education NAICS Employees
Experience
in FI
Position
Experience in
P
Scientific data Ȥ26.781 8.604 8.059 14.731 10.161 10.366 8.615
p0.148 0.377 0.428 0.065 0.254 0.240 0.376
Human factors specialist
and ergonomists
Ȥ27.841 5.964 9.560 15.308 5.529 7.187 8.407
p0.098 0.651 0.297 0.053 0.700 0.517 0.395
A HF/E team or department Ȥ215.601 3.427 10.324 22.258 3.118 17.860 10.371
p0.004* 0.905 0.243 0.004* 0.927 0.022* 0.240
Training employees Ȥ212.683 11.406 25.514 10.686 12.541 8.153 15.752
p0.013* 0.180 0.001* 0.220 0.129 0.419 0.046*
Training managers Ȥ212.538 7.571 14.635 9.168 8.996 8.192 9.616
p0.014* 0.476 0.067 0.328 0.343 0.415 0.293
Resources Ȥ26.746 11.027 17.465 12.651 5.502 9.081 10.216
p0.150 0.200 0.026* 0.124 0.703 0.336 0.250
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p
: p-value (The level of statistical significance).
Figure 37 Mississippi vs. other states concerning the necessity of a team or department
for human factors and ergonomics problems
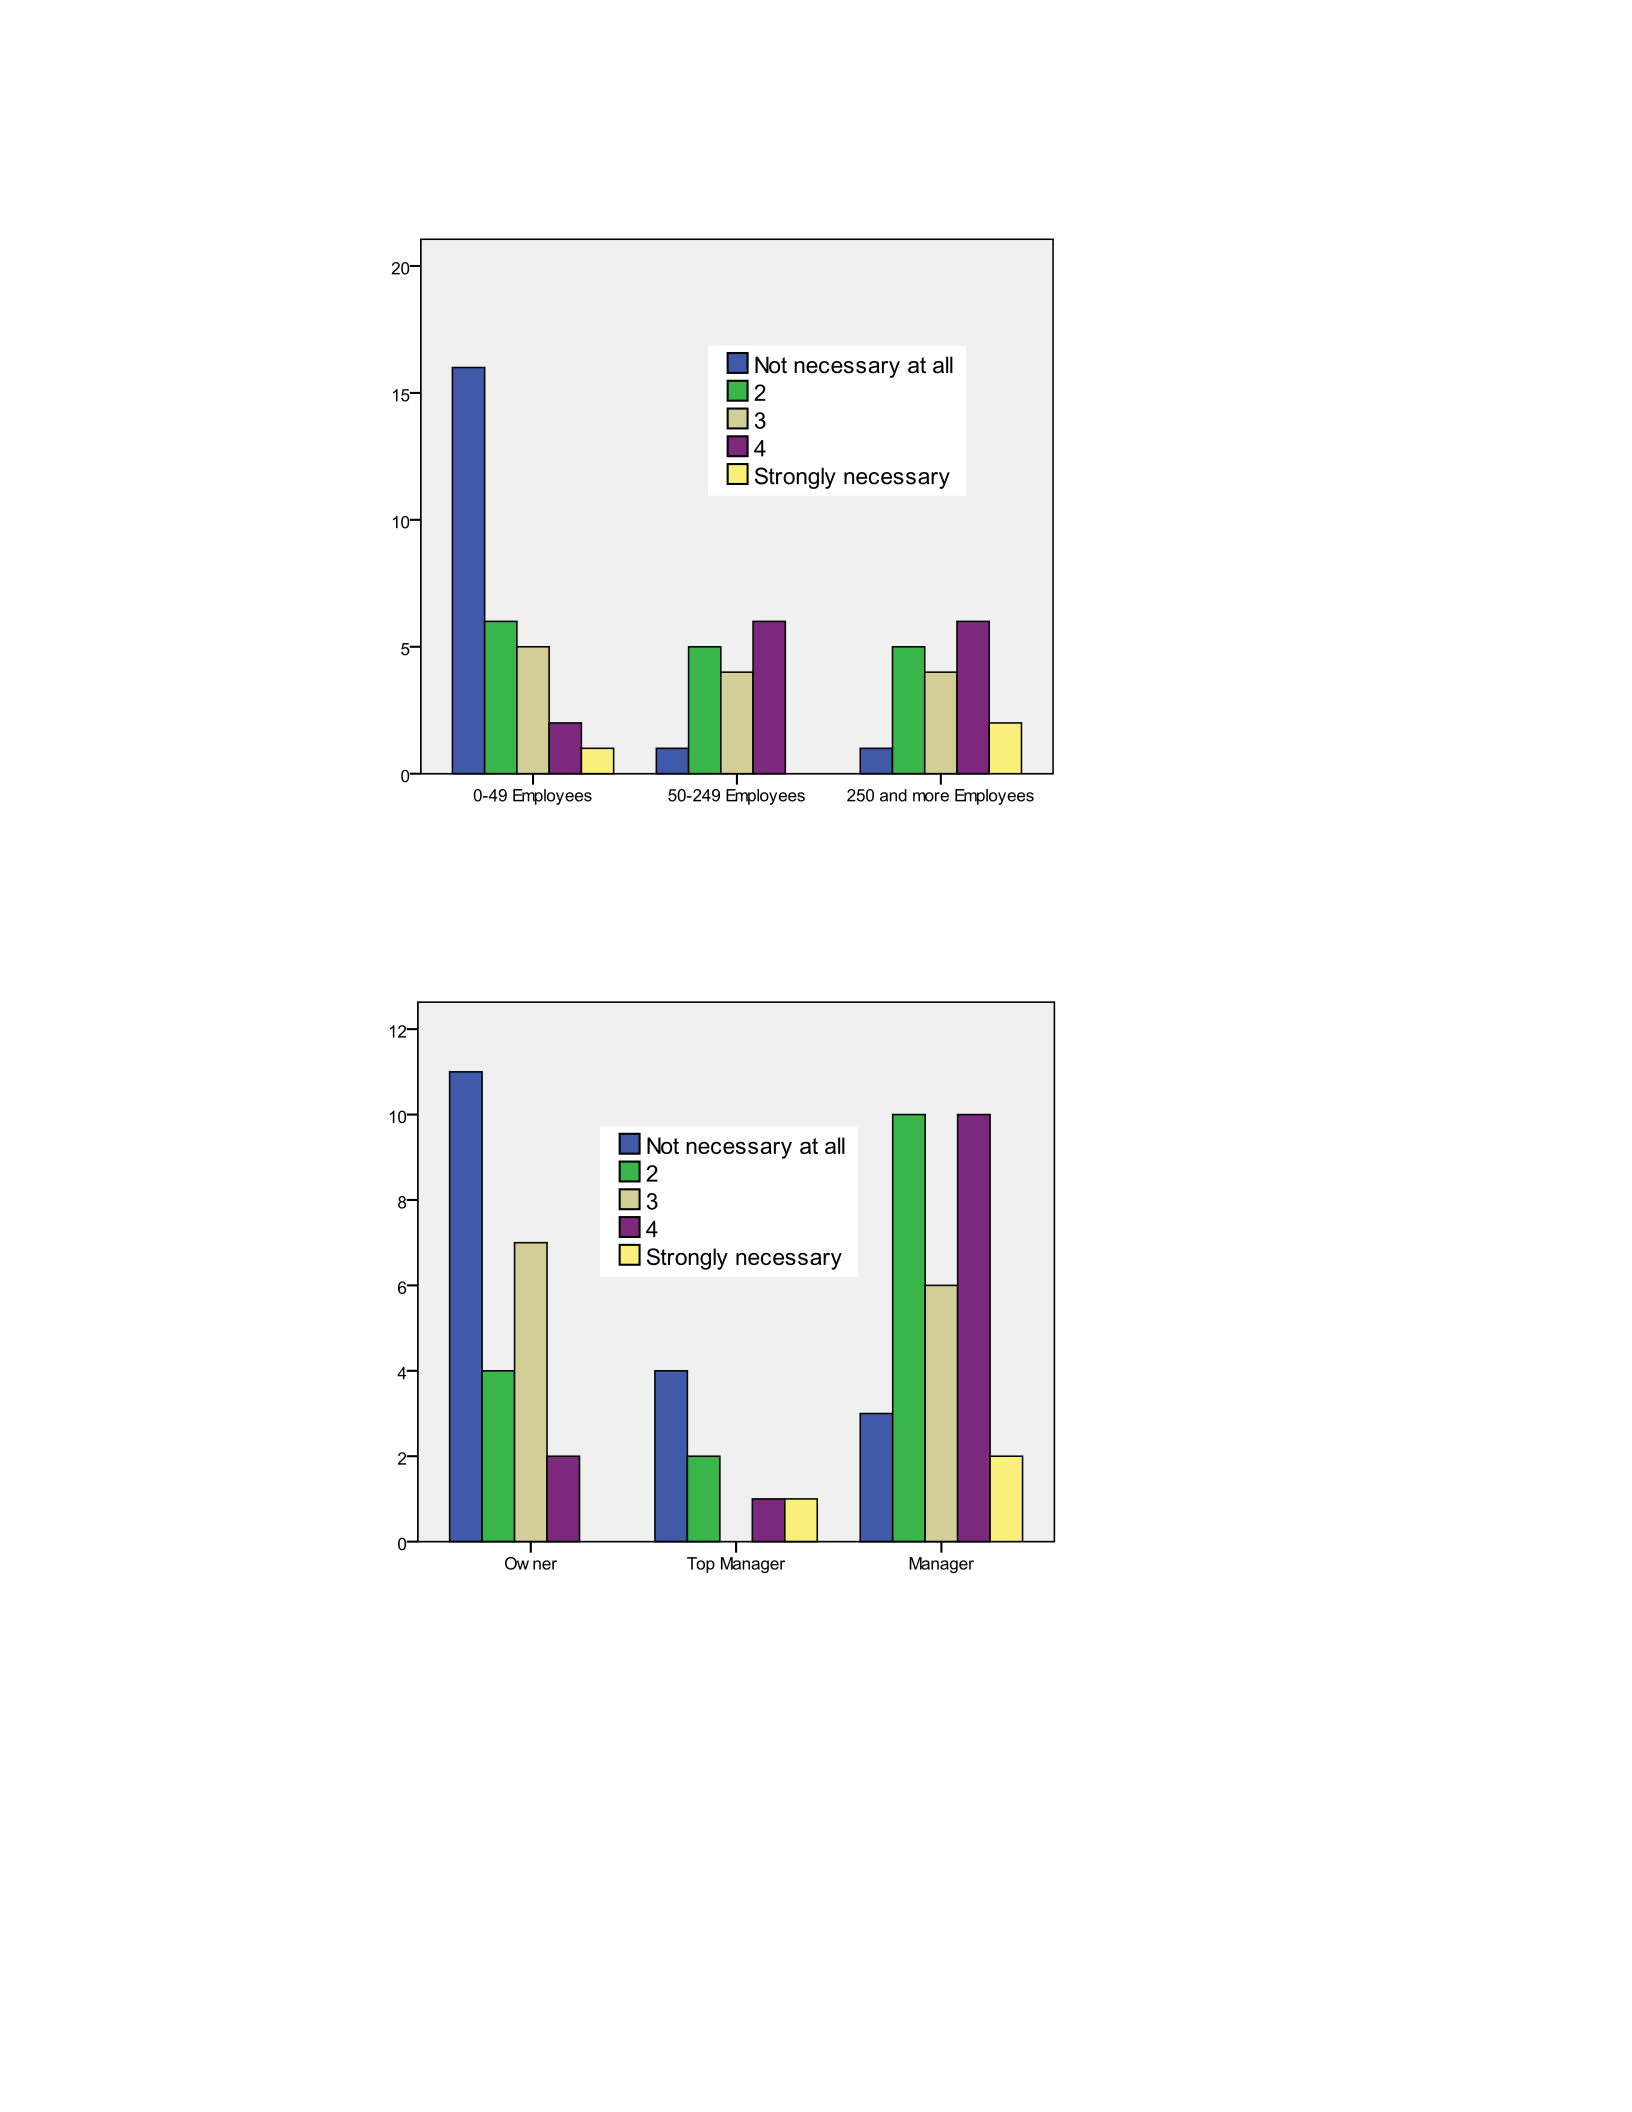
100
Figure 38 Company size and the necessity of a team or department for
human factors and ergonomics problems
Figure 39 Manager’s current position and its affect of their opinion on the necessity of a
team or department for human factors and ergonomics problems
Fortunately, the percentage of managers who believed that training workers for
HF/E was not necessary was not high (totally 17.4). The rest of managers took a neutral
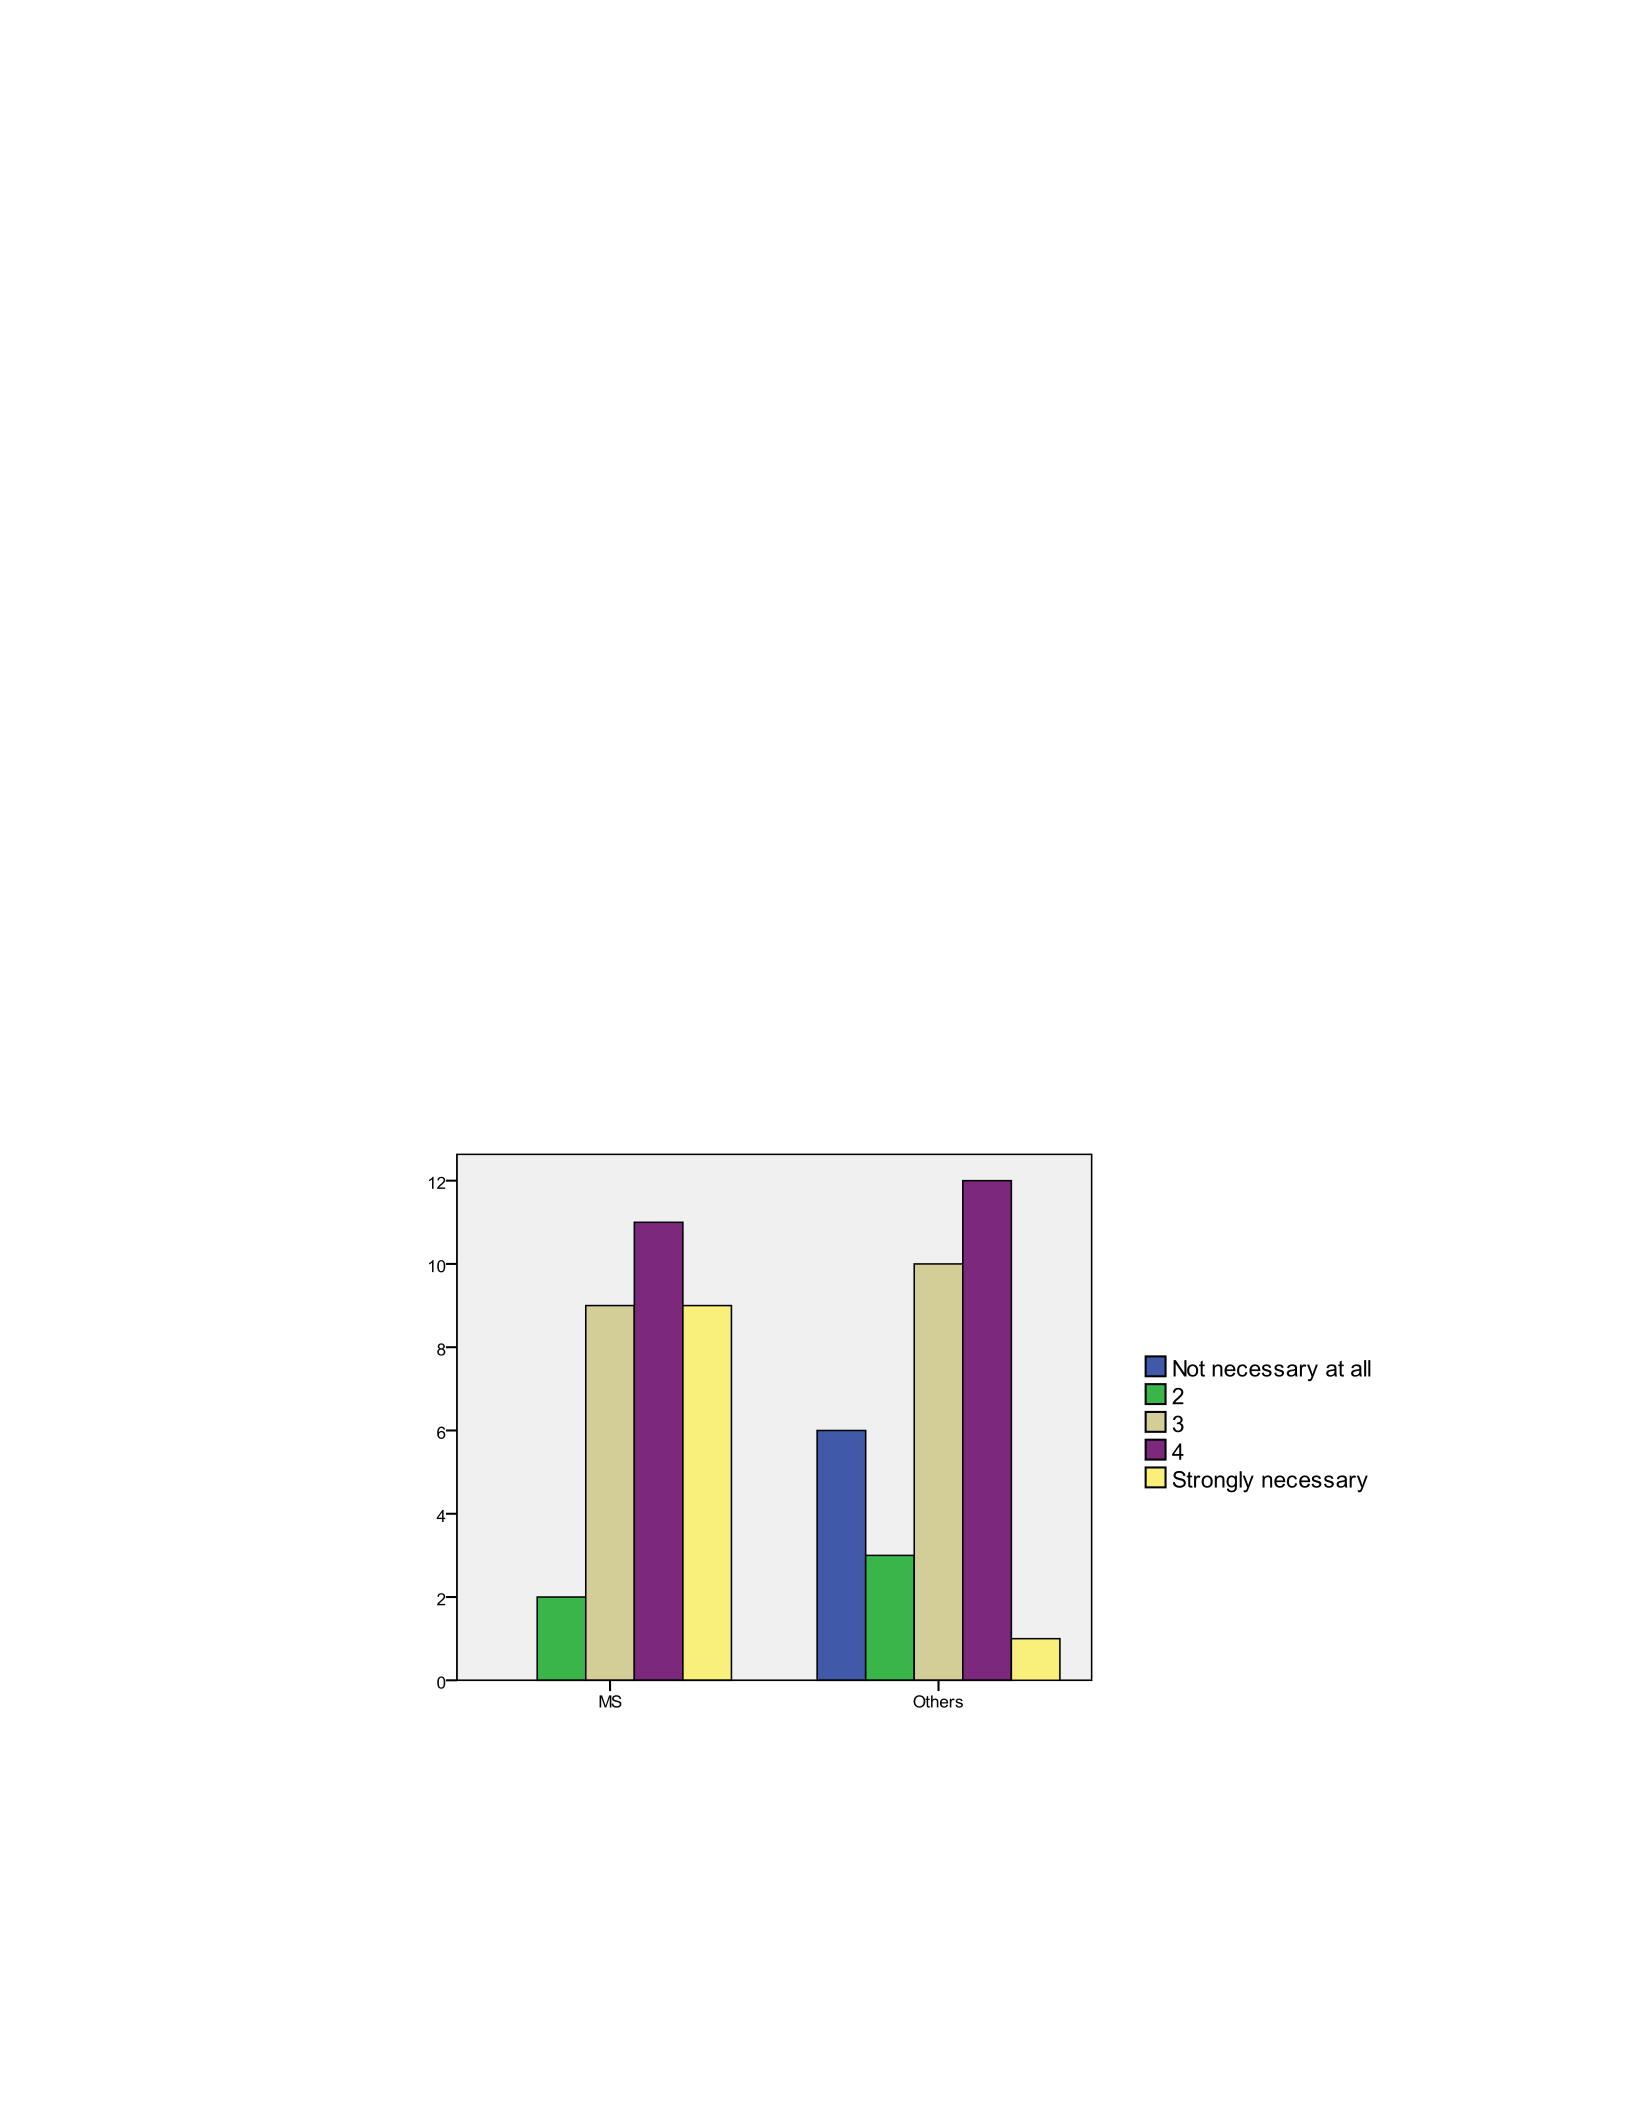
101
(30.2%) or positive stance (52.4%) toward the necessity of employee training. Training
employees can help to (1) obtain the ability to identify HF/E problems, (2) report
problems early so that they can be solved before they become chronic and costly, (3)
increase employee awareness, and (4) have the employees equipped with the tools
necessary for problem solving (AFMA and NCDOL 2003). Managers from Mississippi
(Figure 40) working in the Household furniture subsector (Figure 41) believed that
training employees was necessary while managers from other states working in other
furniture related subsectors believed the opposite way. Their significant levels of
relationships were 0.013 and 0.001, respectively. The relationship between managers’
experiences and the thinking of the necessity of a team or department for HF/E problems
was significant as well (0.046). Managers with over 10 years experience took a neutral
stance toward the necessity of training employees for HF/E interventions (Figure 42).
Figure 40 Mississippi vs. other states concerning the necessity of training workers
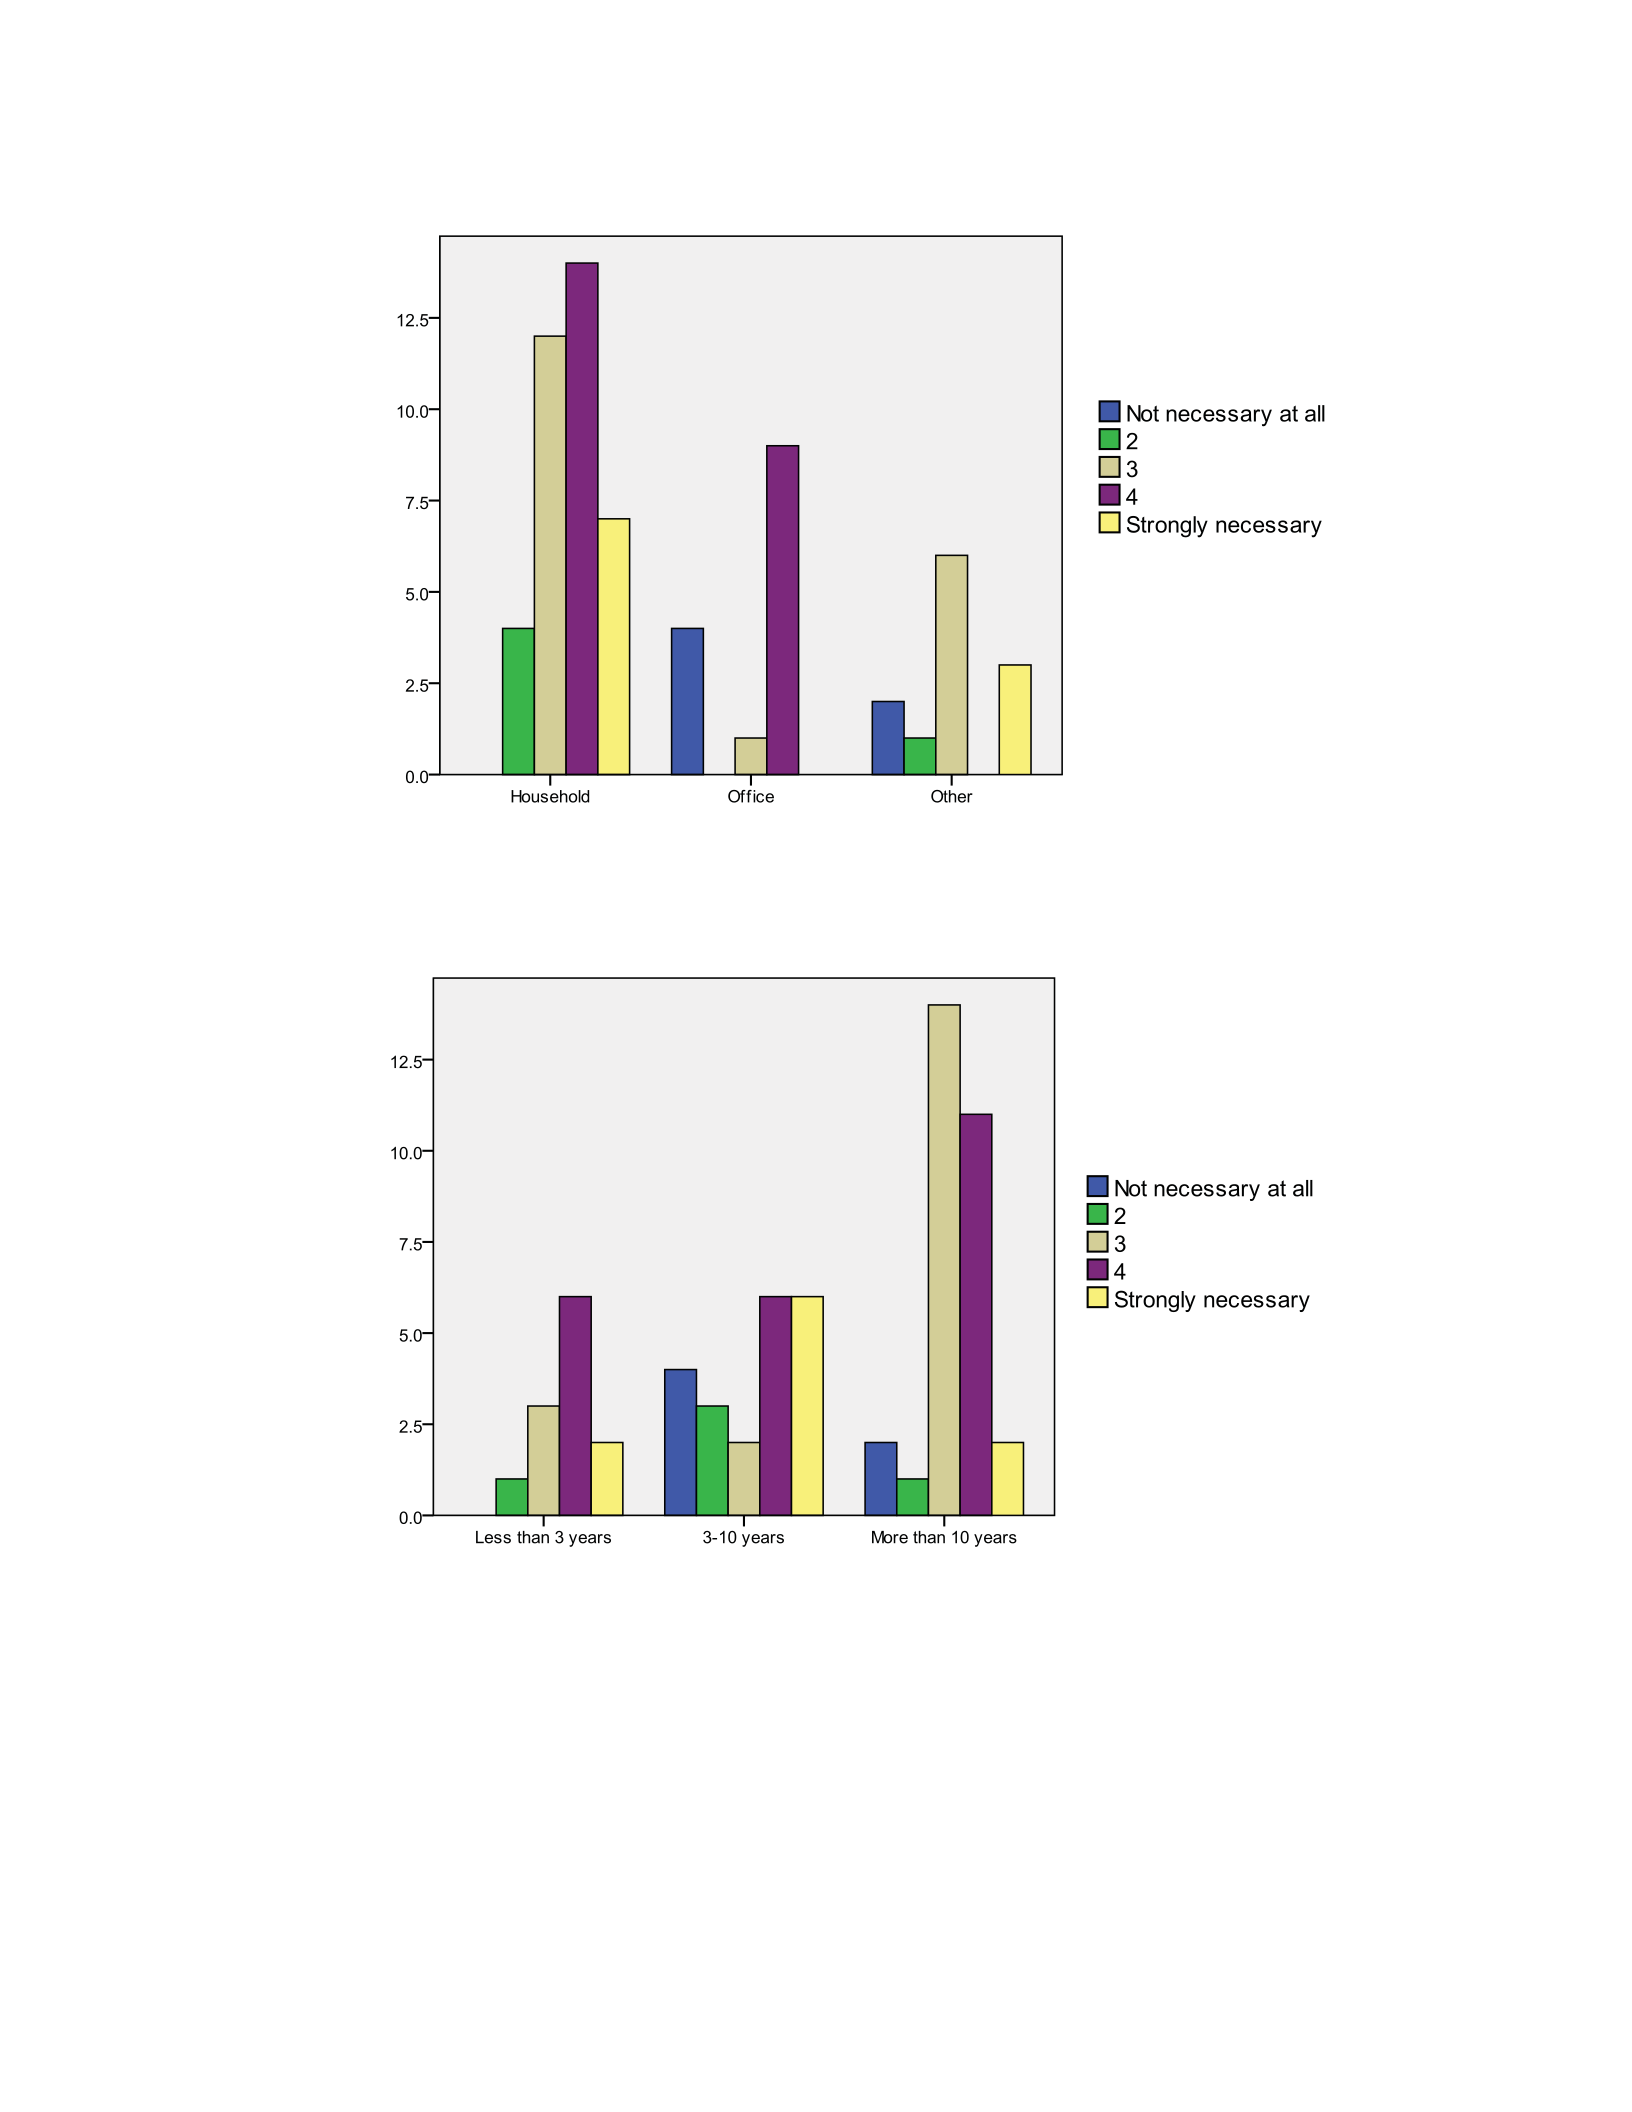
102
Figure 41 Sector and its affect on the necessity of training workers
Figure 42 Managers’ experience in their current position and its affect on the necessity of
training workers
Likewise, training managers for HF/E was, in general, believed to be necessary
(51.1%). Management training can provide better understanding of how problems
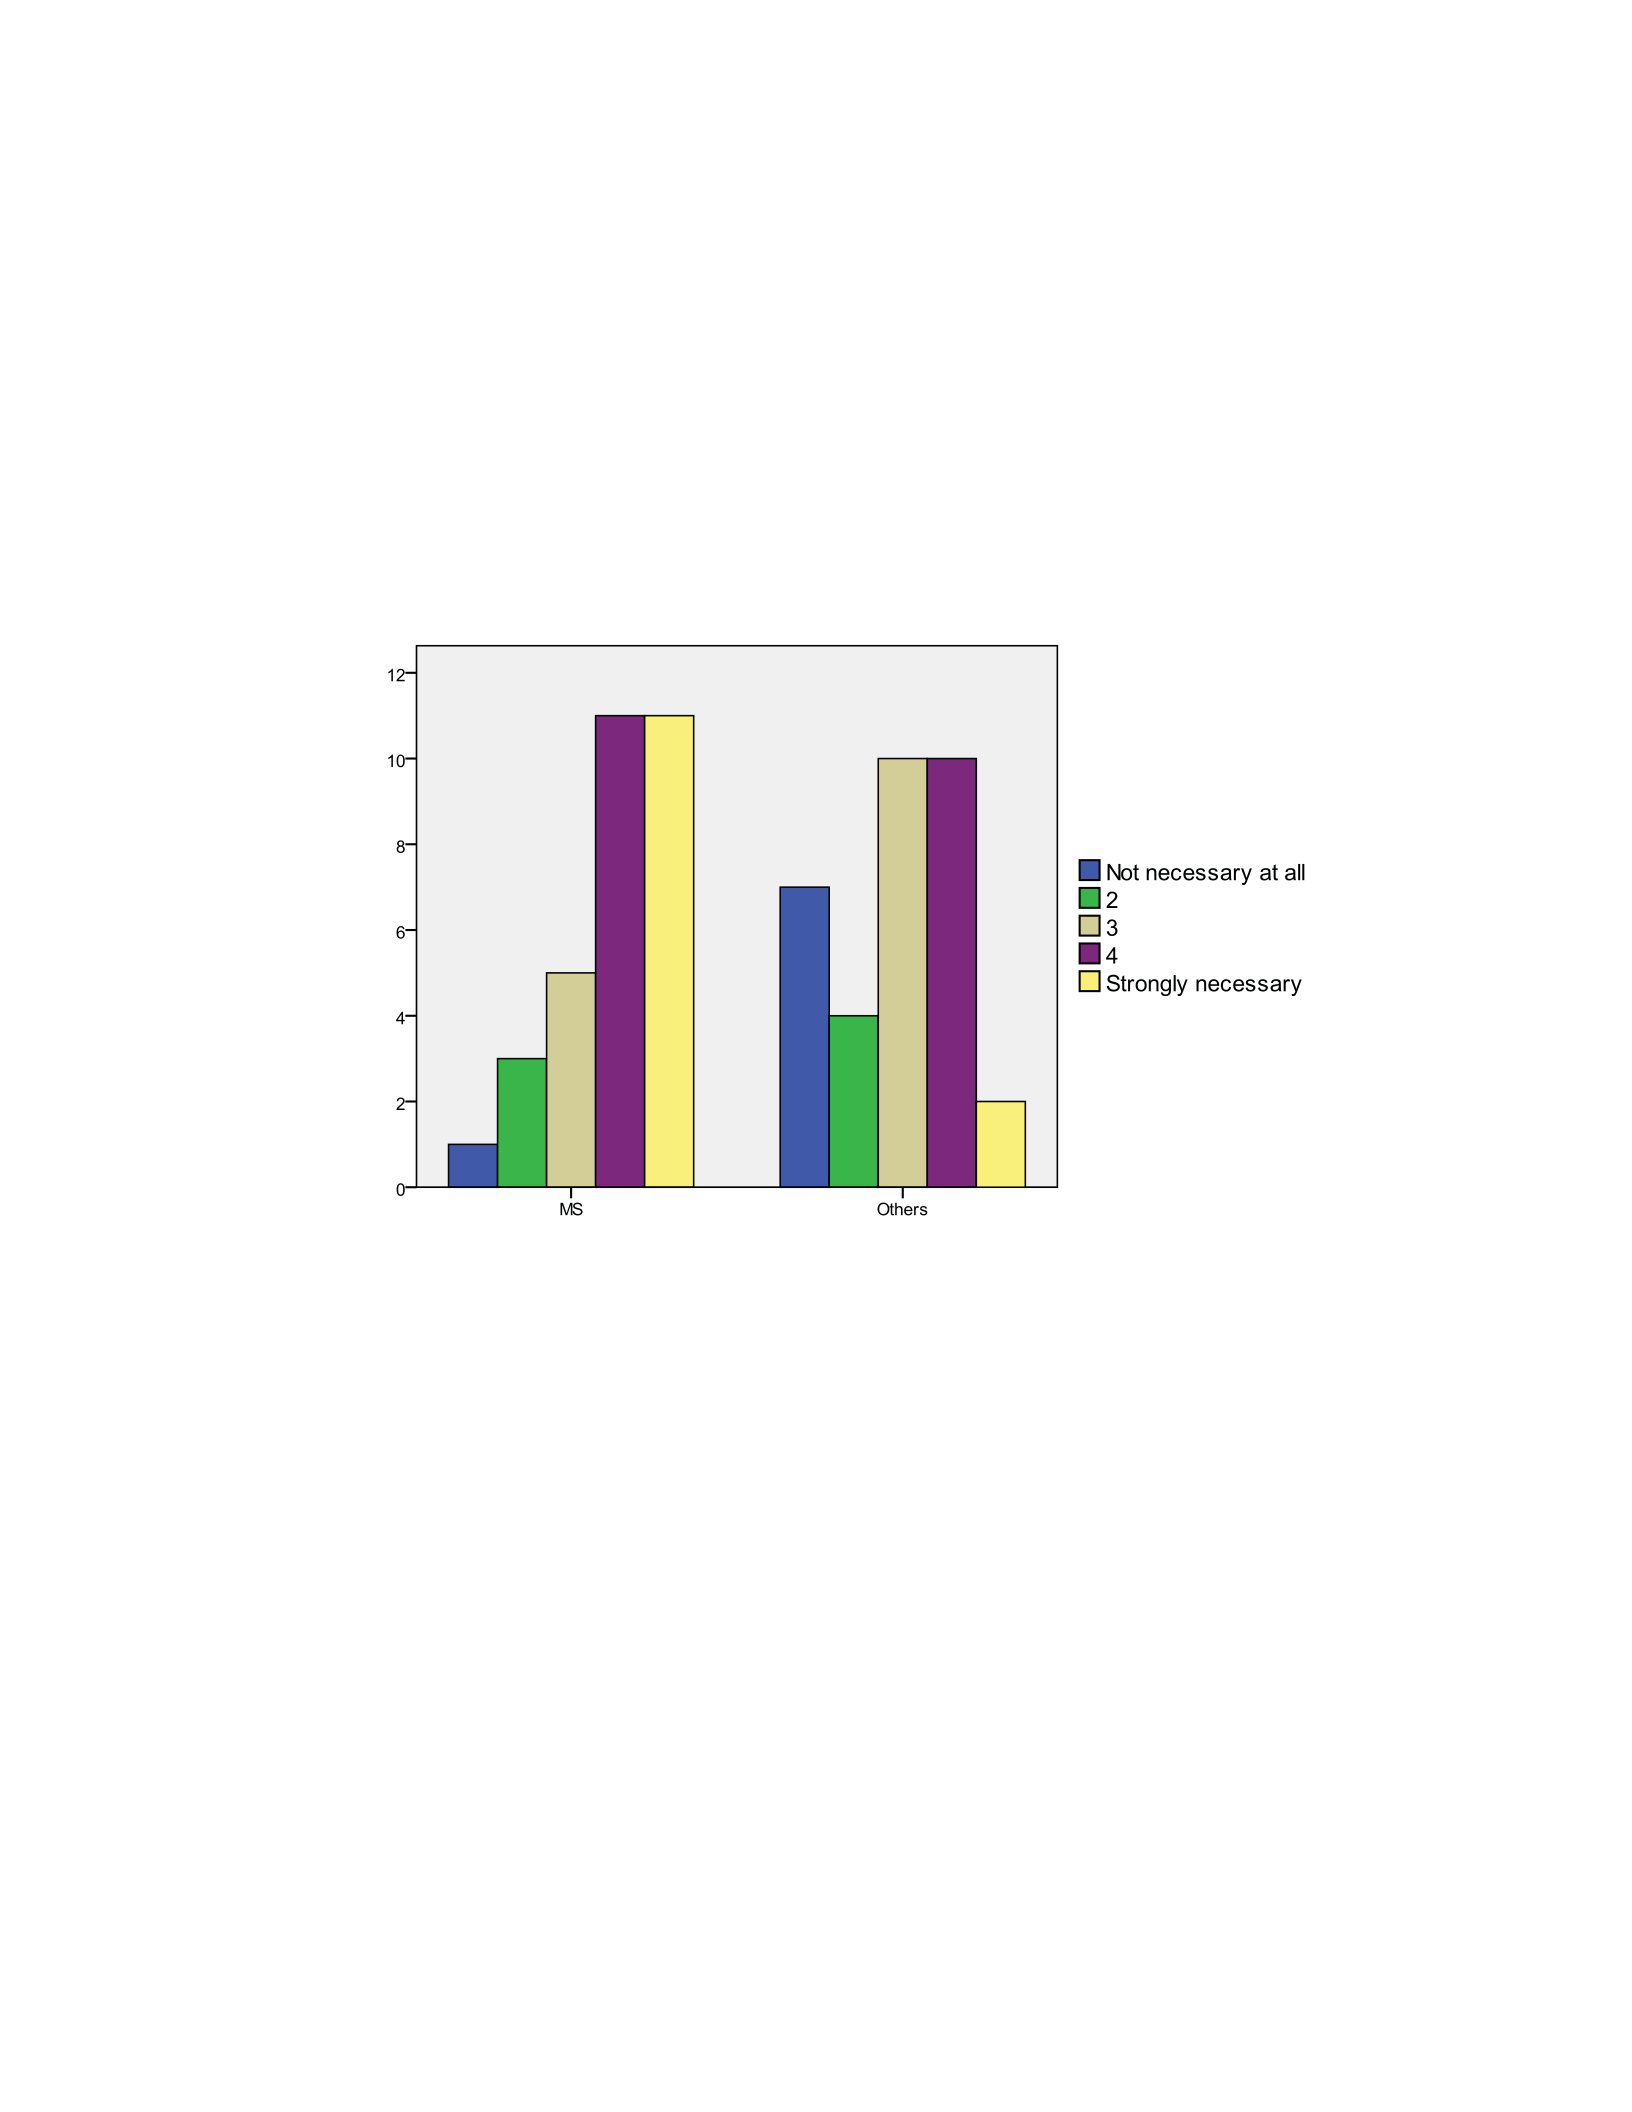
103
develop, how problems can be avoided, and solidification of management’s commitment
to the ergonomics process (AFMA and NCDOL 2003). Only 23.4 percent of managers
believed training was not necessary for them. The results of statistic analysis showed that
Mississippi furniture manufacturer managers took a positive stance toward training for
themselves (p )LJXUH
Figure 43 Mississippi vs. other states concerning the necessity of training managers
Lastly, managers were asked to rate the level of necessity of resources for HF/E
issues. The mean of the respondents’ scores for the necessity of resources for HF/E was
3.27.
Managers’ Opinions on the Likely Causes of Occupational
Injuries, Accidents, and Illnesses
Before being given the results of this survey, providing a comprehensive literature
review can support broad perspective occupational risk factors in the furniture

104
manufacturing industry. Physical factors such as cold, heat, lighting, and noise in
manufacturing work environments can directly influence worker comfort, efficiency, and
productivity, while increasing the risk of injuries and illnesses. However, research and
surveys generally have not been conducted considering the dimension of psychological
and social factors. The result of a survey with a high number of Sweden participants
suggests that psychosocial dimension of the work environment should be given greater
attention (Andersson 2008). The National Institute of Occupational Safety and Health
(NIOSH) revealed that psychosocial factors are as important as physical factors at
workplaces (Rooney et al. 1993). However, here, literature will be provided with stress
resources and types of injuries and illnesses rather than separating them into whether they
are physical or physiological stressors.
Manager’s Opinions on the Risk Factors for Occupational Injuries
in the Furniture Manufacturing Industry
Environmental conditions such as noise, lighting, extreme temperatures, and
vibration in the furniture manufacturing industry have an impact on worker well-being.
Some research and investigations were performed to determine the quality of workplaces
and to determine occupational stressors, if there were any, in workplaces. Research in
Poland demonstrated that environmental conditions were stressful in the furniture
industry (Bielski et al. 1976). For example, the noise level at all locations exceeded 90
dB (A), which is OSHA’s current permissible exposure limit for workplace noise, code
29 CFR 1910.95 (OSHA Standards). Excessive noise exposure adversely affects
employees’ health. Temporary or permanent hearing loss, interference with

105
communication and performance, speech, audible warning signals, and other physical and
psychological effects such as fatigue, irritability, muscle tension, increased blood
pressure, ulcers, stress, and anxiety are some effects of excessive noise exposure (Keller
2008). Gradual hearing loss occurs when an individual is exposed to intense noise
repeatedly and for a long time. To control noise in workplaces, engineering controls
(replacement or isolation of the source of noise, increasing the distance from the noise,
and sound swallowing ceilings) and administrative and work practice controls (reducing
the exposure time, shift employees, and providing personal protective equipment) should
be made available if the solution is effective, practical, and affordable (Keller 2008). The
same Polish research also found that lighting in the furniture facilities was inadequate
(Bielski et al. 1976).
Another environmental condition that seriously affects workers safety,
productivity, and efficiency is extreme temperatures. Hot workplaces can cause
heatstroke, sunstroke, heat exhaustion, harmful heat stress related illnesses, increased
possibility of injuries, and decreased productivity (Beevis and Slade 2003; Keller 2008;
BLS 2008). Furniture manufacturer workers, particularly ones close to heat radiating
machines, will be exposed to high temperatures. The other extreme temperature is cold,
but cold conditions are not commonly found in the furniture manufacturing industry. It is
known that cold temperatures cause frequent accidents, skin burns and pains, tingling and
itching, snow blindness, freezing, and frostbite (Keller 2008; BLS 2008). Engineering
controls, good work practices, and managerial controls can prevent extreme temperature

106
stresses. The simple intervention for workplaces in extreme temperatures is either to wear
proper clothes or acclimatize the workplaces.
Another occupational risk factor in the furniture manufacturing industry is
vibration caused from moving vehicles, machinery, and hand-held power tools. As a
result of the excessive exposure to vibration, vascular, neurological, and musculoskeletal
disorders are widely experienced among workers. For example, the prevalence of soft-
tissue disorders in the upper limbs is significantly greater among furniture manufacturer
workers than among the rest of the population (Bovenzi et al. 2005). Severe vibration
exposure causes a variety of adversely effects such as discomfort, chest pain, abdominal
pain, increased pulse rate or respiratory rate, low back pain, Raynaud’s phenomena
(white fingers), and more. The effects depend on the body part exposed (whole-body or
segmental exposure), the characteristic of the vibration (magnitude, frequency, and
direction), and the duration of exposure. Control and prevention techniques have a
significant impact on reducing occupational risks in the furniture manufacturing
industries. For example, a research to evaluate and design an orbital sander showed a
reduction in risk factors when the sander was designed to reduce exposure to vibration
(Smith et al. 2000). Because sanders are widely used in the furniture manufacturing
industry, they should be taken into consideration to control and prevent hand-transmitted
vibration.
The task itself causes occupational injuries and illnesses. Exposure to repetitive
motions, forceful exertion, contact stresses, vibrations, or awkward postures over a period
of time results in musculoskeletal disorders (AFMA and NCDOL 2003; Keller 2008).

107
Musculoskeletal disorders (MSDs) can be called cumulative trauma disorders because
repeated mechanical stresses on a particular body result in microtraumas which develop
gradually over a period of time. Musculoskeletal disorders are related to injuries or
traumas that affect soft tissues of the body. Soft tissues of the body are muscles, nerves,
tendons, tendon sheaths, and ligaments of the upper extremities (hands, wrists, and
elbows) and lower extremities (hip, thigh, knee, and ankle), shoulders, necks, and upper
backs and lower backs (waists) (Guo et al. 2004; Keller 2008).
The most common occupational MSDs are tendon disorders (tendonitis,
tenosynovitis, bursitis, DeQuervain’s disease, trigger finger, tennis elbow, golfer’s elbow,
rotator cuff injuries, and ganglionic cysts), nerve disorders (carpal tunnel syndrome), and
neurovascular disorders (Raynaud’s syndrome or white finger). Musculoskeletal
disorders alone are the most expensive work-related health problem (Leigh et al. 1997).
According to the Swedish Union for technical and clerical employees and the salaried
employees’ union, over half of the members of these unions were suffering from pain in
backs, necks, shoulders, and joints (Andersson 2008). The furniture industry is one of the
industries that is at risk in terms of occupational injuries (Christensen et al. 1995;
Paskiewicz and Fathallah 2003; Bovenzi et al. 2005; Ferguson et al. 2008). After
conducting a country wide survey in Taiwan with a total of 18,942 participants, Guo et
al. (2004) indicated that furniture industries and fixture manufacturing and wood and
bamboo products were in the group of industries with high prevalence of musculoskeletal
type injuries. Ergonomics is an effective approach to reducing the number and severity of
MSDs. Ergonomics programs, when all levels and functions are involved in their

108
implementation, can be very effective in reducing MSDs (AFMA and NCDOL 2003).
Some possible effective control and prevention techniques for the reduction of MSDs
among workers in the furniture manufacturing industry are to eliminate or reduce:
xexcessive or repetitive bending, twisting, and reaching,
xpulling, pushing, lifting, holding, and carrying too heavy and too large loads,
xawkward, poor, and static postures,
xvibrations, and
xpoor environmental conditions (cold temperature, etc.).
Managers’ Opinions on the Risk Factors for Occupational Illnesses
in the Furniture Manufacturing Industry
Air contaminants are occupational illness risk factors for the furniture
manufacturing workers. Airborne contaminants such as dusts, gases, fumes, hazardous
biological agents, and vapors can be taken into the body by inhalation, which may result
in occupational illnesses if they exceed the permissible exposure limits (Keller 2008).
After investigation case reports and epidemiological studies related to the furniture and
cabinet making industries, the International Agency for Research on Cancer (IARC)
indicated “Furniture and cabinet-making are carcinogenic to human” (IARC 1987).
Exposure to dusts, particularly wood dusts, is fairly excessive in the furniture
manufacturing industry, which generates occupational health risks for workers (Scheeper
et al. 1995; Schlunssen et al. 2001; Vinzents et al. 2001; Mikkelsen et al. 2002;
Kauppinen et al. 2006; Kalliny et al. 2008; Scarselli et al. 2008).
There are several epidemiological studies which indicate that some hardwoods
such as oak, beech, birch, elm, ash, walnut, and mahogany are associated with cancer
risk, generally nasal cancer risk (Scarselli et al. 2008). However, this association is still

109
controversial among scientists because many researchers have failed to find this
association. For example, a study was conducted by Rang and Acheson (1981) with 5,371
workers worked in furniture factories in Buckinghamshire, UK, so as to determine the
incidence of cancer and the mortality from cancer. Researchers found a significant
relationship between the incidence of the tumor nasal adenocarcinoma and the high
exposure to wood dust: the incidence of tumors among workers in the furniture industry
was about one hundred times higher than the incidence of tumors among the local
population. However, the same relationship between wood dust exposure and the
incidence of other cancer types including bronchial cancer was not significant (Rang and
Acheson 1981). Another research in 25 European Union member countries showed that
about 3.6 million workers (700,000 workers in the furniture industry) were exposed to
wood dust in their workplaces in 2001-2002 (Kauppinen et al. 2006). This number is two
percent of the total employees in these 25 countries. Thus, the furniture industry is,
unfortunately, one of the highest exposure level industries in which most factories may
exceed the recommended exposure limit (Kauppinen et al. 2006). As mentioned before,
even though woodworking is considered as associated with cancer, there is no strong
evidence to show a relationship between the exposure to wood dust and respiratory health
effects among furniture workers (Goldsmith and Shy 1988).
The type of work activity determines the dust content in the environment. For
example, the sanding process and surface cleaning are the most dust producing tasks
(Scheeper et al. 1995). However, all employees, not just those responsible for sanding,
are exposed the high amount of wood dust (Scheeper et al. 1995). Employees in sawing

110
and milling departments can be considered to be exposed in intermediate level wood dust
(Kalliny et al. 2008).
In addition to the task type, worker sensitivity is important for evaluation. Some
workers can be sensitive to some specific woods. For instance, a Danish research found
that some workers in the furniture industry were sensitized against pine wood dust
(Skovsted et al. 2003).
Besides wood dust, there are some other stressors for occupational illnesses in the
furniture manufacturing industry. Breathing biological agents, chemicals, gases, vapors
from organic solvents, or fumes is one of the common stressors in the furniture
manufacturing workplaces. Resins and varnishes are highly used in the furniture industry.
Because of the chemical structure of resins and varnishes, they can cause occupational
illnesses. Adhesives or resins such as melamine-formaldehyde resins (Aalto-Korte et al.
2003) and epoxy resins (Rademaker 2000) have been studied to determine the significant
relationship between the exposure to adhesives and the prevalence of occupational
illnesses. After the exposure to a glue containing 1-bromopropane, employees had severe
illness symptoms and abnormal findings like high urinary arsenic concentrations
(Raymond and Ford 2007). Formaldehyde, also highly used in the furniture industry, is
classified as probably carcinogenic to human beings (Gichner 1995). Research in Turkey
to determine the relationship of exposure to polyester resin (styrene monomer: a potential
carcinogen and mutagen) and genotoxic damage was performed on 53 employees in a
furniture manufacturing company, and the results emphasized the possibility of genotoxic
damage (Karakaya et al. 1997).

111
Another potential occupational risk factor for illnesses is carcinogenic solvents.
Research in Poland conducted by Posniak et al. (2005) found that the exposure to organic
solvents in the furniture manufacturing industry, particularly in the tasks of varnishing
and cleaning, was pretty high, even higher than normal limits, which can be harmful to
employees’ health. Methylene chloride, another type of solvent, is highly exposed to
employees stripping furniture (Estill and Spencer 1996). Acrylate varnishes, highly used
in the furniture manufacturing industry, make acute toxic skin reactions more severe
among exposed individuals (Voog and Jansson 1992). Pinter et al. (2003) conducted
research to determine the effect of the occupation on colorectal cancer, and they found no
evidence that occupational exposure to asbestos, EMF, formaldehyde, lead, or solvents
were associated with colorectal cancer risk.
Exposure to airborne contaminants in the furniture manufacturing workplace not
only results in cancers but also other illnesses. Sneezing and eye irritation (Goldsmith and
Shy 1988), skin problems (Surakka et al. 2001; Shao et al. 2001), poisoning, and
respiratory problems such as asthma (Balmes et al. 2003; Tomioka et al. 2006; Koh et al.
2008) can be significantly correlated with wood dust exposure.
Risk factors or stressors can be divided to two parts: occupational stressors and
organizational stressors. Occupational (also known as physical, traditional, or task
related) stressors are called micro stressors while organizational stressors are called
macro stressors.

112
1. Occupational (micro) stressors include, but are not limited to;
xForce (mechanical compression and shear forces) and moments
xAwkward and heavy loads (lifting and lowering heavy loads, tools, equipment)
xAwkward and static working body posture
xThe frequency and duration of exposure to stressors
oRepetition (repetitive tasks)
oOverexertion
xContact stress (soft tissue contact stressors)
xWorker related stressors
oFatigue
oStrength
oEndurance
oPrevious injury and illness history
xEnvironmental factors
oExtreme temperatures
oHumidity
oNoise
oLighting (glare, inadequate lighting, poor lighting)
oVibration (whole body and segmental vibration)
xChange itself
oChanges in workplaces (tasks, equipment, tools, scheduling)
oChanges in the environment

113
2. Organizational (macro) stressors include, but are not limited to;
xOrganizational limitations
oInsufficient financial resources
oStaff shortage
oPoor scheduling (excessive overtime, inadequate resting time, and faster
deadlines)
oLack of worker motivation
xInadequate or lack of proper personal protective equipment and clothing
xJob related stressors
oImproper management for job rotation, job enlargement, and job
enrichment
oAwkward work processing methods
xLack of individual and group trainings
xOrganization’s environment related external stressors
oTechnological changes in the industry
oPolitical and regulatory considerations (e.g., OSHA regulations)
oEconomic factors (e.g., global competition)
xOther social and psychosocial issues
The most reliable and desirable intervention method to avoid occupational
stressors is engineering design and controls. Engineers are responsible for adjusting the
work and the environment to the workers’ capabilities in order to arrange for a proper
match between demands and capabilities (Black and Hunter 2003; Goggins et al. 2008).
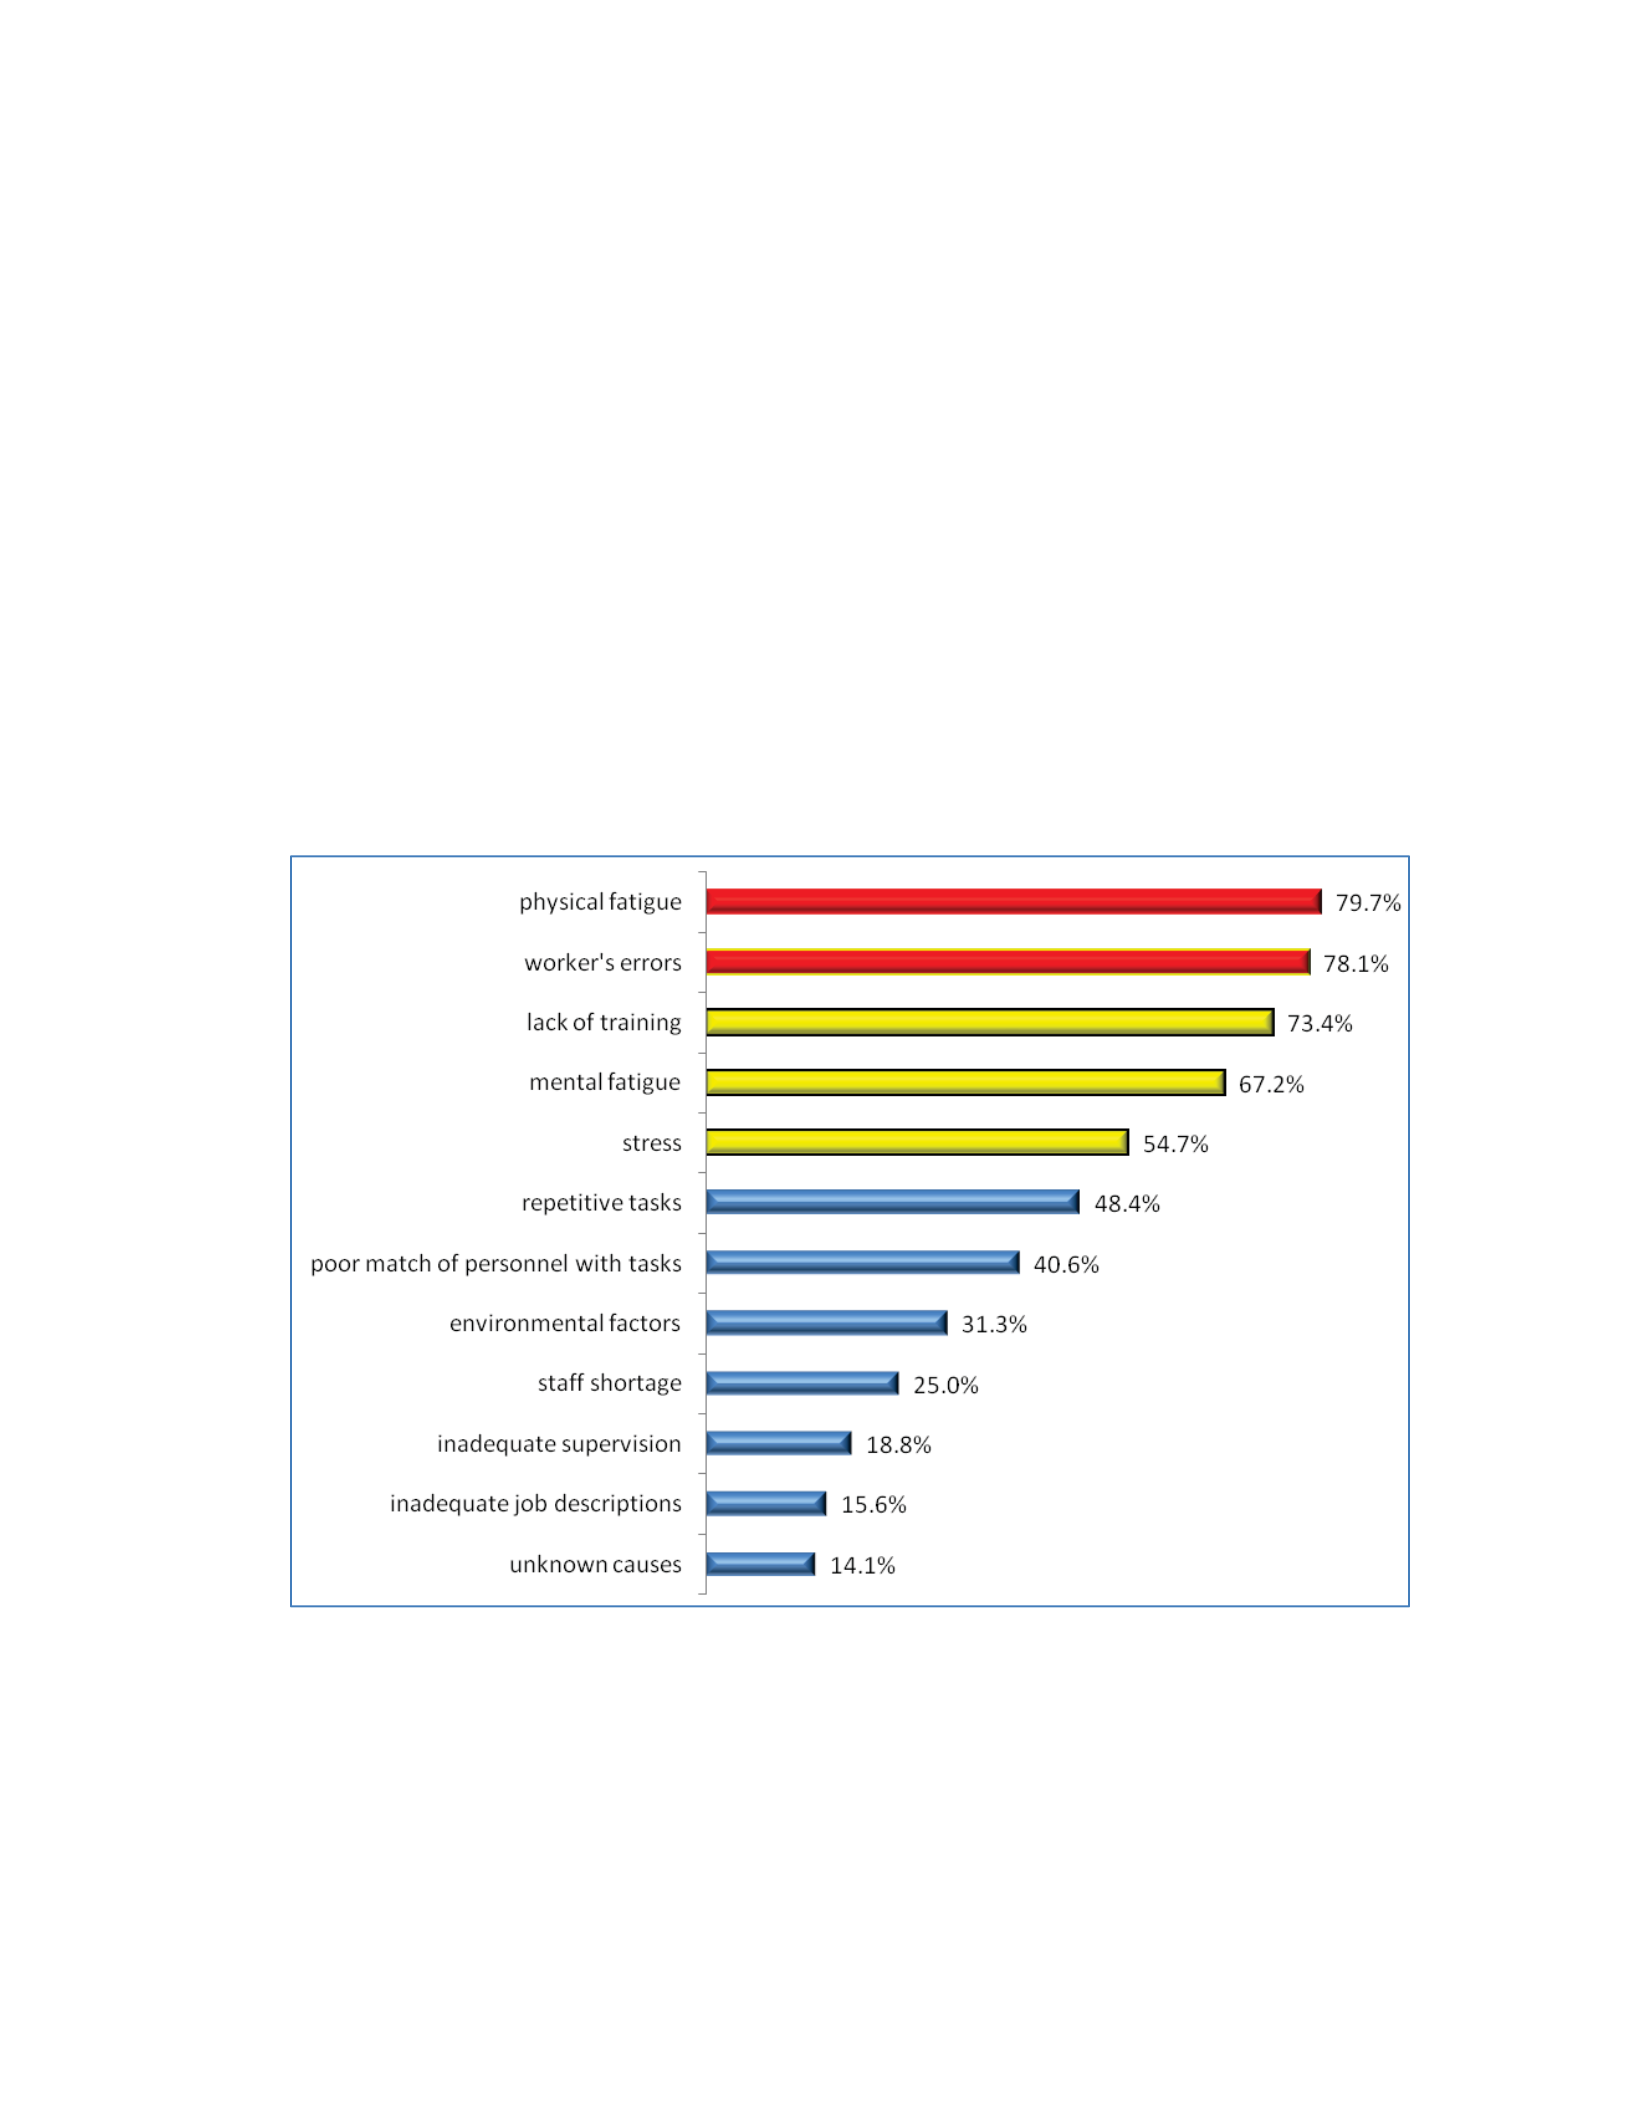
114
On the other hand, organizational stressors can be reduced by applying
administrative design and controls. For example, worker rotation, frequent rest breaks,
and training are some good administrative controls. Training alone can prevent even 20
percent of occupational injuries and illnesses (Oxenburgh 1991).
In the questionnaire, participants were asked about the likely causes of
occupational injuries, accidents, and illnesses in order to better understand the knowledge
and opinions of managers. Managers’ responses are given in Figure 44 from the highest
to the lowest percentages.
Figure 44 Managers’ opinions on the likely causes of occupational injuries, accidents,
and illnesses

115
Over seventy percent of managers replied that physical fatigue (79.7%) and
worker errors (78.1%) were the main causes of all occupational injuries, accidents, and
illnesses. Likewise, over half of the managers believed that occupational injuries,
accidents, and illnesses were caused from lack of training for the employees (73.4%),
mental fatigue (67.2%), and stress (54.7%). Other causes were expressed by less than half
of the managers.
Heavy and repetitive tasks, awkward or static body postures, vibration, contact
stress, and uncomfortable environments are common stress factors in the furniture
industry that can directly cause the worker be exhausted both physically and mentally and
can indirectly influence risk of occupational injuries and illnesses. One of the objectives
of this question was to address some stress factors in the American furniture
manufacturing industry regarding occupational safety and health issues.
There were some statistically significant relationships between managers’
demographic properties and their opinions about the possible causes of occupational
injuries, accidents, and illnesses (Table 24).
Of the managers from other states, 78. 8 percent significantly (p
expressed that mental fatigue caused occupational injuries and illnesses (Figure 45).
Managers with high school degrees believed (p WKDWVWUHVVZDVDULVNIDFWRU
while managers with graduate school degrees did not believe so (Figure 46). Managers
from Office Furniture (including Fixtures) Manufacturing and Other Furniture Related
Product Manufacturing subsectors replied (p WKDWUHSHWLWLYHWDVNVFDXVHG
occupational injuries and illnesses (Figure 47). None of managers with less than 3 years
116
Table 24 Statistical analysis of managers’ demographic properties and managers’
opinion about the possible causes of occupational injuries and illnesses
State Education NAICS Employees
Experience
in FI
Position
Experience in
P
Stress Ȥ20.229 6.301 5.126 1.120 1.428 3.573 3.023
P0.632 0.043* 0.077 0.571 0.490 0.168 0.221
Mental fatigue Ȥ24.159 0.738 4.740 0.975 1.320 8.782 0.398
P0.041* 0.691 0.093 0.614 0.517 0.012* 0.820
Physical fatigue Ȥ20.034 4.833 1.433 2.126 0.491 5.818 0.702
P0.854 0.089 0.489 0.345 0.782 0.055 0.704
Lack of training Ȥ21.601 0.122 1.818 2.341 1.540 2.634 5.392
P0.206 0.941 0.403 0.310 0.463 0.268 0.067
Repetitive task Ȥ22.231 2.168 6.454 3.613 2.120 0.517 2.825
P0.135 0.338 0.040* 0.164 0.346 0.772 0.244
Environmental factors Ȥ20.829 5.049 2.510 1.034 0.500 0.442 2.262
P0.362 0.080 0.285 0.596 0.779 0.802 0.323
Worker error Ȥ22.832 0.017 0.393 0.130 0.808 1.371 1.122
P0.092 0.992 0.821 0.937 0.668 0.504 0.571
Being understaffed Ȥ21.022 1.533 2.530 4.178 0.073 0.005 1.698
P0.312 0.465 0.282 0.124 0.964 0.997 0.428
Poor match Ȥ20.513 0.781 0.559 0.092 0.041 0.054 1.193
P0.474 0.677 0.756 0.955 0.980 0.973 0.551
Job description Ȥ20.634 2.117 0.079 1.801 6.348 0.554 6.455
P0.426 0.347 0.961 0.406 0.042* 0.758 0.040*
Supervision Ȥ20.014 3.186 2.357 1.130 3.000 2.436 1.593
P0.904 0.203 0.308 0.568 0.223 0.296 0.451
Unknown Ȥ20.067 1.899 0.829 2.123 2.745 1.506 1.670
P0.796 0.387 0.661 0.346 0.253 0.471 0.434
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value, p: p-value (The level of statistical significance).
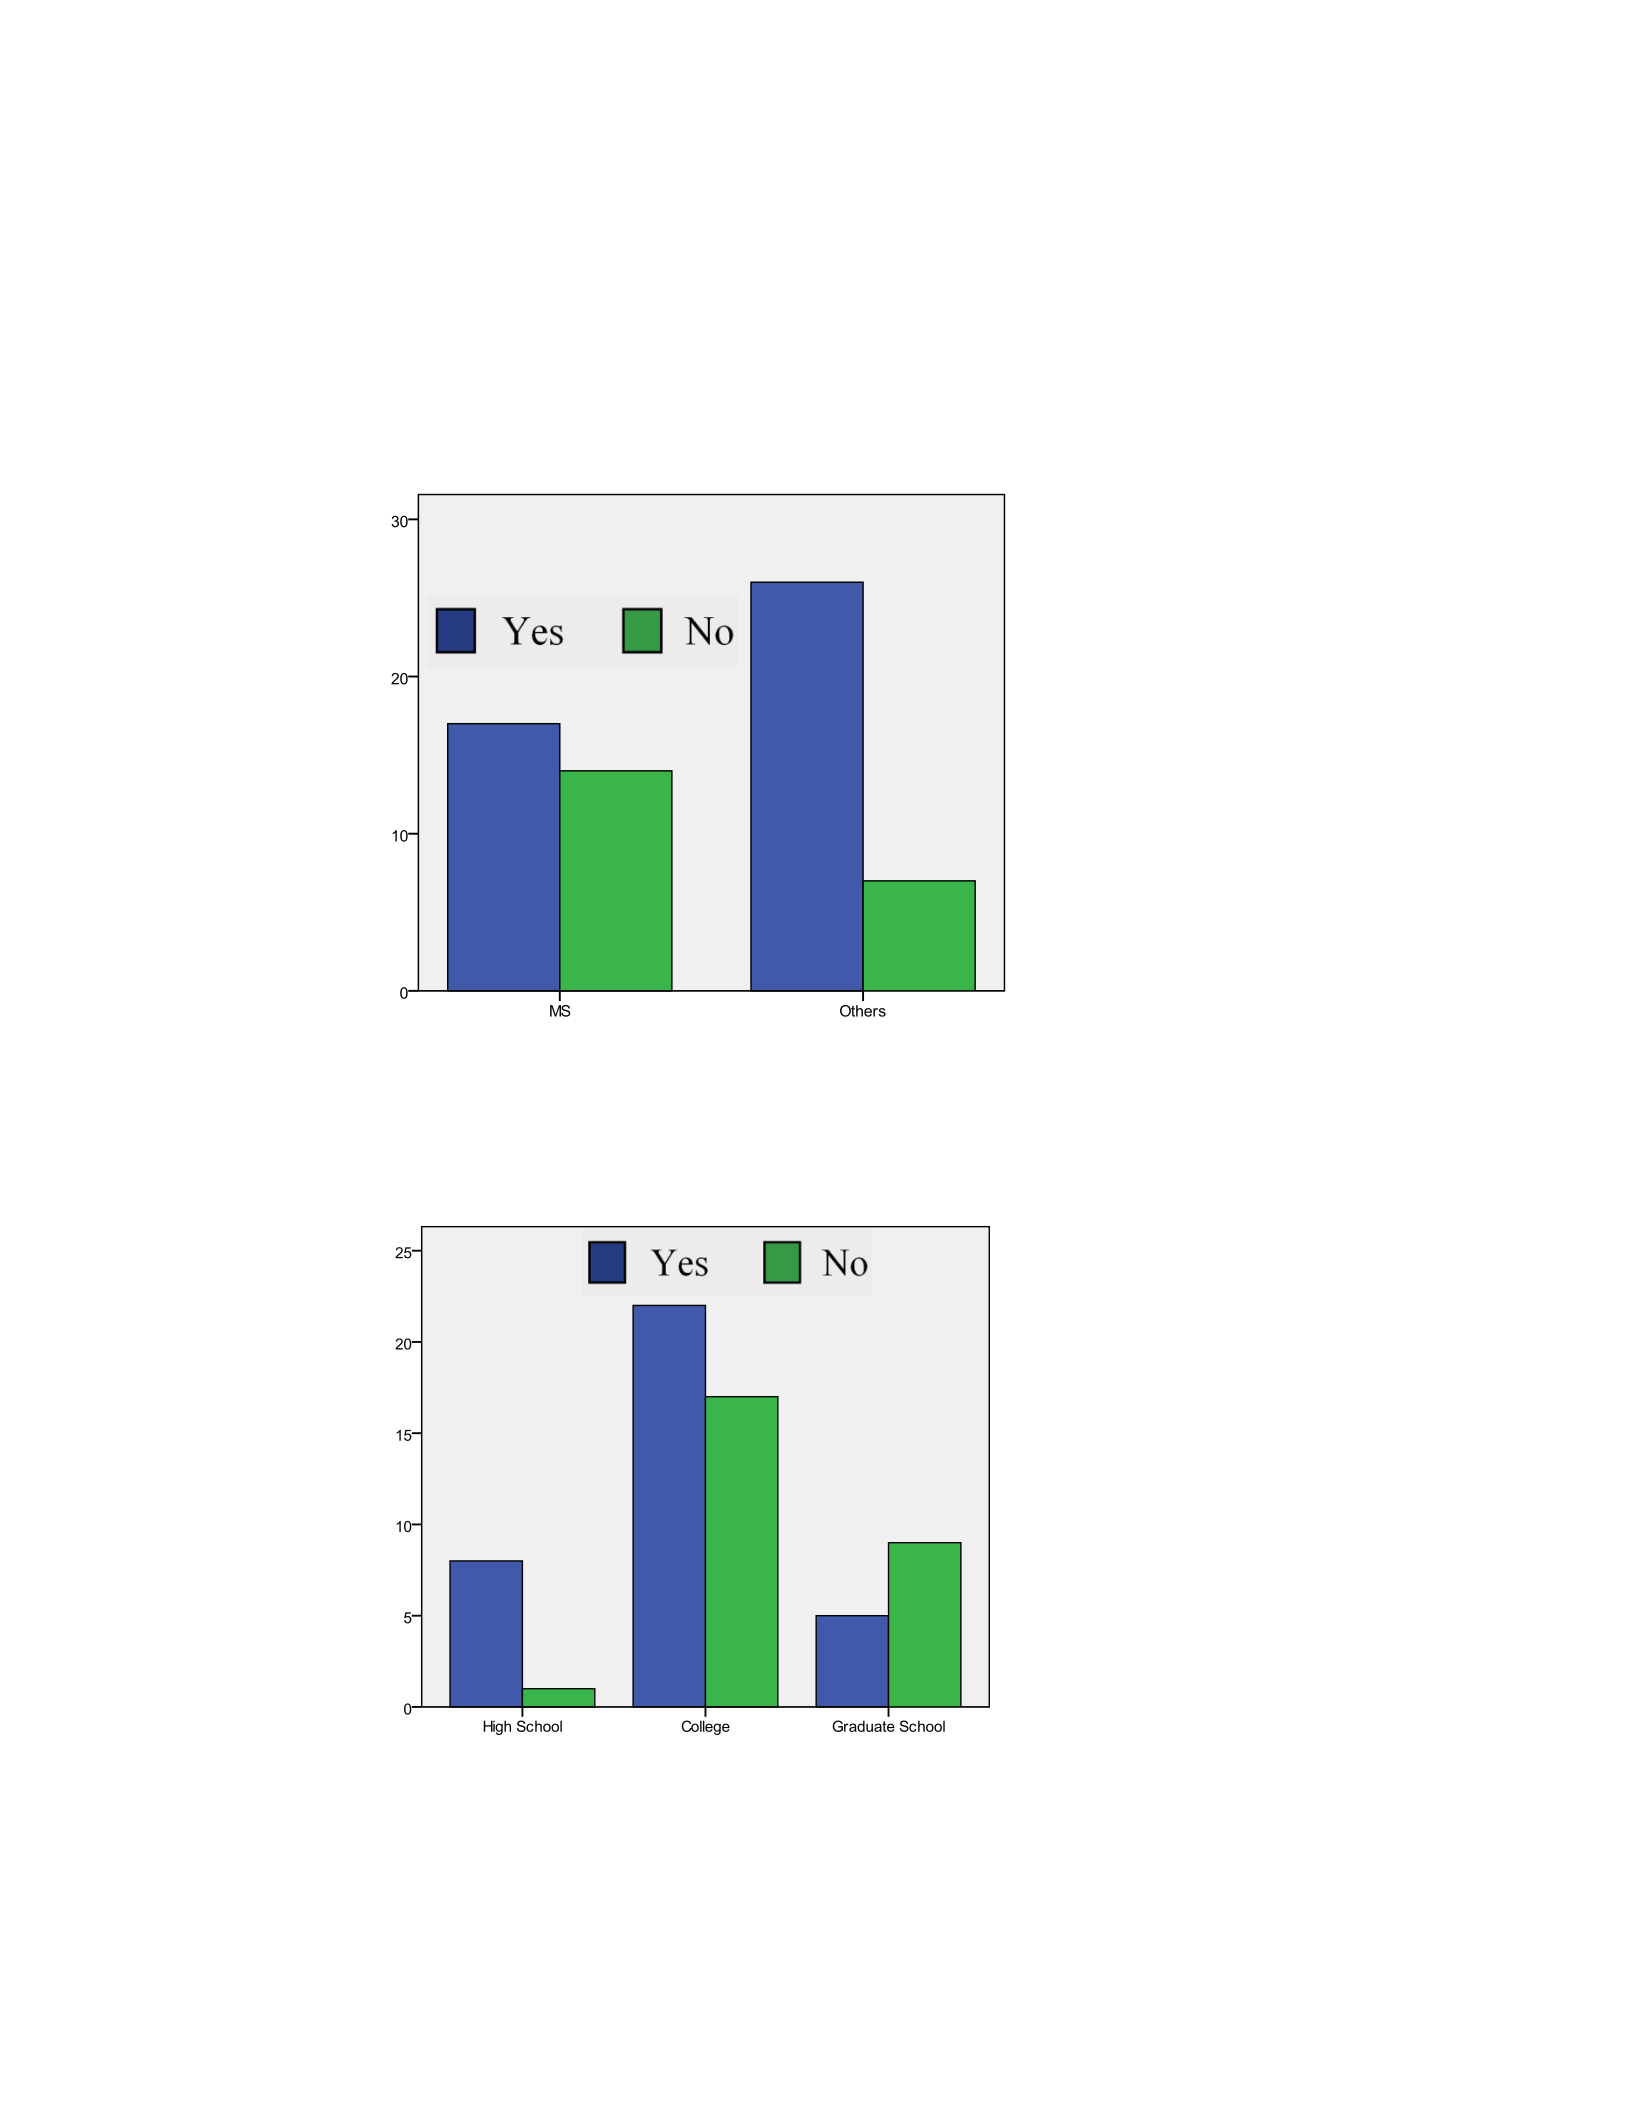
117
experience managers with 3-10 years experience in the furniture industry (p
(Figure 48) and in the current position (p )LJXUHWKRXJKWWKDWLQDGHTXDWHMRE
descriptions could cause occupational injuries and illnesses.
Figure 45 Mississippi vs. other states concerning managers’ opinions about likely causes
of mental fatigue
Figure 46 Manager’s education level, and its affect on their opinion about the likely
causes of stress
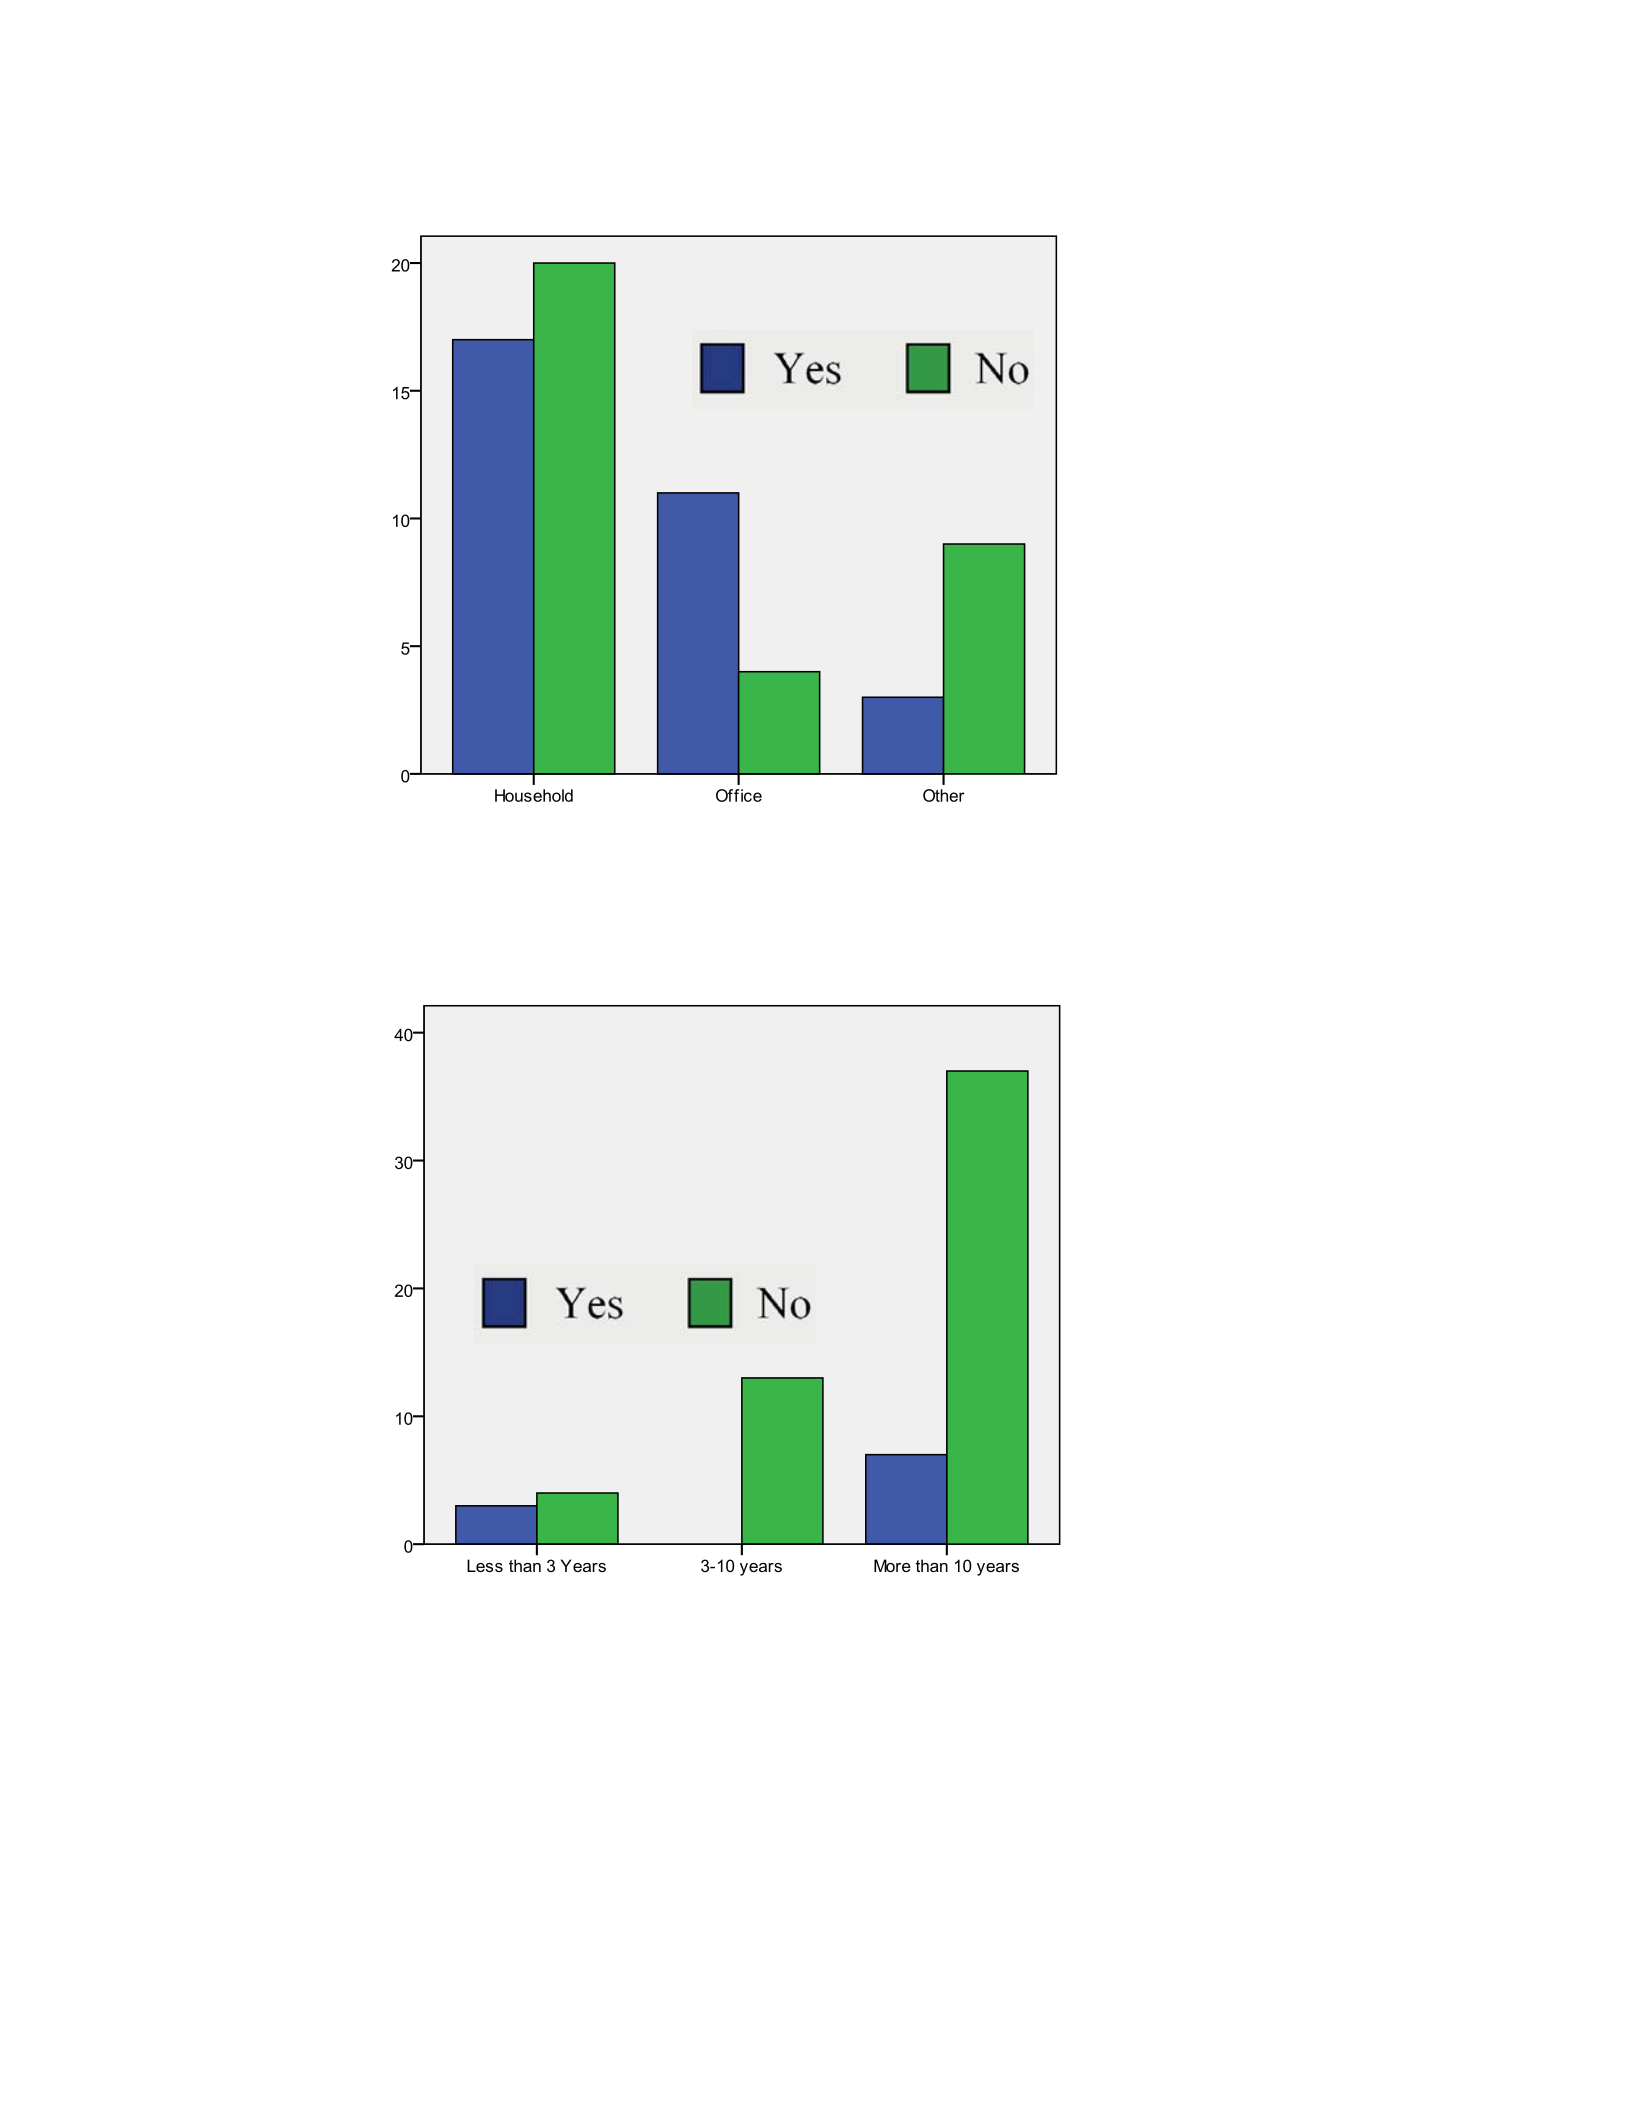
118
Figure 47 Sector and its affect on manager opinion about the likely
causes of repetitive tasks
Figure 48 Managers’ experience in the furniture industry and its affect
on their opinion about inadequate job description
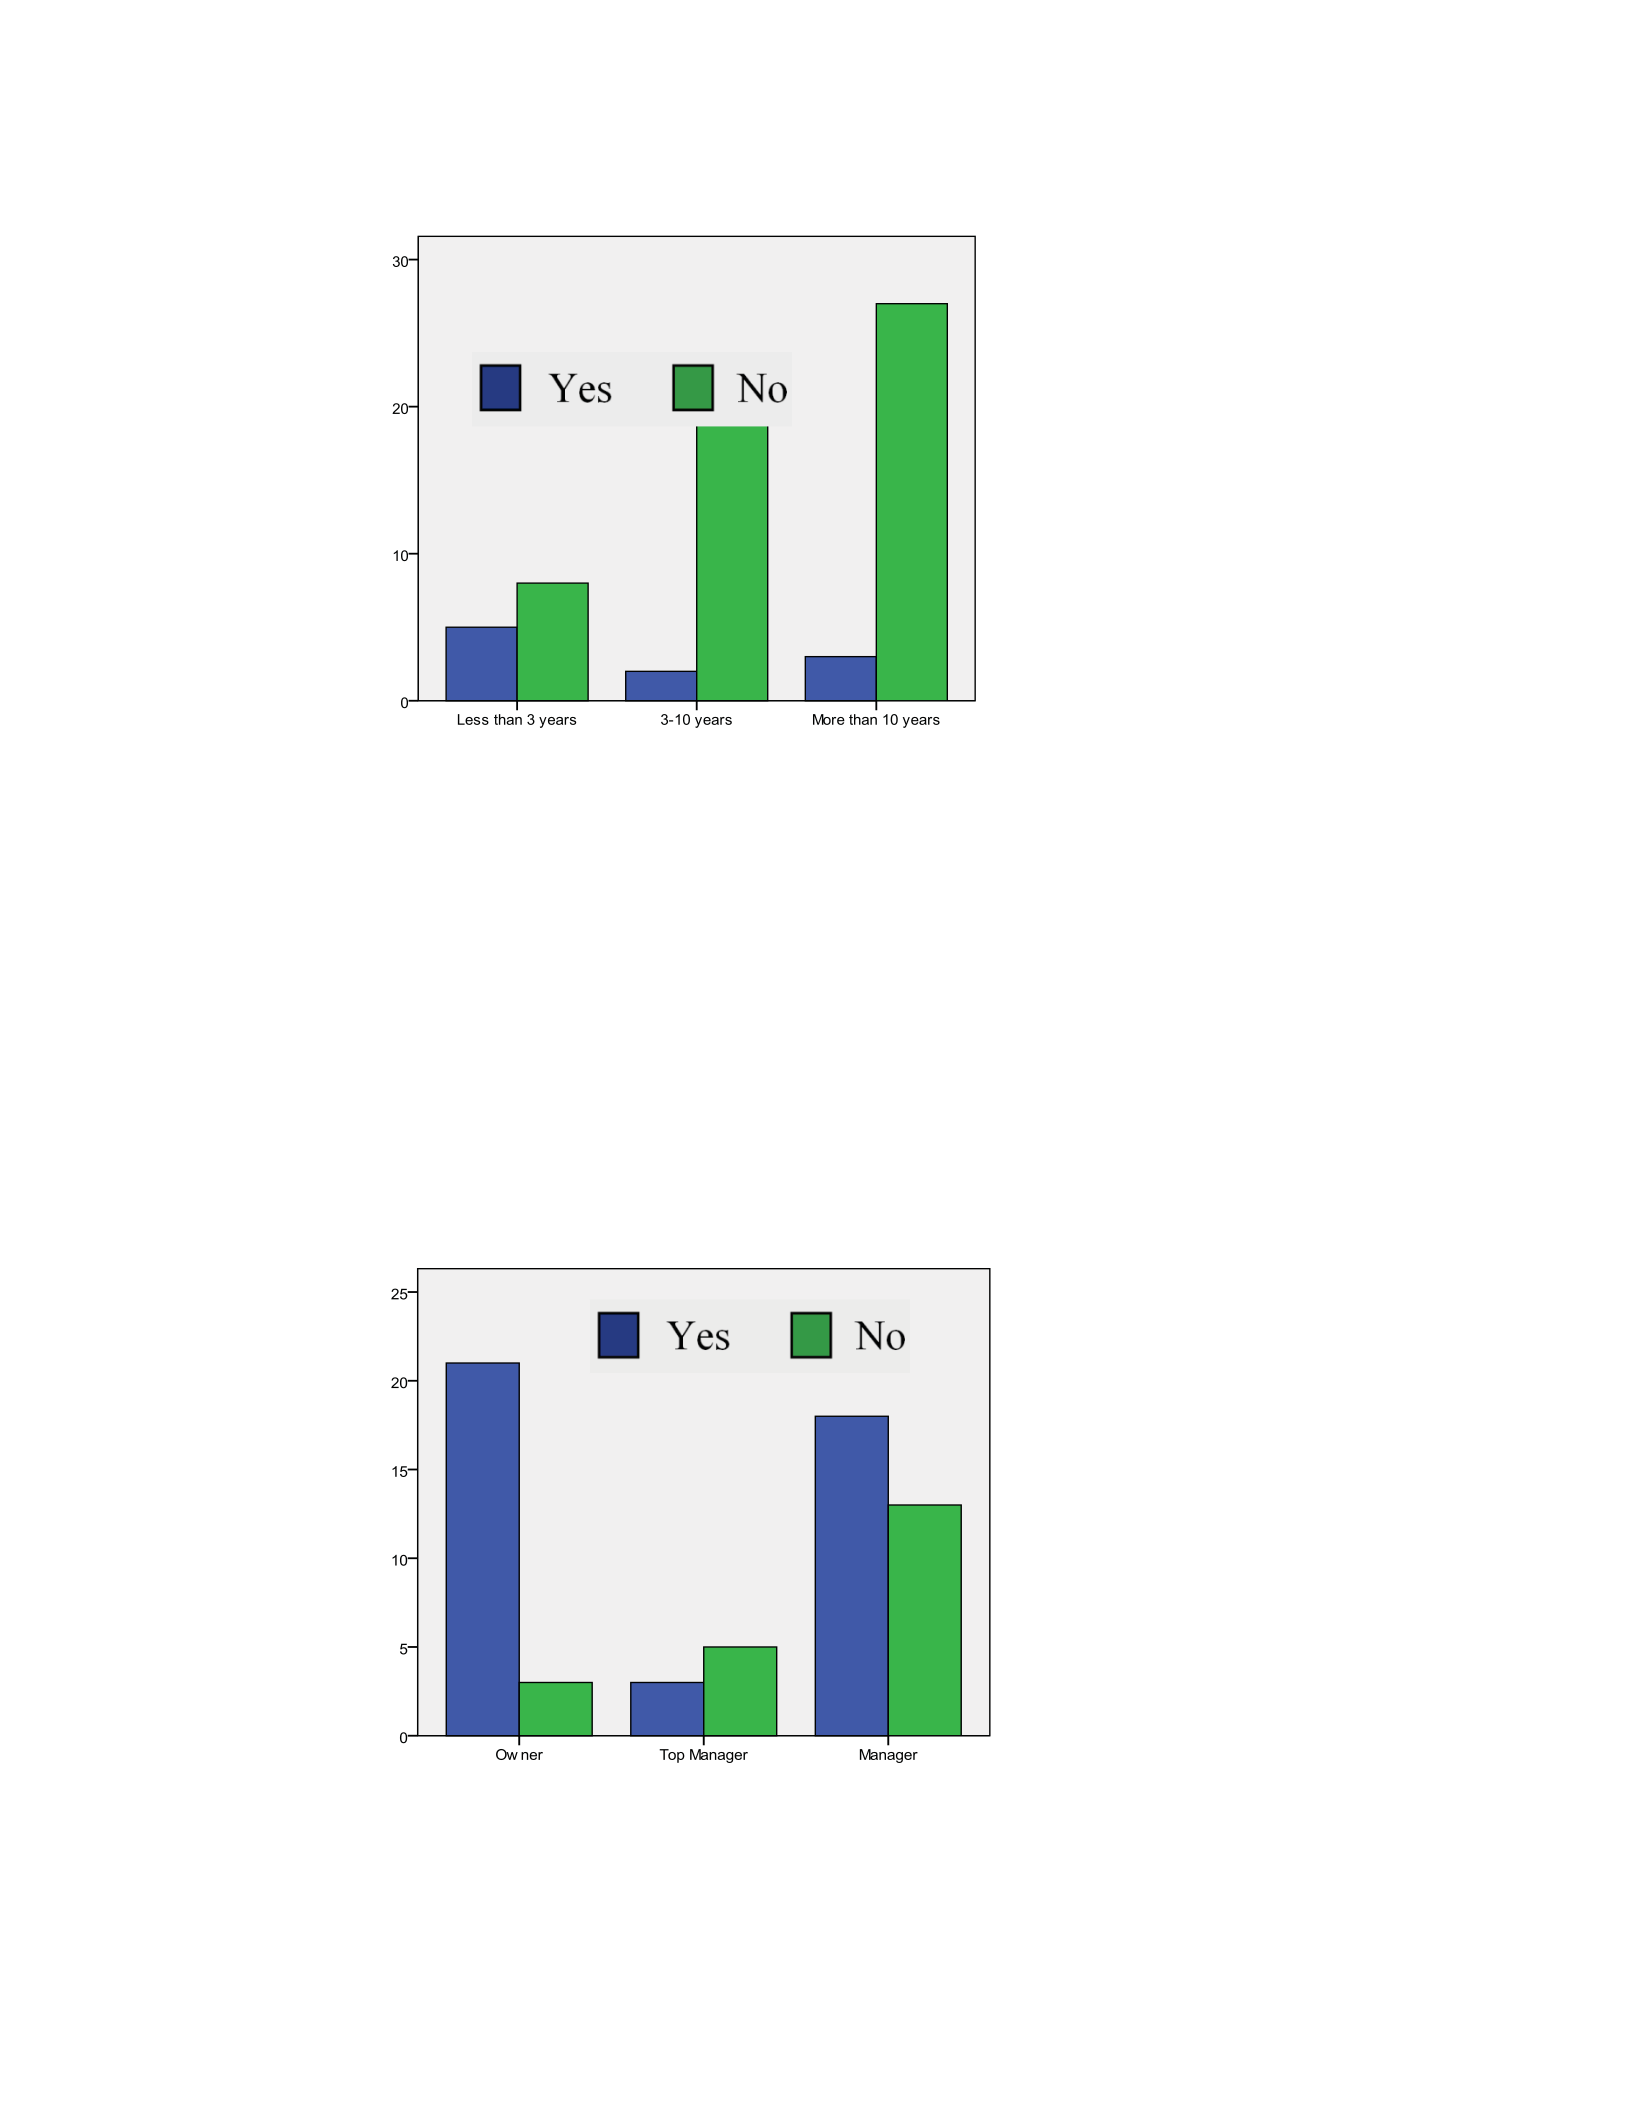
119
Figure 49 Experience in current position and its affect on their opinion about the likely
causes inadequate job description
The last significant relationship (p ZDVEHWZHHQWKHFXUUHQWSRVLWLRQDQG
the opinion that mental fatigue causes occupational injuries and illnesses. Owners
believed that mental fatigue was a risk factor for occupational injuries and illnesses while
lower-level managers did not believe so (Figure 50).
Figure 50 Managers’ position and its affect on their opinion about the likely causes of
mental fatigue

120
Managers’ Opinions about Responsibility Levels
Furniture manufacturer managers were asked to rate the level of responsibilities
for themselves, engineers, and employees in their companies, the company as a whole,
employees’ families, consumers of the company’s products, and the government. The
distribution of responses is given in Table 25.
Managers gave their company the highest responsibility and gave consumers the
least amount of responsibility. In addition to the company (3.05 rating average), lower-
level managers (2.98 rating average), workers (2.92 rating average), top-level managers
(2.89 rating average), and owners (2.73 rating average) were considered as responsible
for HF/E issues. Engineers (2.31 rating average), technicians (2.16 average rating), and
the government (2.05 rating average) were rated as somewhat responsible. Workers’
families (1.41 rating average) and consumers (1.34 rating average) were thought of as not
responsible for any HF/E related problems.
A few of the managers did not answer the responsibility level for workers’
families, consumers, and the government. It may be caused from not understanding the
interaction. They could not associate families, consumers, and the government with
responsibility. It may be considered that there is no responsibility of these people.
However, researchers did not combine the answers. The result of statistical analysis is
given in Table 26.
121
Table 25 Managers’ opinions about responsibility levels
Not
Responsible
Somewhat
Responsible Responsible Highly
Responsible Total
Score
Rating
Average
Total
Respond
(N) (%) (N) (%) (N) (%) (N) (%)
Company 2 3.2 12 19 30 47.6 19 30.2 192 3.05 63
Lower-level managers 2 3.2 14 22.2 30 47.6 17 27 188 2.98 63
Workers 3 4.8 13 20.6 33 52.4 14 22.2 184 2.92 63
Top-level managers 3 4.8 14 22.2 33 52.4 13 20.6 182 2.89 63
Owner 5 7.9 16 25.4 33 52.4 9 14.3 172 2.73 63
Engineer 14 22.6 23 37.1 17 27.4 8 12.9 143 2.31 62
Technician 15 24.2 26 41.9 17 27.4 4 6.5 134 2.16 62
Government 21 34.4 21 34.4 14 23 5 8.2 125 2.05 61
Worker's families 40 65.6 18 29.5 2 3.3 1 1.6 86 1.41 61
Consumers 43 70.5 16 26.2 1 1.6 1 1.6 82 1.34 61
Rating score: 1: Not responsible, 2: Somewhat responsible, 3: Responsible, 4: Highly responsible
122
Table 26 Statistical analysis of managers’ demographic properties and managers’
opinions about responsibilities
State Education NAICS Employees
Experience
in FI
Position
Experience in
P
Company Ȥ21.200 7.478 4.073 3.742 3.084 3.556 4.489
P0.753 0.279 0.667 0.712 0.798 0.737 0.611
Owner Ȥ20.923 8.616 6.170 2.637 5.656 2.247 8.745
P0.819 0.196 0.404 0.853 0.463 0.896 0.188
Top-level managers Ȥ21.930 9.920 2.502 1.873 6.067 7.615 9.388
P0.587 0.128 0.868 0.931 0.416 0.268 0.153
Lower-level managers Ȥ22.820 16.072 4.551 4.502 7.241 4.023 5.624
P0.420 0.013* 0.603 0.609 0.299 0.674 0.467
Engineer Ȥ22.441 11.780 4.329 2.673 4.103 3.152 1.236
P0.486 0.067 0.632 0.849 0.663 0.789 0.975
Technician Ȥ21.489 9.823 8.447 7.625 9.689 6.792 4.134
P0.685 0.132 0.207 0.267 0.138 0.340 0.659
Workers Ȥ27.482 3.549 6.020 9.754 4.685 7.569 2.833
P0.058 0.738 0.421 0.135 0.585 0.271 0.829
Family Ȥ22.960 4.506 5.523 5.948 7.915 6.574 3.732
P0.398 0.608 0.479 0.429 0.244 0.362 0.713
Consumers Ȥ22.440 5.480 6.285 8.072 5.598 4.827 4.358
P0.486 0.484 0.392 0.233 0.470 0.306 0.628
Government Ȥ21.580 6.302 4.413 5.019 3.703 7.688 5.581
P0.664 0.390 0.621 0.541 0.717 0.262 0.472
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p: p-value (The level of statistical significance).
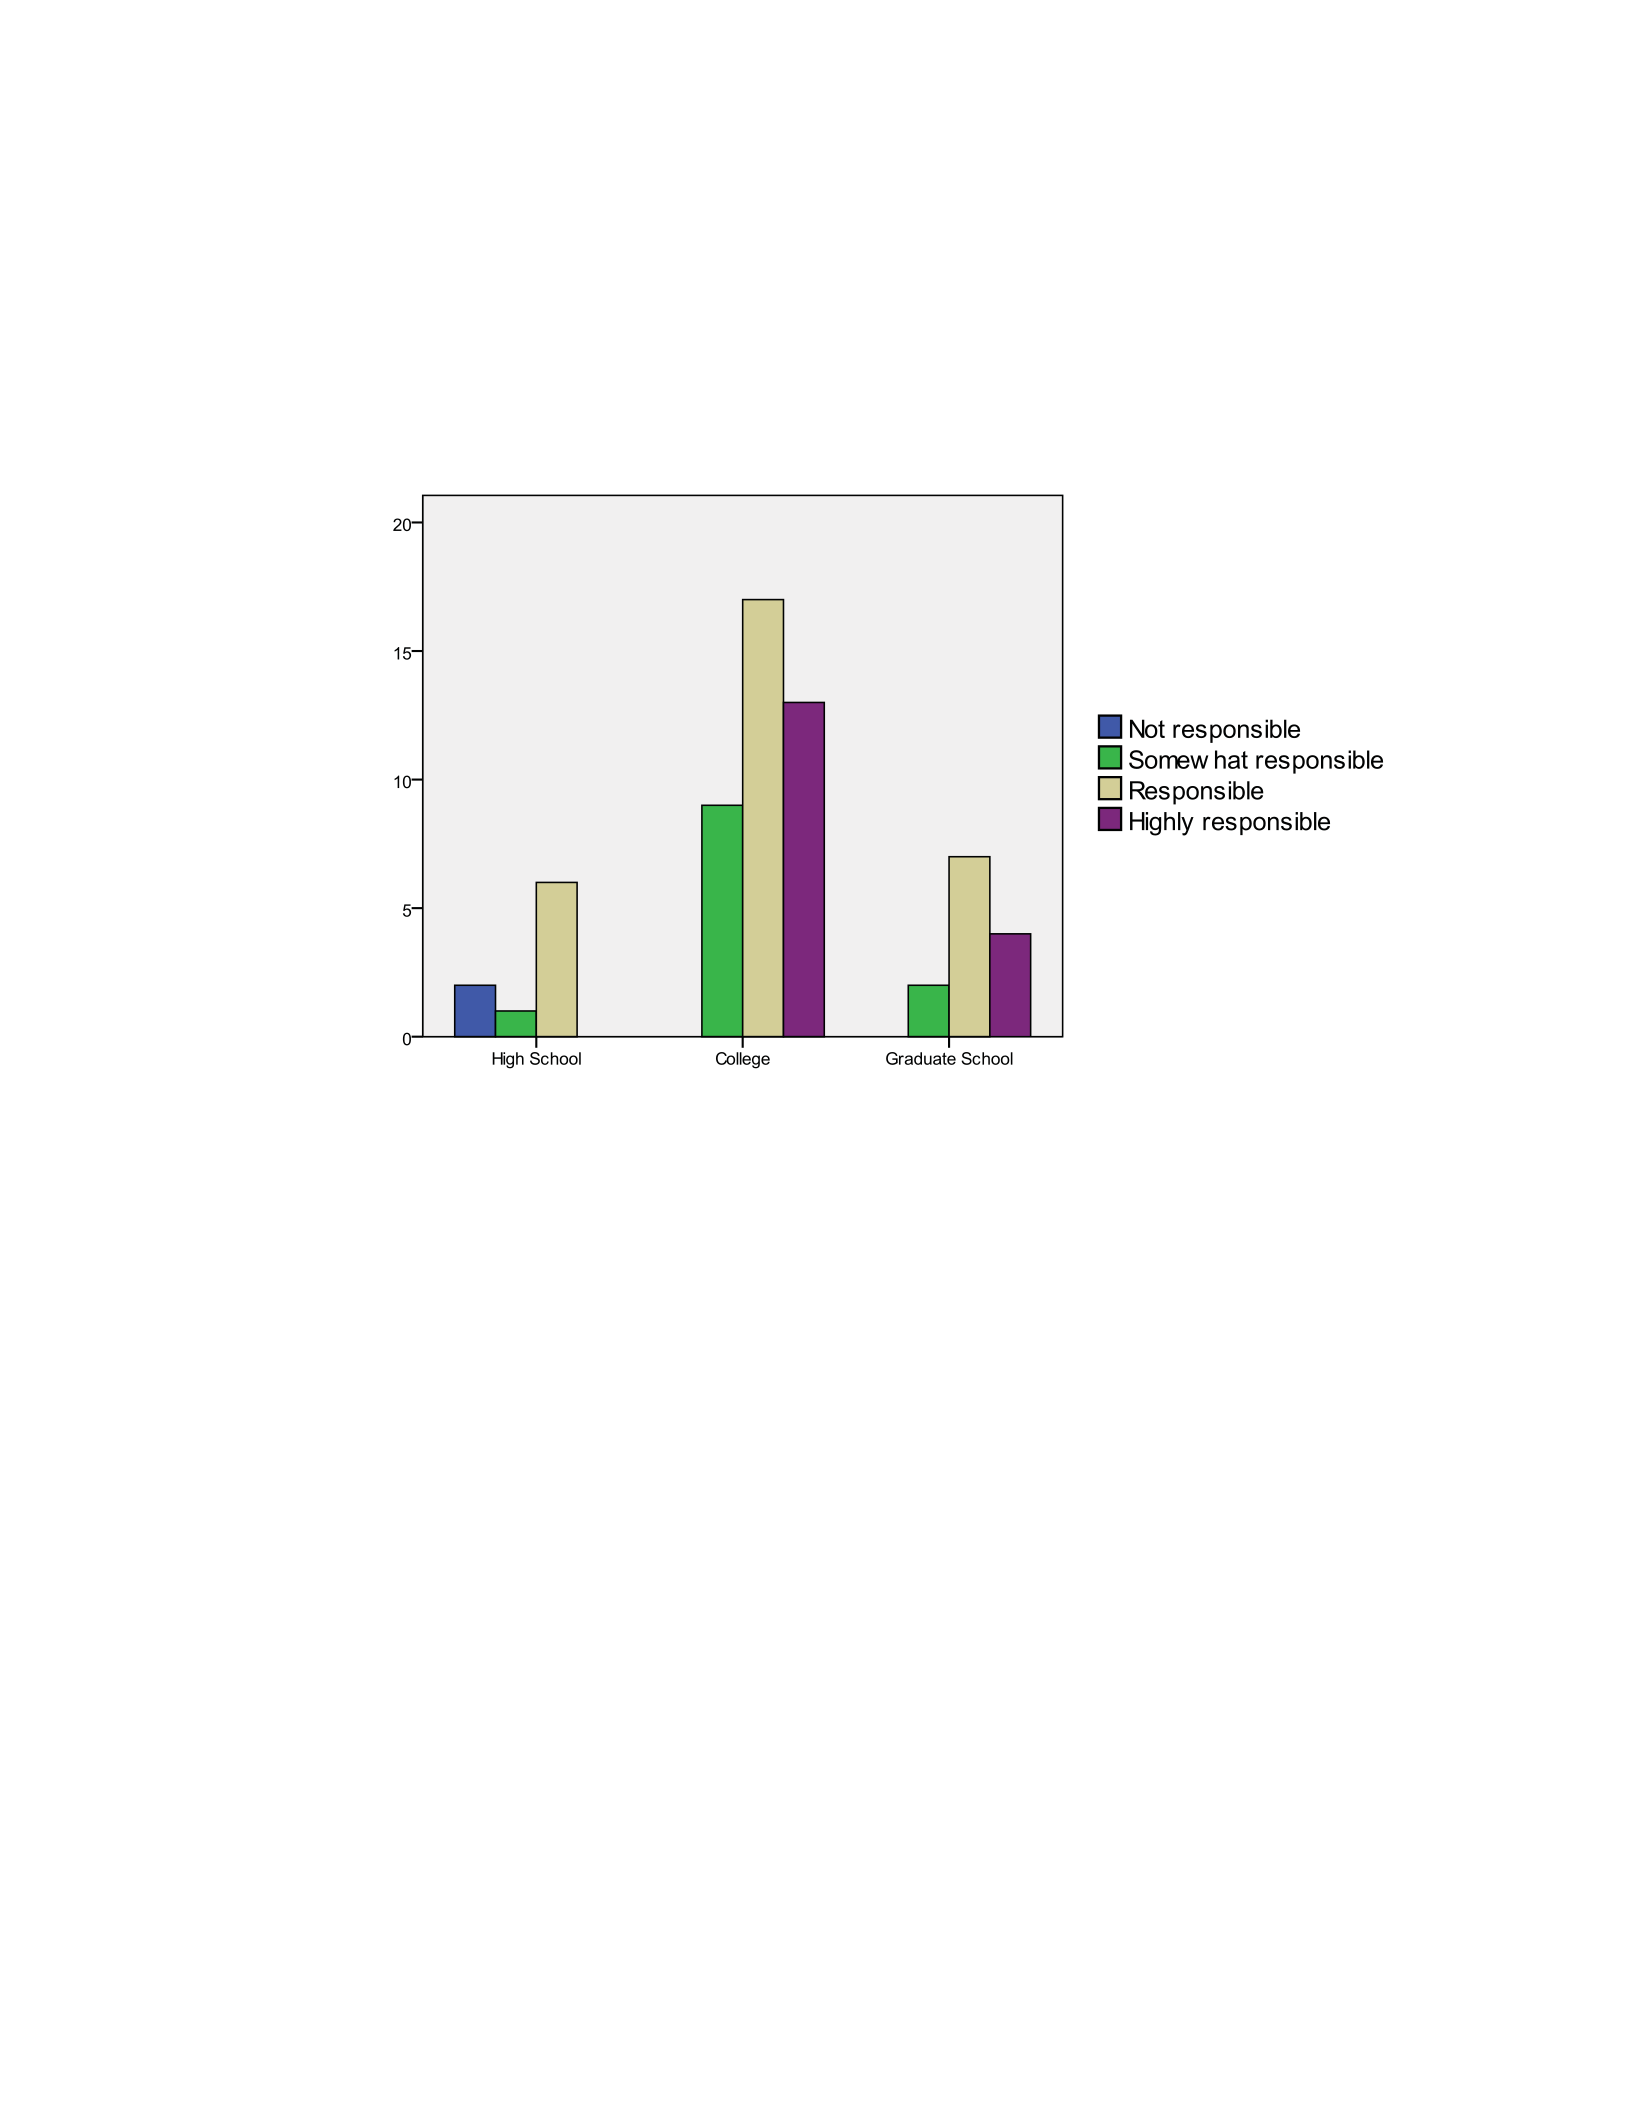
123
The only significant relationship was found between education and the
responsibility level of lower-level managers (p 0DQDJHUVZLWKDKLJK school
level education rated less than the rest of the managers for responsibility (Figure 51).
Figure 51 Managers’ education and its affect on their opinion about
the level of responsibility
Because of the small response number in each cell in Table 26, responses were
combined in two categories. The first two categories, not responsible and somewhat
responsible, were combined as “not responsible”, and the other categories, responsible
and highly responsible, were combined as “responsible.” Even through this
categorization, no more significant relationships among demographic properties and
responsibilities could be found.
The analysis of how owners, top level- and lower level-mangers rated themselves
in the responsibility rating scale can be beneficial to better understanding their
124
commitments to HF/E. The average ratings are given in Table 27. The average rating was
2.73 for owners; however, the average of the owners’ rating themselves was 2.61. It
means they believed they had less responsibility than the others’ thoughts. However, top-
and lower-level managers thought themselves more responsible than the average ratings.
Twenty three owners rated them the least responsible among owners, top- and
lower-level managers. On the other hand, top-level managers rated themselves as the
most responsible person for human factors problems among themselves, owners, and
lower-level managers. Lower-level managers also gave themselves the highest
responsibility.
Table 27 Managers’ average responsibility ratings for themselves
Responsible
Owner
Top-level
manager
Lower-level
managers
Owner (23) 2.61 2.74 2.78
Top-level manager (8) 3.00 3.38 3.13
Lower-level manager (31) 2.81 2.97 3.13
Average 2.73 2.89 2.98
Rating score:
1: Not responsible, 2: Somewhat responsible, 3: Responsible, 4: Highly responsible
Managers’ Opinions about Benefit Levels
Managers were asked to rate the benefit levels for themselves, engineers,
employees, companies, employees’ families, consumers, and the government considering
HF/E. The distribution of responses is given in Table 28.
,
125
Table 28 Managers’ opinions about benefits levels
No
Benefit
Little
Benefit
Much
Benefit
Most
Benefit
Total
Score
Rating
Average
Total
Respond
(N) (%) (N) (%) (N) (%) (N) (%)
Workers 0 0 2 3.2 21 33.9 39 62.9 223 3.60 62
Company 00003250.8 31 49.2 220 3.49 63
Lower-level managers 0 0 8 12.9 30 48.4 24 38.7 202 3.26 62
Owner 0 0 10 15.9 31 49.2 22 34.9 201 3.19 63
Top-level managers 0 0 10 16.1 32 51.6 20 32.3 196 3.16 62
Worker's families 4 6.3 11 17.5 27 42.9 21 33.3 191 3.03 63
Government 10 15.9 17 27 21 33.3 15 23.8 167 2.65 63
Engineer 10 16.1 16 25.8 23 37.1 13 21 163 2.63 62
Technician 11 17.7 16 25.8 22 35.5 13 21 161 2.60 62
Consumers 19 30.2 15 23.8 17 27 12 19 148 2.35 63
Rating score:
1: No benefit, 2: Little benefit, 3: Much benefit, 4: Most benefit
126
Table 29 Statistical analysis of managers’ demographic properties and managers’
opinion about benefits levels
State Education NAICS Employees
Experience
in FI
Position
Experience
in P
Company Ȥ22.670 0.197 0.384 0.406 1.929 1.893 2.647
P0.102 0.906 0.825 0.816 0.381 0.388 0.266
Owner Ȥ21.795 0.768 1.231 1.992 6.994 1.465 1.296
P0.408 0.943 0.873 0.737 0.136 0.833 0.862
General manager Ȥ23.739 3.867 1.144 0.765 7.929 1.035 1.481
P0.154 0.424 0.887 0.943 0.094 0.904 0.830
Production manager Ȥ25.241 2.287 1.954 4.153 4.011 0.179 0.732
P0.073 0.683 0.744 0.386 0.404 0.996 0.947
Engineer Ȥ26.580 1.164 6.518 1.045 4.406 2.516 2.111
P0.087 0.979 0.368 0.984 0.622 0.867 0.909
Technician Ȥ22.262 2.666 8.497 0.655 4.580 0.992 0.963
P0.520 0.849 0.204 0.995 0.599 0.986 0.987
Workers Ȥ23.771 14.185 3.905 1.205 1.827 0.457 1.554
P0.152 0.007* 0.419 0.877 0.768 0.978 0.817
Family Ȥ20.924 3.669 4.092 2.967 2.172 0.894 3.307
P0.820 0.721 0.664 0.813 0.903 0.989 0.769
Consumers Ȥ21.635 4.795 9.216 5.715 4.952 7.235 6.102
P0.651 0.570 0.162 0.456 0.550 0.300 0.412
Government Ȥ24.797 11.214 6.392 4.055 1.350 10.644 5.631
P0.187 0.082 0.381 0.669 0.969 0.100 0.466
A * indicates a significant relationship between managers’ demographic properties and their answers at p .
Ȥ2: Chi-square value,
p: p-value (The level of statistical significance).
127
Managers believed that workers would get the most benefits (3.60 rating average)
from HF/E interventions. Companies (3.49 rating average), lower-level managers (3.26
rating average), owners (3.19 rating average), top-level managers (3.16 rating average)
workers’ families (3.03 rating average), the government (2.65 rating average), engineers
(2.63 rating average), and technicians (2.60 rating average) were believed to get a great
deal of benefit from HF/E. Consumers, who were rated as not responsible for HF/E
problems, were also believed to get the least benefits from HF/E (2.35 rating scale). The
result of statistical analysis is given Table 29. The only significant relationship was found
between education and the benefit level of workers (p
Self evaluation of managers was also performed (Table 30). In general, managers
rated the benefits for themselves as the others rated. Owners rated themselves the person
who would get the most benefit from HF/E. Both top- and lower-level managers believed
that lower-level managers would get the most benefit.
Table 30 Managers’ average benefit ratings for themselves
HF/E will Benefit:
Owner
Top-level
manager
Lower-level
Managers
Owner (23) 3.30 3.18 3.22
Top-level manager (8) 3.00 3.13 3.25
Lower-level manager (31) 3.16 3.16 3.27
Average 3.19 3.16 3.26
Rating score: 1: No benefits, 2: Little benefit, 3: Much benefit, 4: Most benefit
Rating averages of both the responsibility level and the benefit level are given in
one figure (Figure 52). In the chart, bars with light color are the level of responsibility in
HF/E interventions, and bars with dark color are the benefits level from HF/E
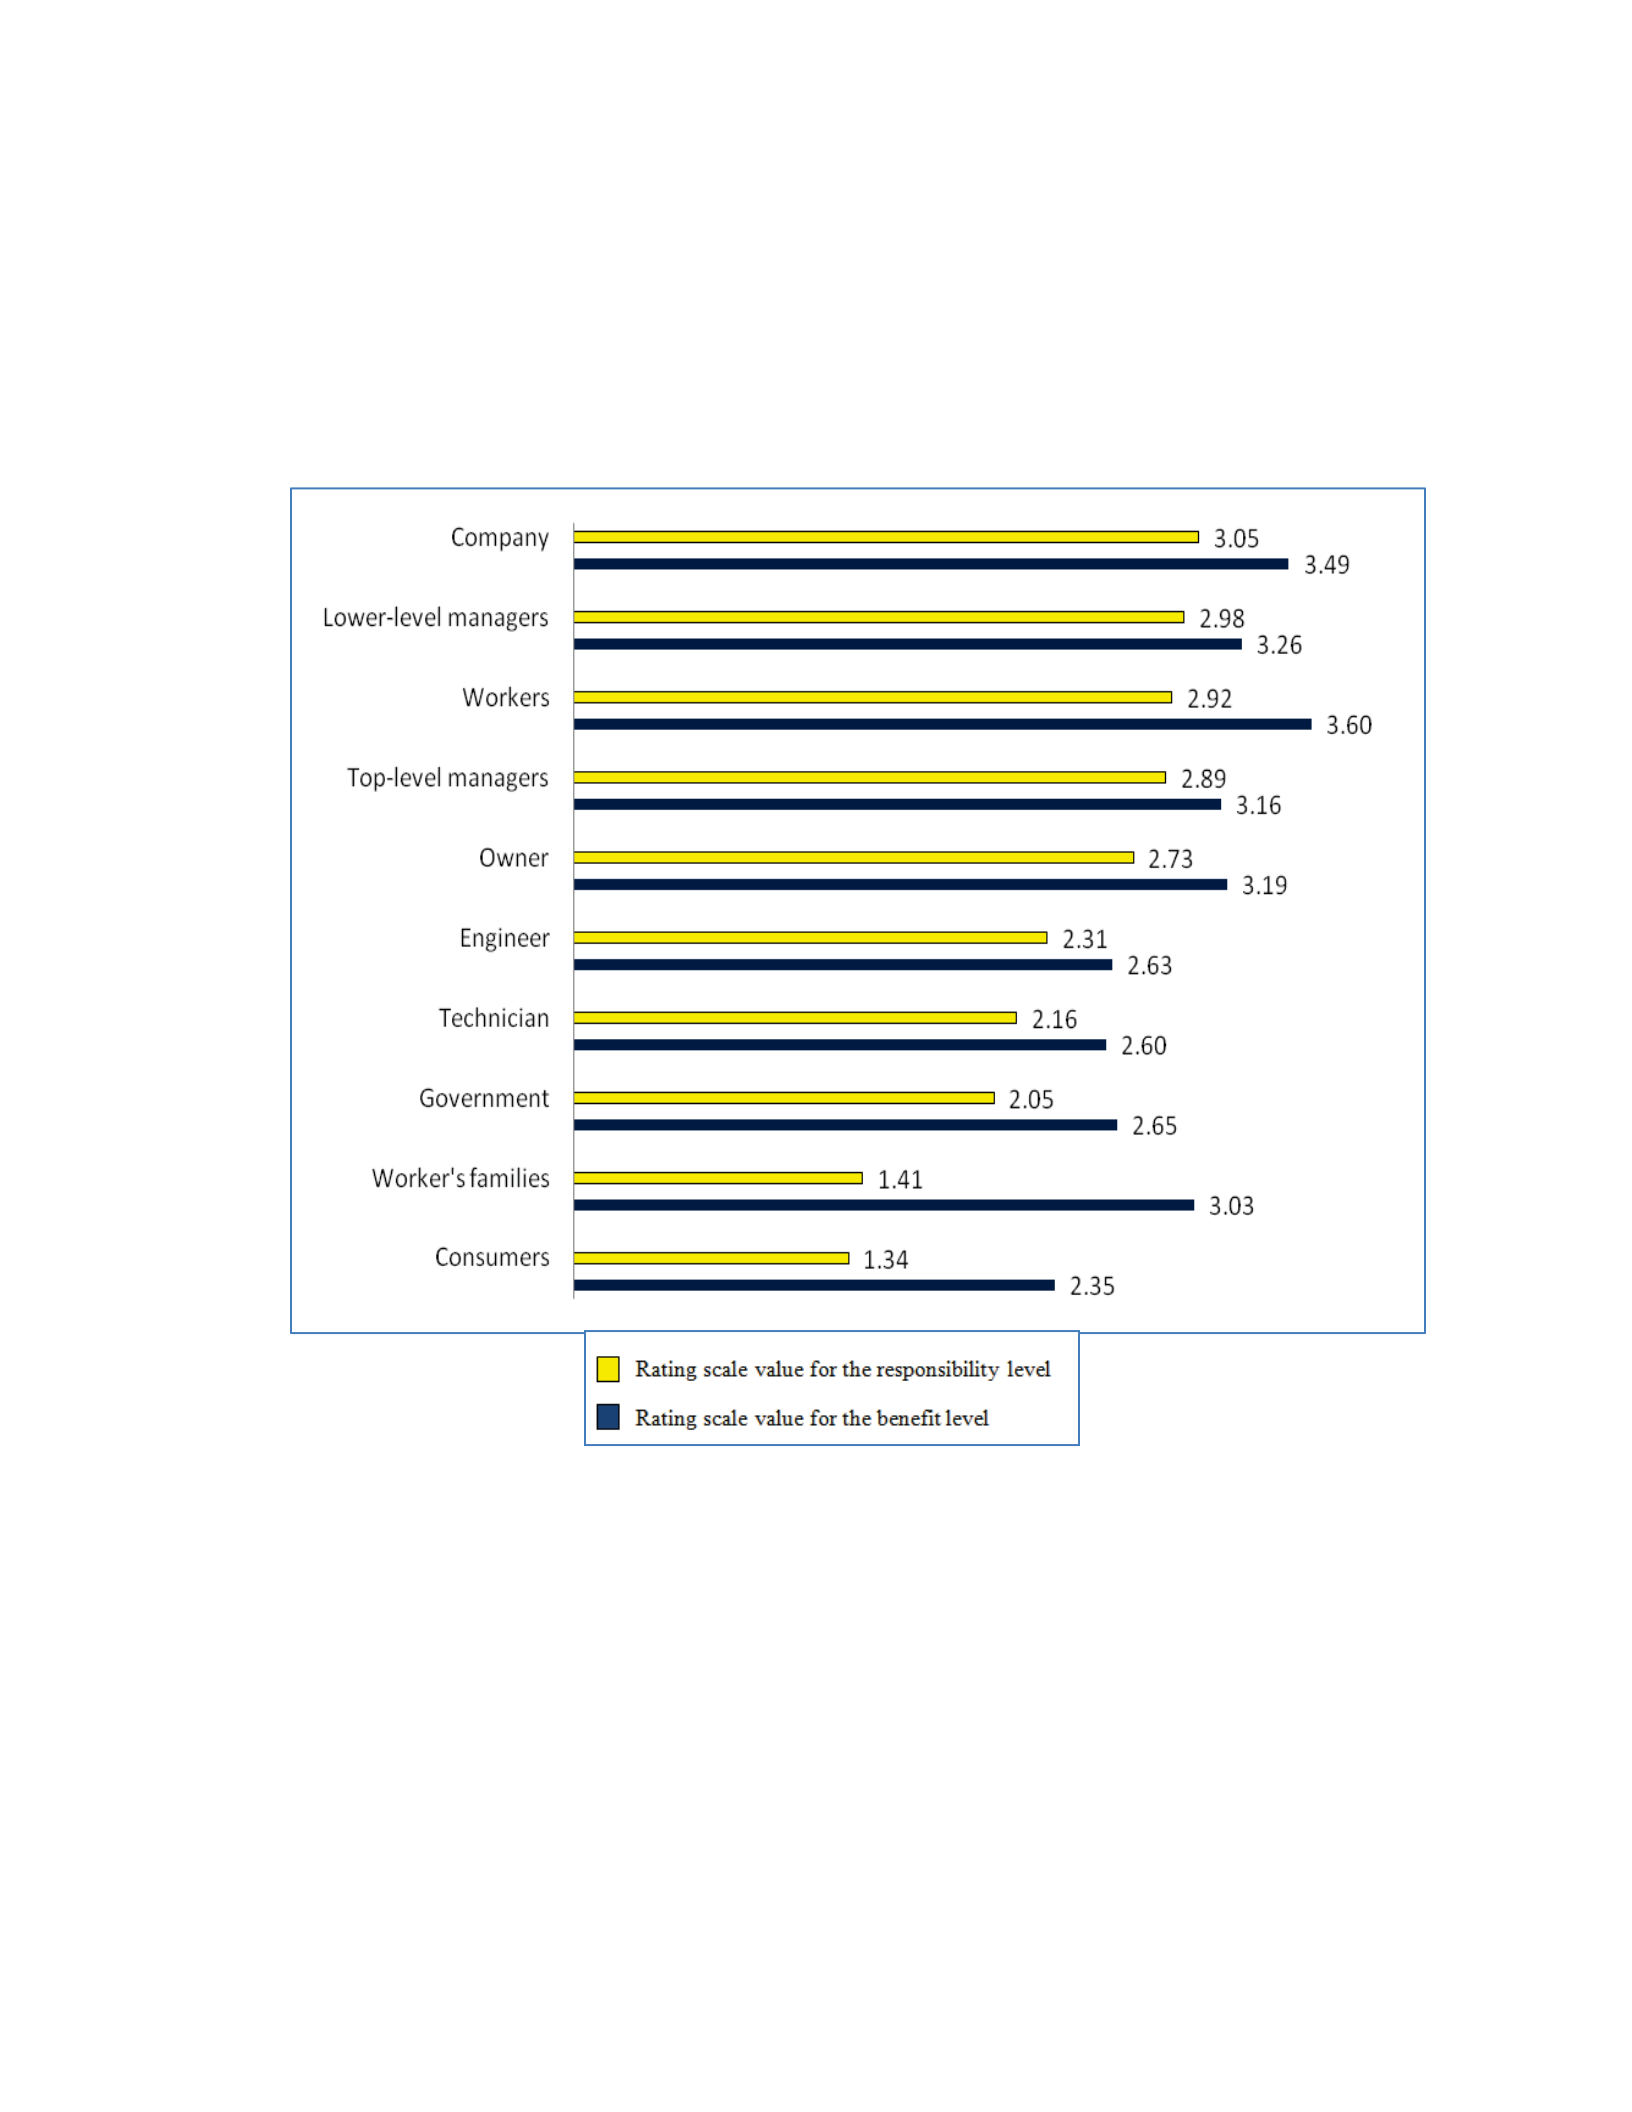
128
interventions. Therefore, managers, in general, believed that HF/E was beneficial,
especially for workers. Besides, companies and lower-level managers were the most
responsible for HF/E interventions.
Figure 52 Rating averages of responsibilities and benefits

129
CHAPTER V
CONCLUSIONS & RECOMMENDATIONS
Conclusions
This study sought to explore the degree of manager awareness of HF/E in the
American furniture industry and whether there was a relationship between managers’
demographic properties and their awareness. The study aimed to act as a catalyst for
manager awareness about HF/E in the furniture manufacturing industry. The familiarity
of managers with HF/E increases the success of managers in handling problems resulting
from poorly designed systems. The study also aimed to provide managers with some
knowledge in order to evaluate their systems in terms of HF/E issues. The study
introduces some advantages of HF/E programs and interventions to managers. For
example, managers are provided the information about how beneficial an HF/E program
could be. There is no doubt that HF/E programs result in financial benefits for a
company. Besides financial benefits, prevention or reducing occupational injuries and
illnesses is the ethical thing for companies to do; “Ergonomics is good economics, and
should be justified from both a humanitarian and an economic standpoint” (Douphrate
and Rosecrance 2004).
With the aim of better understanding of managers’ awareness through HF/E, a
web-based questionnfaire survey was used as the experimental instrument. Sixty-four

130
managers from the American furniture manufacturing industry participated in the survey.
After the data collection process, statistical analyses were performed.
Mirka (2005) stated, “Many companies in the furniture manufacturing industry
have been keenly aware of the importance of ergonomics and the positive impact that
ergonomics can have both in terms of loss prevention and productivity.” Even though the
results of this study often comply with Mirka’s statement, there were some contrasts to
the statement. In general, managers were unaware of some aspects related to HF/E. The
worst result was that some of the managers did not want to allocate their resources to
HF/E issues. Without managers’ support, all endeavors are useless and the real
achievement is not reachable. The awareness level of managers depended on some
manager demographic profiles and company characteristics. The important findings will
be given below.
First of all, to remind the demographic properties of managers and the
characteristics of their companies can help better judge the results. Thirty-one of sixty-
four managers were from Mississippi and the others were from different states in the U.S.
Half of the managers were lower-level managers (49.2%), the other half of the managers
were owners (38.1%) and top-level managers (12.7%). Most of the managers had college
degrees (62.9%). About seventy percent of the managers had more than 10 years of
experience in the furniture manufacturing industry (68.8%), and about half of the
managers had worked in the same position for more than 10 years (46.9%). Half of the
managers had worked in the Household and Institutional Furniture and Kitchen Cabinet
Manufacturing (NAICS 3371) subsector. As for company characteristics, about half of

131
the managers were from small companies (46.9%), and the rest of the managers were
from middle size (25%) and large size (28.1%) companies.
Company size is one of the factors that affects managers’ awareness level in
HF/E. Anderson (2008) points out the strong correlation between company size and HF/E
interventions by saying “the larger the company, the better the work environment”
(Andersson 2008).
Most of managers (71.4%) had not attended a formal training program in HF/E.
Particularly, managers from states other than Mississippi and from small companies
showed lower participation ratios for training programs. It can be a consequence of
economic status of companies. Small companies might not be able to afford the cost of
training programs. Owners preferred attending training programs less than top- and
lower-level managers did.
Analyses showed that large companies had more opportunity to provide
opportunities for (1) training programs for both managers and employees and (2)
attending conferences, meetings, and conventions. Training programs in general help to
prevent occupational injuries and illnesses. If the industry statistics are investigated (see
Chapter 2), it can be seen that the rate of occupational injuries and illnesses was higher in
small companies in 2007. The higher ratio can be the result of a lack of training
programs. Therefore, small companies should be provided more training programs.
Unfortunately, there were no managers in the survey who had a certification in
HF/E. In general, lower-level managers pay more attention than owners, so they attend
conferences, meetings, and conventions relating to HF/E more than owners.

132
Managers rated their knowledge on HF/E as close to average. Most of managers
(75%) rated their knowledge level as poor, fair, or average.
Reading hardcopies (e.g. books, journals, newspapers, and magazines) and
searching on the Internet were the most preferred information resources. About twenty
percent of the managers were, unfortunately, not aware of information resources about
HF/E. Mississippi managers preferred attending conferences, meetings, and conventions
and consulting an expert more than the managers from other states. Larger companies
could afford to send their managers to conferences, meetings, and conventions relating to
HF/E. Generally, lower-level managers attend conferences, meetings, and conventions
more than owners. The Other Furniture Related Product Manufacturing (NAICS 3379)
subsector showed more awareness on information resources than the other two
subsectors. To sum up, because reading books, journals, newspapers, and magazines and
using the Internet were the more preferred information resources, they were preferred as
the media of information resource.
When the likely advantages of HF/E were asked, increasing worker performance
(90.6%), reducing occupational injuries (87.5%), decreasing worker compensation costs
(75%), and improving the quality in work places (75%) were the most preferred answers.
More regulations to follow (54.7%) and higher cost in training new employees (53.1%)
were most the preferred answers for the likely disadvantages of HF/E.
Most of the responders (87.5%) that believed that HF/E does not have an impact
on reducing occupational injuries were from other states. Mississippi managers believed
more than other states’ managers that HF/E can increase furniture quality, enhance

133
competitiveness, and ensure longer survival time. Managers from the Other Furniture
Related Products Manufacturing (NAICS 3379) subsector believed that HF/E does not
increase worker’s safety. Managers working in middle and large companies believed
more than small companies that HF/E can reduce compensation costs and can cause other
cost savings (e.g. lower insurance cost). Lower-level managers believed more than top-
level managers and owners that HF/E can reduce compensation costs and can cause other
cost savings (e.g. lower insurance cost).
More experienced managers in both the industry and the position believed that
HF/E results in more time consuming processes in production. When managers in the
furniture industry were compared to panel designers, furniture manufacturing managers
were more aware of the advantages of HF/E and less concerned about the disadvantages.
That is, managers in the furniture manufacturing industry accepted HF/E as a beneficial
tool rather than panel designers.
Most managers agreed that scientific data about HF/E was not too complex to
understand and apply (87.5%); HF/E did not cause more expenses than the benefits
returned (84.4%); small changes in environmental factors in workplaces could have a
considerable impact on worker's productivity, comfort, health, and safety (68.7%);
workers could understand what HF/E deal with (17.2%); using personal protective
equipment could prevent occupational injuries and illnesses (85.9%); and working
posture can cause or prevent musculoskeletal injuries (82.9%). Managers in the Office
Furniture (Including Fixtures) Manufacturing (NAICS Code 3372) subsector agreed more
than other subsectors that their workers could understand what HF/E dealt with.

134
Unfortunately, about half of the managers mentioned that their companies had
never been inspected for HF/E problems (46.9%). A large amount of these companies
were small companies (66.7%).
Only 34.4 percent of companies had a team or department for HF/E interventions.
The ratio was lower in small companies (16.7%). Forty percent of managers expressed
that workers in their factories received training for HF/E. Only 20 percent of small
companies trained their employees.
Seventeen percent of managers mentioned that they did not prefer ergonomically
designed equipment even if it might help to reduce occupational hazards and accidents.
Mississippi manager were more willing to use ergonomically designed equipment than
the managers from other states.
Thirty percent of managers mentioned that they had sufficient resources to
allocate ergonomics interventions. Small companies did not have sufficient resources for
HF/E interventions. Managers with 3-10 years of experience in their positions mentioned
they had sufficient resources.
Managers rated the necessities of resources for HF/E. They believed that
employing an ergonomist(s) or a human factors' professional(s) was not necessary.
Likewise, a team or department to handle HF/E problems was rated as not necessary.
Managers took a neutral stance toward the necessity of scientific data, employees’
training, managers’ training, and allocation resources to HF/E. Fortunately, a small
percent of managers believed that training workers for HF/E was not necessary (17.4%).
Managers from other states, managers from small companies, managers from the Office

135
Furniture (Including Fixtures) Manufacturing (NAICS 3372) subsector, managers with
more than 10 years experience, and managers with the position of owner believed that a
team or department was not necessary. Mississippi managers took a positive stance
toward training management.
Physical fatigue (79.7%) and worker errors (78.1%) were rated as the major
causes of occupational injuries, accidents, and illness. Managers from other states
believed that mental fatigue causes occupational injuries and illnesses. Repetitive tasks
were rated by managers from the Office Furniture (including Fixtures) Manufacturing
(NAICS 3372) and the Other Furniture Related Product Manufacturing (NAICS 3379)
subsectors as a risk factor for occupational injuries and illnesses.
Managers with 3-10 years of experience in the furniture industry and managers
with less than 3 years of experience in their position did not believe that inadequate job
descriptions could cause occupational injuries and illnesses. Owners more rated mental
fatigue as a risk factor than other managers did.
Managers gave the company, lower-level managers, and workers the highest
responsibility for HF/E problems. Owners rated themselves as the least responsible, and
lower- and top-level managers rated themselves as the most responsible for HF/E
problems.
Managers believed that workers, companies, and lower-level managers would get
the most benefits from HF/E interventions. Owners believed that they would get the most
benefit among top- and lower-level managers, but top- and lower-level managers
believed that lower-level managers would get the most benefit.

