


INDUSTRIAL MICROBIOLOGY
Definition:
Industrial microbiology is basically associated with the commercial use of microbes for
the benefit of mankind. These microbial products have direct or indirect impact on the
economics, environment and social parameters of the society. The use of microbes for
the production of industrially important products is not a recent event. Mankind has
been producing alcoholic beverages and dairy products since the beginning of the
civilization but they were not known about the role of microbes in the production of
these products.
Industrial microbiology deals with the production of microbial biomass or microbial
products by a process called fermentation.
Fermentation:
Any process in which a product of economic value is obtained by using microorganisms
is called fermentation.
Industrial microbiology is an important branch of microbiology dealing with those areas
of microbiology involving economic aspects, where valuable products are prepared from
cheaper and waste material by using microorganisms. The cost of production of
antibiotics or other chemicals by fermentation is less than chemical process.
Scope of Industrial Microbiology:
Many different branches of microbiology and non-microbiological fields are directly or
indirectly involved in the study of industrial microbiology. Which include: soil and
Agricultural Microbiology, Medical Microbiology, Microbial Physiology, Cytology and
Morphology, Virology, Genetics, Marine Microbiology, Food and Dairy Microbiology and
Immunology.
Disciplines important to industrial microbiology include organic, inorganic and physical
chemistry, biochemistry, engineering, medicine, economics, sales and law, particularly
patent law and labor law, governmental regulations on the use of certain substrates and
the sale of certain products also are relevant to industrial microbiology.
Historical Events of Industrial Microbiology
S/ No. Events Time /Era Scientists
1 Fermentation to produce alcoholic
beverages
6000-2000 BC
2 Vinegar formation Pre-3000 BC
3 Production of beer 4000 BC
4 Visualization of microbes mid-17th
century
Anton Van
Leeuwenhoek
5 Discovery of alcohol fermentation by
yeasts
1818 Louis Pasteur
6 Involvement of microbes in the
production of lactic acid
1881
7 Discovery of fermentation enzymes
from yeast
1897
8 Microbial process for the production 1915
of butanol and acetone
9 Discovery of penicillin 1930 Alexander
Fleming
10 Microbial transformations 1937
11 Commercial production of penicillin 1941-44
12 Discovery of other antibiotics 1950
13 Production of single–cell protein 1960
14 Use of immobilized enzymes 1960
15 Commercial use of genetically
engineered microbes
1982
16 Cloning of secondary metabolite
operons
1990
17 High throughput screening of
industrially significant metabolites
2000
Phase Period Main products Scientists
I Period before 1900 Alcohol, Vinegar, Bakers
yeast, glycerol, citric acid,
lactic acid and acetone
/butanol
Louis Pasteur,
Hansen
II Period between
1900-1940
Penicillin, streptomycin other
antibiotics
Alexander
Fleming,
Waksman et al.
III Period between
1940-1964
Gibberellins, amino acids,
nucleotides, enzymes,
transformations
IV Period between
1964-1979
Single cell protein using
hydrocarbons and other feed
stocks
V Period 1979-
onward
Production of heterogenous
proteins by microbial and
animal cells;
Monoclonal antibodies
produced by animal cells
A vast range of industrial products which were earlier made by chemical processes are
now being made with the help of microbes.
Microbial products of industrial
importance Category
Products
Primary metabolites Enzymes, amino acids, nucleotides, organic
acids, ethanol, butanediol
Secondary metabolites Antibiotics, gibberellins, hormones,
pigments, alkaloids
Microbial biomass Baker’s yeast, single cell protein (SCP),
probiotics, vaccines
Recombinant products Insulin, streptokinase, interferons,
Interleukins, growth hormones, vaccines
Category Name of Product Producing organism Use
Alcohol Ethyl alcohol Saccharomyces
cerevisae
Alcoholic
beverages,
Industrial solvent
Antibiotics Penicillin Penicillium notatum Treatment of
bacterial infection
Cephalosporin Cephalosporium
acremonium
Streptomycin Streptomyces griseus
Acids Citric acid Aspergillus niger Soft drink,
preservative,
detergents
Amino acids Glutamic acid,
Lysine
Corynebacterium
glutamicum
Food supplement
Enzymes amylases Bacillus, Aspergillus starch hydrolysis
Protease Aspergillus niger Prevention of haze
formation
Foods Sauerkraut Lactobacilli,
Leuconostoc
Lactic acid
production
Bread, Idli, Dosa, Saccharomyces,
Lactobacilli,
Fermented food
Hormones
Insulin E. coli, Pichia pastoris Control of
diabetes
Human growth
hormone
E. coli Increase in height
Milk products Butter, Curd,
Cheese, Youghrt,
Probiotics,
Lactobacilli,
Leuconostoc
Lactic acid, flavor
and vitamins
production
Vaccines BCG Mycobacterium
tuberculosis
Protection against
tuberculosis
Typhoid Salmonella typhi Protection against
typhoid
Vitamins Vit. A Blakeslea trispora Eye and skin care
Vit. B complex Ashbya gossypii Improve metabolism
Lay out of fermentation process in industry
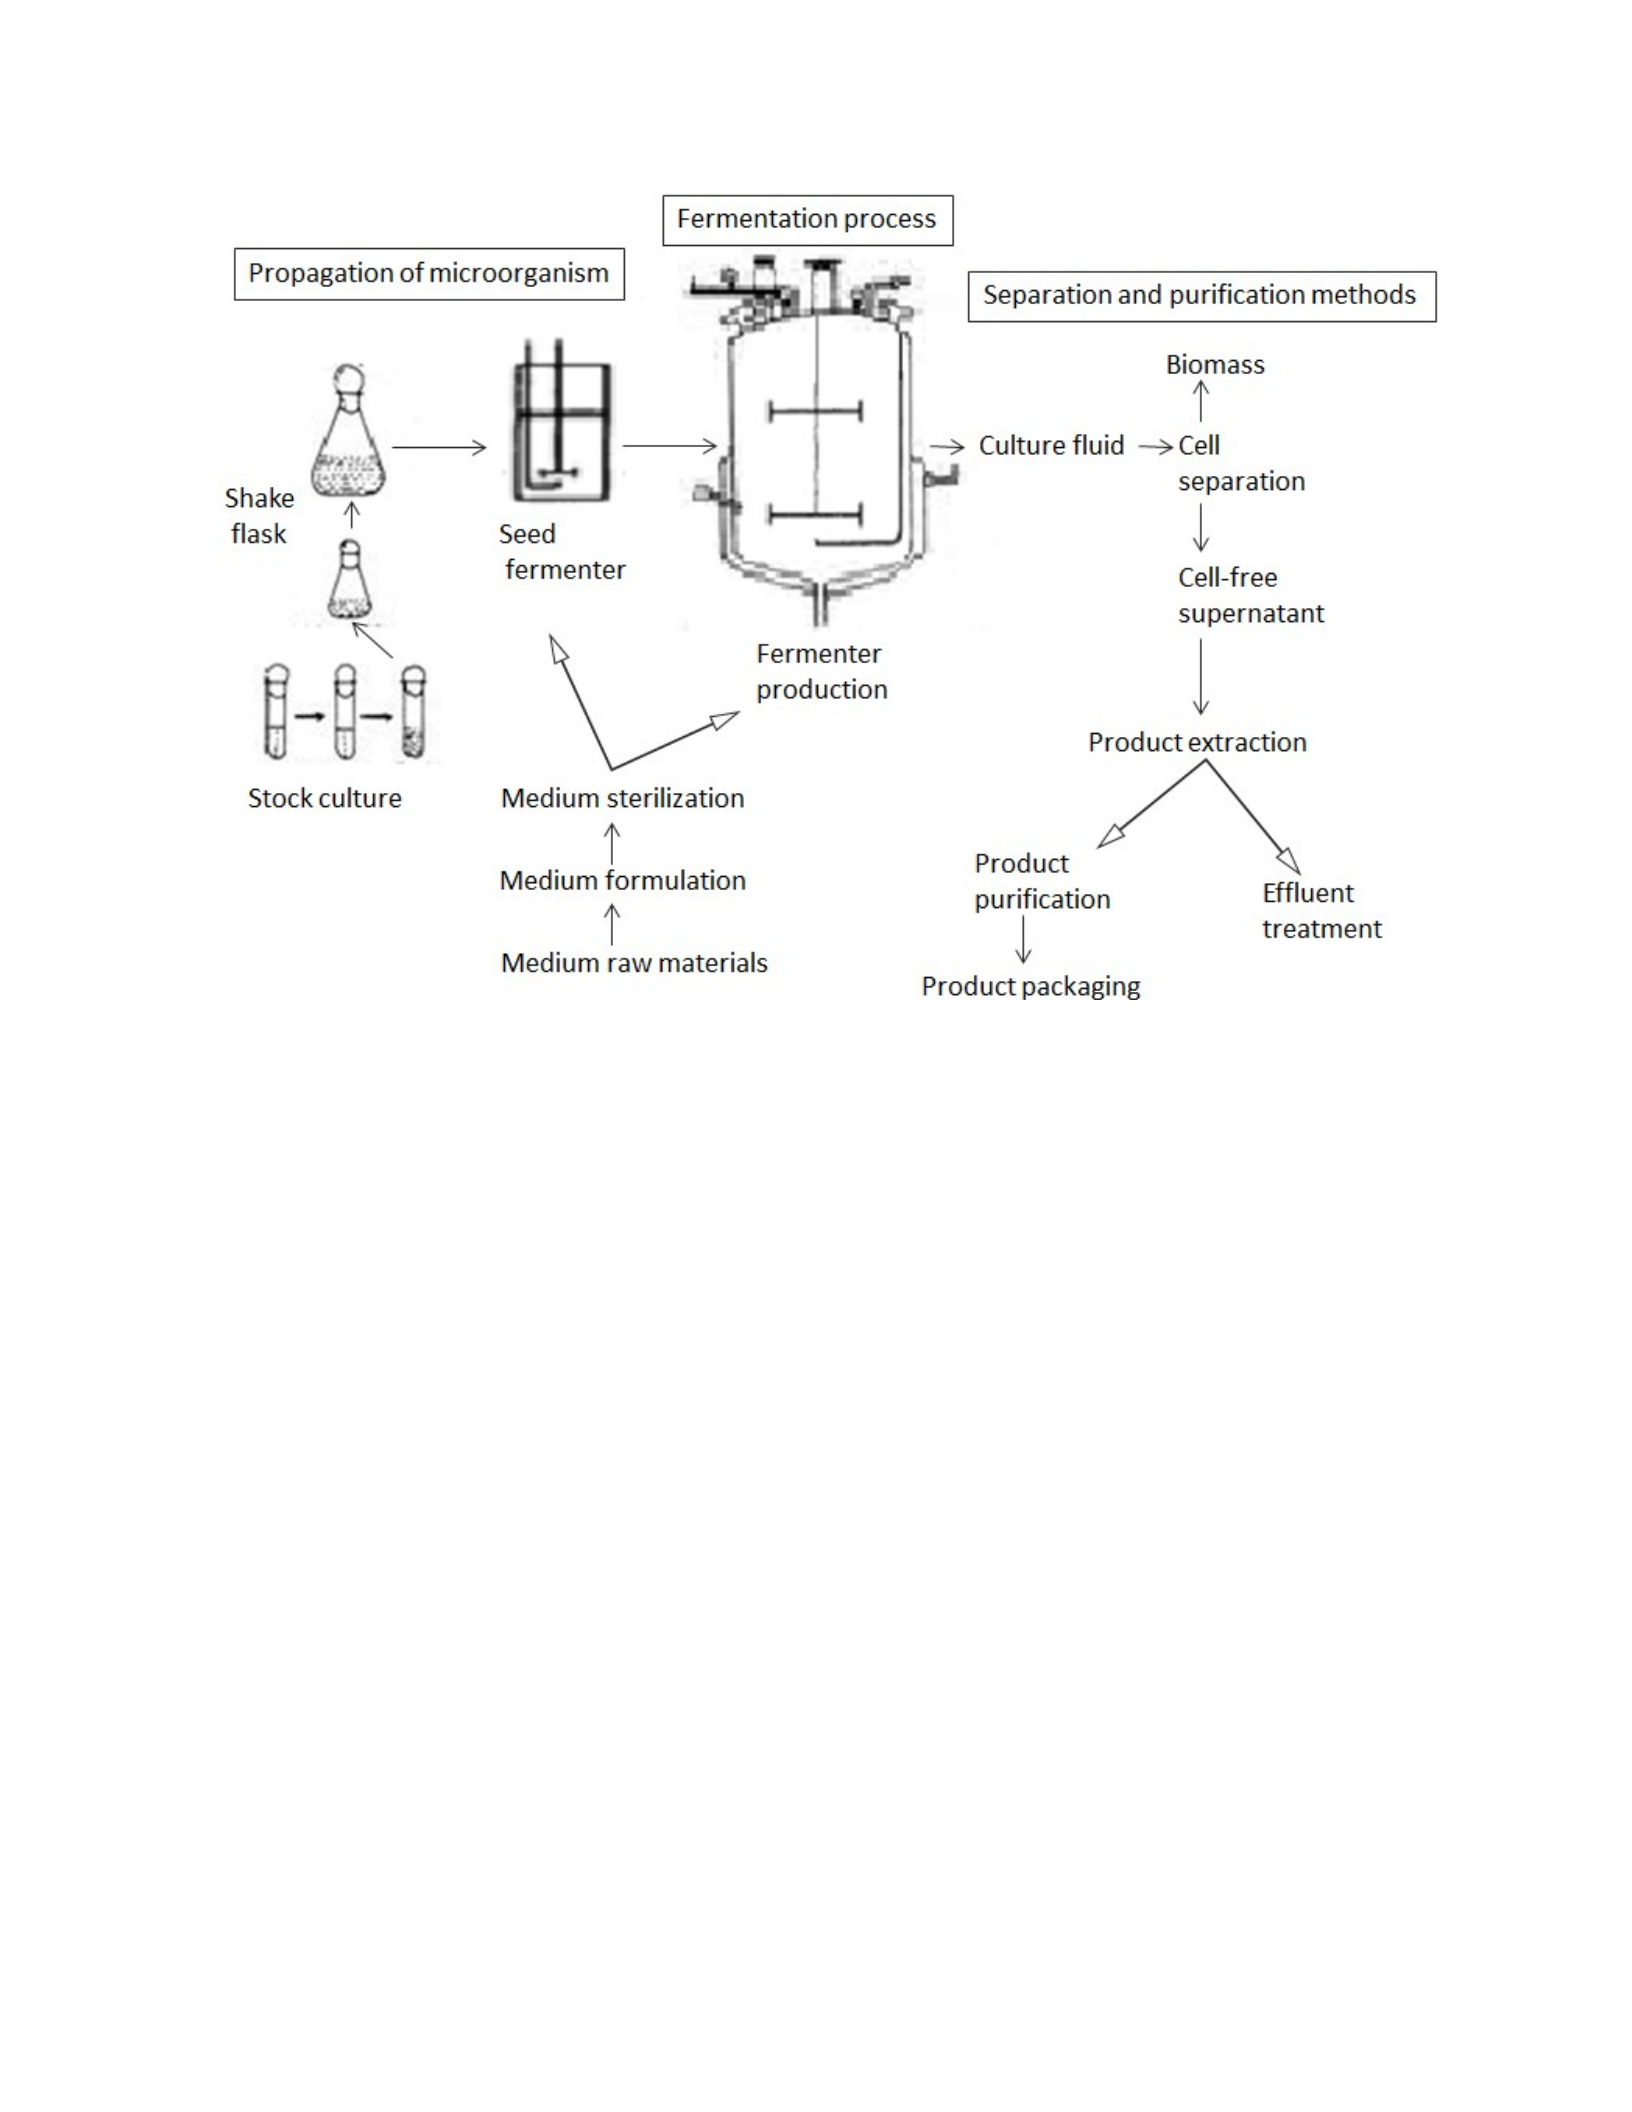
=======================================================
Different units / departments in the fermentation industry and their functions
Following are the different units / departments in the fermentation industry
A) Upstream processing unit
B) Fermentation process unit
C) Downstream processing unit
D) Quality Control and Quality Assurance unit
E) Research and Development unit
F) Packaging Unit
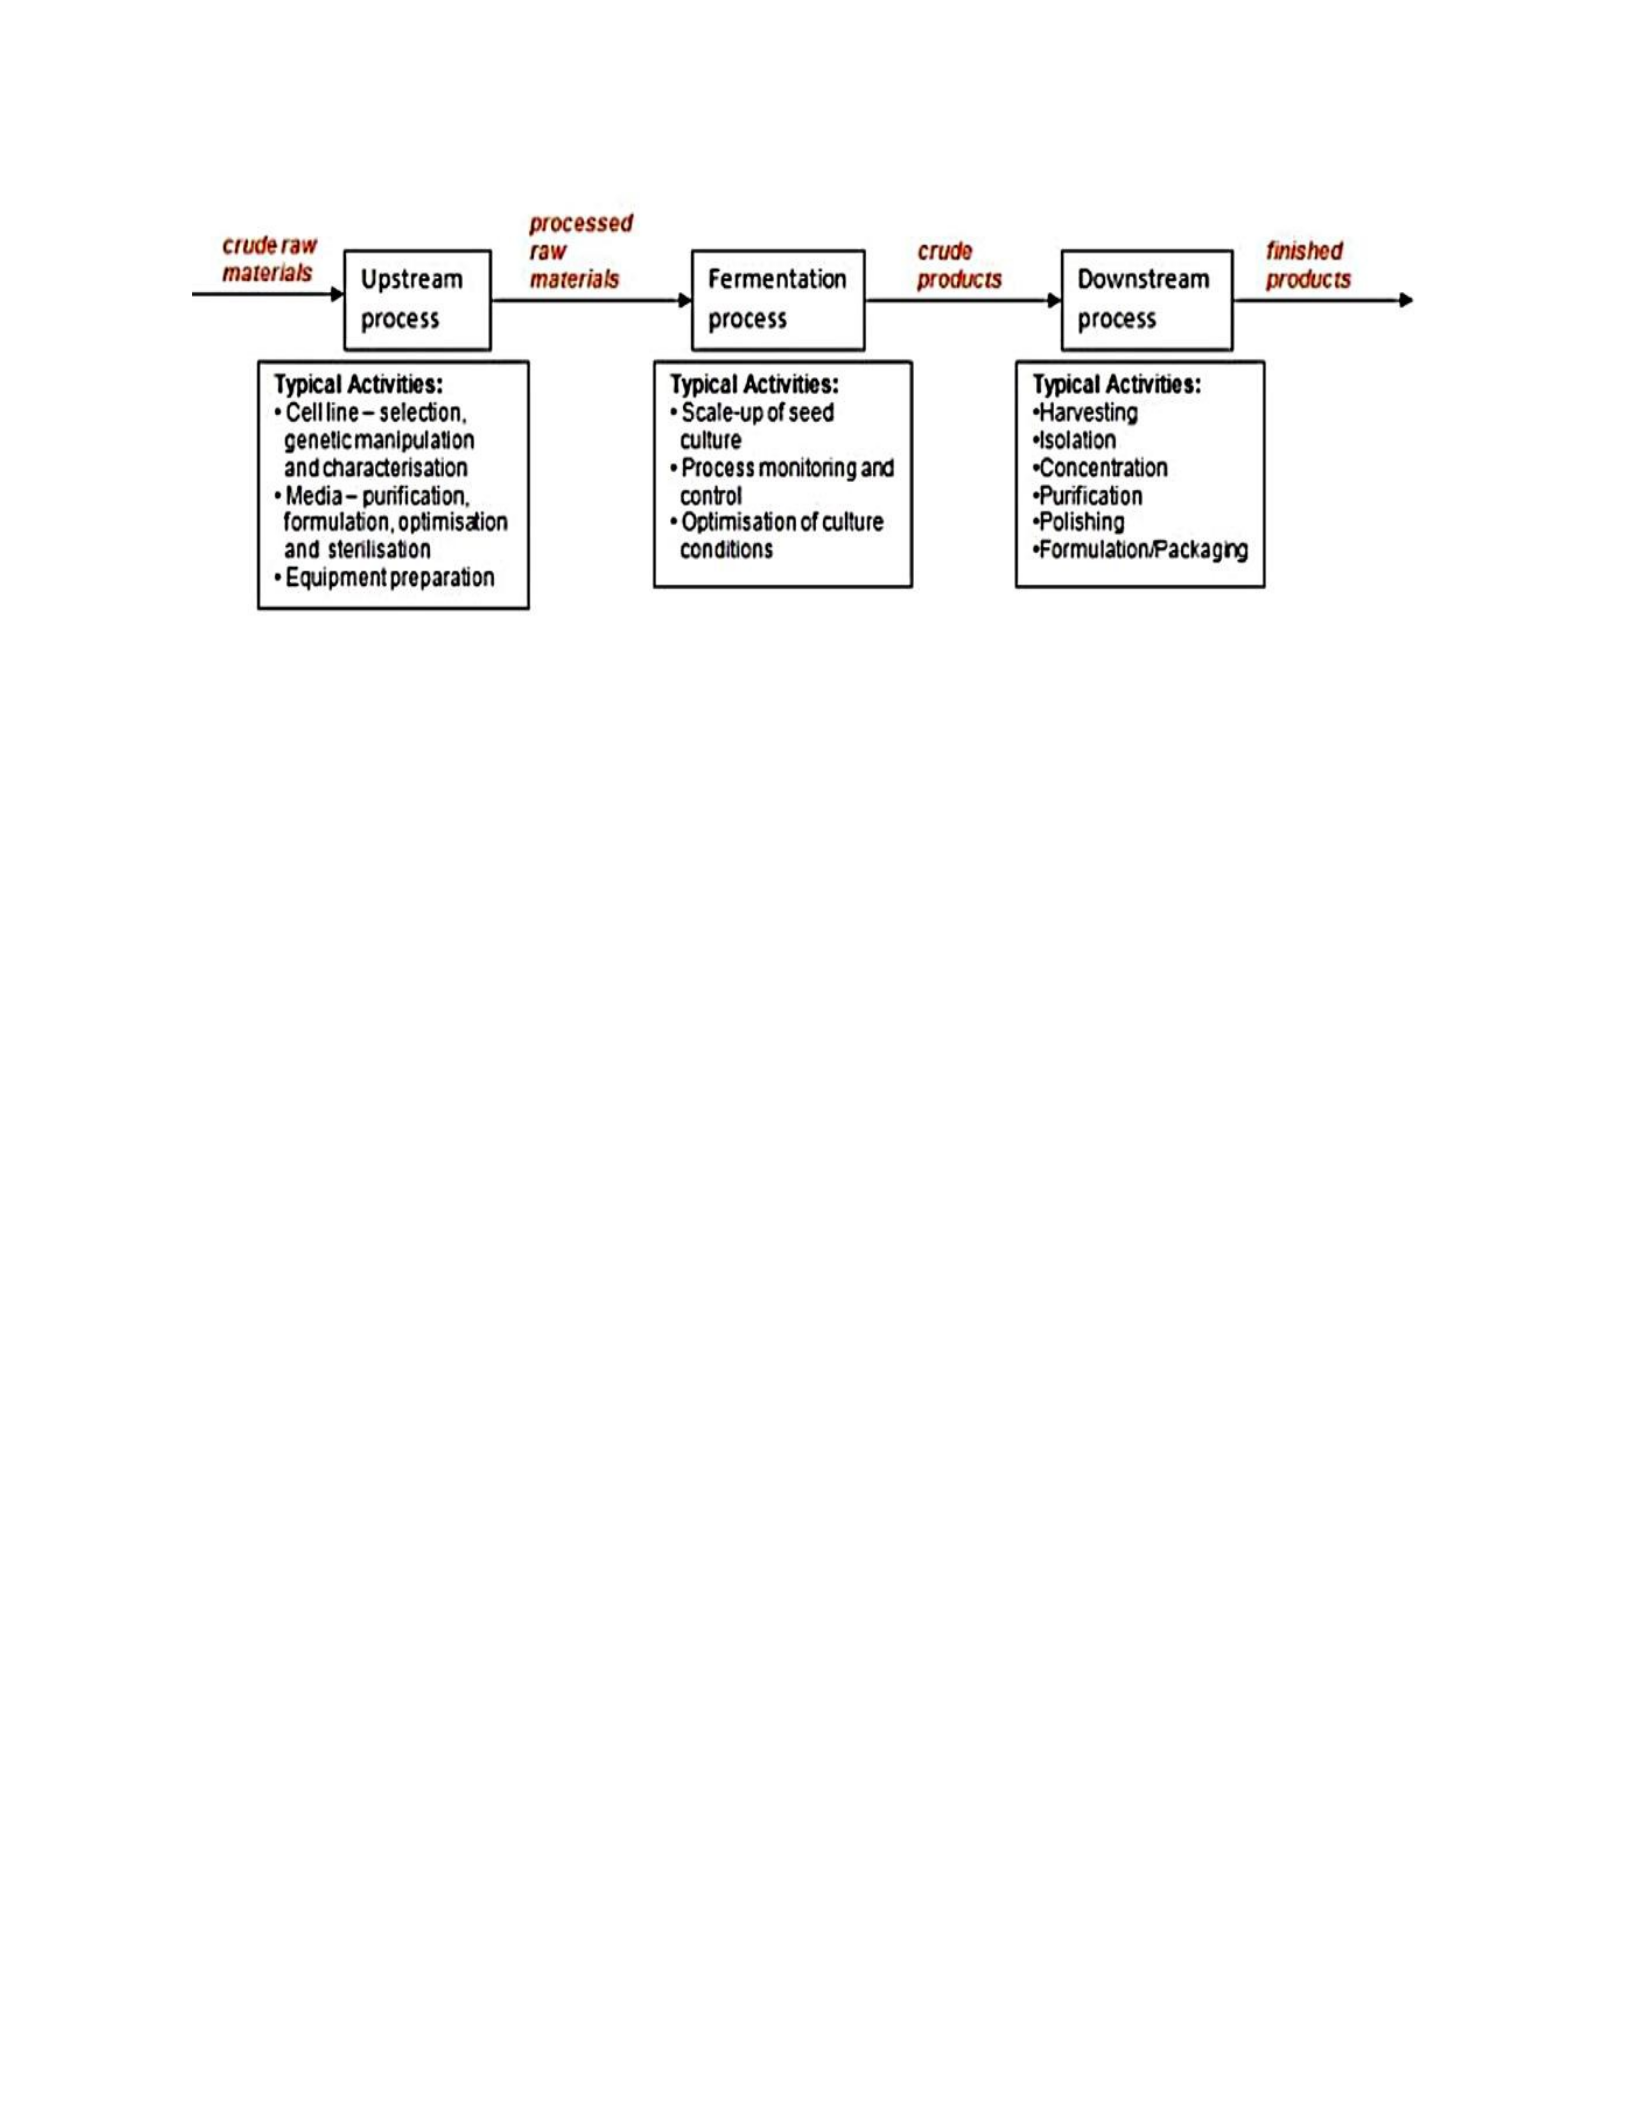
A) Upstream processing unit:
Includes:
1. Formulation of the fermentation medium unit
2. Sterilization of air, fermentation medium and the fermentor unit
3. Stock culture maintenance and Inoculum preparation unit
B) Fermentation process unit:
Includes:
1. Fermentation and Production unit
C) Downstream processing unit: includes
1. Recovery of the products in a pure state
2. Effluent treatment
D) Quality Control and Quality Assurance unit
E) Research and Development unit
F) Packaging Unit
Upstream processing unit:

This includes
1. Formulation of the fermentation medium unit
2. Sterilization of air, fermentation medium and the fermentor unit
3. Stock culture maintenance and Inoculum preparation unit
1. Formulation of the fermentation medium unit
The fermentation medium should contain an energy source, a carbon source, a nitrogen
source and micronutrients required for the growth of the microorganism along with water
and oxygen, if necessary. A medium which is used for large scale fermentation should
have the following characteristics;
a) It should be cheap and easily available.
b) It should maximize the growth of the microorganism, productivity and the rate of
formation of the desired product.
c) It should minimize the formation of undesired products. Usually, waste products from
other industrial processes, such as molasses, lignocellulosic wastes, cheese whey and
corn steep liquor, after modifying with the incorporation of additional nutrients, are used
as the substrate for many industrial fermentations.
2. Sterilization of air, fermentation medium and the fermentor unit
Sterilization is essential for preventing the contamination with any undesired
microorganisms. Air is sterilized by membrane filtration while the medium is usually heat
sterilized. Any nutrient component which is heat labile is filter-sterilized and later added
to the sterilized medium. The fermentor may be sterilized together with the medium or
separately.

3. Stock culture maintenance and Inoculum preparation unit
Inoculum build up is the preparation of the seed culture in amounts sufficient to be used
in the large fermentor vessel. This involves growing the microorganisms obtained from
the pure stock culture in several consecutive fermentors. This process cuts down the
time required for the growth of microorganisms in the fermentor, thereby increasing the
rate of productivity. Then the seed culture obtained through this process is used to
inoculate the fermentation medium.
Fermentation process unit
1. Fermentation and Production unit
The fermentation process involves the growth of the microorganism and production of
the desired product. The fermentation process can be categorized depending on
various parameters. It can be either aerobic fermentation, carried out in the presence of
oxygen or anaerobic fermentation, carried out in the absence of oxygen. Most of the
industrial fermentations are carried out under aerobic conditions where a few processes
such as ethanol production by yeast require strictly anaerobic environments.
The fermentation process can also be divided into three basic systems, namely batch,
continuous or fed-batch, depending on the feeding strategy of the culture and the
medium into the fermentor. Each of these processes has their own advantages and
disadvantages.
In a batch operation, the medium and the culture are initially fed into the vessel and it
is then closed. After that, no components are added apart from oxygen (in an aerobic

process) and acid or alkali for the pH adjustment. The fermentation is allowed to run for
a predetermined period of time and the product is harvested at the end.
In a continuous process, fresh medium is continuously added and the products, along
with the culture is removed at the same rate, thus maintaining constant concentrations
of nutrients and cells are maintained throughout the process.
A fed-batch system is a combination of these two systems where additional nutrients
are added to the fermentor as the fermentation is in progress. This extends the time of
operation but the products are harvested at the end of the production cycle as in a batch
fermentor.
The process can also be categorized as solid state fermentation (SSF) or submerged
fermentation (SmF), depending on the amount of free water in the medium.
Solid state fermentation: In this process, the medium contains no free flowing water.
The organisms are grown in a solid substrate which is moistened. This is used in certain
industrial process such as ‘koji’ fermentation from soybeans, production of amylase and
protease by Aspergillus oryzae on roasted soybeans and wheat, bioremediation,
detoxification of agro-industrial wastes, etc.
Submerged fermentation: In this process, microorganisms grow submerged in a liquid
medium where free water is abundant. This is the method of choice for many industrial
operations over SSF although SSF is also rapidly gaining interest in the present.
Downstream processing unit:
This includes
1. Recovery of the products in a pure state

2. Effluent treatment
1. Recovery of the products in a pure state:-
Product recovery is carried out through a series of operations including cell separation
by settling, centrifugation or filtration; product recovery by disruption of cells (if the
product is produced intracellularly); extraction and purification of the product.
2. Effluent treatment: -
The effluents are treated by chemical, physical or biological methods.
D) Quality Control and Quality Assurance unit
Quality Control
The term quality control may generally be defined as a system that maintains a desired
level of quality. This is done by comparing a specific quality characteristic of some
product or service with a reference. Process analysis is the complete analysis of the
industrial process including every single activity involved in the manufacturing of the
product. Thereby, all material and virtual flows are considered. Process analysis is
performed on an instrumental basis.
Quality control is accomplished by
i) Off-line quality control procedures,
ii) Statistical process control
i) Off-line quality control procedures: - involves selecting and defining controllable
product and process parameters in such a way that deviations between process output
and a standard will be minimized. A typical tool for such a product or process design is
the statistical experimental design approach or design of experiment (DoE). Quality is

here basically defined ‘off-line’ before the process has actually been implemented or
started.
ii) Statistical process control (SPC): - It compares the results or output of a process
with the selected reference states and measures are taken when deviations from a
desired condition of a process are statistically significant. When the process is poorly
designed (by inappropriate off-line quality control measures, that is, unsuitable or sub-
optimal processes) these deviations may be large and cannot be compensated for by
statistical process control. Hence, it is obvious that off-line quality control by well-
designed processes which are based on a thorough understanding of the effects of the
involved process factors on the critical quality features of the product will govern the
achievable product performance, or in other words: quality cannot be tested into
products afterwards.
Quality Assurance
Quality assurance ensures that all procedures that have been designed and planned to
produce quality of a certain level are appropriately followed. Hence, quality assurance
acts on a meta-level and continually surveys the effectiveness of the quality philosophy
of a company. Internal and external audits, standardized procedures and
comprehensive documentation systems (traceability) are important tools to achieve this
‘watchdog’ function within the company.
Strict process descriptions determining every single step required during manufacturing
a product, including the required evaluation procedures, may be defined, and deviations
from these fixed procedures may be indicative of potential deteriorations in quality.

Good Manufacturing Practice (GMP) approach or ISO certifications are typical for
quality assurance on a highly sophisticated level. However, defined procedures and
certification alone do not necessarily lead to improved performance or functionality of a
product. Specified procedures must be followed for quality assurance of the product.
Pre-defined and fixed processes that are certified and commissioned by the regulatory
authorities like Food and Drug Administration (FDA) may even prove to be hard, sub-
optimal and difficult to develop further. But every small deviation from the standard
routine processing is considered a potential quality risk and, especially in the case of
pharmaceuticals or biologicals, may comprise a potential health hazard. All such
deviations are required to be communicated to the authorities. FDA has promoted the
PAT (Process Analytical Technology) initiative which, in a similar form, is also supported
by the European Medicine Agency (EMA).
E) Research and Development unit
A company's research and development department plays an important role in the life
cycle of a product. While the department usually is separate from sales, production and
other divisions, the functions of these areas are related and often require collaboration.
A thorough understanding of the functions of the research and development department
allows you to maximize those duties at your small business, even if you don't have a big
department.
New Product Research
Before a new product is developed, a research and development department conducts
a thorough study to support the project. The research phase includes determining
product specifications, production costs and a production time line. The research also is

likely to include an evaluation of the need for the product before the design begins to
ensure it is a functional product that customers want to use.
New Product Development
The research covers the way for the development phase. This is the time when the new
product is actually developed based on the requirements and ideas created during the
research phase. The developed product must meet the product guidelines and any
regulatory specifications.
Existing Product Updates
Existing products of the company also fall under the scope of research and
development. The department regularly evaluates the products offered by the company
to ensure they are still functional. Potential changes or upgrades are considered. In
some cases, the research and development department is asked to determine a
problem with an existing product that works insufficiently or to find a new solution if the
manufacturing process must change.
Importance of sterility maintenance and checking
Fermentation product is produced by the culture of certain organism, or organisms, in a
nutrient medium. If any foreign microorganism enters the fermentation process, then
product will not be produced thus it is very necessary to sterilize the medium and other
materials so that only required organisms which we inoculate will grow and give high
yield of fermentation product. Thus process of sterilization plays very important role in
the fermentation processes.

Fermentor has various openings or points through which contaminants many enter
inside the vessel
- Improperly sterilized media
- Partially sterilized air
- Water used for cooling system
- Through different openings like outlets, inlets or other openings
- Defect in inoculum procedure
- Due to defective process of pretreatment of crude ingredients
- Due to leakage in fermentor vessel
Why sterilization is required?
If foreign microorganisms enter in the fermentation, then the following problems may
occur
- The medium would have to support the growth of both the production organism and
the contaminant, resulting in a loss of productivity.
- Foreign microorganism destroys or decrease product.
- If the fermentation is a continuous one then the contaminant may 'outgrow' the
production organism and displace it from the fermentation.
- The foreign organism may contaminate the final product, e.g. single-cell protein
where the cells, separated from the broth, constitute the product.
- The contaminant may produce compounds which make subsequent extraction of the
final product difficult.
- The contaminant may degrade the desired product; this is common in bacterial
contamination of antibiotic fermentations where the contaminant would have to be

resistant to the normal inhibitory effects of the antibiotic and degradation of the
antibiotic is a common resistance mechanism, e.g. the degradation of β-lactam
antibiotics by β-lactamase-producing bacteria.
- Contamination of a bacterial fermentation with phage (virus) could result in the lysis
of the culture.
Avoidance of contamination may be achieved by
- Using a pure inoculum to start the fermentation.
- Sterilizing the medium to be used.
- Sterilizing the fermentor vessel.
- Sterilizing everything that is used during the process.
- Maintaining aseptic conditions during the fermentation.
Principles of Sterilization
Microorganisms will be removed by sterilization process which otherwise will create
problems in fermentation process.
There are two main methods for the sterilization
1. Destruction of microorganism
2. Removal of microorganism
There are many methods for sterilization
Methods of Sterilization
Sterilization is carried out by many methods like
1. Filtration

2. Radiations
3. Ultra sonic treatment
4. Heat treatment
5. Chemical treatment
FERMENTOR: DESIGN AND ROLE OF DIFFERENT PARTS OF FERMENTOR /
BIOREACTOR
In fermentation industries, microbes are to be grown in specially designed vessels
loaded with particular type of nutritive media. These vessels are called as Fermentor or
Bioreactors.
For production of a desired microbial product, it is of extreme importance to optimize
physical (pH, temperature, aeration etc) and chemical (carbon, nitrogen, mineral
sources etc) composition of the fermentation medium. To maintain these stringent
conditions, microbes are grown in containers called as fermentors or bioreactors.
Bioreactors or fermentors are complicated in design, because they must provide for the
control and observation of many facts of microbial growth and biosynthesis. The design
of fermentor depends upon the purpose for which it is to be utilized. Industrial
fermentors are designed to provide the best possible growth and biosynthesis
conditions for industrially important microorganisms and allow no difficulty of
manipulation for all operations associated with the use of the fermentors.

(Fermentor is the proper term for an apparatus, i.e. a bioreactor, while fermenter is the
proper term for an organism that uses fermentation as a metabolic process, i.e. the
thing that goes in the fermentor.)
Characteristics of an Ideal Fermentor or bioreactor:
There cannot be a fermentor ideal for almost all fermentation processes. But fermentors
should have following characteristics:
1. Material used in the manufacture of fermentor should be strong enough to resist the
interior pressure due to the fermentation media, it should be resistant to corrosion
and free form any toxic effect for the microbial culture and the product formed by the
microbial culture.
2. A fermentor should permit easy control of contaminating microbes.
3. It should be provided with the inoculation point for aseptic transfer of inoculum.
4. Should be equipped with the aerating device (Spargers).
5. Should be equipped with a stirring device for uniform distribution of air, nutrients and
microbes (Impellers).
6. There should be provision of baffles to avoid vortex formation.
7. Fermentor should be provided with a sampling valve for aseptic withdrawing of
sample for different laboratory tests.
8. Fermentor should possess a device for controlling temperature (Temperature sensor
and water jacket internally fitted with heating coil).
9. Fermentor should be provided with pH controlling device for monitoring and
maintaining pH of media during fermentation process (pH probe and Acid base
reservoir).

10. Should be provided with a facility for intermittent addition of antifoam agents for
controlling foam formation (Reservoir of sterile Antifoming agents or mechanical
foam breakers).
11. There should be provision for feeding certain media components during the
progress of fermentation (Precursors).
12. A drain at the bottom is essential for the removal of the completed fermentation
broth for further processing.
13. A man hole should be provided at the top of fermentor for entry inside the fermentor
for different purposes like repairing and thorough cleaning of fermentors between
runs.
14. An exit valve should be provided at the top for the exit of metabolic gases produced
during fermentation processes.

