


based case study. The seven -facing DMAIC-In this module we will develop a business
article readings and your own supporting research have provided a variety of example
will case embedded case studies. You -case holistic to multiple-designs to include single
synthesize Case Study research as well as the practical use of Lean Six Sigma is crucial
based case study. The combined efforts of Case -facing DMAIC-to developing a business
.Study research and LSS tools offer business solutions methodology

BUSI 830
DMAIC (FINAL) CASE STUDY ASSIGNMENT INSTRUCTIONS
In this final module, you will synthesize the qualitative research methodology of Case
Study research (and applications) (Yin, 2018) as well as the practical use of Lean Six Sigma
(Hall & Scott, 2016; George et al., 2005) to develop a business-facing DMAIC-based case study.
Also, the seven article readings and your own supporting research has provided a variety of
example designs to include single-case holistic to multiple-case embedded case studies. After
reviewing the Reading & Study material for this module and review of the rest of the course, in
current APA format, design a comprehensive (non-Kaizen) DMAIC Case Study integrated with
Lean Six Sigma tools and biblical worldviews. This must include a plan overview section, as
well as design, measure, analyze, improve, control phases.
Create a real-world case (that is, make sure the story is believable, i.e. it consists of
sequence of time and events, problems and issues to solve, identities [positions/titles] and so on.)
Sanitize all names and use only fictitious data. Use at least 3 Lean Six Sigma tools (George et al.
(2005) by chapter [e.g. a value stream mapping and process flow tool, a data collection tool, an
identifying and verifying causes tool, etc.]) and show your work (i.e. if using a value stream
map, measurement selection matrix, scatter plot, etc.; design a graph, chart, or figure as
appropriate, insert, and refer to such as per APA.) If there could be any doubt, the emphasis of
this project is the DMAIC Case Study process. (HINT: The Cabrita et al. (2016) article serves as
an excellent example.)
Required Format
This 2400 minimum, 3000 maximum word paper needs to be written with these main sections:
Cover page
Abstract
Introduction
Case Study ‘Plan’
Define Phase
Measure Phase
Analyze Phase
Improve Phase
Control Phase
Conclusion
References
Other Requirements
Materials submitted to fulfill requirements in one course may not be submitted in another course.
Concerns about the propriety of obtaining outside assistance and acknowledging sources should
be addressed to the instructor of the course before the work commences and as necessary as the
work proceeds.

BUSI 830
The cover page must include this statement as an author’s note: “By submitting this
assignment, I attest this submission represents my own work, and not that of another
student, scholar, or internet source. I understand I am responsible for knowing and
correctly utilizing referencing and bibliographical guidelines. I have not submitted this
work for any other class.”
In addition to the course textbook(s) and the Bible, this paper must include at least 10
references from scholarly articles that have publication dates no older than 5 years. Do
not use any books other than the Bible and the textbooks. Do not conduct interviews.
There should be at least one instance of biblical integration (at least one scripture
reference).
In-text citations are required to support your statements, points, assertions, issues,
arguments, concerns, paragraph topic sentences, and statements of fact and opinion.
The required cover page, abstract and the reference pages are not included in the required
assignment word count but are required as part of your paper.
The APA required abstract and conclusion section headings and subject headings (see
above) are expected. For papers this length, there should be at least three (3) ‘levels of
headings’.
The introduction and conclusion sections should not be longer than ½ page each since the
assignment is short in word count.
The required abstract should be written as a stand-alone document and not written as an
introduction since an introduction section is required. Therefore, refrain from using
phrases such as, “in this paper,” and do not use citations. See example in APA manual.
Sources of information from Wikipedia, dictionaries, and encyclopedia will not be
accepted. Similarity scores must not exceed 20%.
Paragraph lengths: Each paragraph should have a topic sentence unless it continues from
or provides support to the prior paragraph. A paragraph is defined in this course as being
at least 4 sentences in length.
All parts of the assignment must be based on scholarly and biblical literature.
Avoid clichés, slang, jargon, exaggerations, abbreviations, figurative language, and
language that is too informal and too subjective.
Submit your final document for grading with file name syntax: Last NameFirst Initial
Project#. For example: PhilebaumJ Project8.doc (no .pdfs)
Grading Metrics
Consult the accompanying rubric for how your instructor will grade this assignment. Also, any
form of plagiarism, including cutting and pasting, will result in zero points for the entire
assignment. All quoted materials must be properly cited in current APA format.
Note: Your assignment will be checked for originality via the SafeAssign plagiarism tool.
BUSI 830
DMAIC (FINAL) Case Study Grading Rubric
Criteria
Levels of Achievement
Content ‐ 98 Points
Advanced
Proficient
Developing
Not present
Points
Earned
Abstract,
Introduction,
Case
Study ‘Plan’
10 Points
10 to 10 points
Abstract clearly states the
purpose and main conclusion
and Introduction provides a
complete overview of the
discussion. Provides a
complete discussion for doing
a case study to include the
overarching case study ‘plan’.
Flow is logical and fully cited.
8 to 9 points
Abstract and Introduction
provides a partial purpose,
main conclusion, and
overview of the discussion
and provides a partial
discussion for doing a case
study to include the
overarching case study ‘plan’.
Flow is mostly logical and
partially cited.
1 to 7 points
Abstract and Introduction
present but does not provide
an adequate overview of the
discussion and provides a
minimal discussion for doing
a case study to include the
overarching case study
‘plan’. Flow is not logical
and/or insufficiently cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Define Phase
15 Points
14 to 15 points
Section provides a
comprehensive description of
the Define Phase (includes
key steps such as: customers,
problem statement, resources,
crucial support, high-level
process map, etc.). Flow is
logical and fully cited.
13 to 13 points
Section provides a partial
description of the Define
Phase (includes most key
steps such as: customers,
problem statement, resources,
crucial support, high-level
process map, etc.). Flow is
logical and partially cited.
1 to 12 points
Section provides a minimal
description of the Define
Phase (includes few key
steps such as: customers,
problem statement,
resources, crucial support,
high-level process map, etc.).
Flow is not logical and/or
insufficiently cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Measure Phase
15 Points
14 to 15 points
Section provides a complete
and thorough description of
the Measure Phase (includes
key steps such as: defects,
opportunities, units, metrics,
data collection plan, validating
the measurement system,
etc.). Flow is logical and fully
cited.
13 to 13 points
Section provides a partial
description of the Measure
Phase (includes most key
steps such as: defects,
opportunities, units, metrics,
data collection plan, validating
the measurement system,
etc.). Flow is mostly logical
and partially cited.
1 to 12 points
Section provides a minimal
description of the Measure
Phase (includes few key
steps such as: defects,
opportunities, units, metrics,
data collection plan,
validating the measurement
system, etc.). Flow is not
logical and/or insufficiently
cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Analyze Phase
15 Points
14 to 15 points
Demonstrates critical thinking
to include analysis, evaluation,
and synthesis of the analyze
phase (includes key steps
such as: performance
objectives, value vs NVA,
opportunities to improve root
cause, variation, etc.). Flow is
logical and fully cited.
13 to 13 points
Mostly demonstrates critical
thinking to include analysis,
evaluation, synthesize of the
analyze phase (includes most
key steps such as:
performance objectives, value
vs NVA, opportunities to
improve root cause, variation,
etc.). Flow is mostly logical
and/or partially cited.
1 to 12 points
Only partially demonstrates
critical thinking, analysis,
evaluation, and/or limited
synthesis of analyze phase
(includes few key steps such
as: performance objectives,
value vs NVA, opportunities
to improve root cause,
variation, etc.). Flow is not
logical and/or insufficiently
cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
BUSI 830
Improve Phase
15 Points
14 to 15 points
Section provides a complete
and thorough description of
the Improve Phase (includes
key steps such as:
experiments, solutions,
operating tolerances,
implementing the best
solution, etc.). Flow is logical
and fully cited.
13 to 13 points
Section provides a partial
description of the Improve
Phase (includes most key
steps such as: experiments,
solutions, operating
tolerances, implementing the
best solution, etc.). Flow is
mostly logical and partially
cited.
1 to 12 points
Section provides a minimal
description of the Improve
Phase (includes few key
steps such as: experiments,
solutions, operating
tolerances, implementing the
best solution, etc.). Flow is
not logical and/or
insufficiently cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Control Phase
15 Points
14 to 15 points
Section provides a complete
and thorough description of
the Control Phase (includes
key steps such as: standards,
process control/capability,
documentation/report, etc.).
Flow is logical and fully cited.
13 to 13 points
Section provides a partial
description of the Control
Phase (includes most key
steps such as: standards,
process control/capability,
documentation/report, etc.).
Flow is mostly logical and
partially cited.
1 to 12 points
Section provides a minimal
description of the Control
Phase (includes few key
steps such as: standards,
process control/capability,
documentation/report, etc.).
Flow is not logical and/or
insufficiently cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Conclusion &
Biblical Worldview
Integration
13 Points
13 to 13 points
Conclusion provides a
complete summary of the
discussion and highlights key
points as well as a thoroughly
integrated biblical worldview
with at least 1 scripture
reference.
11 to 12 points
Conclusion provides a partial
summary of the discussion
and highlights at least one key
point and a partially integrated
biblical worldview with at least
1 scripture reference.
1 to 10 points
Conclusion present but does
not summarize discussion or
highlight key points and
either a reference to a
biblical worldview or no
scripture reference.
0 to 0 points
Not completed.
Structure ‐ 42
Points
Advanced
Proficient
Developing
Not present
Points
Earned
Mechanics,
Composition,
Grammar, Word
Count
21 Points
20 to 21 points
Mechanics, Composition, 3 or
more Lean Six Sigma Tools &
Word Count is thorough
(2400-3000 words).
18 to 19 points
Mechanics, Composition, 2
Lean Six Sigma Tools & Word
Count is satisfactory (+/- 2%).
1 to 17 points
Mechanics, Composition, at
least 1 Lean Six Sigma Tool
& Word Count is insufficient
(+/- 3-4%).
0 to 0 points
There are many errors
in mechanics,
composition, grammar,
no Lean Six Sigma
Tools, or Word Count
(>4% diff).
APA Format,
Structure, &
References and
Citations
21 Points
20 to 21 points
Proper cover page and
section headings included.
Met all of the required
formatting. References
exceed requirements in
number and quality and/or
most statements are
supported by a variety of
citations.
18 to 19 points
Proper cover page and
section headings included.
Met most of the required
formatting. References meet
requirements in number and
quality and/or many
statements are supported by a
variety of citations.
1 to 17 points
No cover page and/or section
headings included. Met some
required formatting.
References do not meet
requirements in number and
quality and/or some
statements are supported by
a variety of citations.
0 to 0 points
No structure or
formatting provided.
Missing references
and/or citations are
rare, repetitious or non-
existent.
Total Points
/140
Instructor Comments:
236
I
nt. J. Productivity and Quality Management, Vol. 17, No. 2, 2016
Copyright © 2016 Inderscience Enterprises Ltd.
Six Sigma through DMAIC phases: a literature review
K. Srinivasan*
Department of Mechanical Engineering,
Adhiyamaan College of Engineering,
Hosur – 635 109, India
Email: [email protected]
*Corresponding author
S. Muthu
Department of Mechanical Engineering,
Dr. N.G.P Institute of Technology,
Coimbatore – 641 048, India
Email: smuthu231155@gmail.com
S.R. Devadasan
Department of Production Engineering,
PSG College of Technology,
Coimbatore – 641 004, India
Email: devadasan[email protected]
C. Sugumaran
Department of Mechanical Engineering,
Salem College of Engineering and Technology,
Salem – 636 111, India
Email: mailsugum[email protected]
Abstract: In this paper, the details of a literature review carried out to examine
the application of DMAIC (stands for define, measure, analyse, improve and
control) in companies to achieve the goals of Six Sigma concept are presented.
While conducting this literature review, the papers containing DMAIC in their
titles were gathered and studied. The outcomes of the researches reported in
these papers have confirmed that, DMAIC is the model compatible for
nourishing the benefits of Six Sigma concept in manufacturing, service and
unconventional sectors. An important inference drawn at the end of conducting
this literature review is that, the investigations on applying DMAIC in an
unconventional sector are yet to begin widely and intensively. In this
background, this paper is concluded by suggesting the future researchers to
examine the application of DMAIC in several unconventional sectors.
Keywords: Six Sigma; define, measure, analyse, improve and control;
DMAIC; belt-based training; literature review; project charter; cause and effect
diagram.
Six Sigma through DMAIC phases 237
Reference to this paper should be made as follows: Srinivasan, K., Muthu, S.,
Devadasan, S.R. and Sugumaran, C. (2016) ‘Six Sigma through DMAIC
phases: a literature review’, Int. J. Productivity and Quality Management,
Vol. 17, No. 2, pp.236–257.
Biographical notes: K. Srinivasan is currently an Associate Professor in the
Mechanical Engineering Department of Adhiyamaan College of Engineering,
Hosur, India. He holds a Bachelor in Mechanical Engineering and a Master in
Computer Aided Design, which he obtained from University of Madras, India.
He has 19 years of teaching experience. His research interests include total
productive maintenance, quality function deployment and Six Sigma concepts.
S. Muthu is currently Professor and Dean in the Mechanical Engineering
Department of Dr. N.G.P Institute of Technology, Coimbatore, India. He
obtained his Bachelor in Production Engineering and his Master in Industrial
Engineering from University of Madras, India. He has 33 years of teaching and
research experience. He received his PhD degree from Bharathiyar University
in the year 2003. He has published over 15 papers in international journals. His
areas of research interest include total productive maintenance, work systems
engineering, total quality management, benchmarking and risk management.
S.R. Devadasan is currently a Professor in the Production Engineering
Department of PSG College of Technology, Coimbatore, India. He holds a
Bachelor in Mechanical Engineering, a Master in Industrial Engineering, a PhD
in Mechanical Engineering and a DSc in Mechanical Engineering. He has
24 years of teaching and research experience. He has published over 120 papers
in international journals. He is an editorial advisory board member in the
European Journal of Innovation Management, UK. His areas of research
interest include strategic quality management, total productive maintenance,
productivity engineering and management, agile manufacturing, business
process reengineering, innovation management and risk management.
C. Sugumaran is currently Professor and Dean in the Mechanical Engineering
Department of Salem College of Engineering and Technology, Salem, India.
He obtained his Bachelor in Mechanical Engineering from Bharathiyar
University, India. He obtained his Master in Production Engineering from
Annamalai University, India. He has 19 years of teaching experience. His
research interests include total productive maintenance, benchmarking and
quality function deployment.
1 Introduction
Modern organisations are trying hard to improve their overall performance to face the
ever increasing intensity of competition (Prashar, 2014; Natarajan et al., 2011a, 2011b).
While carrying out this task, modern organisations are striving to apply appropriate
strategies in all of their endeavours (Sugumaran et al., 2013; Cesarotti and Spada, 2009;
Vassilakis and Besseris, 2009; Ahuja and Khamba, 2008b; Pramod et al., 2008). One of
the strategies that has been finding wide and deep applications in modern organisations is
‘continuous quality improvement’ (Pramod and Devadasan, 2011; Pramod et al., 2010).
In order to deploy this strategy, organisations have been applying ‘total quality

238
K
. Srinivasan et al.
management (TQM)’ (Vassilakis and Besseris, 2009; Arca and Prado, 2008). While
applying TQM, organisations have adopted and applied numerous utilities under the
names ‘techniques’, ‘tools’, ‘methods’ and ‘systems’ (Sugumaran et al., 2013; Agus and
Hajinoor, 2012; Marksberry, 2012; Sankaran et al., 2008a, 2008b). Most of these utilities
have facilitated the modern organisations to achieve ‘continuous quality improvement’
(Sugumaran et al., 2013; Breja et al., 2011; Pramod and Devadasan, 2011; Ahmed and
Amagoh, 2010; Pramod et al., 2010, 2008; Cesarotti and Spada, 2009; Vassilakis and
Besseris, 2009; Ahuja and Khamba, 2008a). However, seldom these utilities have
enabled the organisations to achieve profitability. In order to bring out profitability
through the implementation of TQM, in Motorola, Six Sigma model was developed
(Jirasukprasert et al., 2014; Kumaravadivel and Natarajan, 2013; Chakraborty and Chuan,
2013).
Six Sigma concept facilitates to achieve nearly ‘zero defect manufacturing’ and
garner high profit (Kumaravadivel and Natarajan, 2013; Antony et al., 2012). Six Sigma
concept permits the organisations to make mistakes less than 3.4 defects per million
opportunities (DPMO). In order to achieve this goal, two approaches are followed. One is
that, the projects leading to the defect prevention are to be carried out in the organisation
by applying define, measure, analyse, improve and control (DMAIC) phases
(Jirasukprasert et al., 2014; Prashar, 2014; Kumaravadivel and Natarajan, 2013; Sarkar
et al., 2013; Antony et al., 2012; Cheng and Kuan, 2012; Mast and Lokkerbol, 2012;
Franchetti and Yanik, 2011; Roth and Franchetti, 2010). The other approach is the
imparting of formal training by assigning designations as champion, master black belt,
black belt, green belt and white belt (Chakraborty and Chuan, 2013; Marques et al., 2013;
Tjahjono et al., 2010; Kumar et al., 2008a) to the personnel. This method of imparting
formal training is also known as belt-based training infrastructure.
The capability of Six Sigma concept in facilitating organisations to garner high profit
attracted many quality managers. As a result, Six Sigma was first implemented in many
leading companies like general electric and allied signals (Jirasukprasert et al., 2014;
Chakraborty and Chuan, 2013; Pepper and Spedding, 2010). Today, Six Sigma is widely
applied in many parts of the world (Jirasukprasert et al., 2014; Kumaravadivel and
Natarajan, 2013; Chakraborty and Chuan, 2013). However, the conduct of belt-based
training is so expensive that it prevents the implementation of Six Sigma in the
companies with meagre revenue. In order to overcome this situation, during the recent
years, researchers and practitioners have been examining the way of implementing
DMAIC only to implement Six Sigma program in companies (Jirasukprasert et al., 2014).
Few researches dealing with the application of DMAIC in achieving the goals of Six
Sigma have been reported in literature arena. It is very prudent to study the nature and
outcome of these researches, as this study will be useful to evolve economical and
powerful DMAIC-based Six Sigma models. In order to fulfil this requirement, the
literature review reported in this paper was carried out.
2 Methodology
The literature review being reported here was carried out in three steps. In the first step,
the papers whose titles contain the phrase DMAIC were downloaded from the websites of
leading databases namely Emerald Insight (http://www.emeraldinsight.com), Science

Six Sigma through DMAIC phases 239
Direct (http://www.sciencedirect.com), Springerlink (http://www.springerlink.com) and
Taylor and Francis (http://www.tandf.co.uk). On overviewing these papers, it was
realised that DMAIC has been applied in three domains. In the first domain, the DMAIC
has been applied in manufacturing sectors (Jirasukprasert et al., 2014; Ghosh and Maiti,
2014; Kumaravadivel and Natarajan, 2013; Kumar et al., 2013; Kaushik et al., 2012;
Li et al., 2011; Kumar and Sosnoski, 2009; Chen et al., 2009; Lo et al., 2009; Tong et al.,
2004). In the second domain, the DMAIC has been applied in service sectors (Mayer,
2014; Yu and Ueng, 2012; Antony et al., 2012; Chen et al., 2012; Kumar, 2012; Southard
et al., 2012; Kumar et al., 2009, 2008a, 2008b). In the third domain, the DMAIC has been
applied in unconventional sectors (He et al., 2014; Franchetti and Yanik, 2011; Kaushik
and Khanduja, 2009; Yeh et al., 2007). In the second step of the literature review being
reported here, the above papers were segregated into three categories addressing the
researches on applying DMAIC under the above mentioned three domains. After that,
these papers were studied and extracts were drawn about applying DMAIC in the above
three domains. In the third step of the literature review being reported here, the
information and knowledge derived by studying these papers were used to identify future
direction of research. The details of these activities are presented in the following
sections of this paper.
3 Statistics
As mentioned earlier, before beginning the literature review being reported here, the
papers whose titles contained the phrase ‘DMAIC’ were gathered. Twenty-three such
papers containing DMAIC in the titles could be identified. This number is very small
compared to the large number of papers reporting the researches on Six Sigma that have
been reported in the literature arena (Antony and Desai, 2009). As mentioned in the
previous section, these papers were classified under the three domains in which the
implementation of DMAIC is addressed. The statistics of these three categories of papers
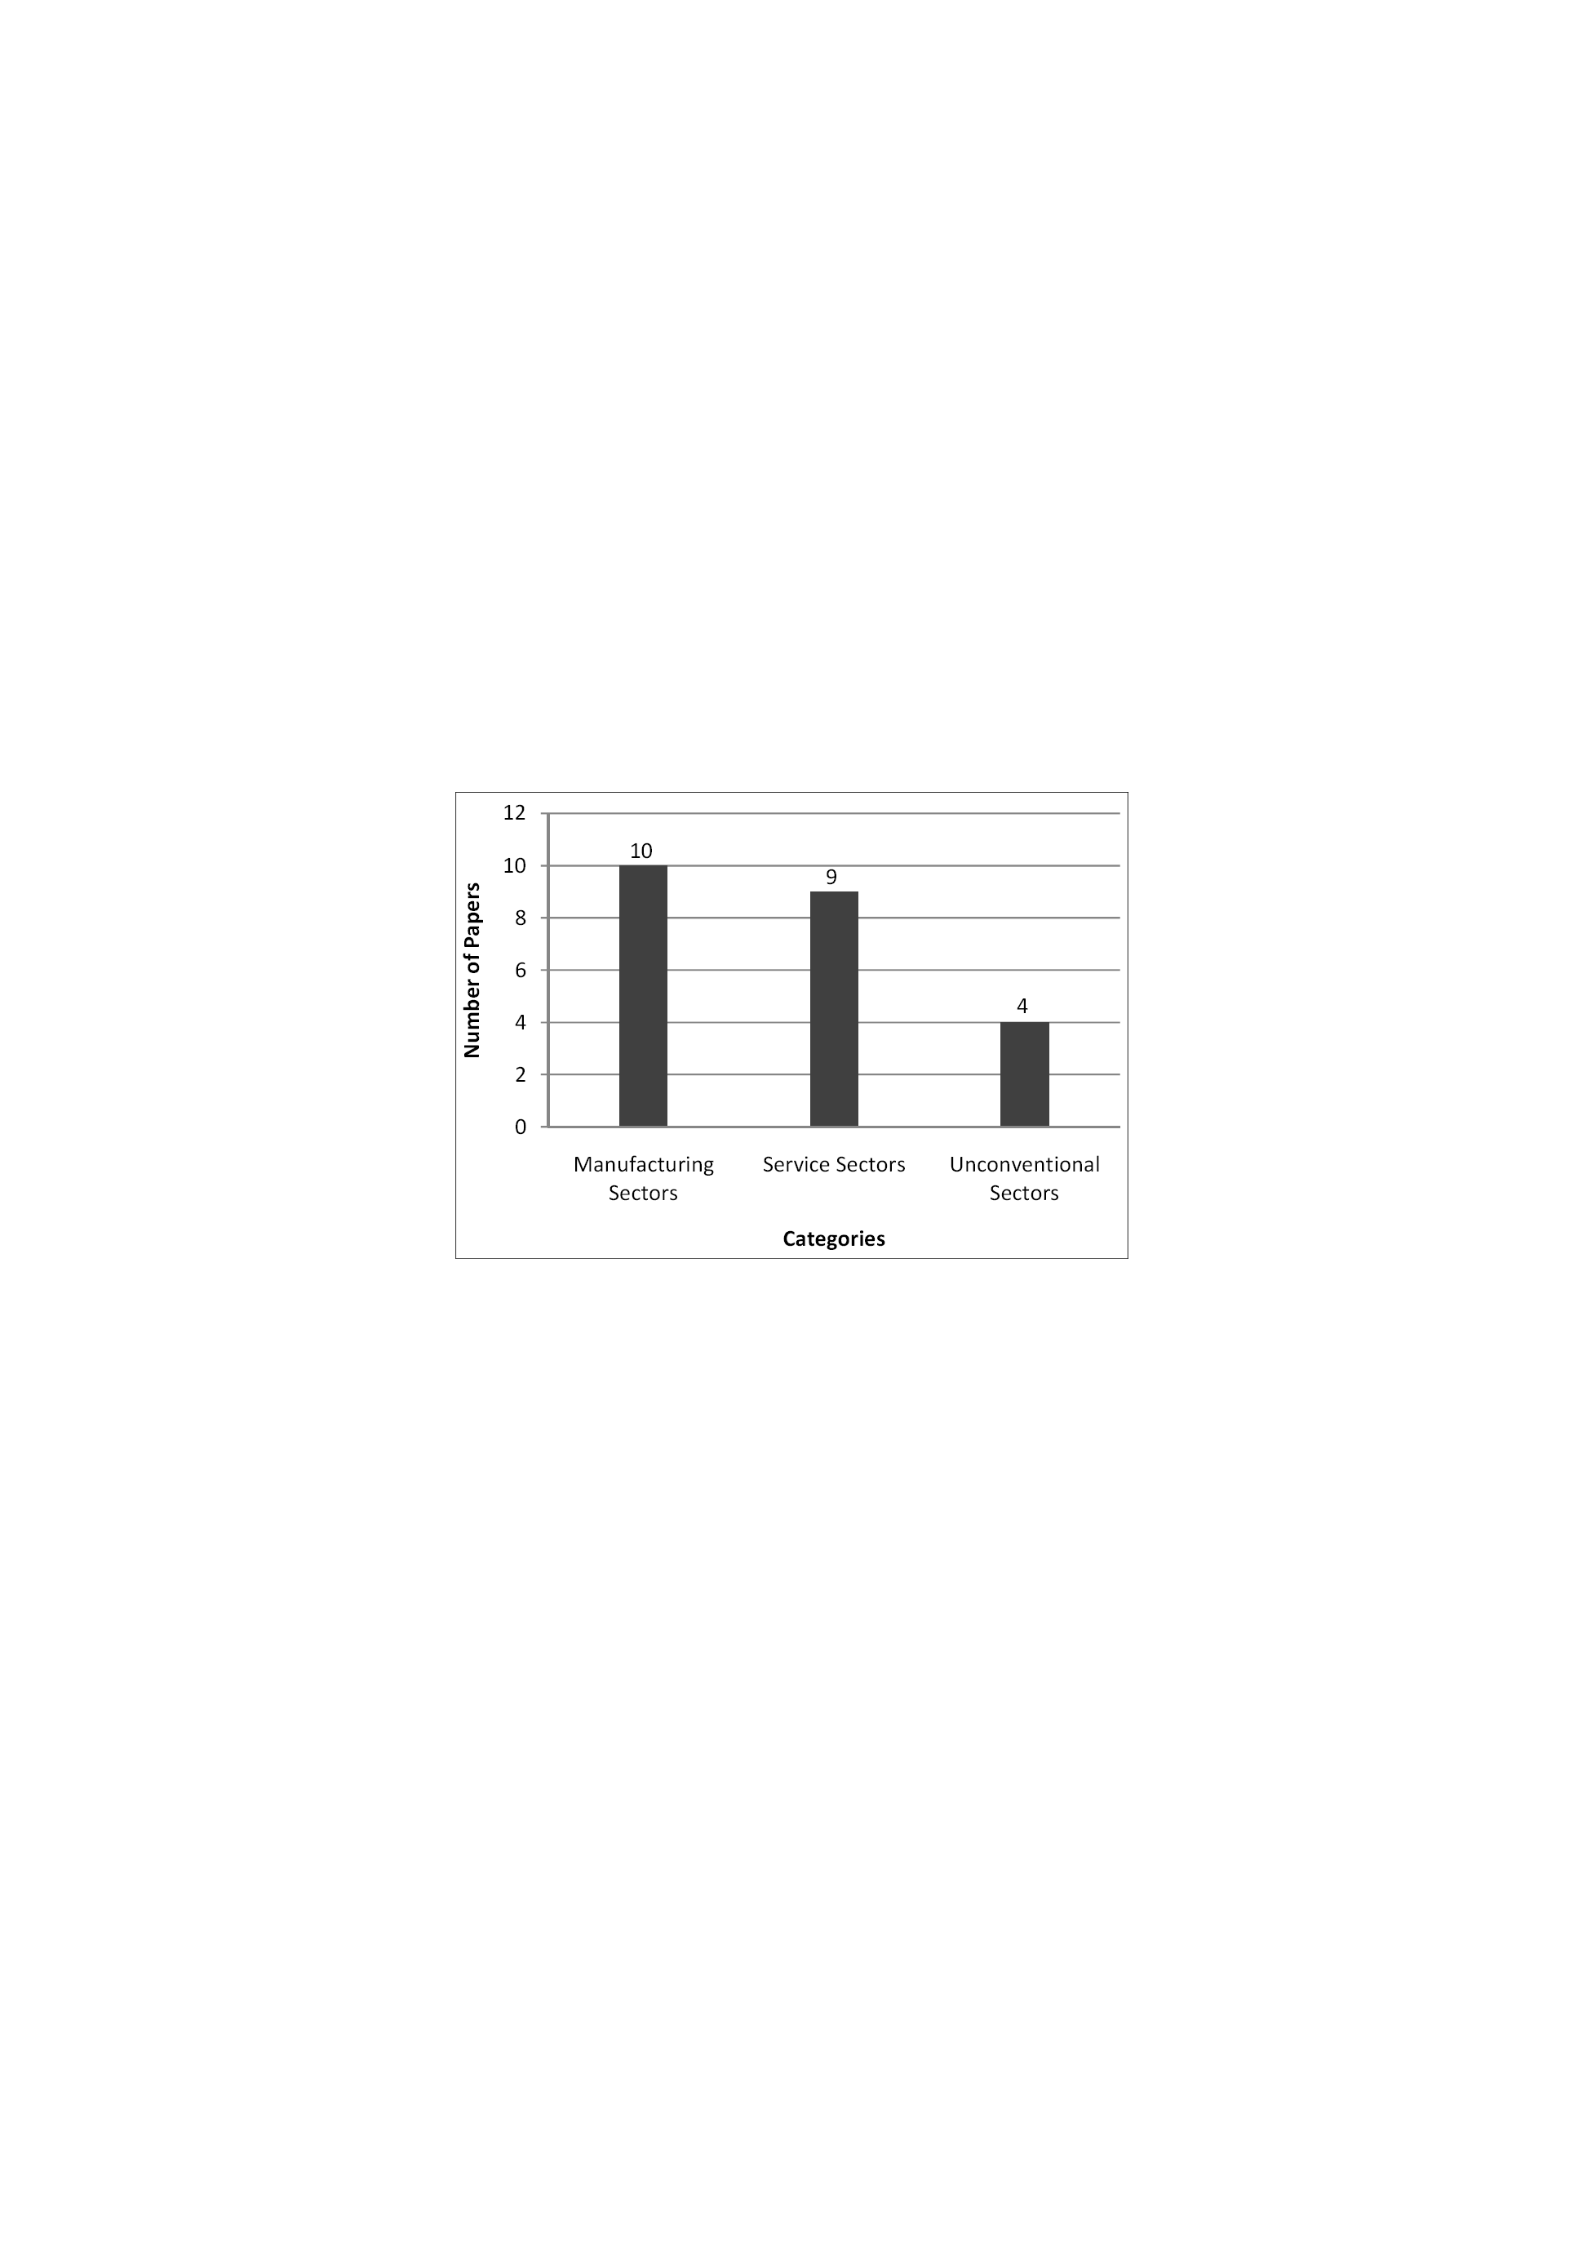
is shown in Figure 1. As shown, nearly equal number of papers reporting the applications
of DMAIC in manufacturing and service sectors have appeared in the literature arena.
Little less than half the number of papers reporting the application of DMAIC in
unconventional sectors have appeared. The information and knowledge gathered by
reviewing these papers have been described in the following three sections.
4 DMAIC in manufacturing sectors
As shown in Figure 1, ten papers reporting the application of DMAIC in manufacturing
sector were reviewed during the literature review being reported here. The extracts
derived by conducting this literature review are presented in this section.
Jirasukprasert et al. (2014) reported the implementation of DMAIC methodology for
reducing defects in rubber gloves manufacturing process. In define phase, the problem
was identified. This problem was that, a large amount of rubber gloves had been rejected
by the customers due to defective gloves. In measure phase, the defects were measured,
and the gloves that more leaking and dirty were identified. Furthermore, the Pareto
240
K
. Srinivasan et al.
analysis was carried out to identify the complaints that were most frequently reported by
the customers. The present level of sigma was found to be 2.4 with 1,95,095 DPMO. In
analyse phase, ‘oven’s temperature’ and ‘conveyor speed’ were identified as the critical
to quality (CTQ) parameters of manufacturing gloves. In improve phase, the design of
experiment (DOE) was conducted to identify the best oven’s temperature and the best
conveyor speed. The analysis of the results of these experiments indicated that, the best
oven’s temperature would be 230°C and best conveyor speed would be 650 rpm. In the
control phase, the trial run was conducted with best values of the CTQ parameters. As a
result of applying the best values of CTQ parameters in the manufacturing of gloves, the
quantity of gloves leaking was reduced by 50%. The reduction of DPMO was achieved
from 1,95,095 to 83,750, and sigma level improvement from 2.4 to 2.9 was observed.
Figure 1 Statistics of papers reporting researches on DMAIC
Ghosh and Maiti (2014) proposed a data mining driven DMAIC framework for
improving quality of the casting of six-cylinder engine head. During the define phase, it
was found that, the rejection and rework of the casting of six-cylinder engine head were
more than 20%. The company set the objective to reduce the total defect rate by these
castings to less than 5% within six months. A process map was drawn to identify the
influential factors. During the measure phase, the cost of poor quality (COPQ) was
calculated to estimate the impact of casting defects on business profit. This estimation
revealed that, the annual extrapolated total COPQ was more than Indian National Rupees
(INR) 31 million (US $0.54 million). Pareto chart was drawn to identify the major
defects. The study of this chart revealed that, results of 80% of rejections were caused
due to gas porosity. Further, the conducting of brainstorming sessions indicated that, gas
defects originated from four functions namely
1 core making
2 wash application
3 melting and pouring
4 gating and venting.

Six Sigma through DMAIC phases 241
In analysis phase, two data mining-based tools called ‘classification and regression tree’
(CART) and ‘chi-squared automatic interaction and detection’ (CHAID) were applied to
identify the most significant factors causing gas defects in casting. Four parameters
namely
1 horizontal drill vents
2 pouring temperature
3 zircon wash source
4 core sand type
were found to be influencing the most on the gas defect generation. In improve phase,
remedial actions were determined. The recommendations were made to
1 use zircon wash source B
2 use coarser core sand
3 apply pouring temperature between 1,445°C and 1,450°C
4 run the process without horizontal drill vents.
In control phase, the continuous monitoring of processing stage was carried out for
15 days to identify the process behaviour after the actions were taken. It was observed
that, the gas defect has been reduced significantly. The annual savings were calculated to
be INR 16 million (US $0.28 million).
Kumaravadivel and Natarajan (2013) carried out a research to reduce the defects
while manufacturing the casting of flywheel by using DMAIC methodology. The tools
used during the pursuance of this research were process map, cause and effect diagram
and failure mode effect analysis (FMEA). The influential factors which cause the defects
in the casting process were found to be the moisture content, green strength, permeability
and loss of ignition. These factors were analysed by using the response surface
methodology (RSM) technique. The primary objective of pursuing this research was to
reduce the unhidden waste and improve the quality by examining the human as well as
the technical factors. During the define phase, it was found that, 6.94% of the casting of
the flywheels manufactured were rejected. The reasons for rejecting these castings were
attributed to sand inclusions, blow holes and slag. In measure phase, the supplier, input,
process, output and customer (SIPOC) diagram was drawn to map the flywheel
casting process. Subsequently, voice of customer (VOC) was applied to identify CTQ
parameters. The intensiveness of these CTQ parameters was checked by considering
these variables under the names ‘key process input variables’ (KPIV) and ‘key process
output variables’ (KPOV). At the end of this phase, Pareto diagram was drawn. This
diagram indicated that, blow holes, slag and sand inclusion caused 24, 36 and 40% of
defects respectively in the total defects in the casting of the flywheel. These three defects
were considered for overcoming the same and improving the quality of flywheel casting
process. During this phase, the sigma value was found to be 3.49. During analyse phase,
cause and effect matrix, FMEA and cause and effect diagram were used to identify KPIV
and KPOV against the selected CTQ parameters. During the execution of improve phase,
RSM and analysis of variance (ANOVA) were applied to determine the solutions for
achieving quality improvement of flywheel casting process. At the end of executing this
phase, 15 remedial actions were suggested to improve the quality of flywheel casting
242
K
. Srinivasan et al.
process. In improve phase, the significant factors were controlled by using the RSM to
make the process as robust as possible. In the control phase, the solutions evolved in the
previous phase were applied in practice. This application resulted in the decreasing of the
rejection level from 6.94% to 4.69% and increase in the sigma level from 3.49 to 3.65.
Kumar et al. (2013) investigated the DMAIC approach in reducing the variation and
increasing the sigma level of the casting process in the foundry. In define phase, the
defects currently occurring in the foundry were determined through VOC. The CTQ was
evaluated by using VOC, process flow diagram and brainstorming technique. In measure
phase, the current sigma level of the casting process in the foundry was found to be 3.18.
The objective was to increase the sigma level of the process by reducing the occurrence
of the defects by carrying out this research. In the analysis phase, the data collected from
the different treatment conditions as fixed by making use of the orthogonal array (OA)
have been analysed by using the Taguchi’s parameter design approach. In improve phase,
the factors that influence the occurrence of the casting defects were identified. Then, the
corresponding signal to noise ratio for all the trial runs were calculated. In the control
phase, the optimal factors and levels were maintained consistently by generating the
control plan for the optimal factors and levels to control the variation within the
confidence interval. Overall, by pursuing this research, the efficiency and performance of
the casting process in the foundry were increased by using the DMAIC approach.
Kaushik et al. (2012) reported that, the implementation of Six Sigma methodology in
small and medium-sized enterprise (SME) by using DMAIC as a tool to control the
variation in the processing stages of the product. The DMAIC methodology was applied
to solve the high rejection of bushes in bi-cycle chain assembly. In define phase, process
map and a SIPOC diagram were developed to document the manufacturing sequence of
bush and to identify the process or product for achieving improvement. In measure phase,
gauge ‘repeatability and reproducibility’ (R and R) was conducted to ensure that, the
measurement system is statistically sound. The result of this study indicated that, the
micrometer used was facilitating accurate measurement values. In the analysis phase, the
data gathered during the measure phase were analysed to identify the basic cause of the
major rejection of bushes. The process capability chart was drawn by grouping up the
samples into five. The sigma level was found to be 1.4. In order to increase the sigma
level, the cause and effect diagram was used to identify the causes and CTQ which
caused the rejection of the bushes. In improve phase, the two CTQs were considered to
design 2 × 2 DOE, which was conducted for two replications. In control phase, the X/R
chart was plotted by making the trial runs with a sample size 100. The results shown in
this chart indicated that, the process was within the control limit. After the
implementation of DMAIC phases in this bicycle manufacturing unit, the sigma level
increased from 1.40 to 5.46. In the end, the application of DMAIC in this company gave
rise to the annual monetary savings of INR 0.288 million.
Li et al. (2011) reported the application of DMAIC methodology for improving the
efficiency of information technology (IT) help desk service quality through eHelp-desk
system of the Compal Company in Taiwan. In define phase, it was found that, the IT help
desk system needed improvement since the average processing time was as high as
168 minutes, and also the processors were unable to handle the multiple requests at a
time. In measure phase, it was measured that, 74% of the processing time accounted for
the data transfer through personal computer (PC), electronic network and e-mail. The
SIPOC diagram was drawn to determine the time between the submission of the request

Six Sigma through DMAIC phases 243
by the users and processing of the requests by the helpdesk. From the process capability
chart, it was found that, the current sigma level of the company was 0.84. In analyse
phase, it was confirmed that the waiting time accounted for 79% of the total processing
time. In improve phase, the solution conception (eHelp-desk system) was developed by
using the cause and effect diagram. The eHelp-desk system was generated and
implemented. In control phase, the performance of the IT help-desk system was assessed
by drawing data by supplying a questionnaire among the users. The eHelp-desk system
showed a drastic improvement in sigma level from 0.84 to 2.07. The waiting time was
reduced from 131 to 71 minutes and also the monetary savings of New Taiwan Dollars
(NTD) 26,856 per month was achieved.
Chen et al. (2009) have reported a research in which, DMAIC phases were applied to
determine the optimum process parameters while using the plasma-cutting machine. This
research was conducted in an electrical switchboard manufacturing company. In define
phase, brainstorming sessions were conducted to investigate the deviations encountered
in the process of making hole by using the plasma-cutting machine. It was found out that,
deviations in the bevelling and roundness in the hole were the bottlenecks that prevented
the hardware to fit the switchboard. All possible causes of making defective holes while
using plasma cutting machine were depicted in cause and effect diagram. In measure and
analysis phases, the Taguchi experiments were carried out to evolve solutions for
preventing the occurrence of bevel and smallest diameter deviations. The optimum values
of the parameters were found out. Subsequently, response graphs were drawn. Then t-test
was conducted. Using this test, the significance of the factors was examined. In improve
phase, a confirmation test was conducted by applying the solutions evolved in the
previous phase. The examination of the holes cut by applying these solutions indicated
that, the bevelness and roundness deviation fell within the admissible levels. In control
phase, the details of parameters and their optimum values were informed to the
production department of the company. The Six Sigma team of this department was
required to apply these values in real time practice. If necessary, the real-time Taguchi
experiments would have to be conducted further to reduce bevelness and roundness
deviations.
Kumar and Sosnoski (2009) have concentrated on reducing the amount of the warp
incurred in the Amada-A station punches during the heat treatment process by applying
DMAIC phases. In define phase, Pareto analysis was conducted to identify the defects
occurred in punches. This analysis indicated that, the occurrence of warped parts was a
major problem to be overcome. After identification of the problem, the project charter
containing problem statement and project objective statement was developed. In measure
phase, the process capability analysis, descriptive statistics and histogram were used to
determine the present quality levels. Particularly, during this phase, the defects per
million were determined as 1,350. In the analysis phase, cause and effect diagram was
drawn to depict CTQs and the causes of the warp forming in the punches. In improve
phase, the common and special causes were differentiated. Further, their interactions
between the factors were determined. This differentiation facilitated the redesigning of
fixture to eliminate the warp formation in the punches. In the control phase, the hanging
parts were produced using the newly designed punches. In some cases, warpage was still
prevalent on using the newly designed punches. However, the quantum of warpage
encountered was less compared to those that are currently occurring. The cost saving due
to the reduction of the occurrence of the warp formation on using the new fixture was
estimated to be two million dollars.
244
K
. Srinivasan et al.
Lo et al. (2009) reported the implementation of DMAIC approach for improving the
quality of injection-moulded optical lenses. In define phase, the surface performance
quality of lenses were identified. The optical performances of the systems are based on
the image forming capability of an optical system. The actual image of an object is
compared with the ideal image (referred to as image forming capability). In measure
phase, the process capability index was calculated by referring to the surface contour
measurement data to identify the most significant characteristics of moulded lenses. The
surface precision using ‘waviness or peak-to-valley’ (PV) value was measured in the
moulded lenses. In the analysis phase, the data were analysed. Because of poor PV
values, the lens was thicker at its centre. The cause and effect diagram was drawn to
depict the significant processing parameters namely melt temperature, screw speed,
injection speed, injection pressure, packing time, mould temperature and cooling time.
The Taguchi method of DOE was conducted for identifying the most significant
parameters with the corresponding optimal combinations. The objective was to minimise
the waviness of lenses based upon the optimal conditions. In improve phase, the optimal
parameters were implemented and as a result, the capability index enhanced from 0.57 to
1.75, and the Six Sigma target was achieved. In the control phase, the continuous pursuit
for determining the optimal combinations was illustrated with the help of control plan
and consistently monitoring the process capability to retain the fruitful improvement in
the mould shop.
Tong et al. (2004) presented a case study in which the quality of printed circuit board
(PCB) was improved by applying the DMAIC approach. In define phase, the solder paste
volume (height) on the solder pads of the screening process was identified as CTQ
characteristic. In measure phase, the Cyberoptics Cybersentry system was used to
measure the solder paste height on five PCBs for every four hours. Subsequently, the
solder paste height data were recorded in the statistical process control (SPC) data record
sheet by the operators. Further, X-R control chart was plotted. In analyse phase, the
process capability for solder paste height in all six semi-automatic screening machines
was analysed against the current printing performance. In improve phase, DOE was
conducted to determine the optimal settings of all CTQ factors in the screening process.
The parameters considered while conducting DOE were solder paste viscosity, speed of
squeegee, pressure of the squeegee, age of stencil, solder paste volume, blade type and
side of the stencil. In the control phase, the control strategies were recommended to
sustain the improvement of the sigma level in the screening process. The sigma level of
the screening process could be improved from 1.162 to 5.924. Thus, the Six Sigma level
was nearly achieved.
On the whole, the authors of the above papers have claimed that the application of
DMAIC resulted in an increase of sigma values in the performance of the manufacturing
companies in which case studies have been conducted. Some authors have also pointed
out that, DMAIC application facilitates to achieve substantial financial savings.
5 DMAIC in service sectors
As shown in Figure 1, nine papers reporting the application of DMAIC in service sectors
could be overcome during the literature review being reported here. The extracts derived
by reviewing these papers are presented in this section.

Six Sigma through DMAIC phases 245
Mayer (2014) reported a case study to report the achievement of the increase in
efficiency and reduction in the instructor time spent while conducting patient education
classes through the implementation of DMAIC approach in healthcare. In define phase,
the project team was set up to identify the goal and business needs. The objective was to
increase the number of patients attending each class session and reduce the number of
class sessions taught. The topics covered in the classes were temporomandibular disorder
(TMD), blood pressure and chronic kidney disease stage 4 (CKD4). The stakeholders
were the resource centre’s administrators, management personnel, instructor team,
resource centre staff, patients and healthcare providers. The project team interviewed
several patients and gathered data to assess the patients’ satisfactory level. During the
measure phase, it was found out that, the class attendance formed a baseline record for
gathering data regarding the number of patients attended along with class sessions held
for the past three quarters prior to interviewing the patients. In analyse phase, the project
team was asked to assess the processing stages to identify the factors that cause decreased
satisfaction or quality of service offered. The project team analysed the viability
of performing small group teaching on each class topic by considering patient
confidentiality, diagnosis and difficulties on combining the patients. The project team
also investigated the hurdles of combining patients of different categories and that the
sessions which are not fruitful due to the delivery of inappropriate lectures. The project
team called the experts to train the instructors for handling small group teaching to
overcome these deficiencies. The team investigated the woes faced by conducting small
group teaching due to provider referral. The team continuously monitored the classes and
realised that, a small group teaching was ineffective in moving forward the individual
sessions. In improve phase, the action was taken to change the scheduling rules for TMD,
CKD4 and blood pressure class sessions to allow more than one patient for registration.
The project team also monitored the class sessions and data about the participants over
second and third quarters of 2012. In control phase, the project team found out that, the
group teaching on CKD4 class sessions was ineffective. Hence, CKD4 class session had
to be changed to adopt individual teaching procedure. Thus, the project team could not
find the right path to perform small group teaching.
Yu and Ueng (2012) proposed a case study on embarking the teaching effectiveness
in higher educational institutions (HEIs) by applying DMAIC phases. In define phase, the
stakeholders and experts created a list of valid attributes to form a questionnaire that
would facilitate to find out the attributes which are said to be vital for evaluating the
instructors’ teaching performance. In measure phase, teaching performance indicator
(TPI) was proposed to measure the performance of each attribute by evaluating the
questionnaire using the five-point Likert’s scale. The imperative and influential attributes
were niched through importance rating to identify the satisfaction level among students
and instructors. In analyse phase, a modified approach of importance performance
analysis (IPA) called teaching effectiveness analysis matrix (TEAM) was used to
evaluate the teaching performance level that met the HEIs’ expectation level (HEIs’
expectation level is 0.80). The possible factors causing the teaching problems were
identified through cause and effect diagram that had high importance rating on teaching
effectiveness in HEI. In improve phase, a number of improvement methods were
suggested against the identified factors to achieve higher teaching effectiveness in the
selected school. In control phase, the effectiveness of these improvements was verified
over a period after execution of improvement actions. The verification revealed the

246
K
. Srinivasan et al.
achievement of the improvements by making use of the documented standard operating
procedures to sustain the teaching effectiveness in HEI.
Antony et al. (2012) investigated and streamlined the communication and information
management (CIM) system by using the DMAIC phases of Six Sigma methodology in an
infrastructure support company to increase the quality of service. In define phase, the
major processes and the customer requirement were identified by using the Six Sigma
tools namely the SIPOC, VOC and affinity diagram. The SIPOC was used to identify the
basic relationship between the processing stages namely the supplier, input, process,
output and customer. The VOC data were collected from the employees, and the same
were analysed to check whether the requirements of the customer were satisfied, and the
flaws in the process were reduced. The affinity diagram was used to convert the
unstructured data into the structured ones to identify the solution for the problem. In
measure phase, the major KPOV were identified based on which the gauge R and R study
was conducted. The initial step started with the identification of defects in the process by
constructing the CTQ tree and conducting the VOC analysis. The major metrics
identified while constructing the CTQ tree were completeness, correctness and
timeliness. Based on the collected data, the Pareto chart was drawn to identify the major
factors which impacted the CTQ factors. The correctness and completeness of the CIM
system were the major CTQ factors. In the analysis phase, the data that were collected
from the previous phase were identified, and the same were analysed to identify the
causes. The cause and effect diagram was plotted to depict the causes under the title, data,
communication methods, measurements and people. These causes were identified by
conducting brainstorming sessions and applying the multi-voting methodology. Survey
was conducted among the 30 internal employees in the concern, and the corresponding
ratings were given by making use of the Likert’s scale. In improve phase, the solution for
the problem was identified by deriving the information from the previous measure and
analysis phases. This exercise was started with the mapping of the process flow by which
the non-value adding activities were removed to make the process effective. Further, it
was suggested to effect centralised information flow and automation in CIM system. In
the control phase, the vital steps were considered to standardise, monitor and integrate the
changes. In order to carry out this task, standard operating procedures (SOP) were
developed. Further, the control charts were drawn to control the deviation in the future.
Chen et al. (2012) conducted a study on the usage of credit card in Taiwan. The
objective was to reduce the financial risk involved during the registration of the credit
card review process along with the identification of the normal and the default customers
by using DMAIC methodology. In define phase, the major concern faced by the banking
industry during the credit card review process was identified using the decision tree. The
details of the customer were collected from customer relationship management (CRM)
desk and analysed to identify the current trend in the banking industry along with the
differentiation of normal and the faulty customers. In measure phase, the data were
collected from different banks about the credit card review process. The rules were
created for collecting data, which were to be precised, completed and correlated. These
data were used for identifying the normal and the faulty customers. In the analysis phase,
the credit card basic data variable chart was developed, and the questionnaires were
included in the chart. The feedback from the chart was evaluated by using the three
models namely ‘non-group’, ‘the training and testing group’ and ‘the crossover group’.
Initially, the evaluation was carried out by using the non-group model to plot the decision
tree which indicated optimal data at each and every point of the credit card review

Six Sigma through DMAIC phases 247
process whose accuracy level was above 75%. In improve phase, the cross-over
evaluation was carried out on the feedback by referring to the variable chart for finding
the degree of correlation between the nodes of the tree. The results of the decision tree
were framed as the rules that were followed to identify the normal and the faulty
customers. In this case, the following findings were made:
• high yearly income persons had the consistent and robust repaying capabilities than
the low-income people
• females had lower bad debt ratio than males
• the old persons had less desirability over the credit card compared to young people
and students
• married persons had less desirability over bachelors
• the persons with high educational background had higher repaying capability.
In the control phase, the decision tree rules were followed to find the differentiation
between the normal and the faulty customers.
Kumar (2012) reported the application of DMAIC in preventing disruptions occurring
due to the avian flu on global operations. Wal-Mart (retail sector) and Dell computers
(manufacturing sector) supply chain systems were selected for this study. In define phase,
the products were delivered to Wal-Mart from Asia and China. The avian flu began
spreading from China to Hong Kong, Canada, Africa, Asia and Europe. In measure
phase, disruptions that occurred due to the avian flu in the supply chain process were
measured. A situation analysis was conducted by using Decision Focus software on
disruptions that occurred due to the avian flu in Wal-Mart and Dell computers supply
chain. This process is a tool to solve issues that are broad and complex and has multiple
causes and effects that cannot be resolved by carrying out one action. In the analysis
phase, FMEA was used to manage supply chain risk. The result of conducting FMEA
indicated that, failures were wider if risks were not managed effectively. Dell computer’s
and Wal-Mart’s supply chains were examined by conducting FMEA. In improve phase,
the measures were proposed for supply chain improvements. These measures are listed as
follows:
• continuous operation plan reviewing and carrying out vendor capability assessments
• defining preventive measures in an operational action plan
• ensuring business continuity in case of epidemic problem
• drawing better practices from experts and other business firms
• encouraging the trust and openness culture
• educating to understand the symptoms and risks
• educating to acquire preparedness talent for facing emergency
• encouraging the trust and implementing better public health policies in workplaces
In control phase, the control measures were recommended as follows:
• continuous monitoring and identification of infected members

248
K
. Srinivasan et al.
• sending of infected members to their homes
• encouraging teleconferences and avoiding direct meetings
• encouraging employees’ hygienic state
• introducing electronic transfers and avoiding document transfers
• vaccination of employees, suppliers and distributors.
Southard et al. (2012) reported a case study involving the application of radio frequency
identification (RFID) in healthcare through DMAIC phases. In define phase, the CTQ
parameters were identified. These CTQ parameters were ‘identification of the patients’
and ‘availability of the facilities’. In measure phase, cycle time of individual tasks,
overall throughput time of the process, cost of providing the procedures, utilisation of the
resources and reduction in errors in the existing system were measured. The current state
of value stream map (VSM) was also analysed. The problems were identified as improper
procedures and sterilisation which occurred prior to, during, and between surgeries. It
was aimed to overcome these problems by achieving process improvement using RFID
technology. In the analysis phase, the way of incorporating RFID in order to improve the
system was examined. Simulation model was developed to analyse the incorporation of
RFID. The focus in this study was to estimate the difference in overall time and costs
associated with and without RFID in the healthcare system. In improve phase, the
theoretical implementation of RFID to the process under study was investigated by
simulating those processes as if that technology were in place. The model with RFID
showed the potential to improve the performance of the outpatient surgical system. The
improved VSM was developed to eliminate non-value added activities. In the control
phase, policies and procedures to be put in place to achieve improvements were created.
It was emphasised that, the process must be continuously monitored and maintained to
retain the improved state. In the end, it was estimated that, annual cost savings would be
$1.93 million if the model with RFID was implemented.
Kumar et al. (2009) conducted a study on summer lodging operation and analysed the
service system in hotel industry. The objective was consistent to deliver high quality
service with improvised customer satisfaction by using the Six Sigma tools like service
blueprint, service quality (SERVQUAL), cause and effect diagram and Poka-yokes. In
define phase, the service blueprint was prepared for the whole process covering the entry
and exit of the customer during the business and non-business hours. The major problems
were that, the unavailability of lodging staff to greet and accommodate the customer and
also the unavailability of receptionist during the time of customer calling for a
reservation. In measure phase, these problems were evaluated by using the SERVQUAL
by obtaining the feedback from the customers. The questionnaires were prepared to
gather the expectation and perception of the information under the five main attributes
namely tangibles, responsiveness, reliability, assurance, and empathy. These attributes
were weighed according to the feedback received from an external customer. The sorting
was performed based on the feedback by using the gap score methodology. In analysis
phase, the major factors which impacted the reservation system and the customer
perception during the check-in and checkout in the lodging were identified. Initially, the
cause and effect diagram was drawn pertaining to the inferior customer service which
indicated the major causes as delinking of reservation system with online booking engine
and detracting of the customer preferences in the reservation section. In improve phase,

Six Sigma through DMAIC phases 249
the online booking engine was introduced. The customer got their room reserved any
time during the day along with the recruitment of well trained persons to serve the
customers throughout their stay of time in the lodge. The working hours of the employees
with high perks and incentives were slightly increased for offering better service to the
customer. Further, the renovated blueprint was introduced in the reservation system along
with the customer services and preferences with the effective Poka-yokes in lodging for
achieving the customer satisfaction. In the control phase, the control plan, and SOPs were
generated to highly satisfy the customers while performing the reservation. Greetings of
the customer during their stay in lodging will gradually increase the sigma level in the
retail and leisure business.
Kumar et al. (2008a) proposed the improved service system design for the Best Buy
(a major consumer electronics and appliance retailer) using DMAIC approach in the
USA. The competitors to Best Buy are Wal-Mart, Costco and Circuit City. The products
sold by the Best Buy are electronic gadgets, movies, music, computers and electronic
appliances. Best Buy tries to differentiate from its competitor through offering higher
quality service to its customer. In order to improve its service, Best Buy conducted the
SERVQUAL survey to identify the areas lacking quality. In define phase, the ‘customers
and their priorities’, ‘customers’ need and feedback’ and CTQ characteristics that the
customer considered having the highest impact on quality were identified. In measure
phase, the processes and their performances were measured. The internal processes that
influence CTQs were identified, and the defects related to the processes were measured.
In analyse phase, the causes of the defects were determined and the variables that create
the process variation were identified. In improve phase, the methods to remove the cause
of defects, that cause the significant variation and their effects on the CTQs were
identified. The maximum acceptance ranges of the significant variables, a system for
measuring deviations of variables and modifying the process to stay within the acceptable
ranges were identified. In the control phase, the improvements to ensure the key variables
remain within the maximum acceptance ranges under the modified process were
sustained. The improved process will allow Best Buy to provide their customer with
reliable service and also retain the customers’ trust. It will attract the subsidiary of Best
Buy namely Geek Squad to gain more market shares in the electronics repair and
installation service industry.
Kumar et al. (2008b) analysed the credit card initiation in the financial industry by
applying DMAIC phases. The objective of this research was to increase the effectiveness
of the credit card initiation process by reducing the lead time of the approval from
20 days to the period of 15 days. In define phase, the major problems faced while
underwriting of the midmarket customers by the credit card initiation team in the
payment system unit division were defined. In measure phase, the one-shot diagram of
the credit card initiation process was plotted by using the previous five months data
drawn from the company database. The number of days required for a credit card
initiation process against all the mid-market requests in the financial services operation
was identified. In the analysis phase, the data collected from the previous phase were
analysed and picturised with the help of a bar chart. Out of 442 requests, nearly 190
requests took the lead time more than 20 days that should be reduced to 15 days. The
cause and effect diagram was drawn to depict the major causes. The sales team and
‘underwriting and approval team’ were found to play key roles in ensuring credit card
responses. In improve phase, the cause and effect diagram was drawn to depict the
failures that may occur in sales and approval stages. Subsequently, the Poka-yokes were

250
K
. Srinivasan et al.
recommended and implemented to overcome all the failures in the financial operations.
In the control phase, the changes were made in the processing stages of the sales
department. Furthermore, the direct review meetings were held with the sales manager
and credit manager to reduce the lead time in the credit initiation process in the financial
concern.
On the whole, the researches reported in the above papers have confirmed that,
DMAIC is a promising model for implementing Six Sigma in companies offering service
to the customers. Most of the authors of the above papers have presented models for
applying DMAIC in the service sector to appropriately utilise the tools of Six Sigma.
6 DMAIC in unconventional sectors
As shown in Figure 1, during the literature review being reported here, four papers
reporting the application of DMAIC in unconventional sectors could be encountered. The
extracts drawn by reviewing these papers are presented in this section.
He et al. (2014) reported a case study on reducing the voluntary turnover rate of
dispatched employees by using DMAIC methodology in a company situated in China. In
define phase, the project team consisting of employees from human resource (HR),
production planning and manufacturing department was formed. This team conducted a
survey and found that many dispatched employees were not satisfied with the salary,
frequent change of work schedules and obscure futures. This team set its goal as to
reduce the turnover rate from 2.5% to 1.5%. In measure phase, the team gathered the data
required for establishing the baseline of the project. The questionnaire was developed by
modifying Price’s causal model and weighing through a five-point Likert’s scale.
Measurement system analysis (MSA) was carried out to evaluate the quality and
reliability of data collected for finding the key factors of voluntary turnover. In analyse
phase, these factors were analysed and ranked through partial correlation analysis. The
results of this analysis revealed that, the salary and benefits were the most important
factors that affect the dispatched employees’ retention will. Converting opportunity and
job hunting were also the key factors influencing turnover. In improve phase, salary and
benefits, converting opportunities, rotation system, career development, training and
human care were found to be the significant factors for achieving improvement.
Brainstorming and mind mapping were conducted to choose the best solution for
reducing the turnover. The team suggested and implemented the increase of salary by
12.5%, increase of the converting number by 30%, military and regular training, regular
sports activity, offering of birthday and festival gifts. A pilot run was conducted, and its
results showed a drastic decrease in turnover rate from 2.5% to 1.4% and also the gaining
of considerable savings in recruiting and training costs. In control phase, the project team
provided the necessary suggestions to sustain the achieved improvement by continuous
monitoring of the same.
Franchetti and Yanik (2011) reported the implementation of lean DMAIC Six Sigma
approach in a company to reduce costs and achieve continuous improvement. In define
phase, the objective was set to increase the capacity by 10% and reduce the cost by 15%
by employing brainstorming technique, conducting the CTQ analysis and defining the
scope. In measure phase, the SIPOC diagram was drawn to measure the manufacturing
capacity and operating costs to establish the Six Sigma metrics namely the process cycle
time, weekly operating costs, value addition and material handling flows/costs. In

Six Sigma through DMAIC phases 251
analysis phase, the data collected from the previous phase was evaluated by using the Six
Sigma tools namely VSM, Pareto analysis, root cause analysis and FMEA to identify the
significant factors which influenced the CTQ. Pareto analysis was conducted to
determine the largest contributors to cost overruns. This analysis indicated that, over 60%
of the problems occurred due to the lack of standard procedures and monitoring
mechanisms. 30% of the problems occurred due to the inefficiency of the existing layout.
The FMEA was conducted to identify the major failure modes, potential effects, severity,
occurrences and detection. The CTQs were analysed and listed by referring to the risk
priority number (RPN) rating. In improve phase, the improvement proposals were
suggested. These proposals included the implementation of supermarket and Kanban,
rationalisation of the layout, monitoring the labour utilisation, standardisation and
documentation of all processes through the conduct of brainstorming sessions.
Furthermore, the computerised relative allocation facility technique (CRAFT) was
employed to design new layouts to reduce the cost. In control phase, the system was
developed to monitor and sustain the improvement proposals. The improvements were
achieved through the development of SOP, training and daily progress tracking of all the
employees in the facility. The log books were maintained in the work centre to record the
key metrics. After the implementation of the improvement proposals, the sigma level
increased and the operating cost of the process reduced steeply.
Kaushik and Khanduja (2009) reported the application of DMAIC approach in a
thermal power plant. In define phase, the objective was to eliminate the unwanted usage
of demineralised (DM) water in the thermal power plant that will increase the expenses.
The reduction of consumption of DM water in thermal power plant was selected as CTQ.
Furthermore, a process map was drawn for DM water consumption to define the
customer requirements and identify the project goals. In measure phase, the DM water
flow was measured using a flow meter. A gauge R and R study was carried out by using
another flow meter. In the analysis phase, based on the data collected using the flow
meter, the process capability analysis was drawn for the DM water consumption. The
cause and effect diagram was drawn to show the possible causes of the problem. The
actual DM water wastage from different points was measured. In improve phase,
brainstorming sessions were conducted to address the problems and identify the vital
factors through screening and understanding the correlation of the vital factors. In the
control phase, the optimum usage of the DM water level was identified and controlled
with the help of the control plan along with the work instruction sheet. In the end, the
sigma level increased from –0.75 to 1.63 and the annual cost saving of INR 296.09 lakhs
was achieved.
Yeh et al. (2007) have presented the method of evaluating the performance of
supply chain management (SCM) based on DMAIC process through fuzzy linguistic
computing (FLC) model. In define phase, the characteristics namely effectiveness,
rapidity, responsiveness, and customer satisfaction to withstand intensified competition
were identified as SCM goals. The objective was to modify the two-tuple FLC model by
utilising geometric operator and modifying symbolic translation functions. In measure
phase, in order to improve the consistency, an algorithm namely two-tuple technique was
introduced. The criteria namely weighting identification and performance appraisal were
ranked. In the analysis phase, the outcome of the process was analysed using two-tuple
FLC model. The aggregated outcomes could be easily compared, and analysed against
each criterion and sub-criterion to examine the capability of FLC model. In improve
phase, the optimal improvement strategy to accelerate the performance of the suppliers in
252
K
. Srinivasan et al.
SCM system was evolved. In the control phase, the continuous monitoring processes and
response plan developments were executed through the modified FLC model for
evaluating the performance of SCM.
On the whole, the researches reported in the above papers have confirmed that,
DMAIC is a compatible model for achieving the goals of Six Sigma not only in
manufacturing and service sectors, but also in other sectors.
7 Inferences
The review of papers mentioned in the previous three sections was useful to draw the
following inferences.
• DMAIC is a suitable model for implementing in all types of organisations.
• Even in the absence of belt-based training infrastructure, a Six Sigma program
encompassing DMAIC phases facilitates the achievement of the goals of Six Sigma.
• The researchers who strove to implement DMAIC have reported certain benefits.
The benefits reported by them are enumerated in Tables 1, 2 and 3.
Table 1 Benefits of applying DMAIC in manufacturing sectors
S. no. Paper Benefits
1 Jirasukprasert et
al. (2014)
a The sigma level increased from 2.4 to 2.9.
b The reduction of DPMO from 1,95,095 to 83,750.
2 Ghosh and Maiti
(2014)
a Significant reduction in gas defects.
b The annual cost savings achieved up to INR 16 million.
3 Kumaravadivel
and Natarajan
(2013)
a The sigma level increased from 3.49 to 3.65.
b The process capability increased from 1.163 to 1.22.
c The rejection of components reduced from 50 to 32.
d The percentage of rejection reduced from 6.94 to 4.69.
4 Kumar et al.
(2013)
a The sigma level increased from 3.18 to 3.42.
b The cost savings were achieved up to INR 1,124,350 in a year.
5 Kaushik et al.
(2012)
a The sigma level increased from 1.40 to 5.46.
b The cost savings were achieved up to INR 0.288 million per
annum.
6 Li et al. (2011) a The sigma level increased from 0.84 to 2.07.
b The waiting time was reduced from 131 to 71 minutes.
c Monthly monetary savings were achieved up to NTD 26,856.
7 Chen et al. (2009) Significant reduction of time and cost was achieved.
8 Kumar and
Sosnoski (2009)
The profit increased by 2% of company’s annual revenue.
9 Lo et al. (2009) The process capability increased from 0.57 to 1.75.
10 Tong et al. (2004) a The sigma level increased from 1.162 to 5.924.
b The process capability increased from 1.021 to 1.975.
Six Sigma through DMAIC phases 253
Table 2 Benefits of applying DMAIC in service sectors
S. no. Paper Benefits
1 Mayer (2014) Significant improvement in patient and instructor satisfaction was
achieved.
2 Yu and Ueng
(2012)
Recommended the improvement methods to enhance the teaching
effectiveness.
3 Antony et al.
(2012)
Cost savings were achieved up to £400,000 per annum.
4 Chen et al. (2012) Significant reduction of bank credit risks and losses was achieved.
5 Kumar (2012) a Enhancement in awareness about avian flu’s impact on
businesses and humans could be achieved.
b Contingency planning was carried out to avoid losses.
6 Southard et al.
(2012)
Cost savings were achieved up to $1.93 million per annum.
7 Kumar et al.
(2009)
Significant enhancement in customer service and satisfaction was
achieved.
8 Kumar et al.
(2008a)
Enhancement in service quality and increase in customer
satisfaction were achieved.
9 Kumar et al.
(2008b)
The process cycle time decreased from 20 days to 15 days.
Table 3 Benefits of applying DMAIC in unconventional sectors
S. no. Paper Benefits
1 He et al. (2014) a The dispatched employees’ turnover rate significantly reduced
from 2.5% to 1.4%.
b Substantial savings in recruiting and training costs.
2 Franchetti and
Yanik (2011)
The cost savings achieved up to $659,412 per annum.
3 Kaushik and
Khanduja (2009)
a The Six Sigma level increased from –0.75 to 1.63.
b The cost savings achieved up to INR 296.09 lakhs per annum.
4 Yeh et al. (2007) Significant increase in the performance of supply chain.
As shown in Table 1, the application of DMAIC facilitates to achieve the goals of Six
Sigma concept in manufacturing sectors. The researchers who strove to implement
DMAIC have reported the gaining of certain benefits in the service sectors. These
benefits are enumerated in Table 2. The researchers who strove to implement DMAIC
have reported the reaping of certain benefits in unconventional sectors. These benefits are
presented in Table 3. On the whole, as shown in Tables 1, 2 and 3, the benefits of
applying DMAIC are clearly established in manufacturing, service and unconventional
sectors. However, the implementation of DMAIC in unconventional sectors is yet to be
widely investigated by the researchers.

254
K
. Srinivasan et al.
8 Conclusions
The Six Sigma model emerged at Motorola in the 1980s (Jirasukprasert et al., 2014;
Chakraborty and Chuan, 2013; Marques et al., 2013; Pepper and Spedding, 2010).
Thereafter, many papers reporting the applications of Six Sigma in all sectors emerged.
While this trend continuous even today, a section of researchers found out that, the
belt-based training infrastructure of Six Sigma concept is quite expensive. Hence, a few
researchers began to apply only DMAIC in few sectors to achieve the goals of Six Sigma.
On realising this new trend of research, the literature review presented in this paper was
carried out. During the conduct of this literature review, it was discernable that, the
application of DMAIC is powerful enough to restrict the companies belonging to
manufacturing and service sectors to produce goods and offer services by making
mistakes less than 3.4 DPMO (Jirasukprasert et al., 2014; Kumaravadivel and Natarajan,
2013). However, the outcome of implementing DMAIC in unconventional sectors is not
clearly spelt out. Moreover, the number of researches conducted in unconventional
sectors on applying DMAIC is very less. In this background, it is suggested that, many
researches involving the applications of DMAIC are required to be conducted in
companies belonging to unconventional sectors. Some of the unconventional sectors are
those manufacturing furnace accessories, automobile accessories, food products and
components in unconventional machines like electrical discharge machining (EDM) and
electro-chemical machining (ECM). The researchers may concentrate on applying
DMAIC in these unconventional sectors by applying DMAIC and analysing the results. If
found necessary, systems may be developed for implementing DMAIC in specific
sectors. This kind of contribution of these researchers will aid the unconventional sectors
to acquire competitive strength for facing today’s intensified competition (Jirasukprasert
et al., 2014; Sugumaran et al., 2013; Natarajan et al., 2011a, 2011b).
References
Agus, A. and Hajinoor, M.S. (2012) ‘Lean production supply chain management as driver towards
enhancing product quality and business performance: case study of manufacturing companies
in Malaysia’, International Journal of Quality & Reliability Management, Vol. 29, No. 1,
pp.92–121.
Ahmed, S. and Amagoh, F. (2010) ‘Application of QFD in product development of a glass
manufacturing company in Kazakhstan’, Benchmarking: An International Journal, Vol. 17,
No. 2, pp.195–213.
Ahuja, I.P.S. and Khamba, J.S. (2008a) ‘Justification of total productive maintenance initiatives in
Indian manufacturing industry for achieving core competitiveness’, Journal of Manufacturing
Technology Management, Vol. 19, No. 5, pp.645–669.
Ahuja, I.P.S. and Khamba, J.S. (2008b) ‘Total productive maintenance: literature review and
directions’, International Journal of Quality and Reliability Management, Vol. 25, No. 7,
pp.709–756.
Antony, J. and Desai, D.A. (2009) ‘Assessing the status of Six Sigma implementation in the Indian
industry’, Management Research News, Vol. 32, No. 5, pp.413–423.
Antony, J., Bhuller, A.S., Kumar, M., Mendibil, K. and Montgomery, D.C. (2012) ‘Application of
Six Sigma DMAIC methodology in a transactional environment’, International Journal of
Quality and Reliability Management, Vol. 29, No. 1, pp.31–53.

Six Sigma through DMAIC phases 255
Arca, J.G. and Prado, J.C.P. (2008) ‘Personnel participation as a key factor for success in
maintenance program implementation: a case study’, International Journal of Productivity
and Performance Management, Vol. 57, No. 3, pp.247–258.
Breja, S.K., Banwet, D.K. and Iyer, K.C. (2011) ‘Quality strategy for transformation: a case study’,
The TQM Journal, Vol. 23, No. 1, pp.5–20.
Cesarotti, V. and Spada, C. (2009) ‘A systemic approach to achieve operational excellence in hotel
services’, International Journal of Quality and Service Sciences, Vol. 1, No. 1, pp.5–66.
Chakraborty, A. and Chuan, T.K. (2013) ‘An empirical analysis on Six Sigma implementation in
service organisations’, International Journal of Lean Six Sigma, Vol. 4, No. 2, pp.141–170.
Chen, J.C., Li, Y. and Cox, R.A. (2009) ‘Taguchi-based Six Sigma approach to optimize plasma
cutting process: an industrial case study’, International Journal of Advanced Manufacturing
Technology, Vol. 41, Nos. 7-8, pp.760–769.
Chen, Y.C., Chen, S.C., Huang, M.Y. and Tsai, C.L. (2012) ‘Application of Six Sigma DMAIC
methodology to reduce financial risk: a study of credit card usage in Taiwan’, International
Journal of Management, Vol. 29, No. 3, pp.166–176.
Cheng, C.S. and Kuan, C.M. (2012) ‘Research on product reliability improvement by using
DMAIC process: a case study of cold cathode fluorescent lamp’, Asian Journal on Quality,
Vol. 13, No. 1, pp.67–76.
Franchetti, M. and Yanik, M. (2011) ‘Continuous improvement and value stream analysis through
the lean DMAIC Six Sigma approach: a manufacturing case study from Ohio, USA’,
International Journal of Six Sigma and Competitive Advantage, Vol. 6, No. 4, pp.278–300.
Ghosh, S. and Maiti, J. (2014) ‘Data mining driven DMAIC framework for improving foundry
quality – a case study’, Production Planning and Control, Vol. 25, No. 6, pp.478–493.
He, Z., Zhang, X.T. and Zhang, M. (2014) ‘Reducing the voluntary turnover rate of dispatched
employees by the DMAIC process’, Total Quality Management, Vol. 25, Nos. 7–8,
pp.842–855.
Jirasukprasert, P., Garza-Reyes, J.A., Kumar, V. and Lim, M.K. (2014) ‘A Six Sigma and DMAIC
application for the reduction of defects in a rubber gloves manufacturing process’,
International Journal of Lean Six Sigma, Vol. 5, No. 1, pp.2–21.
Kaushik, P. and Khanduja, D. (2009) ‘Application of Six Sigma DMAIC methodology in thermal
power plants: a case study’, Total Quality Management, Vol. 20, No. 2, pp.197–207.
Kaushik, P., Kanduja, D., Mittal, K. and Jaglan, P. (2012) ‘A case study: application of Six Sigma
methodology in a small and medium-sized manufacturing enterprise’, The TQM Journal,
Vol. 24, No. 1, pp.4–16.
Kumar, S. (2012) ‘Planning for avian flu disruptions on global operations: a DMAIC case study’,
International Journal of Health Care Quality Assurance, Vol. 25, No. 3, pp.197–215.
Kumar, S. and Sosnoski, M. (2009) ‘Reflective practice using DMAIC Six Sigma to systematically
improve shop floor production quality and costs’, International Journal of Productivity and
Performance Management, Vol. 58, No. 3, pp.254–273.
Kumar, S., Phillips, A. and Rupp, J. (2009) ‘Using Six Sigma DMAIC to design a high-quality
summer lodge operation’, Journal of Retail and Leisure Property, Vol. 8, No. 3, pp.173–191.
Kumar, S., Satsangi, P.S. and Prajapati, D.R. (2013) ‘Improvement of Sigma level of a foundry: a
case study’, The TQM Journal, Vol. 25, No. 1, pp.29–43.
Kumar, S., Strandlund, E. and Thomas, D. (2008a) ‘Improved service system design using Six
Sigma DMAIC for a major US consumer electronics and appliance retailer’, International
Journal of Retail and Distribution Management, Vol. 36, No. 12, pp.970–994.
Kumar, S., Wolfe, A.D. and Wolfe, K.A. (2008b) ‘Reflective practice using Six Sigma DMAIC to
improve credit initiation process in a financial services operation’, International Journal of
Productivity and Performance Management, Vol. 57, No. 8, pp.659–676.
Kumaravadivel, A. and Natrajan, U. (2013) ‘Application of Six-Sigma DMAIC methodology to
sand-casting process with response surface methodology’, International Journal of Advanced
Manufacturing Technology, Vol. 69, Nos. 5–8, pp.1403–1420.

256
K
. Srinivasan et al.
Li, S.H., Wu, C.C., Yen, D.C. and Lee, M.C. (2011) ‘Improving the efficiency of IT help-desk
service by Six Sigma management methodology (DMAIC) – a case study of C company’,
Production Planning and Control, Vol. 22, No. 7, pp.612–627.
Lo, W.C., Tsai, K.M. and Hsieh, C.Y. (2009) ‘Six Sigma approach to improve surface precision of
optical lenses in the injection-molding process’, International Journal of Advanced
Manufacturing Technology, Vol. 41, Nos. 9–10, pp.885–896.
Marksberry, P. (2012) ‘Investigating ‘the way’ for Toyota suppliers: a quantitative outlook on
Toyota’s replicating efforts for supplier development’, Benchmarking: An International
Journal, Vol. 19, No. 2, pp.277–298.
Marques, P., Requeijo, J., Saraiva, P. and Frazao-Guerreiro, F. (2013) ‘Integrating Six Sigma with
ISO 9001’, International Journal of Lean Six Sigma, Vol. 4, No. 1, pp.36–59.
Mast, J.D. and Lokkerbol, J. (2012) ‘An analysis of the Six Sigma DMAIC method from the
perspective of problem solving’, International Journal of Production Economics, Vol. 139,
No. 2, pp.604–614.
Mayer, S.H. (2014) ‘Redesigning services in a patient education resource center setting: a DMAIC
quality improvement project’, Journal of Hospital Librarianship, Vol. 14, No. 2, pp.140–148.
Natarajan, M., Senthil, V., Devadasan, S.R. and Mohan, N.V. (2011a) ‘QUARNEWSS: a model for
applying Six Sigma framework to achieve continuous quality and reliability improvement in
new product development’, International Journal of Productivity and Quality Management,
Vol. 7, No. 1, pp.44–73.
Natarajan, M., Senthil, V., Devadasan, S.R., Mohan, N.V. and Shalij, P.R. (2011b) ‘Adoption of
Six-Sigma concept in new product development: a literature survey and analysis’,
International Journal of Services and Operations Management, Vol. 8, No. 4, pp.487–515.
Pepper, P.J. and Spedding, T.A. (2010) ‘The evolution of lean Six Sigma’, International Journal of
Quality & Reliability Management, Vol. 27, No. 2, pp.138–155.
Pramod, V.R. and Devadasan, S.R. (2011) ‘Synergising TPM and QFD: a case of electronic switch
manufacturing’, International Journal of Quality and Innovation, Vol. 1, No. 4, pp.298–325.
Pramod, V.R., Devadasan, S.R. and Jagathyraj, V.P. (2010) ‘Quality improvement in engineering
education through the synergy of TPM and QFD’, International Journal of Management in
Education, Vol. 4, No. 1, pp.1–24.
Pramod, V.R., Devadasan, S.R., Jagathyraj, V.P. and Murugesh, R. (2008) ‘MQFD and its
receptivity analysis in an Indian electronic switches manufacturing company’, International
Journal of Management Practice, Vol. 3, No. 1, pp.82–95.
Prashar, A. (2014) ‘Adoption of Six Sigma DMAIC to reduce cost of poor quality’, International
Journal of Productivity and Performance Management, Vol. 63, No. 1, pp.103–126.
Roth, N. and Franchetti, M. (2010) ‘Process improvement for printing operations through the
DMAIC, Lean Six Sigma approach: a case study from Northwest Ohio, USA’, International
Journal of Lean Six Sigma, Vol. 1, No. 2, pp.119–133.
Sankaran, R.A., Senthil, V., Devadasan, S.R. and Babu, E. (2008a) ‘Innovative quality function
deployment in an Indian automobile electrical accessories manufacturing company: an
implementation study’, International Journal of Process Management and Benchmarking,
Vol. 2, No. 3, pp.249–269.
Sankaran, R.A., Senthil, V., Devadasan, S.R. and Pramod, V.R. (2008b) ‘Design and development
of innovative quality function deployment model’, International Journal of Business
Innovation and Research, Vol. 2, No. 2, pp.203–222.
Sarkar, S.A., Mukhopadhyay, A.R. and Ghosh, S.K. (2013) ‘Improvement of claim processing
cycle time through lean Six Sigma methodology’, International Journal of Lean Six Sigma,
Vol. 4, No. 2, pp.171–183.
Southard, P.B., Chandra, C. and Kumar, S. (2012) ‘RFID in healthcare: a Six Sigma DMAIC and
simulation case study’, International Journal of Health Care Quality Assurance, Vol. 25,
No. 4, pp.291–321.

Six Sigma through DMAIC phases 257
Sugumaran, C., Muthu, S., Devadasan, S.R., Pramod, V.R. and Srinivasan, K. (2013) ‘Continuous
maintenance quality improvement using analytic maintenance quality function deployment
technique’, International Journal of Services and Operations Management, Vol. 14, No. 4,
pp.509–543.
Tjahjono, B., Ball, P., Vitanov, V.I., Scorzafave, C., Nogueira, J., Calleja, J., Minguet, M.,
Narasimha, L., Rivas, A., Srivastava, A., Srivastava, S. and Yadav, A. (2010) ‘Six Sigma: a
literature review’, International Journal of Lean Six Sigma, Vol. 1, No. 3, pp.216–233.
Tong, J.P.C., Tsung, F. and Yen, B.P.C. (2004) ‘A DMAIC approach to printed circuit board
quality improvement’, International Journal of Advanced Manufacturing Technology, Vol. 23,
Nos. 7–8, pp.523–531.
Vassilakis, E. and Besseris, G. (2009) ‘An application of TQM tools at a maintenance division of a
large aerospace company’, Journal of Quality in Maintenance Engineering, Vol. 15, No. 1,
pp.31–46.
Yeh, D.Y., Cheng, C.H. and Chi, M.L. (2007) ‘A modified two-tuple FLC model for evaluating the
performance SCM: by the Six Sigma DMAIC process’, Applied Soft Computing, Vol. 7,
No. 3, pp.1027–1034.
Yu, K.T. and Ueng, R.G. (2012) ‘Enhancing teaching effectiveness by using the Six-Sigma
DMAIC model’, Assessment and Evaluation in Higher Education, Vol. 37, No. 8,
pp.949–961.

DMAIC (DRAFT) CASE STUDY 1
DMAIC (Draft) Case Study - Garment Industry
School of Business, Liberty University
Author Note
By submitting this assignment, I attest this submission represents my own work, and not
that of another student, scholar, or internet source. I understand I am responsible for
knowing and correctly utilizing referencing and bibliographical guidelines. I have not
submitted this work for any other class. Correspondence concerning this article should be
addressed to
Email:

DMAIC (DRAFT) CASE STUDY
2
Abstract
Color Line Company has been experiencing defect in their garment production for some
time now, and the continuous rejection of products by the consumers is seeking improvement. The
improvement will include incorporating DMAIC methodology and Lean Six Sigma tools to
discover the root of the challenge. Unlike all manufacturing companies globally, having a large
consumer base is critical and reduces operating costs while still maintaining efficiency. When
employed appropriately, the DMAIC methodology can realize cost-saving and improved quality
in manufacturing processes. More so, to remain competitive in the industry, firms are expected to
develop strategies that can utilize the available resources effectively and efficiently at a low cost
to maximize returns.
Keywords: DMAIC, Lean Six Sigma, Defect, Sigma level, cost reduction, quality, VOC

DMAIC (DRAFT) CASE STUDY
3
DMAIC Case Study (Garment Industry)
All manufacturing companies worldwide are faced with turbulent economic conditions
such as demand for quality, reduced lead time, and global competition. In this case, the garment
industry in the U.S., known as the Color Lines Clothing firm, is working to remain competitive in
the industry and will need to work on several areas. These areas include but are not limited to
production cost reduction, improved quality of goods, and enhanced productivity. All these factors
are met by implementing Six Sigma tools and Define, Measure, Analyze, Improve and Control
(DMAIC). DMAIC is a methodology used to measure objectives and create a cycle that
continuously improves a manufacturing sector (Srinivasan et al., 2016). Color Lines Company
has had several challenges with consumers complaining of defects in their garments. The DMAIC
Six Sigma can improve consumer satisfaction by reducing the rate of defects in products (Zaman
& Zerin, 2017). This article will incorporate Lean Six Sigma tools to better define the defect
problem at Color Lines Firm and establish how to adjust improvements.
Case Study Plan
Clothing manufacturing consists of dividing the overall process such as sewing, cutting,
finishing into many operations necessary for making the product. Each particular stage must be
well completed to ensure that the final product is of quality. Color Lines is a garment making
company located in the U.S., and its manufacturing process is defective as consumers have been
complaining of poor quality for some time now. The company, therefore, has an obligation of
measuring its manufacturing process to find out the primary defect that is leading to the challenge.
Therefore, breaking down the manufacturing process into a reasonable number of sub-operations
will enable us to find out the root cause.
DMAIC (DRAFT) CASE STUDY
4
The Lean Six Sigma (LSS) method seeks to minimize waste and maximize consumer's
satisfaction. Consumer satisfaction is critical in ensuring that the business will remain in operation.
On the other hand, the better the production process, the higher chance of becoming competitive
in the garment industry. LSS approaches to process and quality improvement is DMAIC
methodology which systematically assists the organization in solving problems and improving the
productivity of their operations (Srinivasan et al., 2016). More so, the application of LSS can also
lead to benefits such as participation of employees in the projects, problem-solving, increase in
process knowledge, among others.
Table 1 (Mohamad et al., 2019)
Seven Waste of Lean Manufacturing
Type of Waste
Explanation
Transportation
With the movement of a product from one place to another,
either from the factory to the retail shop. This movement does
not add any value to the product.
Inventory
In most cases, firms tend to hold rawer materials than is
required to produce goods and services in response to the
demand from the consumers.
Waiting
This waste occurs when workers are meant to work slowly or
to stop as they wait for a previous step in a process to be
complete. On the other hand, employees can slowly work
since they have run out of raw materials.
DMAIC (DRAFT) CASE STUDY
5
Over-processing
For example, the garments can have extra pockets included or
a design that will not be visible, which is more valuable than
the consumer requires.
Motion
The waste of motion refers to when a product is moving and
not necessarily because of work. For instance, once the
garments are completed, they may need to get moved to the
warehouse for storage which is not beneficial.
Defect
This waste refers to when the final goods are not what the
consumer ordered. Defects result from many challenges, such
as missed steps in the manufacturing process, which makes a
slight change in the design and quality of the product (Hall &
Scott, 2016).
Overproduction
This waste refers to the production of too many goods that
surpass the demand, which leads to excessive inventory.
Six Sigma and DMAIC Application
In this article, the DMAIC methodology is used at the manufacturing floor of the Color
Lines Company. This method is structured to analyze the process in a detailed way them
implements the improvement required for change. Through this method, Color Lines Company
will have a better road map where the issue is dealt with from the start of the manufacturing process
to the end. A Six Sigma of 3.4 defects per million opportunities is considered normal, and any
figure above that is too high (George et al., 2005). The benefits reaped from employing Six Sigma
are not only applicable to the manufacturing industry like in this case as it has been tested in other
DMAIC (DRAFT) CASE STUDY
6
industries as well, such as the service sector. Six Sigma consist of several approaches that work
towards improving the process and quality of products. The DMAIC methodology consists of five
interconnected stages and works concurrently to solve a firm’s challenge (Rahman et al., 2017).
The process stages can be defined as follows:
What is the
problem?
What information
is available
What is the cause of
the problem?
What are the
right solutions
we have?
What are the
recommendations
or plan for
implementation?
This method allows organizations to make decisions based on accurate and scientific facts
rather than experience and previously acquired knowledge (Rahman et al., 2017). Color Line firms
first line of defect rate was more than 59%, while the projects defect rate is 42%. The project's
target is to reduce the defect rate to less than 2%, which will ensure that consumer needs and
requirements are met. The methods used in this will be Six Sigma, Pareto Analysis and DMAIC
to reduce the garments defects. A cause-and-effect diagram will also get used to finding better the
relation between the causes that lead to the defect.
1. Define Phase
A Six Sigma project needs to get selected based on the firm's issues, which should be
directly related to achieving consumer expectations. The chosen project of Color Lines Company
Define
Measure
Analyze
Improve
Control
Figure 1 (Rahman et al., 2017)
DMAIC Process
DMAIC (DRAFT) CASE STUDY
7
focuses on having a significant impact on consumer satisfaction with their garments, which meets
their value for money. The project selected in the firm was to reduce the quality defects in the
garments, which will also save the organization money in terms of production. According to
George et al. (2005), listening to consumers is critical for all businesses to succeed in the long run.
The voice of consumer concept (VOC) identifying what the customers want and serving them as
the top priority. On the other hand, the defects in the production process become a priority for the
firm to improve and work on a better strategy to prevent future defects in their system.
Table 2 (Rahman et., 2017)
Color Line Company Summary of Project
Title of Project:
Defect reduction in the production of garments
Background and reason for selecting
project:
There has been a large number of garments that
consumers have rejected because they are
defective. This problem has led to several
losses for Color Line Co., such as materials,
time used, and increased consumer
dissatisfaction, which negatively impacts the
business.
The goal of the project:
Reduce defects by 35% with the use of
DMAIC and Six Sigma as part of the
manufacturing procedures
VOC:
High product quality
Expected consumer benefit:
Attained value for money and desired
qualifications of quality met
DMAIC (DRAFT) CASE STUDY
8
Expected financial benefit:
Cost-saving from defect reduction
Team members:
Employees, Production Manager, Factory
floor operator and improvement project leader
A project summary is a tool issued to document all the targets of the project and what Color
Line Co. intend to achieve. According to Yin (2018), a project summary is helpful to ensure that
the goals, VOC, teams’ role in the project are well outlined. This arrangement of an action plan is
essential in ensuring that the ultimate goal is achieved and no step is missed. Meeting consumer
needs is one of the responsibilities that companies have to meet to ensure that the goods meet
recommended criteria. One of the biblical principles relevant to this section is moral order which
has to do with the obligation of doing what is right. God's moral order is designed for the good of
all humans and the surrounding community. Romans 13:3 states, "Do you want to be afraid of the
authority? Do what is good, and you will receive praise from the same" (King James Bible, 2017).
Companies should do what is morally right and work for the benefit of the larger community.
2. Measure Phase
This phase consists of creating metrics that are reliable in monitoring the progress towards
achieving the goal. In this project, the measure phase defines and selects an effective measure to
clarify the significant defects required to get reduced. The defects will get outlined, the highest to
the lowest, and the total number of defects should add up to 100%. The defects get analyzed for
only two months from November 1st, December 31st 2018. The project is based on total quality
management with a 2% reduction in defects.
DMAIC (DRAFT) CASE STUDY
9
Table 3 (Rahman et., 2017)
Defects before Changes
Type of Defect
No. of Defects
% of Defects
Broken
410
47.53
Skip
213
25.85
Open
190
20.97
Puckering
36
5.65
Total
849
100
Table 3 shows the highest defects cause was broken stitches, which contributed to 47.53%
of the overall defects. Pareto analysis is essential to identify the most occurring defect and
prioritize the critical problem which needs to get tackled immediately (Tuna, 2018). Out of the
four defects, the improvement team and Color Line Co. decided to focus on reducing the broken
stitch first. The broken stitch has a sigma level of 1.6, and this calculation has allowed the team to
have more details of the current state of the clothing manufacturing process. The Sigma level is
illustrated in table 4.
Figure 2 (Rahman et., 2017)
Pareto for Project Line Defect before Improvement
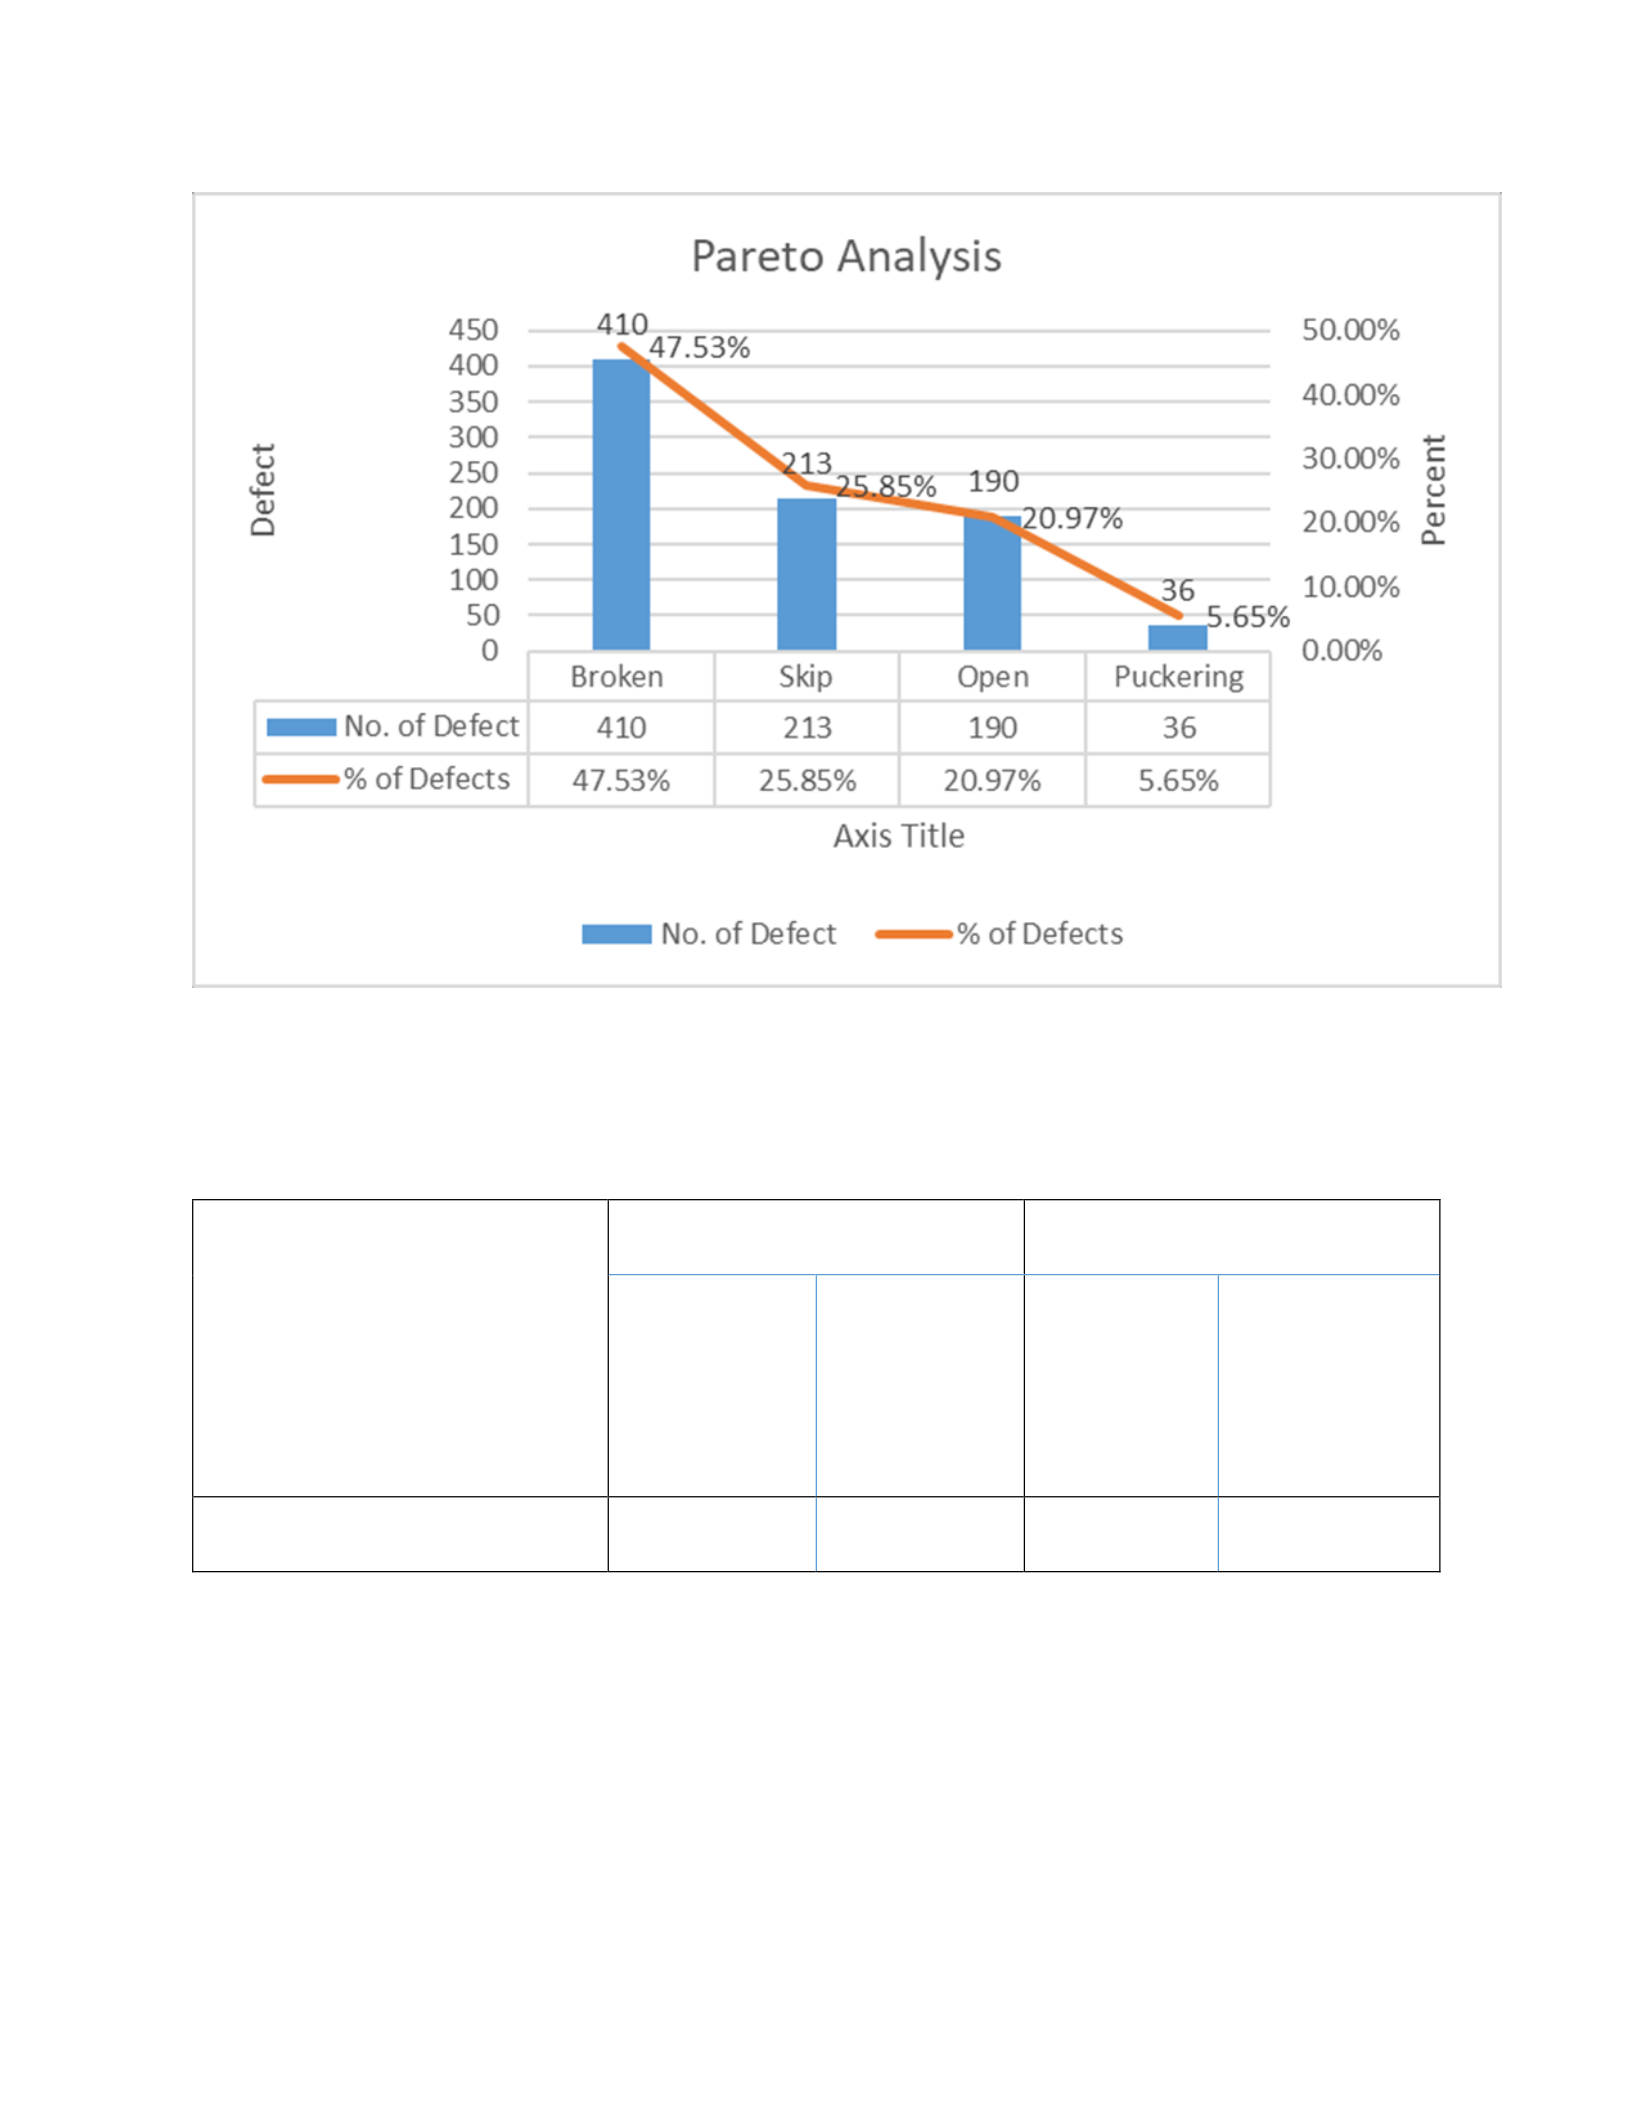
DMAIC (DRAFT) CASE STUDY
10
Table 4 (Rahman et., 2017)
Manufacturing process current and expected states
Major Defect types
Number of Major defects
Sigma Level
Current
Performance
of process
Expected
Performance
of process
Current
Performance
of process
Expected
Performance
of process
Broken
410
170
1.6
3.4
3. Analyze Phase
This phase consists of analyzing the garment manufacturing system of Color Line Co. to
find ways to reduce the gap between the desired goal and the current Performance. Bridging the
gap will require the investigation of the root cause of the problem through a cause-effect diagram.

DMAIC (DRAFT) CASE STUDY
11
According to Tahiduzzaman et al., (2018), a fishbone diagram assists the firm to understand the
garment production process in sub-operations and the main changes to deal with the effect. The
improvement team at Color Line Co. carried out an analysis to identify the root cause of the broken
stitches. Based on the team experience and knowledge of the production process, the following
were the probable causes of the defect.
Figure 3 below is a fishbone diagram that illustrates the relationship between the causes
and effects on the product. According to Tahiduzzaman et al., (2018), when the diagram is
complete, firms can see the root causes and areas that require improvement to ensure that the
production process is effective and working efficiently. Five main factors are considered in this
diagram, known as the 5M; they include manpower, material, machinery, measurement, and
method (Ershadi et al., 2018). The additional factor is the environment which also affects the
production process. The root causes include improper threading, not following the cut mark, and
others caused the broken stitch defect. See the fishbone diagram (Tahiduzzaman et al., 2018).
Figure 3 (Tahiduzzaman et al., 2018)
Cause and Effect Diagram
DMAIC (DRAFT) CASE STUDY
12
Uneven Cutting part Poor Fabric Quality Unskilled
Mismatch of size Improper Thread Not following cut mark
Production Rush Improper Technique Improper feed dog
Follow up Thread Tension
Bobbin Tension
4. Improve Phase
Once the root cause is determined, the DMAIC's improvement phase focuses on
recognizing the solutions that will best suit to reduce the broken stitch defects. The design of
experiments is analyzed through the ANOVA tool, which highlights the effects of multiple factors
(Rahman et., 2017). This design also confirms that the parameters indeed harm the garment
manufacturing process leading to defective clothes. ANOVA model compares the difference in
statistics like illustrated below. The analysis results in table 5 show the effect in the complete
process that leads to the defect in garments.
Measurement
Material
Man
Broken
Stitch
Mother
Methods
Machines
DMAIC (DRAFT) CASE STUDY
13
Table 5 (Rahman et., 2017)
ANOVA with 5% level of significance
Source
Degree of
Freedom
Adj S.S.
Adj MSS
F-Value
P-Value
Defect
3
90.53
21.38
7.59
0.000
Parts
4
5.24
02.12
0.37
0,694
Process
21
75.62
03.83
1.22
0.214
Error
398
1228.04
3.075
Lack of fit
76
182.82
2.477
0.79
0.915
Pure error
320
1044.21
3.215
Total
429
1489.03
The P-value is statistically significant as it is less than 0.05. Color Line's improvement
team will need to make changes to the effects, such as not following the cut mark correctly to
ensure that the final products match the consumer's quality. Additionally, production planning in
the firm is a significant factor that needs to get addressed. Planning refers to seeing ahead of all
the steps taken to complete the manufacturing process and ensure it is done at the right time and
place. More so, every operation will eventually get performed at maximum efficiency.
5. Control Phase
This phase is the game-changer for the other four sections as it determines whether or not
the improvements needed will get abruptly adapted. Finding the problem and coming up with the
most appropriate solutions is not a huge bump as the real challenge in the implementation phase.
It takes time before the implementation starts showing changes, and regular evaluation is required
for the improvement team to ensure that they are still on track. Maintaining the improvement is

DMAIC (DRAFT) CASE STUDY
14
the difficult part, and this phase ensures that the implementation is successful in the long run
(Zaman & Zerin, 2017). The new methods are becoming the standard operating procedures that
require all employees within the garment factory to be part of the project for its success. The
control phase consists of the norm ways and transfers responsibilities to the appropriate individuals
within the production process.
After the implementation, the defect rate is expected to reduce until the desired result is
achieved. Additionally, the sigma level was at 1.6, which is also expected to increase with the
decrease in defect rate. The primary goal of this project is to reduce the defect rate by employing
LSS and DMAIC methodology to come up with the best solution for the strategy (Zaman & Zerin,
2017). The reduction of defects is targeted at increasing consumer satisfaction and offering them
garments that match their value for money. This goal was meant to reduce the costs of production
and losses the Color Line Co. has been undergoing.
Conclusion
The firm's competitive advantage is expected to be much better after the changes in the
defect rate, which will work towards guaranteeing the long-term operation of the business. Another
biblical principle that corresponds with this article is that humans were given the ability to make
moral choices. Genesis 2:15-17 states, "Then the Lord God took the man and put him in the garden
of Eden to tend and keep it. He then commanded the man, saying that every tree in the garden man
can freely eat but not form the tree of the knowledge of good and evil. The day that you eat, you
shall surely die" (King James Bible, 2017). Therefore, human beings were given the ability to
choose that which is right or wrong, and, in this case, correcting the errors from the garments is
the right choice.
DMAIC (DRAFT) CASE STUDY
15
References
Ershadi, M. J., Aiasi, R., & Kazemi, S. (2018). Root cause analysis in quality problem solving of
research information systems: a case study. International Journal of Productivity and
Quality Management, 24(2), 284-299.
George, M. L., Rowlands, D., Price, M., & Maxey, J., (2005). The lean six sigma pocket toolbook.
McGraw-Hill.
Hall, J. & Scott, T. (2016). Lean six sigma: A beginners guide to understanding and practicing
lean six sigma. CreateSpace Independent Publishing.
King James Bible. (2017). King James Bible Online.
https://www.kingjamesbibleonline.org/Psalms-25-21/ (Original work published 1769)
Mohamad, N., Ahmad, S., Samat, H. A., Seng, C. K., & Lazi, F. M. (2019, June). The Application
of DMAIC to Improve Production: Case Study for Single-Sided Flexible Printed Circuit
Board. In IOP Conference Series: Materials Science and Engineering (Vol. 530, No. 1, p.
012041). IOP Publishing. https://iopscience.iop.org/article/10.1088/1757-
899X/530/1/012041/pdf
Rahman, A., Shaju, S. U. C., Sarkar, S. K., Hashem, M. Z., Hasan, S. K., Mandal, R., & Islam, U.
(2017). A case study of six sigma define-measure-analyze-improve-control (DMAIC)
methodology in garment sector. Independent Journal of Management & Production, 8(4),
1309-1323. https://www.redalyc.org/pdf/4495/449553639009.pdf
Srinivasan, K., Muthu, S., Devadasan, S. R., & Sugumaran, C. (2016). Six Sigma through DMAIC
phases: a literature review. International Journal of Productivity and Quality Management,
17(2), 236-257.
DMAIC (DRAFT) CASE STUDY
16
Tahiduzzaman, M., Rahman, M., Dey, S. K., & Kapuria, T. K. (2018). Minimization of sewing
defects of the apparel industry in Bangladesh with 5S & PDCA. American Journal of
Industrial Engineering, 5(1), 17-24. DOI:10.12691/ajie-5-1-3
Tuna, S. (2018). Keeping track of garment production process and process improvement using
quality control techniques. Periodicals of Engineering and Natural Sciences, 6(1), 11-26.
http://dx.doi.org/10.21533/pen.v6i1.162
Yin, R. K. (2018). Case study research and applications: Design and methods, (6TH edition).
SAGE.
Zaman, D. M., & Zerin, N. H. (2017). Applying DMAIC methodology to reduce defects of sewing
section in RMG: a case study. American Journal of Industrial and Business Management,
7(12),1320.http://www.scirp.org/journal/PaperInformation.aspx?PaperID=81178&#abstr
act
BUSI 830 Mod/Wk7
Rubric
DMAIC Case Study (DRAFT) Grading Rubric
Criteria
Levels of Achievement
Content ‐ 35 Points
Advanced
Proficient
Developing
Not present
Case Study
‘Plan’
5 Points
(5)
4 to 5 points
Section provides a topic
sentence for doing a case
study and the study ‘plan’.
2 to 3 points
Section provides either the
topic sentence for doing a
case study or the study ‘plan’.
1 point
Section provides a bullet for
doing a case study or the
study ‘plan’.
0 points
Not completed
Define Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the Define Phase
(with bullets for key steps such
as: customers, problem
statement, resources, crucial
support, high-level process
map, etc.).
3 to 4 points
Section provides a topic
sentence for the Define Phase
(with bullets for only a few key
steps such as: customers,
problem statement, resources,
crucial support, high-level
process map, etc.).
1 to 2 points
Section provides a topic
sentence for the Define
Phase (with no bullets for
key steps such as:
customers, problem
statement, resources,
crucial support, high-level
process map, etc.).
0 points
Not completed or not
related to
requirements for the
section
Measure Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the Measure
Phase (includes key steps
such as: defects,
opportunities, units, metrics,
data collection plan,
validating the measurement
system, etc.).
3 to 4 points
Section provides a topic
sentence for the Measure
Phase (with bullets for only a
few key steps such as:
defects, opportunities, units,
metrics, data collection plan,
validating the measurement
system, etc.).
1 to 2 points
Section provides a topic
sentence for the Measure
Phase (with no bullets for
key steps such as: defects,
opportunities, units, metrics,
data collection plan,
validating the measurement
system, etc.).
0 points
Not completed
Analyze Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the analyze
phase (includes hey steps
such as: performance
objectives, value vs NVA,
opportunities to improve root
cause, variation, etc.)
3 to 4 points
Section provides a topic
sentence for the analyze
phase (with bullets for only a
few key steps such as:
performance objectives,
value vs NVA, opportunities
to improve root cause,
variation, etc.)
1 to 2 points
Section provides a topic
sentence for the analyze
phase (with no bullets for
key steps such as:
performance objectives,
value vs NVA, opportunities
to improve root cause,
variation, etc.)
0 points
Not completed
Improve Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the Improve
Phase (includes key steps
such as: experiments,
solutions, operating
tolerances, implementing the
best solution, etc.).
3 to 4 points
Section provides a topic
sentence for the Improve
Phase (with bullets for only a
few key steps such as:
experiments, solutions,
operating tolerances,
implementing the best
solution, etc.).
1 to 2 points
Section provides a topic
sentence for the Improve
Phase (with no bullets for
key steps such as:
experiments, solutions,
operating tolerances,
implementing the best
solution, etc.).
0 points
Not completed
BUSI 830 Mod/Wk7
Rubric
Control Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the Control
Phase (includes key steps
such as: standards, process
control/ capability,
documentation/ report, etc.).
3 to 4 points
Section provides a topic
sentence for the Control
Phase (with bullets for only a
few key steps such as:
standards, process control/
capability, documentation/
report, etc.).
1 to 2 points
Section provides a topic
sentence for the Control
Phase (with no bullets for
key steps such as:
standards, process control/
capability, documentation/
report, etc.).
0 points
Not completed
Structure ‐ 15
Points
Advanced
Proficient
Developing
Not present
ID’d the Lean Six
Sigma Tools
5 Points
(5)
4 to 5 points
ID’d 3 or more Lean Six Sigma
Tools
2 to 3 points
ID’d 2 Lean Six Sigma Tools
1 point
ID’d 1 Lean Six Sigma Tools
0 points
no Lean Six Sigma
Tools
References and
Citations
5 Points
(1)
4 to 5 points
References >10
2 to 3 points
References = 10
1 point
References <10
0 points
No references
APA Format &
Structure
5 Points
(5)
4 to 5 points
Required section headings
included.
2 to 3 points
Most required section headings
included.
1 point
Partial section headings
included.
0 points
No structure
provided
46 > You have most of the points, but a lot of extraneous, misplaced content, unfocused or underdeveloped sections, formatting
issues. Great draft, but some work to do for final

BUSI 830
DMAIC (FINAL) CASE STUDY ASSIGNMENT INSTRUCTIONS
In this final module, you will synthesize the qualitative research methodology of Case
Study research (and applications) (Yin, 2018) as well as the practical use of Lean Six Sigma
(Hall & Scott, 2016; George et al., 2005) to develop a business-facing DMAIC-based case study.
Also, the seven article readings and your own supporting research has provided a variety of
example designs to include single-case holistic to multiple-case embedded case studies. After
reviewing the Reading & Study material for this module and review of the rest of the course, in
current APA format, design a comprehensive (non-Kaizen) DMAIC Case Study integrated with
Lean Six Sigma tools and biblical worldviews. This must include a plan overview section, as
well as design, measure, analyze, improve, control phases.
Create a real-world case (that is, make sure the story is believable, i.e. it consists of
sequence of time and events, problems and issues to solve, identities [positions/titles] and so on.)
Sanitize all names and use only fictitious data. Use at least 3 Lean Six Sigma tools (George et al.
(2005) by chapter [e.g. a value stream mapping and process flow tool, a data collection tool, an
identifying and verifying causes tool, etc.]) and show your work (i.e. if using a value stream
map, measurement selection matrix, scatter plot, etc.; design a graph, chart, or figure as
appropriate, insert, and refer to such as per APA.) If there could be any doubt, the emphasis of
this project is the DMAIC Case Study process. (HINT: The Cabrita et al. (2016) article serves as
an excellent example.)
Required Format
This 2400 minimum, 3000 maximum word paper needs to be written with these main sections:
Cover page
Abstract
Introduction
Case Study ‘Plan’
Define Phase
Measure Phase
Analyze Phase
Improve Phase
Control Phase
Conclusion
References
Other Requirements
Materials submitted to fulfill requirements in one course may not be submitted in another course.
Concerns about the propriety of obtaining outside assistance and acknowledging sources should
be addressed to the instructor of the course before the work commences and as necessary as the
work proceeds.

BUSI 830
The cover page must include this statement as an author’s note: “By submitting this
assignment, I attest this submission represents my own work, and not that of another
student, scholar, or internet source. I understand I am responsible for knowing and
correctly utilizing referencing and bibliographical guidelines. I have not submitted this
work for any other class.”
In addition to the course textbook(s) and the Bible, this paper must include at least 10
references from scholarly articles that have publication dates no older than 5 years. Do
not use any books other than the Bible and the textbooks. Do not conduct interviews.
There should be at least one instance of biblical integration (at least one scripture
reference).
In-text citations are required to support your statements, points, assertions, issues,
arguments, concerns, paragraph topic sentences, and statements of fact and opinion.
The required cover page, abstract and the reference pages are not included in the required
assignment word count but are required as part of your paper.
The APA required abstract and conclusion section headings and subject headings (see
above) are expected. For papers this length, there should be at least three (3) ‘levels of
headings’.
The introduction and conclusion sections should not be longer than ½ page each since the
assignment is short in word count.
The required abstract should be written as a stand-alone document and not written as an
introduction since an introduction section is required. Therefore, refrain from using
phrases such as, “in this paper,” and do not use citations. See example in APA manual.
Sources of information from Wikipedia, dictionaries, and encyclopedia will not be
accepted. Similarity scores must not exceed 20%.
Paragraph lengths: Each paragraph should have a topic sentence unless it continues from
or provides support to the prior paragraph. A paragraph is defined in this course as being
at least 4 sentences in length.
All parts of the assignment must be based on scholarly and biblical literature.
Avoid clichés, slang, jargon, exaggerations, abbreviations, figurative language, and
language that is too informal and too subjective.
Submit your final document for grading with file name syntax: Last NameFirst Initial
Project#. For example: PhilebaumJ Project8.doc (no .pdfs)
Grading Metrics
Consult the accompanying rubric for how your instructor will grade this assignment. Also, any
form of plagiarism, including cutting and pasting, will result in zero points for the entire
assignment. All quoted materials must be properly cited in current APA format.
Note: Your assignment will be checked for originality via the SafeAssign plagiarism tool.
BUSI 830
DMAIC (FINAL) Case Study Grading Rubric
Criteria
Levels of Achievement
Content ‐ 98 Points
Advanced
Proficient
Developing
Not present
Points
Earned
Abstract,
Introduction,
Case
Study ‘Plan’
10 Points
10 to 10 points
Abstract clearly states the
purpose and main conclusion
and Introduction provides a
complete overview of the
discussion. Provides a
complete discussion for doing
a case study to include the
overarching case study ‘plan’.
Flow is logical and fully cited.
8 to 9 points
Abstract and Introduction
provides a partial purpose,
main conclusion, and
overview of the discussion
and provides a partial
discussion for doing a case
study to include the
overarching case study ‘plan’.
Flow is mostly logical and
partially cited.
1 to 7 points
Abstract and Introduction
present but does not provide
an adequate overview of the
discussion and provides a
minimal discussion for doing
a case study to include the
overarching case study
‘plan’. Flow is not logical
and/or insufficiently cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Define Phase
15 Points
14 to 15 points
Section provides a
comprehensive description of
the Define Phase (includes
key steps such as: customers,
problem statement, resources,
crucial support, high-level
process map, etc.). Flow is
logical and fully cited.
13 to 13 points
Section provides a partial
description of the Define
Phase (includes most key
steps such as: customers,
problem statement, resources,
crucial support, high-level
process map, etc.). Flow is
logical and partially cited.
1 to 12 points
Section provides a minimal
description of the Define
Phase (includes few key
steps such as: customers,
problem statement,
resources, crucial support,
high-level process map, etc.).
Flow is not logical and/or
insufficiently cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Measure Phase
15 Points
14 to 15 points
Section provides a complete
and thorough description of
the Measure Phase (includes
key steps such as: defects,
opportunities, units, metrics,
data collection plan, validating
the measurement system,
etc.). Flow is logical and fully
cited.
13 to 13 points
Section provides a partial
description of the Measure
Phase (includes most key
steps such as: defects,
opportunities, units, metrics,
data collection plan, validating
the measurement system,
etc.). Flow is mostly logical
and partially cited.
1 to 12 points
Section provides a minimal
description of the Measure
Phase (includes few key
steps such as: defects,
opportunities, units, metrics,
data collection plan,
validating the measurement
system, etc.). Flow is not
logical and/or insufficiently
cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Analyze Phase
15 Points
14 to 15 points
Demonstrates critical thinking
to include analysis, evaluation,
and synthesis of the analyze
phase (includes key steps
such as: performance
objectives, value vs NVA,
opportunities to improve root
cause, variation, etc.). Flow is
logical and fully cited.
13 to 13 points
Mostly demonstrates critical
thinking to include analysis,
evaluation, synthesize of the
analyze phase (includes most
key steps such as:
performance objectives, value
vs NVA, opportunities to
improve root cause, variation,
etc.). Flow is mostly logical
and/or partially cited.
1 to 12 points
Only partially demonstrates
critical thinking, analysis,
evaluation, and/or limited
synthesis of analyze phase
(includes few key steps such
as: performance objectives,
value vs NVA, opportunities
to improve root cause,
variation, etc.). Flow is not
logical and/or insufficiently
cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
BUSI 830
Improve Phase
15 Points
14 to 15 points
Section provides a complete
and thorough description of
the Improve Phase (includes
key steps such as:
experiments, solutions,
operating tolerances,
implementing the best
solution, etc.). Flow is logical
and fully cited.
13 to 13 points
Section provides a partial
description of the Improve
Phase (includes most key
steps such as: experiments,
solutions, operating
tolerances, implementing the
best solution, etc.). Flow is
mostly logical and partially
cited.
1 to 12 points
Section provides a minimal
description of the Improve
Phase (includes few key
steps such as: experiments,
solutions, operating
tolerances, implementing the
best solution, etc.). Flow is
not logical and/or
insufficiently cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Control Phase
15 Points
14 to 15 points
Section provides a complete
and thorough description of
the Control Phase (includes
key steps such as: standards,
process control/capability,
documentation/report, etc.).
Flow is logical and fully cited.
13 to 13 points
Section provides a partial
description of the Control
Phase (includes most key
steps such as: standards,
process control/capability,
documentation/report, etc.).
Flow is mostly logical and
partially cited.
1 to 12 points
Section provides a minimal
description of the Control
Phase (includes few key
steps such as: standards,
process control/capability,
documentation/report, etc.).
Flow is not logical and/or
insufficiently cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Conclusion &
Biblical Worldview
Integration
13 Points
13 to 13 points
Conclusion provides a
complete summary of the
discussion and highlights key
points as well as a thoroughly
integrated biblical worldview
with at least 1 scripture
reference.
11 to 12 points
Conclusion provides a partial
summary of the discussion
and highlights at least one key
point and a partially integrated
biblical worldview with at least
1 scripture reference.
1 to 10 points
Conclusion present but does
not summarize discussion or
highlight key points and
either a reference to a
biblical worldview or no
scripture reference.
0 to 0 points
Not completed.
Structure ‐ 42
Points
Advanced
Proficient
Developing
Not present
Points
Earned
Mechanics,
Composition,
Grammar, Word
Count
21 Points
20 to 21 points
Mechanics, Composition, 3 or
more Lean Six Sigma Tools &
Word Count is thorough
(2400-3000 words).
18 to 19 points
Mechanics, Composition, 2
Lean Six Sigma Tools & Word
Count is satisfactory (+/- 2%).
1 to 17 points
Mechanics, Composition, at
least 1 Lean Six Sigma Tool
& Word Count is insufficient
(+/- 3-4%).
0 to 0 points
There are many errors
in mechanics,
composition, grammar,
no Lean Six Sigma
Tools, or Word Count
(>4% diff).
APA Format,
Structure, &
References and
Citations
21 Points
20 to 21 points
Proper cover page and
section headings included.
Met all of the required
formatting. References
exceed requirements in
number and quality and/or
most statements are
supported by a variety of
citations.
18 to 19 points
Proper cover page and
section headings included.
Met most of the required
formatting. References meet
requirements in number and
quality and/or many
statements are supported by a
variety of citations.
1 to 17 points
No cover page and/or section
headings included. Met some
required formatting.
References do not meet
requirements in number and
quality and/or some
statements are supported by
a variety of citations.
0 to 0 points
No structure or
formatting provided.
Missing references
and/or citations are
rare, repetitious or non-
existent.
Total Points
/140
Instructor Comments:
236
I
nt. J. Productivity and Quality Management, Vol. 17, No. 2, 2016
Copyright © 2016 Inderscience Enterprises Ltd.
Six Sigma through DMAIC phases: a literature review
K. Srinivasan*
Department of Mechanical Engineering,
Adhiyamaan College of Engineering,
Hosur – 635 109, India
Email: [email protected]
*Corresponding author
S. Muthu
Department of Mechanical Engineering,
Dr. N.G.P Institute of Technology,
Coimbatore – 641 048, India
Email: smuthu231155@gmail.com
S.R. Devadasan
Department of Production Engineering,
PSG College of Technology,
Coimbatore – 641 004, India
Email: devadasan[email protected]
C. Sugumaran
Department of Mechanical Engineering,
Salem College of Engineering and Technology,
Salem – 636 111, India
Email: mailsugum[email protected]
Abstract: In this paper, the details of a literature review carried out to examine
the application of DMAIC (stands for define, measure, analyse, improve and
control) in companies to achieve the goals of Six Sigma concept are presented.
While conducting this literature review, the papers containing DMAIC in their
titles were gathered and studied. The outcomes of the researches reported in
these papers have confirmed that, DMAIC is the model compatible for
nourishing the benefits of Six Sigma concept in manufacturing, service and
unconventional sectors. An important inference drawn at the end of conducting
this literature review is that, the investigations on applying DMAIC in an
unconventional sector are yet to begin widely and intensively. In this
background, this paper is concluded by suggesting the future researchers to
examine the application of DMAIC in several unconventional sectors.
Keywords: Six Sigma; define, measure, analyse, improve and control;
DMAIC; belt-based training; literature review; project charter; cause and effect
diagram.
Six Sigma through DMAIC phases 237
Reference to this paper should be made as follows: Srinivasan, K., Muthu, S.,
Devadasan, S.R. and Sugumaran, C. (2016) ‘Six Sigma through DMAIC
phases: a literature review’, Int. J. Productivity and Quality Management,
Vol. 17, No. 2, pp.236–257.
Biographical notes: K. Srinivasan is currently an Associate Professor in the
Mechanical Engineering Department of Adhiyamaan College of Engineering,
Hosur, India. He holds a Bachelor in Mechanical Engineering and a Master in
Computer Aided Design, which he obtained from University of Madras, India.
He has 19 years of teaching experience. His research interests include total
productive maintenance, quality function deployment and Six Sigma concepts.
S. Muthu is currently Professor and Dean in the Mechanical Engineering
Department of Dr. N.G.P Institute of Technology, Coimbatore, India. He
obtained his Bachelor in Production Engineering and his Master in Industrial
Engineering from University of Madras, India. He has 33 years of teaching and
research experience. He received his PhD degree from Bharathiyar University
in the year 2003. He has published over 15 papers in international journals. His
areas of research interest include total productive maintenance, work systems
engineering, total quality management, benchmarking and risk management.
S.R. Devadasan is currently a Professor in the Production Engineering
Department of PSG College of Technology, Coimbatore, India. He holds a
Bachelor in Mechanical Engineering, a Master in Industrial Engineering, a PhD
in Mechanical Engineering and a DSc in Mechanical Engineering. He has
24 years of teaching and research experience. He has published over 120 papers
in international journals. He is an editorial advisory board member in the
European Journal of Innovation Management, UK. His areas of research
interest include strategic quality management, total productive maintenance,
productivity engineering and management, agile manufacturing, business
process reengineering, innovation management and risk management.
C. Sugumaran is currently Professor and Dean in the Mechanical Engineering
Department of Salem College of Engineering and Technology, Salem, India.
He obtained his Bachelor in Mechanical Engineering from Bharathiyar
University, India. He obtained his Master in Production Engineering from
Annamalai University, India. He has 19 years of teaching experience. His
research interests include total productive maintenance, benchmarking and
quality function deployment.
1 Introduction
Modern organisations are trying hard to improve their overall performance to face the
ever increasing intensity of competition (Prashar, 2014; Natarajan et al., 2011a, 2011b).
While carrying out this task, modern organisations are striving to apply appropriate
strategies in all of their endeavours (Sugumaran et al., 2013; Cesarotti and Spada, 2009;
Vassilakis and Besseris, 2009; Ahuja and Khamba, 2008b; Pramod et al., 2008). One of
the strategies that has been finding wide and deep applications in modern organisations is
‘continuous quality improvement’ (Pramod and Devadasan, 2011; Pramod et al., 2010).
In order to deploy this strategy, organisations have been applying ‘total quality

238
K
. Srinivasan et al.
management (TQM)’ (Vassilakis and Besseris, 2009; Arca and Prado, 2008). While
applying TQM, organisations have adopted and applied numerous utilities under the
names ‘techniques’, ‘tools’, ‘methods’ and ‘systems’ (Sugumaran et al., 2013; Agus and
Hajinoor, 2012; Marksberry, 2012; Sankaran et al., 2008a, 2008b). Most of these utilities
have facilitated the modern organisations to achieve ‘continuous quality improvement’
(Sugumaran et al., 2013; Breja et al., 2011; Pramod and Devadasan, 2011; Ahmed and
Amagoh, 2010; Pramod et al., 2010, 2008; Cesarotti and Spada, 2009; Vassilakis and
Besseris, 2009; Ahuja and Khamba, 2008a). However, seldom these utilities have
enabled the organisations to achieve profitability. In order to bring out profitability
through the implementation of TQM, in Motorola, Six Sigma model was developed
(Jirasukprasert et al., 2014; Kumaravadivel and Natarajan, 2013; Chakraborty and Chuan,
2013).
Six Sigma concept facilitates to achieve nearly ‘zero defect manufacturing’ and
garner high profit (Kumaravadivel and Natarajan, 2013; Antony et al., 2012). Six Sigma
concept permits the organisations to make mistakes less than 3.4 defects per million
opportunities (DPMO). In order to achieve this goal, two approaches are followed. One is
that, the projects leading to the defect prevention are to be carried out in the organisation
by applying define, measure, analyse, improve and control (DMAIC) phases
(Jirasukprasert et al., 2014; Prashar, 2014; Kumaravadivel and Natarajan, 2013; Sarkar
et al., 2013; Antony et al., 2012; Cheng and Kuan, 2012; Mast and Lokkerbol, 2012;
Franchetti and Yanik, 2011; Roth and Franchetti, 2010). The other approach is the
imparting of formal training by assigning designations as champion, master black belt,
black belt, green belt and white belt (Chakraborty and Chuan, 2013; Marques et al., 2013;
Tjahjono et al., 2010; Kumar et al., 2008a) to the personnel. This method of imparting
formal training is also known as belt-based training infrastructure.
The capability of Six Sigma concept in facilitating organisations to garner high profit
attracted many quality managers. As a result, Six Sigma was first implemented in many
leading companies like general electric and allied signals (Jirasukprasert et al., 2014;
Chakraborty and Chuan, 2013; Pepper and Spedding, 2010). Today, Six Sigma is widely
applied in many parts of the world (Jirasukprasert et al., 2014; Kumaravadivel and
Natarajan, 2013; Chakraborty and Chuan, 2013). However, the conduct of belt-based
training is so expensive that it prevents the implementation of Six Sigma in the
companies with meagre revenue. In order to overcome this situation, during the recent
years, researchers and practitioners have been examining the way of implementing
DMAIC only to implement Six Sigma program in companies (Jirasukprasert et al., 2014).
Few researches dealing with the application of DMAIC in achieving the goals of Six
Sigma have been reported in literature arena. It is very prudent to study the nature and
outcome of these researches, as this study will be useful to evolve economical and
powerful DMAIC-based Six Sigma models. In order to fulfil this requirement, the
literature review reported in this paper was carried out.
2 Methodology
The literature review being reported here was carried out in three steps. In the first step,
the papers whose titles contain the phrase DMAIC were downloaded from the websites of
leading databases namely Emerald Insight (http://www.emeraldinsight.com), Science

Six Sigma through DMAIC phases 239
Direct (http://www.sciencedirect.com), Springerlink (http://www.springerlink.com) and
Taylor and Francis (http://www.tandf.co.uk). On overviewing these papers, it was
realised that DMAIC has been applied in three domains. In the first domain, the DMAIC
has been applied in manufacturing sectors (Jirasukprasert et al., 2014; Ghosh and Maiti,
2014; Kumaravadivel and Natarajan, 2013; Kumar et al., 2013; Kaushik et al., 2012;
Li et al., 2011; Kumar and Sosnoski, 2009; Chen et al., 2009; Lo et al., 2009; Tong et al.,
2004). In the second domain, the DMAIC has been applied in service sectors (Mayer,
2014; Yu and Ueng, 2012; Antony et al., 2012; Chen et al., 2012; Kumar, 2012; Southard
et al., 2012; Kumar et al., 2009, 2008a, 2008b). In the third domain, the DMAIC has been
applied in unconventional sectors (He et al., 2014; Franchetti and Yanik, 2011; Kaushik
and Khanduja, 2009; Yeh et al., 2007). In the second step of the literature review being
reported here, the above papers were segregated into three categories addressing the
researches on applying DMAIC under the above mentioned three domains. After that,
these papers were studied and extracts were drawn about applying DMAIC in the above
three domains. In the third step of the literature review being reported here, the
information and knowledge derived by studying these papers were used to identify future
direction of research. The details of these activities are presented in the following
sections of this paper.
3 Statistics
As mentioned earlier, before beginning the literature review being reported here, the
papers whose titles contained the phrase ‘DMAIC’ were gathered. Twenty-three such
papers containing DMAIC in the titles could be identified. This number is very small
compared to the large number of papers reporting the researches on Six Sigma that have
been reported in the literature arena (Antony and Desai, 2009). As mentioned in the
previous section, these papers were classified under the three domains in which the
implementation of DMAIC is addressed. The statistics of these three categories of papers
is shown in Figure 1. As shown, nearly equal number of papers reporting the applications
of DMAIC in manufacturing and service sectors have appeared in the literature arena.
Little less than half the number of papers reporting the application of DMAIC in
unconventional sectors have appeared. The information and knowledge gathered by
reviewing these papers have been described in the following three sections.
4 DMAIC in manufacturing sectors
As shown in Figure 1, ten papers reporting the application of DMAIC in manufacturing
sector were reviewed during the literature review being reported here. The extracts
derived by conducting this literature review are presented in this section.
Jirasukprasert et al. (2014) reported the implementation of DMAIC methodology for
reducing defects in rubber gloves manufacturing process. In define phase, the problem
was identified. This problem was that, a large amount of rubber gloves had been rejected
by the customers due to defective gloves. In measure phase, the defects were measured,
and the gloves that more leaking and dirty were identified. Furthermore, the Pareto
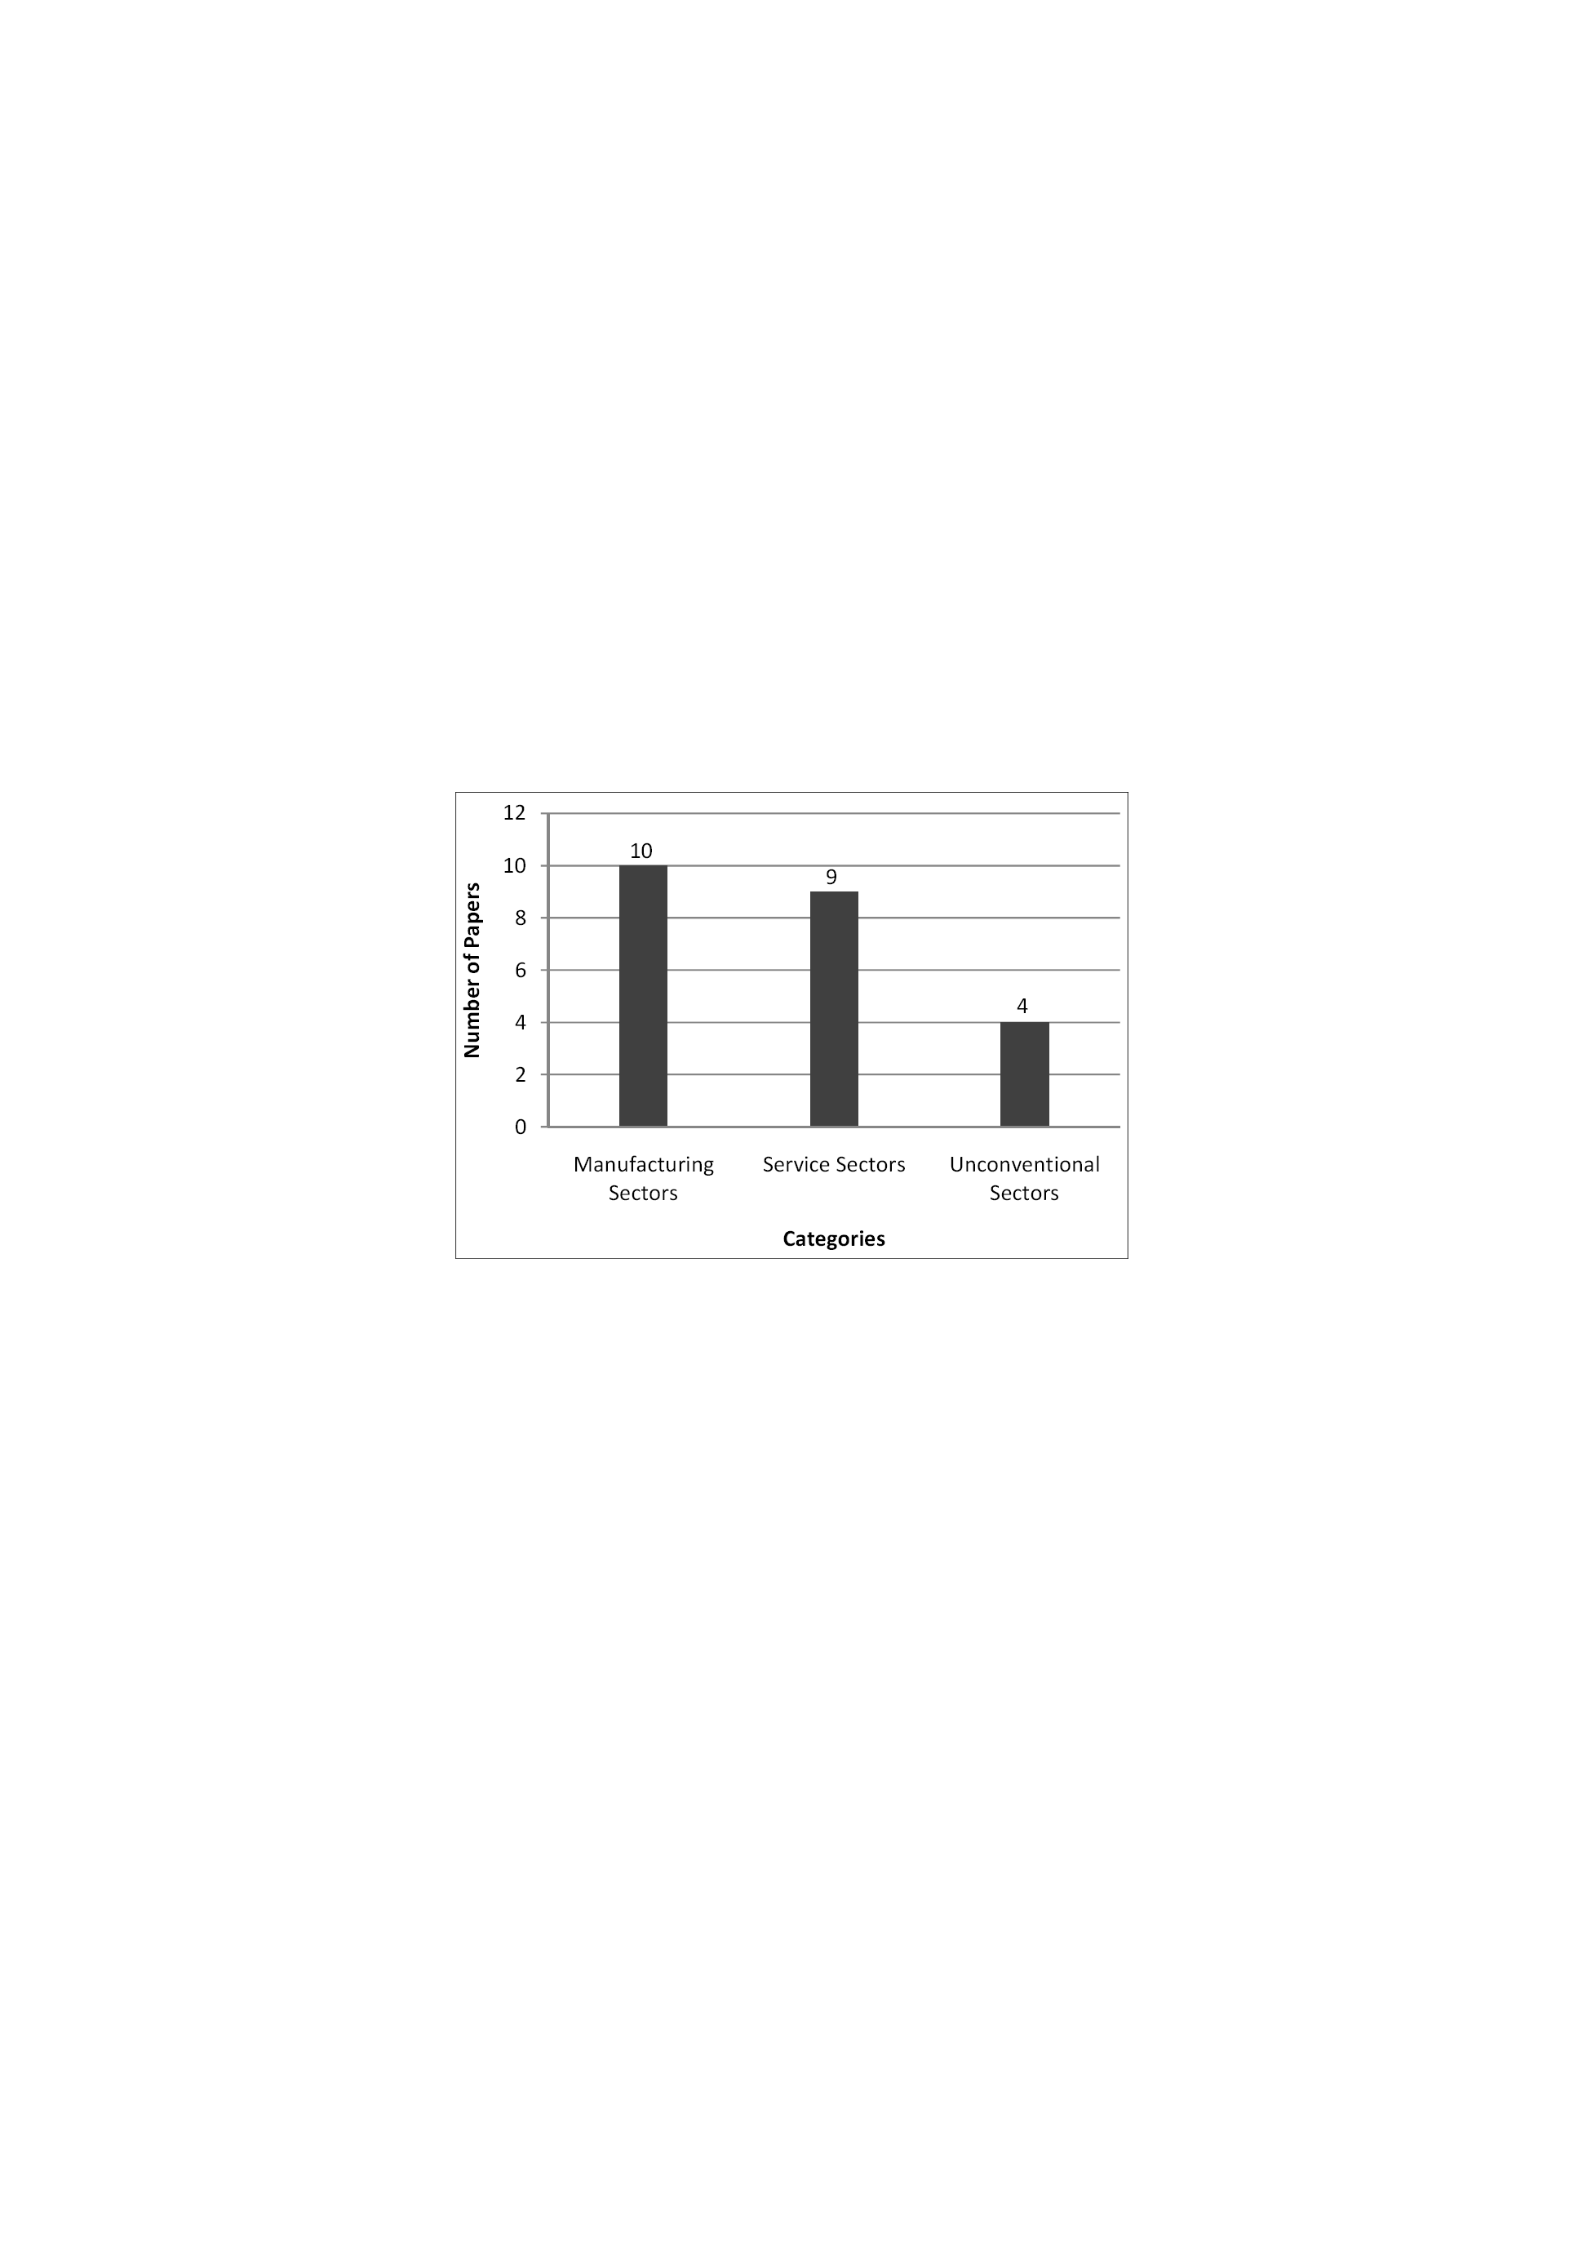
240
K
. Srinivasan et al.
analysis was carried out to identify the complaints that were most frequently reported by
the customers. The present level of sigma was found to be 2.4 with 1,95,095 DPMO. In
analyse phase, ‘oven’s temperature’ and ‘conveyor speed’ were identified as the critical
to quality (CTQ) parameters of manufacturing gloves. In improve phase, the design of
experiment (DOE) was conducted to identify the best oven’s temperature and the best
conveyor speed. The analysis of the results of these experiments indicated that, the best
oven’s temperature would be 230°C and best conveyor speed would be 650 rpm. In the
control phase, the trial run was conducted with best values of the CTQ parameters. As a
result of applying the best values of CTQ parameters in the manufacturing of gloves, the
quantity of gloves leaking was reduced by 50%. The reduction of DPMO was achieved
from 1,95,095 to 83,750, and sigma level improvement from 2.4 to 2.9 was observed.
Figure 1 Statistics of papers reporting researches on DMAIC
Ghosh and Maiti (2014) proposed a data mining driven DMAIC framework for
improving quality of the casting of six-cylinder engine head. During the define phase, it
was found that, the rejection and rework of the casting of six-cylinder engine head were
more than 20%. The company set the objective to reduce the total defect rate by these
castings to less than 5% within six months. A process map was drawn to identify the
influential factors. During the measure phase, the cost of poor quality (COPQ) was
calculated to estimate the impact of casting defects on business profit. This estimation
revealed that, the annual extrapolated total COPQ was more than Indian National Rupees
(INR) 31 million (US $0.54 million). Pareto chart was drawn to identify the major
defects. The study of this chart revealed that, results of 80% of rejections were caused
due to gas porosity. Further, the conducting of brainstorming sessions indicated that, gas
defects originated from four functions namely
1 core making
2 wash application
3 melting and pouring
4 gating and venting.

Six Sigma through DMAIC phases 241
In analysis phase, two data mining-based tools called ‘classification and regression tree’
(CART) and ‘chi-squared automatic interaction and detection’ (CHAID) were applied to
identify the most significant factors causing gas defects in casting. Four parameters
namely
1 horizontal drill vents
2 pouring temperature
3 zircon wash source
4 core sand type
were found to be influencing the most on the gas defect generation. In improve phase,
remedial actions were determined. The recommendations were made to
1 use zircon wash source B
2 use coarser core sand
3 apply pouring temperature between 1,445°C and 1,450°C
4 run the process without horizontal drill vents.
In control phase, the continuous monitoring of processing stage was carried out for
15 days to identify the process behaviour after the actions were taken. It was observed
that, the gas defect has been reduced significantly. The annual savings were calculated to
be INR 16 million (US $0.28 million).
Kumaravadivel and Natarajan (2013) carried out a research to reduce the defects
while manufacturing the casting of flywheel by using DMAIC methodology. The tools
used during the pursuance of this research were process map, cause and effect diagram
and failure mode effect analysis (FMEA). The influential factors which cause the defects
in the casting process were found to be the moisture content, green strength, permeability
and loss of ignition. These factors were analysed by using the response surface
methodology (RSM) technique. The primary objective of pursuing this research was to
reduce the unhidden waste and improve the quality by examining the human as well as
the technical factors. During the define phase, it was found that, 6.94% of the casting of
the flywheels manufactured were rejected. The reasons for rejecting these castings were
attributed to sand inclusions, blow holes and slag. In measure phase, the supplier, input,
process, output and customer (SIPOC) diagram was drawn to map the flywheel
casting process. Subsequently, voice of customer (VOC) was applied to identify CTQ
parameters. The intensiveness of these CTQ parameters was checked by considering
these variables under the names ‘key process input variables’ (KPIV) and ‘key process
output variables’ (KPOV). At the end of this phase, Pareto diagram was drawn. This
diagram indicated that, blow holes, slag and sand inclusion caused 24, 36 and 40% of
defects respectively in the total defects in the casting of the flywheel. These three defects
were considered for overcoming the same and improving the quality of flywheel casting
process. During this phase, the sigma value was found to be 3.49. During analyse phase,
cause and effect matrix, FMEA and cause and effect diagram were used to identify KPIV
and KPOV against the selected CTQ parameters. During the execution of improve phase,
RSM and analysis of variance (ANOVA) were applied to determine the solutions for
achieving quality improvement of flywheel casting process. At the end of executing this
phase, 15 remedial actions were suggested to improve the quality of flywheel casting
242
K
. Srinivasan et al.
process. In improve phase, the significant factors were controlled by using the RSM to
make the process as robust as possible. In the control phase, the solutions evolved in the
previous phase were applied in practice. This application resulted in the decreasing of the
rejection level from 6.94% to 4.69% and increase in the sigma level from 3.49 to 3.65.
Kumar et al. (2013) investigated the DMAIC approach in reducing the variation and
increasing the sigma level of the casting process in the foundry. In define phase, the
defects currently occurring in the foundry were determined through VOC. The CTQ was
evaluated by using VOC, process flow diagram and brainstorming technique. In measure
phase, the current sigma level of the casting process in the foundry was found to be 3.18.
The objective was to increase the sigma level of the process by reducing the occurrence
of the defects by carrying out this research. In the analysis phase, the data collected from
the different treatment conditions as fixed by making use of the orthogonal array (OA)
have been analysed by using the Taguchi’s parameter design approach. In improve phase,
the factors that influence the occurrence of the casting defects were identified. Then, the
corresponding signal to noise ratio for all the trial runs were calculated. In the control
phase, the optimal factors and levels were maintained consistently by generating the
control plan for the optimal factors and levels to control the variation within the
confidence interval. Overall, by pursuing this research, the efficiency and performance of
the casting process in the foundry were increased by using the DMAIC approach.
Kaushik et al. (2012) reported that, the implementation of Six Sigma methodology in
small and medium-sized enterprise (SME) by using DMAIC as a tool to control the
variation in the processing stages of the product. The DMAIC methodology was applied
to solve the high rejection of bushes in bi-cycle chain assembly. In define phase, process
map and a SIPOC diagram were developed to document the manufacturing sequence of
bush and to identify the process or product for achieving improvement. In measure phase,
gauge ‘repeatability and reproducibility’ (R and R) was conducted to ensure that, the
measurement system is statistically sound. The result of this study indicated that, the
micrometer used was facilitating accurate measurement values. In the analysis phase, the
data gathered during the measure phase were analysed to identify the basic cause of the
major rejection of bushes. The process capability chart was drawn by grouping up the
samples into five. The sigma level was found to be 1.4. In order to increase the sigma
level, the cause and effect diagram was used to identify the causes and CTQ which
caused the rejection of the bushes. In improve phase, the two CTQs were considered to
design 2 × 2 DOE, which was conducted for two replications. In control phase, the X/R
chart was plotted by making the trial runs with a sample size 100. The results shown in
this chart indicated that, the process was within the control limit. After the
implementation of DMAIC phases in this bicycle manufacturing unit, the sigma level
increased from 1.40 to 5.46. In the end, the application of DMAIC in this company gave
rise to the annual monetary savings of INR 0.288 million.
Li et al. (2011) reported the application of DMAIC methodology for improving the
efficiency of information technology (IT) help desk service quality through eHelp-desk
system of the Compal Company in Taiwan. In define phase, it was found that, the IT help
desk system needed improvement since the average processing time was as high as
168 minutes, and also the processors were unable to handle the multiple requests at a
time. In measure phase, it was measured that, 74% of the processing time accounted for
the data transfer through personal computer (PC), electronic network and e-mail. The
SIPOC diagram was drawn to determine the time between the submission of the request

Six Sigma through DMAIC phases 243
by the users and processing of the requests by the helpdesk. From the process capability
chart, it was found that, the current sigma level of the company was 0.84. In analyse
phase, it was confirmed that the waiting time accounted for 79% of the total processing
time. In improve phase, the solution conception (eHelp-desk system) was developed by
using the cause and effect diagram. The eHelp-desk system was generated and
implemented. In control phase, the performance of the IT help-desk system was assessed
by drawing data by supplying a questionnaire among the users. The eHelp-desk system
showed a drastic improvement in sigma level from 0.84 to 2.07. The waiting time was
reduced from 131 to 71 minutes and also the monetary savings of New Taiwan Dollars
(NTD) 26,856 per month was achieved.
Chen et al. (2009) have reported a research in which, DMAIC phases were applied to
determine the optimum process parameters while using the plasma-cutting machine. This
research was conducted in an electrical switchboard manufacturing company. In define
phase, brainstorming sessions were conducted to investigate the deviations encountered
in the process of making hole by using the plasma-cutting machine. It was found out that,
deviations in the bevelling and roundness in the hole were the bottlenecks that prevented
the hardware to fit the switchboard. All possible causes of making defective holes while
using plasma cutting machine were depicted in cause and effect diagram. In measure and
analysis phases, the Taguchi experiments were carried out to evolve solutions for
preventing the occurrence of bevel and smallest diameter deviations. The optimum values
of the parameters were found out. Subsequently, response graphs were drawn. Then t-test
was conducted. Using this test, the significance of the factors was examined. In improve
phase, a confirmation test was conducted by applying the solutions evolved in the
previous phase. The examination of the holes cut by applying these solutions indicated
that, the bevelness and roundness deviation fell within the admissible levels. In control
phase, the details of parameters and their optimum values were informed to the
production department of the company. The Six Sigma team of this department was
required to apply these values in real time practice. If necessary, the real-time Taguchi
experiments would have to be conducted further to reduce bevelness and roundness
deviations.
Kumar and Sosnoski (2009) have concentrated on reducing the amount of the warp
incurred in the Amada-A station punches during the heat treatment process by applying
DMAIC phases. In define phase, Pareto analysis was conducted to identify the defects
occurred in punches. This analysis indicated that, the occurrence of warped parts was a
major problem to be overcome. After identification of the problem, the project charter
containing problem statement and project objective statement was developed. In measure
phase, the process capability analysis, descriptive statistics and histogram were used to
determine the present quality levels. Particularly, during this phase, the defects per
million were determined as 1,350. In the analysis phase, cause and effect diagram was
drawn to depict CTQs and the causes of the warp forming in the punches. In improve
phase, the common and special causes were differentiated. Further, their interactions
between the factors were determined. This differentiation facilitated the redesigning of
fixture to eliminate the warp formation in the punches. In the control phase, the hanging
parts were produced using the newly designed punches. In some cases, warpage was still
prevalent on using the newly designed punches. However, the quantum of warpage
encountered was less compared to those that are currently occurring. The cost saving due
to the reduction of the occurrence of the warp formation on using the new fixture was
estimated to be two million dollars.
244
K
. Srinivasan et al.
Lo et al. (2009) reported the implementation of DMAIC approach for improving the
quality of injection-moulded optical lenses. In define phase, the surface performance
quality of lenses were identified. The optical performances of the systems are based on
the image forming capability of an optical system. The actual image of an object is
compared with the ideal image (referred to as image forming capability). In measure
phase, the process capability index was calculated by referring to the surface contour
measurement data to identify the most significant characteristics of moulded lenses. The
surface precision using ‘waviness or peak-to-valley’ (PV) value was measured in the
moulded lenses. In the analysis phase, the data were analysed. Because of poor PV
values, the lens was thicker at its centre. The cause and effect diagram was drawn to
depict the significant processing parameters namely melt temperature, screw speed,
injection speed, injection pressure, packing time, mould temperature and cooling time.
The Taguchi method of DOE was conducted for identifying the most significant
parameters with the corresponding optimal combinations. The objective was to minimise
the waviness of lenses based upon the optimal conditions. In improve phase, the optimal
parameters were implemented and as a result, the capability index enhanced from 0.57 to
1.75, and the Six Sigma target was achieved. In the control phase, the continuous pursuit
for determining the optimal combinations was illustrated with the help of control plan
and consistently monitoring the process capability to retain the fruitful improvement in
the mould shop.
Tong et al. (2004) presented a case study in which the quality of printed circuit board
(PCB) was improved by applying the DMAIC approach. In define phase, the solder paste
volume (height) on the solder pads of the screening process was identified as CTQ
characteristic. In measure phase, the Cyberoptics Cybersentry system was used to
measure the solder paste height on five PCBs for every four hours. Subsequently, the
solder paste height data were recorded in the statistical process control (SPC) data record
sheet by the operators. Further, X-R control chart was plotted. In analyse phase, the
process capability for solder paste height in all six semi-automatic screening machines
was analysed against the current printing performance. In improve phase, DOE was
conducted to determine the optimal settings of all CTQ factors in the screening process.
The parameters considered while conducting DOE were solder paste viscosity, speed of
squeegee, pressure of the squeegee, age of stencil, solder paste volume, blade type and
side of the stencil. In the control phase, the control strategies were recommended to
sustain the improvement of the sigma level in the screening process. The sigma level of
the screening process could be improved from 1.162 to 5.924. Thus, the Six Sigma level
was nearly achieved.
On the whole, the authors of the above papers have claimed that the application of
DMAIC resulted in an increase of sigma values in the performance of the manufacturing
companies in which case studies have been conducted. Some authors have also pointed
out that, DMAIC application facilitates to achieve substantial financial savings.
5 DMAIC in service sectors
As shown in Figure 1, nine papers reporting the application of DMAIC in service sectors
could be overcome during the literature review being reported here. The extracts derived
by reviewing these papers are presented in this section.

Six Sigma through DMAIC phases 245
Mayer (2014) reported a case study to report the achievement of the increase in
efficiency and reduction in the instructor time spent while conducting patient education
classes through the implementation of DMAIC approach in healthcare. In define phase,
the project team was set up to identify the goal and business needs. The objective was to
increase the number of patients attending each class session and reduce the number of
class sessions taught. The topics covered in the classes were temporomandibular disorder
(TMD), blood pressure and chronic kidney disease stage 4 (CKD4). The stakeholders
were the resource centre’s administrators, management personnel, instructor team,
resource centre staff, patients and healthcare providers. The project team interviewed
several patients and gathered data to assess the patients’ satisfactory level. During the
measure phase, it was found out that, the class attendance formed a baseline record for
gathering data regarding the number of patients attended along with class sessions held
for the past three quarters prior to interviewing the patients. In analyse phase, the project
team was asked to assess the processing stages to identify the factors that cause decreased
satisfaction or quality of service offered. The project team analysed the viability
of performing small group teaching on each class topic by considering patient
confidentiality, diagnosis and difficulties on combining the patients. The project team
also investigated the hurdles of combining patients of different categories and that the
sessions which are not fruitful due to the delivery of inappropriate lectures. The project
team called the experts to train the instructors for handling small group teaching to
overcome these deficiencies. The team investigated the woes faced by conducting small
group teaching due to provider referral. The team continuously monitored the classes and
realised that, a small group teaching was ineffective in moving forward the individual
sessions. In improve phase, the action was taken to change the scheduling rules for TMD,
CKD4 and blood pressure class sessions to allow more than one patient for registration.
The project team also monitored the class sessions and data about the participants over
second and third quarters of 2012. In control phase, the project team found out that, the
group teaching on CKD4 class sessions was ineffective. Hence, CKD4 class session had
to be changed to adopt individual teaching procedure. Thus, the project team could not
find the right path to perform small group teaching.
Yu and Ueng (2012) proposed a case study on embarking the teaching effectiveness
in higher educational institutions (HEIs) by applying DMAIC phases. In define phase, the
stakeholders and experts created a list of valid attributes to form a questionnaire that
would facilitate to find out the attributes which are said to be vital for evaluating the
instructors’ teaching performance. In measure phase, teaching performance indicator
(TPI) was proposed to measure the performance of each attribute by evaluating the
questionnaire using the five-point Likert’s scale. The imperative and influential attributes
were niched through importance rating to identify the satisfaction level among students
and instructors. In analyse phase, a modified approach of importance performance
analysis (IPA) called teaching effectiveness analysis matrix (TEAM) was used to
evaluate the teaching performance level that met the HEIs’ expectation level (HEIs’
expectation level is 0.80). The possible factors causing the teaching problems were
identified through cause and effect diagram that had high importance rating on teaching
effectiveness in HEI. In improve phase, a number of improvement methods were
suggested against the identified factors to achieve higher teaching effectiveness in the
selected school. In control phase, the effectiveness of these improvements was verified
over a period after execution of improvement actions. The verification revealed the

246
K
. Srinivasan et al.
achievement of the improvements by making use of the documented standard operating
procedures to sustain the teaching effectiveness in HEI.
Antony et al. (2012) investigated and streamlined the communication and information
management (CIM) system by using the DMAIC phases of Six Sigma methodology in an
infrastructure support company to increase the quality of service. In define phase, the
major processes and the customer requirement were identified by using the Six Sigma
tools namely the SIPOC, VOC and affinity diagram. The SIPOC was used to identify the
basic relationship between the processing stages namely the supplier, input, process,
output and customer. The VOC data were collected from the employees, and the same
were analysed to check whether the requirements of the customer were satisfied, and the
flaws in the process were reduced. The affinity diagram was used to convert the
unstructured data into the structured ones to identify the solution for the problem. In
measure phase, the major KPOV were identified based on which the gauge R and R study
was conducted. The initial step started with the identification of defects in the process by
constructing the CTQ tree and conducting the VOC analysis. The major metrics
identified while constructing the CTQ tree were completeness, correctness and
timeliness. Based on the collected data, the Pareto chart was drawn to identify the major
factors which impacted the CTQ factors. The correctness and completeness of the CIM
system were the major CTQ factors. In the analysis phase, the data that were collected
from the previous phase were identified, and the same were analysed to identify the
causes. The cause and effect diagram was plotted to depict the causes under the title, data,
communication methods, measurements and people. These causes were identified by
conducting brainstorming sessions and applying the multi-voting methodology. Survey
was conducted among the 30 internal employees in the concern, and the corresponding
ratings were given by making use of the Likert’s scale. In improve phase, the solution for
the problem was identified by deriving the information from the previous measure and
analysis phases. This exercise was started with the mapping of the process flow by which
the non-value adding activities were removed to make the process effective. Further, it
was suggested to effect centralised information flow and automation in CIM system. In
the control phase, the vital steps were considered to standardise, monitor and integrate the
changes. In order to carry out this task, standard operating procedures (SOP) were
developed. Further, the control charts were drawn to control the deviation in the future.
Chen et al. (2012) conducted a study on the usage of credit card in Taiwan. The
objective was to reduce the financial risk involved during the registration of the credit
card review process along with the identification of the normal and the default customers
by using DMAIC methodology. In define phase, the major concern faced by the banking
industry during the credit card review process was identified using the decision tree. The
details of the customer were collected from customer relationship management (CRM)
desk and analysed to identify the current trend in the banking industry along with the
differentiation of normal and the faulty customers. In measure phase, the data were
collected from different banks about the credit card review process. The rules were
created for collecting data, which were to be precised, completed and correlated. These
data were used for identifying the normal and the faulty customers. In the analysis phase,
the credit card basic data variable chart was developed, and the questionnaires were
included in the chart. The feedback from the chart was evaluated by using the three
models namely ‘non-group’, ‘the training and testing group’ and ‘the crossover group’.
Initially, the evaluation was carried out by using the non-group model to plot the decision
tree which indicated optimal data at each and every point of the credit card review

Six Sigma through DMAIC phases 247
process whose accuracy level was above 75%. In improve phase, the cross-over
evaluation was carried out on the feedback by referring to the variable chart for finding
the degree of correlation between the nodes of the tree. The results of the decision tree
were framed as the rules that were followed to identify the normal and the faulty
customers. In this case, the following findings were made:
• high yearly income persons had the consistent and robust repaying capabilities than
the low-income people
• females had lower bad debt ratio than males
• the old persons had less desirability over the credit card compared to young people
and students
• married persons had less desirability over bachelors
• the persons with high educational background had higher repaying capability.
In the control phase, the decision tree rules were followed to find the differentiation
between the normal and the faulty customers.
Kumar (2012) reported the application of DMAIC in preventing disruptions occurring
due to the avian flu on global operations. Wal-Mart (retail sector) and Dell computers
(manufacturing sector) supply chain systems were selected for this study. In define phase,
the products were delivered to Wal-Mart from Asia and China. The avian flu began
spreading from China to Hong Kong, Canada, Africa, Asia and Europe. In measure
phase, disruptions that occurred due to the avian flu in the supply chain process were
measured. A situation analysis was conducted by using Decision Focus software on
disruptions that occurred due to the avian flu in Wal-Mart and Dell computers supply
chain. This process is a tool to solve issues that are broad and complex and has multiple
causes and effects that cannot be resolved by carrying out one action. In the analysis
phase, FMEA was used to manage supply chain risk. The result of conducting FMEA
indicated that, failures were wider if risks were not managed effectively. Dell computer’s
and Wal-Mart’s supply chains were examined by conducting FMEA. In improve phase,
the measures were proposed for supply chain improvements. These measures are listed as
follows:
• continuous operation plan reviewing and carrying out vendor capability assessments
• defining preventive measures in an operational action plan
• ensuring business continuity in case of epidemic problem
• drawing better practices from experts and other business firms
• encouraging the trust and openness culture
• educating to understand the symptoms and risks
• educating to acquire preparedness talent for facing emergency
• encouraging the trust and implementing better public health policies in workplaces
In control phase, the control measures were recommended as follows:
• continuous monitoring and identification of infected members

248
K
. Srinivasan et al.
• sending of infected members to their homes
• encouraging teleconferences and avoiding direct meetings
• encouraging employees’ hygienic state
• introducing electronic transfers and avoiding document transfers
• vaccination of employees, suppliers and distributors.
Southard et al. (2012) reported a case study involving the application of radio frequency
identification (RFID) in healthcare through DMAIC phases. In define phase, the CTQ
parameters were identified. These CTQ parameters were ‘identification of the patients’
and ‘availability of the facilities’. In measure phase, cycle time of individual tasks,
overall throughput time of the process, cost of providing the procedures, utilisation of the
resources and reduction in errors in the existing system were measured. The current state
of value stream map (VSM) was also analysed. The problems were identified as improper
procedures and sterilisation which occurred prior to, during, and between surgeries. It
was aimed to overcome these problems by achieving process improvement using RFID
technology. In the analysis phase, the way of incorporating RFID in order to improve the
system was examined. Simulation model was developed to analyse the incorporation of
RFID. The focus in this study was to estimate the difference in overall time and costs
associated with and without RFID in the healthcare system. In improve phase, the
theoretical implementation of RFID to the process under study was investigated by
simulating those processes as if that technology were in place. The model with RFID
showed the potential to improve the performance of the outpatient surgical system. The
improved VSM was developed to eliminate non-value added activities. In the control
phase, policies and procedures to be put in place to achieve improvements were created.
It was emphasised that, the process must be continuously monitored and maintained to
retain the improved state. In the end, it was estimated that, annual cost savings would be
$1.93 million if the model with RFID was implemented.
Kumar et al. (2009) conducted a study on summer lodging operation and analysed the
service system in hotel industry. The objective was consistent to deliver high quality
service with improvised customer satisfaction by using the Six Sigma tools like service
blueprint, service quality (SERVQUAL), cause and effect diagram and Poka-yokes. In
define phase, the service blueprint was prepared for the whole process covering the entry
and exit of the customer during the business and non-business hours. The major problems
were that, the unavailability of lodging staff to greet and accommodate the customer and
also the unavailability of receptionist during the time of customer calling for a
reservation. In measure phase, these problems were evaluated by using the SERVQUAL
by obtaining the feedback from the customers. The questionnaires were prepared to
gather the expectation and perception of the information under the five main attributes
namely tangibles, responsiveness, reliability, assurance, and empathy. These attributes
were weighed according to the feedback received from an external customer. The sorting
was performed based on the feedback by using the gap score methodology. In analysis
phase, the major factors which impacted the reservation system and the customer
perception during the check-in and checkout in the lodging were identified. Initially, the
cause and effect diagram was drawn pertaining to the inferior customer service which
indicated the major causes as delinking of reservation system with online booking engine
and detracting of the customer preferences in the reservation section. In improve phase,

Six Sigma through DMAIC phases 249
the online booking engine was introduced. The customer got their room reserved any
time during the day along with the recruitment of well trained persons to serve the
customers throughout their stay of time in the lodge. The working hours of the employees
with high perks and incentives were slightly increased for offering better service to the
customer. Further, the renovated blueprint was introduced in the reservation system along
with the customer services and preferences with the effective Poka-yokes in lodging for
achieving the customer satisfaction. In the control phase, the control plan, and SOPs were
generated to highly satisfy the customers while performing the reservation. Greetings of
the customer during their stay in lodging will gradually increase the sigma level in the
retail and leisure business.
Kumar et al. (2008a) proposed the improved service system design for the Best Buy
(a major consumer electronics and appliance retailer) using DMAIC approach in the
USA. The competitors to Best Buy are Wal-Mart, Costco and Circuit City. The products
sold by the Best Buy are electronic gadgets, movies, music, computers and electronic
appliances. Best Buy tries to differentiate from its competitor through offering higher
quality service to its customer. In order to improve its service, Best Buy conducted the
SERVQUAL survey to identify the areas lacking quality. In define phase, the ‘customers
and their priorities’, ‘customers’ need and feedback’ and CTQ characteristics that the
customer considered having the highest impact on quality were identified. In measure
phase, the processes and their performances were measured. The internal processes that
influence CTQs were identified, and the defects related to the processes were measured.
In analyse phase, the causes of the defects were determined and the variables that create
the process variation were identified. In improve phase, the methods to remove the cause
of defects, that cause the significant variation and their effects on the CTQs were
identified. The maximum acceptance ranges of the significant variables, a system for
measuring deviations of variables and modifying the process to stay within the acceptable
ranges were identified. In the control phase, the improvements to ensure the key variables
remain within the maximum acceptance ranges under the modified process were
sustained. The improved process will allow Best Buy to provide their customer with
reliable service and also retain the customers’ trust. It will attract the subsidiary of Best
Buy namely Geek Squad to gain more market shares in the electronics repair and
installation service industry.
Kumar et al. (2008b) analysed the credit card initiation in the financial industry by
applying DMAIC phases. The objective of this research was to increase the effectiveness
of the credit card initiation process by reducing the lead time of the approval from
20 days to the period of 15 days. In define phase, the major problems faced while
underwriting of the midmarket customers by the credit card initiation team in the
payment system unit division were defined. In measure phase, the one-shot diagram of
the credit card initiation process was plotted by using the previous five months data
drawn from the company database. The number of days required for a credit card
initiation process against all the mid-market requests in the financial services operation
was identified. In the analysis phase, the data collected from the previous phase were
analysed and picturised with the help of a bar chart. Out of 442 requests, nearly 190
requests took the lead time more than 20 days that should be reduced to 15 days. The
cause and effect diagram was drawn to depict the major causes. The sales team and
‘underwriting and approval team’ were found to play key roles in ensuring credit card
responses. In improve phase, the cause and effect diagram was drawn to depict the
failures that may occur in sales and approval stages. Subsequently, the Poka-yokes were

250
K
. Srinivasan et al.
recommended and implemented to overcome all the failures in the financial operations.
In the control phase, the changes were made in the processing stages of the sales
department. Furthermore, the direct review meetings were held with the sales manager
and credit manager to reduce the lead time in the credit initiation process in the financial
concern.
On the whole, the researches reported in the above papers have confirmed that,
DMAIC is a promising model for implementing Six Sigma in companies offering service
to the customers. Most of the authors of the above papers have presented models for
applying DMAIC in the service sector to appropriately utilise the tools of Six Sigma.
6 DMAIC in unconventional sectors
As shown in Figure 1, during the literature review being reported here, four papers
reporting the application of DMAIC in unconventional sectors could be encountered. The
extracts drawn by reviewing these papers are presented in this section.
He et al. (2014) reported a case study on reducing the voluntary turnover rate of
dispatched employees by using DMAIC methodology in a company situated in China. In
define phase, the project team consisting of employees from human resource (HR),
production planning and manufacturing department was formed. This team conducted a
survey and found that many dispatched employees were not satisfied with the salary,
frequent change of work schedules and obscure futures. This team set its goal as to
reduce the turnover rate from 2.5% to 1.5%. In measure phase, the team gathered the data
required for establishing the baseline of the project. The questionnaire was developed by
modifying Price’s causal model and weighing through a five-point Likert’s scale.
Measurement system analysis (MSA) was carried out to evaluate the quality and
reliability of data collected for finding the key factors of voluntary turnover. In analyse
phase, these factors were analysed and ranked through partial correlation analysis. The
results of this analysis revealed that, the salary and benefits were the most important
factors that affect the dispatched employees’ retention will. Converting opportunity and
job hunting were also the key factors influencing turnover. In improve phase, salary and
benefits, converting opportunities, rotation system, career development, training and
human care were found to be the significant factors for achieving improvement.
Brainstorming and mind mapping were conducted to choose the best solution for
reducing the turnover. The team suggested and implemented the increase of salary by
12.5%, increase of the converting number by 30%, military and regular training, regular
sports activity, offering of birthday and festival gifts. A pilot run was conducted, and its
results showed a drastic decrease in turnover rate from 2.5% to 1.4% and also the gaining
of considerable savings in recruiting and training costs. In control phase, the project team
provided the necessary suggestions to sustain the achieved improvement by continuous
monitoring of the same.
Franchetti and Yanik (2011) reported the implementation of lean DMAIC Six Sigma
approach in a company to reduce costs and achieve continuous improvement. In define
phase, the objective was set to increase the capacity by 10% and reduce the cost by 15%
by employing brainstorming technique, conducting the CTQ analysis and defining the
scope. In measure phase, the SIPOC diagram was drawn to measure the manufacturing
capacity and operating costs to establish the Six Sigma metrics namely the process cycle
time, weekly operating costs, value addition and material handling flows/costs. In

Six Sigma through DMAIC phases 251
analysis phase, the data collected from the previous phase was evaluated by using the Six
Sigma tools namely VSM, Pareto analysis, root cause analysis and FMEA to identify the
significant factors which influenced the CTQ. Pareto analysis was conducted to
determine the largest contributors to cost overruns. This analysis indicated that, over 60%
of the problems occurred due to the lack of standard procedures and monitoring
mechanisms. 30% of the problems occurred due to the inefficiency of the existing layout.
The FMEA was conducted to identify the major failure modes, potential effects, severity,
occurrences and detection. The CTQs were analysed and listed by referring to the risk
priority number (RPN) rating. In improve phase, the improvement proposals were
suggested. These proposals included the implementation of supermarket and Kanban,
rationalisation of the layout, monitoring the labour utilisation, standardisation and
documentation of all processes through the conduct of brainstorming sessions.
Furthermore, the computerised relative allocation facility technique (CRAFT) was
employed to design new layouts to reduce the cost. In control phase, the system was
developed to monitor and sustain the improvement proposals. The improvements were
achieved through the development of SOP, training and daily progress tracking of all the
employees in the facility. The log books were maintained in the work centre to record the
key metrics. After the implementation of the improvement proposals, the sigma level
increased and the operating cost of the process reduced steeply.
Kaushik and Khanduja (2009) reported the application of DMAIC approach in a
thermal power plant. In define phase, the objective was to eliminate the unwanted usage
of demineralised (DM) water in the thermal power plant that will increase the expenses.
The reduction of consumption of DM water in thermal power plant was selected as CTQ.
Furthermore, a process map was drawn for DM water consumption to define the
customer requirements and identify the project goals. In measure phase, the DM water
flow was measured using a flow meter. A gauge R and R study was carried out by using
another flow meter. In the analysis phase, based on the data collected using the flow
meter, the process capability analysis was drawn for the DM water consumption. The
cause and effect diagram was drawn to show the possible causes of the problem. The
actual DM water wastage from different points was measured. In improve phase,
brainstorming sessions were conducted to address the problems and identify the vital
factors through screening and understanding the correlation of the vital factors. In the
control phase, the optimum usage of the DM water level was identified and controlled
with the help of the control plan along with the work instruction sheet. In the end, the
sigma level increased from –0.75 to 1.63 and the annual cost saving of INR 296.09 lakhs
was achieved.
Yeh et al. (2007) have presented the method of evaluating the performance of
supply chain management (SCM) based on DMAIC process through fuzzy linguistic
computing (FLC) model. In define phase, the characteristics namely effectiveness,
rapidity, responsiveness, and customer satisfaction to withstand intensified competition
were identified as SCM goals. The objective was to modify the two-tuple FLC model by
utilising geometric operator and modifying symbolic translation functions. In measure
phase, in order to improve the consistency, an algorithm namely two-tuple technique was
introduced. The criteria namely weighting identification and performance appraisal were
ranked. In the analysis phase, the outcome of the process was analysed using two-tuple
FLC model. The aggregated outcomes could be easily compared, and analysed against
each criterion and sub-criterion to examine the capability of FLC model. In improve
phase, the optimal improvement strategy to accelerate the performance of the suppliers in
252
K
. Srinivasan et al.
SCM system was evolved. In the control phase, the continuous monitoring processes and
response plan developments were executed through the modified FLC model for
evaluating the performance of SCM.
On the whole, the researches reported in the above papers have confirmed that,
DMAIC is a compatible model for achieving the goals of Six Sigma not only in
manufacturing and service sectors, but also in other sectors.
7 Inferences
The review of papers mentioned in the previous three sections was useful to draw the
following inferences.
• DMAIC is a suitable model for implementing in all types of organisations.
• Even in the absence of belt-based training infrastructure, a Six Sigma program
encompassing DMAIC phases facilitates the achievement of the goals of Six Sigma.
• The researchers who strove to implement DMAIC have reported certain benefits.
The benefits reported by them are enumerated in Tables 1, 2 and 3.
Table 1 Benefits of applying DMAIC in manufacturing sectors
S. no. Paper Benefits
1 Jirasukprasert et
al. (2014)
a The sigma level increased from 2.4 to 2.9.
b The reduction of DPMO from 1,95,095 to 83,750.
2 Ghosh and Maiti
(2014)
a Significant reduction in gas defects.
b The annual cost savings achieved up to INR 16 million.
3 Kumaravadivel
and Natarajan
(2013)
a The sigma level increased from 3.49 to 3.65.
b The process capability increased from 1.163 to 1.22.
c The rejection of components reduced from 50 to 32.
d The percentage of rejection reduced from 6.94 to 4.69.
4 Kumar et al.
(2013)
a The sigma level increased from 3.18 to 3.42.
b The cost savings were achieved up to INR 1,124,350 in a year.
5 Kaushik et al.
(2012)
a The sigma level increased from 1.40 to 5.46.
b The cost savings were achieved up to INR 0.288 million per
annum.
6 Li et al. (2011) a The sigma level increased from 0.84 to 2.07.
b The waiting time was reduced from 131 to 71 minutes.
c Monthly monetary savings were achieved up to NTD 26,856.
7 Chen et al. (2009) Significant reduction of time and cost was achieved.
8 Kumar and
Sosnoski (2009)
The profit increased by 2% of company’s annual revenue.
9 Lo et al. (2009) The process capability increased from 0.57 to 1.75.
10 Tong et al. (2004) a The sigma level increased from 1.162 to 5.924.
b The process capability increased from 1.021 to 1.975.
Six Sigma through DMAIC phases 253
Table 2 Benefits of applying DMAIC in service sectors
S. no. Paper Benefits
1 Mayer (2014) Significant improvement in patient and instructor satisfaction was
achieved.
2 Yu and Ueng
(2012)
Recommended the improvement methods to enhance the teaching
effectiveness.
3 Antony et al.
(2012)
Cost savings were achieved up to £400,000 per annum.
4 Chen et al. (2012) Significant reduction of bank credit risks and losses was achieved.
5 Kumar (2012) a Enhancement in awareness about avian flu’s impact on
businesses and humans could be achieved.
b Contingency planning was carried out to avoid losses.
6 Southard et al.
(2012)
Cost savings were achieved up to $1.93 million per annum.
7 Kumar et al.
(2009)
Significant enhancement in customer service and satisfaction was
achieved.
8 Kumar et al.
(2008a)
Enhancement in service quality and increase in customer
satisfaction were achieved.
9 Kumar et al.
(2008b)
The process cycle time decreased from 20 days to 15 days.
Table 3 Benefits of applying DMAIC in unconventional sectors
S. no. Paper Benefits
1 He et al. (2014) a The dispatched employees’ turnover rate significantly reduced
from 2.5% to 1.4%.
b Substantial savings in recruiting and training costs.
2 Franchetti and
Yanik (2011)
The cost savings achieved up to $659,412 per annum.
3 Kaushik and
Khanduja (2009)
a The Six Sigma level increased from –0.75 to 1.63.
b The cost savings achieved up to INR 296.09 lakhs per annum.
4 Yeh et al. (2007) Significant increase in the performance of supply chain.
As shown in Table 1, the application of DMAIC facilitates to achieve the goals of Six
Sigma concept in manufacturing sectors. The researchers who strove to implement
DMAIC have reported the gaining of certain benefits in the service sectors. These
benefits are enumerated in Table 2. The researchers who strove to implement DMAIC
have reported the reaping of certain benefits in unconventional sectors. These benefits are
presented in Table 3. On the whole, as shown in Tables 1, 2 and 3, the benefits of
applying DMAIC are clearly established in manufacturing, service and unconventional
sectors. However, the implementation of DMAIC in unconventional sectors is yet to be
widely investigated by the researchers.

254
K
. Srinivasan et al.
8 Conclusions
The Six Sigma model emerged at Motorola in the 1980s (Jirasukprasert et al., 2014;
Chakraborty and Chuan, 2013; Marques et al., 2013; Pepper and Spedding, 2010).
Thereafter, many papers reporting the applications of Six Sigma in all sectors emerged.
While this trend continuous even today, a section of researchers found out that, the
belt-based training infrastructure of Six Sigma concept is quite expensive. Hence, a few
researchers began to apply only DMAIC in few sectors to achieve the goals of Six Sigma.
On realising this new trend of research, the literature review presented in this paper was
carried out. During the conduct of this literature review, it was discernable that, the
application of DMAIC is powerful enough to restrict the companies belonging to
manufacturing and service sectors to produce goods and offer services by making
mistakes less than 3.4 DPMO (Jirasukprasert et al., 2014; Kumaravadivel and Natarajan,
2013). However, the outcome of implementing DMAIC in unconventional sectors is not
clearly spelt out. Moreover, the number of researches conducted in unconventional
sectors on applying DMAIC is very less. In this background, it is suggested that, many
researches involving the applications of DMAIC are required to be conducted in
companies belonging to unconventional sectors. Some of the unconventional sectors are
those manufacturing furnace accessories, automobile accessories, food products and
components in unconventional machines like electrical discharge machining (EDM) and
electro-chemical machining (ECM). The researchers may concentrate on applying
DMAIC in these unconventional sectors by applying DMAIC and analysing the results. If
found necessary, systems may be developed for implementing DMAIC in specific
sectors. This kind of contribution of these researchers will aid the unconventional sectors
to acquire competitive strength for facing today’s intensified competition (Jirasukprasert
et al., 2014; Sugumaran et al., 2013; Natarajan et al., 2011a, 2011b).
References
Agus, A. and Hajinoor, M.S. (2012) ‘Lean production supply chain management as driver towards
enhancing product quality and business performance: case study of manufacturing companies
in Malaysia’, International Journal of Quality & Reliability Management, Vol. 29, No. 1,
pp.92–121.
Ahmed, S. and Amagoh, F. (2010) ‘Application of QFD in product development of a glass
manufacturing company in Kazakhstan’, Benchmarking: An International Journal, Vol. 17,
No. 2, pp.195–213.
Ahuja, I.P.S. and Khamba, J.S. (2008a) ‘Justification of total productive maintenance initiatives in
Indian manufacturing industry for achieving core competitiveness’, Journal of Manufacturing
Technology Management, Vol. 19, No. 5, pp.645–669.
Ahuja, I.P.S. and Khamba, J.S. (2008b) ‘Total productive maintenance: literature review and
directions’, International Journal of Quality and Reliability Management, Vol. 25, No. 7,
pp.709–756.
Antony, J. and Desai, D.A. (2009) ‘Assessing the status of Six Sigma implementation in the Indian
industry’, Management Research News, Vol. 32, No. 5, pp.413–423.
Antony, J., Bhuller, A.S., Kumar, M., Mendibil, K. and Montgomery, D.C. (2012) ‘Application of
Six Sigma DMAIC methodology in a transactional environment’, International Journal of
Quality and Reliability Management, Vol. 29, No. 1, pp.31–53.

Six Sigma through DMAIC phases 255
Arca, J.G. and Prado, J.C.P. (2008) ‘Personnel participation as a key factor for success in
maintenance program implementation: a case study’, International Journal of Productivity
and Performance Management, Vol. 57, No. 3, pp.247–258.
Breja, S.K., Banwet, D.K. and Iyer, K.C. (2011) ‘Quality strategy for transformation: a case study’,
The TQM Journal, Vol. 23, No. 1, pp.5–20.
Cesarotti, V. and Spada, C. (2009) ‘A systemic approach to achieve operational excellence in hotel
services’, International Journal of Quality and Service Sciences, Vol. 1, No. 1, pp.5–66.
Chakraborty, A. and Chuan, T.K. (2013) ‘An empirical analysis on Six Sigma implementation in
service organisations’, International Journal of Lean Six Sigma, Vol. 4, No. 2, pp.141–170.
Chen, J.C., Li, Y. and Cox, R.A. (2009) ‘Taguchi-based Six Sigma approach to optimize plasma
cutting process: an industrial case study’, International Journal of Advanced Manufacturing
Technology, Vol. 41, Nos. 7-8, pp.760–769.
Chen, Y.C., Chen, S.C., Huang, M.Y. and Tsai, C.L. (2012) ‘Application of Six Sigma DMAIC
methodology to reduce financial risk: a study of credit card usage in Taiwan’, International
Journal of Management, Vol. 29, No. 3, pp.166–176.
Cheng, C.S. and Kuan, C.M. (2012) ‘Research on product reliability improvement by using
DMAIC process: a case study of cold cathode fluorescent lamp’, Asian Journal on Quality,
Vol. 13, No. 1, pp.67–76.
Franchetti, M. and Yanik, M. (2011) ‘Continuous improvement and value stream analysis through
the lean DMAIC Six Sigma approach: a manufacturing case study from Ohio, USA’,
International Journal of Six Sigma and Competitive Advantage, Vol. 6, No. 4, pp.278–300.
Ghosh, S. and Maiti, J. (2014) ‘Data mining driven DMAIC framework for improving foundry
quality – a case study’, Production Planning and Control, Vol. 25, No. 6, pp.478–493.
He, Z., Zhang, X.T. and Zhang, M. (2014) ‘Reducing the voluntary turnover rate of dispatched
employees by the DMAIC process’, Total Quality Management, Vol. 25, Nos. 7–8,
pp.842–855.
Jirasukprasert, P., Garza-Reyes, J.A., Kumar, V. and Lim, M.K. (2014) ‘A Six Sigma and DMAIC
application for the reduction of defects in a rubber gloves manufacturing process’,
International Journal of Lean Six Sigma, Vol. 5, No. 1, pp.2–21.
Kaushik, P. and Khanduja, D. (2009) ‘Application of Six Sigma DMAIC methodology in thermal
power plants: a case study’, Total Quality Management, Vol. 20, No. 2, pp.197–207.
Kaushik, P., Kanduja, D., Mittal, K. and Jaglan, P. (2012) ‘A case study: application of Six Sigma
methodology in a small and medium-sized manufacturing enterprise’, The TQM Journal,
Vol. 24, No. 1, pp.4–16.
Kumar, S. (2012) ‘Planning for avian flu disruptions on global operations: a DMAIC case study’,
International Journal of Health Care Quality Assurance, Vol. 25, No. 3, pp.197–215.
Kumar, S. and Sosnoski, M. (2009) ‘Reflective practice using DMAIC Six Sigma to systematically
improve shop floor production quality and costs’, International Journal of Productivity and
Performance Management, Vol. 58, No. 3, pp.254–273.
Kumar, S., Phillips, A. and Rupp, J. (2009) ‘Using Six Sigma DMAIC to design a high-quality
summer lodge operation’, Journal of Retail and Leisure Property, Vol. 8, No. 3, pp.173–191.
Kumar, S., Satsangi, P.S. and Prajapati, D.R. (2013) ‘Improvement of Sigma level of a foundry: a
case study’, The TQM Journal, Vol. 25, No. 1, pp.29–43.
Kumar, S., Strandlund, E. and Thomas, D. (2008a) ‘Improved service system design using Six
Sigma DMAIC for a major US consumer electronics and appliance retailer’, International
Journal of Retail and Distribution Management, Vol. 36, No. 12, pp.970–994.
Kumar, S., Wolfe, A.D. and Wolfe, K.A. (2008b) ‘Reflective practice using Six Sigma DMAIC to
improve credit initiation process in a financial services operation’, International Journal of
Productivity and Performance Management, Vol. 57, No. 8, pp.659–676.
Kumaravadivel, A. and Natrajan, U. (2013) ‘Application of Six-Sigma DMAIC methodology to
sand-casting process with response surface methodology’, International Journal of Advanced
Manufacturing Technology, Vol. 69, Nos. 5–8, pp.1403–1420.

256
K
. Srinivasan et al.
Li, S.H., Wu, C.C., Yen, D.C. and Lee, M.C. (2011) ‘Improving the efficiency of IT help-desk
service by Six Sigma management methodology (DMAIC) – a case study of C company’,
Production Planning and Control, Vol. 22, No. 7, pp.612–627.
Lo, W.C., Tsai, K.M. and Hsieh, C.Y. (2009) ‘Six Sigma approach to improve surface precision of
optical lenses in the injection-molding process’, International Journal of Advanced
Manufacturing Technology, Vol. 41, Nos. 9–10, pp.885–896.
Marksberry, P. (2012) ‘Investigating ‘the way’ for Toyota suppliers: a quantitative outlook on
Toyota’s replicating efforts for supplier development’, Benchmarking: An International
Journal, Vol. 19, No. 2, pp.277–298.
Marques, P., Requeijo, J., Saraiva, P. and Frazao-Guerreiro, F. (2013) ‘Integrating Six Sigma with
ISO 9001’, International Journal of Lean Six Sigma, Vol. 4, No. 1, pp.36–59.
Mast, J.D. and Lokkerbol, J. (2012) ‘An analysis of the Six Sigma DMAIC method from the
perspective of problem solving’, International Journal of Production Economics, Vol. 139,
No. 2, pp.604–614.
Mayer, S.H. (2014) ‘Redesigning services in a patient education resource center setting: a DMAIC
quality improvement project’, Journal of Hospital Librarianship, Vol. 14, No. 2, pp.140–148.
Natarajan, M., Senthil, V., Devadasan, S.R. and Mohan, N.V. (2011a) ‘QUARNEWSS: a model for
applying Six Sigma framework to achieve continuous quality and reliability improvement in
new product development’, International Journal of Productivity and Quality Management,
Vol. 7, No. 1, pp.44–73.
Natarajan, M., Senthil, V., Devadasan, S.R., Mohan, N.V. and Shalij, P.R. (2011b) ‘Adoption of
Six-Sigma concept in new product development: a literature survey and analysis’,
International Journal of Services and Operations Management, Vol. 8, No. 4, pp.487–515.
Pepper, P.J. and Spedding, T.A. (2010) ‘The evolution of lean Six Sigma’, International Journal of
Quality & Reliability Management, Vol. 27, No. 2, pp.138–155.
Pramod, V.R. and Devadasan, S.R. (2011) ‘Synergising TPM and QFD: a case of electronic switch
manufacturing’, International Journal of Quality and Innovation, Vol. 1, No. 4, pp.298–325.
Pramod, V.R., Devadasan, S.R. and Jagathyraj, V.P. (2010) ‘Quality improvement in engineering
education through the synergy of TPM and QFD’, International Journal of Management in
Education, Vol. 4, No. 1, pp.1–24.
Pramod, V.R., Devadasan, S.R., Jagathyraj, V.P. and Murugesh, R. (2008) ‘MQFD and its
receptivity analysis in an Indian electronic switches manufacturing company’, International
Journal of Management Practice, Vol. 3, No. 1, pp.82–95.
Prashar, A. (2014) ‘Adoption of Six Sigma DMAIC to reduce cost of poor quality’, International
Journal of Productivity and Performance Management, Vol. 63, No. 1, pp.103–126.
Roth, N. and Franchetti, M. (2010) ‘Process improvement for printing operations through the
DMAIC, Lean Six Sigma approach: a case study from Northwest Ohio, USA’, International
Journal of Lean Six Sigma, Vol. 1, No. 2, pp.119–133.
Sankaran, R.A., Senthil, V., Devadasan, S.R. and Babu, E. (2008a) ‘Innovative quality function
deployment in an Indian automobile electrical accessories manufacturing company: an
implementation study’, International Journal of Process Management and Benchmarking,
Vol. 2, No. 3, pp.249–269.
Sankaran, R.A., Senthil, V., Devadasan, S.R. and Pramod, V.R. (2008b) ‘Design and development
of innovative quality function deployment model’, International Journal of Business
Innovation and Research, Vol. 2, No. 2, pp.203–222.
Sarkar, S.A., Mukhopadhyay, A.R. and Ghosh, S.K. (2013) ‘Improvement of claim processing
cycle time through lean Six Sigma methodology’, International Journal of Lean Six Sigma,
Vol. 4, No. 2, pp.171–183.
Southard, P.B., Chandra, C. and Kumar, S. (2012) ‘RFID in healthcare: a Six Sigma DMAIC and
simulation case study’, International Journal of Health Care Quality Assurance, Vol. 25,
No. 4, pp.291–321.

Six Sigma through DMAIC phases 257
Sugumaran, C., Muthu, S., Devadasan, S.R., Pramod, V.R. and Srinivasan, K. (2013) ‘Continuous
maintenance quality improvement using analytic maintenance quality function deployment
technique’, International Journal of Services and Operations Management, Vol. 14, No. 4,
pp.509–543.
Tjahjono, B., Ball, P., Vitanov, V.I., Scorzafave, C., Nogueira, J., Calleja, J., Minguet, M.,
Narasimha, L., Rivas, A., Srivastava, A., Srivastava, S. and Yadav, A. (2010) ‘Six Sigma: a
literature review’, International Journal of Lean Six Sigma, Vol. 1, No. 3, pp.216–233.
Tong, J.P.C., Tsung, F. and Yen, B.P.C. (2004) ‘A DMAIC approach to printed circuit board
quality improvement’, International Journal of Advanced Manufacturing Technology, Vol. 23,
Nos. 7–8, pp.523–531.
Vassilakis, E. and Besseris, G. (2009) ‘An application of TQM tools at a maintenance division of a
large aerospace company’, Journal of Quality in Maintenance Engineering, Vol. 15, No. 1,
pp.31–46.
Yeh, D.Y., Cheng, C.H. and Chi, M.L. (2007) ‘A modified two-tuple FLC model for evaluating the
performance SCM: by the Six Sigma DMAIC process’, Applied Soft Computing, Vol. 7,
No. 3, pp.1027–1034.
Yu, K.T. and Ueng, R.G. (2012) ‘Enhancing teaching effectiveness by using the Six-Sigma
DMAIC model’, Assessment and Evaluation in Higher Education, Vol. 37, No. 8,
pp.949–961.

DMAIC (DRAFT) CASE STUDY 1
DMAIC (Draft) Case Study - Garment Industry
School of Business, Liberty University
Author Note
By submitting this assignment, I attest this submission represents my own work, and not
that of another student, scholar, or internet source. I understand I am responsible for
knowing and correctly utilizing referencing and bibliographical guidelines. I have not
submitted this work for any other class. Correspondence concerning this article should be
addressed to
Email:

DMAIC (DRAFT) CASE STUDY
2
Abstract
Color Line Company has been experiencing defect in their garment production for some
time now, and the continuous rejection of products by the consumers is seeking improvement. The
improvement will include incorporating DMAIC methodology and Lean Six Sigma tools to
discover the root of the challenge. Unlike all manufacturing companies globally, having a large
consumer base is critical and reduces operating costs while still maintaining efficiency. When
employed appropriately, the DMAIC methodology can realize cost-saving and improved quality
in manufacturing processes. More so, to remain competitive in the industry, firms are expected to
develop strategies that can utilize the available resources effectively and efficiently at a low cost
to maximize returns.
Keywords: DMAIC, Lean Six Sigma, Defect, Sigma level, cost reduction, quality, VOC

DMAIC (DRAFT) CASE STUDY
3
DMAIC Case Study (Garment Industry)
All manufacturing companies worldwide are faced with turbulent economic conditions
such as demand for quality, reduced lead time, and global competition. In this case, the garment
industry in the U.S., known as the Color Lines Clothing firm, is working to remain competitive in
the industry and will need to work on several areas. These areas include but are not limited to
production cost reduction, improved quality of goods, and enhanced productivity. All these factors
are met by implementing Six Sigma tools and Define, Measure, Analyze, Improve and Control
(DMAIC). DMAIC is a methodology used to measure objectives and create a cycle that
continuously improves a manufacturing sector (Srinivasan et al., 2016). Color Lines Company
has had several challenges with consumers complaining of defects in their garments. The DMAIC
Six Sigma can improve consumer satisfaction by reducing the rate of defects in products (Zaman
& Zerin, 2017). This article will incorporate Lean Six Sigma tools to better define the defect
problem at Color Lines Firm and establish how to adjust improvements.
Case Study Plan
Clothing manufacturing consists of dividing the overall process such as sewing, cutting,
finishing into many operations necessary for making the product. Each particular stage must be
well completed to ensure that the final product is of quality. Color Lines is a garment making
company located in the U.S., and its manufacturing process is defective as consumers have been
complaining of poor quality for some time now. The company, therefore, has an obligation of
measuring its manufacturing process to find out the primary defect that is leading to the challenge.
Therefore, breaking down the manufacturing process into a reasonable number of sub-operations
will enable us to find out the root cause.
DMAIC (DRAFT) CASE STUDY
4
The Lean Six Sigma (LSS) method seeks to minimize waste and maximize consumer's
satisfaction. Consumer satisfaction is critical in ensuring that the business will remain in operation.
On the other hand, the better the production process, the higher chance of becoming competitive
in the garment industry. LSS approaches to process and quality improvement is DMAIC
methodology which systematically assists the organization in solving problems and improving the
productivity of their operations (Srinivasan et al., 2016). More so, the application of LSS can also
lead to benefits such as participation of employees in the projects, problem-solving, increase in
process knowledge, among others.
Table 1 (Mohamad et al., 2019)
Seven Waste of Lean Manufacturing
Type of Waste
Explanation
Transportation
With the movement of a product from one place to another,
either from the factory to the retail shop. This movement does
not add any value to the product.
Inventory
In most cases, firms tend to hold rawer materials than is
required to produce goods and services in response to the
demand from the consumers.
Waiting
This waste occurs when workers are meant to work slowly or
to stop as they wait for a previous step in a process to be
complete. On the other hand, employees can slowly work
since they have run out of raw materials.
DMAIC (DRAFT) CASE STUDY
5
Over-processing
For example, the garments can have extra pockets included or
a design that will not be visible, which is more valuable than
the consumer requires.
Motion
The waste of motion refers to when a product is moving and
not necessarily because of work. For instance, once the
garments are completed, they may need to get moved to the
warehouse for storage which is not beneficial.
Defect
This waste refers to when the final goods are not what the
consumer ordered. Defects result from many challenges, such
as missed steps in the manufacturing process, which makes a
slight change in the design and quality of the product (Hall &
Scott, 2016).
Overproduction
This waste refers to the production of too many goods that
surpass the demand, which leads to excessive inventory.
Six Sigma and DMAIC Application
In this article, the DMAIC methodology is used at the manufacturing floor of the Color
Lines Company. This method is structured to analyze the process in a detailed way them
implements the improvement required for change. Through this method, Color Lines Company
will have a better road map where the issue is dealt with from the start of the manufacturing process
to the end. A Six Sigma of 3.4 defects per million opportunities is considered normal, and any
figure above that is too high (George et al., 2005). The benefits reaped from employing Six Sigma
are not only applicable to the manufacturing industry like in this case as it has been tested in other
DMAIC (DRAFT) CASE STUDY
6
industries as well, such as the service sector. Six Sigma consist of several approaches that work
towards improving the process and quality of products. The DMAIC methodology consists of five
interconnected stages and works concurrently to solve a firm’s challenge (Rahman et al., 2017).
The process stages can be defined as follows:
What is the
problem?
What information
is available
What is the cause of
the problem?
What are the
right solutions
we have?
What are the
recommendations
or plan for
implementation?
This method allows organizations to make decisions based on accurate and scientific facts
rather than experience and previously acquired knowledge (Rahman et al., 2017). Color Line firms
first line of defect rate was more than 59%, while the projects defect rate is 42%. The project's
target is to reduce the defect rate to less than 2%, which will ensure that consumer needs and
requirements are met. The methods used in this will be Six Sigma, Pareto Analysis and DMAIC
to reduce the garments defects. A cause-and-effect diagram will also get used to finding better the
relation between the causes that lead to the defect.
1. Define Phase
A Six Sigma project needs to get selected based on the firm's issues, which should be
directly related to achieving consumer expectations. The chosen project of Color Lines Company
Define
Measure
Analyze
Improve
Control
Figure 1 (Rahman et al., 2017)
DMAIC Process
DMAIC (DRAFT) CASE STUDY
7
focuses on having a significant impact on consumer satisfaction with their garments, which meets
their value for money. The project selected in the firm was to reduce the quality defects in the
garments, which will also save the organization money in terms of production. According to
George et al. (2005), listening to consumers is critical for all businesses to succeed in the long run.
The voice of consumer concept (VOC) identifying what the customers want and serving them as
the top priority. On the other hand, the defects in the production process become a priority for the
firm to improve and work on a better strategy to prevent future defects in their system.
Table 2 (Rahman et., 2017)
Color Line Company Summary of Project
Title of Project:
Defect reduction in the production of garments
Background and reason for selecting
project:
There has been a large number of garments that
consumers have rejected because they are
defective. This problem has led to several
losses for Color Line Co., such as materials,
time used, and increased consumer
dissatisfaction, which negatively impacts the
business.
The goal of the project:
Reduce defects by 35% with the use of
DMAIC and Six Sigma as part of the
manufacturing procedures
VOC:
High product quality
Expected consumer benefit:
Attained value for money and desired
qualifications of quality met
DMAIC (DRAFT) CASE STUDY
8
Expected financial benefit:
Cost-saving from defect reduction
Team members:
Employees, Production Manager, Factory
floor operator and improvement project leader
A project summary is a tool issued to document all the targets of the project and what Color
Line Co. intend to achieve. According to Yin (2018), a project summary is helpful to ensure that
the goals, VOC, teams’ role in the project are well outlined. This arrangement of an action plan is
essential in ensuring that the ultimate goal is achieved and no step is missed. Meeting consumer
needs is one of the responsibilities that companies have to meet to ensure that the goods meet
recommended criteria. One of the biblical principles relevant to this section is moral order which
has to do with the obligation of doing what is right. God's moral order is designed for the good of
all humans and the surrounding community. Romans 13:3 states, "Do you want to be afraid of the
authority? Do what is good, and you will receive praise from the same" (King James Bible, 2017).
Companies should do what is morally right and work for the benefit of the larger community.
2. Measure Phase
This phase consists of creating metrics that are reliable in monitoring the progress towards
achieving the goal. In this project, the measure phase defines and selects an effective measure to
clarify the significant defects required to get reduced. The defects will get outlined, the highest to
the lowest, and the total number of defects should add up to 100%. The defects get analyzed for
only two months from November 1st, December 31st 2018. The project is based on total quality
management with a 2% reduction in defects.
DMAIC (DRAFT) CASE STUDY
9
Table 3 (Rahman et., 2017)
Defects before Changes
Type of Defect
No. of Defects
% of Defects
Broken
410
47.53
Skip
213
25.85
Open
190
20.97
Puckering
36
5.65
Total
849
100
Table 3 shows the highest defects cause was broken stitches, which contributed to 47.53%
of the overall defects. Pareto analysis is essential to identify the most occurring defect and
prioritize the critical problem which needs to get tackled immediately (Tuna, 2018). Out of the
four defects, the improvement team and Color Line Co. decided to focus on reducing the broken
stitch first. The broken stitch has a sigma level of 1.6, and this calculation has allowed the team to
have more details of the current state of the clothing manufacturing process. The Sigma level is
illustrated in table 4.
Figure 2 (Rahman et., 2017)
Pareto for Project Line Defect before Improvement
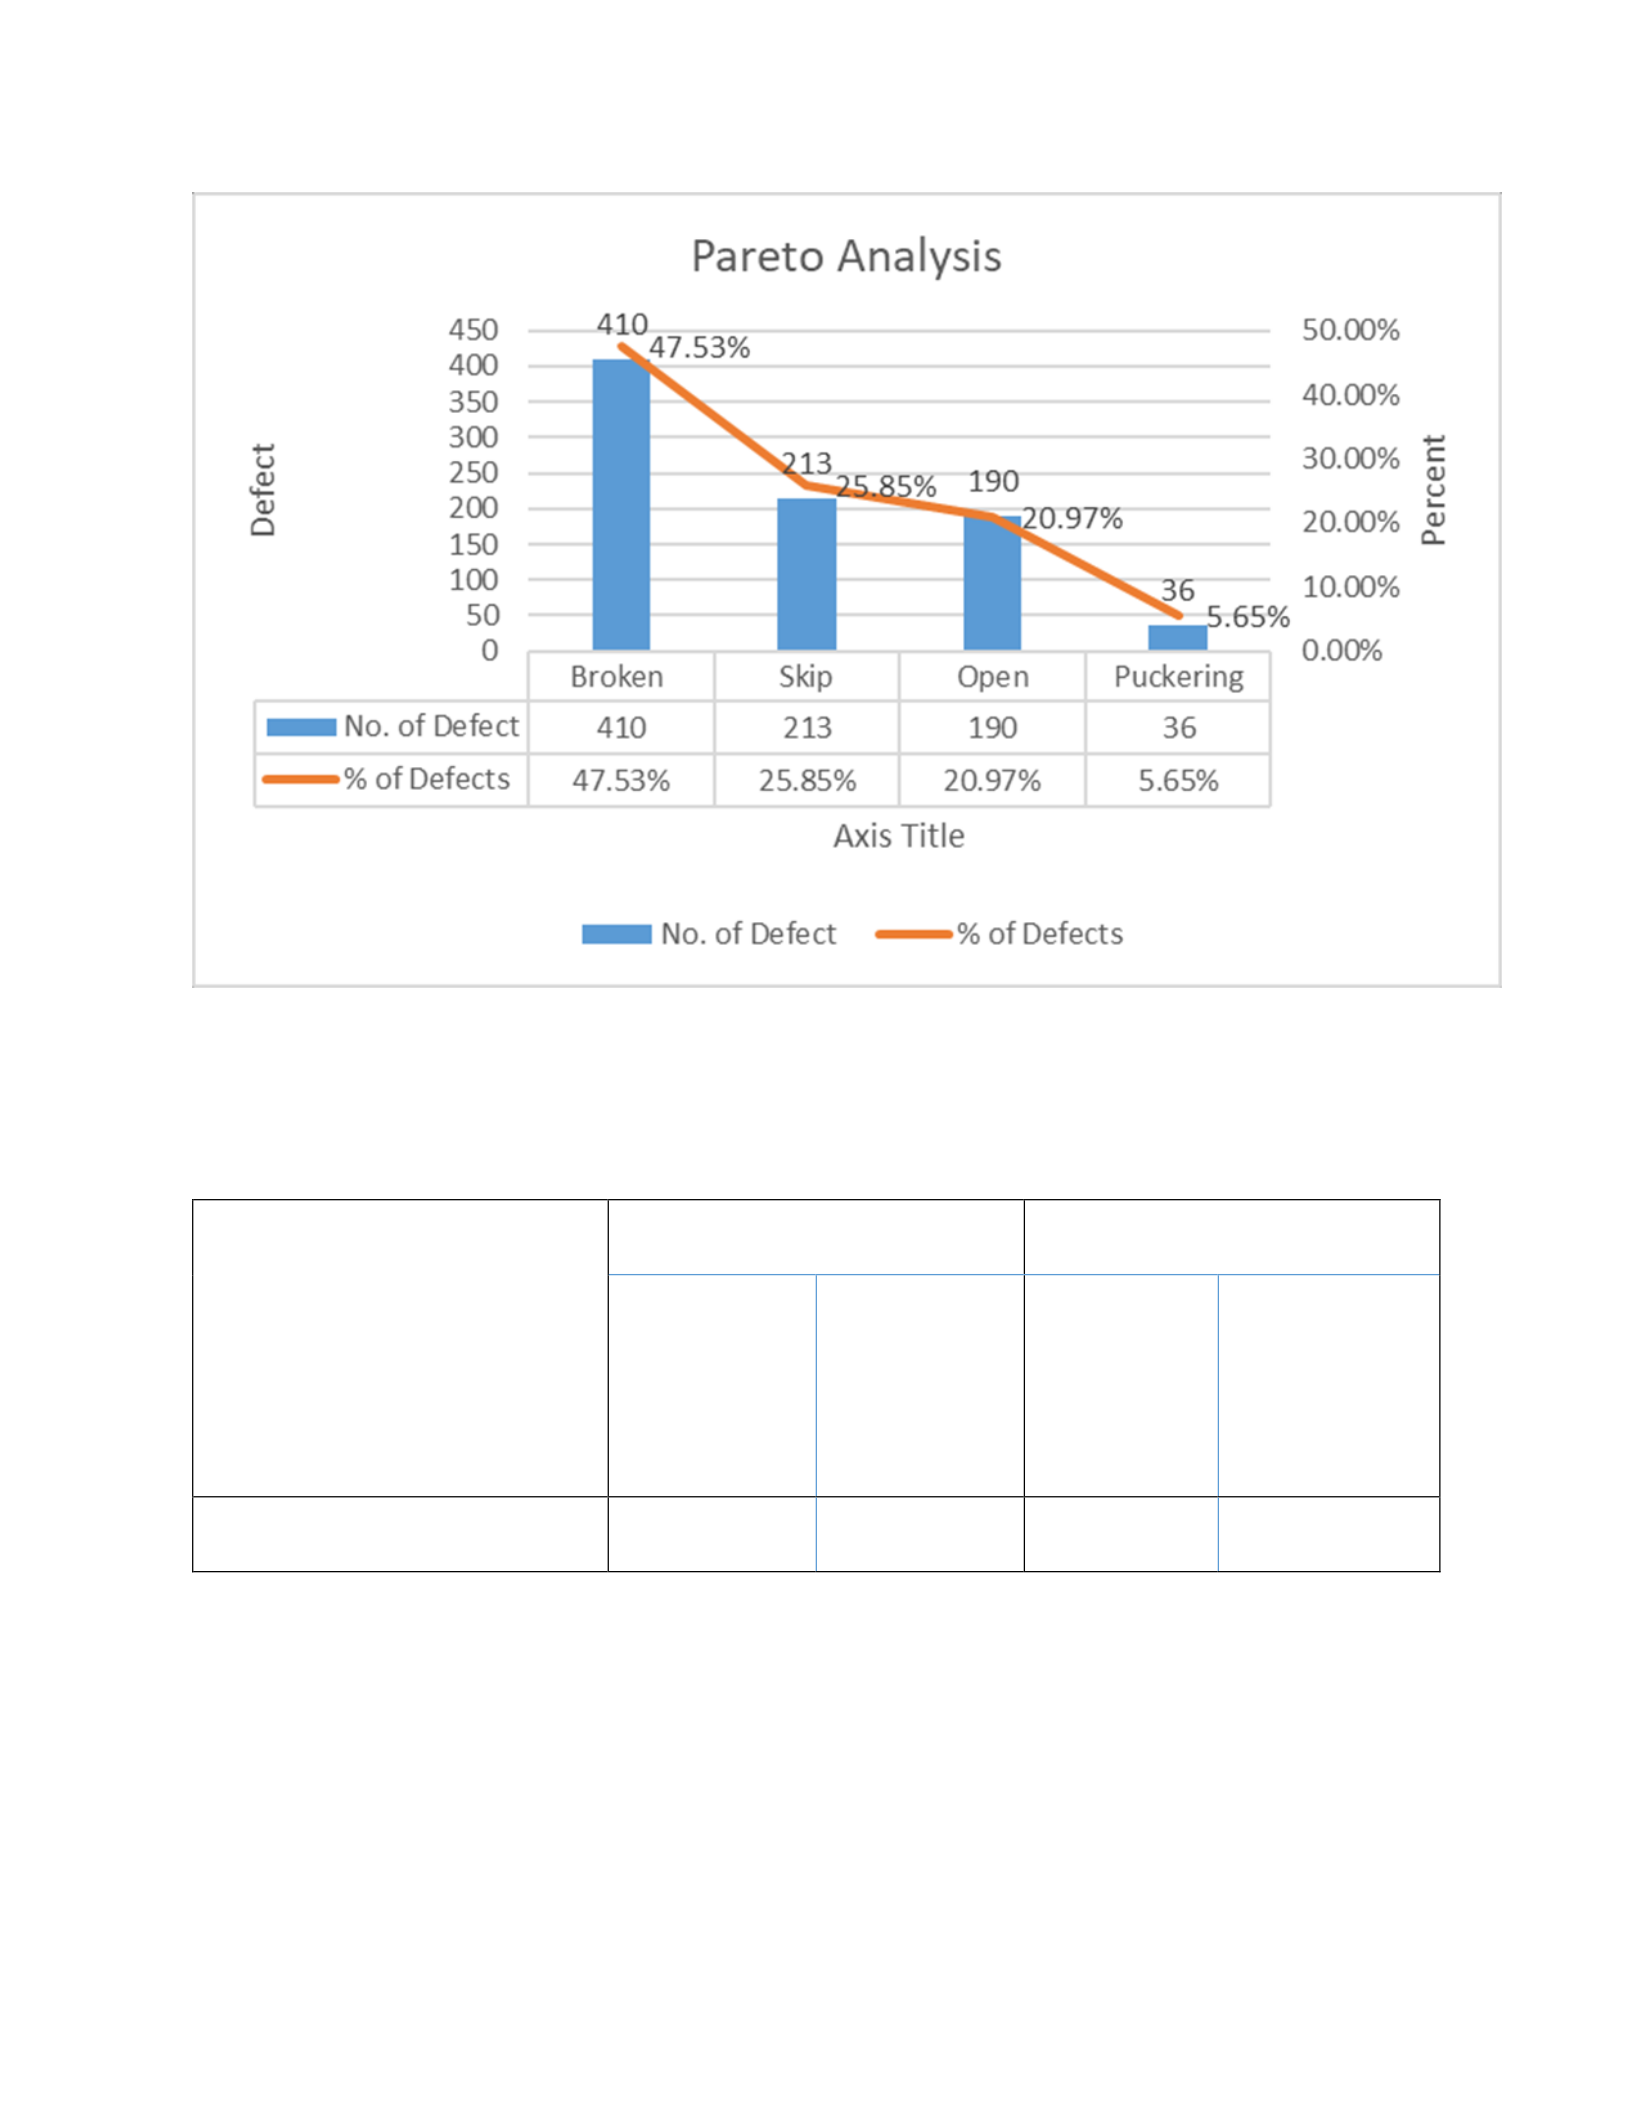
DMAIC (DRAFT) CASE STUDY
10
Table 4 (Rahman et., 2017)
Manufacturing process current and expected states
Major Defect types
Number of Major defects
Sigma Level
Current
Performance
of process
Expected
Performance
of process
Current
Performance
of process
Expected
Performance
of process
Broken
410
170
1.6
3.4
3. Analyze Phase
This phase consists of analyzing the garment manufacturing system of Color Line Co. to
find ways to reduce the gap between the desired goal and the current Performance. Bridging the
gap will require the investigation of the root cause of the problem through a cause-effect diagram.

DMAIC (DRAFT) CASE STUDY
11
According to Tahiduzzaman et al., (2018), a fishbone diagram assists the firm to understand the
garment production process in sub-operations and the main changes to deal with the effect. The
improvement team at Color Line Co. carried out an analysis to identify the root cause of the broken
stitches. Based on the team experience and knowledge of the production process, the following
were the probable causes of the defect.
Figure 3 below is a fishbone diagram that illustrates the relationship between the causes
and effects on the product. According to Tahiduzzaman et al., (2018), when the diagram is
complete, firms can see the root causes and areas that require improvement to ensure that the
production process is effective and working efficiently. Five main factors are considered in this
diagram, known as the 5M; they include manpower, material, machinery, measurement, and
method (Ershadi et al., 2018). The additional factor is the environment which also affects the
production process. The root causes include improper threading, not following the cut mark, and
others caused the broken stitch defect. See the fishbone diagram (Tahiduzzaman et al., 2018).
Figure 3 (Tahiduzzaman et al., 2018)
Cause and Effect Diagram
DMAIC (DRAFT) CASE STUDY
12
Uneven Cutting part Poor Fabric Quality Unskilled
Mismatch of size Improper Thread Not following cut mark
Production Rush Improper Technique Improper feed dog
Follow up Thread Tension
Bobbin Tension
4. Improve Phase
Once the root cause is determined, the DMAIC's improvement phase focuses on
recognizing the solutions that will best suit to reduce the broken stitch defects. The design of
experiments is analyzed through the ANOVA tool, which highlights the effects of multiple factors
(Rahman et., 2017). This design also confirms that the parameters indeed harm the garment
manufacturing process leading to defective clothes. ANOVA model compares the difference in
statistics like illustrated below. The analysis results in table 5 show the effect in the complete
process that leads to the defect in garments.
Measurement
Material
Man
Broken
Stitch
Mother
Methods
Machines
DMAIC (DRAFT) CASE STUDY
13
Table 5 (Rahman et., 2017)
ANOVA with 5% level of significance
Source
Degree of
Freedom
Adj S.S.
Adj MSS
F-Value
P-Value
Defect
3
90.53
21.38
7.59
0.000
Parts
4
5.24
02.12
0.37
0,694
Process
21
75.62
03.83
1.22
0.214
Error
398
1228.04
3.075
Lack of fit
76
182.82
2.477
0.79
0.915
Pure error
320
1044.21
3.215
Total
429
1489.03
The P-value is statistically significant as it is less than 0.05. Color Line's improvement
team will need to make changes to the effects, such as not following the cut mark correctly to
ensure that the final products match the consumer's quality. Additionally, production planning in
the firm is a significant factor that needs to get addressed. Planning refers to seeing ahead of all
the steps taken to complete the manufacturing process and ensure it is done at the right time and
place. More so, every operation will eventually get performed at maximum efficiency.
5. Control Phase
This phase is the game-changer for the other four sections as it determines whether or not
the improvements needed will get abruptly adapted. Finding the problem and coming up with the
most appropriate solutions is not a huge bump as the real challenge in the implementation phase.
It takes time before the implementation starts showing changes, and regular evaluation is required
for the improvement team to ensure that they are still on track. Maintaining the improvement is

DMAIC (DRAFT) CASE STUDY
14
the difficult part, and this phase ensures that the implementation is successful in the long run
(Zaman & Zerin, 2017). The new methods are becoming the standard operating procedures that
require all employees within the garment factory to be part of the project for its success. The
control phase consists of the norm ways and transfers responsibilities to the appropriate individuals
within the production process.
After the implementation, the defect rate is expected to reduce until the desired result is
achieved. Additionally, the sigma level was at 1.6, which is also expected to increase with the
decrease in defect rate. The primary goal of this project is to reduce the defect rate by employing
LSS and DMAIC methodology to come up with the best solution for the strategy (Zaman & Zerin,
2017). The reduction of defects is targeted at increasing consumer satisfaction and offering them
garments that match their value for money. This goal was meant to reduce the costs of production
and losses the Color Line Co. has been undergoing.
Conclusion
The firm's competitive advantage is expected to be much better after the changes in the
defect rate, which will work towards guaranteeing the long-term operation of the business. Another
biblical principle that corresponds with this article is that humans were given the ability to make
moral choices. Genesis 2:15-17 states, "Then the Lord God took the man and put him in the garden
of Eden to tend and keep it. He then commanded the man, saying that every tree in the garden man
can freely eat but not form the tree of the knowledge of good and evil. The day that you eat, you
shall surely die" (King James Bible, 2017). Therefore, human beings were given the ability to
choose that which is right or wrong, and, in this case, correcting the errors from the garments is
the right choice.
DMAIC (DRAFT) CASE STUDY
15
References
Ershadi, M. J., Aiasi, R., & Kazemi, S. (2018). Root cause analysis in quality problem solving of
research information systems: a case study. International Journal of Productivity and
Quality Management, 24(2), 284-299.
George, M. L., Rowlands, D., Price, M., & Maxey, J., (2005). The lean six sigma pocket toolbook.
McGraw-Hill.
Hall, J. & Scott, T. (2016). Lean six sigma: A beginners guide to understanding and practicing
lean six sigma. CreateSpace Independent Publishing.
King James Bible. (2017). King James Bible Online.
https://www.kingjamesbibleonline.org/Psalms-25-21/ (Original work published 1769)
Mohamad, N., Ahmad, S., Samat, H. A., Seng, C. K., & Lazi, F. M. (2019, June). The Application
of DMAIC to Improve Production: Case Study for Single-Sided Flexible Printed Circuit
Board. In IOP Conference Series: Materials Science and Engineering (Vol. 530, No. 1, p.
012041). IOP Publishing. https://iopscience.iop.org/article/10.1088/1757-
899X/530/1/012041/pdf
Rahman, A., Shaju, S. U. C., Sarkar, S. K., Hashem, M. Z., Hasan, S. K., Mandal, R., & Islam, U.
(2017). A case study of six sigma define-measure-analyze-improve-control (DMAIC)
methodology in garment sector. Independent Journal of Management & Production, 8(4),
1309-1323. https://www.redalyc.org/pdf/4495/449553639009.pdf
Srinivasan, K., Muthu, S., Devadasan, S. R., & Sugumaran, C. (2016). Six Sigma through DMAIC
phases: a literature review. International Journal of Productivity and Quality Management,
17(2), 236-257.
DMAIC (DRAFT) CASE STUDY
16
Tahiduzzaman, M., Rahman, M., Dey, S. K., & Kapuria, T. K. (2018). Minimization of sewing
defects of the apparel industry in Bangladesh with 5S & PDCA. American Journal of
Industrial Engineering, 5(1), 17-24. DOI:10.12691/ajie-5-1-3
Tuna, S. (2018). Keeping track of garment production process and process improvement using
quality control techniques. Periodicals of Engineering and Natural Sciences, 6(1), 11-26.
http://dx.doi.org/10.21533/pen.v6i1.162
Yin, R. K. (2018). Case study research and applications: Design and methods, (6TH edition).
SAGE.
Zaman, D. M., & Zerin, N. H. (2017). Applying DMAIC methodology to reduce defects of sewing
section in RMG: a case study. American Journal of Industrial and Business Management,
7(12),1320.http://www.scirp.org/journal/PaperInformation.aspx?PaperID=81178&#abstr
act
BUSI 830 Mod/Wk7
Rubric
DMAIC Case Study (DRAFT) Grading Rubric
Criteria
Levels of Achievement
Content ‐ 35 Points
Advanced
Proficient
Developing
Not present
Case Study
‘Plan’
5 Points
(5)
4 to 5 points
Section provides a topic
sentence for doing a case
study and the study ‘plan’.
2 to 3 points
Section provides either the
topic sentence for doing a
case study or the study ‘plan’.
1 point
Section provides a bullet for
doing a case study or the
study ‘plan’.
0 points
Not completed
Define Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the Define Phase
(with bullets for key steps such
as: customers, problem
statement, resources, crucial
support, high-level process
map, etc.).
3 to 4 points
Section provides a topic
sentence for the Define Phase
(with bullets for only a few key
steps such as: customers,
problem statement, resources,
crucial support, high-level
process map, etc.).
1 to 2 points
Section provides a topic
sentence for the Define
Phase (with no bullets for
key steps such as:
customers, problem
statement, resources,
crucial support, high-level
process map, etc.).
0 points
Not completed or not
related to
requirements for the
section
Measure Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the Measure
Phase (includes key steps
such as: defects,
opportunities, units, metrics,
data collection plan,
validating the measurement
system, etc.).
3 to 4 points
Section provides a topic
sentence for the Measure
Phase (with bullets for only a
few key steps such as:
defects, opportunities, units,
metrics, data collection plan,
validating the measurement
system, etc.).
1 to 2 points
Section provides a topic
sentence for the Measure
Phase (with no bullets for
key steps such as: defects,
opportunities, units, metrics,
data collection plan,
validating the measurement
system, etc.).
0 points
Not completed
Analyze Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the analyze
phase (includes hey steps
such as: performance
objectives, value vs NVA,
opportunities to improve root
cause, variation, etc.)
3 to 4 points
Section provides a topic
sentence for the analyze
phase (with bullets for only a
few key steps such as:
performance objectives,
value vs NVA, opportunities
to improve root cause,
variation, etc.)
1 to 2 points
Section provides a topic
sentence for the analyze
phase (with no bullets for
key steps such as:
performance objectives,
value vs NVA, opportunities
to improve root cause,
variation, etc.)
0 points
Not completed
Improve Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the Improve
Phase (includes key steps
such as: experiments,
solutions, operating
tolerances, implementing the
best solution, etc.).
3 to 4 points
Section provides a topic
sentence for the Improve
Phase (with bullets for only a
few key steps such as:
experiments, solutions,
operating tolerances,
implementing the best
solution, etc.).
1 to 2 points
Section provides a topic
sentence for the Improve
Phase (with no bullets for
key steps such as:
experiments, solutions,
operating tolerances,
implementing the best
solution, etc.).
0 points
Not completed
BUSI 830 Mod/Wk7
Rubric
Control Phase
6 Points
(6)
5 to 6 points
Section provides a topic
sentence for the Control
Phase (includes key steps
such as: standards, process
control/ capability,
documentation/ report, etc.).
3 to 4 points
Section provides a topic
sentence for the Control
Phase (with bullets for only a
few key steps such as:
standards, process control/
capability, documentation/
report, etc.).
1 to 2 points
Section provides a topic
sentence for the Control
Phase (with no bullets for
key steps such as:
standards, process control/
capability, documentation/
report, etc.).
0 points
Not completed
Structure ‐ 15
Points
Advanced
Proficient
Developing
Not present
ID’d the Lean Six
Sigma Tools
5 Points
(5)
4 to 5 points
ID’d 3 or more Lean Six Sigma
Tools
2 to 3 points
ID’d 2 Lean Six Sigma Tools
1 point
ID’d 1 Lean Six Sigma Tools
0 points
no Lean Six Sigma
Tools
References and
Citations
5 Points
(1)
4 to 5 points
References >10
2 to 3 points
References = 10
1 point
References <10
0 points
No references
APA Format &
Structure
5 Points
(5)
4 to 5 points
Required section headings
included.
2 to 3 points
Most required section headings
included.
1 point
Partial section headings
included.
0 points
No structure
provided
46 > You have most of the points, but a lot of extraneous, misplaced content, unfocused or underdeveloped sections, formatting
issues. Great draft, but some work to do for final

Define-Measure-Analyze-Improve-Control Methodology in the Garment Industry
Student Name
Tutors Name
School of Business, Liberty University
Due Date
Author Note
(Student name)
By submitting this assignment, I attest this submission represents my work and not that of
another student, scholar, or internet source. I understand I am responsible for knowing
and correctly utilizing referencing and bibliographical guidelines. I have not submitted
this work for any other class. Correspondence concerning this article should be addressed
to (student name).

1
Abstract
Color Line Company has been experiencing defect in their garment production for some time now,
and the continuous rejection of products by the consumers is seeking improvement. The
improvement will include incorporating DMAIC methodology and Lean Six Sigma tools to
discover the root of the challenge. Unlike all manufacturing companies globally, having a large
consumer base is critical and reduces operating costs while still maintaining efficiency. When
employed appropriately, the DMAIC methodology can realize cost-saving and improved quality
in manufacturing processes. More so, to remain competitive in the industry, firms are expected to
develop strategies that can utilize the available resources effectively and efficiently at a low cost
to maximize returns.
Keywords: DMAIC, Lean Six Sigma, Defect, Sigma level, cost reduction, quality, VOC

2
Define-Measure-Analyze-Improve-Control Methodology in the Garment Industry
All manufacturing companies worldwide are faced with turbulent economic conditions
such as demand for quality, reduced lead time and global competition. In this case, the garment
industry in the U.S., known as the Color Lines Clothing firm, is working to remain competitive
in the industry and will need to work on several areas. These areas include but are not limited to
production cost reduction, improved quality of goods, and enhanced productivity. All these
factors can get met by implementing Six Sigma tools and DMAIC. DMAIC is a methodology
used to measure objectives and create a cycle that continuously improves a manufacturing sector
(Srinivasan et al., 2016). Color Lines Company has had several challenges with consumers
complaining of defects in their garments. The DMAIC Six Sigma can improve consumer
satisfaction by reducing the rate of defects in products (Zaman & Zerin, 2017). This article will
incorporate Lean Six Sigma tools to better define the defect problem at Color Lines Firm and
establish how to adjust improvements.
Case Study Plan
Clothing manufacturing consists of dividing the overall process such as sewing, cutting,
finishing into many operations necessary for making the product. Each particular stage must be
well completed to ensure that the final product is of quality. Color Lines is a garment making
company located in the U.S., and its manufacturing process is defective as consumers have been
complaining of poor quality for some time now. The company, therefore, has an obligation of
measuring its manufacturing process to find out the primary defect that is leading to the challenge.

3
Therefore, breaking down the manufacturing process into a reasonable number of sub-operations
will enable us to find out the root cause.
The Lean Six Sigma (LSS) method seeks to minimize waste and maximize consumer's
satisfaction. Consumer satisfaction is critical in ensuring that the business will remain in operation.
On the other hand, the better the production process, the higher chance of becoming competitive
in the garment industry. LLS approaches to process and quality improvement is DMAIC
methodology which systematically assists the organization in solving problems and improving the
productivity of their operations (Srinivasan et al., 2016). More so, the application of LSS can also
lead to benefits such as participation of employees in the projects, problem-solving, increase in
process knowledge, among others.
Six Sigma and DMAIC Application
In this article, the DMAIC methodology is used at the manufacturing floor of the Color
Lines Company. This method is structured to analyze the process in a detailed way them
implements the improvement required for change. Through this method, Color Lines Company
will have a better road map where the issue is dealt with from the start of the manufacturing process
to the end. A Six Sigma of 3.4 defects per million opportunities is considered normal, and any
figure above that is too high (George et al., 2005). The benefits reaped from employing Six Sigma
are not only applicable to the manufacturing industry like in this case as it has been tested in other
industries as well, such as the service sector. Six Sigma consist of several approaches that work
towards improving the process and quality of products. The DMAIC methodology consists of five
interconnected stages and works concurrently to solve a firm’s challenge. The process stages can
be defined as follows:
4
What is the
problem?
What information
is available
What is the cause of
the problem?
What are the
right solutions
we have?
What are the
recommendations
or plan for
implementation?
This method allows organizations to make decisions based on accurate and scientific facts
rather than experience and previously acquired knowledge. Color Line firms first line of defect
rate was more than 59%, while the projects defect rate is 42%. The project's target is to reduce the
defect rate to less than 2%, which will ensure that consumer needs and requirements are met. As
discussed earlier the DMAIC approach will get used to deal with the defect while the Pareto effect
tool will also be combined. A cause and effect diagram will also get used to finding better the
relation between the causes that lead to the defect and define the root cause of the defects.
1. Define Phase
A project summary is a tool issued to document all the targets of the project and what Color
Line Co. intend to achieve. According to Yin (2018), a project summary is helpful to ensure that
the goals, VOC, teams role in the project are well outlined. This arrangement of an action plan is
essential in ensuring that the ultimate goal is achieved and no step is missed. Meeting consumer
Define
Measure
Analyze
Improve
Control
Figure 1: DMAIC Process (Rahman et al., 2017)
5
needs is one of the responsibilities that companies have to meet to ensure that the goods meet
recommended criteria. One of the biblical principles relevant to this section is moral order which
has to do with the obligation of doing what is right. God's moral order is designed for the good of
all humans and the surrounding community. Romans 13:3 states, "Do you want to be afraid of the
authority? Do what is good, and you will receive praise from the same" (King James Bible,
1769/2017). Companies should do what is morally right and work for the benefit of the larger
community.
Table 1: Color Line Company Project Summary (Rahman et., 2017)
Title of Project:
Defect reduction in the production of garments
Background and reason for selecting
project:
There has been a large number of garments that
consumers have rejected because they are
defective. This problem has led to several
losses for Color Line Co., such as materials,
time used, and increased consumer
dissatisfaction, which negatively impacts the
business.
The goal of the project:
Reduce defects by 35% with the use of
DMAIC and Six Sigma as part of the
manufacturing procedures
VOC:
High product quality
Expected consumer benefit:
Attained value for money and desired
qualifications of quality met
Expected financial benefit:
Cost-saving from defect reduction
6
Team members:
Employees, Production Manager, Factory
floor operator and improvement project leader
A Six Sigma project needs to get selected based on the firm's issues, which should be
directly related to achieving consumer expectations. The chosen project of Color Lines Company
focuses on having a significant impact on consumer satisfaction with their garments, which meets
their value for money. The project selected in the firm was to reduce the quality defects in the
garments, which will also save the organization money in terms of production. According to
George et al. (2009), listening to consumers is critical for all businesses to succeed in the long run.
The voice of consumer concept (VOC) identifying what the customers want and serving them as
the top priority. On the other hand, the defects in the production process become a priority for the
firm to improve and work on a better strategy to prevent future defects in their system.
2. Measure Phase
This phase consists of creating metrics that are reliable in monitoring the progress towards
achieving the goal. In this project, the measure phase defines and selects an effective measure to
clarify the significant defects required to get reduced. The defects will get outlined, the highest to
the lowest, and the total number of defects should add up to 100%. The defects get analyzed for
only two months from November 1st, December 31st 2018. Table 3 shows the highest defects cause
was broken stitches, which contributed to 47.53% of the overall defects.
7
Table 2: Defects before Changes (Rahman et al., 2017)
Type of Defect
No. of Defects
% of Defects
Broken
410
47.53
Skip
213
25.85
Open
190
20.97
Puckering
36
5.65
Total
849
100
3. Analyze Phase
Pareto analysis is essential to identify the most occurring defect and prioritize the critical
problem which needs to get tackled immediately (Tuna, 2018). Out of the four defects, the
improvement team and Color Line Co. decided to focus on reducing the broken stitch first. The
broken stitch has a sigma level of 1.6, and this calculation has allowed the team to have more
details of the current state of the clothing manufacturing process. The Sigma level is illustrated in
table 4.
Figure 2: Pareto for Project Line Defect before Improvement (Rahman et al., 2017)
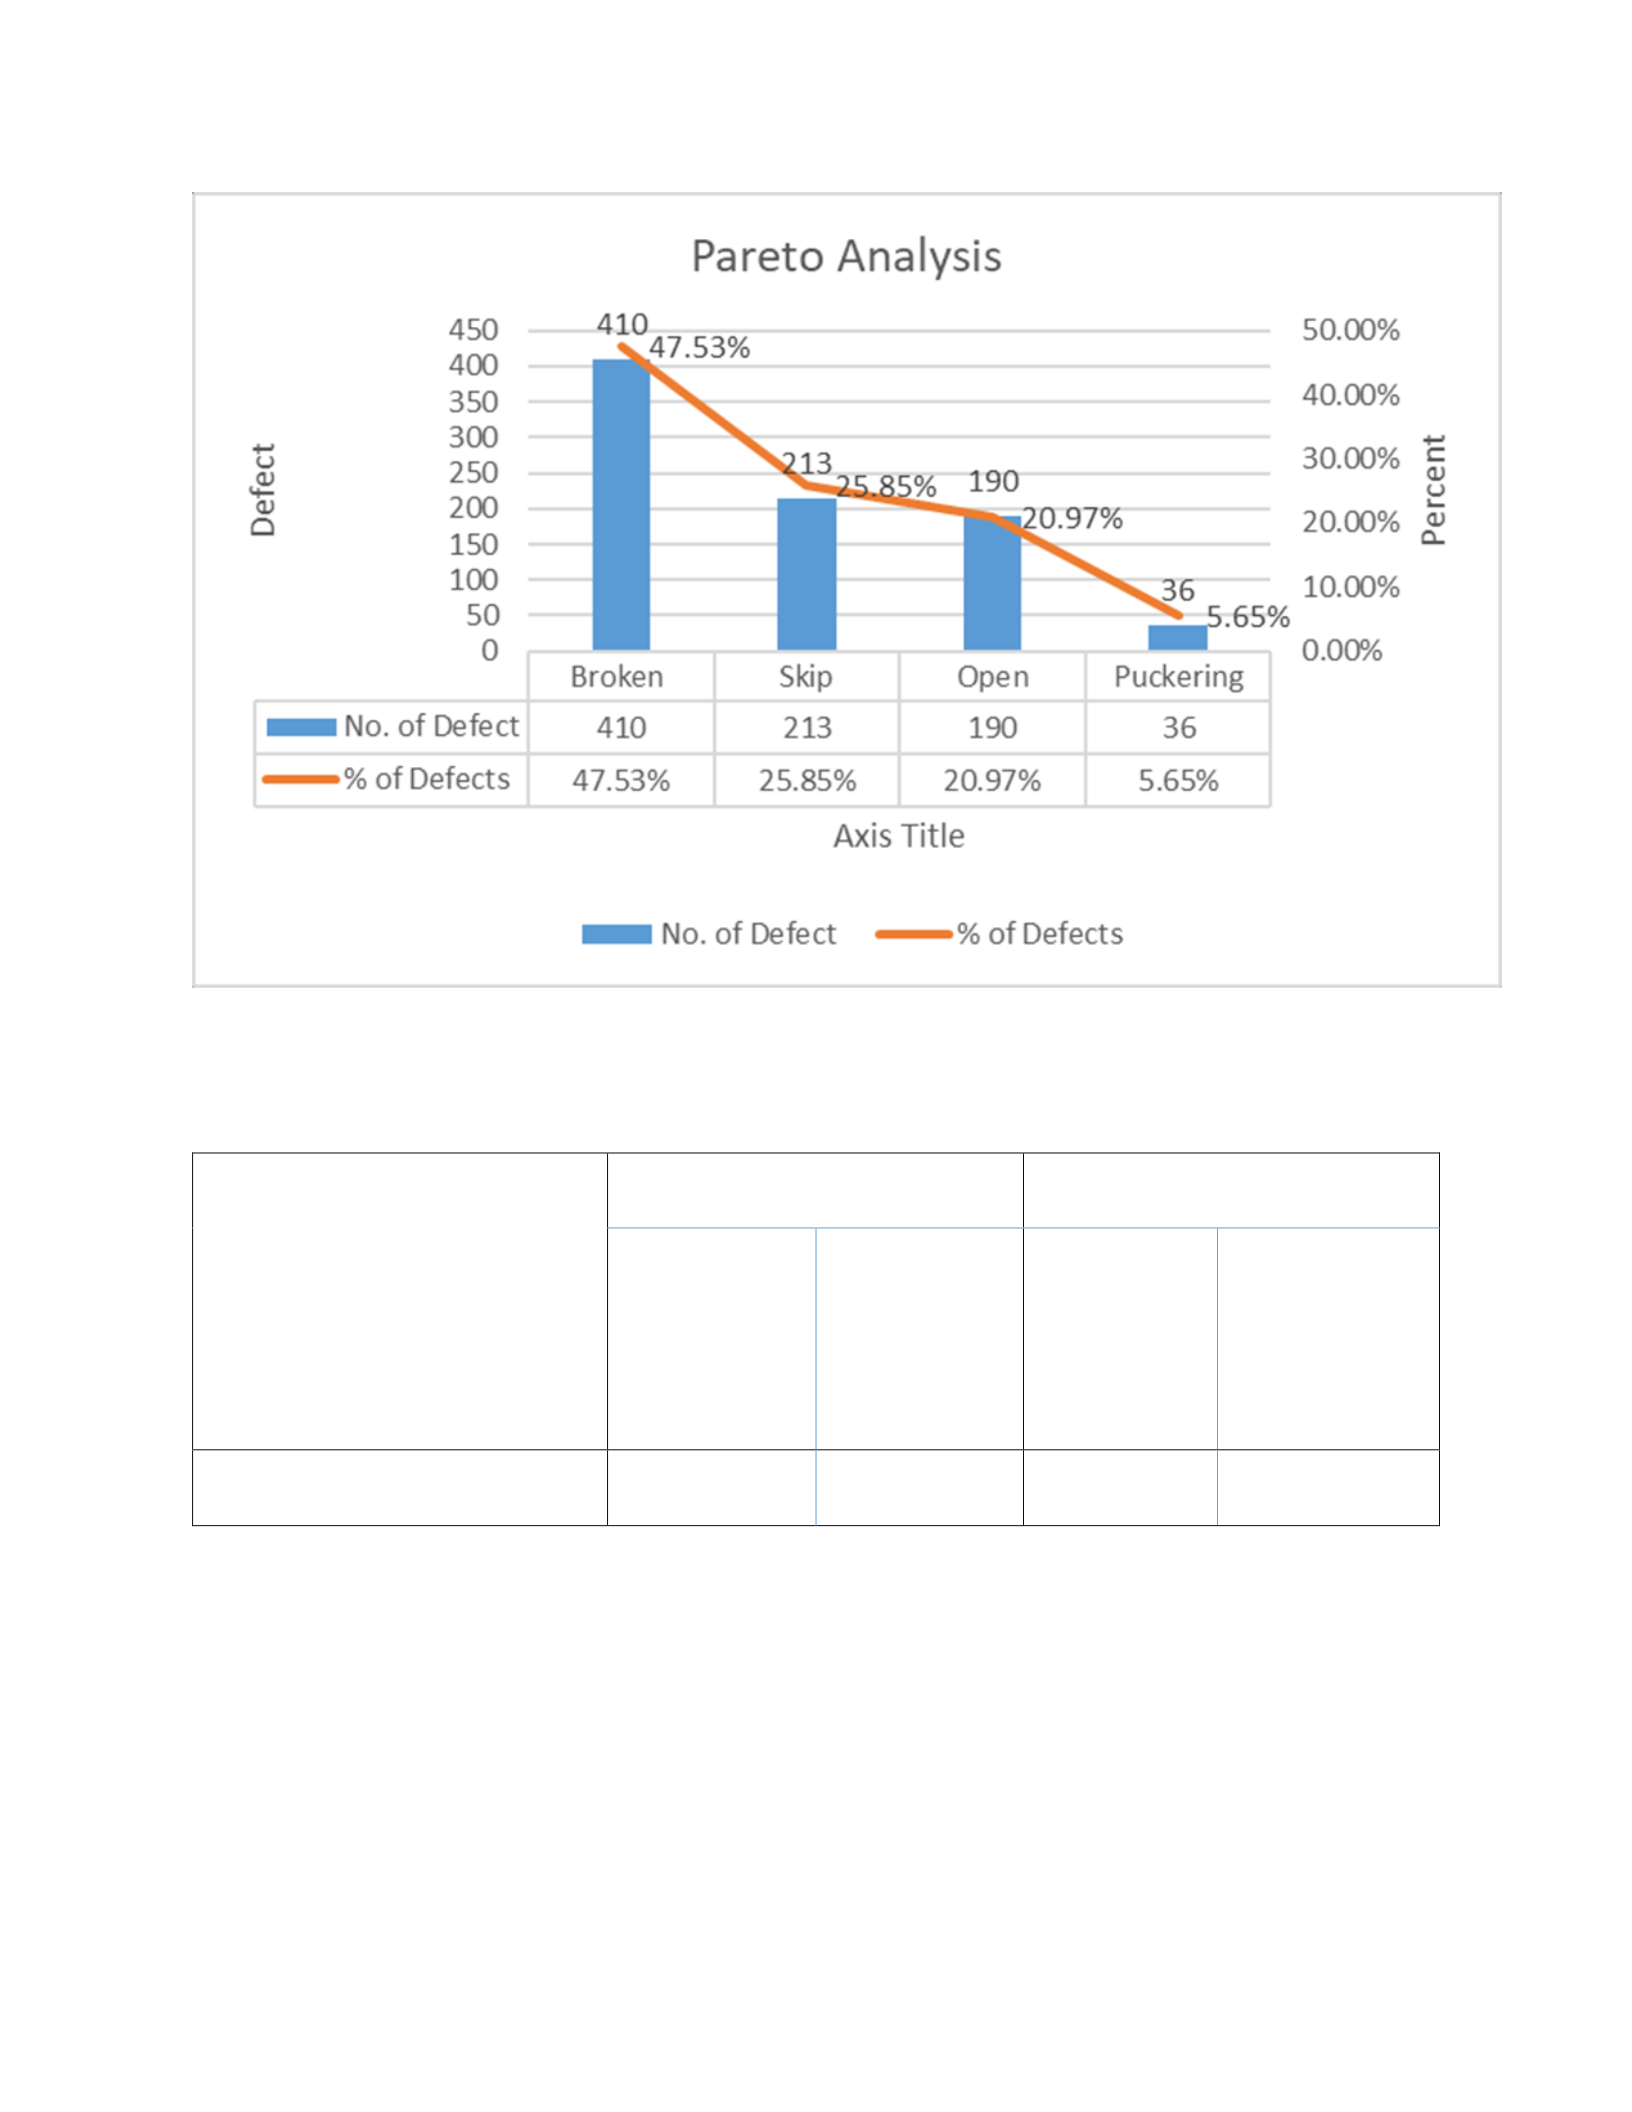
8
Table 3: Manufacturing process current and expected states (Rahman et al., 2017)
Major Defect types
Number of Major defects
Sigma Level
Current
Performance
of process
Expected
Performance
of process
Current
Performance
of process
Expected
Performance
of process
Broken
410
170
1.6
3.4
This phase consists of analyzing the garment manufacturing system of Color Line Co. to
find ways to reduce the gap between the desired goal and the current Performance. Bridging the
gap will require the investigation of the root cause of the problem through a cause-effect diagram.
According to Tahiduzzaman et al. (2018), a fishbone diagram assists the firm to understand the
9
garment production process in sub-operations and the main changes to deal with the effect. The
improvement team at Color Line Co. carried out an analysis to identify the root cause of the broken
stitches. Based on the team experience and knowledge of the production process, the following
were the probable causes of the defect.
Figure 3 below is a fishbone diagram that illustrates the relationship between the causes
and effects on the product. According to Tahiduzzaman et al. (2018), when the diagram is
complete, firms can see the root causes and areas that require improvement to ensure that the
production process is effective and working efficiently. Five main factors are considered in this
diagram, known as the 5M; they include manpower, material, machinery, measurement and
method (Ershadi et al., 2018). The additional factor is the environment which also affects the
production process. The root causes include improper threading, not following the cut mark, and
others caused the broken stitch defect.
Measurement
Material
Man
Figure 3: Cause and Effect Diagram (Rahman et al., 2017)
10
Uneven Cutting part Poor Fabric Quality Unskilled
Mismatch of size Improper Thread Not following cut mark
Production Rush Improper Technique Improper feed dog
Follow up Thread Tension
Bobbin Tension
4. Improve Phase
Once the root cause is determined, the DMAIC's improvement phase focuses on
recognizing the solutions that will best suit to reduce the broken stitch defects. The design of
experiments is analyzed through the ANOVA tool, which highlights the effects of multiple factors.
This design also confirms that the parameters indeed harm the garment manufacturing process
leading to defective clothes. ANOVA model compares the difference in statistics like illustrated
below. The analysis results in table 5 show the effect in the complete process that leads to the
defect in garments.
Table 4: ANOVA with 5% level of significance (Rahman et al., 2017)
Source
Degree of
Freedom
Adj S.S.
Adj MSS
F-Value
P-Value
11
Defect
3
90.53
21.38
7.59
0.000
Parts
4
5.24
02.12
0.37
0,694
Process
21
75.62
03.83
1.22
0.214
Error
398
1228.04
3.075
Lack of fit
76
182.82
2.477
0.79
0.915
Pure error
320
1044.21
3.215
Total
429
1489.03
The P-value is statistically significant as it is less than 0.05. Color Line's improvement
team will need to make changes to the effects, such as not following the cut mark correctly to
ensure that the final products match the consumer's quality. Additionally, production planning in
the firm is a significant factor that needs to get addressed. Planning refers to seeing ahead of all
the steps taken to complete the manufacturing process and ensure it done at the right time and
place. More so, every operation will eventually get performed at maximum efficiency.
5. Control Phase
This phase is the game-changer for the other four sections as it determines whether or not
the improvements needed will get abruptly adapted. Finding the problem and coming up with the
most appropriate solutions is not a huge bump as the real challenge in the implementation phase.
It takes time before the implementation starts showing changes, and regular evaluation is required
for the improvement team to ensure that they are still on track. Some of the tools that can get used
include what if analysis as well as a checklist. Maintaining the improvement is the difficult part,
and this phase ensures that the implementation is successful in the long run (Zaman & Zerin, 2017).
The new methods are becoming the standard operating procedures that require all employees
within the garment factory to be part of the project for its success. The control phase consists of

12
the norm ways and transfers responsibilities to the appropriate individuals within the production
process.
After the implementation, the defect rate is expected to reduce until the desired result is
achieved. Additionally, the sigma level was at 1.6, which is also expected to increase with the
decrease in defect rate. The primary goal of this project is to reduce the defect rate by employing
LSS and DMAIC methodology to come up with the best solution for the strategy (Zaman & Zerin,
2017). The reduction of defects is targeted at increasing consumer satisfaction and offering them
garments that match their value for money. This goal was meant to reduce the costs of production
and losses the Color Line Co. have been undergoing.
Conclusion
The firm's competitive advantage is expected to be much better after the changes in the
defect rate, which will work towards guaranteeing the long-term operation of the business. Another
biblical principle that corresponds with this article is that humans were given the ability to make
moral choices. Genesis 2:15-17 states, "Then the Lord God took the man and put him in the garden
of Eden to tend and keep it. He then commanded the man, saying that every tree in the garden man
can freely eat but not form the tree of the knowledge of good and evil. The day that you eat, you
shall surely die" (King James Bible, 1769/2017). Therefore, human beings were given the ability
to choose that which is right or wrong and in this case, correcting the errors from the garments is
the right choice. Based on certain biblical worldviews integrated with moral values human beings
as individuals make choices on choosing the best options. Therefore, Color Line’s option to choose
to change the defects in their manufacturing process was to benefit the company and the
consumers. The step was essential as it was indeed the right move to make.
13
References
Ershadi, M. J., Aiasi, R., & Kazemi, S. (2018). Root cause analysis in quality problem solving of
research information systems: a case study. International Journal of Productivity and
Quality Management, 24(2), 284-299. https://doi.org/10.1504/IJPQM.2018.091797
George, M. L., Rowlands, D., Price, M., & Maxey, J., (2005). The Lean Six Sigma Pocket
Toolbook. New York, NY: McGraw-Hill. ISBN: 9780071441193.
Hall, J. & Scott, T. (2016). Lean Six Sigma: A Beginners Guide to Understanding and Practicing
Lean Six Sigma. Columbia, SC: Create Space Receiving. ISBN: 9781541059559.
King James Bible. (2017). King James Bible Online.
https://www.kingjamesbibleonline.org/Psalms-25-21/ (Original work published 1769)
Mohamad, N., Ahmad, S., Samat, H. A., Seng, C. K., & Lazi, F. M. (2019, June). The Application
of DMAIC to Improve Production: Case Study for Single-Sided Flexible Printed Circuit
Board. In IOP Conference Series: Materials Science and Engineering (Vol. 530, No. 1, p.
012041). IOP Publishing. https://iopscience.iop.org/article/10.1088/1757-
899X/530/1/012041/pdf
Rahman, A., Shaju, S. U. C., Sarkar, S. K., Hashem, M. Z., Hasan, S. K., Mandal, R., & Islam, U.
(2017). A case study of six sigma define-measure-analyze-improve-control (DMAIC)
methodology in garment sector. Independent Journal of Management & Production, 8(4),
1309-1323. https://www.redalyc.org/pdf/4495/449553639009.pdf
14
Srinivasan, K., Muthu, S., Devadasan, S. R., & Sugumaran, C. (2016). Six Sigma through DMAIC
phases: a literature review. International Journal of Productivity and Quality Management,
17(2), 236-257.
Tahiduzzaman, M., Rahman, M., Dey, S. K., & Kapuria, T. K. (2018). Minimization of sewing
defects of the apparel industry in Bangladesh with 5S & PDCA. American Journal of
Industrial Engineering, 5(1), 17-24. DOI:10.12691/ajie-5-1-3
Tuna, S. (2018). Keeping track of garment production process and process improvement using
quality control techniques. Periodicals of Engineering and Natural Sciences, 6(1), 11-26.
http://dx.doi.org/10.21533/pen.v6i1.162
Yin, R. K. (2018). Case study research and applications. Sage.
Zaman, D. M., & Zerin, N. H. (2017). Applying DMAIC methodology to reduce defects of sewing
section in RMG: a case study. American Journal of Industrial and Business Management,
7(12),1320.http://www.scirp.org/journal/PaperInformation.aspx?PaperID=81178&#abstr
act

