


Define-Measure-Analyze-Improve-Control Methodology in the Garment Industry
Student Name
Tutors Name
School of Business, Liberty University
Due Date
Author Note
(Student name)
By submitting this assignment, I attest this submission represents my work and not that of
another student, scholar, or internet source. I understand I am responsible for knowing
and correctly utilizing referencing and bibliographical guidelines. I have not submitted
this work for any other class. Correspondence concerning this article should be addressed
to (student name).

1
Abstract
Color Line Company has been experiencing defect in their garment production for some time
now, and the continuous rejection of products by the consumers is seeking improvement. The
improvement will include incorporating DMAIC methodology and Lean Six Sigma tools to
discover the root of the challenge. Unlike all manufacturing companies globally, having a large
consumer base is critical and reduces operating costs while still maintaining efficiency. When
employed appropriately, the DMAIC methodology can realize cost-saving and improved quality
in manufacturing processes. More so, to remain competitive in the industry, firms are expected to
develop strategies that can utilize the available resources effectively and efficiently at a low cost
to maximize returns.
Keywords: DMAIC, Lean Six Sigma, Defect, Sigma level, cost reduction, quality, VOC

2
Define-Measure-Analyze-Improve-Control Methodology in the Garment Industry
All manufacturing companies worldwide are faced with turbulent economic conditions
such as demand for quality, reduced lead time and global competition. In this case, the garment
industry in the U.S., known as the Color Lines Clothing firm, is working to remain competitive
in the industry and will need to work on several areas. These areas include but are not limited to
production cost reduction, improved quality of goods, and enhanced productivity. All these
factors can get met by implementing Six Sigma tools and DMAIC. DMAIC is a methodology
used to measure objectives and create a cycle that continuously improves a manufacturing sector
(Srinivasan et al., 2016). Color Lines Company has had several challenges with consumers
complaining of defects in their garments. The DMAIC Six Sigma can improve consumer
satisfaction by reducing the rate of defects in products (Zaman & Zerin, 2017). This article will
incorporate Lean Six Sigma tools to better define the defect problem at Color Lines Firm and
establish how to adjust improvements.
Case Study Plan
Clothing manufacturing consists of dividing the overall process such as sewing, cutting,
finishing into many operations necessary for making the product. Each particular stage must be
well completed to ensure that the final product is of quality. Color Lines is a garment making
company located in the U.S., and its manufacturing process is defective as consumers have been
complaining of poor quality for some time now. The company, therefore, has an obligation of
measuring its manufacturing process to find out the primary defect that is leading to the
3
challenge. Therefore, breaking down the manufacturing process into a reasonable number of sub-
operations will enable us to find out the root cause.
The Lean Six Sigma (LSS) method seeks to minimize waste and maximize consumer's
satisfaction. Consumer satisfaction is critical in ensuring that the business will remain in
operation. On the other hand, the better the production process, the higher chance of becoming
competitive in the garment industry. LLS approaches to process and quality improvement is
DMAIC methodology which systematically assists the organization in solving problems and
improving the productivity of their operations (Srinivasan et al., 2016). More so, the application
of LSS can also lead to benefits such as participation of employees in the projects, problem-
solving, increase in process knowledge, among others.
Seven Waste of Lean Manufacturing
Table 1: (Mohamad et al., 2019)
Type of Waste Explanation
Transportation With the movement of a product from one place to another,
either from the factory to the retail shop. This movement
does not add any value to the product.
Inventory In most cases, firms tend to hold rawer materials than is
required to produce goods and services in response to the
demand from the consumers.
Waiting This waste occurs when workers are meant to work slowly or
to stop as they wait for a previous step in a process to be
complete. On the other hand, employees can slowly work
4
since they have run out of raw materials.
Over-processing For example, the garments can have extra pockets included
or a design that will not be visible, which is more valuable
than the consumer requires.
Motion The waste of motion refers to when a product is moving and
not necessarily because of work. For instance, once the
garments are completed, they may need to get moved to the
warehouse for storage which is not beneficial.
Defect This waste refers to when the final goods are not what the
consumer ordered. Defects result from many challenges,
such as missed steps in the manufacturing process, which
makes a slight change in the design and quality of the
product (Hall & Scott, 2016).
Overproduction This waste refers to the production of too many goods that
surpass the demand, which leads to excessive inventory.
Six Sigma and DMAIC Application
In this article, the DMAIC methodology is used at the manufacturing floor of the Color
Lines Company. This method is structured to analyze the process in a detailed way them
implements the improvement required for change. Through this method, Color Lines Company
will have a better road map where the issue is dealt with from the start of the manufacturing
process to the end. A Six Sigma of 3.4 defects per million opportunities is considered normal,
and any figure above that is too high (George et al., 2005). The benefits reaped from employing
5
Six Sigma are not only applicable to the manufacturing industry like in this case as it has been
tested in other industries as well, such as the service sector. Six Sigma consist of several
approaches that work towards improving the process and quality of products. The DMAIC
methodology consists of five interconnected stages and works concurrently to solve a firm’s
challenge. The process stages can be defined as follows:
What is the
problem?
What information
is available
What is the cause
of the problem?
What are the
right solutions
we have?
What are the
recommendations
or plan for
implementation?
This method allows organizations to make decisions based on accurate and scientific
facts rather than experience and previously acquired knowledge. Color Line firms first line of
defect rate was more than 59%, while the projects defect rate is 42%. The project's target is to
reduce the defect rate to less than 2%, which will ensure that consumer needs and requirements
are met. As discussed earlier the DMAIC approach will get used to deal with the defect while the
Pareto effect tool will also be combined. A cause and effect diagram will also get used to
Define Measure Analyze Improve Control
Figure 1: DMAIC Process (Rahman et al., 2017)
6
finding better the relation between the causes that lead to the defect and define the root cause of
the defects.
1. Define Phase
A project summary is a tool issued to document all the targets of the project and what
Color Line Co. intend to achieve. According to Yin (2018), a project summary is helpful to
ensure that the goals, VOC, teams role in the project are well outlined. This arrangement of an
action plan is essential in ensuring that the ultimate goal is achieved and no step is missed.
Meeting consumer needs is one of the responsibilities that companies have to meet to ensure that
the goods meet recommended criteria. One of the biblical principles relevant to this section is
moral order which has to do with the obligation of doing what is right. God's moral order is
designed for the good of all humans and the surrounding community. Romans 13:3 states, "Do
you want to be afraid of the authority? Do what is good, and you will receive praise from the
same" (King James Bible, 1769/2017). Companies should do what is morally right and work for
the benefit of the larger community.
Table 2: Color Line Company Project Summary (Rahman et., 2017)
Title of Project: Defect reduction in the production of
garments
Background and reason for selecting
project:
There has been a large number of garments
that consumers have rejected because they are
defective. This problem has led to several
losses for Color Line Co., such as materials,
time used, and increased consumer
7
dissatisfaction, which negatively impacts the
business.
The goal of the project: Reduce defects by 35% with the use of
DMAIC and Six Sigma as part of the
manufacturing procedures
VOC: High product quality
Expected consumer benefit: Attained value for money and desired
qualifications of quality met
Expected financial benefit: Cost-saving from defect reduction
Team members: Employees, Production Manager, Factory
floor operator and improvement project leader
A Six Sigma project needs to get selected based on the firm's issues, which should be
directly related to achieving consumer expectations. The chosen project of Color Lines Company
focuses on having a significant impact on consumer satisfaction with their garments, which
meets their value for money. The project selected in the firm was to reduce the quality defects in
the garments, which will also save the organization money in terms of production. According to
George et al. (2009), listening to consumers is critical for all businesses to succeed in the long
run. The voice of consumer concept (VOC) identifying what the customers want and serving
them as the top priority. On the other hand, the defects in the production process become a
priority for the firm to improve and work on a better strategy to prevent future defects in their
system.
8
2. Measure Phase
This phase consists of creating metrics that are reliable in monitoring the progress
towards achieving the goal. In this project, the measure phase defines and selects an effective
measure to clarify the significant defects required to get reduced. The defects will get outlined,
the highest to the lowest, and the total number of defects should add up to 100%. The defects get
analyzed for only two months from November 1st, December 31st 2018. Table 3 shows the
highest defects cause was broken stitches, which contributed to 47.53% of the overall defects.
Table 3: Defects before Changes (Rahman et al., 2017)
Type of Defect No. of Defects % of Defects
Broken 410 47.53
Skip 213 25.85
Open 190 20.97
Puckering 36 5.65
Total 849 100
3. Analyze Phase
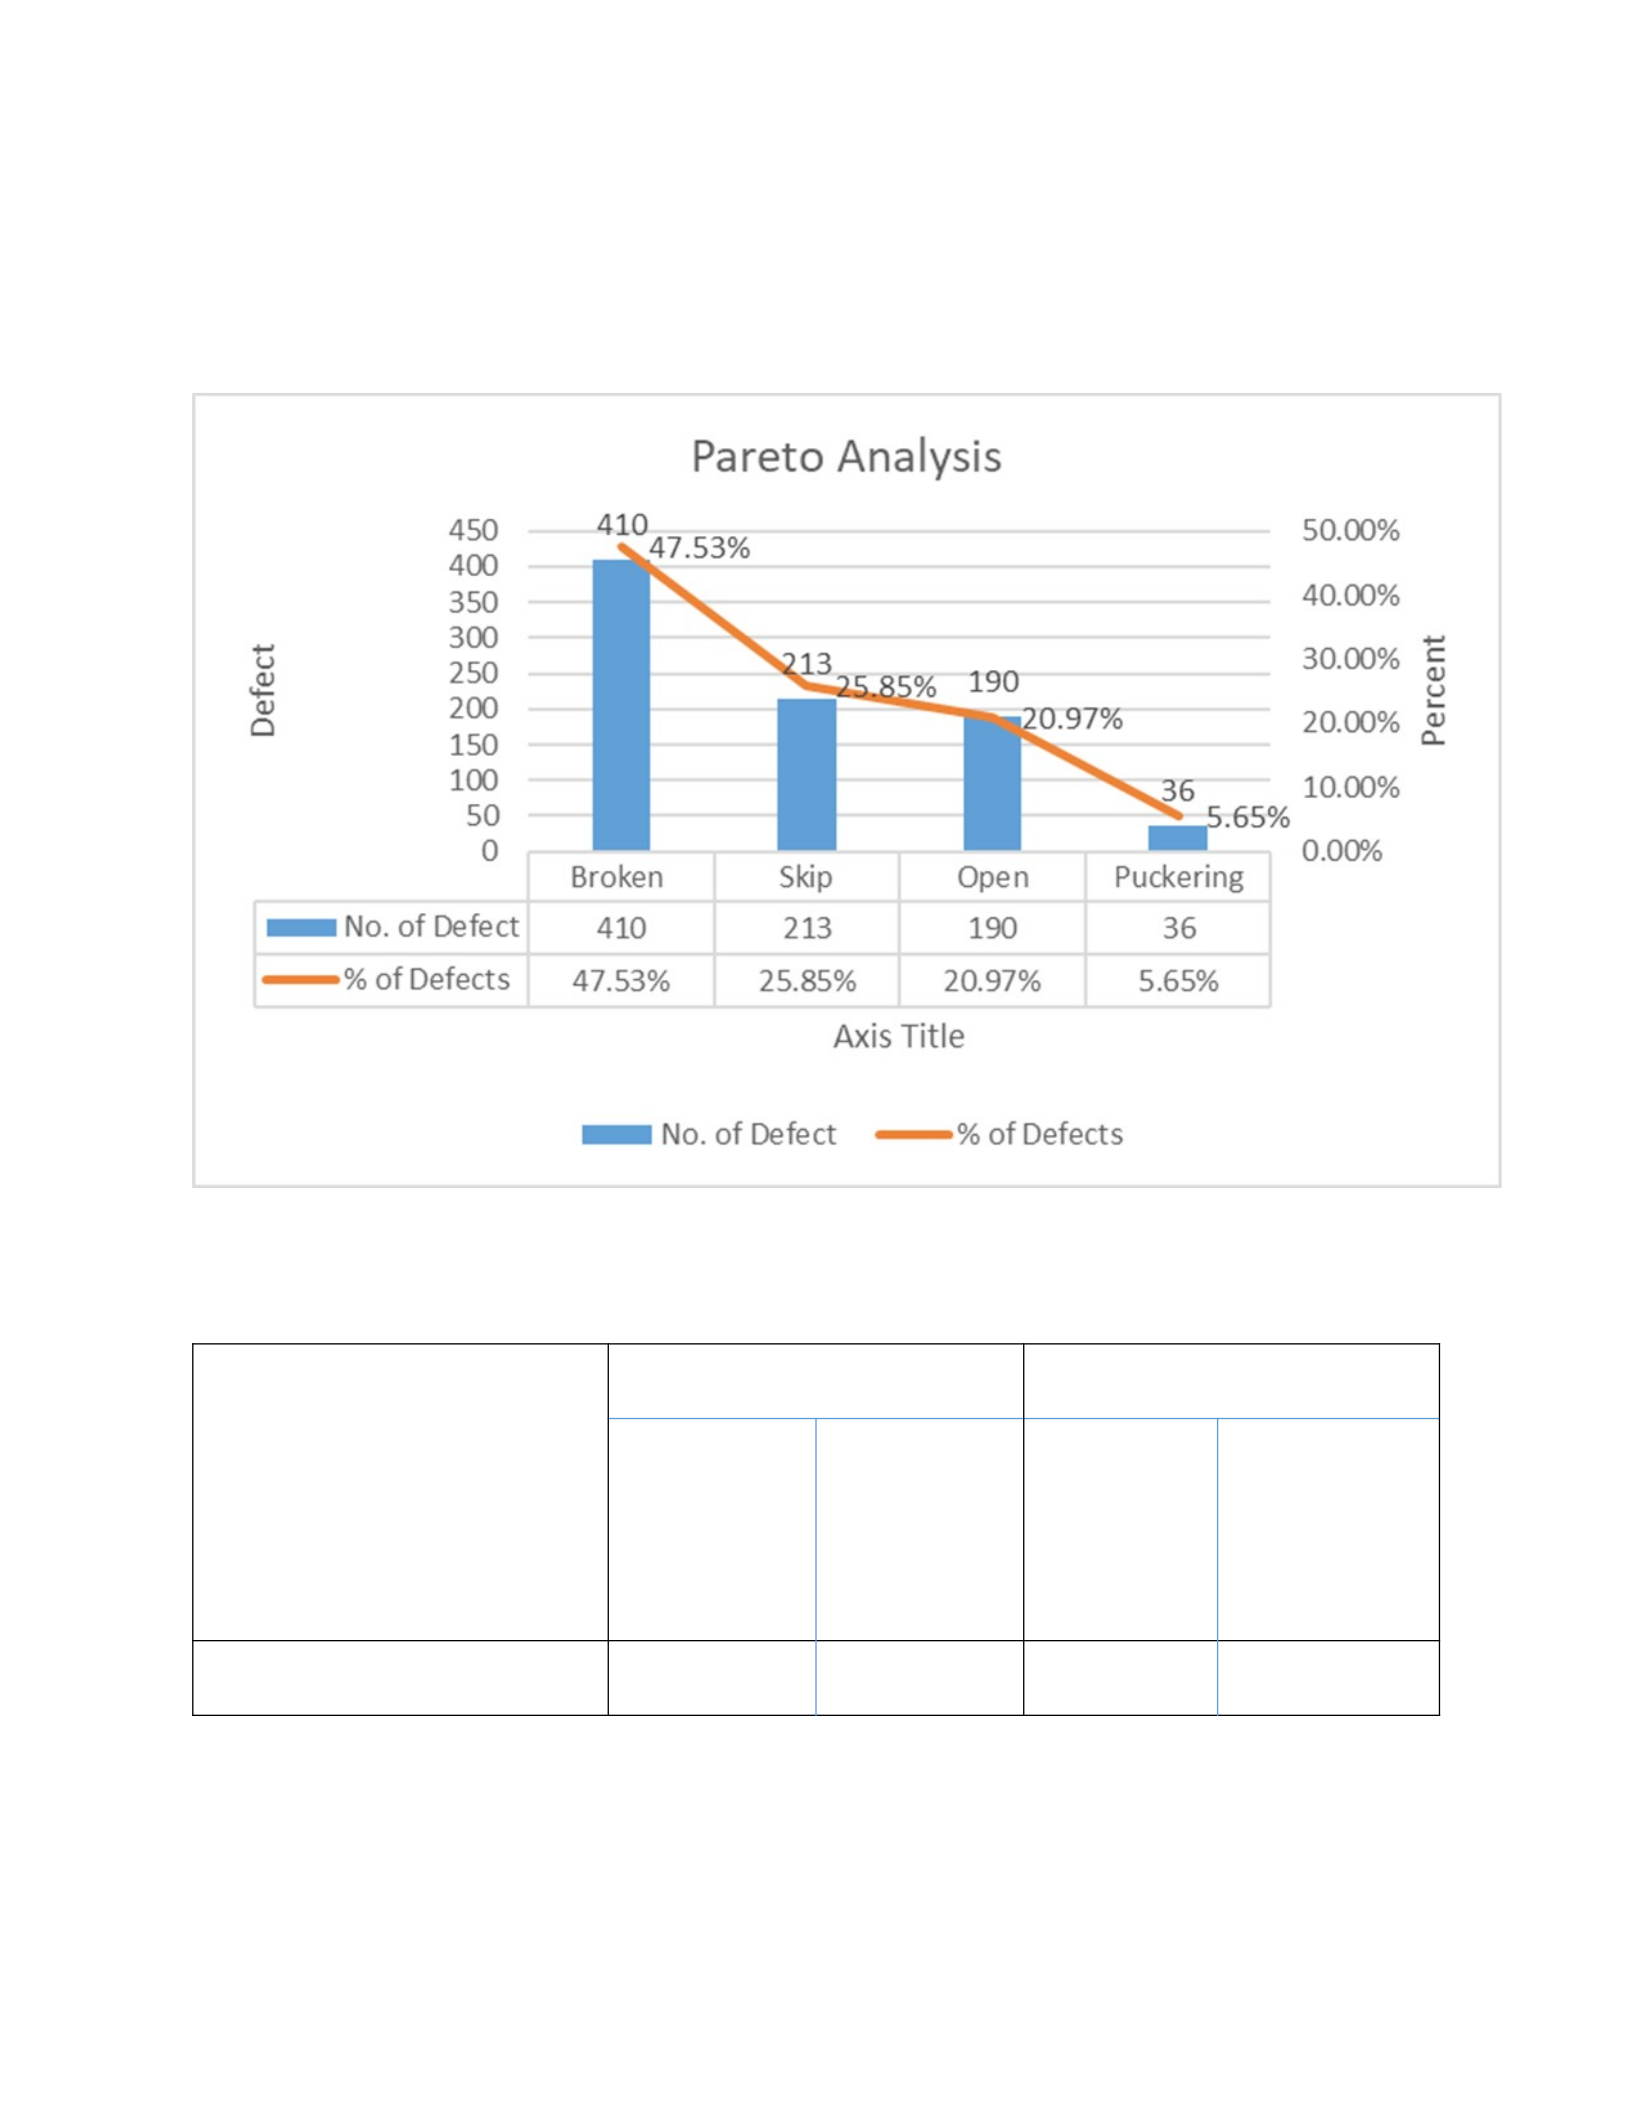
Pareto analysis is essential to identify the most occurring defect and prioritize the critical
problem which needs to get tackled immediately (Tuna, 2018). Out of the four defects, the
improvement team and Color Line Co. decided to focus on reducing the broken stitch first. The
broken stitch has a sigma level of 1.6, and this calculation has allowed the team to have more
details of the current state of the clothing manufacturing process. The Sigma level is illustrated in
table 4.
9
Figure 2: Pareto for Project Line Defect before Improvement (Rahman et al., 2017)
Table 4: Manufacturing process current and expected states (Rahman et al., 2017)
Major Defect types Number of Major defects Sigma Level
Current
Performance
of process
Expected
Performance
of process
Current
Performance
of process
Expected
Performance
of process
Broken 410 170 1.6 3.4

10
This phase consists of analyzing the garment manufacturing system of Color Line Co. to
find ways to reduce the gap between the desired goal and the current Performance. Bridging the
gap will require the investigation of the root cause of the problem through a cause-effect
diagram. According to Tahiduzzaman et al. (2018), a fishbone diagram assists the firm to
understand the garment production process in sub-operations and the main changes to deal with
the effect. The improvement team at Color Line Co. carried out an analysis to identify the root
cause of the broken stitches. Based on the team experience and knowledge of the production
process, the following were the probable causes of the defect.
Figure 3 below is a fishbone diagram that illustrates the relationship between the causes
and effects on the product. According to Tahiduzzaman et al. (2018), when the diagram is
complete, firms can see the root causes and areas that require improvement to ensure that the
production process is effective and working efficiently. Five main factors are considered in this
diagram, known as the 5M; they include manpower, material, machinery, measurement and
method (Ershadi et al., 2018). The additional factor is the environment which also affects the
production process. The root causes include improper threading, not following the cut mark, and
others caused the broken stitch defect.
Figure 3: Cause and Effect Diagram (Rahman et al., 2017)
11
Uneven Cutting part Poor Fabric Quality Unskilled
Mismatch of size Improper Thread Not following cut mark
Production Rush Improper Technique Improper feed dog
Follow up Thread Tension
Bobbin Tension
4. Improve Phase
Once the root cause is determined, the DMAIC's improvement phase focuses on
recognizing the solutions that will best suit to reduce the broken stitch defects. The design of
experiments is analyzed through the ANOVA tool, which highlights the effects of multiple
factors. This design also confirms that the parameters indeed harm the garment manufacturing
process leading to defective clothes. ANOVA model compares the difference in statistics like
illustrated below. The analysis results in table 5 show the effect in the complete process that
leads to the defect in garments.
Measurement Material Man
Broken
Stitch
Mother Nature Methods Machines
12
Table 5: ANOVA with 5% level of significance (Rahman et al., 2017)
Source Degree of
Freedom
Adj S.S. Adj MSS F-Value P-Value
Defect 3 90.53 21.38 7.59 0.000
Parts 4 5.24 02.12 0.37 0,694
Process 21 75.62 03.83 1.22 0.214
Error 398 1228.04 3.075
Lack of fit 76 182.82 2.477 0.79 0.915
Pure error 320 1044.21 3.215
Total 429 1489.03
The P-value is statistically significant as it is less than 0.05. Color Line's improvement
team will need to make changes to the effects, such as not following the cut mark correctly to
ensure that the final products match the consumer's quality. Additionally, production planning in
the firm is a significant factor that needs to get addressed. Planning refers to seeing ahead of all
the steps taken to complete the manufacturing process and ensure it done at the right time and
place. More so, every operation will eventually get performed at maximum efficiency.
5. Control Phase
This phase is the game-changer for the other four sections as it determines whether or not
the improvements needed will get abruptly adapted. Finding the problem and coming up with the
most appropriate solutions is not a huge bump as the real challenge in the implementation phase.
It takes time before the implementation starts showing changes, and regular evaluation is
required for the improvement team to ensure that they are still on track. Some of the tools that

13
can get used include what if analysis as well as a checklist. Maintaining the improvement is the
difficult part, and this phase ensures that the implementation is successful in the long run (Zaman
& Zerin, 2017). The new methods are becoming the standard operating procedures that require
all employees within the garment factory to be part of the project for its success. The control
phase consists of the norm ways and transfers responsibilities to the appropriate individuals
within the production process.
After the implementation, the defect rate is expected to reduce until the desired result is
achieved. Additionally, the sigma level was at 1.6, which is also expected to increase with the
decrease in defect rate. The primary goal of this project is to reduce the defect rate by employing
LSS and DMAIC methodology to come up with the best solution for the strategy (Zaman &
Zerin, 2017). The reduction of defects is targeted at increasing consumer satisfaction and
offering them garments that match their value for money. This goal was meant to reduce the
costs of production and losses the Color Line Co. have been undergoing.
Conclusion
The firm's competitive advantage is expected to be much better after the changes in the
defect rate, which will work towards guaranteeing the long-term operation of the business.
Another biblical principle that corresponds with this article is that humans were given the ability
to make moral choices. Genesis 2:15-17 states, "Then the Lord God took the man and put him in
the garden of Eden to tend and keep it. He then commanded the man, saying that every tree in
the garden man can freely eat but not form the tree of the knowledge of good and evil. The day
that you eat, you shall surely die" (King James Bible, 1769/2017). Therefore, human beings were

14
given the ability to choose that which is right or wrong and in this case, correcting the errors
from the garments is the right choice.
15
References
Ershadi, M. J., Aiasi, R., & Kazemi, S. (2018). Root cause analysis in quality problem solving of
research information systems: a case study. International Journal of Productivity and
Quality Management, 24(2), 284-299. https://doi.org/10.1504/IJPQM.2018.091797
George, M. L., Rowlands, D., Price, M., & Maxey, J., (2005). The Lean Six Sigma Pocket
Toolbook. New York, NY: McGraw-Hill. ISBN: 9780071441193.
Hall, J. & Scott, T. (2016). Lean Six Sigma: A Beginners Guide to Understanding and Practicing
Lean Six Sigma. Columbia, SC: CreateSpace Receiving. ISBN: 9781541059559.
King James Bible. (2017). King James Bible Online.
https://www.kingjamesbibleonline.org/Psalms-25-21/ (Original work published 1769)
Mohamad, N., Ahmad, S., Samat, H. A., Seng, C. K., & Lazi, F. M. (2019, June). The
Application of DMAIC to Improve Production: Case Study for Single-Sided Flexible
Printed Circuit Board. In IOP Conference Series: Materials Science and Engineering
(Vol. 530, No. 1, p. 012041). IOP Publishing.
https://iopscience.iop.org/article/10.1088/1757-899X/530/1/012041/pdf
Rahman, A., Shaju, S. U. C., Sarkar, S. K., Hashem, M. Z., Hasan, S. K., Mandal, R., & Islam,
U. (2017). A case study of six sigma define-measure-analyze-improve-control (DMAIC)
methodology in garment sector. Independent Journal of Management & Production, 8(4),
1309-1323. https://www.redalyc.org/pdf/4495/449553639009.pdf
16
Srinivasan, K., Muthu, S., Devadasan, S. R., & Sugumaran, C. (2016). Six Sigma through
DMAIC phases: a literature review. International Journal of Productivity and Quality
Management, 17(2), 236-257.
Tahiduzzaman, M., Rahman, M., Dey, S. K., & Kapuria, T. K. (2018). Minimization of sewing
defects of the apparel industry in Bangladesh with 5S & PDCA. American Journal of
Industrial Engineering, 5(1), 17-24. DOI:10.12691/ajie-5-1-3
Tuna, S. (2018). Keeping track of garment production process and process improvement using
quality control techniques. Periodicals of Engineering and Natural Sciences, 6(1), 11-26.
http://dx.doi.org/10.21533/pen.v6i1.162
Yin, R. K. (2018). Case study research and applications: Design and methods, (6TH edition).
SAGE.
Zaman, D. M., & Zerin, N. H. (2017). Applying DMAIC methodology to reduce defects of
sewing section in RMG: a case study. American Journal of Industrial and Business
Management, 7(12),1320.http://www.scirp.org/journal/PaperInformation.aspx?
PaperID=81178&#abstract

