


Energy essential to life and survival
Energy is essential to life and survival. Energy may well be the item for which
historians remember the last century. We are at the beginning of a new era of change, an era
of possibly greater fundamental significance than the industrial revolution. For several
centuries mankind has grown lazy, lulled into complacency by the ease with which multitudes
can be fed, housed, and transported using the abundant supplies of low cost energy which
were readily available. Then around 1970-80, the bubble, which had taken so long to swell
finally, burst. Long unheeded warnings took on a prophetic aspect as fuel shortages and rising
costs nearly paralyzed the industrial economies and literally shocked the world into an
inflationary period that is not yet ended [38].
Of course in reality the problem is much more complex, involving not only oil prices
but also the uneven geographical distribution of energy resources, the exponential growth of
populations and fuel consumption, political and national security considerations and long
term environmental effects. When energy problems caused by rapidly increasing demand in
the face of dwindling fuel supply first became apparent, the immediate response was to seek
new supplies and alternative fuels [38].
Later, consideration was given to the user as a means of conserving fuels and capital
by improving end-use efficiency, supply problems were automatically eased. Approaching
energy problems from the user’s end, rather than the supply end, introduces new challenges.
First, the number of users is much greater than the number of suppliers, thus complicating the
problem. Second, communication with users is difficult due to their number and diversity.
Third, due to its diversity, end use is not readily approached by legislative or regulatory
controls. Fourth, the technological sophistication of end users varies widely, as do their
capital resources, limiting the technical improvements that are feasible. Finally, the nearly
infinite variety of uses invokes a need for a great many different technologies, materials and
equipment.
On the positive side, changes made by end-users can have an immediate (days) or
short term (months) impact on energy use, compared to five to ten years needed to add energy
supply capacity. The previous availability of energy with its low cost resulted in situations in
which there was little incentive for more efficient energy use. Both of these conditions are

changing. So users now perceive economic signals (rising prices), which provide positive
encouragement to reduce or eliminate all unnecessary uses of energy. Finally even though the
diversity of enduse technology is considerable, it appears that there are certain basic
approaches or “general principles” which apply in a wide variety of applications [38].
1.2 Energy Management
Energy management is the application of Industrial engineering principles to the
control of energy costs at a facility. The primary goal here is to save money on energy
expenses, resulting in increased profits through improved energy productivity. Often there is
also an interest in conserving energy and reducing harmful environmental emissions
associated with commercial and industrial operations. With this definition, energy
management is just good Industrial engineering, where one of the cost factors to be controlled
is the cost of energy to operate a facility and to produce a product or a service in an
environmentally responsible manner [39].
Business and industry have also realized that their large uses of energy contribute to
global environmental problems such as climate change, acid rain, and ozone depletion.
Commercial and industrial energy use accounts for 45 % of the carbon dioxide released from
the burning of fossil fuels, and 70 % of the sulfur dioxide emissions from stationary
resources. Energy efficiency and energy conservation efforts on the part of business and
industry can have substantial positive impacts on these national and global problems, as well
as the bottom line of the company’s balance sheet [39].
Energy conservation is the need of the hour. It is a continuous process that requires
consistent efforts for identifying potential areas for conservation, formulation of proposals
and implementing the same. Energy is the most critical resource today. Gap between demand
and supply of energy will be continuously widening in the years to come. Scarcity of fuels,
insufficiency in energy systems and ever rising cost of energy, lead to energy crisis and
ultimately to energy conservation. Energy conservation is based on a worldwide BAT (best
available technology) principle. Certain aspects considered while going through the energy
conservation program include:

Up gradation of technology
Systems development
Fine-tuning methods
1.3 Industrial energy conservation
Energy is an integral component of modern industrialized society. It is an essential
ingredient in nearly all goods and services, but its use exacts heavy financial, environmental
and security costs. A key method of reducing energy’s costs while retaining its benefits is to
utilize it more efficiently than before [38]. Important questions that arise in the context of
industrial energy use are as follows:
1. How does industry use energy? What is the outlook for future energy use?
2. What technologies are available to improve energy efficiency? How much energy can
be saved?
3. How do corporations view energy? What are the incentives for using more efficient
technologies?
Industry is a large consumer of energy. U.S. manufacturing plants, mines, farms and
constructions firms currently consume about 25 quads (quadrillion British thermal units or
Btu) of energy each year [38], about 30% of the nations total consumption of energy and
manufacturing industries account for the lion’s share. Industry thus has a major role in
making the U.S. more energy efficient. Industrial energy use and the opportunities for
improving its energy efficiency depend on many technical, economic, institutional and
political factors. The largest energy users are industries, such as petroleum refining,
chemicals, primary metals, pulp and paper, food and ceramics and glass, which chemically or
physically convert matter. These industries account for 74% of total industrial energy use
[38]. The fabricating and assembly industries are the largest electricity users, because of
relative prominence of motor driven devices, lighting and ventilation. There are many energy
efficient technologies and practices, both currently available and under development, that
could save energy if adopted by industry.
Energy efficiency can be improved through the cost effective use of the following:

General housekeeping and maintenance programs
Energy management and accounting programs
Improved method and procedures for existing production methods
New and better production methods
Product changes
Most of the equipment and process enhancements are specific to particular industries,
but several (e.g., heat recovery technologies, high efficiency motors and variable speed
drives, boiler efficiency, sensors and controls and cogeneration) have applications in many
industries. These generic technologies are particularly attractive targets for government
policies.
The costs and benefits of energy efficient improvements vary widely. Minor operational
changes, such as house keeping and maintenance, are typically the cheapest, easiest to
implement, least risky and usually, though not always, yield the smallest energy and cost
savings. Production equipment changes and energy conservation add-on technologies involve
larger investments, typically $100,000 to tens of millions of dollars, and may or may not be
justified by reduced energy costs alone. Major process changes often require building a new
facility, at costs typically exceeding $ 100 million, and usually are justified only by strategic,
market development concerns. Energy savings are seldom sufficient to justify the investments
of this magnitude.
Potentially, the greatest increase in efficiency will come not from direct efforts to reduce
energy consumption but by pursuing other economic goals like improved product quality,
lower capital and operating costs, or specialized product markets. Many projects yield energy
efficiency gains as a secondary consequence. For example, steel makers have installed
continuous casters more for the improved product yield than the energy savings. Metal
stamping plants have implemented new techniques for cushioning presses not for the 10%
energy savings, but for the consistent products and lower maintenance cost [38]. Sometimes,
however, pursuing improved quality or specialized markets can diminish energy efficiency.
Such is the case in petroleum refining where several factors have combined to increase the
energy requirements per unit of product in recent years as shown herein:

The reduction in capacity utilization
The decline in crude oil quality
The increased demand for lighter products relative to heavier products (residual oil)
The requirements for enhanced products such as reformulated gasoline
At any given time, the mix of technologies used by industry ranges from outdated to
state-of-the-art. Energy efficiency improves as the older facilities are replaced with the state-
ofthe-art ones. In the petroleum refining, chemical, pulp and paper, steel, aluminum, cement
and glass industries, most state-of-the-art technologies use 12 to 38 % less energy than the
mix of processes currently used. This comparison does not imply that these industries would
find it economical to bring all their existing plants to state-of-the-art tomorrow. Advanced
technologies, no yet commercialized, could possibly reduce energy use in the various
processes by an additional 9 to 35%.
There are various potential areas that can be identified as prospective candidates for
considering energy conservation measures. Some of them are the lighting, motors,
destratification, insulation of process equipment, boilers and compressors. If we consider
lighting in facilities, modifications to the operation of the lighting system would provide
great opportunities to reduce energy consumption. Simply turning off unnecessary lights, day
and night, and making greater use of available daylight for illumination saves energy for both
lighting and air-conditioning with no added costs. If we consider the boiler, which is used to
generate process steam in facilities usually, the efficiency of the boiler unit drops when the
combustion process is improper or when combustion process increases the stack temperature.
Any percentage increase in seasonal boiler efficiency directly reduces fuel consumption in
the same proportion. If we consider the three phase-induction electrical motors in the
facilities, usually the industrial personnel lack prior knowledge about the high efficient
motors available in the market and the cost savings that can result from a replacement
schedule. Another example would be the employment of de-stratification fans in the
workplaces where heating units have been set up in place but comfort level has not been
attained at work level. Several cases involving various ideas about utilizing the energy
consumers more efficiently can be presented but for the purpose of the work in consideration,
the above in itself would be sufficient to create awareness about this universal problem [38].

1.4 Corporate Viewpoint
Corporation’s internal cultures and external relationships are very important factors
on industrial energy use and efficiency. Here, it is attempted to focus on the question of “why
and when the industrial user would care about energy?” The investment and implementation
steps encompass major hurdles. Technical and economic feasibility are the most commonly
studied factors influencing energy efficiency investments while the company’s general
willingness to invest in process improvements, their energy awareness, their access to
information also have important impacts.
Perhaps the most important factor affecting industrial energy efficiency is the
willingness of firms to invest in new technologies, whether energy conscious or not. Capital
investment in modern equipment usually enhances energy efficiency, even when efficiency is
not the primary purpose of the investment. The propensity to invest depends on the business
climate, corporate culture, manager’s personality and regulations. These determine the
incentives for the corporations in general and managers in particular to improve their
production processes [38].
If there is willingness to invest, the next hurdle for the managers is to know how the
energy is used in their plants and to be aware of technologies available to improve the
situation. Industrial companies consider energy primarily in terms of cost. They have direct
financial incentives for reducing their energy costs by improving their energy efficiency. The
importance that companies attach to reducing costs in general, and energy costs in particular,
varies greatly however. In industries such as steel, aluminum, cement and industrial gases,
where energy is a major portion of the total costs, concerns about energy efficiency are high.
The existence of energy efficiency “Champions”, enlightened management or efficiency
promotion programs can also give energy a high profile in corporate decision making. For
example, Dow Chemical’s Louisiana Division [38] has a very successful contest for
identifying and funding energy efficiency projects. Sudden energy price shocks or availability
problems can also prompt companies to improve their energy efficiency.
Cutting energy costs via technical means is not a high profile concern in most
industrial companies. Energy costs do not command the attention of the senior management
and do not garner the resources needed to implement the improvements. Even in the
operations divisions of the firms, where costs issues are most focused, energy is but one of

the many concerns. An operations manager’s top priorities are keeping the production line up
and running smoothly, making products that meet the consumer’s specifications and
expectations, and meeting regulatory guidelines. Energy costs tend to be secondary concerns.
This could also be because the energy costs are low. The general lack of concern afforded
energy in many corporations is a major barrier to implementation of energy efficiency
improvements.
Low energy awareness is less of a setback to efficiency in situations where there are
new technologies with the production benefits in addition to energy saving characteristics.
Fortunately, many technologies fall in this category. They are implemented primarily to boost
product quality, further automate production or enhance some other characteristics. They
improve energy efficiency as a side benefit. For example, continuous casting is put into steel
mills primarily to improve material yields and product quality and to shorten processing
times. Secondarily, the improved design of the process uses less energy per ton of steel
produced.
Convenient information regarding new technologies and their energy characteristics is
vital to energy efficiency implementation. Managers, especially those in small firms, do not
have the time and the resources for gathering and analyzing large amounts of information to
support their decisions. This is particularly true when equipment fails and needs immediate
replacement. There is little time to research the available best replacement technologies, and
then test and tune them up once they arrive. Consequently, in these situations the managers
usually stick to the technologies that they know well – the ones that have used before.
Providing information is the role that the State and the Federal governments are involved in.
Utilities are also involved in dissemination information as well as conducting audits to inform
companies about energy saving opportunities.
Lastly, technological feasibility and economic feasibility are driving factors as well.
Technologies must not only work successfully, but also be reliable, serviceable and proven. In
addition they must be economical with respect to capital outlays, energy and other input
prices and costs of capital.
Energy and energy management have been in the limelight in various manufacturing
and service operations across the industry in US. The lumber and wood manufacturing
industry has not been a major part of this discussion. So, in this study, wood and lumber

manufacturing industry will be the considered for a thorough analysis of the energy use and
energy management activities. A general background of the wood industry and the wood
manufacturing process will be discussed in the following paragraphs followed by economic
profile and trends in that industry.
1.5 Importance of Wood Industry
Wood has played a leading role in the advancement of the human race. It has been
used by mankind to provide shelter, fuel, weapons, transportation, and in many other ways,
since the beginning of civilization. It is at once the best known and the least known among
the important basic structural materials. Wood is used in many different forms in its service to
man. Although large quantities are utilized as fuel wood, pulpwood, railroad ties, etc, lumber
is the important form in which wood is used. In the United States the volume of wood
converted into lumber exceeds the volume used for all other purposes [32]. In spite of the
tremendous advances that have been made in the development of new ways of using wood, it
is probable that lumber will continue for a long time to be the most important wood product
from a value standpoint. The business of converting trees into lumber will always occupy an
important place in the industrial economy [32].
1.5.1 Definition
Lumber has been defined as “ the product of the saw and planning mill, not further
manufactured than by sawing, re-sawing, and passing length wise through a standard
planning machine, crosscutting to length and working.” [32].
1.5.2 The manufacturing operations
The essential operations in the manufacture of lumber are (1) breakdown of the log
into boards or timbers; (2) cutting the boards or timbers lengthwise in a ripping or edging
operation, with the objective of removing wane, improving the grade, or dimensioning to
width; and (3) cutting the boards across the grain in a cross cutting or trimming operation, for
the purpose of removing defects, improving the grade, or dimensioning to length.

1.5.3 Process
Saw logs are trucked in to the plant by the logger contracted to haul them from the
harvest site. Logs are stored in the area outside the plant and initial inspection and sorting is
done. They are then fed to the Debarker where the bark is abraded off. With the help of a
material handling system they are sent to the Head saw where sideboards are cut off from the
cant. The cant is then cut into desired dimensions. The boards proceed on a conveyor to the
Edger where smooth parallel edges are rendered on to the boards. The Trimmer then cuts the
boards to square and precise lengths. The boards are then sent to grading and then final
sorting and storage. The lumber is then packaged by grade and length and shipped via trucks.
A detailed flow chart of a typical sawmill is shown in the Figure 1.1.
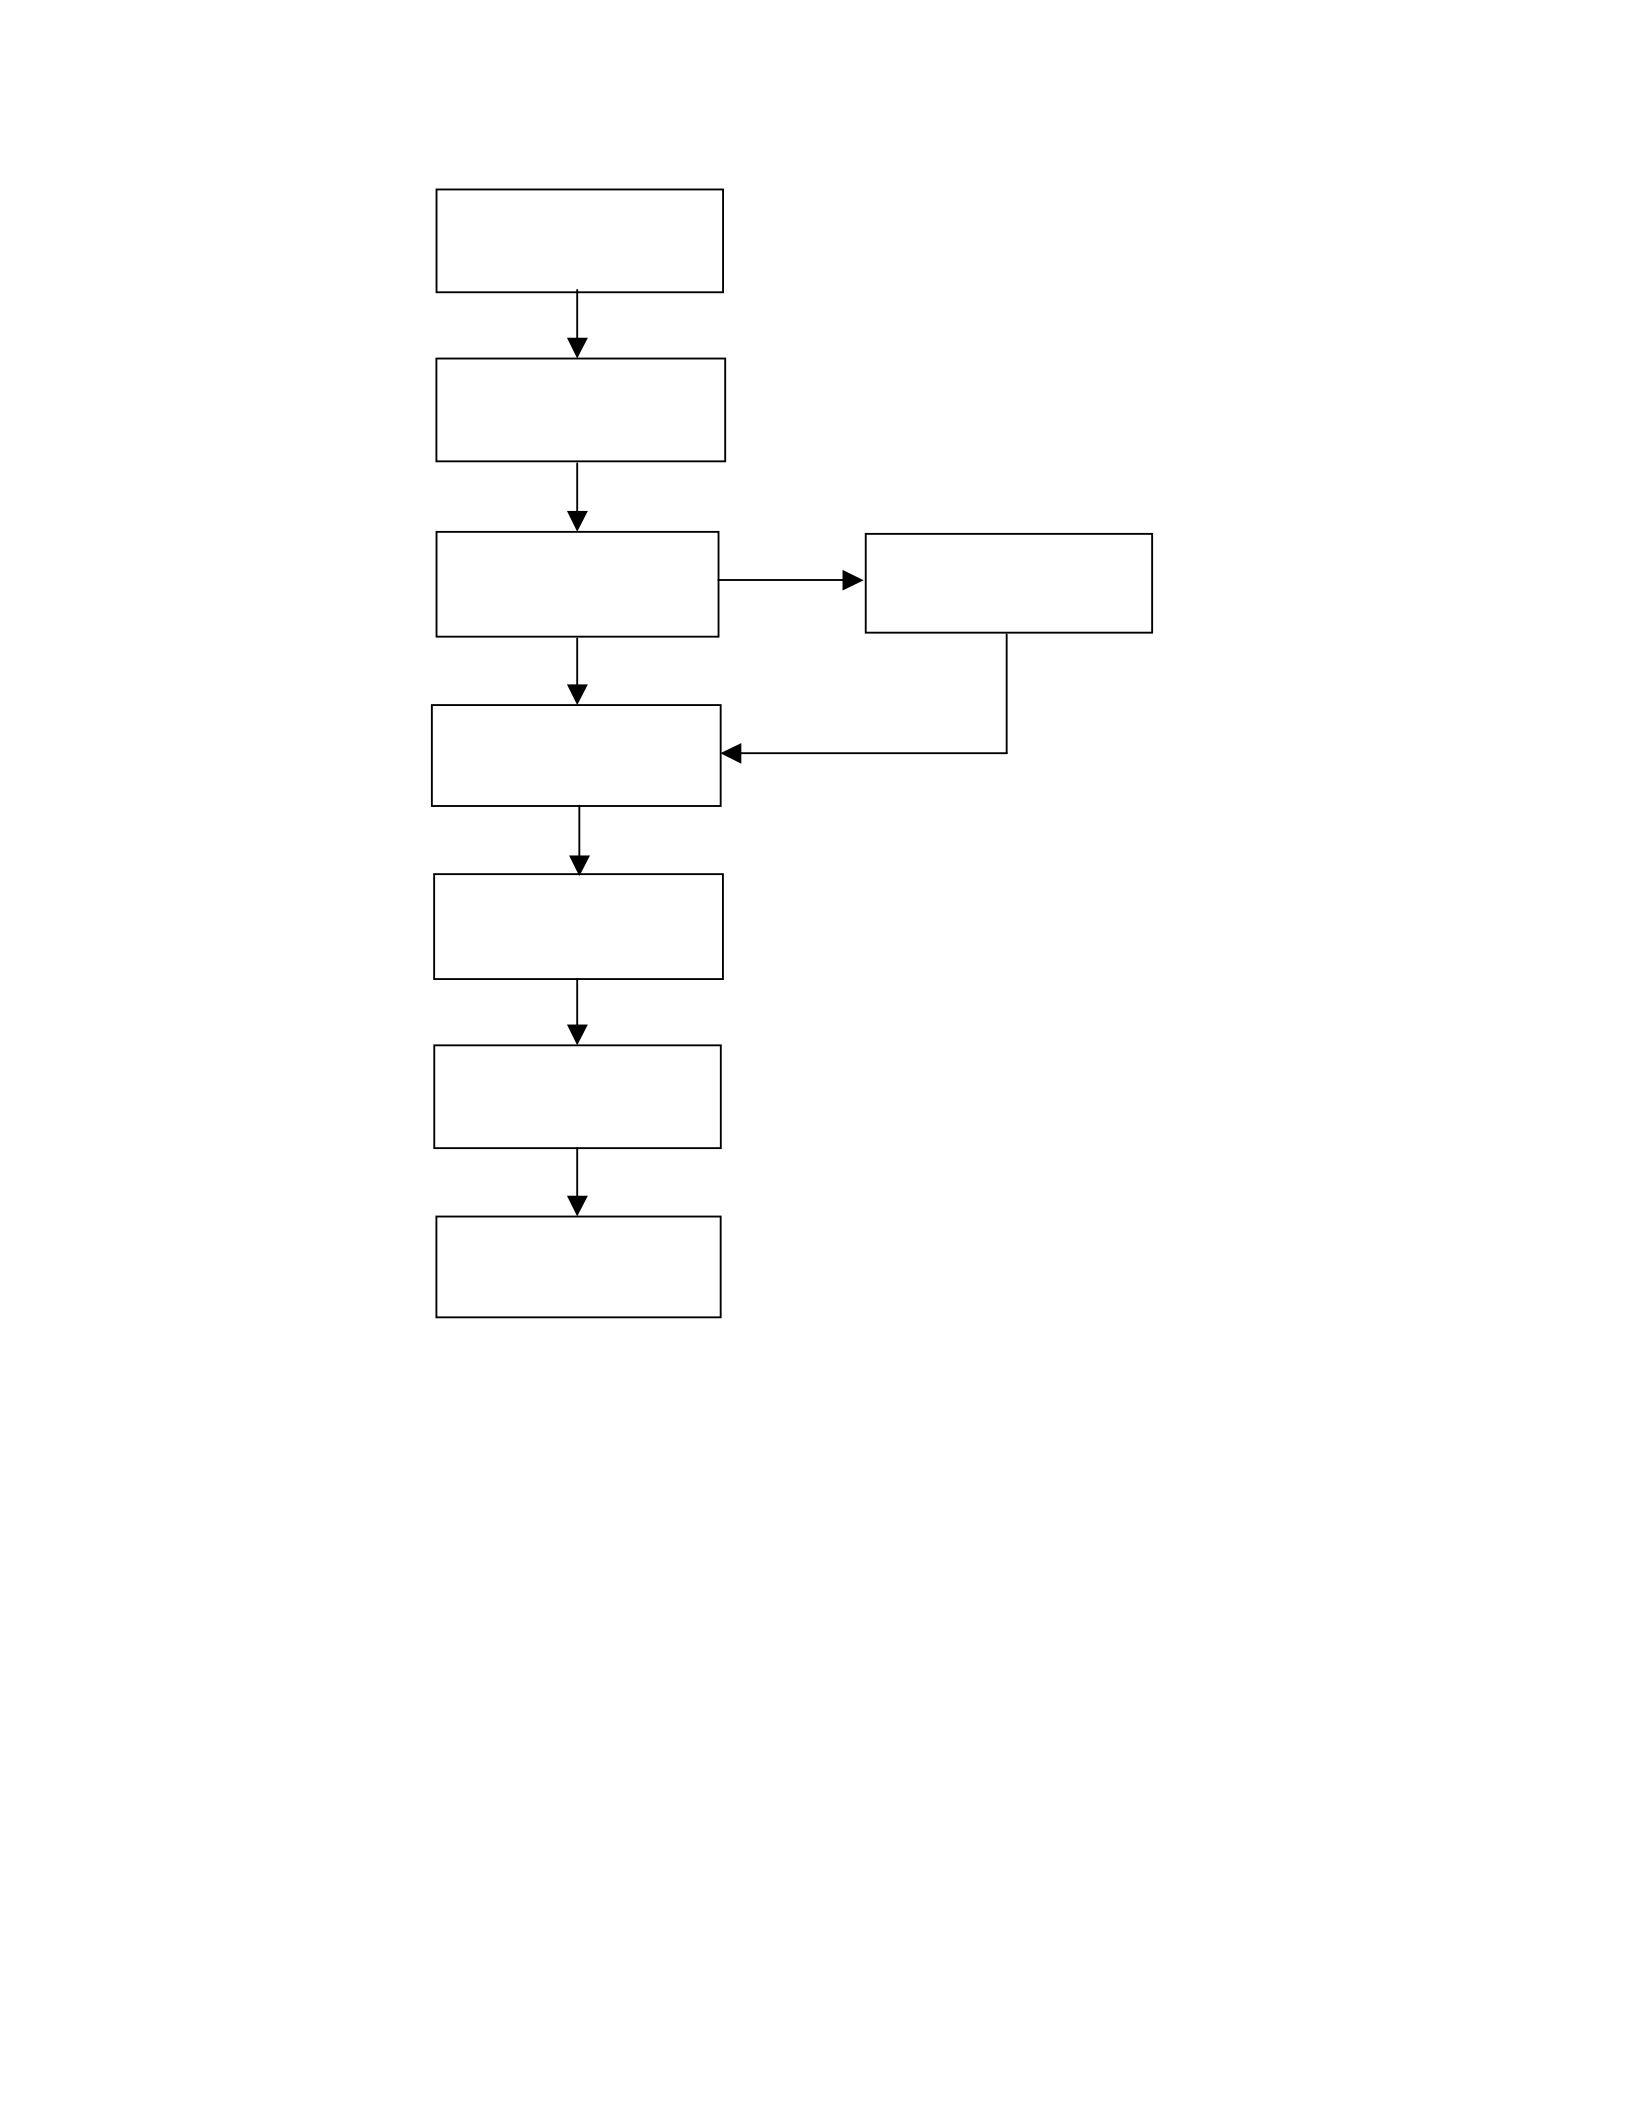
Figure 1.1: Flow Chart of a typical sawmill process
1.5.4 Introduction to the Lumber and wood products industry
The lumber and wood products industry includes establishments engaged in cutting
timber and pulpwood; sawmills, lath mills, shingle mills, cooperage stock mills (wooden
casks or tubs), planing mills, plywood mills; establishments engaged in manufacturing
finished articles made entirely or mainly of wood or related materials such as reconstituted
wood panel products manufacturers. The categorization corresponds to the Standard
Industrial Classification (SIC) code 24 established by the Department of Commerce’s Bureau
Debarker
Head saw
Resaw
Edger
Trimmer
Grader
Sorting
&
Dis patch
Lumber
Cant
Lum ber
Sorting and storing of
logs from Forest
Management Area
of the Census to track the flow of goods and services within the economy. In this profile, the
industry’s processes are divided into four general groups: logging timber; producing lumber;
panel products and wood preserving.
1.6 Economic Profile and Trends of the Lumber and Wood products Industry The
economic profile and trends in the lumber and wood manufacturing industry in the year 1994
& 1998 are obtained from the manufacturing Consumption of Energy Survey in the years
1994 and 1998, which is published by the US Department of Energy’s, Energy Information
Administration. The annual production in the SIC 24 category, the value of shipments for SIC
24 category and the labor productivity in the wood manufacturing industry are discussed in
detail in the following paragraphs.
1.6.1 Annual Production
Lumber and wood products include a wide range of products, including cut timber,
rough wood products, such as hewn posts, lumber and flooring, millwork, such as moldings
and cornices, cabinets, plywood, containers, and wood buildings. The annual production of
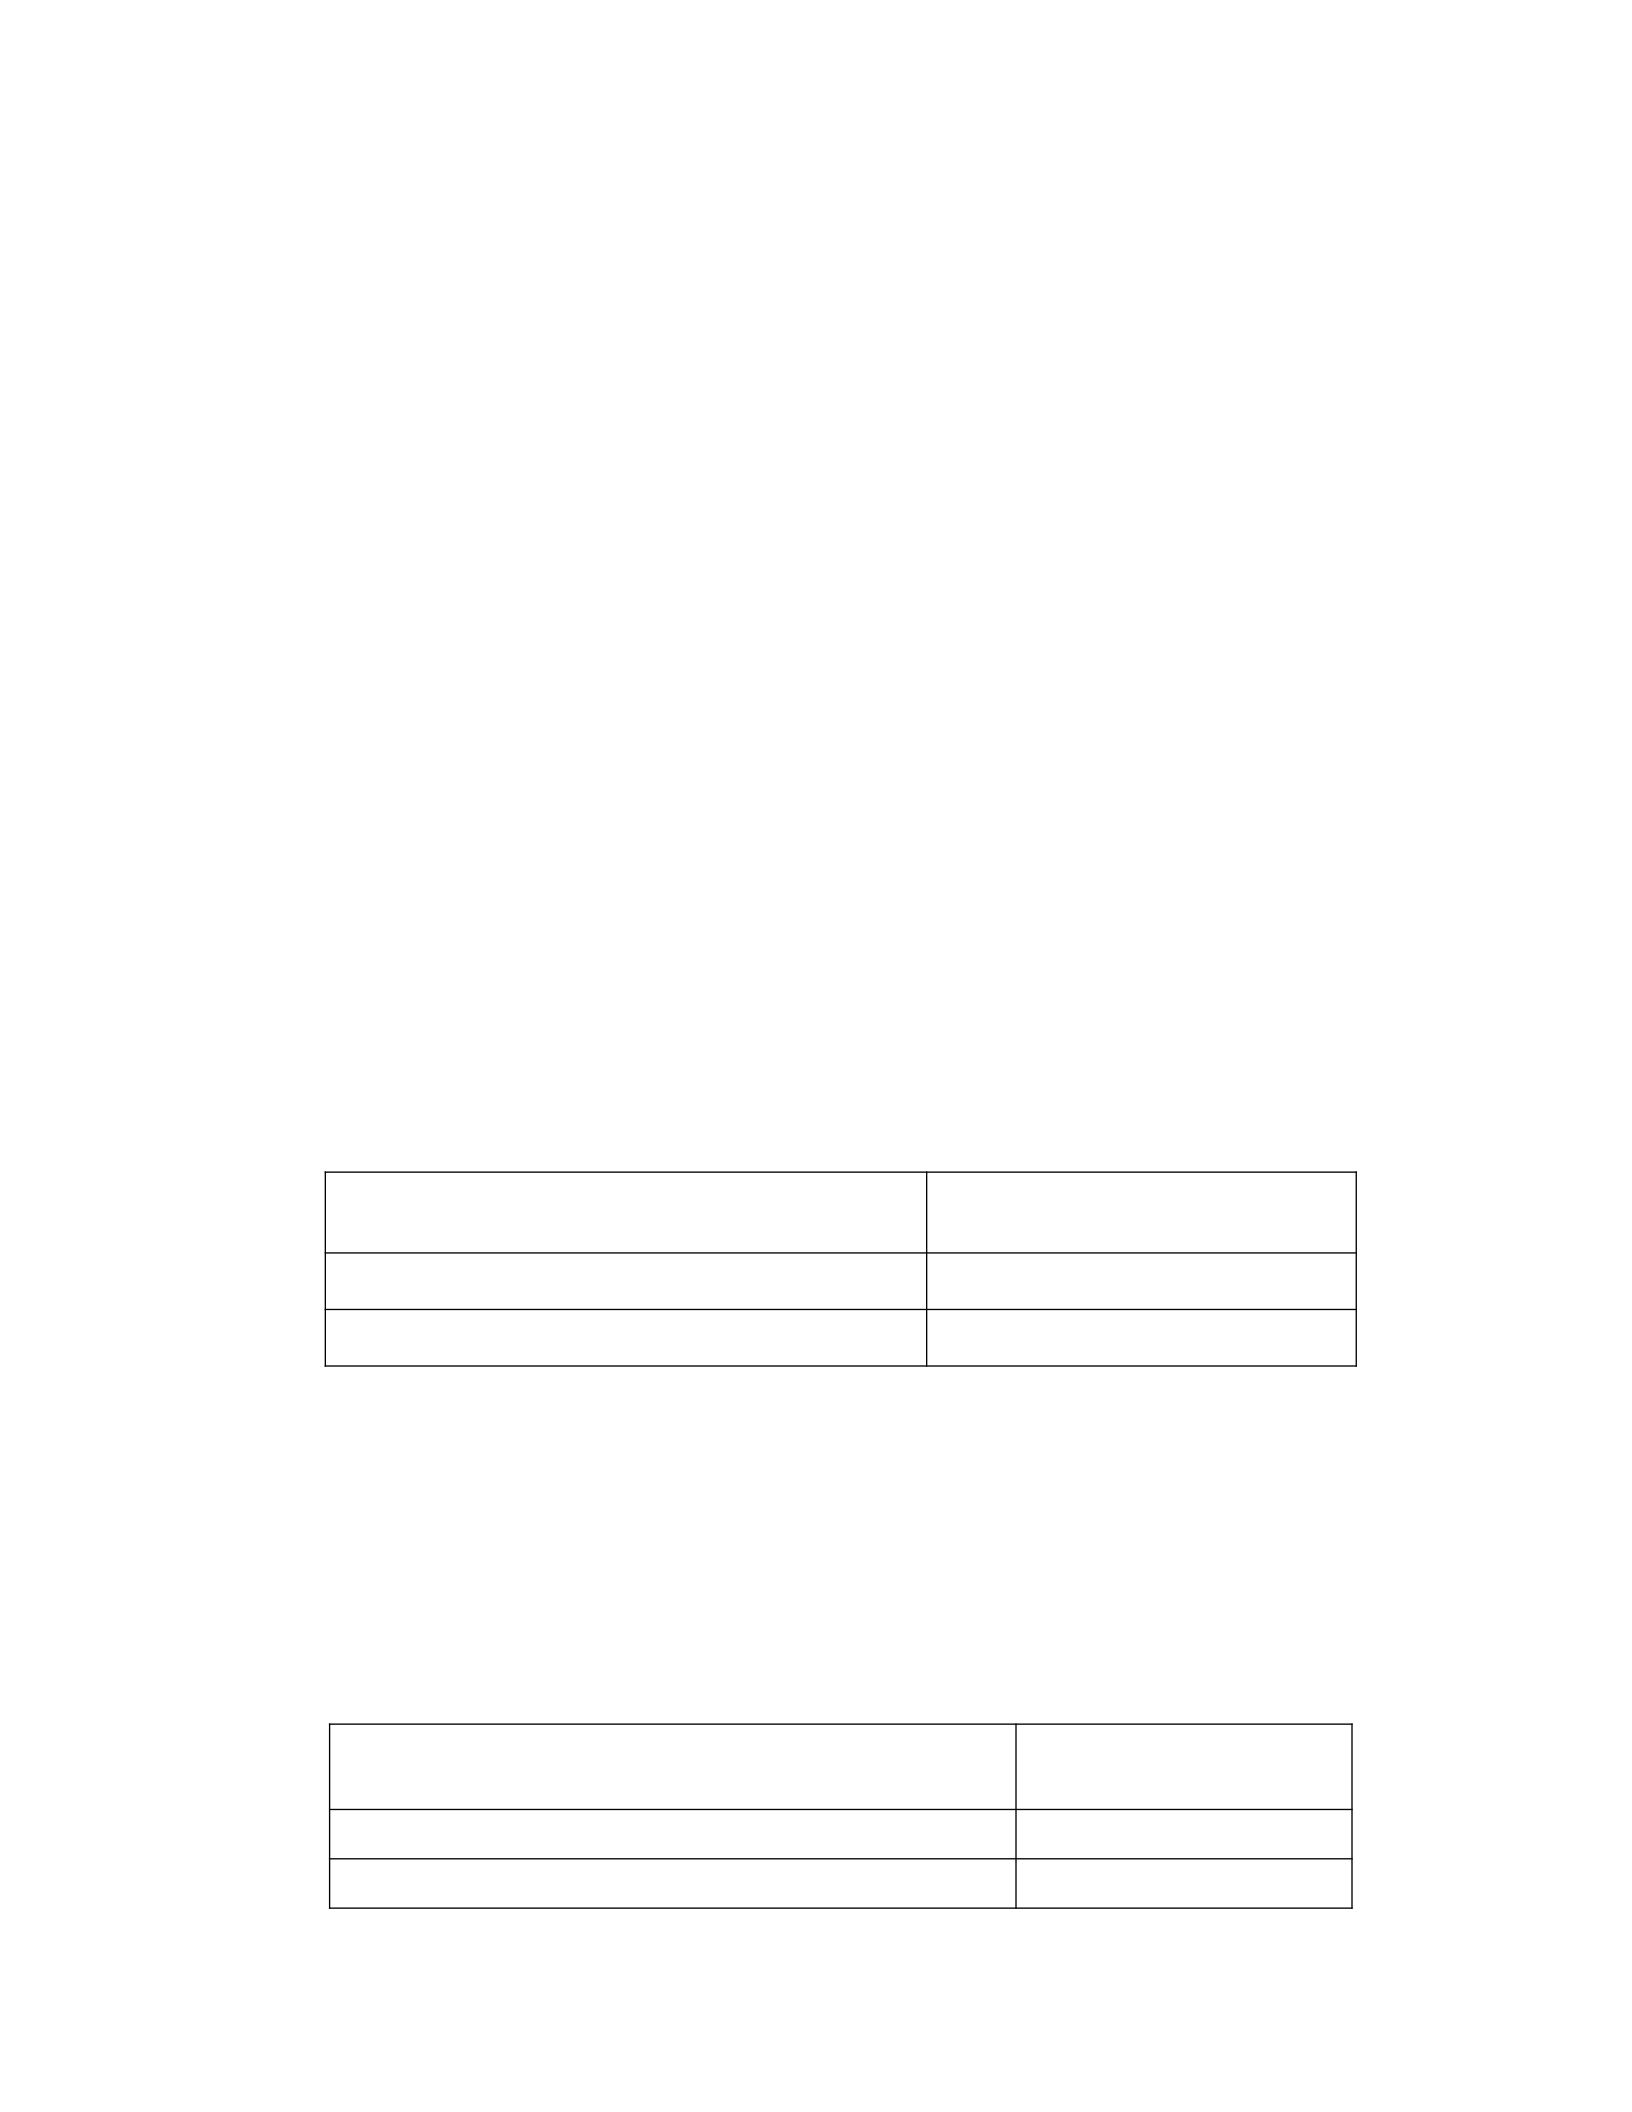
the lumber and wood products is shown in Table 1.1.
Type Annual Production
Quantity
Software Lumber 34.5 billion board feet
Hardwood Lumber 12.9 billion board feet
Table1.1: Annual Production – 1997 [35]
1.6.2 Value of Shipments
The strong U.S. economy of the late 1990’s has revived the pulp and paper industry and also
the lumber industry. Softwood and hardwood lumber production is again climbing, both up
2% from 1996. Table 1.2 shows the value of shipments in 1997.
SIC Type Value of shipments
(Billion $)
Logging (SIC 241) 13.6
Sawmills and Planning mills (SIC 242) 35.2
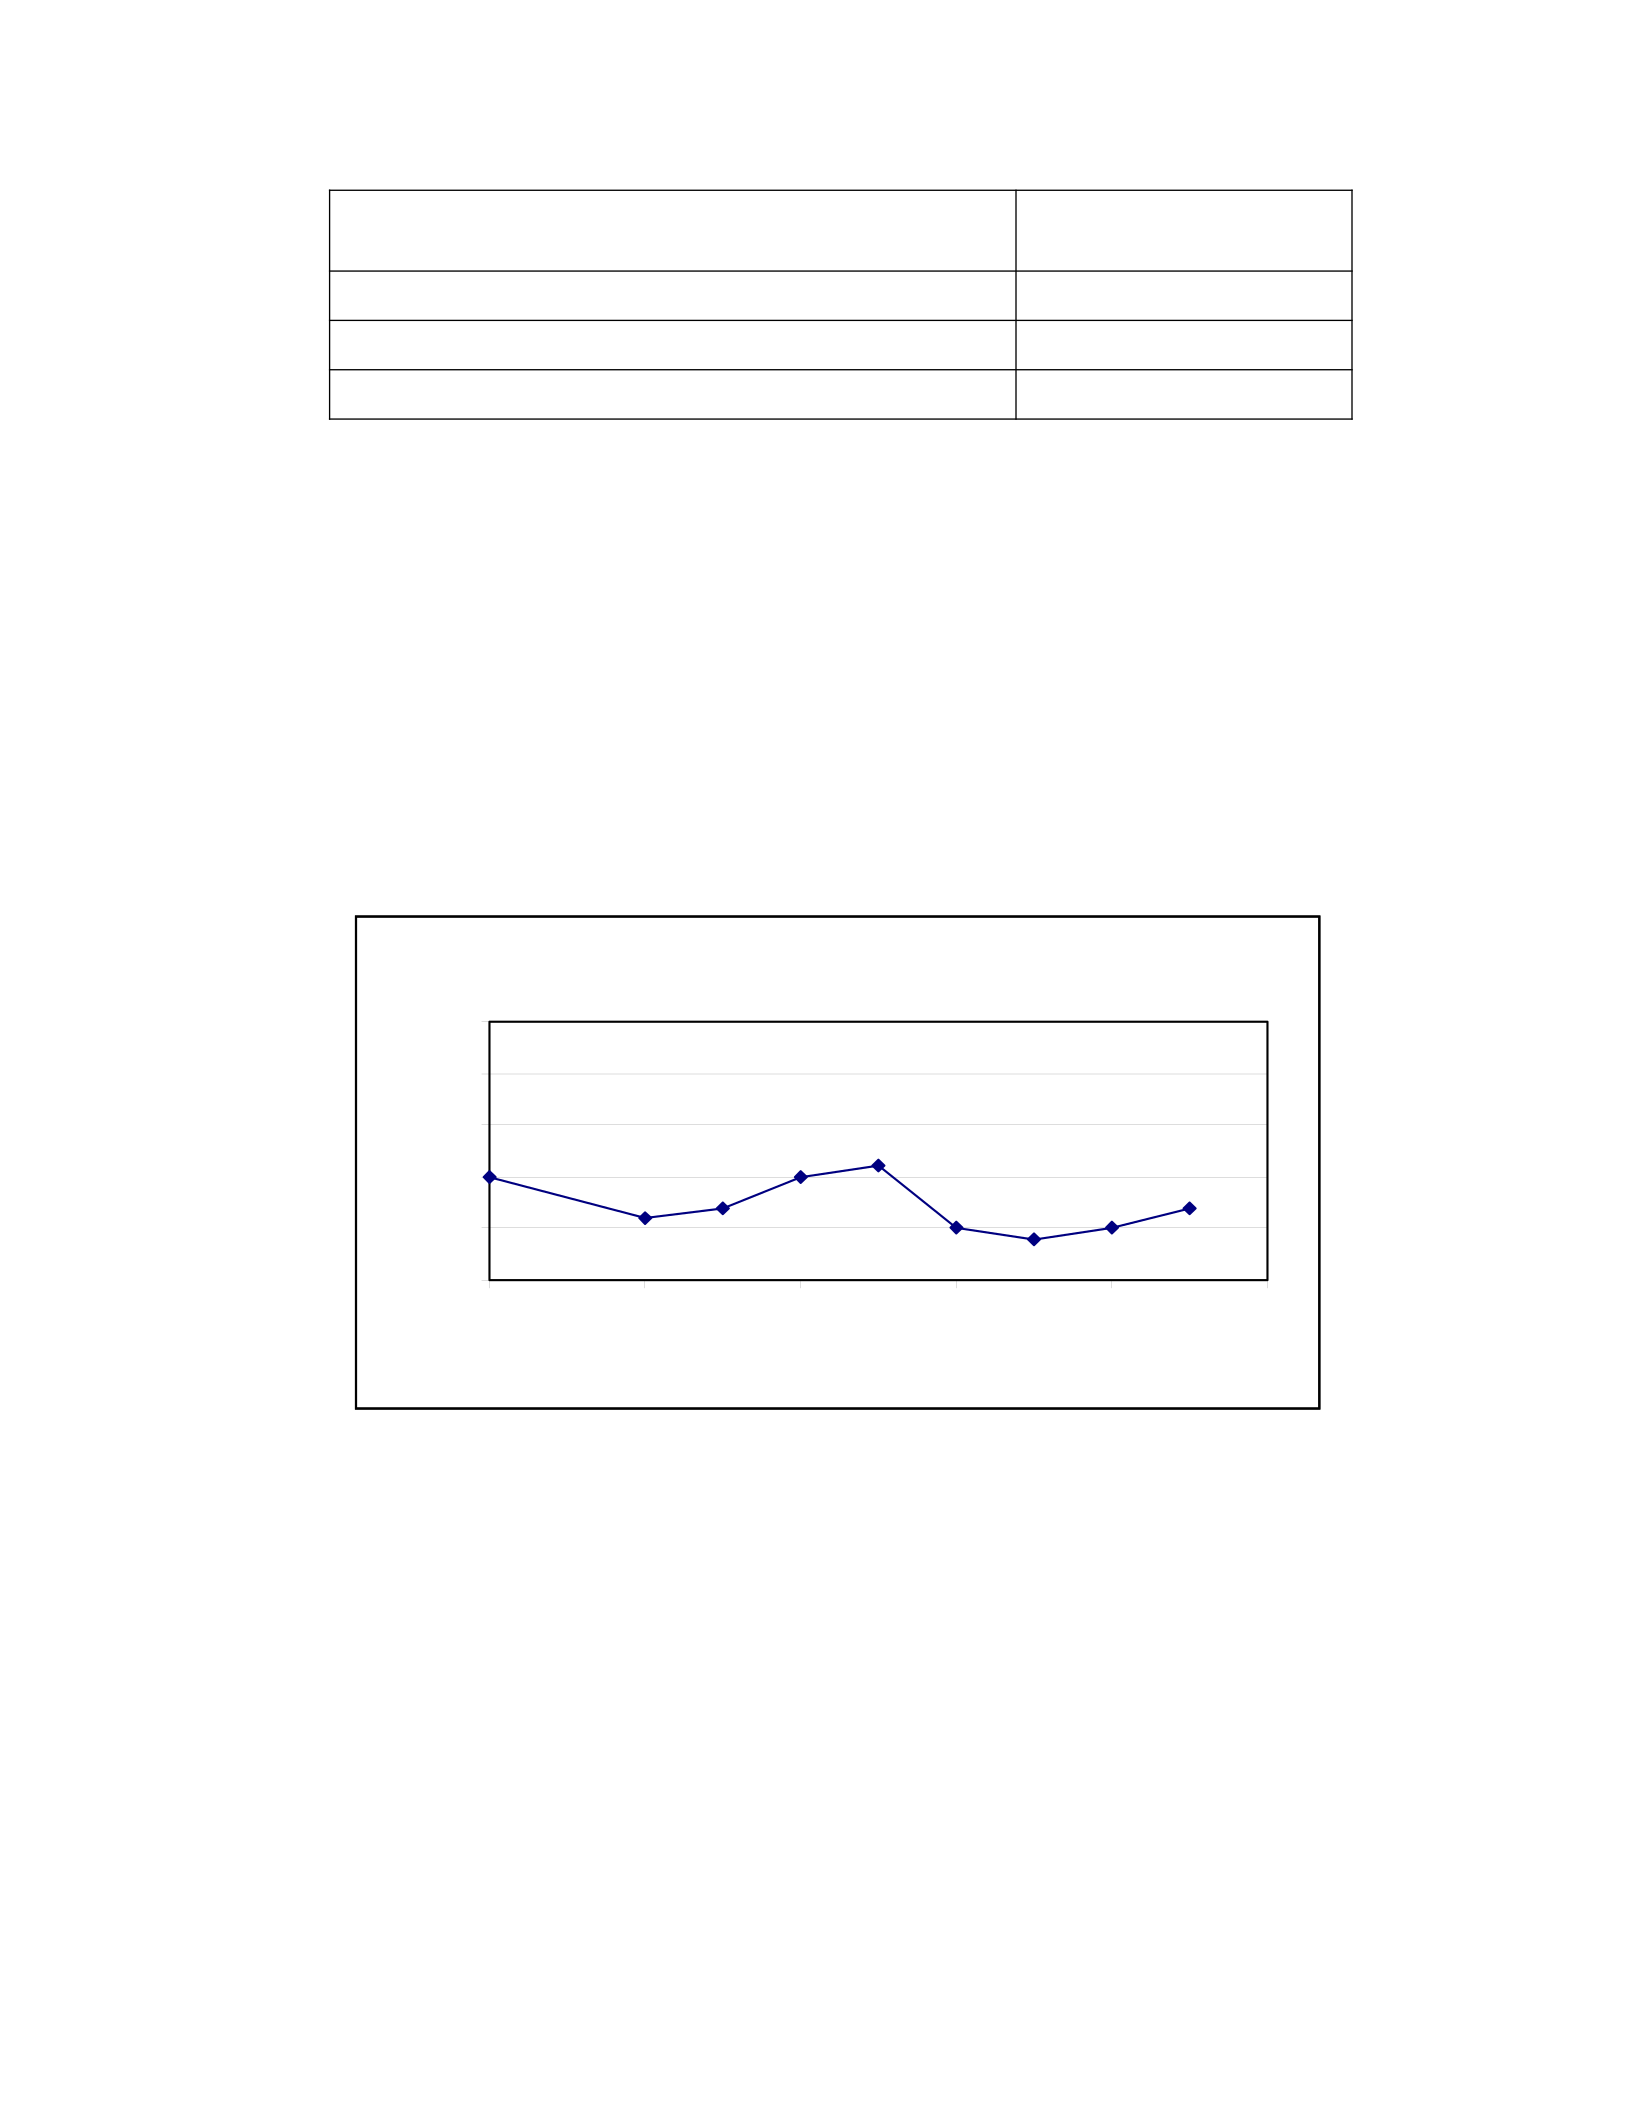
Millwork, Plywood, and Structural members
(SIC 243)
22.4
Wood containers (SIC 244) 4.5
Wood buildings and Mobile homes (SIC 245) 13.2
Miscellaneous wood products (SIC 249) 13.6
Table1.2: Billion $ Shipments – 1997 [35]
1.6.3 Labor Productivity
Technological improvements in the wood products sector have not been as
pronounced as in other sectors. As a result, labor productivity statistics in the lumber and
wood products sector have been either declining or relatively stable during the 1987-1996
time frame. As can be seen in the Figure1.2 below which shows the labor output per hour for
the years 1987 –1996.
Figure1.2: Labor Productivity [35]
1.7 Energy Use in Forest and Wood products industry
The forest products industry consumed more than 3.1 quads of energy in 1994. This
represents about 14% of domestic manufacturing energy use, making the forest products
industry as a whole the third largest industrial consumer of energy, behind only petroleum
and chemicals. Within the forest products industry, the pulp and paper industry (SIC 26) uses
the vast majority of the energy, 2.66 quads, while the lumber and wood products industry
uses only 0.491 quad. The total energy usage for SIC 24 can be seen in the following Table
1.3.
Labor Productivity
90
95
100
105
110
115
1987 1989 1991 1993 1995 1997
Year
Labor output per hour
Year Total Energy Use
(trillion Btu)
1985 325
1988 407
1991 451
1994 491
1998 584
Table 1.3: Annual energy use for SIC 24 [35,36]
1.7.1 Energy Use by Fuel
In 1998, the lumber and wood products sector generated 387 trillion Btu, or 66% of the
industry’s energy needs, from wood residues. Remaining energy needs were met by
electricity, natural gas, and fuel oil. A pie chart of the energy use by fuel is as seen in the
Figure 1.3.
Figure 1.3: Energy Use by Fuel – 1998 [35,36]
1.7.2 Energy Expenditures
The forest products industry spent $7.7 billion on purchased energy in 1994, more
than 11% of total U.S. manufacturing energy expenditures. Of this amount, about $6 billion
was spent by the pulp and paper industry and $1.7 billion by the lumber and wood products
industry. Electricity purchases represent the largest share of energy costs, almost half of the
pulp and paper industry’s energy expenditures and over half of lumber and wood products’
purchases in 1994. Figure 1.4 below shows the distribution of the energy expenditure
according to the fuel type.
Figure 1.4: Energy Expenditures (SIC 24) – 1994 [35,36]
1.7.3 Technologies and Equipment
Transforming whole trees into lumber and wood products require significant physical and
chemical processes that are highly energy intensive. The forest products industries alone
account for over 14% of total industry demand. The technologies used by the lumber and
wood products industry differ significantly from those used by pulp and paper industry.
Principal processes in lumber and wood products as discussed earlier include debarking, log
processing, drying, product fabrication, and finishing. The Table 1.4 shows the various major
technologies used for the different unit operations carried out during the manufacturing of
lumber and wood products.
Unit
Operation
Purpose Major Technologies
Debarking Removes bark from the whole log Barking drum, ring barker
Log Production of round wood (poles, posts),
sawn wood (lumber), veneers
Computer vision mechanical
sawing, cutting and chipping
Drying Removing moisture from wood to
facilitate shipping, handling, preservation
and the application of treatments
Kiln or air drying
Fabrication Additional processing to form desired end
product
Specialized mechanical
sawing, drilling, sanding, high
pressure chemical reformation
Finishing Preserving and treating wood for final use Pressure treatment, chemical
treatment, coating
Process
Heating
To drive pressure, steam and drying
applications
Direct heating, furnaces, kilns,
dryers
Table 1.4: Industry specific technologies [36]
1.7.4 Energy management activities
Manufacturers may conduct a number of energy management activities to improve the
efficiency of energy use at their facilities. The four top management techniques used by the
forest products industry include energy audits, electricity load controls, power factor
correction or improvement, and facility lighting. The most commonly used of these is the
energy audit, employed by almost 2,500 facilities in 1994. The different activities and the
number of establishments doing them can be seen in the following Table 1.5.
Activities Number of
establishments
% Consumed energy for
heat and power
Energy Audits 1,413 24.6%
Power Factor Correction of
Improvement
1,068 21.4%
Electricity load control 1,021 19.8%
Facility lighting 736 11.3%
Table 1.5: Energy Management Activities – 1994 [36]
1.8 Wood Industry in West Virginia
The wood products industry is of growing importance to West Virginia’s economy.
According to the West Virginia Forest Association, the Forestry Industry provides the state
with more than 30,000 full time jobs. The wood industry supported the following list of
operations [37]:
Sawmills 181
Veneer mills 3
Rustic fencing mills 18
Dry kilns 58
Pressure treating plants 11
Concentration yards 46
Manufacturers of wood products 181
Engineered wood products 3
Firewood producers 2
With 11.6 million acres of timberland and 75 billion board feet of inventory, the forest
resources of West Virginia seem endless. The state sits at the geographic center of the world-
renowned Appalachian Hardwood belt. Climate and soils combine to provide an ideal
growing environment for hardwoods. The species type and percent quantity of the total
inventory are shown in the Table 1.6.
Species % Of total Inventory
Red Oak 26 %
White Oak 24 %
Yellow Poplar 21 %
Maple 10 %
Black Cherry 4 %
Other 15 %
Table 1.6: Volume by species of Saw timber - 2001 [37]
1.9 Need for Research
This research work is concerned with the energy analysis and diagnostics in wood
manufacturing industry in West Virginia. The need for this research work stems from the fact
that energy conservation is being considered as a vital issue for the future, considering the
steady increase in primary energy costs, the inability of supplies and predicted limitations.
Energy conservation will allow the earth’s limited resource base of high quality fuels to be
stretched further. It will also allow a portion of the fossil fuel base to be reserved for non-
energy purposes. The fact is that we may be faced with a continuing shortage of fuel and
power unless new sources are developed in the future. Part of the shortage can be
compensated for by conservation measures. Otherwise major dislocations and even
catastrophe may be in store for the companies and institutions.
1.10 Energy research in West Virginia
The Appalachian Hardwood Center at West Virginia University was created by the
West Virginia legislature to assist in the orderly expansion of the hardwood industry in West
Virginia. The West Virginia Development Office has utilized the Center and the College of
Engineering and Mineral Resource’s (CEMR), Industrial and Management Systems
Engineering department to provide information to the industry on marketing opportunities for
wood residue and overall process efficiency opportunities. The intent of this project and
research is to take further advantage of the technical resources to improve operational
efficiency and energy performance of forest industry businesses.
Wood industry in general has not seen much technical improvement over the years in
terms of productivity and energy efficiency as can be seen in the labor productivity data from
the Manufacturing Consumption of Energy 1998. Wood industry in West Virginia is a major
contributor to the state. With recent crisis in the Energy sector, it becomes important to

concentrate our efforts on energy conservation and energy management. Energy costs
contribute to the manufacturing cost of the products. The need for research is justified
because several opportunities have been overlooked by the wood manufacturing industries.
To understand the potential for industrial energy conservation, consider the industrial plant as
a system. We can observe that on one side we have inputs of energy raw materials and labor
and on the other side, the output of goods, waste energy and waste materials. In order to
maximize profits the energy manager attempts to keep the costs of inputs to a minimum. In
the past in many cases, since the cost of energy was low in relation to the other inputs, it was
ignored. However, with today’s spiraling energy prices, more attention is being given to
energy input. Energy savings can occur either by improving the energy conversion process,
by recycling the waste energy or by reusing the waste materials. Many opportunities exist for
the application of the existing technology to yield large energy savings, which in turn means
large cost savings for the company. For this to occur, however, answers must be found for
two major questions:
1. What are the areas of activity in which there may be significant potential for better
use of energy?
2. Within these areas, what are the specific measures or alternative options that could
lead to better and more efficient use of energy?
Usually in an energy management program, the answers to these questions are sought in
specific terms by means of energy audits. This is a phase in the energy management program,
which involves the determination of where and how the energy is being used in the facility.
1.11 Research objectives
The objectives of this work are to actually conduct site audits at several lumber and wood
manufacturing plants in West Virginia, using the collected data, determine energy
conservation opportunities and recommendations. We need to understand the potential for
these assessment recommendations with respect to the parameters governing them. The
specific objectives of the research were:

1) To identify potential recommendations in the field of energy conservation and energy
management.
2) To collect data on site regarding to various potential opportunities available on site.
This might include extensive measurements on major energy consuming equipment
related to electrical consumption, hours of operation, load factor and other data. The
data collection would involve use of data recording devices such as electrical power
analyzers, digital stroboscopes, and temperature guns.
3) Analyze the measured and collected data with respect to the other recommendation
for the plant and get preliminary results. Make extensive use of decision tools such as
Motor Master for better understanding of the collected data especially on the plant
motors. Identify the opportunities for downsizing and replacement of motors in the
plant.
4) Identify the major parameters governing the recommendations. Measure and analyze
the impact of each of these parameters on the resulting savings potential. Do a
thorough diagnosis and sensitivity analysis for all of these major factors governing
the recommendation. Perform a thorough analysis of the plant motors using Motor
Master software.
5) Gain better insight into the various operating parameters, which govern the
recommendations and report them.
1.12 Conclusions
This chapter discussed the nature of energy crisis, highlighted the problem areas and
projected the importance of energy efficiency improvements. It also discussed the wood and
lumber manufacturing industry in general and also in West Virginia. It is proposed to carry
out energy assessments at several wood and lumber manufacturing facilities in West Virginia
and do exhaustive measurements and analysis of the data collected. It is proposed to do a
sensitivity analysis for all the recommendations and the major parameters governing them.

Chapter 2 Literature Review
Although much literature has not been cited in the area of energy management in the
wood manufacturing industry especially under SIC 24, there are some publications in the
pulp and paper industry and forest products industry that are discussed in the following
sections.
2.1 Energy Analysis in Forest products industry
Various recommendations made during IAC audits of over 200 pulp and paper
industries are discussed in [1]. This paper covers the wood products sector (SIC 24) and
paper product sector (SIC 26) and includes the most common energy conservation
opportunities and waste minimization opportunities cited during these assessments. These
assessments contain recommendations for reducing energy use in all forms (oil, natural gas,
electricity, etc.) The energy efficiency of existing dust collection systems in wood furniture
manufacturing plants is investigated in [2]. It is observed that these dust collection systems
are in general running at lower efficiencies. The characteristics, which contribute to this
situation, are identified and discussed in [2]. A wood dust collection system based on
energyefficient concepts utilizing readily available technology is proposed in [2]. The
proposed system is estimated to be nearly 30 to 35% more efficient than the existing
conventional systems.
The use of Motor Master (DOS format) by many within the pulp and paper and other
industries to evaluate and select motors for energy efficiency and lowest life cycle cost, is
discussed in [3]. It also covers Motor Master+, an enhanced version of motor master,
presented in Windows format. The discussion covers Motor Master’s motor and motor driven
system energy management capabilities, the determination of motor load and efficiency from
field-testing measurements, energy savings determination and life cycle costing., use of
utility rate information, and the types of motor selection are also addressed in the paper.
The author discusses a method for estimating motor efficiency and analyzing the
conditions in pulp and paper industry in [4]. Load management measures in a carpentry
factory in Sweden are discussed in detail in [5]. It describes the use of electricity and heat in
a carpentry factory. The results show that energy conservation measures and load

management might be of significant importance in order to make the company more
profitable. Even small savings can make the difference between survival and bankruptcy. The
study finds that much of the equipment for heating purposes is in poor state. The steam
system, which could be useful for decreasing the use of electricity heating, suffers from
leaking steam traps and other imperfections, which lead to severe loss in both kilowatt-hours
and money.
Spreadsheet based decision support system for wood panel manufacturing is
discussed in [6]. It describes an MS Excel – based decision support system for wood panel
manufacturing. The system is easy to use and maintain and gives the shop floor personnel
access to powerful optimization capabilities useful for fine tuning production processes in the
face of changing supply and price situations.
Many areas of the mechanical pulping process are explored for energy saving
opportunities in [7]. Typically, over 50% of the cost associated with the manufacture of
mechanical pulp is energy. Improving the efficiency of energy utilization in the manufacture
of mechanical pulp can result in dramatic savings. The author proposes different ideas for
such improvements in this paper. Influence of lumber grade on machine productivity in the
rough mill is discussed in [8]. Lumber grade effect in hardwood-part processing time is
investigated with a digitally described lumber database in conjunction with a cross cut-first
rough mill yield optimization simulator.
Research in the field of automatic inspection of wood, particularly focusing on
computer vision techniques for improving productivity and reducing waste is discussed in
[9]. The proposed methods are put into an automated visual inspection framework, which is
subdivided into commonly used modules for image acquisition, image enhancement, image
subdivision, feature extraction, and classification. Use of premium efficiency motors in pulp
and paper industry and the resulting savings are discussed in [13]. The author says that pulp
and paper industry doesn’t look upon use of premium efficiency motors with doubt. They
rather claim more of their benefits because their typical mill operations fit the ideal profile for
premium efficiency motors. The author says that this industry requires a relatively large
number of motors, most of them within the size range that shows the biggest savings and
most of them running round the clock. The author also stresses that premium efficiency

motors are highly reliable and they really pay rich dividend in processes where downtimes
might be very expensive.
2.2 Energy Technology Research and Development
Along with this an extensive literature review on the different recommendations was
done. Special emphasis was laid on electric load management, motor efficiency, motor
downsizing, compressor efficiency and belt transmission.
The real costs of energy consumption and detailed description on utility bills and its
various components is discussed in [10]. The author identifies significant but overlooked cost
components of electric power that could allow an energy manager to determine a basic
energy rate more accurately and beneficially. The author discusses the cost components of a
typical quantity of electric power, which include demand, operating and maintenance related
costs.
A logical, systematic and structured approach to reduce energy waste by use of motor
efficiency management techniques is discussed in [11]. The author also presents a motor
performance management process (MPMP), which is designed to evaluate, measure and most
importantly manage electric motors. It is a logical, systematic and structured approach to
reduce energy waste. Use of energy efficient motors and creating efficient motor system is
demonstrated with benefits in [12]. The author says that in industrial and commercial
facilities, motor-driven systems are responsible for as much as 70% of a building’s electric
consumption. But with energy efficient motors and motor systems, energy cost could be cut
down while improving the efficiency of the systems and reducing equipment maintenance.
Energy conservation aspect of induction motors using improved design and power
controllers are studied on irrigation pumps and textile motors in [14]. The author examines a
motor design for energy efficient operation and compares with conventional designs. Energy
conservation through adaptive variation of the supply voltage is examined. The desired
voltage variation of minimum energy consumption at varying loads is obtained by
mathematical modeling and computer simulation, incorporating magnetic non-linearity in the
motor. Quality and reliability of energy efficient motors is tested against standard efficiency
motors and various measurements are taken and discussed in [15]. The test involved two
identical ratings, one of premium efficiency and other of standard design under the same

unbalanced voltage conditions. Measurements of current, power inputs, and the power factor
angles were taken for the unbalanced in voltages ranging from 0% (balanced condition) to
10% at intervals of two percentage points. Results confirmed that motors should not be
operated with any significant amount of voltage unbalance, which would result to losses,
noise, and vibration.
The question, whether, "Are energy- efficient motors a cure-all for energy problems?"
is discussed nicely in [16]. Various challenges posed by the application of energy efficient
motors in highly motor intensive industries like petrochemical, pulp and paper and food
processing is discussed in [16]. The author says that using energy efficient motors instead of
standard efficiency motors can conserve energy considerably. However, he stresses that
application of energy-efficient motors can pose many challenges. Considering the complexity
of industrial plant efficiency and design, it is vital for consultants to keep pace with the
rapidly changing technology. The author says that both clients and consultants must also
recognize that energy efficient motors are not the ultimate solution for an ailing system.
Impact of energy saving technologies on electric distribution system power quality is
discussed in [17]. This paper contains a discussion of several energy saving technologies and
their impact on electric power distribution systems. The reduced power demand of these
energy saving devices reduces the peak system demand. However, there are increased
distribution transformer and distribution network losses due to the distorted load current
wave shape. These losses, when integrated over many services and over the year, represent a
significant cost due to fuel costs and higher peak.
Review of metering plans for demand side management savings verification is
discussed well in [18]. It discusses various load monitoring systems and ways to document
actual savings from demand side management programs. Increasingly, utility commissions
are requiring documentation of actual savings from DSM programs. For constant loads, such
as lighting and constantly loaded motors, this can be done by taking instantaneous before and
after readings and multiplying the difference in kW by a run-hour meter reading to obtain
kWh savings. In varying load applications, however, documenting savings is not simple.
Energy saving with pump's AC adjustable speed drives is discussed in [19]. A detailed
description, benefits and capabilities of Motor Master + are described in [20]. The author
discusses several models and capabilities of Motor Master + such as motor inventory control,

field measurements and operating data storage repository, batch analysis capabilities and life
cycle costing. Several tips for fitting the perfect motor for a silk screen-printing application
is presented by the author in [21]. The motor's speed and torque requirements by the
application and consequent approximation of load's continuous and peak requirements are
discussed in [21]. The author says that special consideration should be given to the selection
of motor type and speed reducer, as well as the optimum motor size.
Application of compound fuzzy control in the power saving of motor is discussed in
[22]. Here the author solves the problem of optimal control while the dynamic plants are
under varying loads. Reducing the cost of compressed air in industrial facilities is described
at length in [23]. The authors evaluated and quantified the energy losses associated with
compresses air systems and their costs to manufacturers. Among the measures investigated in
reducing the cost of compressed air were repairing air leaks, reducing the pressure setting if a
lower pressure setting is inadequate, using a smaller compressor at full load instead of large
one at part load, reducing average inlet temperature using outside air, using waste heat from
the cooling fluid to heat the facility in winter, using high efficiency motors, turning off the
compressor at night and during lunch breaks and using an after cooler.
Energy efficiency in air handling applications and use of variable speed drives is
discussed in [24]. A comparative study of energy saving benefits in soft starters for
threephase induction motors is investigated in [25]. Modern soft starters have both soft starter
capability and energy saving functions, which are especially useful when the motor runs at
low load. This paper investigates modern soft starters for induction motors at three different
power levels. The investigation includes efficiency measurements, start-up measurements and
measurement of the grid current harmonics at different loads to investigate the soft starter’s
performance against new regulations. The measurements are compared with an induction
motor without soft starters. It is concluded that soft starters have energy saving capabilities at
low load up to 4% of rated power for small motors, but it also concluded that the payback
time would be long. Finally they conclude soft starters have problems with new grid
disturbance regulations at low load operation. A survey of characteristics of different belt
types, with a particular emphasis on their energy efficiency, cost effectiveness and field of
application is done in [26].

The energy efficient electric motor selection handbook [27] contains a discussion on
the characteristics, economics, and benefits of standard versus high efficiency motors in the 1
to 500-horse power range. This handbook shows how to assess energy savings and cost
effectiveness when making motor purchase decisions. It also discusses field data acquisition
techniques, high efficiency motor speed/load characteristics, performance under part-load
conditions, and operation with an abnormal power supply.
A fact sheet developed by a program of the U.S. Department of Energy, discusses the
reasons to determine motor loading [28]. It discusses the various methods of testing motor
loads. It also discusses various issues in motor efficiency testing. Another fact sheet [29]
describes the term power factor and shows how to correct low power factors. Reference [30]
is a bulletin developed by Industrial Electrotechnology Laboratory that outlines a policy for
cost effective management of motor purchase and repair. It also provides a checklist for
motor maintenance and repairs. Guidance on using the US DOE developed software MM + is
available in [31], which is a User Guide for the Motor Master + program. It discusses the
various modules in the Motor Master + software and also describes how to create a motors
database, and how to use the “ batch” module and the “compare” module in making motor
replacement and repair decisions.
2.3 Wood manufacturing industry
The manufacturing process for lumber manufacturing and the various equipment involved is
discussed here. Also the recent trends in the energy consumption in wood manufacturing
industry are discussed. In [32] the lumber manufacturing industry is described in detail. The
lumber manufacturing process and various components involved are discussed. In [33], the
design and operations of sawmills is discussed. The major manufacturing equipment and
machinery involved in manufacturing wood products is discussed. In [34] the modern saw
mill techniques are discussed. The modern productive systems on various saw mill equipment
is discussed in detail.
The manufacturing consumption of energy 1994 and 1998 is found in [35]. All the
relevant details like amount of MMBtu used and the dollars spend on different types of fuel
in wood manufacturing industry can be found here. Various data like, total value of
shipments, labor productivity in the wood manufacturing industry in U.S. can be found here.

The Industries of Future (IOF) program and the various initiatives taken in the forest products
area are presented in [36]. The vision, roadmap, implementation and new technology strategy
for forest products industry is reported. The directory for the forest industry of West Virginia
is found in [37]. The different species of wood available and produced in the state of West
Virginia are reported here. It has an overview of the forest industry of West Virginia.
2.4 Conclusion
The above literature gives an idea about the work done in the field of energy conservation.
Many issues related to energy efficiency in industry are discussed. But there is very little
literature found on energy analysis and diagnostics specifically in the wood manufacturing
industry. Most of the efforts have been concentrated on the forest industry as a whole. The
pulp and paper industry has been given special attention all throughout the literature with
very little emphasis on the SIC 24 category, which is wood products industry. Specifically
research in the area of energy conservation and energy analysis and diagnostics in wood
manufacturing industry and especially in a state like West Virginia would be of immense help
to the industry as well as the state.
Chapter 3 Utility Bill Analysis
3.1 Data Collection
The utility bills of all the wood plants visited under the project were collected. The
historic data of the past twelve months at the minimum was collected for further analysis and
evaluation. The utility rate schedule for each plant was carefully analyzed so as to understand
the rate structure and how the electricity charges are obtained. Each plant visited has its own
rate structure with the utility service and therefore each structure is required to be analyzed
separately. Also it is seen in all the visits that electrical energy dominates the energy bill in
most of the wood industries in West Virginia. Other sources of energy like natural gas
constitute a very small percent of the total energy bill. A brief introduction to electrical cost
distribution followed by the analysis of electricity charges for each plant visited is discussed
in this chapter. Various plots are obtained and the load profile of each plant is also obtained.

3.2 Electric Cost Distribution
The analysis of the electrical costs of a facility involves the contribution of the
various components of the electricity bill towards the total cost of electricity. Following is an
example of the utility bill analysis of facility A. The utility bill analysis for the other plants
audited can be seen in Appendix I. As can be seen in the Table 3.1, the various components
used for analysis are kWh used, the demand kW on the plant, the RKVA demand on the plant,
the kWh charge, RKVA charge and the total electricity charge. The electricity billing
information for 15 months is shown in the Table 3.1. It also shows calculation of apparent
power, power factor, load factor, and demand charge as percent of total bill. Detailed
discussion on power factor and load factor is done in the recommendations on the following
pages. Here we only discuss the demand as a percentage of the total cost. The demand kW for
each month is obtained from the electricity bill. Also the demand charge is mentioned in the
schedule 15 – D, which is presently $ 9.45/kW of demand. The total charge of the electricity
is obtained from the bill and the calculation of demand charge as a percent of total charge is
done.
3.2.1 Sample Calculation
Please refer to the Table 3.1. As can be seen in the 11th row, the kW demand is 348.8
for the period from 1/19/01 to 2/21/01.
So demand or kW charge = Demand kW X $ / kW
= 349 X 9.45
= $ 3,297
Also it can be seen that the total charge for this period is $ 5,654.27.
So demand as a percent of total charge = 3297 / 5,654 *100
= 58.3 %
The marginal cost of electricity per MMBtu is calculated by dividing the total cost of
electricity for all the months by the total MMBtu of electricity consumed in all those months.

The average cost of MMBtu is $ 21.95/MMBtu. The plot of various cost components of the
bill is plotted against the months as seen in Figure 3.1. It shows a clear distinction between
the various charge components of the electricity bill and their contribution towards the total
electric charges. It can be seen that demand charge dominates the electricity charges, average
percentage demand charge being around 60%. Also it is seen that the average total electric
cost of electricity hovers around $ 5,000 for most of the months. It should be also noticed that
the demand charge is greater than the usage or the kWh charge in all the months. Appearance
of RKVA charge in the plot shows that the power factor of the plant is very low for that
month and hence this excess charge.
Months
From
Date
To Date No. of
Days
kWh
Used
kW
Demand
RKVA
Demand
kWh
charge
kW
Charge
RKVA
Charge
Total
Charge
Apparent
Power
Power
Factor
Load
Factor
Demand
as % of
( $ ) ( $ ) ( $ ) ( $ ) Total charge
Mar 3/18/2000 4/15/2000 28 61,800 323 588 1711 3022 190 4924 671 0.48 0.28 61
Apr 4/15/2000 5/20/2000 35 79,200 319 589 2193 2982 191 5366 669 0.48 0.30 56
May 5/20/2000 6/21/2000 32 71,400 323 593 1977 3022 192 5191 675 0.48 0.29 58
Jun 6/21/2000 7/21/2000 30 59,400 314 587 1664 2970 191 4825 666 0.47 0.26 62
Jul 7/21/2000 8/22/2000 32 72,600 318 589 2034 3000 191 5225 669 0.47 0.30 57
Aug 8/22/2000 9/20/2000 29 66,600 313 592 1865 2960 193 5018 670 0.47 0.31 59
Sep 9/20/2000 10/19/2000 29 71,400 339 336 2000 3204 87 5292 478 0.71 0.30 61
Oct 10/19/2000 11/18/2000 30 76,800 337 325 2151 3185 83 5419 468 0.72 0.32 59
Nov 11/18/2000 12/20/2000 32 67,200 351 364 1882 3317 97 5296 506 0.69 0.25 63
Dec 12/20/2000 1/19/2001 30 70,800 356 345 1983 3368 88 5439 496 0.72 0.28 62
Jan 1/19/2001 2/21/2001 33 81,600 349 303 2286 3296 72 5654 462 0.75 0.30 58
Feb 2/21/2001 3/20/2001 27 71,400 362 346 2000 3419 88 5507 500 0.72 0.30 62
Mar 3/20/2001 4/23/2001 34 81,000 349 312 2269 3296 76 5641 468 0.75 0.28 58
Apr 4/23/2001 5/22/2001 29 65,400 355 373 1832 3358 100 5289 515 0.69 0.26 63
May 5/22/2001 6/22/2001 31 57,800 335 1063 1619 3164 378 5161 1114 0.30 0.23 61
Total 1,054,400 5,042 7,305 29,466 47,563 2,216 79,245 Average 0.59 0.28 60.00

Table 3.1 Utility bill analysis for facility A
29
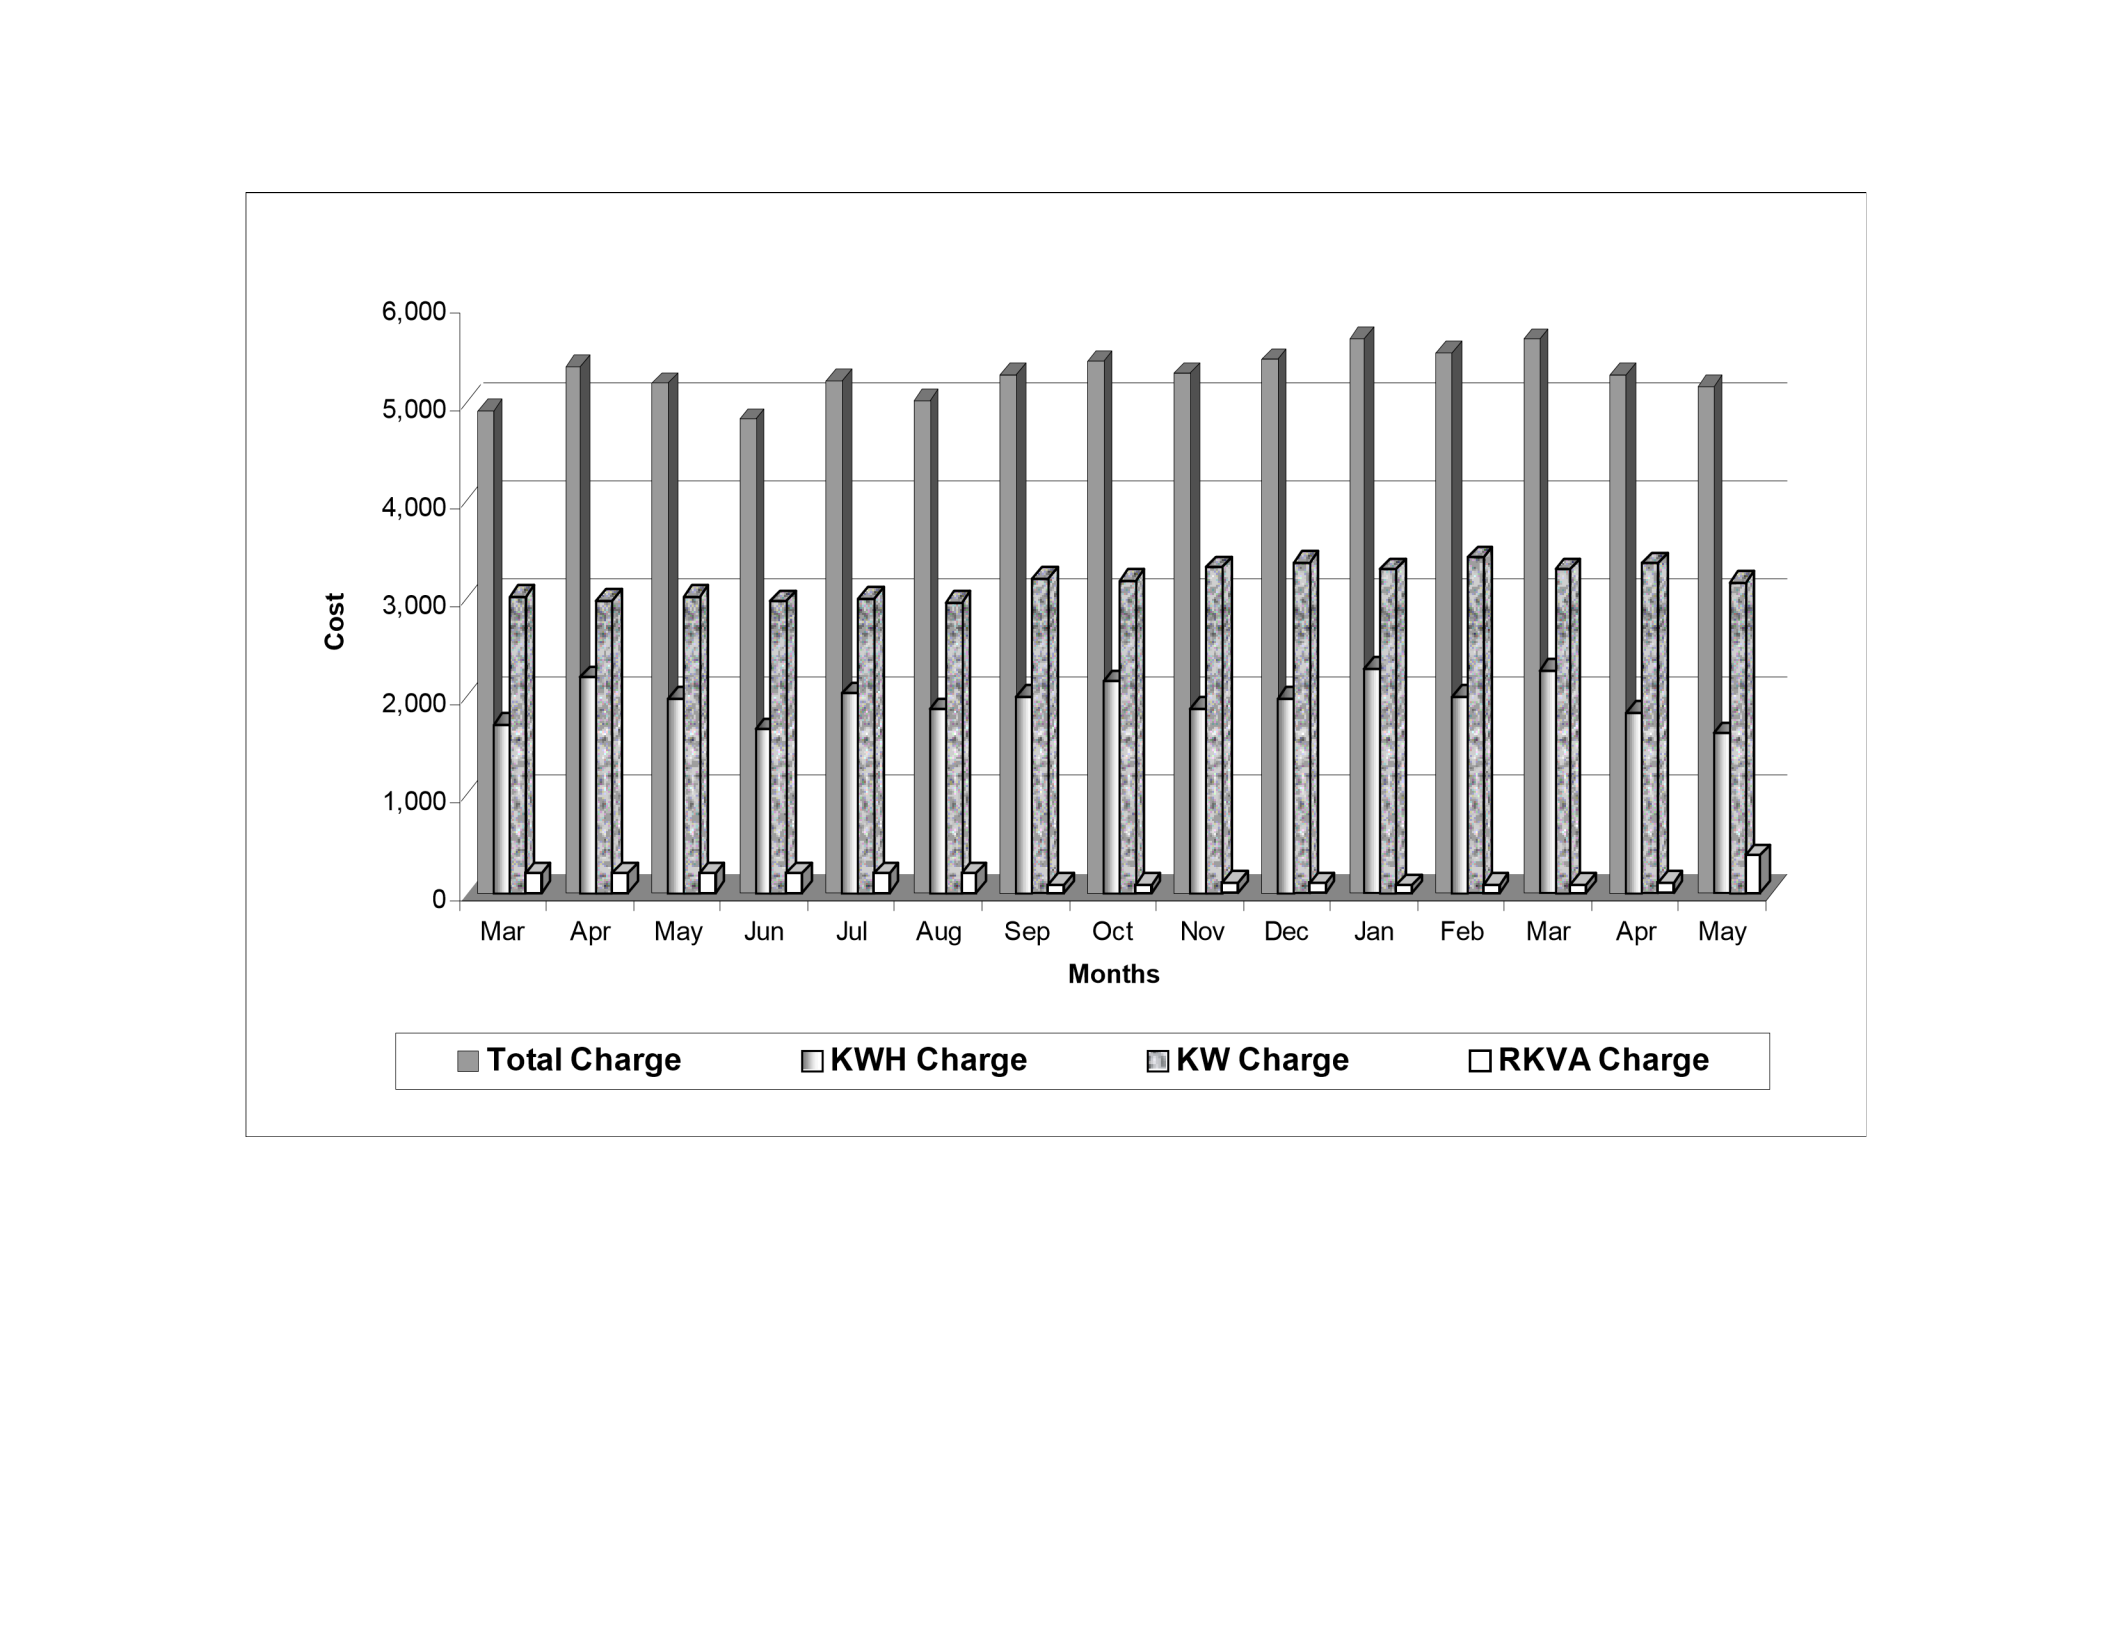

Figure 3.1 Electricity cost distribution for facility A
30

3.2.2 Load Factor Sample Calculation
Please refer to the Table 3.1 and to the first entry in table. It shows the electrical
summary for the month of March 2000. As seen in the table, energy usage is 61,800 kWh,
billed demand is 323 kW and usage cost is $ 1,711. With the above data the load factor is
calculated as follows:
Load factor = 61,800 / (323*24*30)
= 0.28
Similarly the load factor is calculated for all the remaining months.
3.3 Power Factor
Power factor (PF) quantifies the reaction of alternating current (AC) electricity to
various types of electrical loads. Inductive loads, as found in motors, drives and fluorescent
lamp ballast’s, cause the voltage and current to shift out of phase. Electrical utilities must
then supply additional power, measured in kilovolt-amps (KVA), to compensate for phase
shifting. To see why, power must be examined as a combination of two individual elements.
The total power requirement constituents can be broken down into the resistive, also known
as the real component, and reactive component. Useful work performance comes from the
resistive component, measured in kilowatts (kW) by wattmeter. The different components of
electrical power are show in the Figure 3.2.The reactive component, measured in reactive
kilovolt-amps (KVAR), represents current needed to produce the magnetic field for the
operation of a motor, drive or other inductive device but performs no useful work, does not
register on measurement equipment such as the watt meter. The reactive components
significantly contribute to the undesirable heating of electrical generation and transmission
equipment formulating real power losses to the utility.
Power factor derives from the ratio of real, usable power (kW), to apparent power
(KVAR). Assessment recommendations towards reduction of the power factor in fact indicate
reduction of reactive losses. To accomplish this goal, the industrial electricity user must
increase the power factor to a value as close to unity as practical for the entire facility. The
supplying utility should be consulted for the determination of the requisite amount of
33
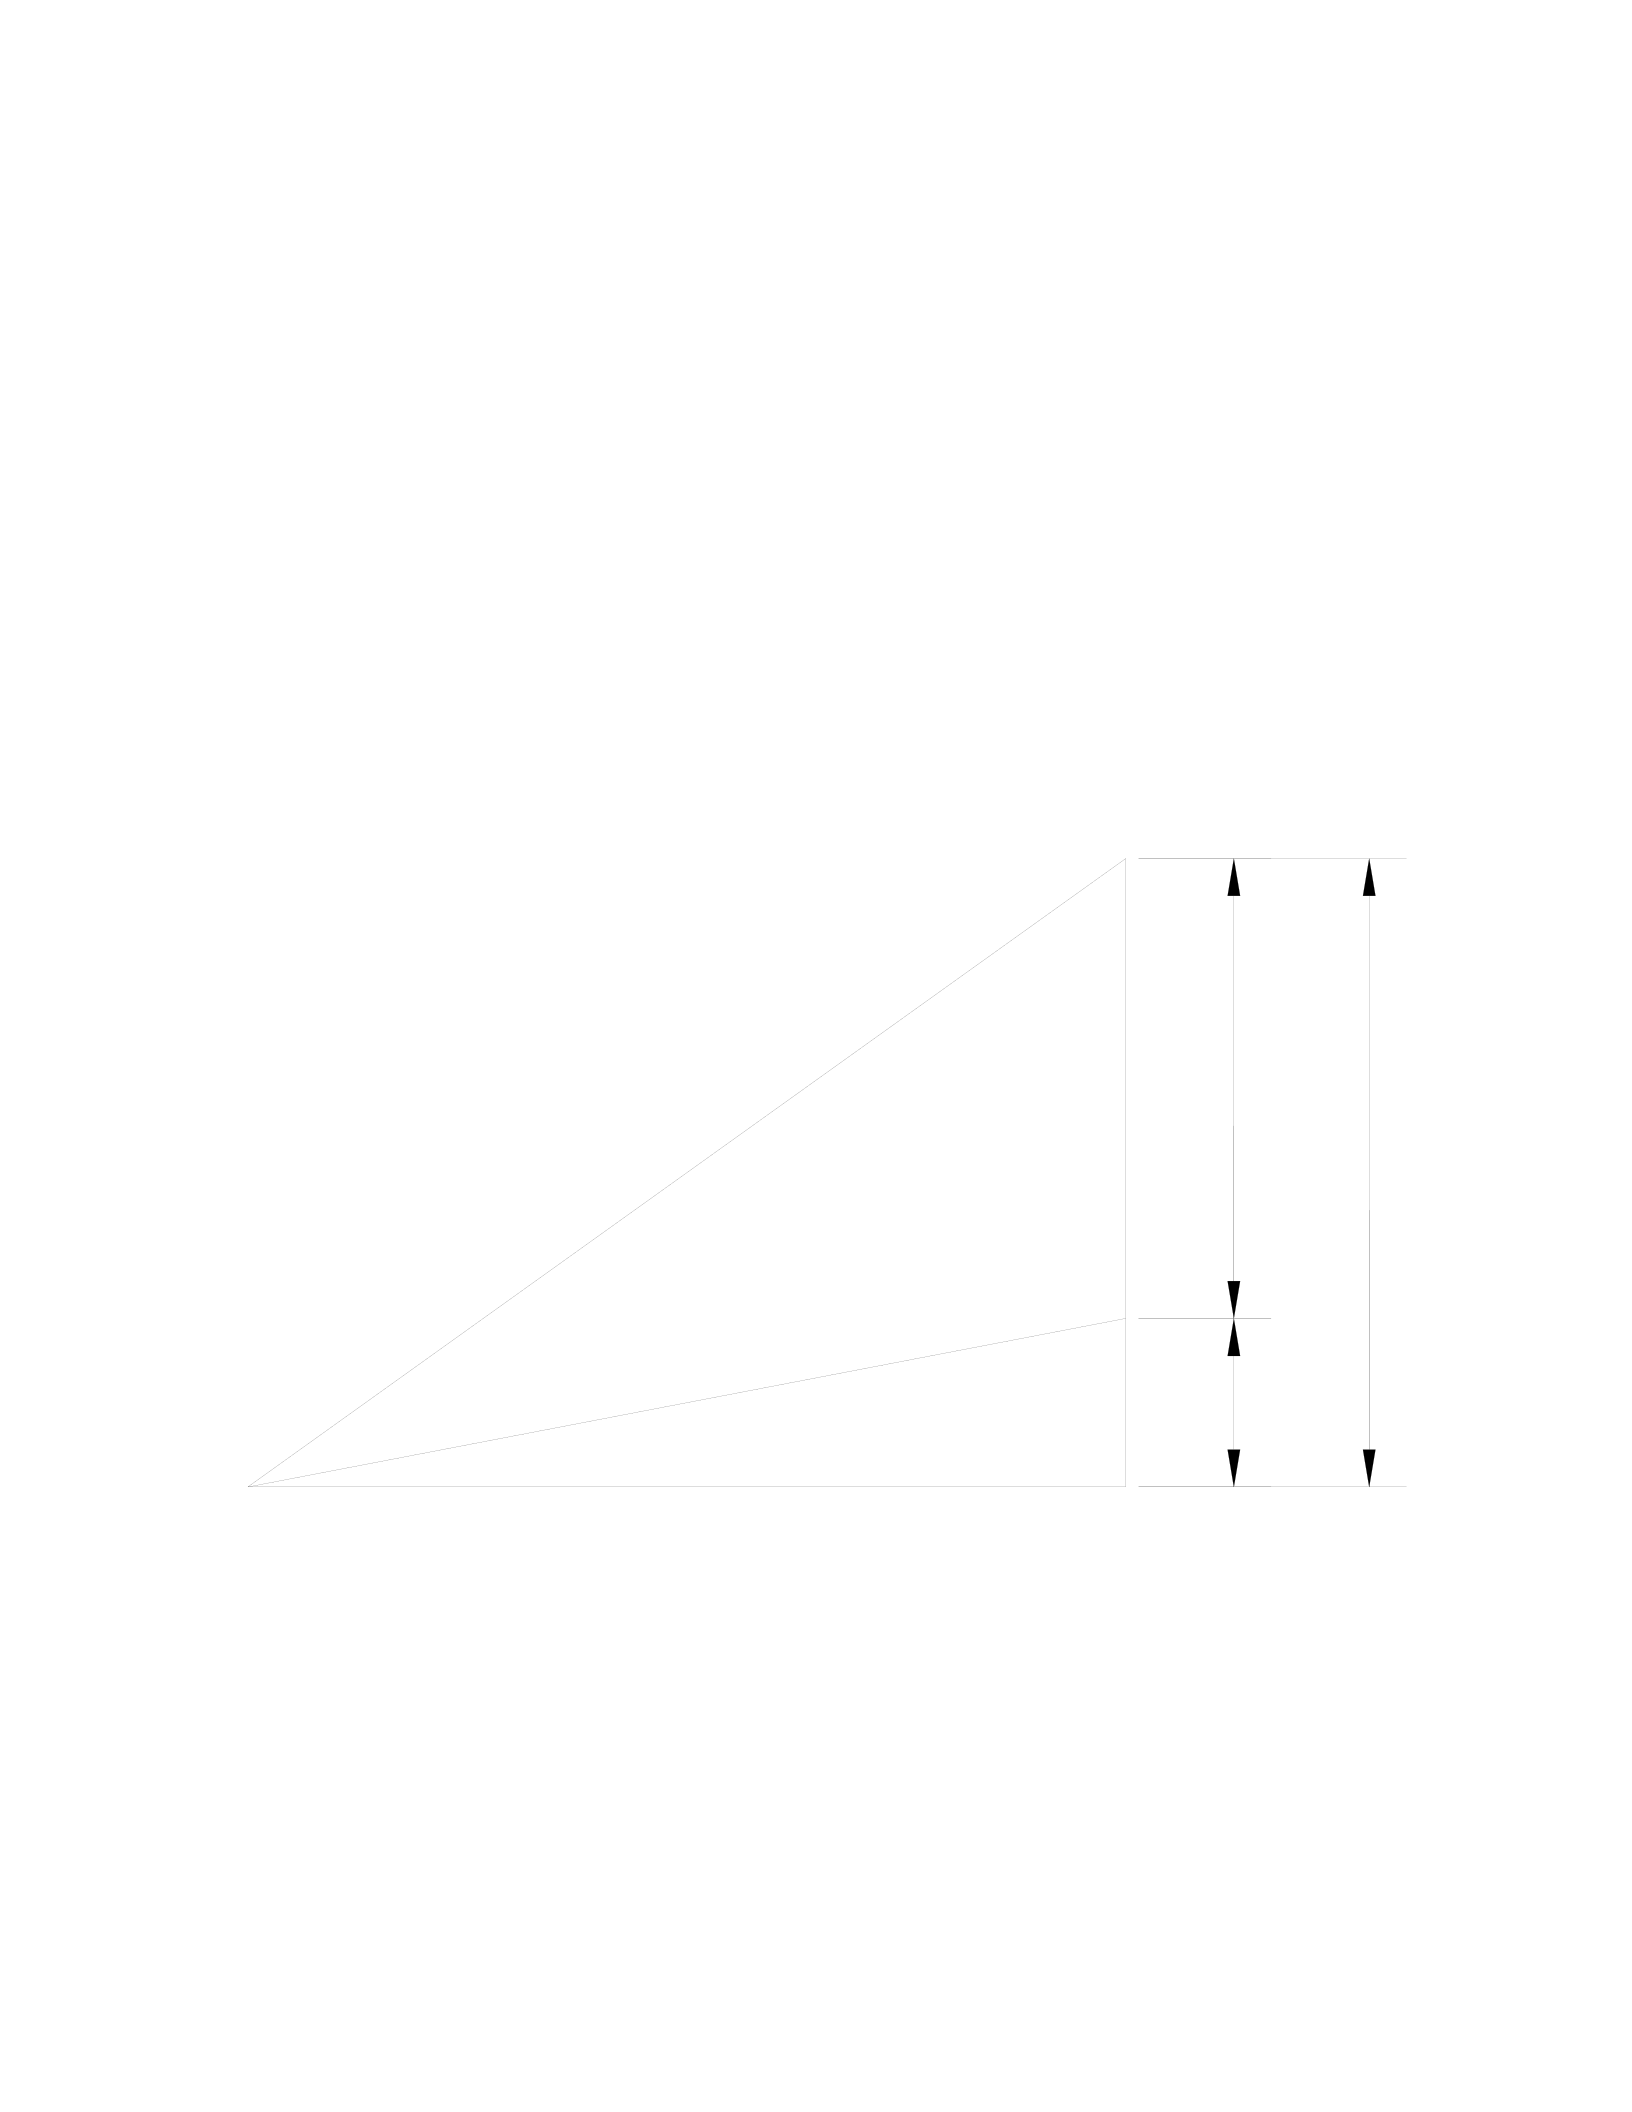
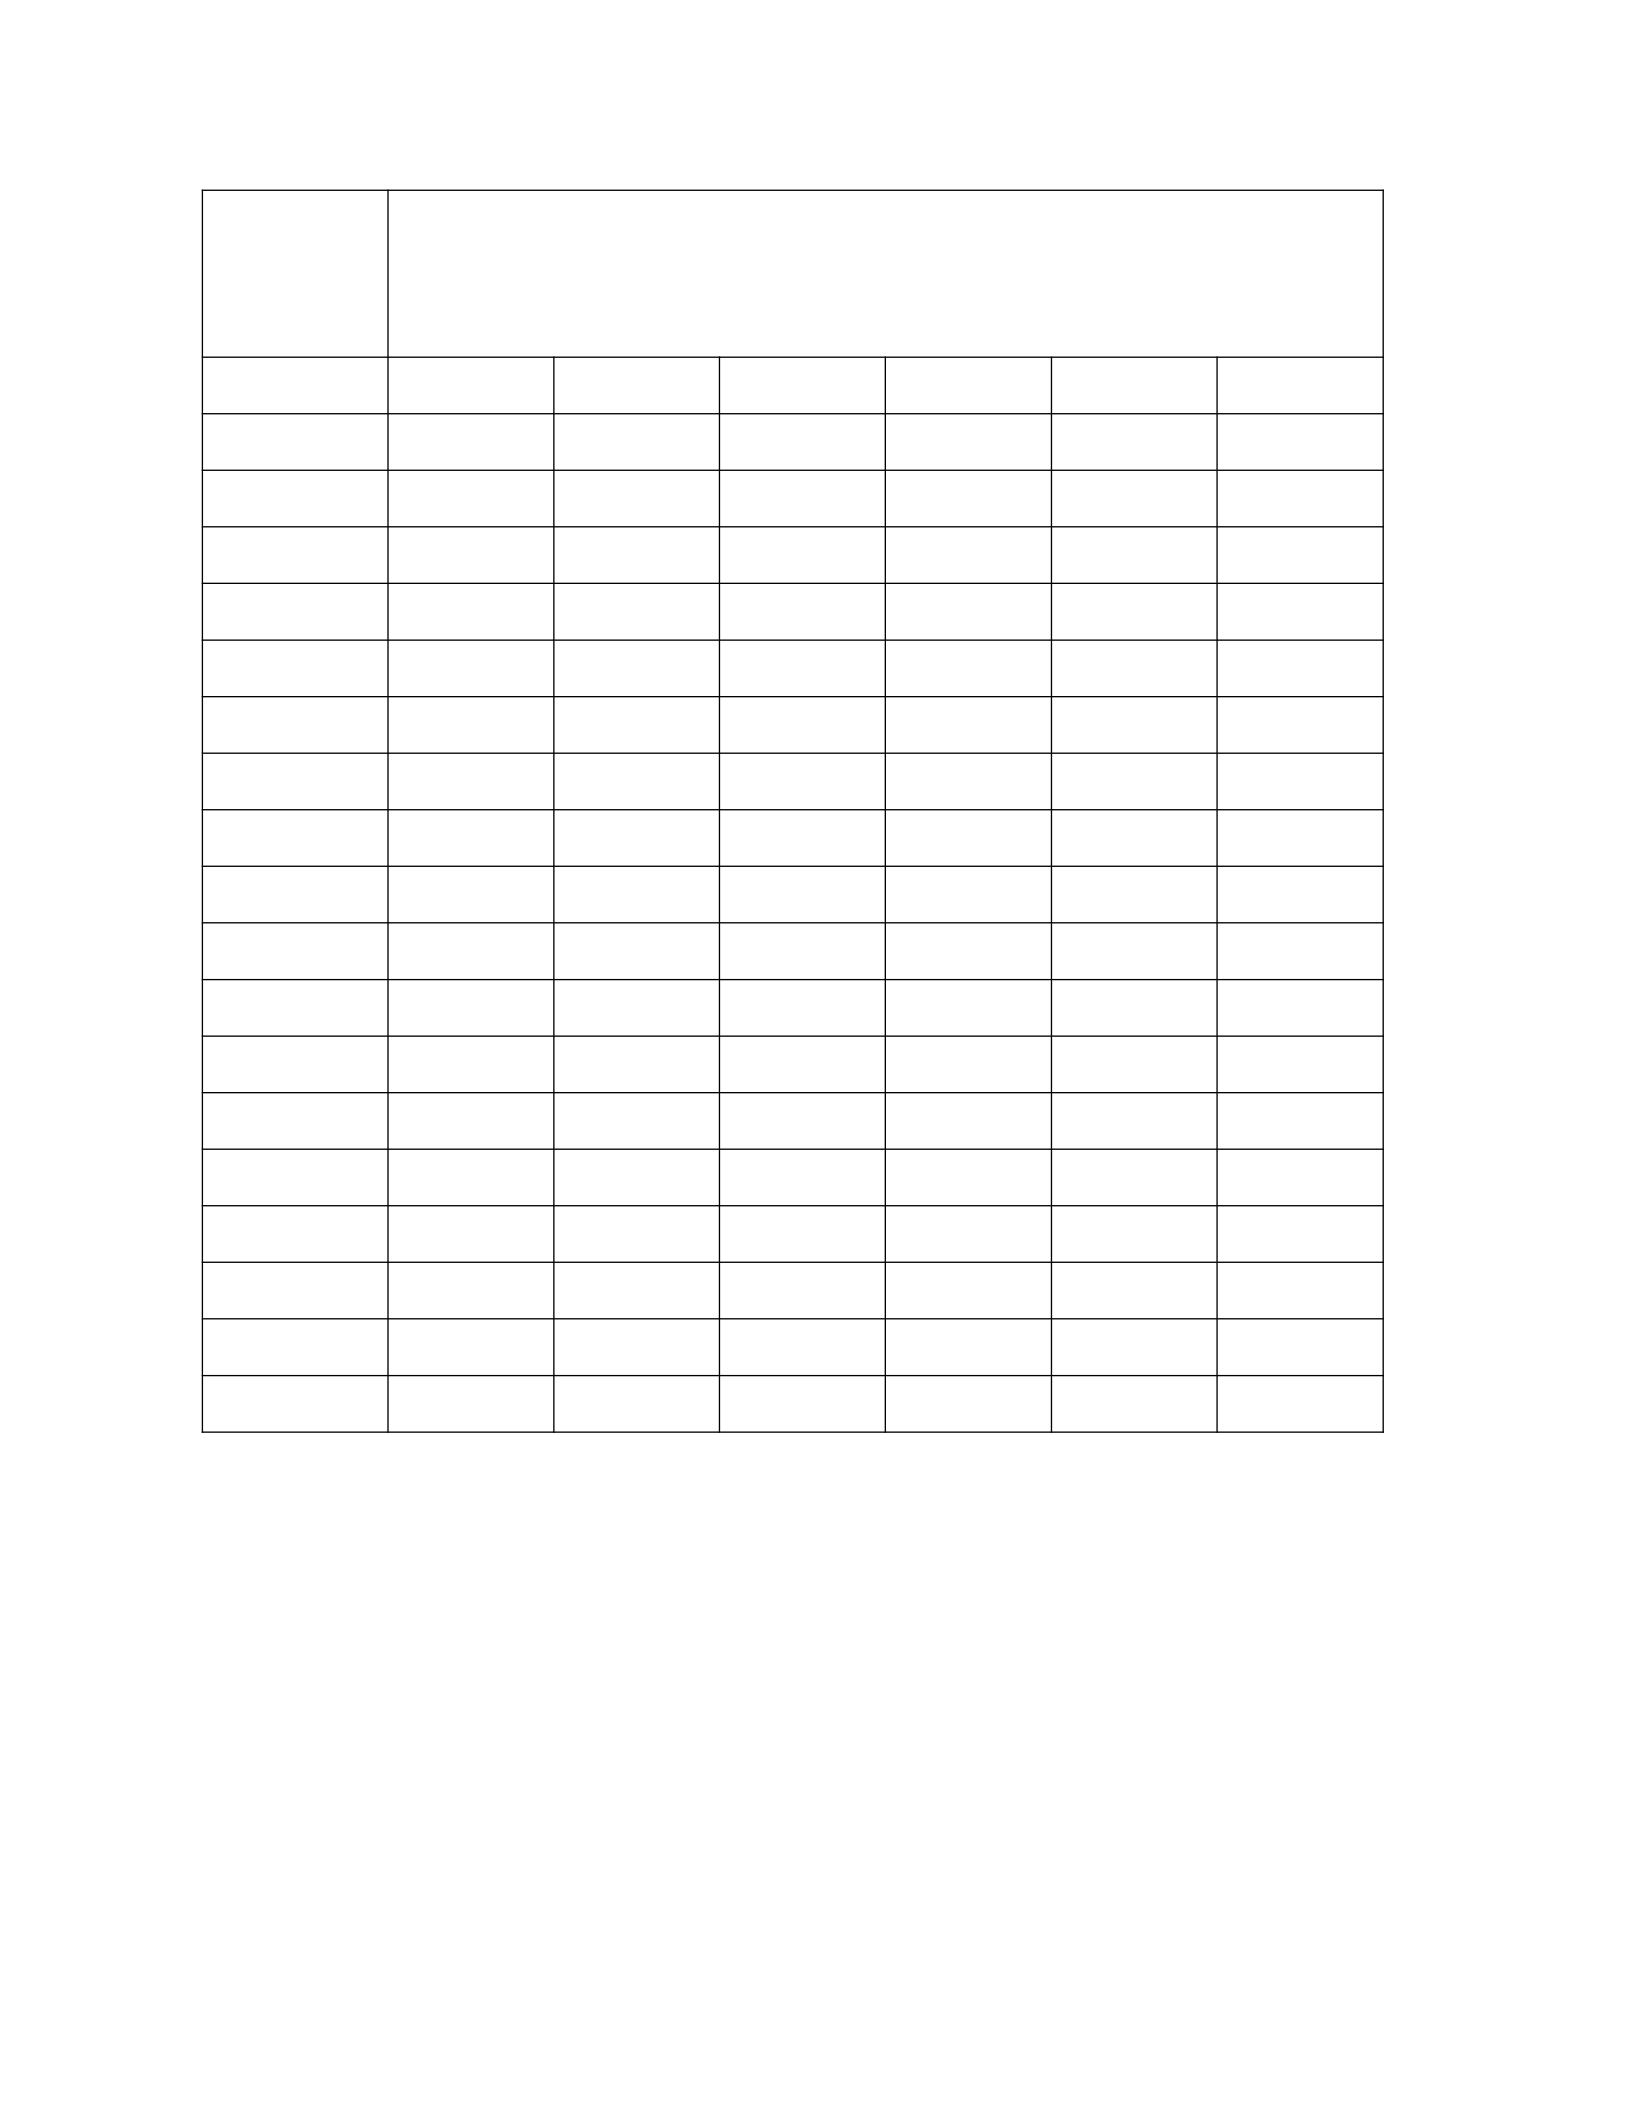
capacitance necessary for correction to the desired power factor. The number in the Table 3.2
is multiplied by the current demand (kW) to get the amount of capacitors (KVAR) needed to
correct from the existing to the desired power factor. This number can be chosen from the
Table 3.2 as follows [29]. First determine the current power factor in the first column and
then determine the new power factor in the first row. The number corresponding to that row
and column is then multiplied by the current demand. Mathematically, power factor is
expressed as
PF = kW / KVA
Figure 3.2: Components of Electrical Power [29]
Example: Consider a 480-volt 3-phase system with an assumed load and instrument readings
as follows: the ammeter indicates 200 amps and wattmeter reads 120 kW. The power factor
of the load can be expressed as follows:
34
KVA Existing
KVA Proposed
KW
Capacitor Correction
Existing
Proposed
KVAR

The apparent power for a 3-phase circuit is given by the expression
KVA = E x I x (3)1/2 / 1000
=480volts x 20amps x 1.73/1000
=290.6KVA Therefore:
PF = kW / KVA
= 120 / 290.6
= 41.2%
From the above example it is apparent that by the decreasing power drawn from the
line (KVA) the power factor can be increased.
3.3.1 Power Factor Improvement
Preventive measures involve selecting high-power-factor equipment. For example,
when considering lighting, only high-power factor ballast’s should be used for fluorescent
and high intensity discharge (HID) lighting. Power factor of so-called normal-power factor
ballasts is notoriously low, on the order of 40 to 55 percent [29].
When induction motors are being selected, the manufacturer’s motor data should be
investigated to determine the motor power factor at full load. In the past few years, some
motor manufacturers have introduced premium lines of high-efficiency, high-power-factor
motors. In some cases, the savings on power factor alone can justify the premium prices
charged for such motors. Motors should also be sized to operate as closely as possible to full
load, because power factor of an induction motor suffers severely at light loads. Power factor
decreases because the inductive component of current that provides the magnetizing force,
necessary for motor operation, remain virtually constant from no load to full load, but the
inphase current component that actually delivers work varies almost directly with motor
loading.
Corrective measures for poor power factor involve canceling the lagging current
component with current that leads the applied voltage. This cancellation can be done with
power-factor-improvement capacitors, or by using synchronous motors. Capacitors have the
effect of absorbing reactive current on a one-to-one basis, because almost all of the current
flowing through a capacitor leads the applied voltage by 90 degrees. A capacitor rated at 100
35

kilovolt-amperes capacitive (KVAC) will, therefore cancel 100 kilovolt-amperes reactive
(KVAR).
Synchronous motors provide an effective method of improving power factor because
they can be operated at leading power factor. This improvement at the load center contributes
to an improvement in overall plant power factor, thereby reducing the power factor penalty
on the plant electricity cost. For example, if a synchronous motor is used in place of an
induction motor, the power factor improves from 85% to 89%.
The Table 3.2 can be also used to determine the amount of capacitors needed to
correct a power factor. The amount of capacitors needed in KVAR can be determined from:
KVAR = D x CF
Where
D = maximum annual demand, kW
CF = correction factor
3.3.2 General Considerations for Power Factor Improvements
Power factor plays a very important role in the facility. If it is maintained at a good
value say above 0.95 then one can say that the plant is in good condition with regards to
power factor. But a lower power factor cause many problems to the plant. It not only creates
problems for the user but also the utility provider. So the utility service company often makes
it mandatory for the plant to maintain a good power factor. Poor power factor penalizes the
user in three ways.
It robs the distribution system of capacity that could be used to handle the
workperforming load.
It results in currents higher than necessary to perform a given job, thereby contributing
to higher voltage drop and electrical system losses.
It can result in electric power billing penalties depending on the schedule terms.
36
EXISTING
POWER
FACTOR
NEW POWER FACTO
R
1.00 0.95 0.90 0.85 0.80 0.75
0.66 1.138 0.810 0.654 0.519 0.388 0.256
0.68 1.078 0.750 0.594 0.459 0.328 0.196
0.70 1.020 0.692 0.536 0.400 0.270 0.138
0.72 0.964 0.635 0.480 0.344 0.214 0.082
0.74 0.909 0.580 0.425 0.289 0.159 0.027
0.76 0.855 0.526 0.371 0.235 0.105
0.78 0.802 0.474 0.318 0.183 0.052
0.80 0.750 0.421 0.266 0.130
0.82 0.698 0.369 0.214 0.078
0.84 0.646 0.317 0.162 0.026
0.86 0.593 0.265 0.109
0.88 0.540 0.211 0.055
0.90 0.484 0.156
0.92 0.426 0.097
0.94 0.363 0.034
0.96 0.292
0.98 0.203
0.99 0.142
Table 3.2: Power Factor Correction [29]
A plant’s power factor penalty can be determined from the monthly utility bills. The
method of billing for low power factor varies widely among utilities. Often no penalty is
imposed unless the power factor falls below a certain minimum, typically 85 percent to 90
percent. In other situations, a penalty is involved for any reduction below 100 percent. For
this reason, each rate schedule must be studied separately to determine the potential savings
involved for improving power factor.
37

Some equipment, such as high power factor lighting ballast’s or synchronous motors,
has inherent power factor improvement. With other equipment, notably induction motors,
power factor is a function of the mode of operation. Operation of an induction motor below
full load will significantly reduce the power factor of the motor. Therefore, motors should be
operated close to full load for the best power factor. Power factor also becomes progressively
lower for slower speed motors. For example, the decline in power factor below 90 percent for
a 1,200 RPM motor is 1.5 times greater than for a 1,800 RPM motor; for a 900 RPM motor,
the decrease is more than double that for a 1,800 RPM motor.
The use of power factor improvement capacitors is the simplest and most direct
method of power factor improvement. Capacitors can be bought in blocks and combined to
provide the required amount of capacitive reactance or individual capacitors can be installed
at each motor. Capacitors already in use should be checked annually to ensure all units are
operating. Inoperative capacitors negate the power factor improvement for which their
installation was intended. Diminishing returns are realized as power factor approaches 100
percent. Generally, 95 percent (based on normal full load) is the economic break-even point
in a power factor improvement program; up to this point, improvements usually show a good
return on investment [27].
3.3.3 Power factor at facility A
Power factor calculations at facility A are shown in the Table 3.1. The table contains
the values for kW and KVAR for all the months shown in the table. The power factor is
calculated using the formula
PF = kW / KVAR
3.3.3.1 Sample Calculation
Consider the first entry in the table. The entries in the row for the month of March are
as follows:
Demand = 323 kW
Apparent Power = 671 KVAR
Power Factor = 323 / 671
38

= 0.48
Similarly, the power factor for all other months is calculated and the average is
calculated. The average power factor is 0.59.
3.3.3.2 Anticipated savings obtained from Power factor improvement
The excess KVAR charge paid by facility A is the result of lower power factor. If the
power factor is improved considerably, this excess charge in the electric bill will reduce. The
total excess charge paid by facility A from the billing information is around $ 1,835/year.
Please refer to the Table 3.1 for the excess charge. Also refer Table 3.2 for selection the
correction factor. The correction factor is calculated by interpolation to be 0.885.
Present Average power factor = 0.59
Maximum kW demand = 361.8 kW
Required Power Factor after correction = 0.90
Additional KVAR required for correction = 0.885 X 361.8
=320.19 KVAR
3.3.3.3 Implementation and payback
Average cost of Capacitor bank required for power factor correction is $15/ KVAR.
So total implementation cost of the capacitor bank is as follows:
= 320.19 KVAR X $15
= $ 4,802.
So the simple payback obtained is as follows:
= 4,802 /1,835
= 2.6 Years.
3.4 Conclusions
The utility bill analysis was performed for all the wood manufacturing facilities in
West Virginia. The utility bill analysis for facility A along with the opportunity for power
factor improvements are discussed in detail in this chapter. The utility bill analyses of the
39

remaining plants can be referred to in Appendix I. Also the power factor recommendations
for other plants where they were cited during the assessment are presented in Appendix I.
This preliminary analysis of the utility bills for the wood manufacturing plants in West
Virginia shows that electricity charges contribute to around 85 % of the total energy charges.
Also it is seen from this analysis that, demand charge of electricity is up to 70 % of the total
electricity charges for this type of industry.
This analysis emphasizes the need for attacking the demand charges of these plants so
as to reduce the overall electricity charges and eventually the total energy charges for these
plants. Thus this chapter on utility bill analysis gives us an insight into as to what component
of the electricity charges needs to be attacked in order to obtain better results in terms of
energy conservation and reduction of total energy bill. So, the electrical demand reduction is
the topic of analysis in the next chapter, in order to explore different ways in which electrical
demand can be reduced and what will be the impact of the reduction on the total energy
charges.
Chapter 4 Electrical Demand Reduction
The analysis in the chapter 3 on the utility bills for the wood manufacturing plants
visited in West Virginia emphasizes the need for concentration of more efforts on reduction of
the total electric demand of these plants. This chapter will discuss in detail and will answer
the following questions: what exactly is this demand charge? How is this demand recorded in
the plants? What is the load factor of a plant? What are the various ways in which one can
reduce this demand? This chapter also includes a detailed sensitivity analysis on the electrical
40
demand reduction and its impact on the annual energy charges and proves its importance in a
plant wide energy assessment program.
4.1 The Demand Charge
This charge component of the electricity bill compensates the utility company for the
capital investment required to serve peak loads, even if that the peak load is only used for a
few hours per week or month. The demand is measured in kilowatts (kW) or kilovolt amperes
(KVA). These units are directly related to the amounts of energy consumed in a given time
interval of the billing period. The demand periods vary with the type of energy demand, the
high fluctuating demand has a short demand period, which can be as short as five minutes,
but generally demand periods are of 15 or 30 minutes. The period with the highest demand is
the one used for billing demand charges. Demand charges can be a significant portion of the
total electricity charges. In some cases, demand charges can amount to as much as 80% of the
total electricity charges. This is referred from [40].
4.1.1 Recording of demand
The demand mentioned above is calculated at 15-minute intervals. During each interval, a
weighted average of the demand is taken for those 15 minutes. The recording procedure is as
discussed using the following example. Suppose demand is recorded after every 15 minutes,
then the level of demand and the time interval for which it exists is measured. Suppose the
demand was 50 kW for the first four minutes of the interval followed by 75 kW for next
seven minutes, 60 kW for next two minutes and 0 kW for the last two minutes of the interval.
Then the weighted average of all recorded demand in this interval is taken and the weighted
demand for that 15-minute interval is calculated.
So weighted average = (50*4)+(75*7)+(60*2)+(0*2)
15
= 845
15
= 56.33 kW
41

So 56.33 kW is the recorded demand for the 15-minute interval. Same procedure is
used to record demand over the whole month. The highest value of these 15-minute intervals
is the value that is reflected on the monthly electricity bill from the utility. The demand
charge is then obtained by multiplying the utility demand rate obtained from the rate schedule
for that particular plant. So if the demand rate is say $ 9.5 / kW in the schedule, then this rate
is multiplied by the peak demand value which is the maximum value of the 15 minute
intervals in which demand is recorded.
4.1.2 Potential Savings
The potential savings in terms of demand reduction depend on such factors as
The plant’s profile (variations in kW demand)
Ability to shed loads
The rate schedule
Together these factors determine the relative importance of the demand charge to the
plant’s total electric bill. Controlling demand becomes more important if the schedule
includes a ratchet clause that involves payment based on the highest peak occurring in the
previous 12 months.
4.1.3 Plant load factor
The plant’s load factor should be analyzed to determine the opportunity for
improvement. Load factor improvement is synonymous with demand control. Load factor is
the ratio of the average kW load over a billing period to the peak demand. For example, if a
facility consumed 800,000 kWh during a 30-day billing period and had a peak demand of
2,000 kW, the Load factor is:
Load factor = (800,000 kWh/720hrs)/2,000 kW = 0.55 or 55 %.
A high load factor usually indicates that less opportunity exists for improvement
because the load is already relatively constant. This means that with a high load factor, the
42

variance between the lower and higher value of the peak kW demand on the load profile is
less and it is almost equal to average kW demand. As a result there is a small opportunity for
peak demand reduction and hence downsizing [27].
4.2 System Analysis
The user will obtain the lowest electric cost by operating as close to a constant load as
possible (load factor 100% in case of a 3 shift operation). The closer a plant can approach this
ideal situation, lower the monthly demand charge will be. The key to high load factor and
corresponding lower demand charge is to even out the peaks and valleys of energy
consumption. To analyze the opportunity for demand reduction, it is necessary to obtain data
on the plant’s demand profile. The demand profile is best obtained from the utility’s records
of the kW demand for each 15-30 minute interval. If no demand recording is made as a
routine part of the billing procedure, the utility will usually install an instrument temporarily
to provide the customer with this information. A plot of this data will show the extent of the
peaks and valleys and indicate the potential for limiting demand. If sharp peaks or an
unusually high demand for one shift or short period occur, the opportunity for demand
control should be investigated further. If the demand curve is relatively level, little
opportunity exists for reducing demand charges by peak shaving. In order to level out the
peaks in the demand profile, it is necessary to identify the various loads that could be reduced
during periods of high demand. The major users of electricity will provide the most likely
sources for limiting demand. Accordingly, a list of the largest users, their loads, and their
operating schedules should be prepared. The smaller loads can be ignored, as they will not be
able to affect the demand materially. An examination of this list will often suggest which
loads do contribute or are likely to peak demands. When the load pattern is not easily
determined, an energy meter can be installed at individual loads to provide a more detailed
record of load variations.
4.3 Ways to reduce demand
The plants demand charge can be reduced in various ways. These vary from
staggering startup loads to increasing local plant generation. Also oversized motors and any
other form of electrical equipment generate an opportunity for possible downsizing and hence
43

reduce the overall demand. All these measures are discussed in the following paragraphs. One
thing, which is common to all these different ways, is that each of them requires a lot of data
collection and a constant tracking of the demand parameters. These methods can be used to
reduce demand only after a thorough analysis of the situation is performed considering all
other plant operating factors and as well as other business aspects [28].
4.3.1 Stagger Startup Loads
A few utilities base their demand charge on a facility’s instantaneous peak. In this
case, short period of intense use such as a ten second start up of a motor (or start up of motors
after a power outage) can significantly affect demand. Eliminate spikes by sequencing the
startup loads of large motors so that their peak demands are staggered. Peaks in demand are
caused by a number of different factors. The two most important of these are the starting of
large motors and the starting of many motors of any size in a single 15-minute period and
sustaining their operation over a significant period. Electric motors can draw between five
and seven times their full load currents during start-ups. These current spikes will last until
the motor has reached nearly full operating speed. For fully loaded motors this is typically
between 30 seconds and two minutes.
Demand spikes from electric motors can be reduced in a number of ways. In general it
is suggested that the starting of small motors be staggered and that of large motors be
electronically controlled. Some startup problems have a hardware solution such as the
placement of sequencers on air conditioning system will prevent more than one air
conditioner from coming on at once. The sequencer will cycle through the units allowing 15
minutes for each unit to cool its respective area. Slow, or soft, start devices will control spikes
in demand by limiting the amount of current that a large motor can draw. They will slowly
increase, or ramp, the current to its operating level. Another problem with high inrush
currents is the voltage imbalance created at the start up. When all the motors are started at
one instant, the voltage across all the other equipment in the plant goes down momentarily
and this might have a very adverse effect on the some equipment, which is sensitive to
voltage imbalance. Proper provision and safety devices must be installed to tackle this
problem of high inrush currents when all the motors are started at same time.
44

4.3.2 Reschedule Loads
Most of the utility companies offer different electricity rates during the daytime and
the night shifts. Also the weekend rates are lower than the normal weekdays in many cases.
So here lies an opportunity for the plant to reschedule some of its loads during these off peak
periods. All the high power equipment can be rescheduled to work in the night shift or in the
weekends, if it doesn’t hamper the process in any form during the normal working hours.
Such a rescheduling of high power equipment will significantly reduce the peak load during
the daytime. Some of the problems with demand can be solved through procedural changes
rather than the installation of hardware. Peak demands are usually established at particular
times during the day shift. A review of the operating schedule may show individual loads can
be rescheduled to other items or shifts to even out the demand. This technique can provide
significant gains at little or no cost. For example, operation of an electric oven might be
rescheduled to the evening shift or on weekends, if the oven is not needed full time. Another
example is conducting routine testing of the fire pump periods when the peak demands are
not likely to occur.
The determination of when a demand spike occurs is typically a difficult job. It is suggested
that a demand meter be installed. This would enable plant personnel to examine the demand.
A determination of when peak demand occurs could then be made. Once the time of peak
demand is found, it is usually easy to determine what is causing it and what must be changed
to reduce it. We can get this information on the peak demand from the utility service
company.
4.3.3 Increase Local plant Generation
When the plant generates some electricity, plant generation can be temporarily
increased to limit demand. In some cases, any venting of excess low-pressure steam from the
turbo generator for short periods may represent a lesser penalty than the increased demand
charge. Plant generation is a good solution for supplying power to those rare times when we
have the peaks in demand. Power generation at the plant site can be done by using some
onsite waste as the fuel for burning and producing the steam to run the turbine. Also portable
onsite power generators are available these days. With an on site generation possible, the
company can reduce their electric demand on the utility service. As a result, considerable cost
45

savings can be achieved which often justify the big investment in cogeneration. In the wood
industry the sawdust, which is obtained as waste from almost every stage of the process, can
be used as a fuel for a boiler, which can generate steam to run a turbine.
4.4 Motors and demand
Motors represent the largest single use of electricity in most plants. The function of an
electric motor is to convert electrical energy into mechanical energy. In a typical three phase
AC motor, current passes through the motor windings and creates a rotating magnetic field.
The magnetic field in turn causes the motor shaft to turn. Motors are designed to perform this
function efficiently; the opportunity for savings with the motors rests primarily in their
selection and use [27].
4.4.1 Idle Running
The most direct power savings can be obtained by shutting off idling motors, thereby
eliminating no-load losses. While the approach is simple, in practice it calls for constant
supervision or automatic control. Often no load power consumption is considered
unimportant. However, the idle no load current is frequently about the same as the full load
current.
4.4.2 Efficiency at Low Load
When a motor has a greater rating than the unit it is driving requires, the motor
operates at only partial load. In this state, the efficiency of the motor is reduced. The use of
oversized motors is fairly common because of the following conditions: [27]
Personnel may not know the actual load; and to be conservative, select a motor larger
than necessary.
The designer or supplier wants to ensure his unit will have ample power, therefore, he
suggests a driver that is substantially larger than the real requirements. The maximum
load is rarely developed in real service. Furthermore, most integral horsepower
46

motors can be safely operated above the full load rating for short periods. (This
problem may be magnified if there are several intermediaries).
When a replacement is needed and a motor with correct rating is not available, personnel
install the next larger motor. Rather than replace the motor when one with the correct
rating becomes available, the oversized unit continues in use.
A larger motor is selected for some unexpected increase in driven equipment load has
not materialized.
Process requirements have been reduced.
For some loads, the starting or breakaway torque is substantially greater than the running
torque; thus, over sizing of the motor is a frequent consequence, with penalties in the
running operation.
Motor is “De-rated due to poor operating conditions”: If a motor is used under extreme
duty conditions, such as high altitude or poor power quality, over sizing the motor
allows it to operate cooler and thus more reliably. However, there may be other, more
efficient strategies to maintain reliability, such as improving power quality or
providing better cooling.
Variable Loads: Motors should be sized to accommodate the greatest expected load. If a
motor is sized for a peak that seldom or never occurs, it may operate inefficiently
most of the time. Pumps and fans that operate with load factors less than 80 % are
good candidates for adjustable speed drives or other speed control strategy to improve
efficiency.
Plant personnel should be sure that none of the above procedures are contributing to
the use of oversized motors and resulting in inefficient operation. Replacement of under
loaded motors with smaller motors will allow a fully loaded smaller motor to operate at
47
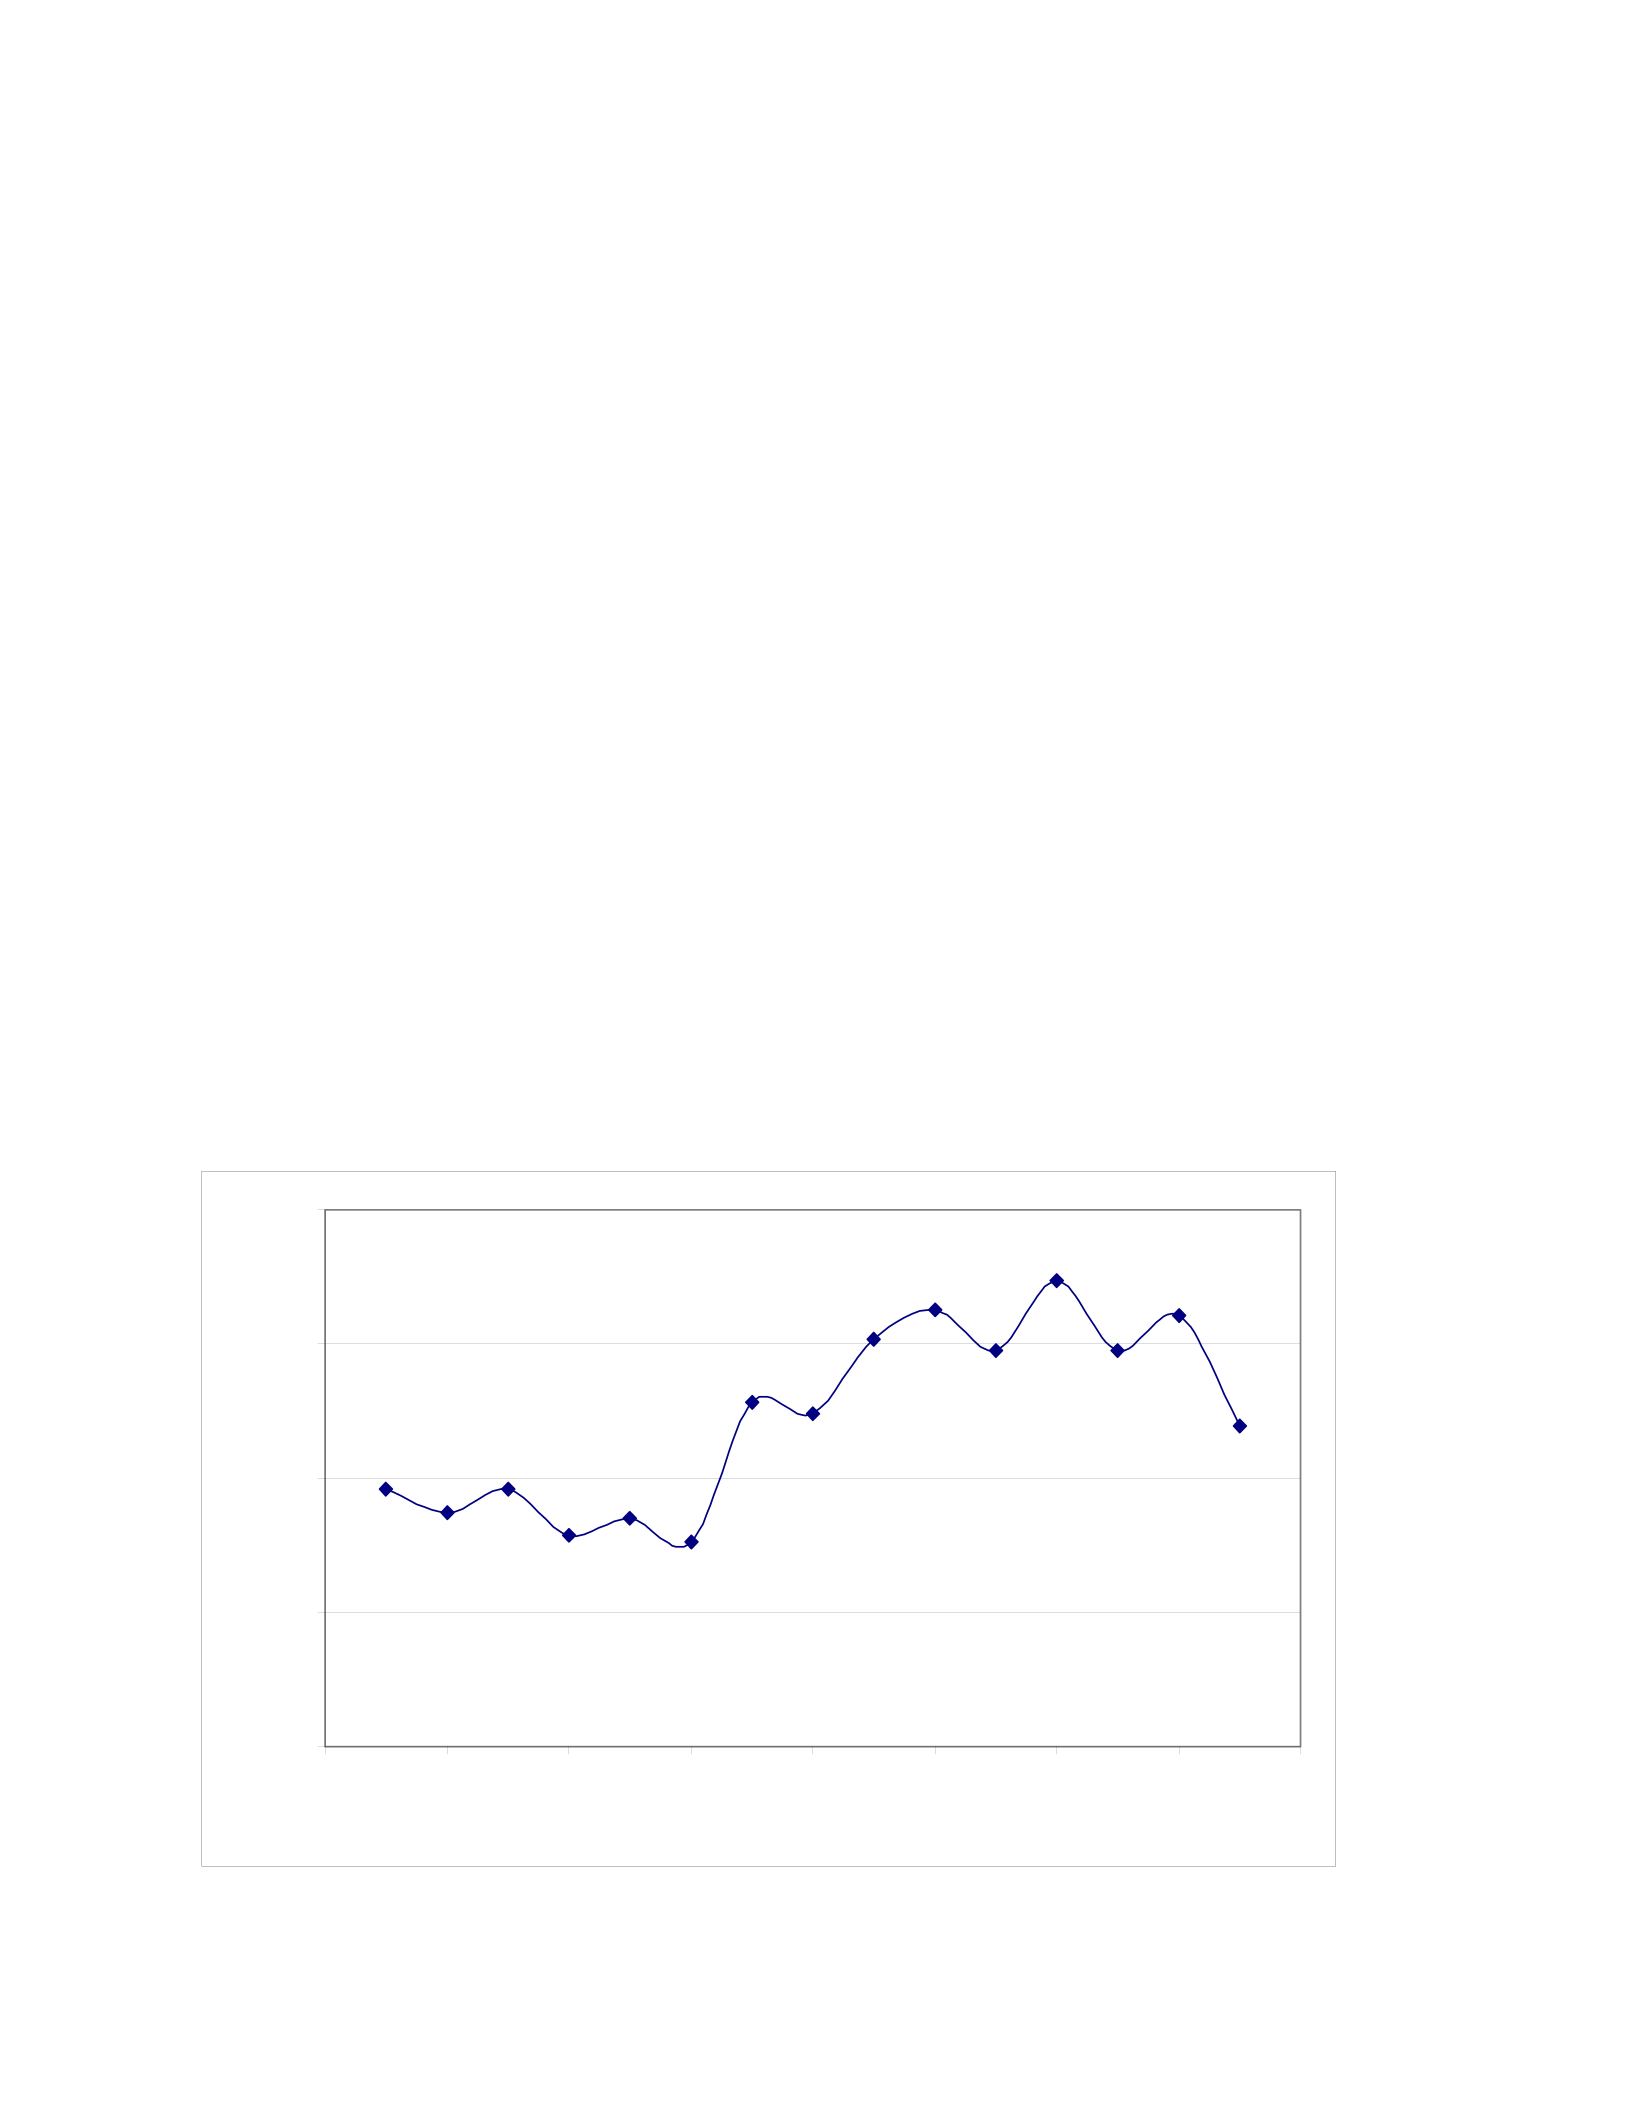
higher efficiency. This arrangement is generally most economical for larger motors, and only
when they are operating at less than 50 % capacity, depending on their size.
4.5 Load profile of the plant
A load profile of the plant is plotted for every plant visited. The peak kW demand for
the plant is plotted for all the months available and a load profile of the connected load
obtained. This is a very important plot with respect to the amount of load variation, and the
opportunities for reduction of demand charges at the plant. The demand data in kW is
obtained from the plants utility service provider. As discussed earlier the load profile for
facility A is discussed here. The plots for the other plants visited can be found in Appendix II.
Please refer Table 3.1 for the data starting from Mar 2000 to May 2001. Also the Figure 4.1
shows the plot of the plant demand in kW against the months of the year 2000-2001. As seen
in the plot, the load curve appears to be non homogeneous. There is a lot of variation on the
load on the plant and doesn’t appear to be stable at all. This is an indication of good potential
for demand reduction in the plant. The average demand on the curve is 336 kW, the upper
limit is 362 kW and the lower limit is 313 kW. Thus there is an opportunity for demand
reduction and leveling the load profile.
48
275
300
325
350
375
0 2 4 6 8 10 12 14 1
Months ( Starting March '00)
KW
6

Figure 4.1: Load profile of facility A
4.5.1 Recommendation Action
As discussed above, we can estimate a reduction of 10% of the existing demand at facility A.
Estimated savings in the total electricity charges are $3,165 per year as can be seen in the
calculations in Table 4.0. This reduction in the existing demand can be achieved by the
following actions :
Downsize the under loaded motors
Reschedule the loads
Onsite power generation
The downsizing of under-loaded motors is very crucial in implementation of the
recommendation. The motor load test should be done to figure out the existing load pattern
on the motor. This test should be done over a shift or longer time period so that the exact load
conditions imposed by the process on the motor can be examined. After identifying the
under-loaded motors, replacing them with a properly sized motor at the next available
opportunity is essential in bringing down the demand. The opportunity for replacement with
an under sized motor appears when the present motor fails or is sent for rewinding. This is the
time when a close look at the load requirements of the process and proper sizing of the
equipment should be looked into. The oversized motors can be identified by a series of
electrical tests, which are also called load tests. Rescheduling of loads and onsite power
generation are also available alternatives, which can be considered here for reducing the
demand on the plant. But motor downsizing is the most attractive, as motors constitute about
80% of the total demand on the plant.
4.5.2 Implementation Cost
The implementation cost for the above recommendation depends on the strategy
adopted to reduce the demand. If the company decides to downsize all their under loaded
motors, then it accounts for a big investment. But proper sizing of motors and other electrical
load will definitely result in lower energy costs. The stagger start up loads or reschedule loads
49

doesn’t require a big investment in machines, but it requires a lot of planning and decision
making on part of the management. So the cost associated is with the labor cost spent in
planning. The increase local plant generation strategy again calls for a huge investment of
time and money, but the results or the savings obtained from this investment are also huge,
i.e. if the company decides to go for onsite generation, then the reduction in demand might
also be 20%, which corresponds to a annual saving of $6,340. So the selection of strategy and
implementation is the decision of the management. The total savings achieved will also vary
accordingly. So a sensitivity analysis of the demand reduction is done and discussed in the
next section, which gives us an insight into the level of savings obtained because of demand
reduction.
4.6 Sensitivity Analysis for Demand Reduction
A sensitivity analysis for the reduction of kW demand is performed so as to have a
better understanding of the demand cost reduction in the plant. This analysis is performed for
the overall plant. The peak demand for every month appears on the utility electricity bill. If
this peak demand would be reduced, what would be the effect on the total electricity charges
each year? The answer to this question is obtained from this analysis. The range for reduction
in peak demand for a plant is considered from 0 % reduction to 20 % reduction in the peak
demand from the current demand. The demand sensitivity analysis performed for facility A
can be seen in the Table 4.1. The table shows the annual cost savings obtained for facility A
for different levels of reduction in demand. Also the percentage change in the total electricity
charge over the current annual charge is calculated. The results obtained from the table are
also plotted and can be seen in the Figure 4.2. The slope of the line in the plot is calculated.
This slope corresponds to the cost savings in annual total electricity charges for one percent
reduction in demand. It is seen that for every one percent reduction in kW demand for facility
A, the total electricity charge will come down by approximately $ 317 /year. Thus the control
over the demand of the plant will play a crucial role in the energy efficiency program
undertaken by the management.
Every plant has its own specific utility structure, so the utility rate structure for each
plant was studied differently for identifying the impact of demand reduction on the overall
electricity charge of the company. Some plants had the demand charge as a separate charge in
50

the rate structure, while in others this charge was hidden in the other components of the
structure. Similar demand analysis was performed on all the other wood manufacturing plants
visited in West Virginia and the analysis tables and the plots and comments for each plant can
be found in Appendix II.
51
Present kW Demand 5 % Red in kW Demand 10 % Red in kW Demand 15 % Red in kW Demand 20 % Red in kW Demand
Demand
Total
Charge Demand
Total
Charge Demand
Total
Charge Demand
Total
Charge Demand
Total
Charge
( kW ) ( $ ) ( kW ) ( $ ) ( kW ) ( $ ) ( kW ) ( $ ) ( kW ) ( $ )
71 2,437 68 2,437 64 2,437 61 2,437 57 2,437
260 3,679 247 3,559 234 3,439 221 3,319 208 3,199
323 4,924 307 4,775 291 4,626 274 4,477 258 4,328
319 5,366 303 5,219 287 5,072 271 4,925 255 4,778
323 5,191 307 5,043 291 4,894 274 4,745 258 4,596
314 4,825 299 4,678 283 4,532 267 4,386 251 4,239
318 5,225 302 5,077 286 4,930 270 4,782 254 4,634
313 5,018 298 4,873 282 4,727 266 4,581 251 4,435
313 5,018 298 4,874 282 4,728 266 4,582 251 4,436
313 5,018 298 4,875 282 4,729 266 4,583 251 4,437
313 5,018 298 4,876 282 4,730 266 4,584 251 4,438
313 5,018 298 4,877 282 4,731 266 4,585 251 4,439
56,738 55,160 53,573 51,985 50,397
Savings Obtained
Over Present
Demand
( $ per Year )
0
1,578
3,165
4,753
6,341
% Change in total
Charge over
Present
0.00
-2.78
-5.58
-8.38
-11.18

Table 4.1: Demand sensitivity analysis for facility A
50
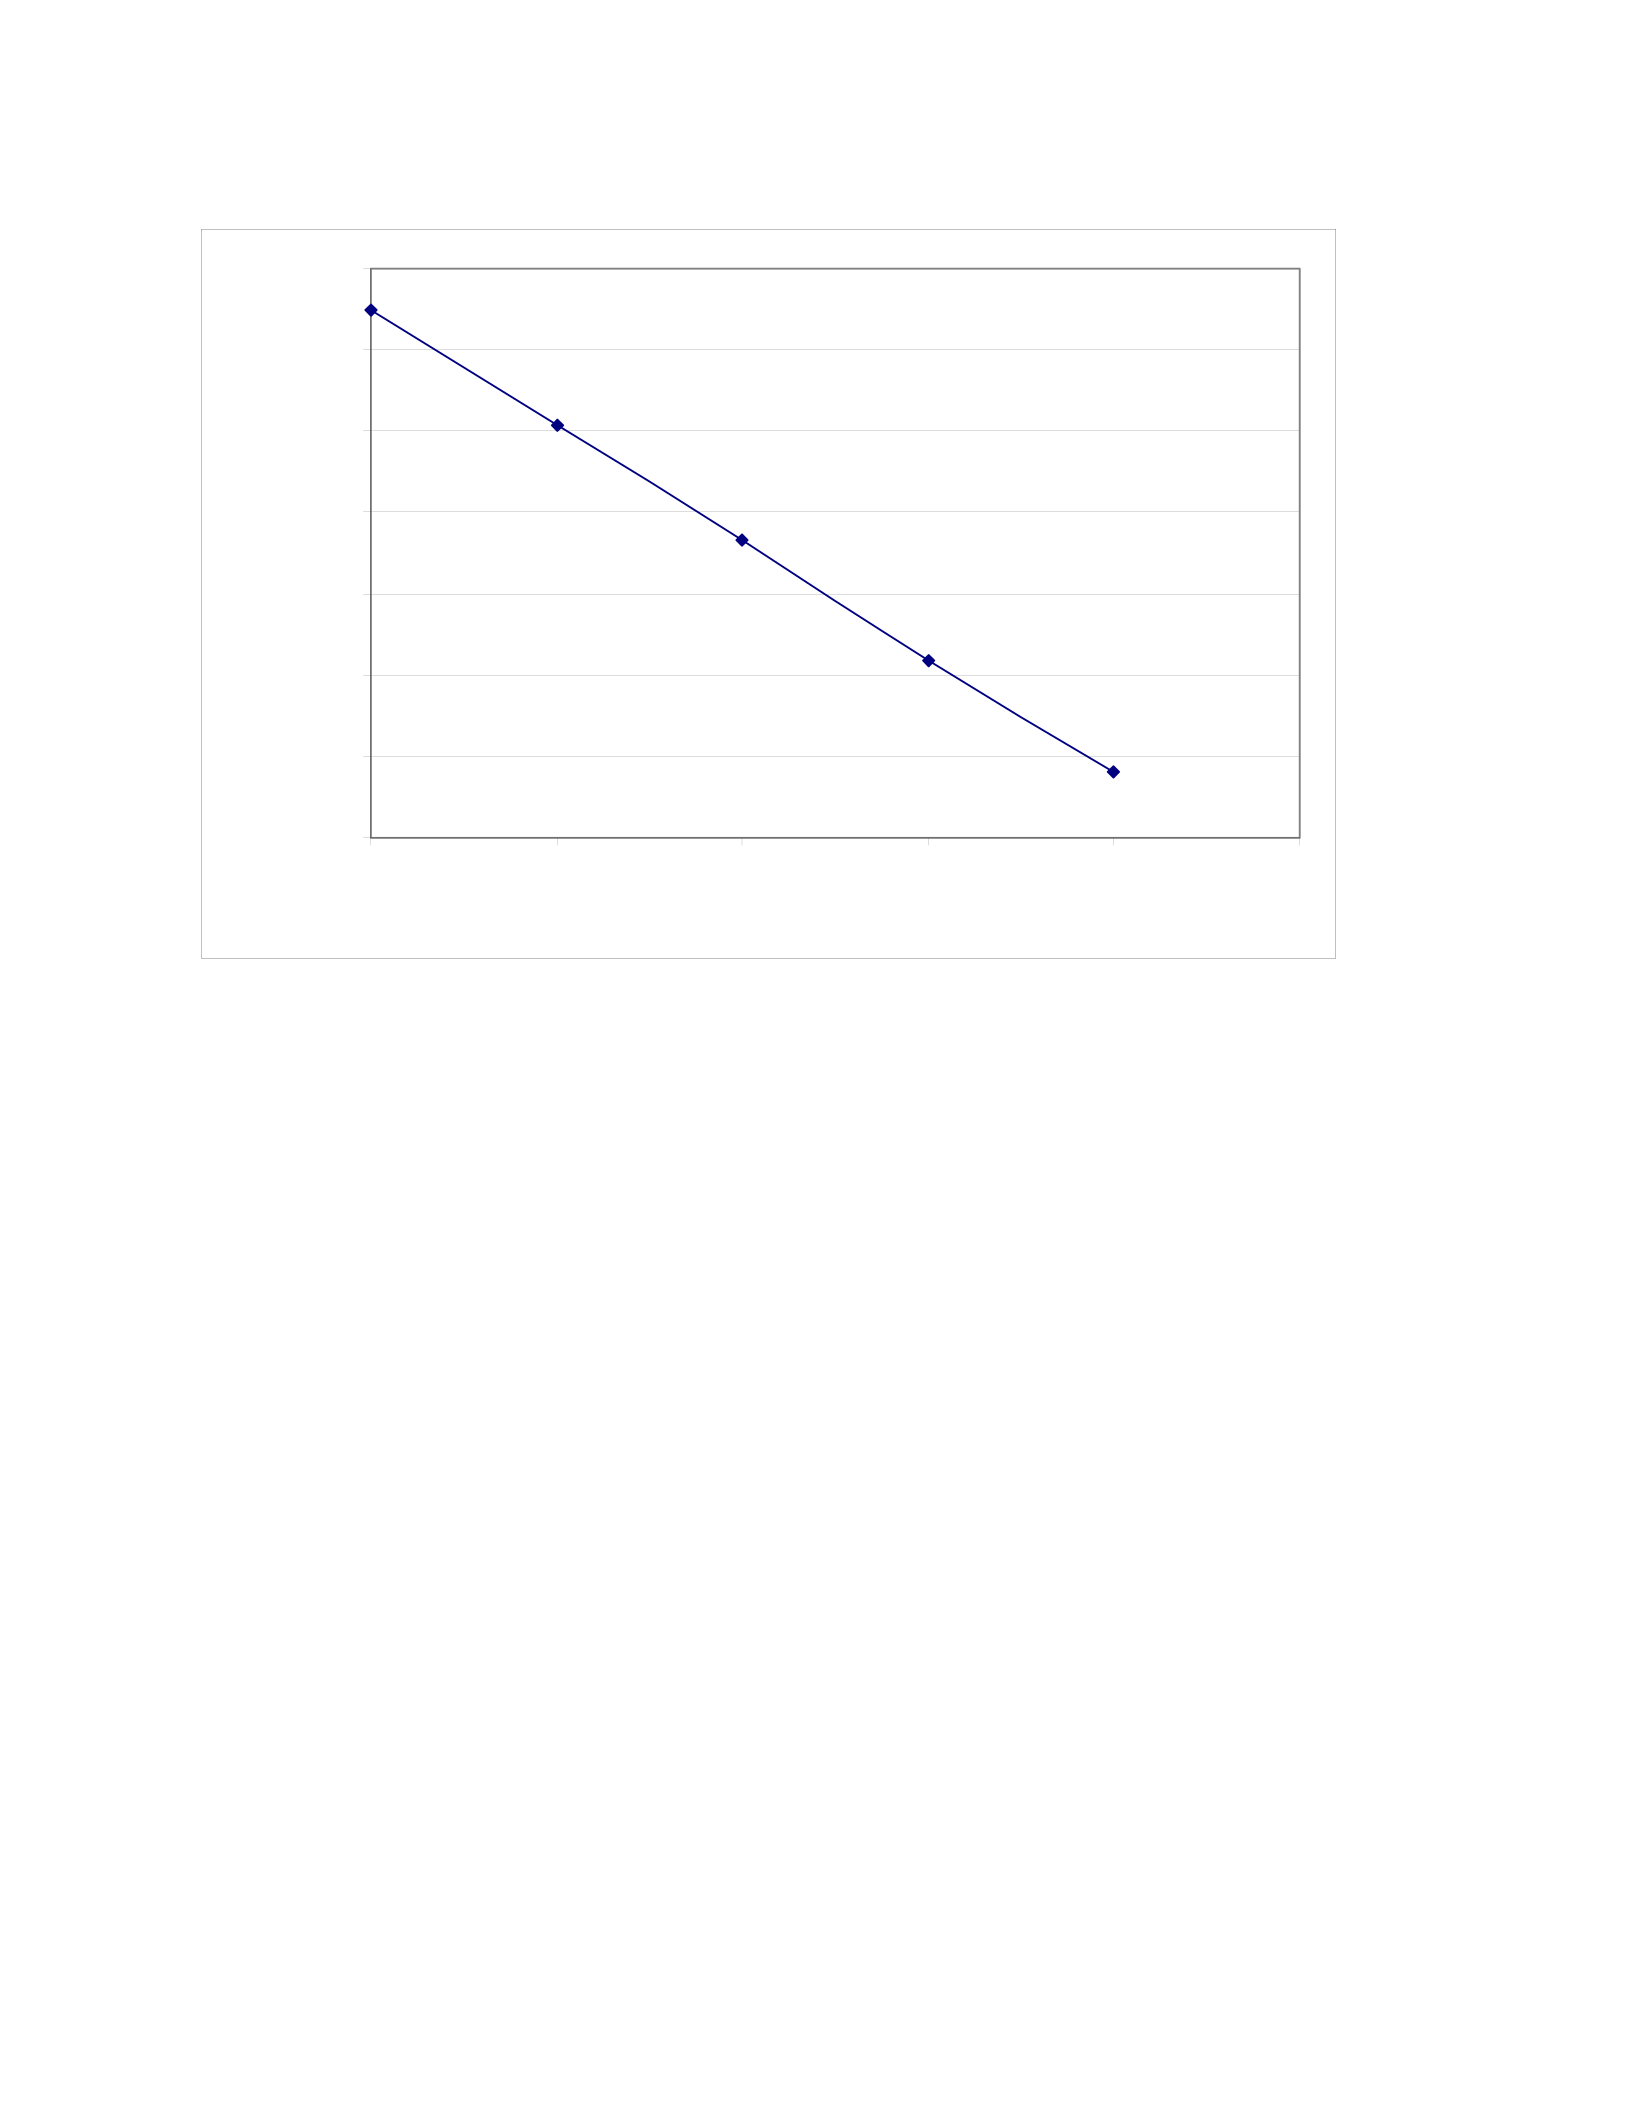
Figure 4.2: Plot for demand sensitivity analysis for facility A
4.7 Conclusions
This chapter discussed the various opportunities for reducing demand in the plant.
Reduction in demand does have a very significant impact on annual energy bill for these
plants. The sensitivity analysis on the demand reduction gives an insight into the magnitude
of cost savings, which can be obtained for different levels of reduction in demand over the
present peak demand. Also discussed in this chapter are the various possible ways in which
demand can be reduced. One of these ways is downsizing motors. As the wood
manufacturing industry is highly motor intensive, downsizing motors to appropriate sizes will
contribute significantly to the overall reduction on peak demand of the plant. But to identify
these motors for downsizing, a motor load test needs to be performed. This motor load test is
described in the next chapter in detail, along with the potential of downsizing oversized
motors to their appropriate size.
54
104,000
105,000
106,000
107,000
108,000
109,000
110,000
111,000
0 5 10 15 20 25
% Reduction in KW
Total Electric Charge ($)

Chapter 5 Motor Load Test
Reduction in overall plant demand can give significant reduction in annual energy bill. Also
the wood manufacturing industry is highly motor intensive. The preliminary results from the
utility bill analysis and the load curves for the plant show that there is some potential for
reduction in demand. Oversized motors in the plants can be downsized to the required
appropriate size so as to reduce the energy as well as the demand charges of the plant. This
chapter emphasizes the need for downsizing motors and also discusses the type of motor load
test used during assessments and the results obtained therewith.
5.1 Reasons to determine motor loading
Most electric motors are designed to run at 50% to 100% of rated load. Maximum
efficiency is usually near 75% of rated load. Thus, a 10 hp motor has an acceptable load
range of 5 to 10 hp, with the peak efficiency at 7.5 hp. A motor’s efficiency tends to decrease
dramatically below about 50% load. A motor is considered under loaded when it is in the
range where efficiency drops significantly with the decreasing load. With decreasing load on
the motor, the power factor also drops down drastically. The power factor tends to drop off
sooner, but less steeply than efficiency, as load decreases. Over loaded motors can overheat
and lose efficiency. Many motors are designed with a service factor that allows occasional
overloading. Service factor is a multiplier that indicates how much a motor can be overloaded
under ideal ambient conditions. Although many motors have service factors of 1.15, running
the motor continuously above rated load reduces efficiency and motor life. Determining if
your motors are properly loaded enables you to make informed decisions about when to
replace motors and which replacements to choose. Measuring motor loads is relative quick
and easy when the proper techniques are used [27].
It is recommended that a survey and test of all the motors operating over 1000 hours
per year should be made. Using the analysis results, the motors can be divided into following
categories:
Motors that are significantly oversized and under loaded – replace with more efficient,
properly sized models at the next opportunity, such as scheduled plant down time.
55
Motors that are moderately oversized and under loaded – replace with more efficient,
properly sized models, when they fail.
Motors that are properly sized and but standard efficiency – replace most of these with
energy efficient models when they fail.
5.1.1 Motor downsizing example
An example [27] will be valuable in appreciating the concept of downsizing motors.
As can be seen in the Table 5.1, an analysis of downsizing a lightly loaded, existing 75 hp
motor is shown. A careful check of the motor load by the electrician reveals that the
maximum (peak) load encountered is 30 hp. The peak load is short in duration (one hour per
day). The potential replacement motor (40 hp, energy efficient) is forecast to operate at 75%
load.
No Description Existing motor
75 hp
Replacement
motor
40 hp
Units
1 Load imposed on motor 40.0% 75.0% %
2 Average volts 476.0 476.0 Volts
3 Average current I 44.2 33.9 Amps
4 Power factor - pf at load point 69.9% 85.0% %
5 Input power – Pin 25.5 23.8 kW
6 Motor efficiency – at load point 87.9% 94.1% %
7 Output power – Pout 22.4 22.4 kW
8 Motor losses (Pin-Pout) 3.1 1.4 kW
9 Power savings 0 1.7 kW
Table 5.1: Motor downsizing example [27]
The values of efficiency and power factor have been selected to reflect the load. Also
it can be seen from this example that there was a net saving of 1.7 kW of demand because of
downsizing. An additional energy saving is obtained which can also be substantial of the
operating hours for this particular motor are above 1,000 hours. Thus the total savings
56

obtained might justify the investment of replacing the present motor with an energy efficient
undersized motor.
5.1.2 Two speed Motors
Two-speed motors are another option to downsizing in case of applications like
chipper motor in wood manufacturing plants, where the motor runs at no load for some time
and only when there is a load or wood particle, the motor is highly loaded. The two-speed
motor can be used along with a sensor unit, which senses the wood coming on the belt
towards the chipper motor. When the sensor detects something on the belt, the motor can be
switched to a higher power mode and the operation conducted successfully.
The above concept can be explained with an example. Assume that a facility has a
chipper motor of 150 hp, which operates continuously. From the assessment experience, it is
seen that this chipper not operating at full load much of the time. So, this chipper motor can
be replaced with a 2-speed motor. By using a 2-speed motor, the chipper will run at 150 hp
when actually chipping operation takes place, and at say 50hp when idling (no chipping
operation performed). This will result in energy savings, as the chipper does not operate at
150 hp at all times. From audit experience, it is estimated that the chipper is idle for 30% of
the time. The energy cost savings are calculated as follows:
ES = CEU - PEU
The current and proposed energy usage values can be estimated as follows:
CEU = hp1 x H x LF1 x C / EFF1 (for 150hp operation)
PEU = hp1 x 0.70H x LF1 x C / EFF1 + (for 150hp operation)
hp2 x 0.30H x LF2 x C / EFF2 (for 50hp operation)
Where
CEU = Annual energy consumption under current conditions.
PEU = Annual energy consumption under proposed conditions.
1 corresponds to 150hp , 2 corresponds to 50hp
hp = Motor horse power
H = annual operating hours
LF = load factor, no units
57

C = conversion factor, 2545 Btu
EFF
= estimated motor efficiency, no units
CEU = 150 x 8736 x .85 x 2545 / .90
PEU = 150 x .70 x 8736 x .85 x 2545 / .95 + 50 x .30 x 8736 x .85 x 2545 / .95
ES = CEU - PEU
ES = 762 MMBtu
Assuming $/Mmbtu is $6.47/MMBtu and the demand cost is $7.34/kW, annual Electricity Cost
Savings, CS, are estimated as:
CS = ES x (average unit cost of electricity)
CS = (762 MMBtu/yr)($6.47/MMBtu)
CS = $4,930/yr
Annual Demand Savings DS can be estimated as:
DS = (MMBtu/y) x 106Btu/MMBtu x 12month/y ÷(YOH x 3412 Btu/kWh)
= (1256 x 106 x 12) ÷ (8736 x 3412)
= 465 kW-mo
Annual Demand Cost Savings, DCS, are estimated as:
DCS = DS x Demand Rate $/kW-mo
DCS = 465 kW-mo x 7.34 $/kW-mo
DCS = $3413/yr
Total Annual Cost Savings = CS + DCS
= 4,930 + 3,413
= $8,343/yr
58

The total cost to replace 150hp single speed motor with 150hp two speed / variable speed
motor and corresponding control can be estimated:
New Variable Speed Motor & Controls = $9,000
Labor Cost = $90
Labor Rate = $18/hr
Labor Time = 5hr
Total implementation cost = $9,090
The cost savings of $8,343/yr pay for the implementation cost of $9,090 in about 14 months.
If the same analysis is performed for downsizing the same chipper motor to a lower
size motor of say 100 hp, the resulting savings for the same usage and demand rates as
obtained from Motor Master + software are as follows:
Total energy savings = $ 735/yr Total
Implementation cost = $ 4,779
Payback period = 6.5 years.
5.1.3 Comparison between downsizing and two-speed motor option
As can be seen in the above example, it is really necessary to perform a load factor test on
the motor to take a wise decision on whether to downsize motors like chipper or to replace
them with a two speed- motor and control unit. The two-speed motors option may not be
applicable in each and every operation in the wood industry. Some processes where the load
is pretty constant and low, then downsizing would be a wise option to consider. The two-
speed option should be carefully evaluated for the different load conditions on the motor and
also a load profile of the motor would be of advantage to find the percentage of time, the
motor is idle and motor is running at full load.
5.2 Determining motor load factor
It is important to determine the load factor of the motors in order to ensure that the
motor is properly sized for the application and to identify potential problems. Field tests are
performed in order to determine the load of the motors in wood manufacturing plants. There
are two types of motor load testing techniques used in the field. They are the electrical
method of load testing (Use of line current measurements) and the slip method.
59
5.2.1 Use of line current measurements
The amperage draw of a motor varies approximately linearly with respect to load
down to about 50% of full load. Below the 50% load point, due to reactive magnetizing
current requirements, power factor degrades, and the amperage curve becomes increasingly
non-linear and is no longer a useful indicator of load. The no load or idle amperage for most
motors is typically on the order of 25 to 40 percent of the nameplate full load current while
the power draw or no load loss is only 4 to 8 % of the name plate horsepower.
Advantages of using the current based load estimation technique are that NEMA MG
1-12.47 allows a tolerance of only 10% when reporting nameplate full load current. In
addition, motor terminal voltages only affect current to the first power, while slip varies with
the square of the voltage. Finally, a motor’s current draw is not directly related to operating
temperature. The equation that related motor load to measured current values is [28]:
Motor load = Amps measured X Volts measured
Amps full load, nameplate X Volts nameplate
5.2.2 The Slip method
The synchronous speed of an induction motor depends on the frequency of the power
supply and on the number of poles for which the motor is wound. The higher the frequency,
the faster a motor runs. The more poles the motor has, the slower it runs. The synchronous
speed (Ns) for a squirrel cage induction motor is given by [27,28]:
Ns = 120 X f
P
Where:
f = frequency of the power supply
p = poles for which the motor is wound
The actual speed of the motor is less than its synchronous speed with the difference between
the synchronous and actual speed referred as slip. The amount of slip present is proportional
60
to the load imposed upon the motor by the driven equipment. Slip is typically expressed as a
percentage where:
Percent slip = (synchronous speed – actual speed) x 100
synchronous speed
The motor load can be estimated with slip measurement as follows:
Slip = RPM sync – RPM measured
Motor load = Slip
RPM sync – RPM full load (nameplate)
For example:
Given : RPM sync = 1,800 RPM measured = 1,770
RPM nameplate = 1,750 Nameplate hp = 25
Then: Slip = 1,800 – 1,770
= 30
Motor load = 30
1,800 –1,750
= 30/50
= 0.6
The speed / slip technique for determining motor load has been favored due to its simplicity
and safety advantages. The two most easily measured motor operating parameters are
temperature and speed. Most motors are constructed such that the shaft is accessible to a
tachometer or a strobe light.
5.3 Field testing
This slip method of load testing was used for testing the load of the motors in the
wood manufacturing facilities visited in West Virginia. The information on the motor input
data was obtained during the assessment and a motor load test was performed using a digital
61
stroboscope. This method is very simple and fairly accurate in an industry like wood
manufacturing. The electrical method is very time consuming and is risky in the sense that
you need to work with the currents and voltages directly. While in the slip method the field
test can be performed standing at some safe distance away from the running motor. Also the
operation need not be stopped or there is no modification in the set up required to perform
this test. Thus it is completely hassle free and doesn’t interfere with the working of the plant
equipment.
Advantage of using a digital stroboscope is that one doesn’t require a reflective tape
to be put on the motor shaft and then measure the rpm. The digital stroboscope flashes in
unison with the monitored object, and the speed of the object or the motor shaft is equal to
the flash rate. The schematic of the motor load test set up can be seen in the Figure 5.1 below.
The figure shows the variable frequency source, which is the supply for the unit. A battery
pack can also be used to provide the AC supply to the stroboscope. The frequency scalar is
used to change the frequency of the flashlight so as to meet the rpm pf the motor shaft. There
is also a digital display, which shows the flashes per minute. The flashing unit produces the
flashlight through a Xenon flasher, which is directly incident on the rotating shaft of the
motor. When the rotating shaft of the motor appears stationary to the eyes of the user, than
the flash per minute equals the rpm of the motor.
Figure 5.1: Schematic diagram for the motor load test
62
Variable
Frequency
Source
– Digit 4
Speed
Display
Flashing
Unit
Frequency
Scalar
Rotating Shaft
Xenon
Flasher
5.4 Example of the field test
The motor load test was performed in various plants during the assessments. During the test,
care was taken that the load test was performed when the motor was aptly loaded. The motor
load test data of on one of the chipper motors encountered during the assessment can be seen
in the Table 5.1. It is seen that the synchronous speed of the motor, the full load rpm of the
motor and the other details of the motor are noted from the motor nameplate data. The
operating speed of the motor is determined using a digital stroboscope.
Company Facility G Location Spencer, WV
Date 04/18/2002 Process Chipper
Motor Name Plate Data
Manufacturer Lincoln Motors Synchronous
speed
1800 rpm
Full load speed 1760 rpm Voltage rating 460 V
Size 150 hp Enclosure type TEFC
Operating speed 1785 rpm
Table 5.2: Motor load test data for a chipper
5.4.1 Calculations for the field test
The data collected from the load test performed on the chipper motor during the assessment
is further used to find the load factor of the motor. The calculations of the motor load test
data are shown as follows:
Slip = RPM sync – RPM measured
Slip = 1800 – 1785
= 15
Motor load = Slip
RPM sync – RPM full load (nameplate)
63
= 15
1800 – 1760
= 0.375
Thus from the calculations it can be seen that the instantaneous load of the chipper
motor is 0.375. Similar tests are carried out on different motors in the plants on different
assessments. The collected data on these motors and the calculation of the motor load is done
for each of these motors and can be seen in the Appendix III. It should be noted that the
operating rpm, which is measured, always lies in between the synchronous and the full load
rpm of the motor. Even though the range or the difference between the synchronous and full
load rpm is small still the measured operating rpm will lie within that range. A summary of
some of the load test conducted at different plants can be seen in the Table 5.3.
Motor Type Motor size
(hp)
Measured
rpm
Full load
rpm
Synchronous
rpm
Motor load
Chipper shaker 40 1780 1760 1800 0.50
Treatment plant 40 1762 1760 1800 0.95
Trimmer 10 1774 1745 1800 0.47
Table 5.3: Summary of some of the load test calculations
5.5 Conclusion
As can be seen in the section 5.4.1 and the Appendix III, the motor load test carried
out on the motors in the wood manufacturing plants indeed show that the load factor of the
motor is smaller than optimal. This shows that there is an opportunity for downsizing the
motors to there appropriate size and thus reduce demand as well as energy for the plant. This
load test is only an instantaneous load test carried out during the field visits of these plants.
Before coming to a final decision on the downsizing, a continuous load test needs to be
performed on the candidate motors at different time intervals so as to make sure of the
downsizing possibility. After the load factor on the motor is obtained, the efficiency for the
motor can be obtained from the Motor Master database. These load and efficiency values of
the motor then can be used for detailed economic analysis using the Motor Master software.
Motor Master will give a better insight into the replacement and downsizing decisions and
will help justify the investment from the economics of the decision. The features of the Motor
64

Master and how the different variables in the Motor Master software affect the replacement
decision are discussed in the next chapter.
Chapter 6 Motor Master Analysis
The motor load test performed on the motors in the wood manufacturing plants
visited suggest that the motors are indeed over loaded for the application and there is
immense potential for downsizing them to the appropriate size. After determining the load
factor, the efficiency values of the motors can be obtained from Motor Master software for
those loads. This chapter will discuss the Motor Master analysis of the various replacement
decisions. A detailed justification on the motor replacement decision can be obtained. Also a
thorough sensitivity analysis of the replacement decision is made by changing the various
parameters that govern the investment decision.
65

6.1 Introduction to Motor Master
Motor Master is a motor management software designed by the US Department of
Energy to support motor management functions at medium sized and large industrial
facilities. It supports motor and motor systems improvement planning through identifying the
most efficient motors for a given repair or motor purchase decision. It can be used to identify
inefficient or oversized inventory motors and compute the energy and demand savings
associated with selection of a replacement energy efficient model. Motor Master + contains a
field data module, a motor price and performance database, energy conservation analysis, life
cycle costing, and energy accounting capabilities [31].
The compare module of the software calculates the annual energy consumption and
energy costs for particular motors in a specific application. It predicts expected energy and
cost savings for replacing an existing motor with an energy efficient model, and shows the
simple payback from energy cost savings. The comparison of two motors can be done in the
following three scenarios:
New: Compare two new motors from the motor catalog.
Rewind: Compare rewinding an existing motor with purchase of a new energy efficient
motor.
Replace existing: Compare an existing motor with a new energy efficient replacement.
These three scenarios are discussed in detail in the following passages. The motor
data collected from the site visits and also the load test results will be used to analyze the
different replacement decisions in detail.
6.2 Compare new motors
This scenario compares the costs of acquiring and operating a standard motor with
those of an energy efficient model. Motor Master + determines the energy and cost savings
possible with the energy efficient model. Then, assuming that the energy efficient motor is also
more expensive to purchase, it calculates the simple payback. The time it takes for the savings
to pay back the difference or premium in the new motor purchase price. The major parameters,
66
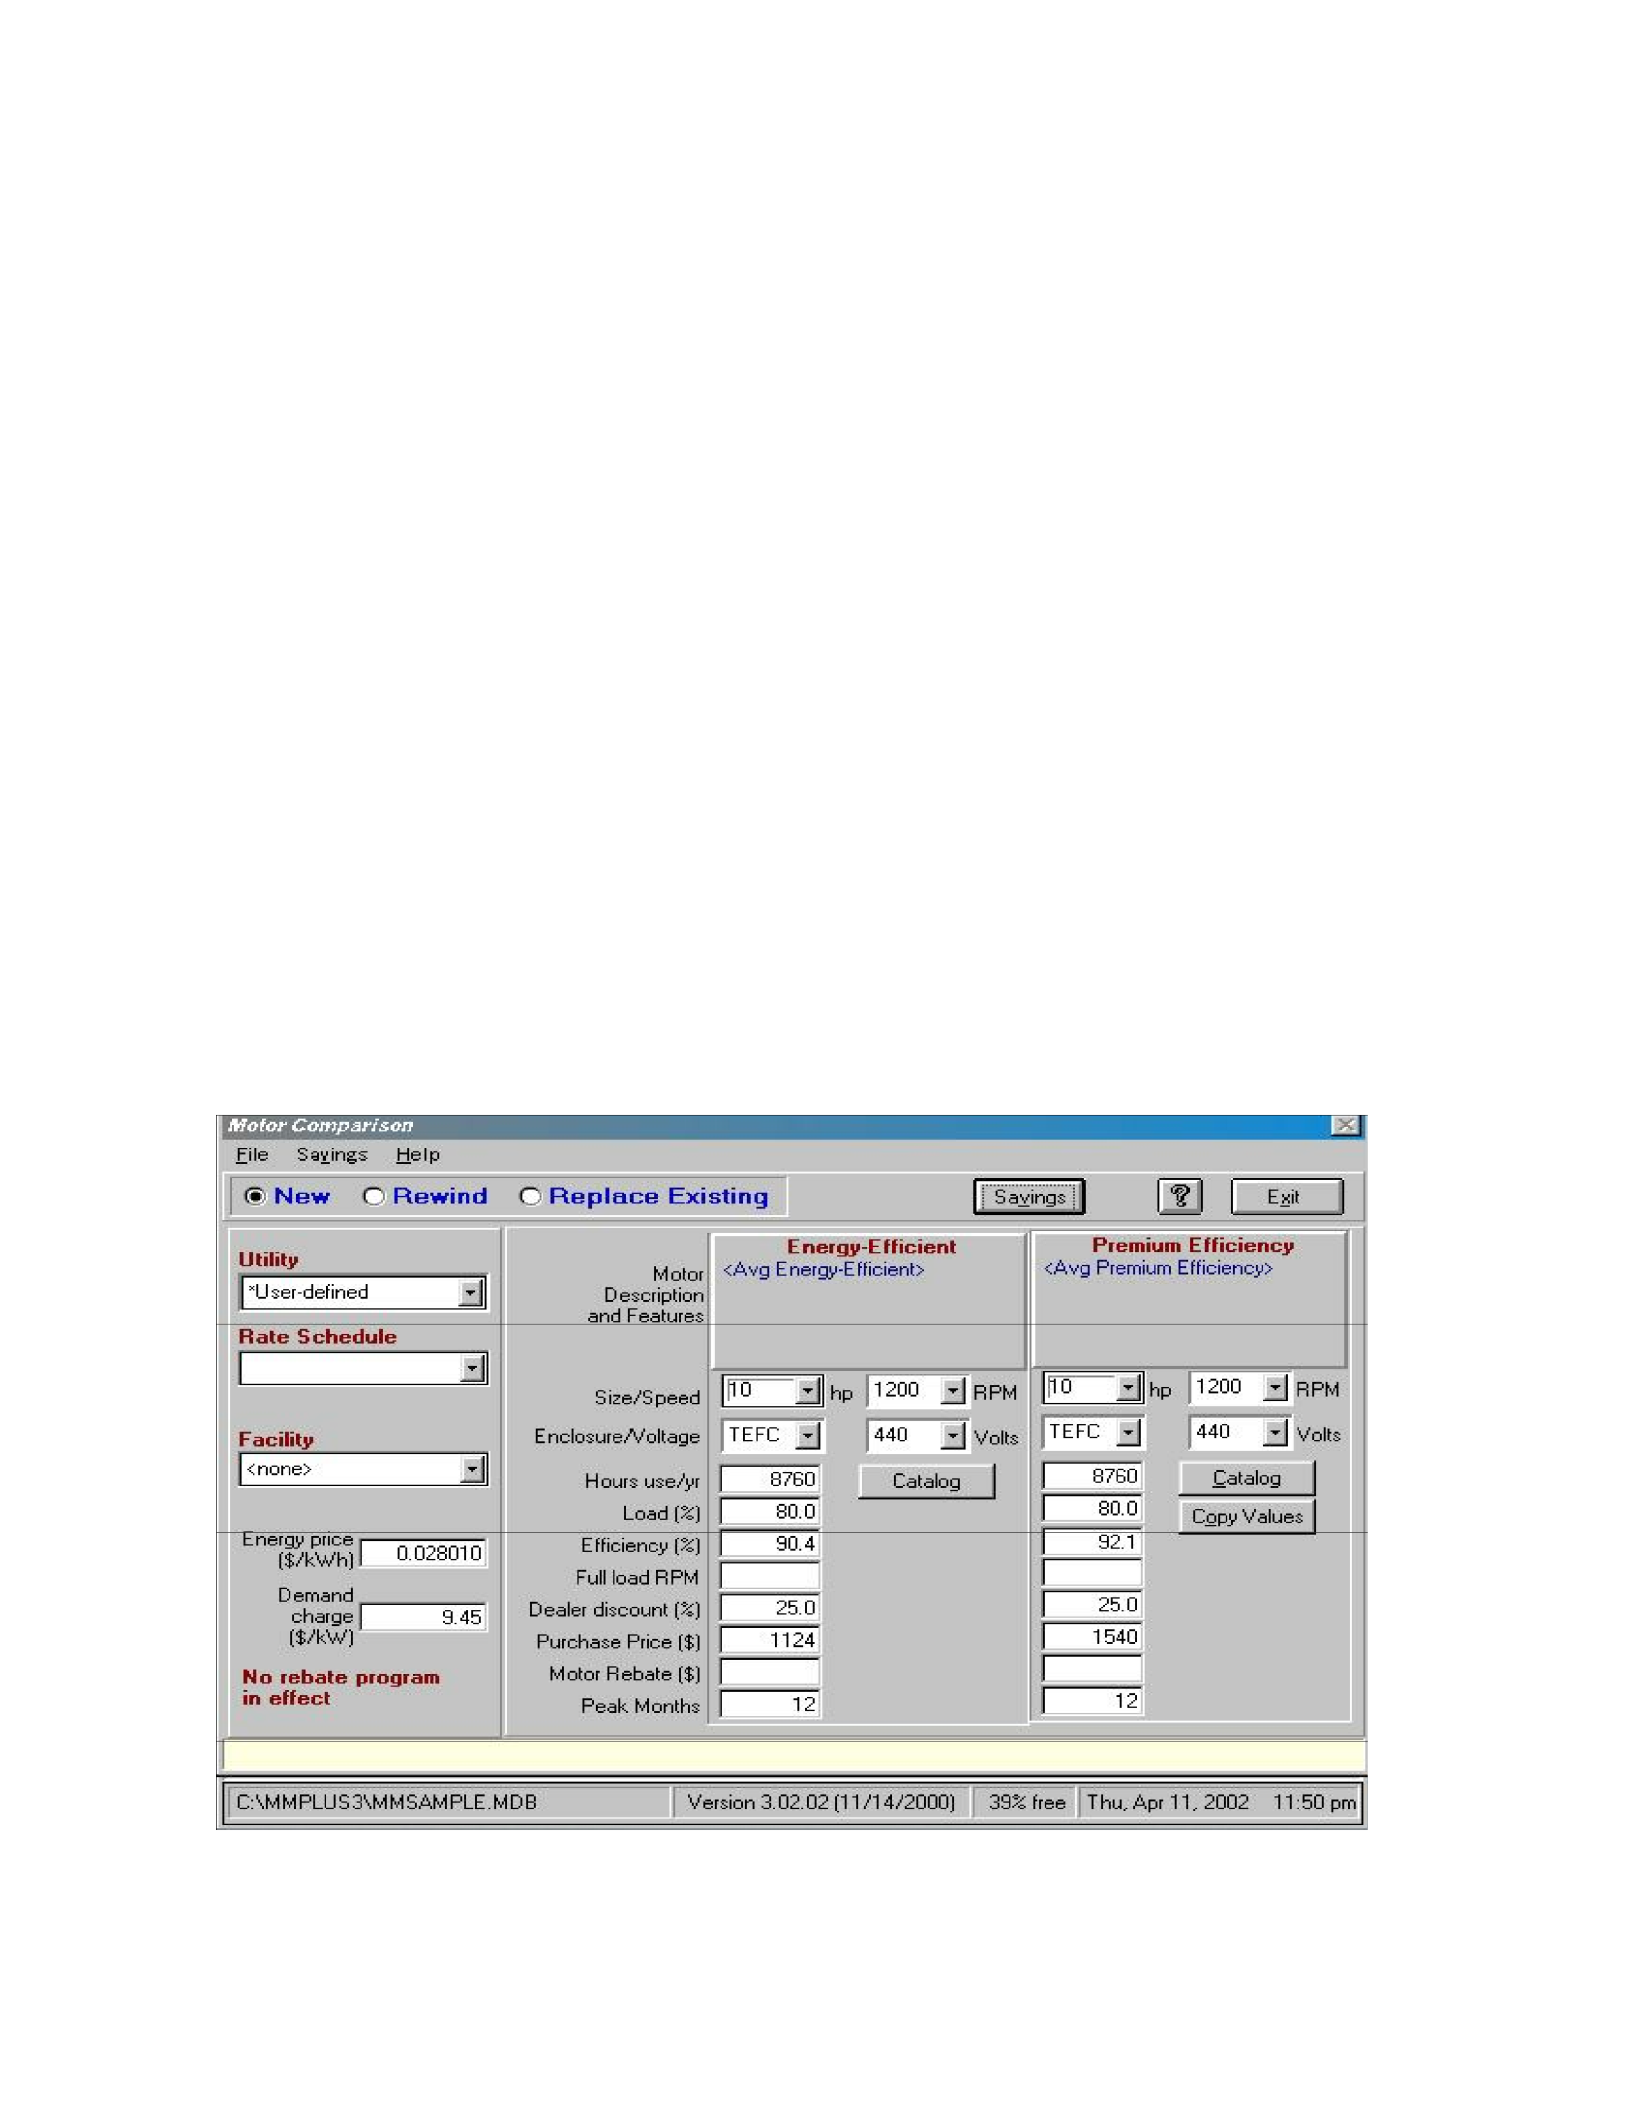
which govern this type of decision, are the purchase price of the standard and energy efficient
model and the operating efficiencies of these motors [31].
As can be seen in the Figure 6.1, the analysis is performed for a 10 hp motor, which runs for
3 shifts, 8760 hours annually. The load factor for the analysis is assumed to be 0.80. The
enclosure type for the motors under comparison is assumed to be of TEFC type. The energy
cost used in the analysis is obtained from the rate schedule for facility A, which is 0.02801 $/
kWh. The demand cost obtained from the schedule is 9.45 $/ kW. This analysis is performed
on motors in the range from 7.5 hp to 200 hp. It was found during the assessments that the
motors in wood manufacturing plants lie in this range. The payback for this analysis is
obtained on the investment, which is the difference of the capital cost of purchasing and
installing a standard motor and an energy efficient model. The Figure 6.2 shows the savings
obtained by making such an investment comparison for new motors. The energy saved and
the demand saved and also the cost savings related to them can be seen here. The simple
payback, which is calculated, can also be seen in this window. The value for the motor
premium is obtained as a difference of the purchase cost of the standard efficiency and the
energy efficient models.
67
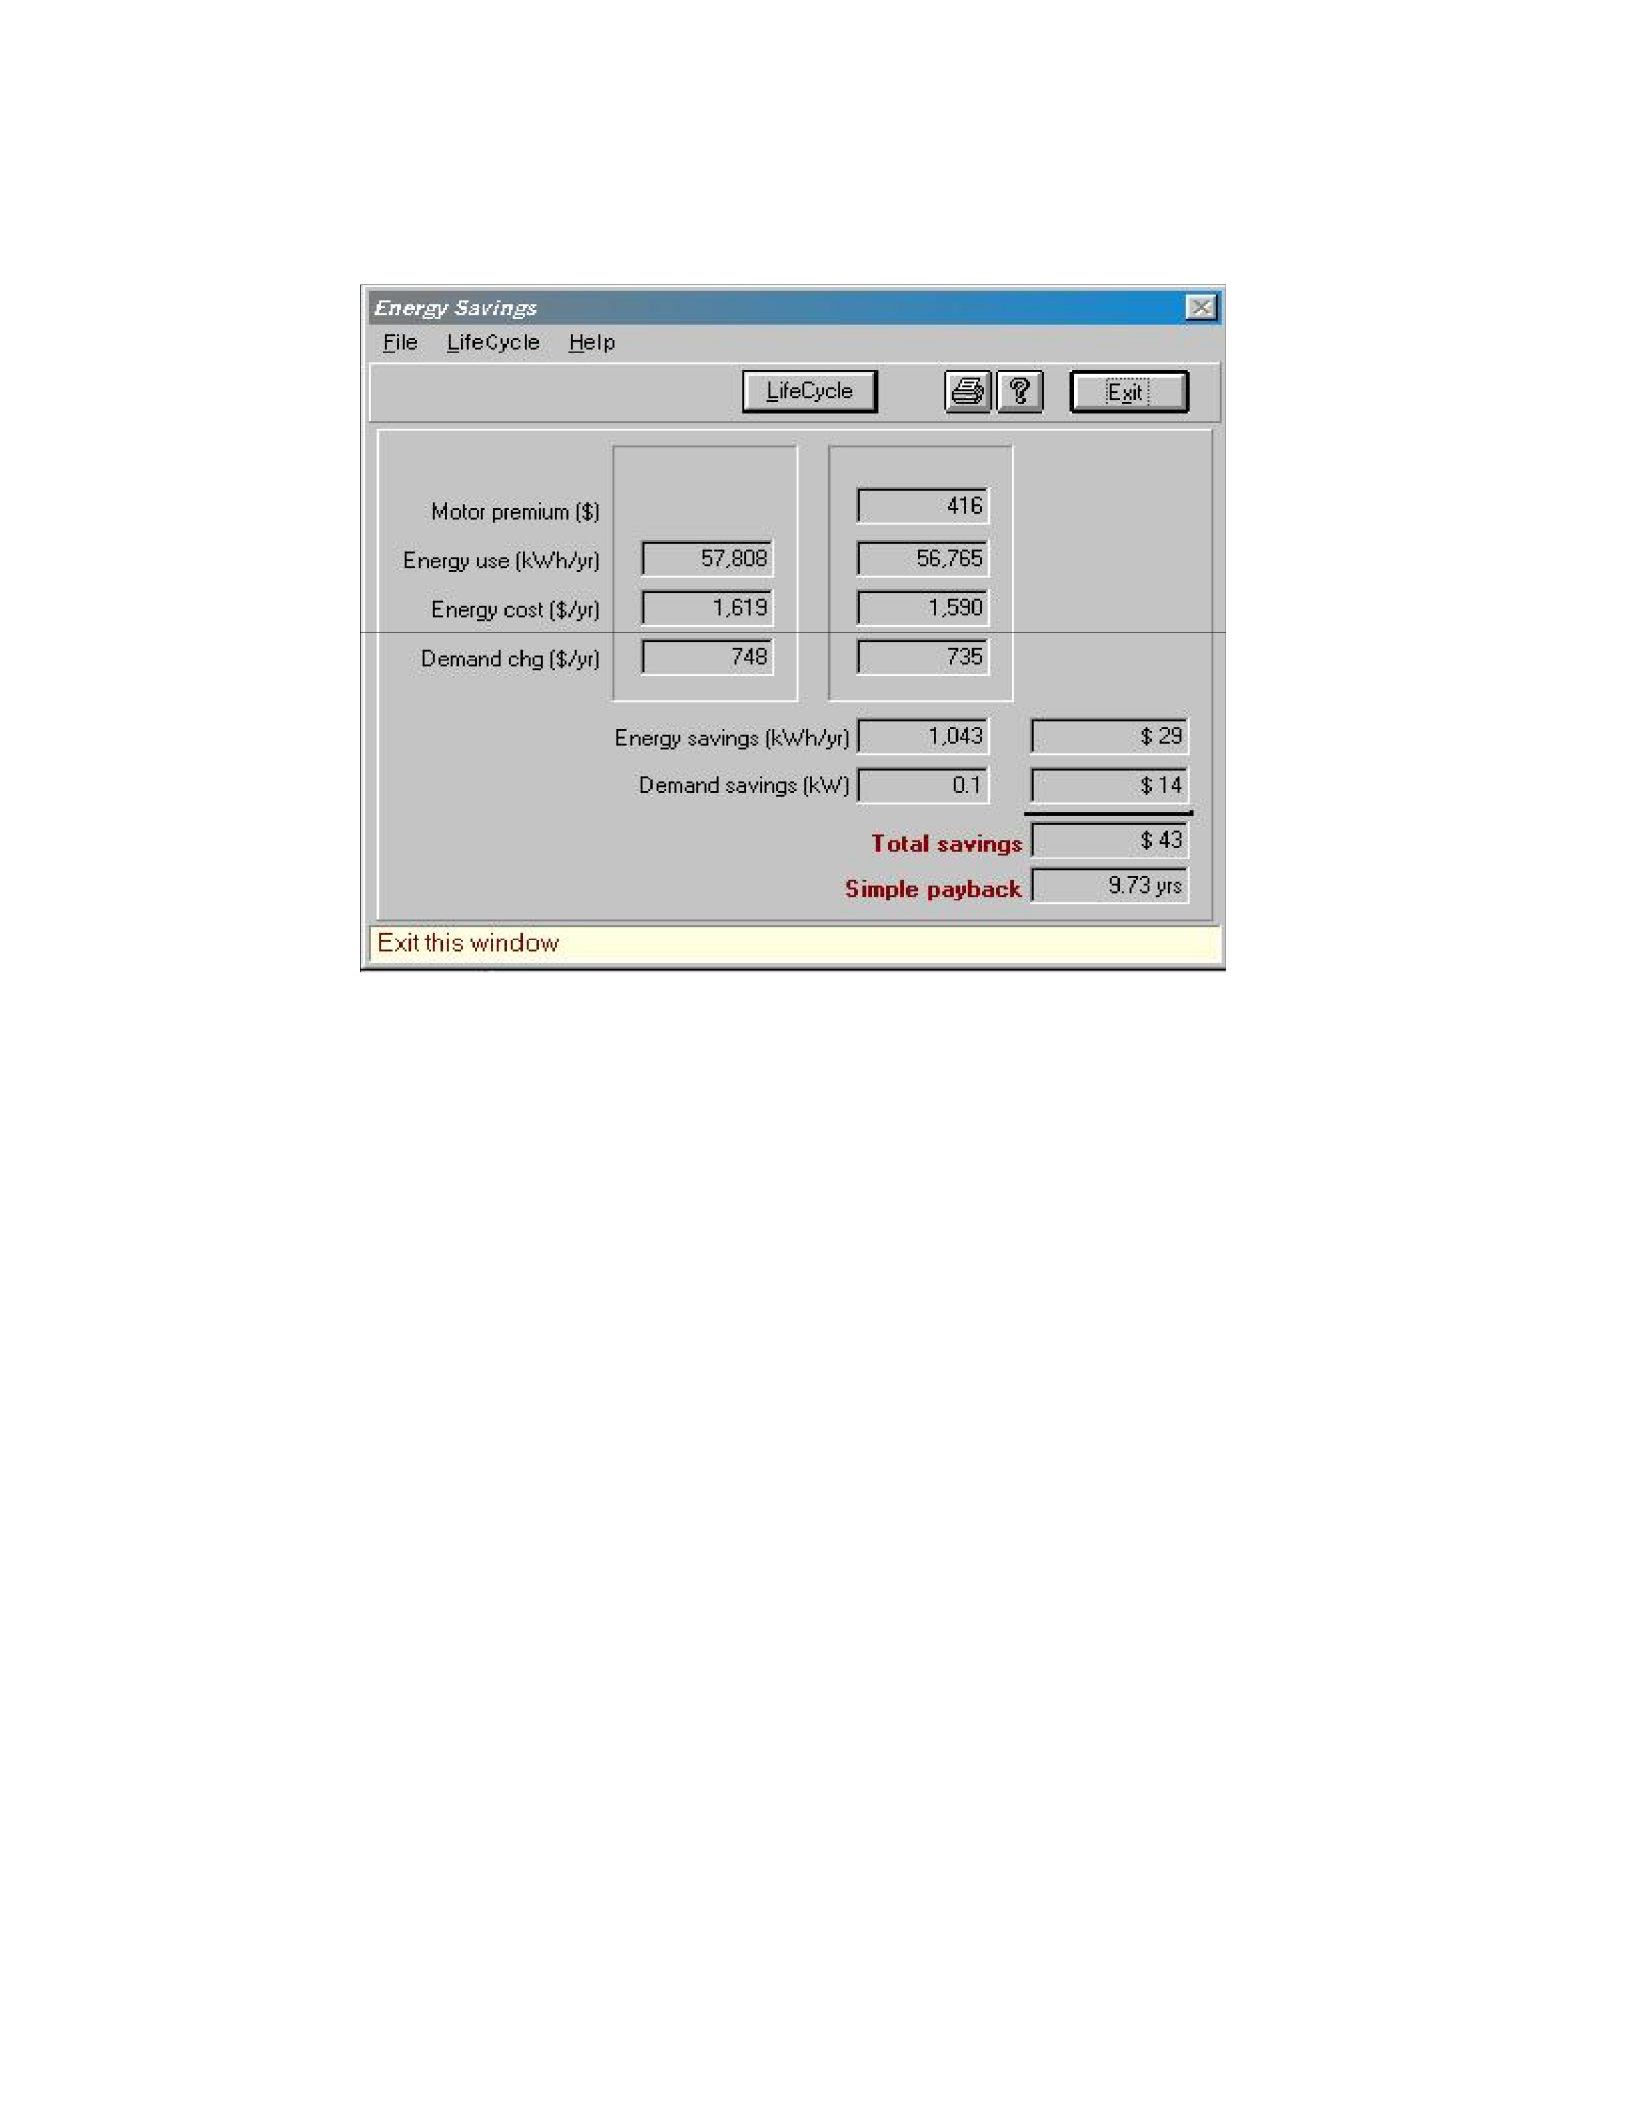
Figure 6.1: Compare module - Compare new motors
Figure 6.2: Savings window - Compare new motors
6.2.1 Analysis of the results
The compare new module of the Motor Master was used to compare the new motor
investment decisions from 7.5 hp to 200 hp. The Table 6.1 shows the results of that analysis.
These results are based on the energy and demand cost obtained from the rate schedule for
facility A. As can be seen in the table, the payback period is significantly high in the analysis
for a 10 hp motor. This is because the motor premium for this size of motor is high. This high
motor premium is not justified by a smaller payback, as the total annual energy savings
obtained are very small.
Other wise a there is no specific trend observed in the simple pay back as the size of
the motors is increased from 7.5 hp to 200 hp. There is no such trend because the motor
premium for each size is different and it does not vary in the proportion. Also it can be seen
that the there is not much difference in the standard and premium energy efficiency values for
the bigger sized motors. Overall this analysis shows that one should always opt for a
premium efficiency motor as compared to a standard efficiency motor when making a new
motor purchasing decision.
68
TEFC Enclosure 1200 rpm 25% Dealer Discount 12 months peak
Energy Efficient Premium Efficiency Analysis
hp Hours Load
factor Eff Investment hp Hours Load
factor Eff Investment Energy
sav
Dem
sav
Pay
back
7.5 8,760 0.8 90.3 1011 7.5 8,760 0.8 91.7 1020 19 9 0.32
10 8,760 0.8 90.4 1124 10 8,760 0.8 92.1 1540 29 14 9.73
15 8,760 0.8 91.3 1586 15 8,760 0.8 92.5 1661 32 15 1.59
20 8,760 0.8 91.4 1878 20 8,760 0.8 92.8 1931 49 23 0.74
25 8,760 0.8 92.4 2194 25 8,760 0.8 93.4 2437 42 19 3.93
30 8,760 0.8 92.6 2634 30 8,760 0.8 93.9 2755 68 32 1.2
40 8,760 0.8 93.4 3344 40 8,760 0.8 94.5 3944 69 32 5.96
50 8,760 0.8 93.5 4005 50 8,760 0.8 94.5 4437 81 37 3.66
60 8,760 0.8 93.9 4860 60 8,760 0.8 95 5086 99 46 1.56
75 8,760 0.8 94.1 5643 75 8,760 0.8 95.2 6056 130 60 2.17
100 8,760 0.8 94.5 7268 100 8,760 0.8 95.4 8193 148 68 4.28
125 8,760 0.8 94.6 8723 125 8,760 0.8 95.7 9950 219 101 3.82
150 8,760 0.8 95.2 9748 150 8,760 0.8 96.1 11469 202 94 5.81
200 8,760 0.8 95.2 12014 200 8,760 0.8 95.9 13018 224 104 3.06
Table 6.1: New motors investment analysis
The user might want to check the premiums for 10 hp motor and recalculate the
savings if he gets a better price for the premium efficiency model. The results for the
comparison are plotted as can be seen in the Figure 6.3 below. The payback period obtained
is plotted against the motor size. It can be seen that there is a spike in the plot for the 10 hp
motor, because of its high premium. Other wise the plot appears to have no specific pattern.
69
Figure 6.3: Comparison for different sizes of the motors with respect to the payback
6.3 Rewind Vs new efficiency motor purchase decision
This compares the cost effectiveness of rewinding a failed motor with the cost of
purchasing a new standard efficiency or energy efficient model. This comparison takes into
account the reduced efficiency for the rewound motor attributable to age and rewind losses.
To perform this analysis the user must select the rewind option in the motor master compare
module. As can be seen in the Figure 6.4 some additional information is required for this type
of analysis. There is additional information required on the rewinding charge for the existing
standard efficiency motor. Also the loss in the efficiency of the standard motor is another
important variable considered here. The default value for this loss is 1% for motors above 40
hp, and for those below 40 hp this default value is 2%. Normally old motors might have a
chance to lose more efficiency after rewinding then as compared to new motors. In this case
again, the load factor of the motor and the efficiency of the motor play a crucial role in the
analysis. The comparison is shown in Figure 6.4 for a 50 hp motor. The savings obtained
from such an option can be seen in the Figure 6.5. The analysis is again performed using the
70
Compare New
0
2
4
6
8
10
12
7.5 10 15 20 25 30 40 50 60 75 100 125 150 200
Motor Size (hp)
Payback Period (Yrs)
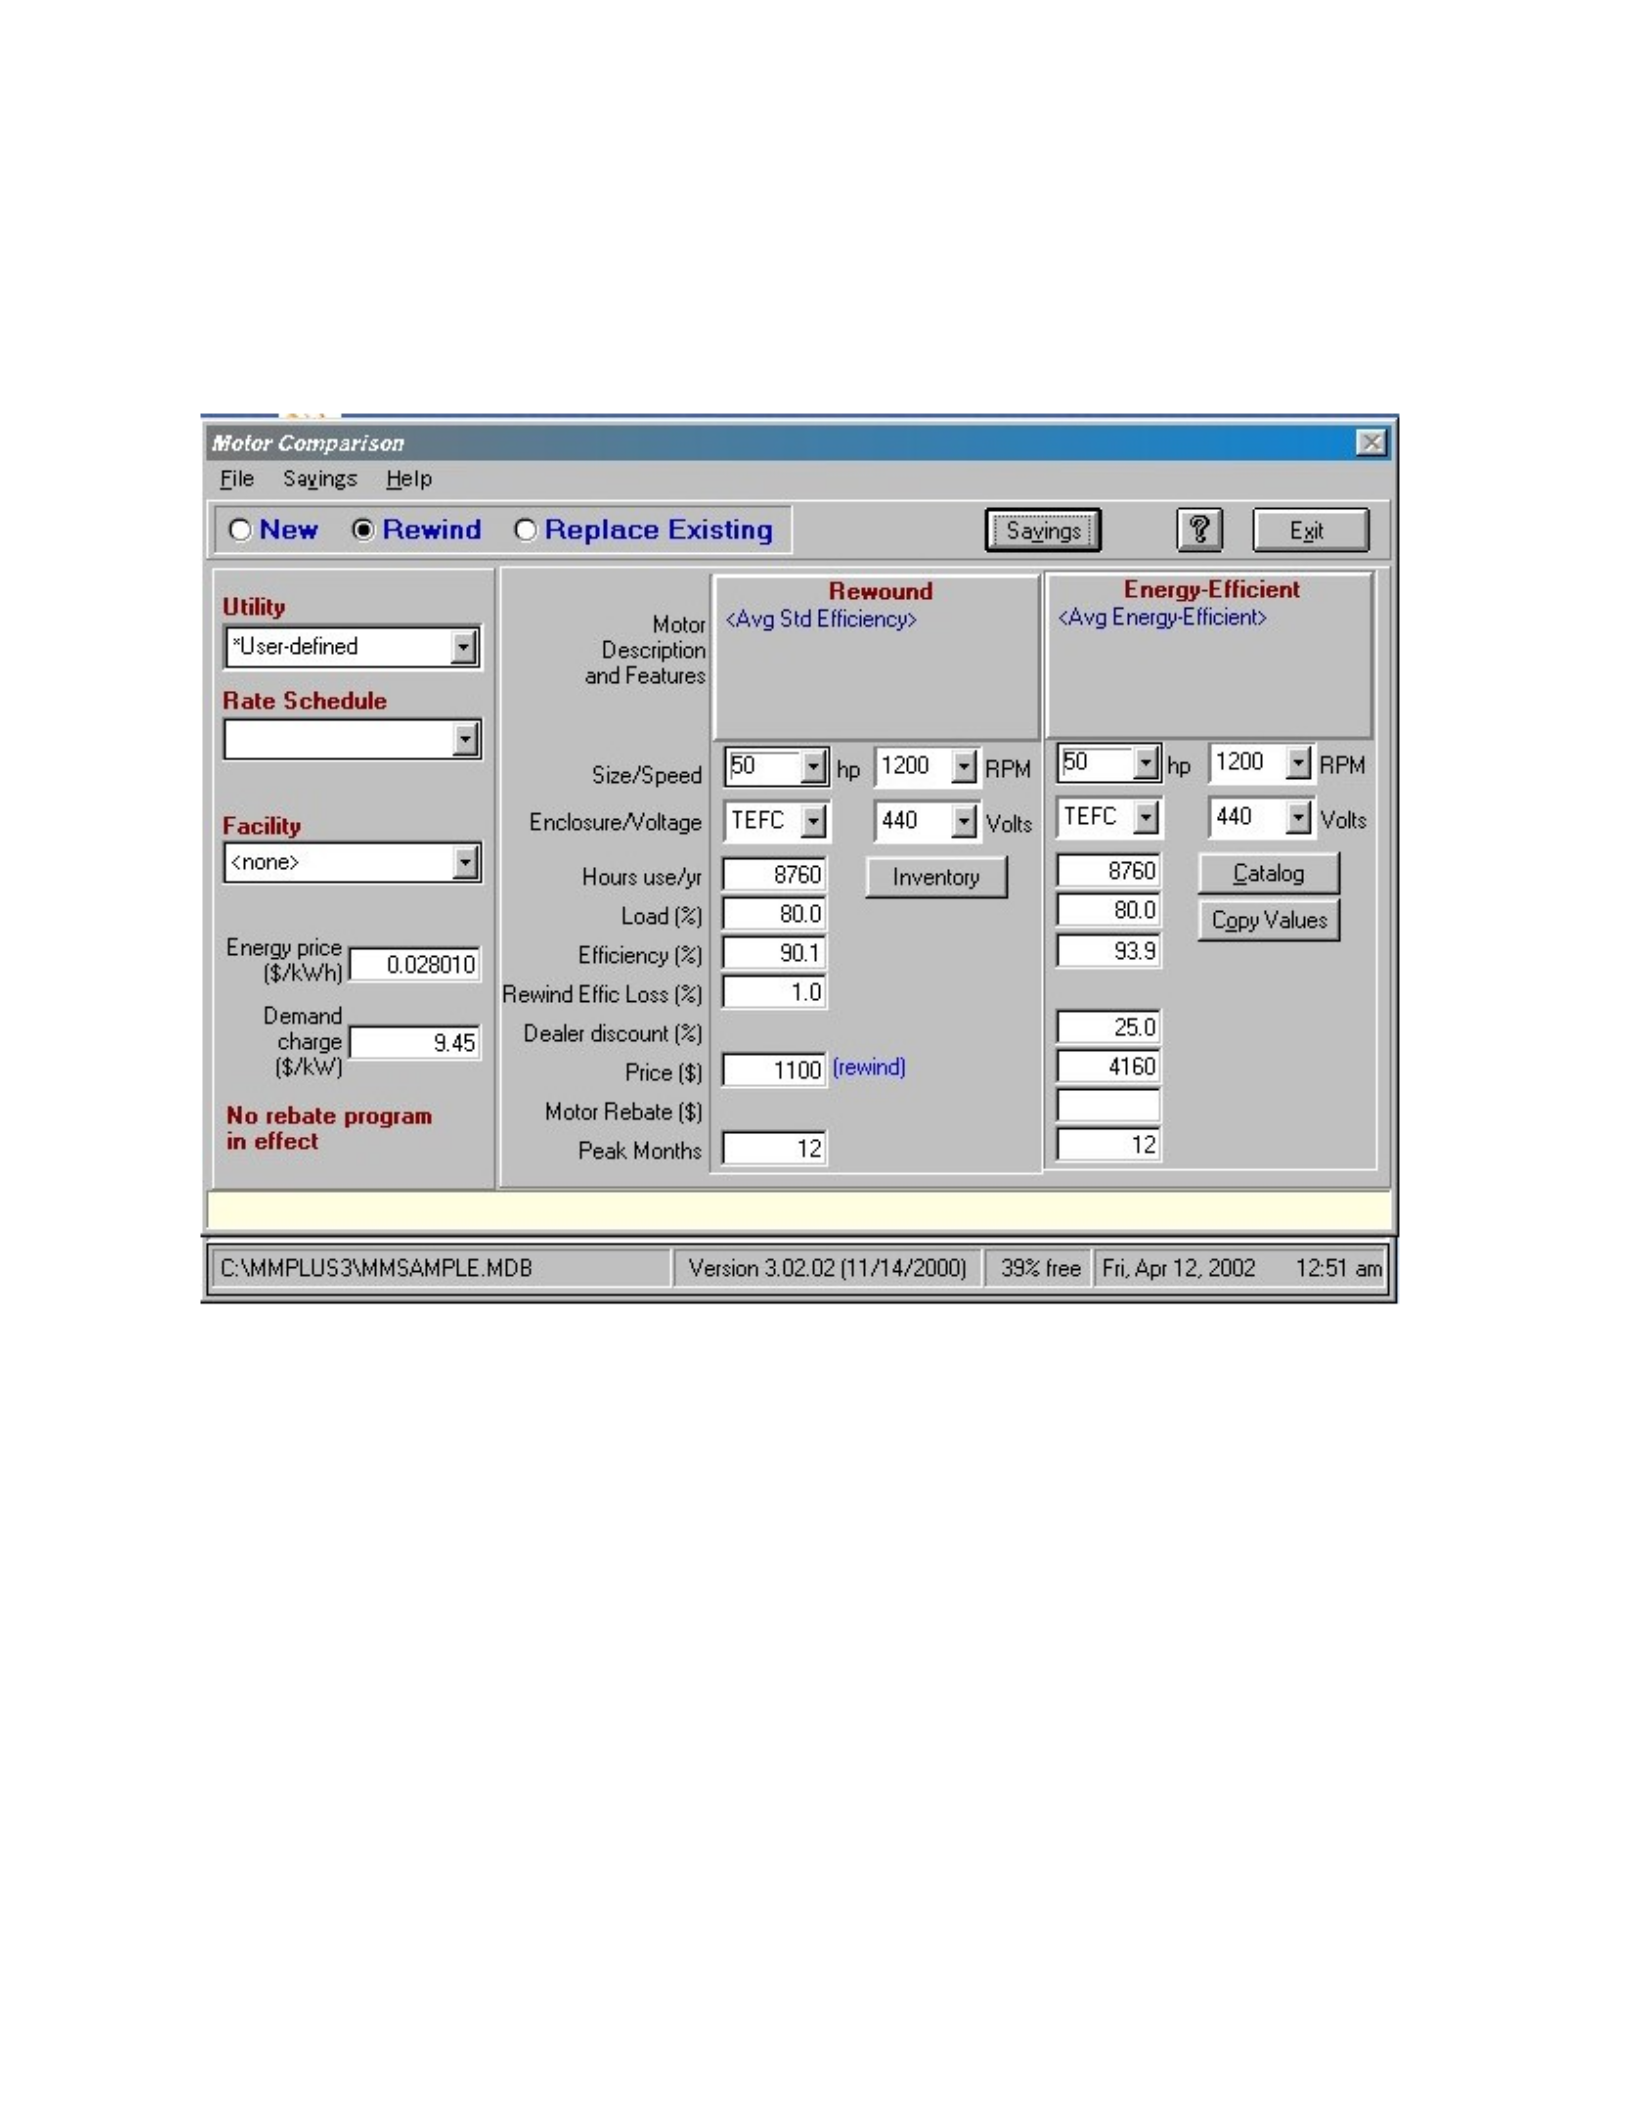
energy and demand cost values obtained from the utility rate schedule for facility A. Again
here the enclosure type of the motors is assumed to be TEFC and the load factor is assumed
to be 0.8.
Figure 6.4: Compare module - Rewind Vs New efficiency motor purchase decision
71
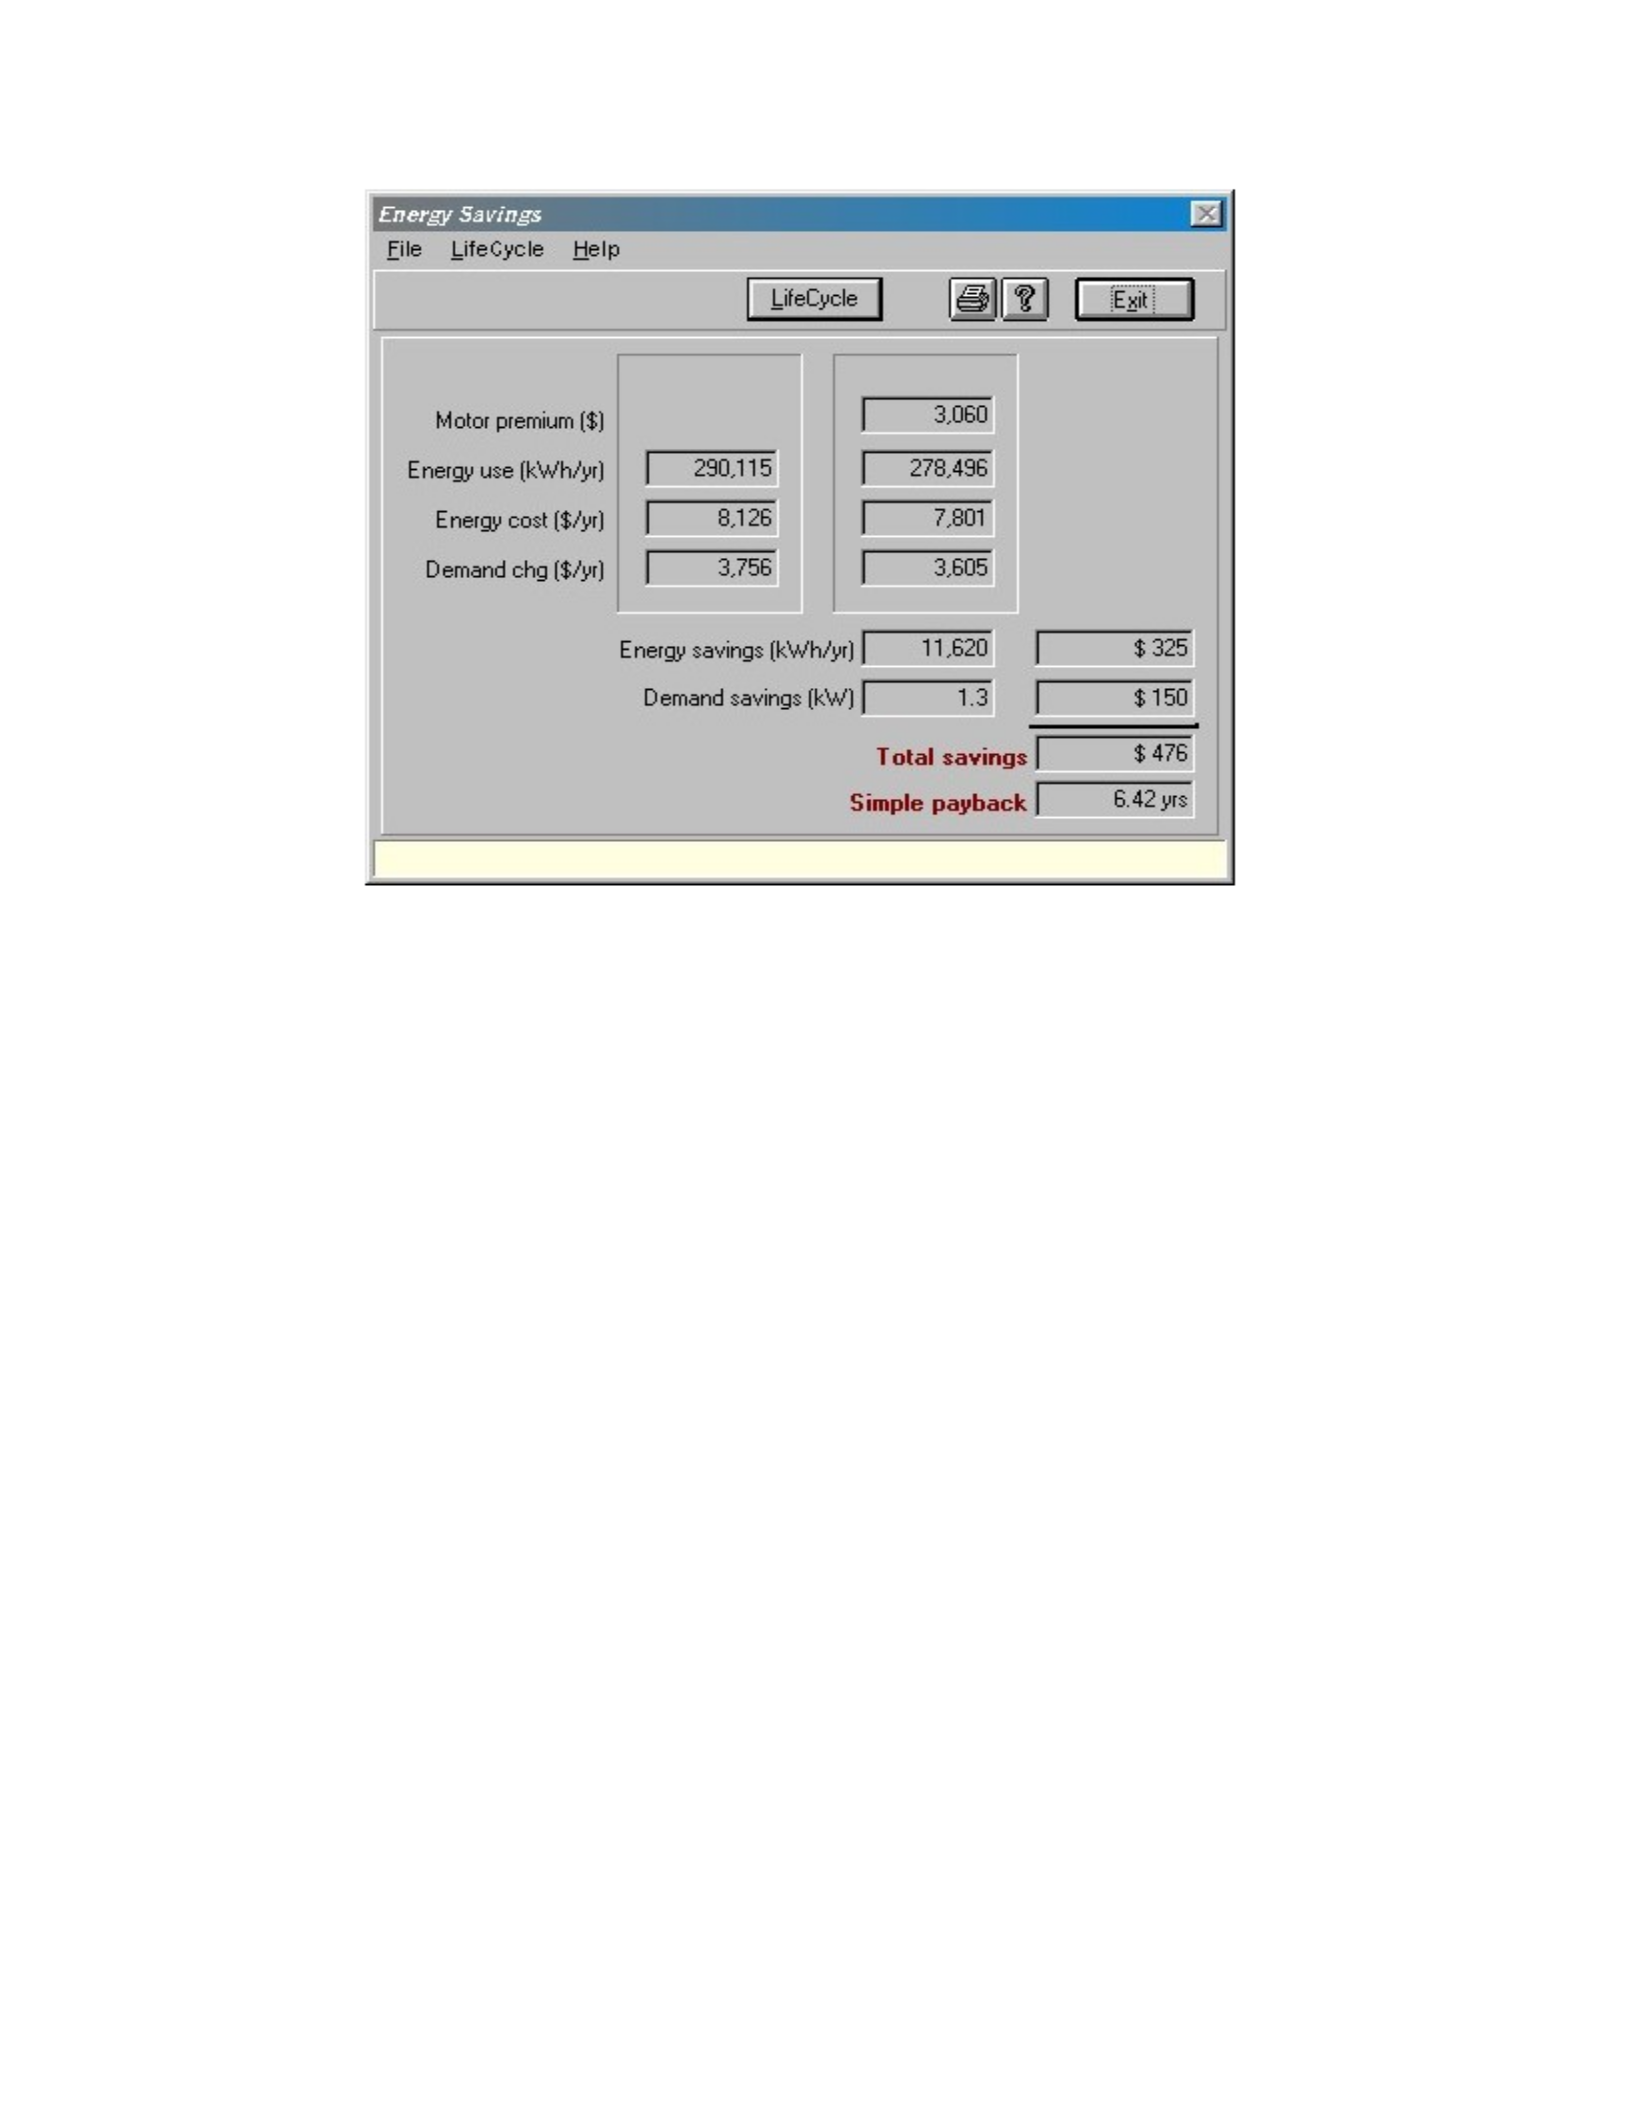
Figure 6.5: Savings window - Rewind Vs New efficiency motor purchase decision
6.3.1 Analysis of the results
The comparison of the cost effectiveness of rewinding a failed motor with the cost of
purchasing a new standard efficiency or energy efficient model was performed from 7.5 hp to
200 hp range of motors. The Table 6.2 shows the results of that analysis. These results are
based on the energy and demand cost obtained from the rate schedule for facility A. The table
shows that purchasing a new energy efficient motor might be more economical up to 40 hp
size of the motors. The payback for the energy efficient motor purchase is above 5 years for
motors above 40 hp. This is because as the size of the motors increase, the cost of the energy
efficient models increases rapidly as compared to the increase in cost of rewinding motors.
For the bigger size motors the motor premium is very high as compared to smaller size
motors up to 40 hp. Also the efficiency of the current motors, which are supposed to be
rewound on failure, plays a very crucial role in the decision. If the current motors are old
motors and if they are going to be rewound a second or third time, then the efficiency values
might be lower then what is assumed here in the analysis. In that case the purchase of energy
72
TEFC Enclosure 1200 rpm 25% Dealer Discount 12 months peak
Existing Proposed Analysis
hp Hours Load
factor Eff Rewinding
Cost hp Hours Load
factor Eff Investment Energy
sav
Dem
sav
Pay
back
7.5 8,760 0.8 82.5 500 7.5 8,760 0.8 90.
5
1,012 118 54 2.97
10 8,760 0.8 83.7 550 10 8,760 0.8 90.
9
1,209 138 64 3.27
15 8,760 0.8 85.2 600 15 8,760 0.8 91.
5
1,604 180 83 3.82
20 8,760 0.8 86.6 660 20 8,760 0.8 91.
8
1,893 192 89 4.38
25 8,760 0.8 87.4 760 25 8,760 0.8 92.
8
2,286 244 113 4.28
30 8,760 0.8 88.2 800 30 8,760 0.8 93 2,660 255 118 4.76
40 8,760 0.8 88.3 980 40 8,760 0.8 93.
8
3,579 390 180 4.55
50 8,760 0.8 90.1 1100 50 8,760 0.8 93.
9
4,160 325 150 6.43
60 8,760 0.8 90.0 1320 60 8,760 0.8 94.
3
4,943 449 207 5.52
75 8,760 0.8 90.6 1650 75 8,760 0.8 94.
4
5,763 483 223 5.82
100 8,760 0.8 90.6 2200 100 8,760 0.8 94.
8
7,581 720 333 5.11
125 8,760 0.8 91.1 2400 125 8,760 0.8 94.
9
9,174 823 381 5.62
150 8,760 0.8 92.3 2650 150 8,760 0.8 95.
5
10,405 811 375 6.53
200 8,760 0.8 92.0 2860 200 8,760 0.8 95.
4
12,363 1124 519 5.78
Table 6.2: Rewind Vs new efficiency motor purchase decision
73
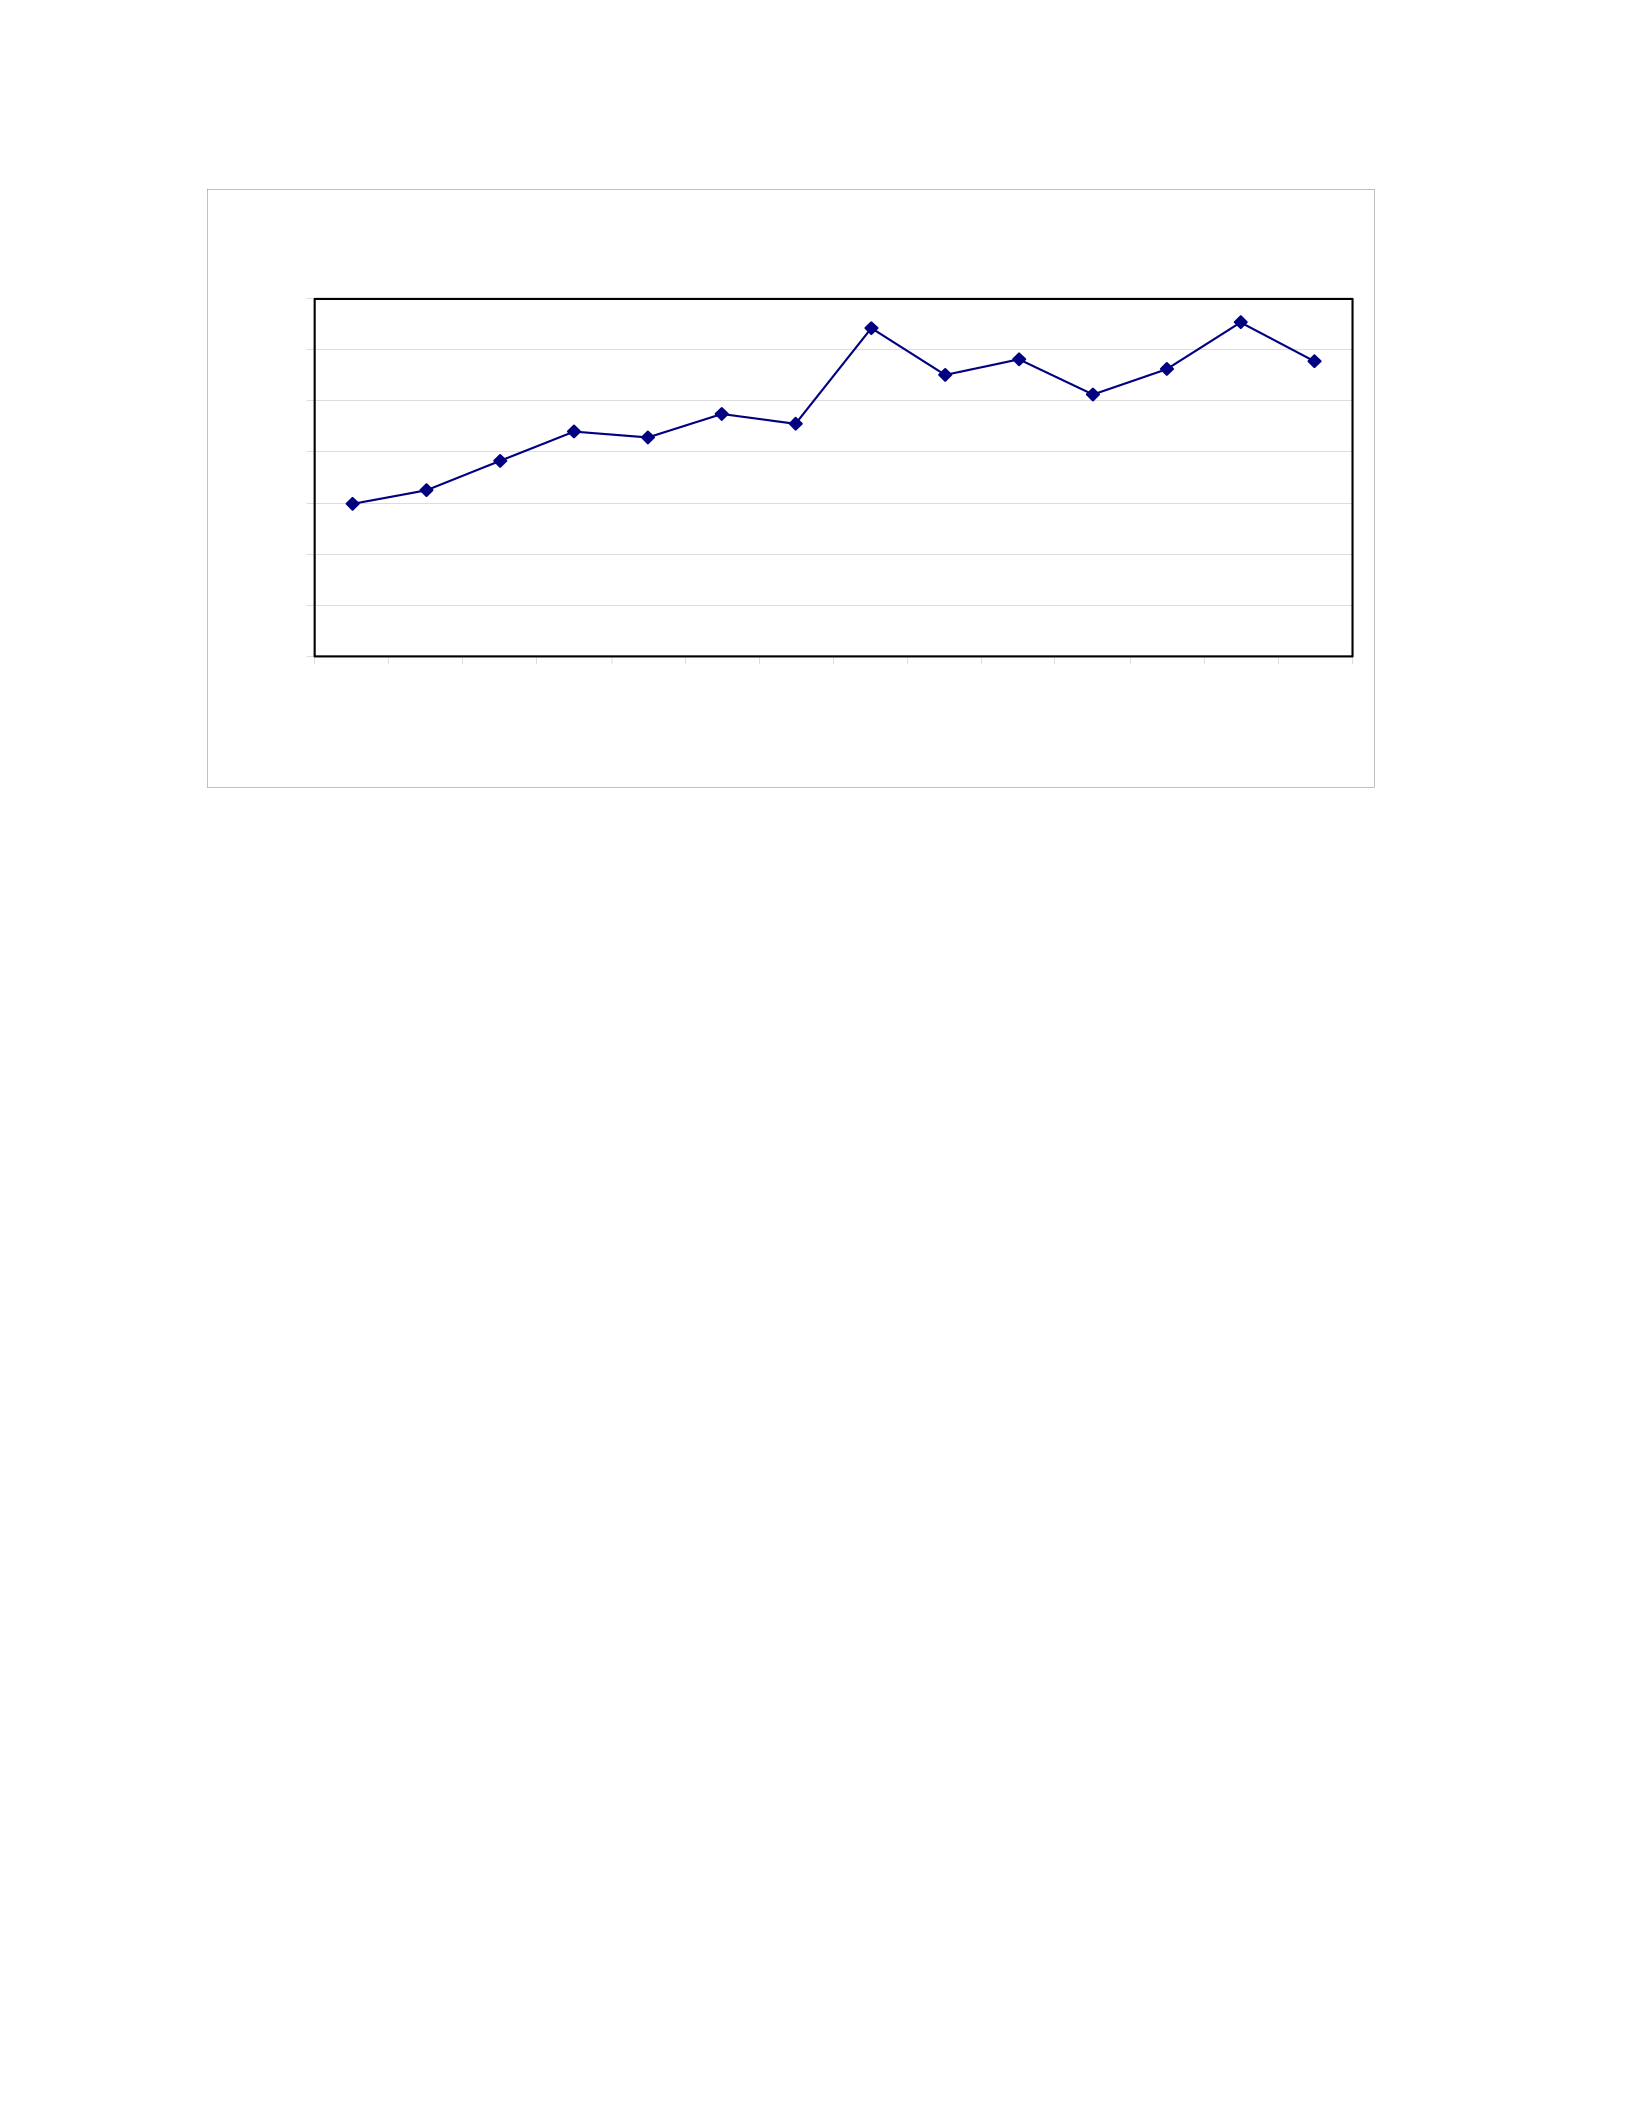
Figure 6.6: Analysis of the Rewind Vs new efficiency motor purchase decision
efficient motor option might be even more favorable. The Figure 6.6 shows the plot of the
payback period against the motor size. It can be seen that, the energy efficient motor
purchase decision instead of the rewinding decision may not be really favorable as the motor
size increases.
6.4 Replace existing
This analyzes the cost effectiveness of replacing an operable standard efficiency motor with
a new energy efficiency motor model of the same size. This calculation is useful for deciding
whether to replace older, low efficiency, and rewound motors. This analysis considers the
entire purchase price and installation costs as the motor premium in determining the simple
payback. In this option various cases are considered for the analysis. This analysis is again
performed for the energy and demand costs obtained from the rate schedule for facility A.
The comparison can be seen in the Figure 6.7.
74
Rewinding Option
0
1
2
3
4
5
6
7
7.5 10 15 20 25 30 40 50 60 75 100 125 150 200
Motor Size (hp)
Payback Period (Yrs)
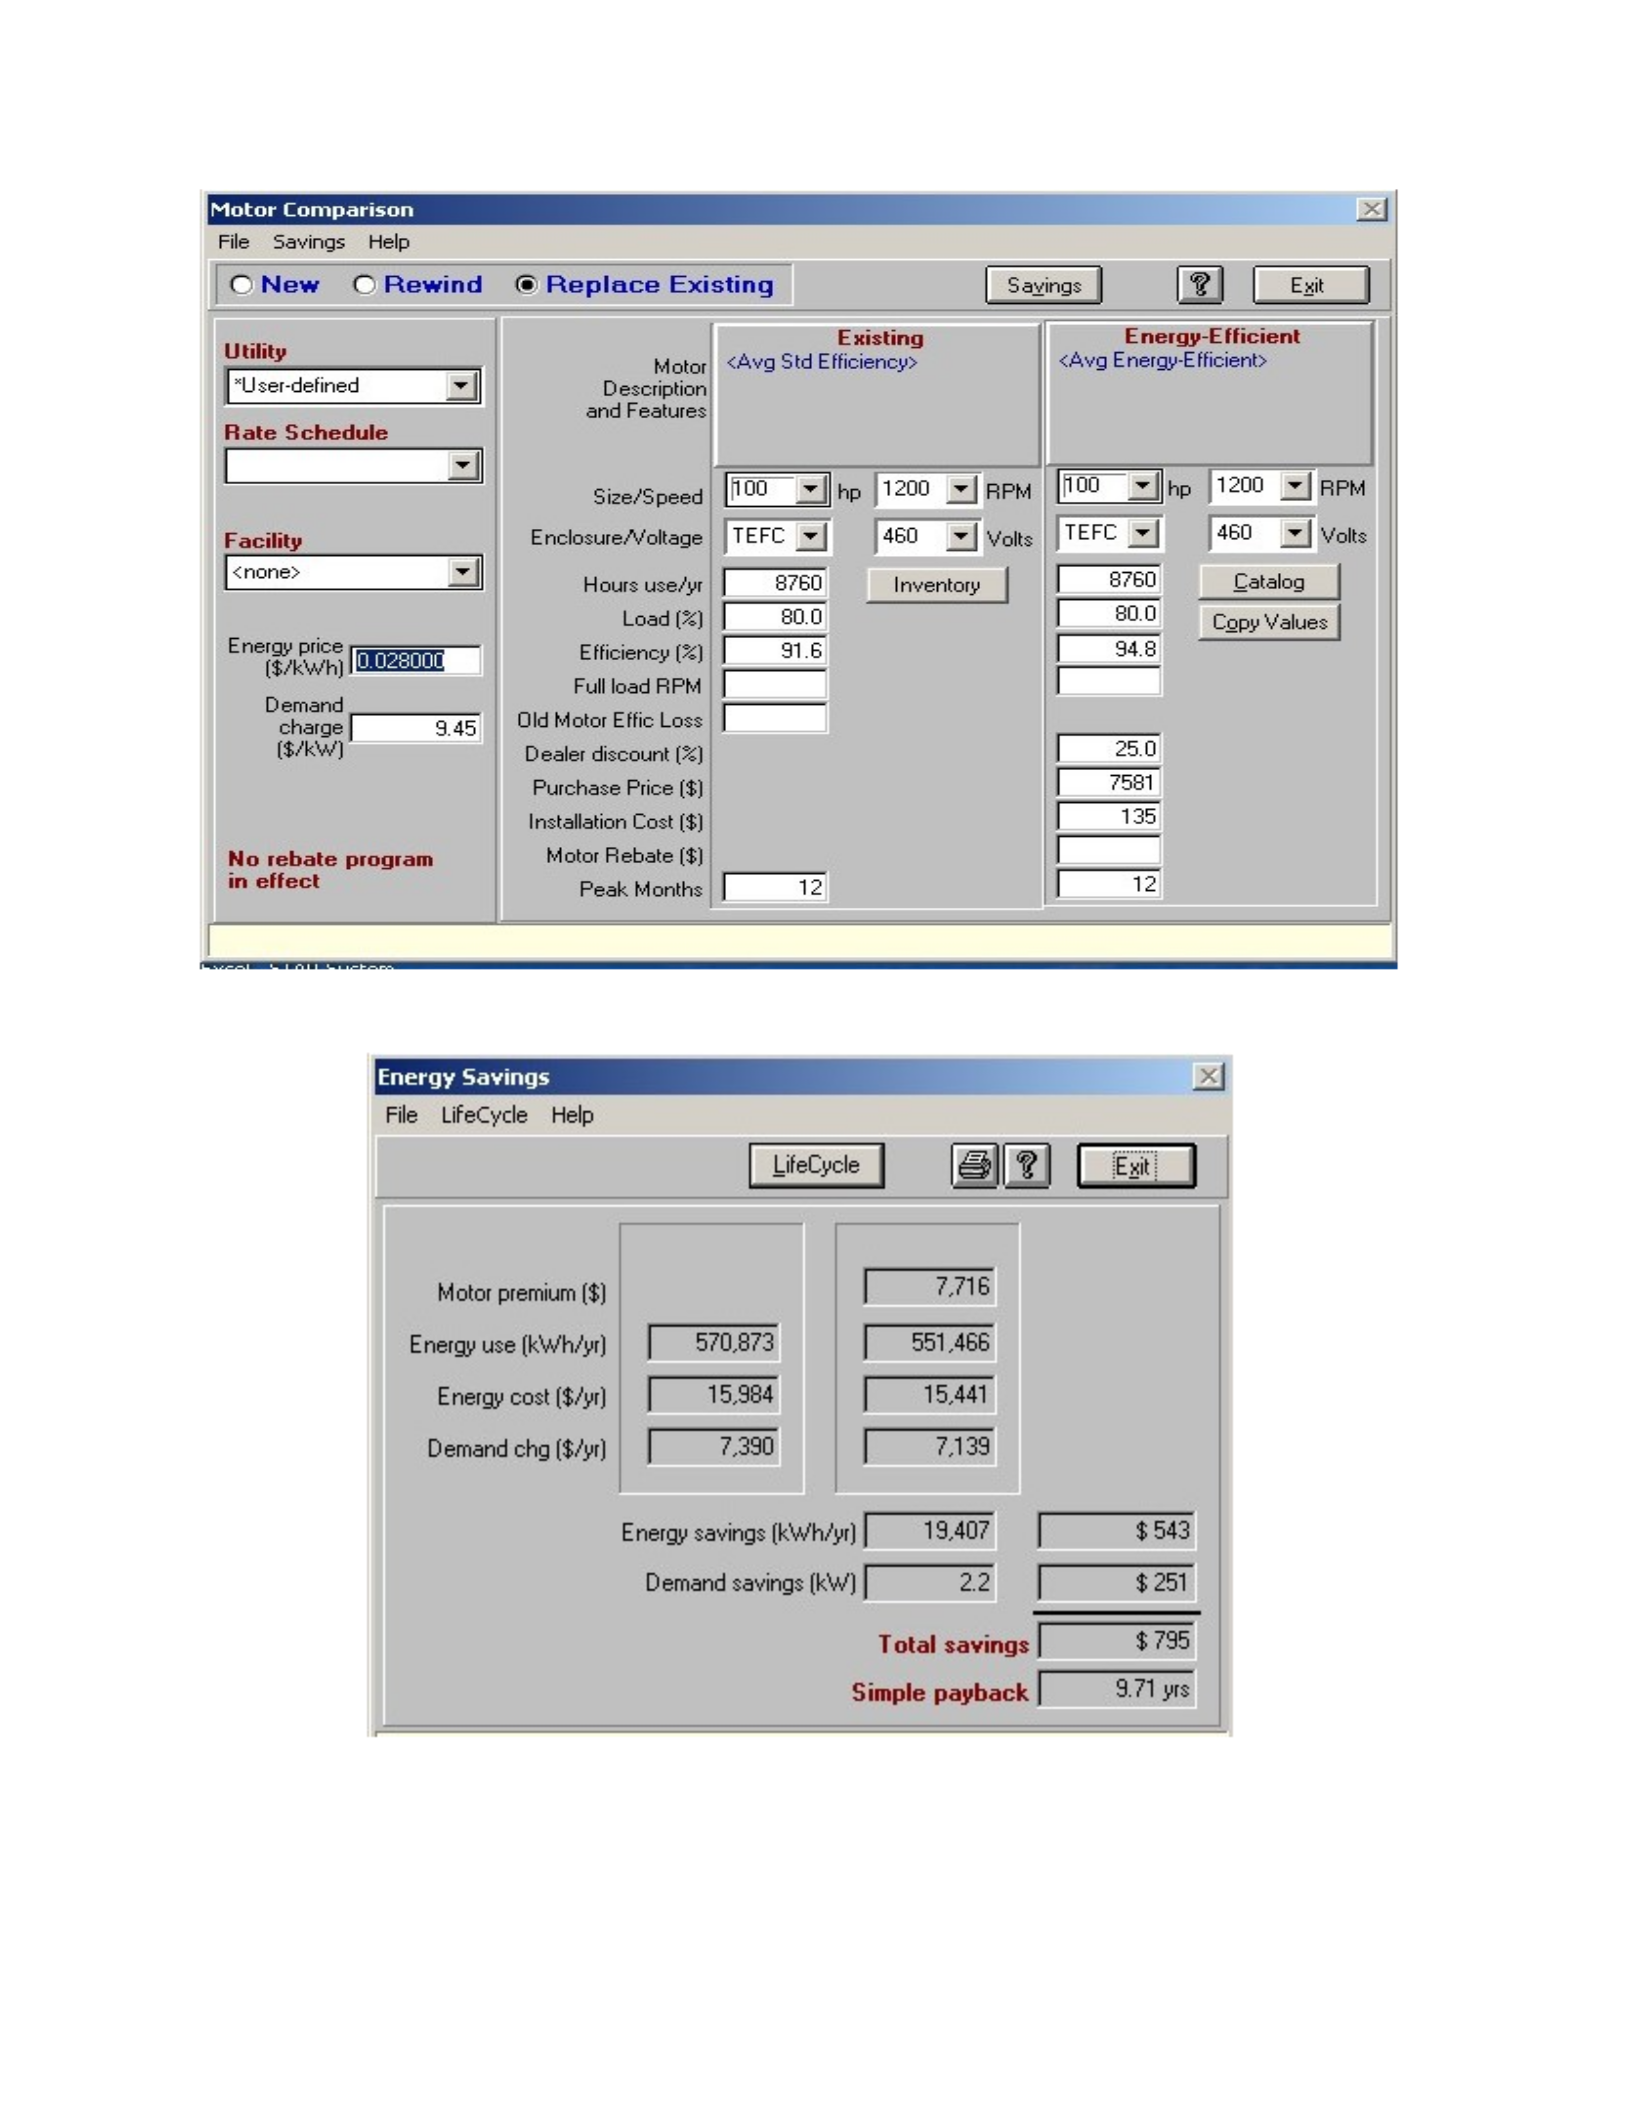
Figure 6.7: Compare module – Replace existing option
Figure 6.8: Savings window - Replace existing option
75

As seen in the Figure 6.8, the savings obtained from a replace existing option can be seen.
This example show in the Figure 6.7 and Figure 6.8 is for replacing an existing standard
efficiency motor with an energy efficient motor of the same size. The motor shown in the
example is a 100 hp motor. There are various parameters here in the replacement analysis,
which affect the outcome or the payback period for the investment decision. The parameters
are:
Type of motor enclosure
Number of operating hours of the motor
Efficiency of the existing standard efficiency motor
6.4.1 Analysis for the replace existing option
In this analysis following different scenarios are considered and the Motor Master is run for
each scenario to get an insight into various situations, which affect the decisionmaking and
also the payback period. These different scenarios are as mentioned below:
Replace existing standard efficiency motor with a same size energy efficient motor for
different enclosure types for the motor – this analysis will show the impact of the
enclosure type on the replacement analysis.
Replace existing standard efficiency motor with a same size energy efficient motor for
different number of hours in operation – this analysis which is performed for 2 shift
operating hours and 3 shift operating hours, shows the impact of the operating hours
on the payback of the investment.
Replace existing standard efficiency motor with a same size energy efficient motor for
different values of current standard efficiencies – this analysis shows the impact of
efficiency of the existing standard motor on the replacement decision.
Replace existing standard efficiency motor with a smaller size energy efficient motor
(downsizing) – this analysis is also performed for different values for efficiency of the
existing standard motors.
76
6.4.1.1 Analysis to measure the impact of the enclosure type of the motor
Many type of motor enclosures are available. Some of them are open, open drip proof
(ODP), guarded, splash proof, totally enclosed non-ventilated (TENV), totally enclosed fan
cooled (TEFC), explosion proof, etc. The enclosure types, which really affect the
decisionmaking in terms of payback and energy saved, are the TEFC and the ODP
enclosures. So this analysis is performed for these two types of enclosures assuming a three-
shift operation and a load factor of 0.8 in both the cases. The analysis is performed and the
results are as seen in the Table 6.3 and Table 6.4. It is evident from the analysis that the
TEFC enclosure motors are expensive as compared to the ODP type. So consequently the
payback for the TEFC enclosure option is higher than the ODP option. Also it can be seen
that the efficiency of the ODP type enclosure is a little better than the TEFC type enclosures
for the motors. The Figure 6.9 shows the plot for such an analysis and it is clear from this
plot that the user should opt for the TEFC enclosure only if the process demands it.
Unnecessary use of TEFC enclosure will result in higher paybacks and also loss of some
efficiency. The ODP type of enclosure should be given preference over the TEFC type of
course depending on the process requirements.
TEFC Enclosure 1200 rpm 25% Dealer Discount 12 months peak
Existing Proposed Analysis
hp Hours Load
factor Eff. hp Hours Load
factor Eff Investment +
Installation
Energy
sav.
Dem
sav.
Pay
back
7.5 8,760 0.8 84.5 7.5 8,760 0.8 90.5 1,087 86 40 8.63
10 8,760 0.8 85.7 10 8,760 0.8 90.9 1,289 97 45 9.09
15 8,760 0.8 87.2 15 8,760 0.8 91.5 1,689 120 56 9.58
20 8,760 0.8 88.6 20 8,760 0.8 91.8 1,983 116 53 11.72
25 8,760 0.8 89.4 25 8,760 0.8 92.8 2,381 150 69 10.84
30 8,760 0.8 90.2 30 8,760 0.8 93 2,760 145 67 13.01
40 8,760 0.8 90.3 40 8,760 0.8 93.8 3,684 243 113 10.35
50 8,760 0.8 91.1 50 8,760 0.8 93.9 4,275 236 109 12.37
60 8,760 0.8 91.0 60 8,760 0.8 94.3 5,068 341 158 10.14
75 8,760 0.8 91.6 75 8,760 0.8 94.4 5,893 351 162 11.49
100 8,760 0.8 91.6 100 8,760 0.8 94.8 7,716 543 251 9.71
125 8,760 0.8 92.1 125 8,760 0.8 94.9 9,314 605 280 10.52
150 8,760 0.8 93.3 150 8,760 0.8 95.5 10,555 556 257 12.97
200 8,760 0.8 93.0 200 8,760 0.8 95.4 12,518 782 361 10.94
77
Table 6.3: Analysis for TEFC enclosure type for motors
ODP Enclosure 25% Dealer Discount 12 months peak
Existing Proposed Analysis
hp Hours Load
factor Eff. hp Hours Load
factor Eff. Investment +
Installation
Energy
sav.
Dem
sav.
Pay
back
7.5 8,760 0.8 85.8 7.5 8760 0.8 90.1 711 62 29 7.81
10 8,760 0.8 87.8 10 8760 0.8 91 845 59 27 9.74
15 8,760 0.8 87.3 15 8760 0.8 91.8 1,061 123 57 5.9
20 8,760 0.8 88.4 20 8760 0.8 92.4 1,293 145 67 6.1
25 8,760 0.8 89.4 25 8760 0.8 92.9 1,561 153 71 6.95
30 8,760 0.8 90.1 30 8760 0.8 93.4 1,747 174 81 6.85
40 8,760 0.8 89.8 40 8760 0.8 93.9 2,488 282 130 6.04
50 8,760 0.8 89.3 50 8760 0.8 94 2,920 412 191 4.84
60 8,760 0.8 91.3 60 8760 0.8 94.6 3,468 331 153 7.15
75 8,760 0.8 91.7 75 8760 0.8 94.7 3,995 374 173 7.29
100 8,760 0.8 92.5 100 8760 0.8 94.8 4,779 379 175 8.62
125 8,760 0.8 92.4 125 8760 0.8 95 5,645 531 245 7.27
150 8,760 0.8 93 150 8760 0.8 95.2 6,427 554 256 7.92
200 8,760 0.8 93.1 200 8760 0.8 95.4 8,470 749 346 7.73
Table 6.4: Analysis for ODP enclosure type for motors
78
Replace Existing
)(Comparison of Enclosure Type
0
2
4
6
8
10
12
14
7.5 10 15 20 25 30 40 50 60 75 100 125 150 200
Motor Size (hp)
Payback Period (Yrs)
TEFC Enclosure ODP Enclosure
Figure 6.9: Comparison for the TEFC and ODP enclosure type
6.4.1.2 Analysis to measure the impact of the operating hours of the motor
The annual number of operating hours of the motor affects the replacement decision. This
analysis is performed for 2 shift and 3 shift operations of the plant, assuming that the motors
run continuously during the shift. This analysis is performed assuming the enclosure type as
TEFC and a load factor of 0.8. The results for the 3-shift operation, i.e. 8,760 hours are same
as that can be seen in the Table 6.3. The results for the 2- shift operation can be seen in the
Table 6.5 below. The analysis obviously suggests that the payback period for the 2-shift
operation is definitely bigger than the 3-shift operation. The payback period reduces around 2
to 3 years for each motor size when the annual operating hours increase to 8,760 hours. The
Figure 6.10 plots the results and shows the comparative payback periods obtained for the 2
shift and the 3 shift operations. This analysis gives an insight that in an energy management
program, first priority should be given to those motors, which run for more number of annual
operating hours. Actions on such motors will give attractive payback periods and quicker
energy savings.
TEFC Enclosure 25% Dealer Discount 12 months peak
Existing Proposed Analysis
hp Hours Load
factor Eff hp Hours Load
factor Eff Investment +
Installation
Energy
sav
Dem
sav
Pay
back
7.5 5,840 0.8 84.5 7.5 5,840 0.8 90.5 1,087 57 40 11.17
10 5,840 0.8 85.7 10 5,840 0.8 90.9 1,289 65 45 11.78
15 5,840 0.8 87.2 15 5,840 0.8 91.5 1,689 80 56 12.42
20 5,840 0.8 88.6 20 5,840 0.8 91.8 1,983 77 53 15.18
25 5,840 0.8 89.4 25 5,840 0.8 92.8 2,381 100 69 14.04
30 5,840 0.8 90.2 30 5,840 0.8 93 2,760 97 67 16.85
40 5,840 0.8 90.3 40 5,840 0.8 93.8 3,684 162 113 13.4
50 5,840 0.8 91.1 50 5,840 0.8 93.9 4,275 157 109 16.03
60 5,840 0.8 91.0 60 5,840 0.8 94.3 5,068 228 158 13.14
75 5,840 0.8 91.6 75 5,840 0.8 94.4 5,893 234 162 14.88
100 5,840 0.8 91.6 100 5,840 0.8 94.8 7,716 362 251 12.57
125 5,840 0.8 92.1 125 5,840 0.8 94.9 9,314 403 280 13.63
150 5,840 0.8 93.3 150 5,840 0.8 95.5 10,555 371 257 16.8
200 5,840 0.8 93.0 200 5,840 0.8 95.4 12,518 521 361 14.18
79
Table 6.5: Replacement analysis for a two-shift operation
Figure 6.10: Analysis for comparing different annual operating hours
6.4.1.3 Analysis to measure the impact of the existing efficiency of the standard motor
The Motor Master database provides the efficiency values of the standard efficiency motors
at various loads. These efficiency values are obtained from the data obtained from many
experiments on various sizes of the motors. In reality it is found during the assessments that
most of the existing motors are very old, some may be even 20 years old. The efficiency of
the existing motors decreases over their lifetime due to rewinding and also due to failures and
maintenance in between. The parts of the motor wear out and reduce the efficiency over a
longer period. This analysis takes this fact into consideration. It is assumed during the
analysis that the motors are of TEFC enclosure type and the load factor is assumed to be 0.8.
The analysis is performed for a three-shift operation. As can be seen in the Table 6.6, the
analysis is performed for the existing standard efficiency motors with a reduction in
80
Replace Existing Comparison for 2 & 3 shift operations
0
2
4
6
8
10
12
14
16
18
7.5 10 15 20 25 30 40 50 60 75 100 125 150 200
Motor Size (hp)
Payback Period (Yrs)
2 shift operation 3 shift operation
efficiency over the standard values available in Motor Master of about 3 %. This decrease in
efficiency by 3% has a substantial impact on the motor replacement decision.
The Table 6.7 shows an analysis for the existing standard motor replacement with standard
efficiency values 5 % less than that what are obtained from the Motor Master database. The
Figure 6.11 shows the comparison for all the three scenarios. The existing values in the
Motor Master and then with 3 % and 5 % reduction in the standard efficiency values of the
existing motors. It can be seen from the plot that the payback period decreases considerably
when the existing efficiency decreases by 3 % and 5%. It is seen that for the 3 % decrease,
the payback period reduces by around 3 years for the lower size motors and up to 6 years for
the higher size motors. For the 5 % decrease in standard efficiency, the payback period
reduces by around 4 years for the lower size motors and up to 7 years for the higher size
motors.
This analysis gives some very crucial insights into the replacement decision. It proves the
efficiency of the existing motors plays a very important role in the decision making process.
Older and long used motors, which are already subject to many rewinding and other
maintenance operations, should be attacked first and given high priority over the other
motors in the plant. Also when making a replacement decision, the older but higher sized
motors should be given higher priority over the smaller sized motors, as they will payback
faster if they are replaced with energy efficient motors of the same size.
TEFC Enclosure 25% Dealer Discount 12 months peak
Existing Proposed Analysis
hp Hours Load
factor Eff Eff hp Hours Load
factor Eff Investment +
Installation
Energy
sav
Dem
sav
Pay
back
7.5 8,760 0.8 84.
5
81.5 7.5 8,760 0.8 90.5 1,087 134 62 5.54
10 8,760 0.8 85.
7
82.7 10 8,760 0.8 90.9 1,289 159 73 5.54
15 8,760 0.8 87.
2
84.2 15 8,760 0.8 91.5 1,689 209 97 5.52
20 8,760 0.8 88.
6
85.6 20 8,760 0.8 91.8 1,983 230 106 5.9
25 8,760 0.8 89.
4
86.4 25 8,760 0.8 92.8 2,381 293 135 5.56
30 8,760 0.8 90.
2
87.2 30 8,760 0.8 93 2,760 312 144 6.04
81
40 8,760 0.8 90.
3
87.3 40 8,760 0.8 93.8 3,684 466 215 5.41
50 8,760 0.8 91.
1
88.1 50 8,760 0.8 93.9 4,275 510 236 5.73
60 8,760 0.8 91.
0
88.0 60 8,760 0.8 94.3 5,068 668 309 5.19
75 8,760 0.8 91.
6
88.6 75 8,760 0.8 94.4 5,893 761 352 5.29
100 8,760 0.8 91.
6
88.6 100 8,760 0.8 94.8 7,716 1081 500 4.88
125 8,760 0.8 92.
1
89.1 125 8,760 0.8 94.9 9,314 1264 584 5.04
150 8,760 0.8 93.
3
90.3 150 8,760 0.8 95.5 10,555 1333 616 5.41
200 8,760 0.8 93.
0
90.0 200 8,760 0.8 95.4 12,518 1848 854 4.63
Table 6.6: Analysis with 3 % reduction in standard efficiency of the existing motors
TEFC Enclosure 25% Dealer Discount 12 months peak
Existing Proposed Analysis
hp Hours Load
factor Eff Eff hp Hours Load
factor Eff Investment +
Installation
Energy
sav
Dem
sav
Pay
back
7.5 8,760 0.8 84.
5
79.5 7.5 8,760 0.8 90.5 1,087 168 78 4.42
10 8,760 0.8 85.
7
80.7 10 8,760 0.8 90.9 1,289 203 94 4.34
15 8,760 0.8 87.
2
82.2 15 8,760 0.8 91.5 1,689 272 126 4.24
20 8,760 0.8 88.
6
83.6 20 8,760 0.8 91.8 1,983 312 144 4.35
25 8,760 0.8 89.
4
84.4 25 8,760 0.8 92.8 2,381 393 182 4.14
30 8,760 0.8 90.
2
85.2 30 8,760 0.8 93 2,760 430 199 4.38
40 8,760 0.8 90.
3
85.3 40 8,760 0.8 93.8 3,684 623 288 4.04
50 8,760 0.8 91.
1
86.1 50 8,760 0.8 93.9 4,275 703 325 4.15
60 8,760 0.8 91.
0
86.0 60 8,760 0.8 94.3 5,068 900 416 3.85
75 8,760 0.8 91.
6
86.6 75 8,760 0.8 94.4 5,893 1048 484 3.84
100 8,760 0.8 91.
6
86.6 100 8,760 0.8 94.8 7,716 1462 676 3.6
125 8,760 0.8 92. 87.1 125 8,760 0.8 94.9 9,314 1735 802 3.67
82
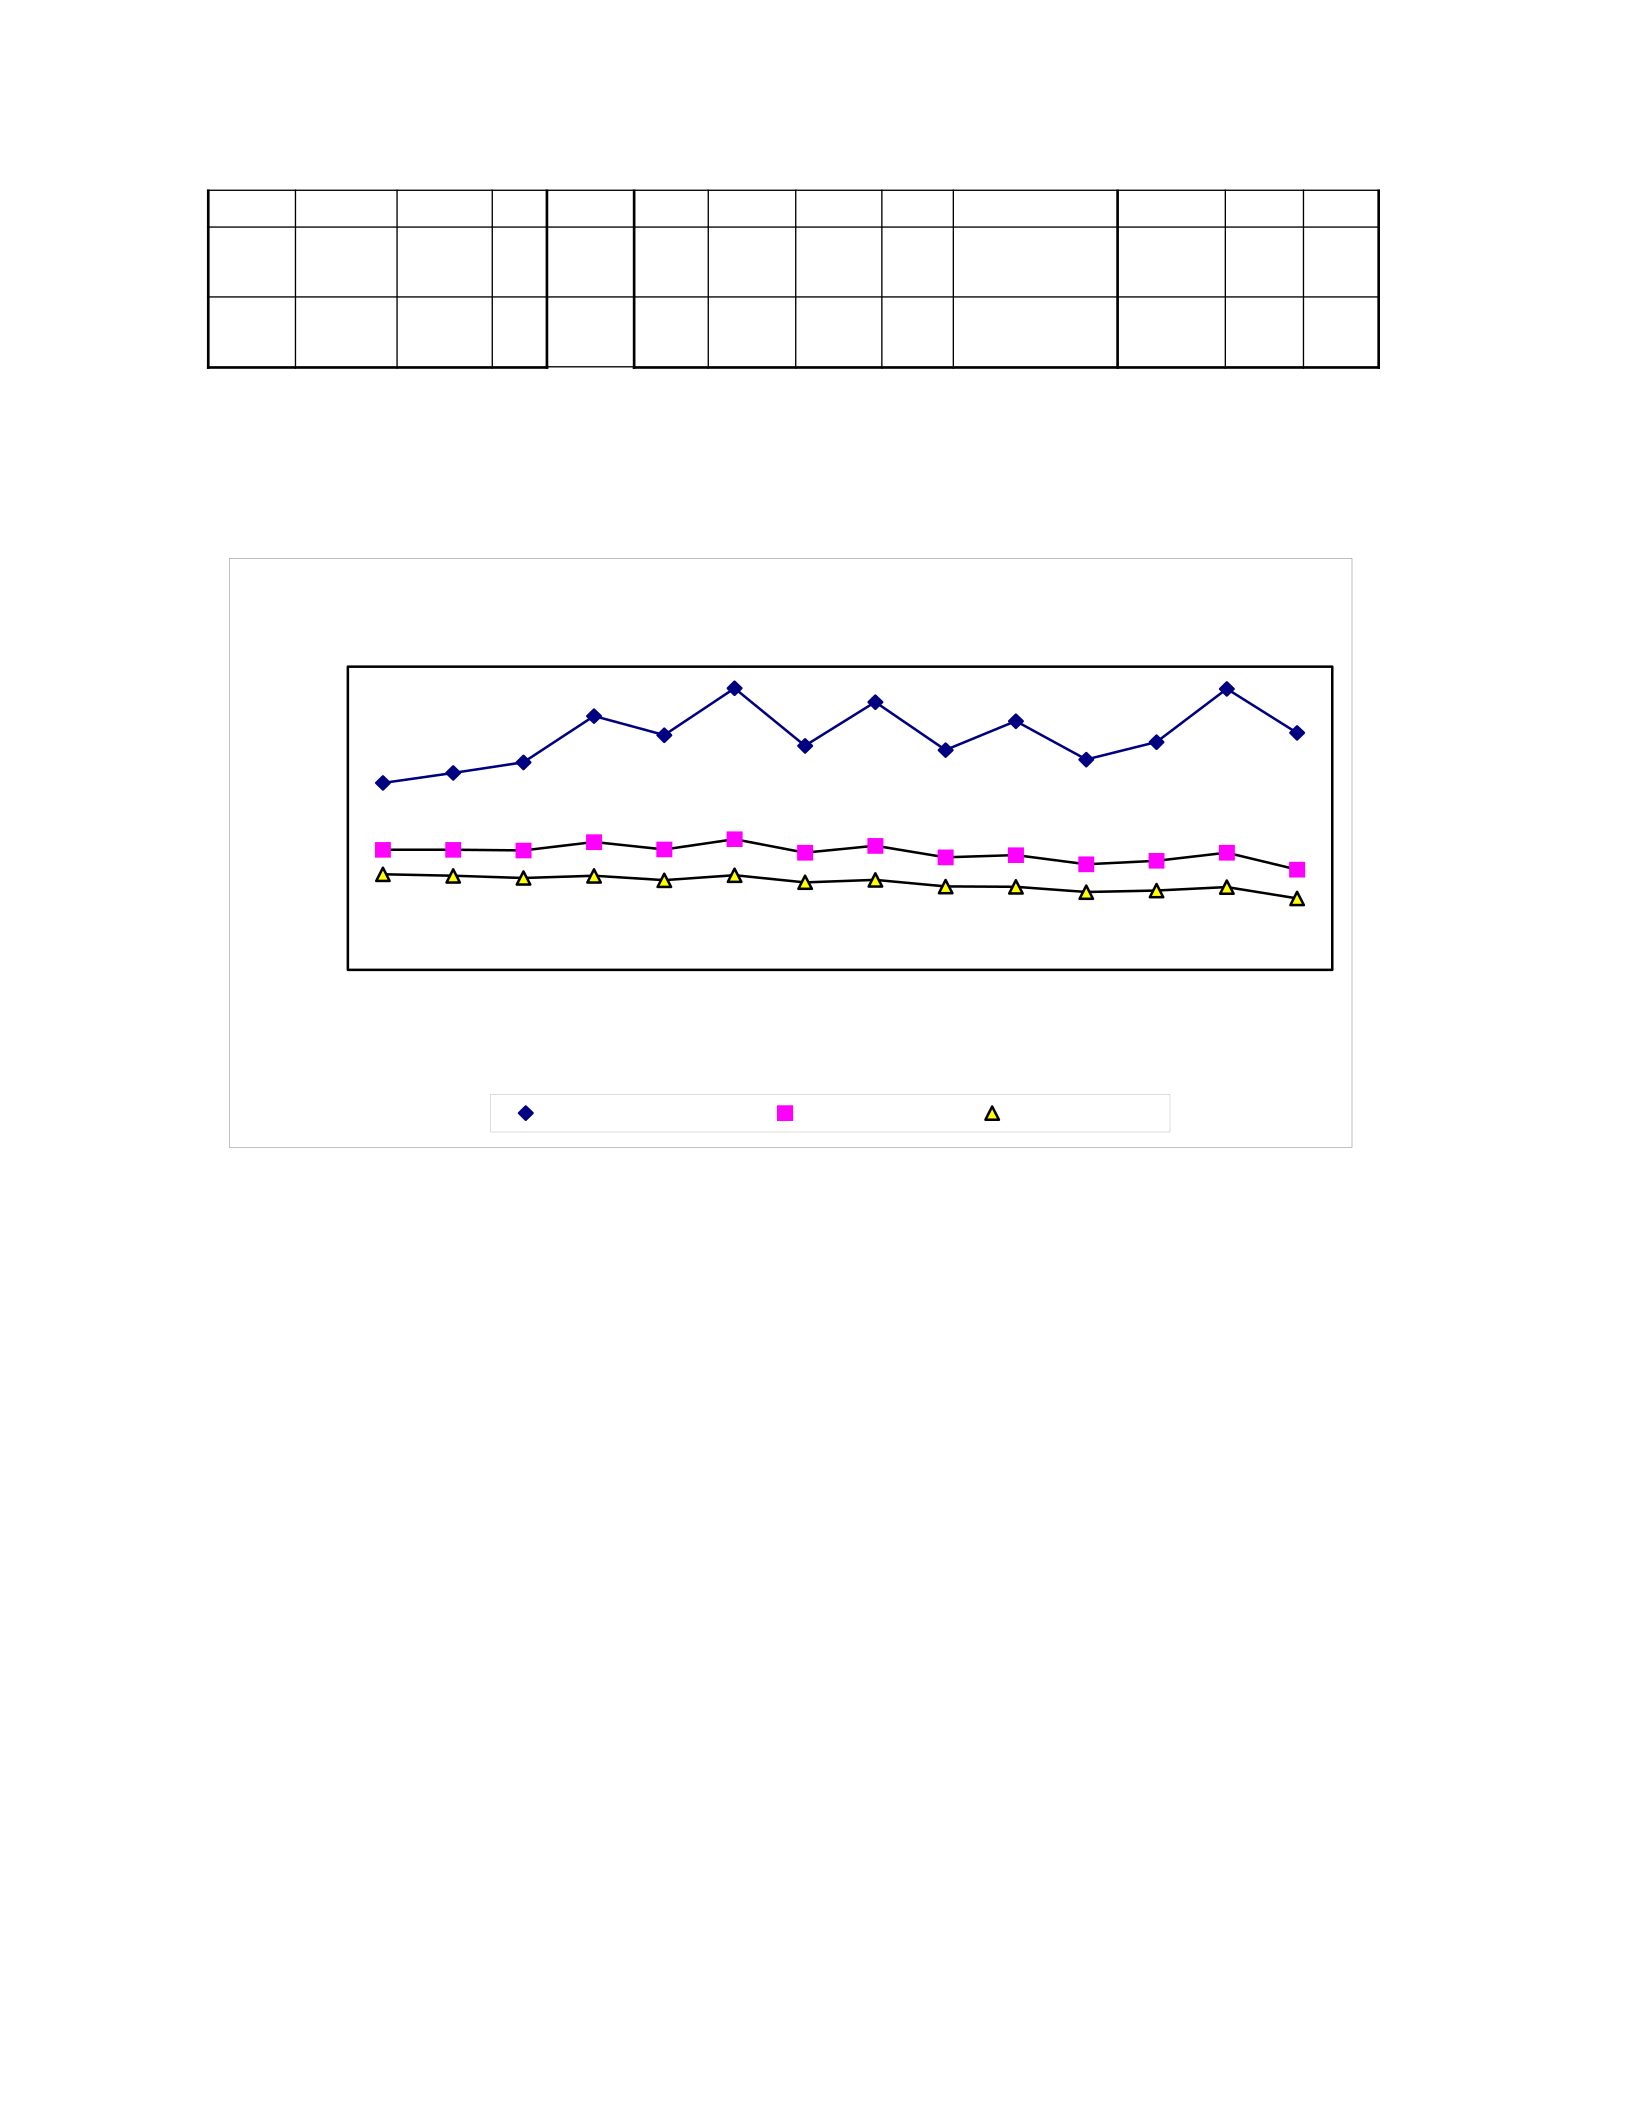
1
150 8,760 0.8 93.
3
88.3 150 8,760 0.8 95.5 10,555 1883 871 3.83
200 8,760 0.8 93.
0
88.0 200 8,760 0.8 95.4 12,518 2587 1196 3.3
Table 6.7: Analysis with 5 % reduction in standard efficiency of the existing motors
Figure 6.11: Comparison of different existing standard efficiencies
6.4.1.4 Analysis for downsizing the existing motors to their appropriate required size
This analyzes the cost effectiveness of replacing an operable standard efficiency motor with a
new energy efficiency motor of smaller size. This analysis is used when there is an
opportunity for downsizing that particular existing standard motor. The compare module in
Motor Master is used again for the analysis, except that the value of the energy efficient
motor is changed to the appropriate rating. The extent to which downsizing is required
depends on the existing load conditions and also the process requirements in future. The
savings are calculated on the basis of which energy efficient motor is selected for down
sizing. This analysis is also performed for two values of efficiency for the existing motors.
83
Replace Existing Comparison for different std. Eff.
0
2
4
6
8
10
12
14
7.5 10 15 20 25 30 40 50 60 75 100 125 150 200
Motor Size (hp)
Payback Period(Yrs)
Std. Existing Eff. 3% less Eff. 5% less Eff.
First scenario is with the default values of efficiency obtained from Motor Master and the
other scenario is assuming 3 % reduction in efficiency of the existing motors.
As can be seen in the Table 6.8, the analysis is performed for all the motors with a TEFC
enclosure and 3-shift operation. The load factor of the existing motors which are considered
for downsizing is assumed to be 0.4, as the load – efficiency curves show a steep dissent in
efficiency below 40 % load. It can be seen from the Table 6.8, that the payback period has
definitely improved because of downsizing the motors to their appropriate size as compared
to replacing existing motors with the same size energy efficient motors. Table 6.9 shows the
analysis for downsizing with 3 % decrease in the standard efficiency of the existing motors.
As earlier the impact of decreased efficiency of the existing motors can be reflected in the
payback periods. The payback periods reduce by around 3 to 4 years for different sizes of the
motors due to the decrease in efficiency. This fact is also seen in the plot drawn in the Figure
6.12 below. Thus it can be said that downsizing motors to their appropriate size definitely is a
better option and it also improves the power factor of the motors. Another thing is that the
older lower efficiency existing motors should be given higher priority over new ones when
replacement decisions are to be considered. The downsizing decision should be carefully
taken. The possible candidate motor should be subject to continuous load test and at different
time intervals to make sure that the motor is over sized for the application. While selecting an
energy efficient motor for downsizing, care should be taken with regards to the speed of the
motor and the torque requirements.
TEFC Enclosure 1200 rpm 25% Dealer Discount 12 months peak
Existing Proposed Analysis
hp Hours
Load
factor Eff hp Hours
Load
factor Eff
Investment +
Installation
Energy
sav
Dem
sav
Pay
back
15 8,760 0.4 83.5 7.5 8,760 0.8 90.5 1,087 102 47 7.27
20 8,760 0.4 86.3 10 8,760 0.8 90.9 1,289 85 39 10.42
25 8,760 0.4 85.6 15 8,760 0.67 91.5 1,689 138 64 8.38
30 8,760 0.4 86.9 15 8,760 0.8 91.5 1,689 129 59 8.97
40 8,760 0.4 87.0 20 8,760 0.8 91.8 1,983 176 81 7.7
50 8,760 0.4 88.7 25 8,760 0.8 92.8 2,381 184 85 8.85
60 8,760 0.4 87.4 30 8,760 0.8 93 2,760 302 140 6.24
75 8,760 0.4 89.0 40 8,760 0.75 93.9 3,684 318 147 7.91
84
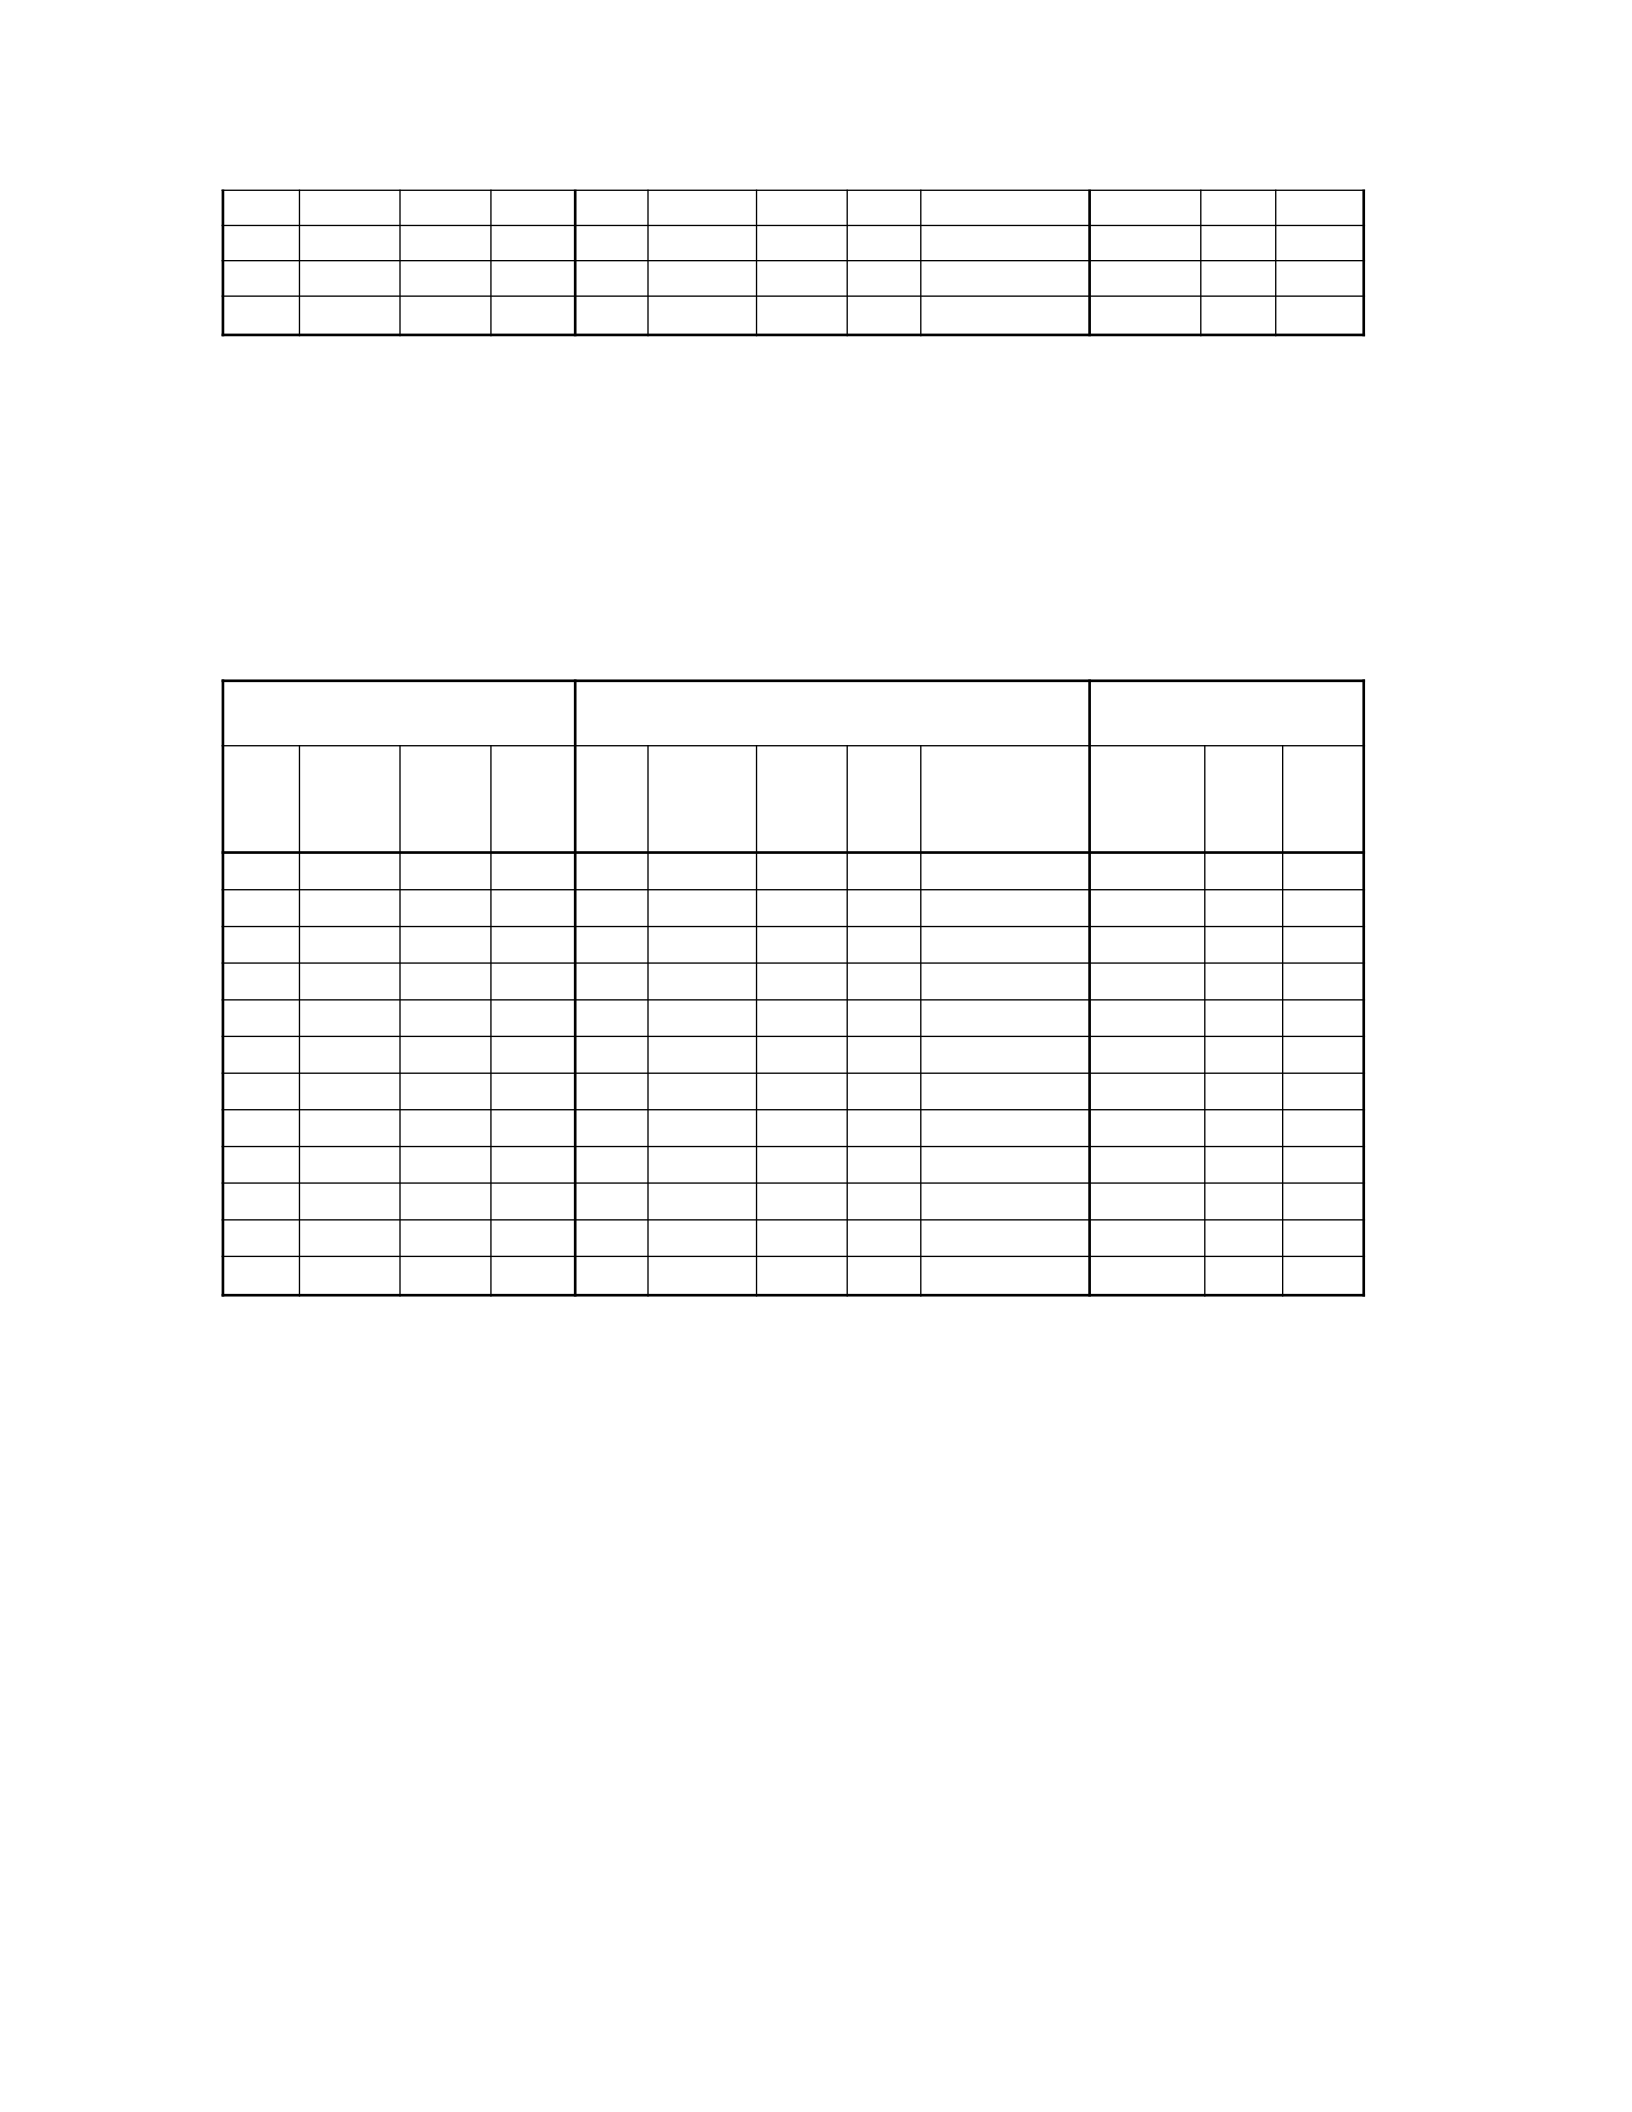
100 8,760 0.4 88.2 50 8,760 0.8 93.9 4,275 504 233 5.8
125 8,760 0.4 89.5 60 8,760 0.83 94.3 5,068 514 238 6.73
150 8,760 0.4 91.9 75 8,760 0.8 94.4 5,839 317 147 12.69
200 8,760 0.4 90.9 100 8,760 0.8 94.8 7,716 671 310 7.85
Table 6.8: Downsizing analysis for default efficiency values for existing motors
TEFC Enclosure 1200 rpm 25% Dealer Discount 12 months peak
Existing Proposed Analysis
hp Hours Load
factor Eff hp Hours Load
factor Eff Investment +
Installation
Energy
sav
Dem
sav
Pay
back
15 8,760 0.4 80.5 7.5 8,760 0.8 90.5 1,087 151 70 4.92
20 8,760 0.4 83.3 10 8,760 0.8 90.9 1,289 146 68 6.03
25 8,760 0.4 82.6 15 8,760 0.67 91.5 1,689 215 100 5.36
30 8,760 0.4 83.9 15 8,760 0.8 91.5 1,689 218 101 5.29
40 8,760 0.4 84.0 20 8,760 0.8 91.8 1,983 295 136 4.59
50 8,760 0.4 85.7 25 8,760 0.8 92.8 2,381 327 151 4.97
60 8,760 0.4 84.4 30 8,760 0.8 93 2,760 479 222 3.93
75 8,760 0.4 86.0 40 8,760 0.75 93.9 3,684 534 247 4.71
100 8,760 0.4 85.2 50 8,760 0.8 93.9 4,275 793 366 3.68
125 8,760 0.4 86.5 60 8,760 0.83 94.3 5,068 872 403 3.97
150 8,760 0.4 88.9 75 8,760 0.8 94.4 5,839 720 333 5.6
200 8,760 0.4 87.9 100 8,760 0.8 94.8 7,716 1212 560 4.35
Table 6.9: Downsizing analysis for 3% reduced efficiency values for existing motors
85
Figure 6.12: Comparison for different values of efficiency for downsizing
6.5 Conclusions
This chapter gives a good insight into the various parameters in the motor
replacement decision-making process. It discusses the various possibilities with new motor
purchase decisions. The comparison for rewinding and new motor purchase decision is also
discussed. In the replacement analysis, various parameters like annual operating hours, motor
enclosure types and efficiency of the existing standard motors are subject to a sensitivity
analysis and their impact on the payback period and replacement decision are made. Thus
after enough load testing of the motors in the plant, the user can use the compare module of
the Motor Master and run different scenarios and come to a wise decision on replacing the
existing standard motor.
Another field of interest connected to the proper working of the motor systems is the
drive belts on these systems. There are losses encountered during transmission of the power
from the motor shaft to the other parts in the system due to use of belts and pulleys. Next
chapter discusses the use of energy efficient belts in motor transmission systems.
86
Downsizing comparison for different std. Eff.
0
2
4
6
8
10
12
14
0 50 100 150 200 250
Motor Size (hp)
Payback Period (Yrs)
Existing Efficiency 3 % less Eff.

Chapter 7
Replace Drive Belts On Large Motors with Energy Efficient Cog Belts
Efficient belt drive systems along with appropriately sized energy efficient motors
make a motor system really efficient. Only having energy efficient motors in the plant will
not help if the belt drive systems used to transfer power are not efficient. V belts have been
traditionally used for power transmission. But recent developments in the field of belt
transmission have given rise to many efficient belt drives, which are very energy efficient
when compared to the standard available belts. This chapter discusses the use of these cog
belt drives in the wood manufacturing industry and also includes a sensitivity analysis on the
crucial parameters of the energy savings equation which affect the energy savings.
7.1 Introduction to cog belt drives
In addition to internal inefficiencies in electric motors, which cause energy loss, the
power available at the drive shaft of the motor cannot be transmitted to a machine through a
belt without some additional energy losses. These losses come in the form of slippage, energy
used to flex the belt as it goes around pulleys, and stretching and compression of the belt. A
recent study has shown that V belts have a maximum efficiency of about 94%. This means
that 94% of the energy transferred to the drive shaft of the electric motor is transferred to the
machinery performing the useful industrial task [41].
There are two readily available means to reduce the losses. One is to replace the belts
with energy efficient cog belts. These belts slip less and can bend more easily that standard V
belts. The other method is to use belts with teeth and also replace the pulleys with ones that
87

have sprocket grooves (essentially installing a “ timing chain”), which is referred to in
industry as a high torque drive belt (HTD). In both cases, the belt can bend with less loss of
energy and need not be stretched as tightly as the standard V belt, which in turn prolongs belt
life. The cog belts also reduce slippage. Following are the factors, which affect the efficiency
of a V belt or for that matter any power transmission belt [41].
7.1.2 Friction
The transfer of power in a belt drive relies critically on friction. The tensions in the
two strands (the nominally straight parts of the belt not in contact with the pulleys) cause a
normal pressure over the belt- pulley contact, and it is the corresponding distributed friction
whose moment about the pulley centre equilibrates the shaft torque provided gross slip of the
belt on the pulley surface does not occur due to friction breakaway. Ideally, for belts, the
torque amplification ratio is equal to the radius ratio, so that the output power equals the input
power and the efficiency is 100%. However sliding friction results in a torque ratio which is
less than ideal. A real belt drive is just the opposite - the torque ratio equals the ideal ratio, but
creep results in the speed ratio being less than ideal. Creep - not to be confused with gross
slip - is due to belt elements changing length as they travel between the maximum and the
minimum tensions, and since the pulley is rigid then there must be relative motion between
belt element and pulley. Since power equals the product of torque and (angular) speed, the
consequence of the foregoing is that efficiency of belts is less than 100%.
7.1.3 Sheave Diameter
While a sheave change may not be possible, in general, the larger the sheave, the
greater the drive efficiency. The V belt is subjected to large compression stresses when
confirming to sheave diameter. The cog belt has less material in the compression section of
the belt, thereby minimizing rubber deformation and compression stresses. The result is
higher operating efficiency for the cog belt.
7.2 Advantages of cogged V belts over conventional V belts
They are more energy efficient as compared to conventional belts. (up to 6% more
efficient than conventional belts)
88
Cogged belts bend more easily as compared to the conventional belts.
As the cogged belts have slots perpendicular to the belt length, they exhibit reduced
friction losses.
Cogged belts run cooler as compared to conventional belts because of their lower energy
absorption.
Cogged belts last 20 to 30% longer than conventional V belts.
They reduce power transmission losses.
They reduce slippage.
7.3 Current Practice and Observations in Wood Industry
It is found in the audits so far, that most of the big size motors in Wood Industry in
West Virginia use standard V belts. Almost every plant has an opportunity here to replace the
existing V belts with energy efficient cog belt drives. Following is the example on the data
and analysis for facility A. Currently, some of the belt motors are using standard V-belts to
transmit power resulting in an unnecessary loss of energy. The list of all the big motors in
facility A was obtained during the audit. The list can be seen in the Table 7.1 below.
MILL MOTORS
hp
Conveyor Motor 7.5
Conveyor Motor 10
Conveyor Motor 15
Conveyor Motor 15
Conveyor Motor 7
Chipper Motor 150
Compressor Motor 40
Conveyor Motor 3
Conveyor Motor 55
Saw dust Motor 10 x 10
Saw dust Motor 15 x 3
Saw dust Motor 75
Saw dust Motor 15
Saw dust Motor 15 x 2
89
Debarkers 165
Table 7.1: List of motors for facility A
7.4 Recommended Action
Replace standard wrapped V-belts with energy efficient cog belts on the respective
drive systems. Only those motors with a horsepower rating of three or greater will be
considered for belt replacement. Motors less than three horsepower provide inadequate
payback justification and, hence, are not considered. The relevant data on the horsepower
ratings for all the belt drive systems in the plants was collected and used for further analysis.
7.5 Anticipated Savings
Many studies in the literature have shown that a typically well-maintained industrial
Vbelt is about 92% efficient. Field tests of cog belts for both large and small drives show
gains in efficiency from 2.0% to 4.5%. For our calculations, we will use the value of 4.0%.
We can calculate the yearly energy savings as shown in the following equation.
ES = Σhp/η x LF x H x S
where:
ES = The anticipated energy savings (Btu/yr)
Σhp = The total horsepower for the large motors using standard V-belts in the
plant. This is estimated to be 981.5 hp based on the audit information
acquired.
η = The average efficiencies of the motors
LF = The average load factor, assumed to be 80% based on industry
averages. H = The annual operating time calculated as 90% of the annual plant
operating time. This is determined by (0.9 x 2340 hrs/yr = 2106 hrs/yr).
S = The estimated energy savings (taken here as 4.0% for cog belts)
Therefore for cog belts, energy savings are calculated as follows:
90

ES = (981.5/0.86) x (2,545 Btu/hp) x 0.8 x 2106 x 0.04
= 195.74 MMBtu/yr
The associated cost savings would be: Savings
= 195.74 MMBtu/yr x $21.95 / MMBtu
= $4,296.58
7.6 Implementation & Payback
The installation of new cog belts could be carried out by maintenance personnel. The
capital cost required would be about $25 per drive. There are 52 belt drive systems, which
should be changed. Therefore, the implementation cost would be:
Implementation Cost = 52 x 25
= $1,300
Based on the above implementation cost of $1,300 and energy cost savings of
$4,296.58, the simple payback period for this recommendation is four months.
7.7 Sensitivity analysis for cog belt drives
A sensitivity analysis of the savings achieved by replacing the conventional V belts
with cog V belt drives is done. The sensitivity is done with respect to two most important
factors of the equation that affect the annual savings obtained. Other factors like the percent
savings obtained are not considered for sensitivity analysis, as it is obvious that with increase
in savings percentage the energy savings will increase. This sensitivity analysis is performed
by varying only one important parameter in the equation and then the impact of that varied
parameter is measure and analyzed. Like wise all the parameters are varied keeping all others
constant and the sensitivity analysis is performed. The key parameters are varied within a
practical range for the purpose of the analysis so as to measure the impact on the energy
savings obtained. This analysis here is performed for the data collected from facility A, the
analysis for other plants can be found in Appendix IV.
These factors are:
91
Efficiency of motors
Load factor of the motors or the drive system
hp Eff. LF H S ES Cost Savings
Sensitivity with respect to efficiency of motors
981.5 0.7 0.8 2,106 4.00% 240.49 5,279
981.5 0.74 0.8 2,106 4.00% 227.49 4,993
981.5 0.78 0.8 2,106 4.00% 215.82 4,737
981.5 0.82 0.8 2,106 4.00% 205.29 4,506
981.5 0.86 0.8 2,106 4.00% 195.74 4,297
981.5 0.9 0.8 2,106 4.00% 187.04 4,106
981.5 0.94 0.8 2,106 4.00% 179.08 3,931
Sensitivity with respect to load factor
981.5 0.86 0.3 2,106 4.00% 73.40 1,611
981.5 0.86 0.4 2,106 4.00% 97.87 2,148
981.5 0.86 0.5 2,106 4.00% 122.34 2,685
981.5 0.86 0.6 2,106 4.00% 146.81 3,222
981.5 0.86 0.7 2,106 4.00% 171.28 3,760
981.5 0.86 0.8 2,106 4.00% 195.74 4,297
Table 7.2: Sensitivity analysis for cog belt drives
7.7.1 Sensitivity with respect to Efficiency of motors
This analysis is done by changing the value of the efficiency of motors in the energy
savings equation and keeping all other parameters of the equation constant. The efficiency of
the motors is varied from 70% to 94%. The efficiency value of a typical standard old motor is
70%, while 94% is the efficiency of a typical new energy efficient motor. That’s the reason
above range is selected for the analysis. As seen in the Figure 7.1, the total savings obtained
decrease with an increase in the efficiency value of the motor. There is a decrease in the total
savings because, the efficiency of the motor appears in the denominator of the energy savings
92
equation. This means that if the plant has electric motors in the high efficiency range say
above 90 %, then this recommendation will result in less cost savings. But when the motors
are standard and old, the efficiency is very low, then there is a potential for a large saving. As
seen in the Table 7.1, when the average efficiency of the motors is 70%, the annual cost
saving obtained is $ 5,279. Also at an efficiency of 94%, the annual saving is $ 3,931.
Figure 7.1: Sensitivity with respect to Efficiency of motor
7.7.2 Sensitivity with respect to the load factor of the motors
If the load factor of the motor changes, the efficiency of the motor changes along with
it. If the motor load factor decreases, then the efficiency of the motor also decreases and if the
motor load factor increases, this efficiency increases up to 75% to 80% load factor. But here
the sensitivity analysis is performed considering a load factor change without any change in
the efficiency of the motor. To get a better insight of the impact of the motor load factor on
the energy saved, the efficiency value of the motor is assumed to be constant at 0.86. This
value is midway through the efficiency range of a standard efficiency motor. The maximum
efficiency of a motor would be around 95 % at full load or at 77 % load, and the efficiency
93
1,500
2,000
2,500
3,000
3,500
4,000
4,500
5,000
5,500
0.6 0.65 0.7 0.75 0.8 0.85 0.9 0.95 1
Efficiency of Motor
Cost Savings
drops to around 75% if the motor load drops below 50%. So 86% efficiency is assumed here
as constant for the change in load.
As seen in the Table 7.1, the load factor of the motor driven systems is varied from
0.3 to 0.8 keeping all other parameters in the savings equation constant. The load factor range
of 0.3 to 0.8 is selected at it is the typical range for most of the motor driven systems in an
industrial set up. The load factor directly affects the total savings obtained. Load factor of
30%, means that the amount of stresses on the belt transmission is less as compared to those
at 80%. So there is a steady increase in the cost savings achieved when the load factor is
increased in that range. As can be seen in the 7.1, at a load of 0.3, the net savings obtained are
$ 1,611, while for a load factor of 0.8, the net savings obtained are $4,297. This is also seen
in the Figure 7.2, which shows a steady increase in the annual cost savings due to
maintaining a higher load factor in the plant.
Figure 7.2: Sensitivity with respect to Load factor of motor
7.8 Application considerations
Replacing the existing standard V belts with energy efficient cog belts should be done
very judiciously. Although cog belts are energy efficient and result in cost savings, they may
not be compatible with the process requirements in some cases. Applications or processes,
which require accurate timing, may not be suitable for a cog belt installation. Also
94
0
500
1,000
1,500
2,000
2,500
3,000
3,500
4,000
4,500
5,000
0.2 0.3 0.4 0.5 0.6 0.7 0.8 0.9
Load factor
Cost Savings

applications, which constantly run at low load, may not be a favorable candidate for cog
belts. Cog belts have been known to create problems at especially low loads. Also there are
some processes that require some slip in the process and the cog belts may not be the right
solution for that. So, before replacement of the standard V belts all these considerations
should be taken into account.
7.9 Conclusions
Use of energy efficient cog belts definitely result in energy savings. The standard V
belts should be replaced with careful consideration to the different application considerations
for each particular situation. As can be seen in the sensitivity analysis performed on the
important parameters of the energy savings equation, it is seen that load factor and efficiency
of the motor systems does play a very significant role in determining the energy savings and
hence the payback period for the investment in cog belt drives.
95

Chapter 8 Summary and comparisons for the assessment findings
The previous chapters discussed the various tools and the analysis conducted during
the assessments conducted in the wood manufacturing industry. The summary of the data
collected and the results are compared across all the plants visited. A comparison matrix of all
the plants across some measured parameters is constructed and discussed in this chapter. A
brief description of each plant is also prepared so as to get a better insight into the results.
Specific energy consumption for different parameters is also calculated and plotted for further
analysis.
8.1 Description of each facility visited
Seven wood manufacturing industries in West Virginia were audited. Each plant had
its own special characteristic. Some general information about the operating hours, special
processes, special energy consumption areas in the plant are discussed here.
8.1.1 Facility A
A manufacturing facility located in Preston County, West Virginia produces quality
wood boards from logs. The plant uses only electrical energy and no oil or natural gas. The
major component of this electrical load is contributed by electric motors. This facility has 75
employees and the average production is 35 mbf (thousand board feet) of lumber per day. A
brief description of the plants manufacturing process is described here. It is not intended to be
a complete detailed description, but rather to provide general information on the processes,
with a focus on energy requirements. Saw logs are trucked in to the plant by the logger
96

contracted to haul them from the harvest site. Logs are stored in the area outside the plant and
initial inspection and sorting is done. They are then fed to the debarker where the bark is
abraded off. With the help of a material handling system they are sent to the Head saw where
sideboards are cut off from the cant. The cant is then cut into desired dimensions. The boards
proceed on a conveyor to the edger where smooth parallel edges are rendered on to the logs.
The Trimmer then cuts the boards to square and precise lengths. The boards are then sent to
grading and then final sorting and storage. The lumber is then packaged by grade and length
and shipped via trucks. Waste is created at every stage in the process, which is in the form of
sawdust and chips of wood. The waste generated is later on collected through conveyors and
sold out. This facility works on a one shift and 5 days a week schedule for 52 weeks a year.
8.1.2 Facility B
B is located in Riverton, West Virginia produces quality wood boards from logs. The
plant uses only electrical energy and no oil or natural gas. The major component of this
electrical load is contributed by electric motors. This facility has 60 employees and the
average production is 18.5 mbf (thousand board feet) of lumber per day. The manufacturing
process for this plant is very similar to that of previously discussed facility A, where in logs
come in at the debarker and the boards are edged and trimmed to required dimensions and
then sent for grading. This facility works 2 shifts and 5 days a week schedule for 52 weeks a
year.
8.1.3 Facility C
Facility C is located in Mt. Storm, West Virginia produces quality wood boards from
logs. The plant uses only electrical energy and no oil or natural gas. The major component of
this electrical load is contributed by electric motors. This facility has 60 employees and the
average production is 18 mbf (thousand board feet) of lumber per day. The manufacturing
process of this plant is same as facility C. This facility works 2 shifts and 5 days a week
schedule for 52 weeks a year.
97

8.1.4 Facility D
The principal product of facility D in Webster Sprigs, WV is rough lumber. The raw material
used is logs from different tree spices. The company has 91 employees. Annual sales for this
company are approximately seven million dollars. A simplified description of the
manufacturing processes performed at this facility is as follows which is slightly different
from the earlier plants. Logs are received and stored in the yard. Logs are then debarked and
moved to the band saw into slabs. The cut slabs are then edged, trimmed and graded. A
portion of the graded lumber is shipped directly to the customer, while some lumber goes to
the kiln for drying and is graded and prepared for shipment. Among other energy consuming
equipment this facility has two drying kilns with a steam boiler.
8.1.5 Facility E
The principal product of facility E, Mount Hope, WV is lumber, wood, and wood pellet fuel.
The raw materials are logs and saw dust. The company has 53 employees. Annual sales for
the facility are approximately $9.5 million. The plant operates for 2 shifts for 5 days a week,
52 weeks a year. The plant is broken down into two production areas. In the first area, the
raw material is logs. These logs are debarked and then sawed into boards. In the second
area, the raw material is the sawdust from the lumber mill, augmented by purchased sawdust.
The second process produces pellet fuel by extruding sawdust into small pellets. The final
products are then inspected, packaged, and shipped.
8.1.6 Facility F
The principal product of facility F, Bartow, WV is rough sawn lumber and kiln dried
lumber. The total employees at this plant are around 185 and there is one 10-hour production
shift 5 days a week, 52 weeks a year. Average production of lumber is around 400 mbf per
week. Along with the conventional lumber manufacturing set up from debarker to grading
this facility also has 16 dry kilns and 12 dehumidifiers. Some portion of the lumber is sent to
dry kilns for drying. The dehumidifiers remove the humidity in the lumber at the same time
dries it. There is a dehumidification refrigeration compressor on each dehumidifier. The
facility also has 1 sawdust boiler and 2 oil boilers for dehumidification kilns. On an average
60 % of green lumber obtained after grading is sent to dry kilns.
98

8.1.7 Facility G
Facility G is situated in Spencer, WV. The principal product of this company is
pressure treated industrialized timber. There are around 75 employees at this plant and it runs
on 2 shifts for 5 days a week, 52 weeks a year. The treatment plant runs in all the three shifts
and is the major energy consumer of the facility. This plant is different from all the above
plants discussed so far. The raw material is in the form of sawn square logs and it is further
trimmed and graded at the plant. Further it is treated in a treatment plant on the site.
Treatment of the trimmed logs is a 20 to 24 hour process. The company produces these
treated logs for rail tiers. The plant also produces compound posts as per the requirement
from the customers. There are two boilers in the treatment plant, one sawdust boiler and other
is a gas boiler, which is a backup for the first boiler.
8.2 Comparison matrix for the facilities visited
A comparison matrix of the various parameters measures and analyzed during the
assessment is made so as to get a better insight into the operations of each facility as regards
to energy. The various parameters, which are compared, are general information about the
plant, the utility bill analysis for each plant and then the demand sensitivity analysis details.
Also some specific energy consumption indicators are calculated for each plant visited. The
comparison matrix can be seen in the Table 8.1.
8.2.1 General information
The parameters compared under this heading are the location of the plant, the total
number of employees in the plant, the average annual production of the plant in mbf (1,000
board feet), and the operating hours of the plant. The total number of employees is mentioned
so as to get an idea of the labor productivity in the plant. The average annual production
values are used for calculating the various specific energy consumption parameters down in
the table.
As can be seen in the Table 8.1, the general information on the plants A to G is
mentioned. The plants normally operate in one or two shift operations. Also can be seen in
the table, the total number of employees is below 100 except for plant F that is a big
99

operation and has 185 employees. Also it is seen that the average annual production of
lumber in mbf is very high for plants E, F and G. These plants have very high capacity and
large product range.
8.2.2 Utility bill analysis parameters
The various parameters, which are compared under utility bill analysis, are utility rate
schedule, which applies to each facility, and all electrical parameters like kW demand, kWh
usage, total electricity charges of the plant, demand as a percent of the total electrical costs,
the load factor of the plants, the power factor correction and the average MMBtu cost for the
facility.
As can be seen in the Table 8.1, the rate schedules are for two utility service providers in the
state. Allegheny Power (ALP) and American Electric Power (AEP). Each facility has its own
rate schedule, which has its own way of calculating the demand cost, usage cost, power
factor and the total electricity costs. Also it can be seen that the plant F has a huge annual
peak demand recorded as compared to the other facilities. As mentioned earlier, the plant F
has 16 dry kilns and 12 dehumidifiers in addition to the conventional lumber manufacturing
set up. This is the reason why it reflects a high demand during the year. Also it can be seen in
the Table 8.1, the demand cost is not calculated for each plant. The demand cost calculation
depends on the utility rate schedule. Some schedules calculate the demand and usage cost
separately while others include all the costs under usage cost. As a result the demand as a
percent of the total energy charges is not obtained for all the plants covered. It can be seen in
the table that the plant A has the maximum demand as a percent of total electricity charges,
which is around 60 %.
The load factor is calculated for each plant. The load factor of the plant depends on the
number of operating shifts for the plant. So for a plant running for 1 shift the industrial plant
average is 37%, while for a 2-shift operation it is around 72 %. So while analysis the load
factor of the plant, the operation hours of the plant should be kept in mind so as to make a
comparison with the industrial average.
The average kW demand, the minimum demand and the maximum demand recorded during
the year are also mentioned for each plant. The difference between the maximum and the
average demand and the difference between the maximum and minimum demand gives a fair
100

idea of the possibility of leveling the load curve around the average. The power factor
correction is not required for each plant. Overall it is observed that the plants maintain a very
good power factor and there are no power factor penalties. As can be seen in the table, the
power factor improvement is suggested for only plants A and E. The average cost of MMBtu
is calculated for each plant. The average cost of MMBtu is calculated by dividing the total
electricity charges of the utility for a year by the total kWh consumed during that year. It is a
very good indicator of how the utility utilizes its energy and what is the cost of electricity
usage in the plant.
101
FACILITIES A B C D E F G
GENERAL
INFORMATION
Location Preston
9100
75
1
Riverton
4680
50
2
Mt. Storm
4680
60
2
Webster
Springs
6000
91
2
Mt. Hope
27500
53
2
Bartow
20800
185
2
Spencer
15000
65
2
Annual Production (mbf)
Total # of employees
Shift Operation
UTILITY BILL ANALYSIS
Rate Schedule ALP 15 - D
5042
1054400
47563 0.60
29466
79245
ALP C - 11
5303
1787904
-
-
100364
100364
ALP C - 12
5096
1892352
-
-
104832
104832
-
9526
3962400
84793
0.44
110605
191437
AEP - LCP
14677
5918400
111648 0.49
112927
227335
ALP 15 - D
28081
11469248
234232 0.43
321253
541199
ALP 11- C
3139
1090538
-
-
90707
91085
Annual kW Demand
Annual kWh Usage
Demand Cost
Demand as a % of total cost
Usage Cost
Annual Electricity Charge
Load Factor 0.28
Yes
313
336
362
Yes
21.95
0.47
Yes
379
451
536
No
16.45
0.52
Yes
408
462
529 No
16.23
0.58
Yes
658
793
986
No
14.13
0.54 Yes
1151
1223
1277 Yes
11.25
0.56 Yes
2131
2340
2488 No
13.83
0.22
Yes
550
584
638
No
23.18
Load Curves
Min Demand
Avg. Demand
Max Demand
Power factor Improvement
Average MMBtu Cost
Table 8.1: Comparison matrix for the various plants
97
FACILITIES A B C D E F G
DEMAND SENSITIVITY ANALYSIS
Demand Sensitivity Analysis
Yes
1578
3165
317.14
No
Yes Yes
Yes
1370
2742
274
No
Yes Yes
Yes
1421
2839
285
No
Yes
No
Yes
9724
19450
2209
No
Yes Yes
Yes
5577
11154
1115
Yes Yes
Yes
Yes
26483
53006
5295
Yes Yes
Yes
No
-
-
-
Yes Yes
Yes
Annual electric cost saved for 5% decrease
in kW
Annual electric cost saved for 10% decrease
in kW
Annual electricity saved per unit of
kW decrease
Motor Load Test Performed
Motor Master Analysis
Cog belts replacement sensitivity analysis
SPECIFIC ENERGY CONSUMPTION
Demand/ mbf of production (kW/mbf) 0.6
116
3
9
1.1
382
21
21
1.1
404
22
22
1.6
660
18
32
0.5
215
4
8
1.4
551
15
26
0.2
73
6
6
Energy Usage/ mbf of production (kWh/mbf)
Usage cost/ mbf of production ($/mbf)
Total Electricity cost/ mbf of production ($/mbf)
Table 8.1: Comparison matrix for the various plants (contd.)

98

8.2.3 Demand sensitivity analysis parameters
A detailed demand sensitivity analysis is performed for each of the plants visited except
facility G where sufficient data on the plant demand is not available. Annual electricity saved
per unit of kW decrease in demand is calculated for the plants A to F. Motor load test is also
performed for the plants E, F and G. After the motor load test, the motor master analysis is
performed for all the plants using Motor Master + software. Also the cog belt replacement
analysis is performed for all the plants except the plant C.
8.2.4 Specific energy consumption parameters
Only absolute energy consumption values for each plant don’t give a good insight into the
energy usage by the plant. For comparing energy consumption parameters across all the
plants, ratios of energy with some common parameter of production are required. Thus the
specific energy consumption values are calculated so as to get a proper basis for comparing
the energy parameters across all the plants visited. Various parameters, which compare the
specific energy consumption of the plant, are compared across all the plants. The various
parameters are kW demand per mbf of production, energy usage kWh per mbf of production,
usage cost in $ per mbf of production and total electricity cost in $ per mbf of production.
Plots for each of these parameters across all the plants A to G are plotted and discussed in the
following section.
8.3 Plots for specific energy consumption
Various parameters, which compare the energy patterns across all the plants, are discussed in
the Table 8.1. Some of these parameters, which are good indicators of the energy usage, are
plotted across all the plants to get a better view of the energy usage in these plants. These
plots are for average MMBtu cost, energy usage per mbf of production, total electricity cost
per mbf of production and usage cost per mbf of production.
8.3.1 Plot of average MMBtu cost
The average MMBtu cost is plotted for each plant. As mentioned earlier the average cost of
MMBtu is the total electricity cost of the plant for the year divided by the total energy usage
of the plant in MMBtu for that year. This parameter is good indicator of the total energy
105

usage in the plant. The value of average MMBtu depends upon the number of operating hours
of the plant. More the operating hours, more the kWh or MMBtu consumed for the plant and
more the usage cost for that plant. The total cost comprises of demand and usage cost, so the
average MMBtu might be high if the demand cost and hence the total cost of the company is
very high for a period. As can be seen in the Figure 8.1, the average MMBtu cost is very high
for plant A and G. The value is around an average of 14 $/MMBtu for all other plants.
In case of A, it is the only one shift operation in all the plants. So the total cost of this
plant constitute the large demand cost and the usage cost of 1 shift per day. The total MMBtu
of energy consumed per year is low for this plant as compared to others. Also the total cost of
electricity is very high for this kind of operation because of power factor penalty cost and
also high demand cost. The plant G has a treatment plant and has a different product as
compared to the plants A to F. It treats the already square shaped logs in the plant for rail
tiers. The treatment plant of this facility is the major energy consumer with other plants not
consuming much energy. But there is big demand cost on this plant and the total energy bill
therefore is high. Also the amount of MMBtu of energy consumed per year by this plant is
very less as compared to other plants. So the average MMBtu cost of this plant is above $
20/MMBtu.
8.3.2 Plot of energy usage per mbf of production
This parameter is calculated by dividing the total annual energy consumed in kWh by the
annual production of lumber in mbf. As can be seen in the Figure 8.2, this parameter largely
varies across all the plants. For plant A, it is a one shift operation, but it produces high
volume of lumber per shift as compared to plants B and C which produce less but consume
more kWh as compared to A. This shows that the plant A is highly efficient operation, in
which produces more and consumes less energy as compared to plants B and C. Plant D is an
operation, which has a kiln for drying along with the conventional lumber manufacturing set
up. As a result it consumes a lot of kWh energy as compared to other plants. Also at the same
time, plant D production of lumber per year is very less as compared to the amount of energy
it consumers. The energy usage per mbf of production is very high.
Plant F also has 16 kilns and 14 dehumidifiers in addition to the conventional lumber
manufacturing process. As a result it consumes high amount of kWh per year. But at the same
106

time the overall plant appears to be efficient as its output production per year is also very
high. Therefore the value of energy usage is 551 kWh/mbf of production, which is still lower,
then the plant D whose value is 660 kWh/mbf. Plant G is as discussed earlier a totally
different process and its value cannot be compared with the other plants.
8.3.3 Plot of total electricity cost per mbf of production
This parameter is obtained by dividing the total electricity cost of the facility by the annual
mbf of lumber production at the plant. As can be seen in the Figure 8.3, this parameter varies
almost same as the usage cost per mbf of production for all the plants. The reasons for such
wide variation in the total electricity cost per mbf of production are same as the previous
section. As the denominator in both the cases is same, there is not much difference in these
plots.
8.3.4 Plot of usage cost per mbf of production
This parameter is obtained by dividing the usage cost of electricity in $ by the total annual
production of lumber in mbf for the facility. The usage cost of electricity is calculated
differently for different rate schedules of the utility service provider. In some schedules, the
rate structure is such that the utility cost include the demand cost and therefore the total cost
and the utility cost are same for these facilities, while for others the demand cost can be
separated from the usage cost. As can be seen in the Figure 8.4, this parameter varies across
all the plants. As can be seen for the plants B, C and G this value of usage cost per mbf of
production is equal to the total electricity cost per mbf of production due to their peculiar rate
structure. This plot depends on the energy usage plot in the Figure 8.2. If the energy usage
values of kWh in the Figure 8.2 are multiplied by the $/kWh cost or the usage cost for each
facility then the plot of usage cost per mbf of production will be as obtained in Figure 8.4. As
it can be seen the variation in the plots is same as that in the Figure 8.2. So the reasons for the
different values for this parameter across all the facilities are same as the reasons mentioned
in the section 8.3.2 earlier.
107

